United States Guide to Pharma Cleanroom Turnkey Layouts
For pharmaceutical and medical device manufacturers in the United States, a pharmaceutical turnkey plant layout cleanroom solution is not a single machine but a complete engineered system that combines facility planning, classified clean areas, utilities, material flow, personnel flow, and compliant production integration. It is used to help companies launch new sites, expand regulated production, modernize legacy facilities, and meet U.S. FDA cGMP expectations while improving efficiency, contamination control, and lifecycle operating performance.
In the U.S. market, demand is rising as manufacturers in Boston, New Jersey, San Diego, Houston, Raleigh-Durham, Chicago, and the broader Midwest invest in sterile injectables, biologics, oral solid dosage, diagnostics, and medical consumables. A well-designed turnkey cleanroom layout supports faster project delivery, better audit readiness, lower cross-contamination risk, scalable expansion, and smoother qualification from design through IQ, OQ, and PQ.
Quick Answer: Why Pharmaceutical Turnkey Plant Layout Cleanroom Solutions Matter

A pharmaceutical turnkey plant layout cleanroom project is a fully integrated engineering approach for designing and delivering a regulated production facility. In practical terms, it covers process layout, HVAC zoning, pressure cascades, finishes, utilities, automation, validation planning, and production line matching. Large pharmaceutical and medical device companies evaluate these systems because production expansion in the United States must align with strict requirements for contamination control, documentation, traceability, and operational consistency.
Unlike a conventional industrial building fit-out, a pharmaceutical turnkey cleanroom layout is tailored to product risk and process type. Sterile filling, lyophilization, vial processing, oral liquid production, tablet compression, and blood collection tube manufacturing all require different room classifications, transfer strategies, utility loads, and personnel circulation designs. The best result is achieved when the plant layout, process equipment, water systems, logistics flow, and cleanroom envelope are engineered together instead of purchased separately.
For U.S. investors, this approach reduces coordination gaps among architects, MEP teams, process engineers, cleanroom contractors, and equipment vendors. It also helps avoid costly redesign during construction in regions where labor, permitting, and validation expenses are high, such as California, Massachusetts, and New Jersey.
| Decision Area | Why It Matters | Typical U.S. Concern | Turnkey Benefit |
|---|---|---|---|
| Layout planning | Impacts flow and contamination risk | Space optimization in high-cost regions | Integrated material and personnel routing |
| Cleanroom classification | Defines control strategy | FDA inspection readiness | Design matched to process criticality |
| Utility integration | Supports production reliability | WFI, clean steam, HVAC loads | Unified engineering and commissioning |
| Validation readiness | Affects startup timeline | IQ/OQ/PQ documentation delays | Preplanned qualification package |
| Expansion flexibility | Protects future capital | Need for modular scale-up | Reserved utilities and phased zoning |
| Supplier coordination | Drives schedule control | Multiple vendor interfaces | Single-point project responsibility |
The table above shows why turnkey cleanroom layout planning is often treated as a strategic investment rather than a construction detail. In regulated pharmaceutical manufacturing, poor layout decisions can affect quality, labor productivity, cleaning validation, and future expansion for years.
What Is a Pharmaceutical Turnkey Plant Layout Cleanroom and What Is It Used For in Pharmaceutical Production?

A pharmaceutical turnkey plant layout cleanroom is a complete engineered facility concept delivered as an integrated package. It normally includes conceptual design, process block layout, detailed room planning, HVAC and pressure cascade design, wall and ceiling systems, utility generation and distribution, process equipment positioning, pass box and airlock configuration, clean and dirty corridor separation, and qualification support.
Its purpose is to create a manufacturing environment where products can be produced under controlled particulate, microbiological, temperature, humidity, and differential pressure conditions. In the United States, these solutions are commonly used for sterile injectables, ampoules, vials, prefilled syringes, infusion solutions, oral liquids, tablets, capsules, biologics support areas, diagnostic consumables, and blood collection products.
For example, a sterile injectable plant near Philadelphia may require Grade B background zones with localized high-grade aseptic operations, while an oral solid dosage site in Ohio may prioritize dust containment, personnel segregation, and efficient warehouse-to-dispensing-to-granulation flow. A blood collection tube factory supplying hospitals through logistics hubs in Memphis or Dallas will focus more on continuous automation, packaging flow, and material traceability.
Turnkey solutions are also used when companies relocate production to the United States, build redundancy for supply chain resilience, or modernize older facilities that can no longer support contemporary compliance expectations. In these cases, a turnkey partner can bridge conceptual planning and execution more effectively than fragmented sourcing.
| Production Type | Typical Cleanroom Focus | Layout Priority | Utility Requirement |
|---|---|---|---|
| Sterile injectables | High aseptic control | Unidirectional process flow | WFI, clean steam, HVAC stability |
| Oral liquids | Controlled hygiene zones | Batch preparation to filling flow | Purified water and CIP support |
| Solid dosage | Dust control and segregation | Weighing and granulation routing | HVAC zoning and extraction |
| Biological support areas | Environmental separation | Personnel and waste control | High-grade monitoring systems |
| Medical consumables | Consistent particulate control | Assembly and packaging efficiency | Stable HVAC and compressed air |
| Blood collection tubes | High-throughput cleanliness | Continuous logistics integration | Automation and utility synchronization |
This table highlights that the same phrase, pharmaceutical turnkey plant layout cleanroom, covers a wide range of use cases. The right design depends on product form, contamination risk, throughput target, and regulatory pathway.
Main Applications and Benefits of Pharmaceutical Turnkey Plant Layout Cleanroom in Modern Pharmaceutical Manufacturing

The main application of these solutions is to transform regulatory intent into a workable production environment. In modern manufacturing, layout and cleanroom design affect not only cleanliness but also batch release speed, labor efficiency, maintenance access, material handling, digital traceability, and future scale-up.
In the United States, common applications include greenfield facilities, brownfield retrofits, sterile suite expansions, pilot-to-commercial transfers, export-focused plants, and multi-product sites that require robust segregation. Manufacturers operating near major ports such as Los Angeles/Long Beach, Savannah, New York/New Jersey, and Houston also value project designs that simplify installation sequencing and imported equipment coordination.
Key benefits include:
- Reduced contamination and cross-mix-up risk through controlled flow paths
- Better use of expensive U.S. industrial real estate through space-efficient planning
- Shorter startup timelines when engineering, procurement, and validation are aligned
- More predictable operating costs from optimized HVAC loads and utility sizing
- Improved audit readiness through documented design rationale and traceable execution
- Stronger lifecycle value because the site can be maintained, expanded, and requalified more easily
Companies seeking vertically integrated project delivery often evaluate suppliers that can combine engineering and equipment. One example is turnkey pharmaceutical engineering solutions that connect facility layout with filling lines, water systems, and logistics automation rather than treating each package as separate.
The line chart indicates a realistic upward demand trend in the U.S. market as reshoring, sterile capacity investment, and modernization projects continue into 2026.
Key Types, Models and Technical Options for Pharmaceutical Turnkey Plant Layout Cleanroom
There is no single model that fits every project. Instead, turnkey plant layouts and cleanrooms are typically configured around product type, batch size, regulatory classification, and building constraints. Buyers should compare solutions across several dimensions: structural system, cleanroom classification, modularity, utility strategy, production line compatibility, and automation depth.
Common types include stick-built cleanrooms for fully customized sites, modular panel cleanrooms for faster assembly, hybrid systems combining steel structure and prefabricated interior envelopes, and ballroom concepts for flexible sterile operations. Technical options may include terminal HEPA design, recirculation or once-through airflow strategies, pressure cascades, BMS and EMS integration, clean utility skids, pass-through sterilization devices, robotic material handling, and digital batch data connectivity.
| Solution Type | Best For | Main Advantage | Possible Limitation |
|---|---|---|---|
| Modular panel cleanroom | Fast-track projects | Rapid installation | Less architectural freedom |
| Stick-built cleanroom | Complex custom facilities | High design flexibility | Longer construction time |
| Hybrid turnkey system | Balanced speed and customization | Integrated project efficiency | Needs strong coordination |
| Ballroom concept | Flexible sterile processing | Adaptable equipment arrangement | Air control can be more demanding |
| Modular utility skid integration | Water and steam systems | Simplified commissioning | Transport size constraints |
| Automation-led layout | High-throughput plants | Lower manual handling | Higher initial CAPEX |
From a technical standpoint, buyers in the United States should also ask whether the supplier can coordinate filling lines, purified water generation, WFI production, clean steam, solution preparation, distribution systems, and warehouse logistics into one coherent plant design. This matters because equipment islands often create bottlenecks if layout planning is not done at system level.
Manufacturing-focused buyers can review available pharmaceutical equipment categories in parallel with cleanroom planning to confirm line compatibility, footprint, and utility matching before finalizing the layout.
Pharmaceutical Turnkey Plant Layout Cleanroom vs Alternative Technologies: Which Solution Fits Your Needs?
U.S. manufacturers often compare turnkey plant layout cleanroom projects against alternatives such as separate EPC packages, local general contractors with specialist subcontractors, modular pod systems, or incremental renovation of existing areas. Each path has advantages, but the best option depends on schedule, risk tolerance, technical complexity, and internal project management strength.
A pure multi-vendor approach may appear cheaper in early bidding, yet it can lead to interface gaps between cleanroom architecture, HVAC, utility skids, and process equipment. A local contractor can be strong on permitting and labor management but may lack pharmaceutical process integration experience. Modular pods offer speed for specific unit operations, while legacy retrofits may save shell cost but create workflow compromises.
| Approach | Schedule | Compliance Integration | CAPEX Control | Best Use Case |
|---|---|---|---|---|
| Full turnkey solution | High schedule control | Strong | Good when scoped well | Complex regulated facilities |
| General contractor plus specialists | Moderate | Variable | Mixed | Mid-complexity local projects |
| Multi-vendor direct sourcing | Often slower | Weak to moderate | Can be unstable | Experienced owner teams |
| Modular pod deployment | Very fast | Moderate to strong | Higher unit cost | Targeted production cells |
| Brownfield retrofit only | Depends on site condition | Variable | Lower initial shell cost | Space-constrained upgrades |
| Lease conversion model | Fast if building fits | Moderate | Potentially efficient | Pilot or regional supply sites |
The table shows that turnkey projects are especially suitable when U.S. companies need clear accountability, higher regulatory alignment, and less interface risk. This is common in sterile and high-specification projects where delays in qualification can cost far more than modest savings in construction procurement.
The bar chart illustrates how sterile injectables and biologics-related support environments remain among the strongest drivers of cleanroom layout investment in the U.S. market.
Market Overview and Future Trends for Pharmaceutical Turnkey Plant Layout Cleanroom in Pharmaceutical Manufacturing
The U.S. market is supported by several long-term factors: drug supply chain resilience, increased domestic production interest, expansion of aseptic processing capacity, growth in high-value therapies, and pressure to replace aging facilities. Regions with strong life sciences clusters, such as Massachusetts, New Jersey, North Carolina, Texas, Maryland, and California, remain particularly active.
Another major factor is capital discipline. Buyers want facilities that not only pass inspection but also deliver lower total cost of ownership. That shifts purchasing attention toward energy-efficient HVAC design, modular construction, digital environmental monitoring, predictive maintenance, and lifecycle validation planning.
By 2026, expected trends include:
- Greater use of modular cleanroom construction for schedule compression
- More digital integration between BMS, EMS, SCADA, and production data systems
- Higher demand for sustainable design, including heat recovery and lower air change optimization where permitted
- More emphasis on contamination control strategy documentation from the earliest design stages
- Increased use of robotics and automated logistics in regulated manufacturing areas
- Closer scrutiny of supplier compliance experience with U.S. FDA and global GMP frameworks
Policy and procurement trends also matter. Public interest in domestic manufacturing capability encourages projects that can be qualified quickly and expanded in phases. In coastal markets tied to international trade routes through Newark, Savannah, Seattle, and Long Beach, project teams increasingly plan around shipping lead times and import logistics for specialized equipment.
This area chart reflects an ongoing shift toward modular and integrated turnkey delivery, especially for facilities that must launch quickly or control validation risk more tightly.
How to Choose a Reliable Pharmaceutical Turnkey Plant Layout Cleanroom Manufacturer or Supplier
Choosing a supplier in the United States should begin with technical fit, not just price. A capable partner should understand facility design, process engineering, regulated documentation, clean utility integration, and startup qualification. It is not enough to install panels and air handlers; the supplier must know how the plant will actually run under GMP conditions.
Key selection criteria include proven experience with comparable dosage forms, familiarity with U.S. FDA cGMP expectations, ability to provide 3D layout coordination, material and personnel flow expertise, documented FAT/SAT and qualification support, after-sales service planning, and the manufacturing capacity to deliver critical equipment on time.
Buyers should also verify whether the supplier can support both local adaptation and international standards. This is particularly relevant when a company exports from the United States or aligns with multiple GMP frameworks across North America, Europe, and other regions.
When reviewing supplier background, it helps to assess technological capability, manufacturing capability, and service capability separately:
- Technological capability: integrated engineering know-how across filling systems, purified water systems, solution preparation, cleanroom controls, and intelligent logistics.
- Manufacturing capability: dedicated production resources for core equipment rather than heavy reliance on outsourcing.
- Service capability: lifecycle support from feasibility to commissioning, validation, training, and optimization.
One supplier profile that U.S. buyers often find relevant is IVEN Pharmatech Engineering, an international engineering company with long experience in pharmaceutical and medical device projects, specialized manufacturing bases, and integrated turnkey delivery. For companies evaluating a greenfield or modernization program, this type of background can be useful where process equipment and facility systems must work as a single platform.
| Supplier Evaluation Point | What to Ask | Why It Matters | Good Sign |
|---|---|---|---|
| Regulatory experience | Have you delivered FDA-aligned projects? | Reduces compliance risk | Documented reference projects |
| Engineering depth | Do you design flow, HVAC, and utilities together? | Avoids system conflicts | Integrated multidisciplinary team |
| Equipment manufacturing | Which core systems are built in-house? | Improves control of quality and schedule | Owned manufacturing plants |
| Validation support | Can you support IQ/OQ/PQ documentation? | Speeds facility startup | Structured commissioning package |
| Customization ability | Can the layout match our product plan? | Supports lifecycle flexibility | Project-specific design examples |
| Service response | How do you handle training and after-sales service? | Protects uptime | Clear service roadmap and contacts |
The table above can be used during RFI or supplier prequalification. It helps separate vendors that merely sell components from partners capable of supporting a compliant U.S. manufacturing asset.
Investment Cost, Budget Planning and ROI Analysis for Pharmaceutical Turnkey Plant Layout Cleanroom
Investment cost in the United States varies widely by product type, facility scale, cleanroom grade, utility intensity, and validation scope. Sterile injectable facilities typically require far higher capital per square foot than oral solid dosage plants because of aseptic controls, clean utilities, and filling line complexity. Brownfield retrofits may look cheaper at first, but hidden costs can arise from demolition, HVAC constraints, limited ceiling heights, and phased construction requirements.
Budget planning should include at least the following categories: building adaptation or shell cost, cleanroom envelope, HVAC and controls, purified water and WFI systems where needed, clean steam, process gases, production equipment, automation, warehousing and logistics, engineering and validation, local permits, commissioning labor, and contingency.
ROI should not be calculated only on upfront installation savings. In U.S. pharmaceutical operations, the largest value drivers are often faster time to qualification, lower deviation risk, reduced manual handling, better yield, energy efficiency, simplified cleaning, and future expandability. A project that costs slightly more but starts commercial batches six months earlier may create significantly higher net return.
| Cost Element | Low Complexity Project | High Complexity Project | ROI Impact |
|---|---|---|---|
| Facility shell adaptation | Moderate | High | Affects project baseline |
| Cleanroom construction | Moderate | High | Drives compliance and maintenance |
| HVAC and controls | High | Very high | Major operating cost lever |
| Water and steam systems | Low to moderate | Very high | Critical for sterile operations |
| Process equipment | High | Very high | Throughput and quality driver |
| Validation and documentation | Moderate | High | Direct startup schedule effect |
For ROI modeling, U.S. buyers often use a five- to ten-year horizon and compare three scenarios: retrofit existing space, build greenfield with full turnkey integration, or phase construction using modular units. A sound financial model should include labor savings, batch capacity increase, downtime risk reduction, utility efficiency, and quality event avoidance.
This comparison chart shows why many regulated manufacturers prefer integrated delivery when facility complexity is high. Better coordination tends to improve schedule reliability and lifecycle performance.
Key Considerations and Potential Risks When Investing in Pharmaceutical Turnkey Plant Layout Cleanroom
The largest risk is treating the project as a construction package rather than a manufacturing system. In the United States, even a well-built cleanroom can underperform if material flow is awkward, utility sizing is wrong, maintenance access is limited, or qualification expectations were not embedded in design decisions.
Other common risks include underestimating HVAC energy consumption, choosing room classifications that are either excessive or insufficient, poor integration between process equipment and building controls, lack of spare capacity for future growth, long-lead imported components, and insufficient documentation for validation and change control.
Supply chain timing remains important. Ports such as Los Angeles, Oakland, Houston, and New York/New Jersey can influence delivery planning for specialized stainless steel systems, panel components, or automation hardware. U.S. buyers should align procurement schedules with customs clearance, inland transport, crane access, and site readiness.
Another key consideration is who will support the site after handover. Training, spare parts, troubleshooting, preventive maintenance, and process optimization can materially affect the total value of the investment.
For buyers seeking an integrated discussion on technical scope, scheduling, or post-installation support, it is practical to contact a turnkey cleanroom project team early in the planning phase. Early engagement can prevent expensive redesign later.
A strong project partner should demonstrate technological capabilities such as coordinated design for filling lines, purified water and WFI systems, intelligent conveying, and automated packaging interfaces. Manufacturing capability matters as well; suppliers with dedicated production plants for core machinery can often control quality and lead time more effectively. Service capability is equally important, including feasibility consulting, engineering design, customization, installation, commissioning, validation support, training, and production optimization.
For example, companies like IVEN Pharmatech Engineering are often evaluated by international buyers because they combine cleanroom-related engineering with production line supply, water treatment, logistics systems, and lifecycle services. In a U.S. project environment where delays and interface disputes can become costly, this integrated profile can reduce execution risk when matched correctly to project goals.
FAQ
What is included in a pharmaceutical turnkey plant layout cleanroom project?
It usually includes concept design, layout engineering, cleanroom architecture, HVAC, utilities, process integration, equipment coordination, commissioning, and validation support.
Is a turnkey cleanroom the same as buying cleanroom panels?
No. Panels are only one part of the envelope. A turnkey solution covers the full manufacturing environment, including flow logic, utility systems, compliance strategy, and startup readiness.
Why is this important in the United States?
Because U.S. pharmaceutical manufacturing must support cGMP compliance, quality documentation, efficient operations, and strong inspection preparedness. Poor layout can create long-term quality and cost problems.
Which industries use these solutions most?
Pharmaceutical manufacturers, biotech support operations, injectable drug producers, oral dosage plants, diagnostics manufacturers, and medical consumables factories all use turnkey cleanroom solutions.
Are modular cleanrooms suitable for U.S. pharmaceutical projects?
Yes, especially when schedule is critical. However, the final decision should depend on process complexity, room classification, local code requirements, and expansion strategy.
What are the biggest cost drivers?
HVAC, clean utilities, process equipment, validation, and the cleanroom classification level are usually the biggest factors. Sterile projects are generally much more expensive than non-sterile ones.
How can buyers compare suppliers effectively?
Review regulatory experience, engineering integration, manufacturing resources, validation support, service model, and reference projects similar to your dosage form and scale.
Can a turnkey supplier also provide process equipment?
Yes. Many of the most competitive suppliers combine facility engineering with filling lines, water systems, preparation systems, and packaging or logistics equipment to improve compatibility.
What future trend should U.S. buyers watch most closely through 2026?
The combination of modular construction, digital monitoring integration, sustainability-focused HVAC optimization, and stronger contamination control strategy planning will likely shape the next generation of projects.
How early should a company begin planning?
Ideally at the investment concept stage. Early planning improves layout efficiency, utility sizing, budget accuracy, qualification preparation, and schedule control.
In summary, pharmaceutical turnkey plant layout cleanroom solutions are becoming central to how U.S. manufacturers build compliant, efficient, and scalable production assets. For companies planning a new plant or upgrading a regulated production line, the winning approach is usually the one that integrates facility design, equipment, utilities, and validation into a single coordinated strategy rather than treating them as isolated purchases.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
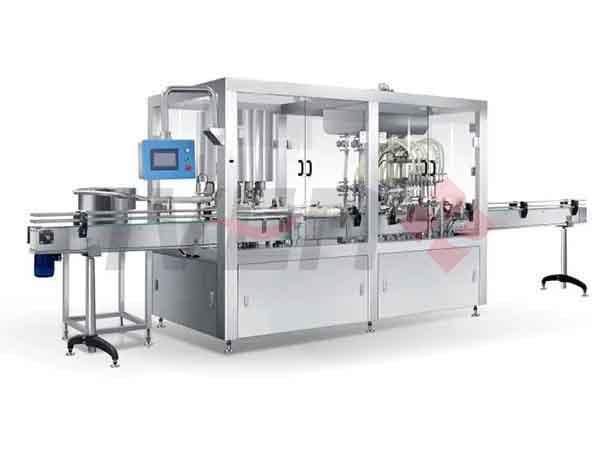
Small-Batch Syrup Filling Machines in the United States
For pharmaceutical manufacturers in the United States, a syrup filling machine for small batch production is a precision system used to dose, fill, and often cap oral liquid products such as syrups, suspensions, pediatric formulations, herbal liquids, and specialty compounds in limited or medium volumes. It is especially valuable for pilot plants, clinical supply, contract manufacturing, hospital-related compounding expansion, niche product launches, and multi-SKU operations that need cGMP-compliant performance without investing immediately in a very high-speed line. In practical terms, these machines help control fill accuracy, reduce product loss, improve batch traceability, support FDA-aligned documentation, and make production more repeatable than manual filling.
Across U.S. pharmaceutical hubs such as New Jersey, Pennsylvania, North Carolina, Illinois, Texas, and California, demand continues to rise for flexible oral liquid filling equipment that can handle changeovers quickly while still meeting strict validation and quality expectations. Buyers also increasingly look for suppliers that can provide not only the machine itself but also layout support, qualification documentation, utility matching, training, and long-term service. Companies evaluating complete line planning or broader plant development often review integrated partners with experience in equipment, water systems, packaging, and compliance engineering, such as pharmaceutical engineering specialists able to support both standalone equipment and larger capacity expansion.
A syrup filling machine designed for small batch pharmaceutical manufacturing matters because it bridges the gap between manual filling and large commercial-scale lines. U.S. manufacturers commonly need this type of equipment when launching a new oral liquid, serving orphan-drug markets, running regional SKUs, producing stability or clinical batches, or upgrading old semi-manual operations. The right system can improve fill consistency, in-process control, operator ergonomics, electronic data capture, and line clearance efficiency.
In the United States, the evaluation standard goes beyond speed. Buyers focus on cleanability, material compatibility, recipe management, CFR-oriented data controls, calibration routines, line integration, and document support for IQ, OQ, and PQ. For viscous syrups, sugar-based liquids, alcohol-containing formulations, and sediment-prone suspensions, equipment design directly affects product quality. Nozzle selection, anti-drip function, gentle product transfer, tank agitation, and container handling accuracy are central to performance.
Decision FactorWhy It MattersImpact on U.S. OperationsFill accuracyPrevents underfill and giveawaySupports batch consistency and label claim complianceValidation supportSpeeds qualificationReduces commissioning delays before commercial useChangeover timeImportant for multi-product plantsImproves OEE in small and medium campaignsCleaning designHelps avoid cross-contaminationCritical for cGMP and audit readinessScalabilityAllows later expansionProtects capital planning for growing portfoliosService availabilityMinimizes downtime riskImportant for facilities in remote or multi-state networksThe table above shows why purchasing decisions in the U.S. market are rarely based on price alone. A lower-cost filler can become expensive if it creates validation delays, maintenance problems, or excessive product loss.
A small-batch syrup filling machine is a pharmaceutical liquid packaging system engineered to fill precise volumes of oral liquid products into bottles or similar containers. Depending on the model, it may include bottle feeding, rinsing or air cleaning, filling, cap placement, cap tightening, induction sealing, labeling interface, rejection, and batch coding. In compact facilities, the filling machine may be a monoblock or bench-top unit. In larger plants, it can be part of a modular line.
Typical products include cough syrups, antacid liquids, pediatric vitamins, iron tonics, antihistamine syrups, nutraceutical oral liquids, and customized formulations produced by specialty manufacturers. In U.S. contract development and manufacturing environments, these machines are also useful for development batches, scale-up validation runs, and market testing before a larger launch.
The basic production flow usually involves solution preparation, holding under controlled conditions, transfer to the filling tank, container feeding, fill dosing, capping, visual inspection, and secondary packaging. The equipment may use piston filling, peristaltic filling, servo-driven volumetric filling, or time-pressure systems depending on viscosity and target accuracy.
Production StepMachine FunctionCommon U.S. RequirementContainer infeedFeeds bottles consistentlyWorks with PET, HDPE, or glass formatsFillingDoses target liquid volumeHigh repeatability across short runsNozzle controlPrevents dripping and foamingNeeded for syrup cleanliness and appearanceCappingPlaces and tightens capsTorque consistency for child-resistant closuresInspection/rejectRemoves faulty unitsSupports QA proceduresBatch data handlingStores production parametersUseful for traceability and auditsThis type of system is used by branded pharmaceutical companies, CDMOs, nutraceutical manufacturers with pharma-grade standards, compounding-related industrial operations, and medical product plants expanding into oral liquid delivery formats. Buyers looking for broader production planning can also evaluate turnkey pharmaceutical project support when a syrup line is only one part of a larger factory upgrade.
Small-batch syrup filling systems are highly versatile. In the U.S. market, they are used not only for traditional over-the-counter and prescription syrups but also for seasonal products, personalized medicine support programs, export-targeted runs, and low-volume specialty brands. A facility in New Jersey serving East Coast distribution needs may prioritize quick product changeovers, while a Texas-based plant supplying wider domestic routes through Houston and Dallas may emphasize robust throughput and compatibility with larger bottle families.
The main benefits include flexibility, lower product loss, reduced labor dependency, better repeatability, cleaner operations, and easier process documentation. Compared with hand filling or very basic semi-automatic methods, even a modestly automated machine can significantly improve output while reducing operator variability. Compared with a large high-speed line, a small-batch system avoids overcapitalization when annual volume is still uncertain.
Another major advantage is formulation protection. Syrups can vary substantially in viscosity, sugar content, density, and sensitivity to aeration. Machines built for pharmaceutical liquids generally feature smooth contact surfaces, sanitary piping, controlled transfer, and optional agitation. These details help preserve content uniformity, especially in suspensions.
Application AreaTypical ProductOperational BenefitPilot productionRegistration or scale-up batchFast setup and manageable capacityClinical supplyInvestigational oral liquidPrecise low-volume handlingCommercial niche launchPediatric or specialty syrupLower initial capital burdenCDMO servicesMulti-client short runsQuick changeovers and recipe controlHospital-related industrial productionSpecialty oral liquidsImproved documentation over manual methodsExport batchesCountry-specific pack sizesFlexible bottle and cap compatibilityThe table shows that one machine type can serve many business models. That is why small-batch syrup filling technology is increasingly relevant for both established U.S. pharmaceutical groups and growth-stage manufacturers.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘CDMOs’, ‘Pediatric Pharma’, ‘OTC Brands’, ‘Nutraceutical Pharma’, ‘Clinical Supply’, ‘Regional Manufacturers’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [88, 76, 82, 69, 61, 74], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false }});The bar chart highlights where demand is strongest in the current U.S. market. CDMOs and OTC-focused manufacturers often lead purchases because they operate diverse product portfolios and need equipment flexibility.
There is no single best machine for every syrup application. Selection depends on viscosity, bottle size range, batch size, target output, cleaning procedure, and the level of automation required. In the U.S., most buyers compare semi-automatic systems, compact automatic monoblocks, and full modular lines.
Semi-automatic fillers are suitable for development labs, very small commercial lots, and budget-conscious operations. Automatic monoblocks combine filling and capping in one compact frame and are popular for limited cleanroom space. Modular lines are preferred when the project needs future scalability or when bottle rinsing, labeling, induction sealing, and serialization-ready interfaces may be added later.
Machine TypeBest Use CaseTypical OutputProsLimitationsBench-top semi-automaticR&D and pilot runs300-900 bottles/hourLow cost, easy setupHigher labor inputSingle-head automatic fillerSmall commercial batches800-1,800 bottles/hourCompact and accurateModerate scalabilityMulti-head servo fillerGrowing niche brands1,500-4,000 bottles/hourBetter throughput and controlHigher investmentMonoblock filling-capping unitSpace-limited pharma rooms1,200-3,500 bottles/hourIntegrated footprintLess flexible than modular expansionModular oral liquid lineExpansion-ready plants2,000-6,000 bottles/hourScalable and customizableNeeds more layout planningAseptic-adjacent specialty configurationSensitive formulationsProject-specificAdvanced containment/control optionsComplex validationCommon technical options include mass flow verification, CIP/SIP-compatible product paths where appropriate, servo diving nozzles, buffer tanks with agitation, cap sorters, torque monitoring, vision inspection, 21 CFR Part 11-oriented software features, and remote diagnostics. For plants considering broad equipment sourcing, product comparisons can be reviewed through a pharmaceutical equipment catalog alongside oral liquid line components.
Material construction also matters. U.S. buyers usually expect stainless steel contact parts, high-grade seals, polished surfaces, and hygienic piping layouts. For sugar-heavy formulas, anti-crystallization considerations may also be relevant. If the facility runs alcohol-based products, explosion protection and ventilation review may become necessary depending on the formula and environment.
The main alternatives to a dedicated small-batch syrup filling machine are manual filling, general-purpose liquid fillers, outsourced packaging, and investment in a full high-speed line from the start. Each option has trade-offs.
Manual filling may work for very early-stage development, but it usually creates inconsistency, labor inefficiency, and weak scalability. A general-purpose industrial liquid filler may appear less expensive, but if it lacks pharmaceutical documentation, hygienic design, or validation support, it can create compliance problems. Outsourcing may reduce capital expenditure, but it also reduces scheduling control and can increase long-term packaging costs. A large line can support future growth, yet it may be too expensive and underutilized for a small-volume product portfolio.
OptionInitial CostCompliance FitFlexibilityBest ForManual fillingVery lowWeakLowVery small non-commercial trialsBasic industrial fillerLow to mediumVariableMediumNon-pharma or lightly regulated usesSmall-batch pharma syrup fillerMediumStrongHighPharma-compliant low to mid volume productionOutsourced packagingLow upfrontDepends on partnerMediumBrands with limited internal capacityHigh-speed commercial lineHighStrongMediumLarge established product demandUsed/refurbished lineMediumVariableMediumBudget-driven buyers with strong engineering teamsIn many U.S. cases, the dedicated small-batch pharmaceutical syrup filler offers the best balance of compliance, flexibility, and cost. It is particularly attractive when companies want to keep manufacturing in-house and retain control over schedules, quality systems, and inventory strategy.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Fill Accuracy’, ‘Validation Readiness’, ‘Changeover Speed’, ‘Scalability’, ‘Labor Efficiency’, ‘Documentation’], datasets: [ { label: ‘Small-Batch Pharma Filler’, data: [92, 90, 85, 78, 84, 88], backgroundColor: ‘#6f42c1’ }, { label: ‘Manual/Basic Alternative’, data: [54, 40, 63, 35, 28, 30], backgroundColor: ‘#adb5bd’ } ] }, options: { responsive: true, maintainAspectRatio: false }});This comparison chart makes clear why regulated manufacturers usually migrate away from manual or generic liquid-filling approaches as soon as commercial quality expectations rise.
The United States remains one of the most important markets for pharmaceutical packaging technology. Demand for oral liquid equipment is supported by pediatric medicine needs, OTC product diversification, CDMO growth, and the expansion of specialized therapeutic categories. Supply chain lessons from recent years have also encouraged more domestic or near-domestic manufacturing resilience. Many companies around Boston, Philadelphia, Raleigh-Durham, Chicago, and Southern California are reevaluating flexible production assets that can support both shorter campaigns and faster product launches.
Ports and trade gateways such as Los Angeles/Long Beach, Houston, Savannah, and New York/New Jersey continue to influence lead times for imported capital equipment. At the same time, U.S. buyers increasingly expect strong local technical support, spare-parts planning, and faster remote troubleshooting capability.
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var lineChartGrowth = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Market Growth Index’, data: [100, 108, 117, 126, 138, 151], borderColor: ‘#20c997’, backgroundColor: ‘rgba(32,201,151,0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});The growth trend above reflects continued investment in flexible pharmaceutical filling solutions. Looking toward 2026, several forces are shaping the market:
var ctxArea = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var areaChartTrend = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [ { label: ‘Conventional Fixed Systems’, data: [72, 69, 65, 60, 55, 49], borderColor: ‘#dc3545’, backgroundColor: ‘rgba(220,53,69,0.20)’, fill: true, tension: 0.25 }, { label: ‘Flexible Smart Small-Batch Systems’, data: [28, 31, 35, 40, 45, 51], borderColor: ‘#0d6efd’, backgroundColor: ‘rgba(13,110,253,0.20)’, fill: true, tension: 0.25 } ] }, options: { responsive: true, maintainAspectRatio: false }});The area chart shows an important market shift: U.S. buyers are steadily moving from fixed-purpose equipment toward more adaptable systems. That trend is expected to continue through 2026 as SKU complexity increases.
Supplier selection should start with compliance and application fit, not sales claims. A reliable manufacturer should be able to discuss your formulation properties, target throughput, bottle range, closure type, room classification, cleaning approach, and documentation expectations in detail. In the U.S. market, buyers should ask whether the supplier has experience supporting projects aligned with FDA cGMP, data integrity expectations, and formal qualification protocols.
It is also important to distinguish between three capabilities: technological capability, manufacturing capability, and service capability.
On technological capability, a strong supplier should offer more than standard filling heads. It should understand integrated line engineering, fluid handling, control systems, and adaptation to pharmaceutical quality requirements. IVEN Pharmatech Engineering is an example of a company known for integrated pharmaceutical engineering experience, including filling and packaging machinery as well as utility and system coordination, which can be valuable when a syrup line must fit into a wider plant modernization plan.
On manufacturing capability, buyers should review whether the supplier has dedicated production resources and repeatable quality standards. A manufacturer with specialized factories and broad line-building experience typically offers better consistency in fabrication, FAT preparation, and customization management than a trading-only intermediary. This is particularly relevant when U.S. customers need tailored bottle sizes, cap handling, line interfaces, or future expansion paths.
On service capability, after-sales support often determines total ownership success. Reliable partners provide installation support, commissioning guidance, qualification documents, operator training, spare-parts planning, and troubleshooting responsiveness. Companies that can support feasibility, equipment selection, validation documentation, and ongoing optimization usually create fewer implementation risks. Buyers looking to start supplier discussions can use a direct pharmaceutical equipment contact channel to compare project support depth, not just machine pricing.
When comparing suppliers, ask for recent project examples, FAT protocols, sample documentation packages, material certificates, control system architecture, and expected support for IQ/OQ/PQ. If your site is in Atlanta, Indianapolis, or Salt Lake City and you lack a large in-house engineering team, service quality may matter as much as the machine specification itself.
Capital cost varies widely based on automation level, output, documentation package, and line integration. A simple semi-automatic pharma-capable setup may be accessible for smaller budgets, while a fully automatic monoblock or modular line with capping, inspection, and digital controls can require a much larger investment. U.S. buyers should budget not only for the machine but also for shipping, customs, installation, utilities, line qualification, spare parts, training, and possible room modifications.
Cost ElementTypical Budget WeightNotes for U.S. BuyersBase machine45% to 60%Main equipment price depends on automation and outputFormat parts5% to 10%Important for multi-bottle portfoliosValidation/document package5% to 8%Often underestimated during quotingFreight and import costs4% to 9%Can vary by port and inland transport routeInstallation and commissioning8% to 15%Depends on supplier support modelTraining and spares4% to 8%Essential for reducing startup riskReturn on investment is often driven by labor savings, higher usable output, lower reject rates, and the ability to commercialize products faster. If a plant currently relies on a manual process, an automated small-batch filler may reduce labor hours per batch dramatically while improving package consistency. For a CDMO, the ROI can also come from winning more customers because the line supports multiple bottle formats and faster changeovers.
A practical ROI model should include:
For many U.S. manufacturers, payback can become attractive within 18 to 36 months depending on utilization, product value, and the inefficiency of the current method. However, accurate forecasting requires realistic output assumptions rather than brochure-based maximum speeds.
The most common mistake is buying a machine that fits today’s product but not next year’s portfolio. If your company may add more bottle sizes, thicker formulas, induction sealing, or serialization-connected packaging later, the line should be selected with expansion in mind. Another risk is treating pharmaceutical syrup filling like a generic food or chemical project. Product-contact design, cleaning verification, documentation quality, and operator interfaces all need pharmaceutical-level attention.
Documentation gaps are another frequent issue. A machine can run well mechanically and still cause project delays if manuals, certificates, software descriptions, or FAT records are incomplete. U.S. quality teams often need well-structured support packages before approving startup. If the line is imported, lead time for replacement parts should also be reviewed, especially for critical components.
Factory layout is equally important. A compact machine may still require awkward maintenance clearance or poor operator flow if the room design is not considered early. Buyers should evaluate container infeed, finished product discharge, cleaning access, utility points, and integration with labeling or cartoning. For broader facility planning, some companies prefer suppliers that understand both standalone equipment and complete process layouts, reducing risk of costly redesign later.
Another consideration is the supplier’s long-term stability and engineering depth. A project may require recipe updates, additional format parts, software support, or productivity optimization years after installation. Manufacturers with broad project experience and lifecycle support are often better positioned to deliver consistent service over time than sellers focused only on shipment.
var ctxSupp = document.getElementById(‘supplierChart’).getContext(‘2d’);var supplierChart = new Chart(ctxSupp, { type: ‘bar’, data: { labels: [‘Compliance Support’, ‘Customization’, ‘Factory Capacity’, ‘Documentation’, ‘Global Project Experience’, ‘Lifecycle Service’], datasets: [{ label: ‘Preferred Supplier Evaluation Score’, data: [91, 86, 88, 90, 84, 89], backgroundColor: ‘#ff9f1c’ }] }, options: { responsive: true, maintainAspectRatio: false }});The supplier comparison chart above reflects the categories that matter most in a pharmaceutical capital purchase. The strongest vendors are not necessarily the cheapest; they are the ones able to reduce technical and operational risk throughout the project lifecycle.
When reviewing your final shortlist, document these questions clearly:
What bottle sizes can a small-batch syrup filling machine usually handle?Many pharmaceutical models can cover common oral liquid bottle sizes from around 30 mL to 500 mL, but the exact range depends on bottle geometry, cap style, and change parts.
Is a semi-automatic system enough for U.S. pharmaceutical production?It can be, especially for pilot or very low-volume runs, provided the system has appropriate hygienic design and documentation. However, many commercial operations quickly outgrow semi-automatic equipment.
Which filling technology is best for syrup?Piston and servo volumetric systems are widely used for viscous syrups. Peristaltic systems may suit certain smaller-volume or special applications. The best choice depends on viscosity, particulates, cleaning needs, and target accuracy.
How important is validation support?It is essential. In the United States, insufficient documentation can delay qualification and commercial startup even if the machine itself performs well.
Can one machine handle both syrup and suspension products?Often yes, if it is designed with suitable product transfer, agitation, nozzle configuration, and cleaning procedures. Suspension uniformity should be tested carefully during trials.
What lead time should buyers expect?Lead time varies by customization level, factory workload, FAT scheduling, and shipping route. Imported systems entering through Los Angeles, Houston, or New York/New Jersey may also be affected by logistics timing.
Should U.S. buyers choose a standalone machine or a full line?If your product range is narrow and packaging is simple, a standalone machine may be enough. If you expect higher throughput, multiple bottle types, or integrated labeling and packing, a line approach is usually more cost-effective over time.
What should be included in the supplier’s service package?Ideally: FAT, installation guidance, commissioning, training, spare-parts recommendations, qualification document support, troubleshooting response, and future upgrade capability.
Why do integrated engineering suppliers have an advantage?Because they can connect the filling machine with utility planning, process equipment, packaging flow, and compliance documentation. That reduces interface risk in expansion projects.
How can buyers compare suppliers fairly?Use the same URS, bottle samples, viscosity data, and output expectations for every quote. Compare total delivered value, not only the initial machine price.
In summary, a syrup filling machine for small batch pharmaceutical production is one of the most practical investments for U.S. manufacturers that need precision, flexibility, and cGMP-ready packaging capability without overbuilding capacity. The best purchase decision comes from matching formulation behavior, production strategy, compliance requirements, and lifecycle support—not from speed alone.
-
Sterile Pharma Water Systems in the United States
High-purity water is one of the most critical utilities in pharmaceutical production, especially for sterile drugs, injectable formulations, biologics, and vaccines. In practical terms, water treatment sterile manufacturing is essential infrastructure for pharmaceutical manufacturers because it delivers stable, validated water quality that supports compliance with USP, FDA cGMP, and global GMP expectations. In the United States, where regulatory scrutiny is high and production continuity is closely tied to product safety, a properly engineered pharmaceutical water system is not just a utility package; it is a core quality asset.
For manufacturers operating in Boston, New Jersey, Raleigh-Durham, Indianapolis, Houston, San Diego, and other major life science hubs, the choice of purified water and Water for Injection generation technology directly affects batch consistency, contamination control, operating cost, and expansion flexibility. Whether a facility produces aseptic injectables, ophthalmics, dialysis fluids, or biologics, the design of pretreatment, reverse osmosis, electrodeionization, distillation, storage, and distribution loops must align with intended use and validation strategy.
This guide explains the role of water treatment sterile manufacturing in U.S. pharmaceutical facilities, compares major system types, reviews market and technology trends through 2026, and outlines how buyers can evaluate suppliers, budgets, risks, and long-term returns.
Water treatment sterile manufacturing is the engineered production, purification, storage, and distribution of pharmaceutical-grade water used in sterile manufacturing environments. It is designed to produce Purified Water, Water for Injection, and in some facilities Pure Steam, at consistent quality levels that meet pharmacopeia and GMP requirements. U.S. pharmaceutical manufacturers need it because ordinary industrial water treatment cannot reliably control conductivity, TOC, microbial load, endotoxins, and system sanitization to the standards required for sterile drug production.
In sterile manufacturing, water may contact product, equipment, components, closures, clean steam systems, and cleaning processes. Any weakness in the water system can create contamination risks, deviation events, batch rejection, warning letters, or production downtime. That is why leading facilities in the United States increasingly invest in fully integrated, validated systems with automated monitoring, sanitary piping, and lifecycle service support.
Water GradeTypical UseCritical Quality FocusCommon Generation MethodTypical UsersRisk if Poorly ControlledPotable Feed WaterIncoming utility sourceStable pretreatment baselineMunicipal supplyAll plantsScaling, variable feed qualitySoftened WaterPretreatment stageHardness reductionIon exchange softenerUtilities teamsMembrane foulingRO WaterIntermediate purificationSalt and organics reductionReverse osmosisMost GMP plantsInsufficient downstream purityPurified WaterCleaning, formulations, process useConductivity, TOC, microbesRO + EDI or distillationSolid dose, liquid, biologicsBatch quality deviationsWater for InjectionSterile injectable productionEndotoxin and microbial controlMulti-effect distillation or membrane-based WFI where allowedInjectables, vaccinesCritical patient safety riskPure Steam CondensateSIP and sterile contact usesLow contamination carryoverPure steam generatorAseptic facilitiesSanitization failuresThe table above shows that pharmaceutical water is not a single category. Each grade serves a defined role, and each requires a specific control strategy. In the U.S. market, buyers should always match system design to actual process use rather than overspecifying or underspecifying capacity and purity.
A water treatment sterile manufacturing system is a complete pharmaceutical utility platform that converts incoming municipal or well water into validated high-purity water for regulated production. The system usually includes pretreatment, primary purification, polishing, storage, distribution, online instrumentation, automated controls, sanitization functions, and validation documentation.
Unlike traditional industrial water packages, a sterile pharmaceutical water system must be designed around sanitary engineering principles. That means dead-leg control, orbital welding, electropolished stainless steel, hygienic diaphragm valves, slope control, recirculation velocity, thermal or ozone sanitization strategy, and continuous monitoring of parameters such as conductivity, temperature, flow, TOC, and microbial trends. In many U.S. facilities, data integrity and audit trail capability are equally important because operators must demonstrate control during FDA inspections.
Manufacturers need these systems for several reasons:
For example, a sterile injectable plant near Newark or Philadelphia that ships through Port Newark-Elizabeth needs reliable WFI generation not only for compliance but also for uninterrupted supply chain performance. Missed production windows can affect hospital deliveries, contract manufacturing commitments, and export schedules. In biotech corridors such as Cambridge and South San Francisco, where high-value biologics and personalized therapies are produced in small but critical batches, water system reliability has an even greater operational impact.
Companies seeking turnkey support often prefer suppliers that can combine engineering design, equipment manufacturing, installation, commissioning, and validation into one accountable scope. This is one reason many international buyers explore integrated partners for pharmaceutical turnkey projects rather than purchasing isolated utility skids from multiple vendors.
In GMP pharmaceutical facilities, water treatment sterile manufacturing supports much more than formulation water. It is involved across production, cleaning, sterilization support, and environmental control processes. The exact application profile depends on whether the site produces oral liquids, injectables, dialysis solutions, vaccines, cell culture products, or medical consumables.
Main applications include:
The main benefits are equally significant. First, the system provides product quality consistency. Second, it reduces microbial excursions and endotoxin risks. Third, it improves audit readiness because records, alarms, trends, and SOP alignment are easier to maintain in automated systems. Fourth, it lowers total cost of ownership when properly sized, especially in states with high utility costs such as California, Massachusetts, and New York. Fifth, it supports expansion by allowing future generation and distribution capacity upgrades.
Application AreaRequired Water LevelOperational BenefitCompliance BenefitTypical U.S. Facility TypePriority LevelAseptic injectablesWFIStable sterile batch productionStrong endotoxin controlInjectable manufacturersVery HighVial and ampoule washingPW or WFI final rinseReduced particulate and residueBetter line clearance evidenceSterile filling plantsHighEquipment final rinsePW or WFICleaner changeoversSupports cleaning validationMulti-product plantsHighOral liquid manufacturingPurified WaterConsistent formulation qualityControlled microbial profileLiquid dose facilitiesMediumBiologics buffer prepPurified Water or WFIProcess reproducibilityBatch traceabilityBiotech sitesHighPure steam generationWFI feed or high-purity waterReliable SIP performanceSterility assurance supportAseptic plantsVery HighThe explanation from this table is straightforward: not every process needs WFI, but every process does need the correct grade delivered with a validated distribution strategy. Overdesign drives unnecessary capital and utility cost, while underdesign increases deviation risk.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chartBar = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Injectables’, ‘Biologics’, ‘Vaccines’, ‘Oral Liquids’, ‘Dialysis’, ‘Medical Consumables’],datasets: [{label: ‘Estimated U.S. demand intensity for pharma water systems’,data: [95, 88, 84, 62, 71, 58],backgroundColor: [‘#3366cc’,’#109618′,’#ff9900′,’#dc3912′,’#990099′,’#0099c6′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});Pharmaceutical manufacturers in the United States typically evaluate four broad technology routes: RO-based systems, RO + EDI systems, distillation-based systems, and hybrid systems. The best choice depends on water grade, source water variability, energy cost, plant footprint, validation philosophy, and expected production volume.
RO systems use semi-permeable membranes to remove dissolved solids, organics, and many contaminants. They are effective as a primary purification step and are common in Purified Water generation. However, RO alone may not be sufficient for final pharmaceutical specifications without additional polishing and microbial control.
EDI systems are often paired with RO to continuously polish water using electricity and ion-exchange media. RO + EDI is widely used for Purified Water applications because it offers high consistency, chemical reduction, and good operating efficiency.
Distillation systems, especially multi-effect water distillers, remain a preferred technology for WFI in many sterile facilities. They are highly respected for robust endotoxin and microbial control, although energy demand, steam integration, and capital cost can be higher.
Hybrid systems combine membrane and thermal technologies. A plant may use double-pass RO + EDI for Purified Water and a multi-effect distiller downstream for WFI, or deploy advanced pretreatment with membrane-based WFI generation depending on regulatory acceptance and risk assessment.
System TypeBest ForMain StrengthMain LimitationUtility ImpactTypical U.S. Buyer ProfileSingle-pass ROBasic pretreatment or low-criticality useLower capital costLimited polishing capabilityModerate electricitySupport utilitiesDouble-pass ROHigher purity feedImproved rejectionNeeds strong pretreatmentModerate electricityPW-focused plantsRO + EDIPurified WaterConsistent quality, low chemical useFeed water sensitivityEfficient overallOral, biotech, cleaning systemsMulti-effect distillationWFIExcellent endotoxin controlHigher capital and steam demandHigher thermal loadSterile injectable plantsVapor compression distillationWFI with compact designEfficient in some duty rangesMechanical complexityBalanced thermal/electricalMedium-large sterile sitesHybrid membrane + thermalFlexible multi-grade systemsOptimized lifecycle performanceMore complex design integrationCustomizableLarge GMP campusesThis table shows why no single technology is universally best. Facilities in Texas or North Carolina with available utility infrastructure may prioritize robust thermal WFI generation, while compact biotech sites in urban clusters may prefer efficient hybrid designs that save floor space and support phased expansion.
From a technological capability perspective, suppliers should be able to engineer not only RO, EDI, and distillation modules but also integrated storage and distribution loops, online monitoring, and validation packages. IVEN Pharmatech Engineering is known in the market for combining pharmaceutical water treatment units, multi-effect water distillers, purified steam generators, and solution preparation systems into broader regulated plant engineering scopes. Buyers who want to review broader corporate capability can explore the company overview at IVEN Pharmatech Engineering.
Traditional water treatment methods serve many industrial sectors well, but they are generally insufficient for sterile pharmaceutical manufacturing. Municipal-grade filtration, softening, standard deionization, and non-sanitary storage tanks may produce technically clean water, yet they do not provide the consistent microbiological control, documentation, and hygienic design expected in regulated sterile operations.
The decision is therefore not between two equal options. For any facility producing injectables, ophthalmics, or high-risk sterile products in the United States, pharmaceutical-grade water treatment is the appropriate choice. The more relevant comparison is how advanced the pharmaceutical water system should be based on the plant’s risk profile.
Comparison PointTraditional Water TreatmentSterile Pharma Water SystemOperational ImpactCompliance ImpactPreferred ChoiceDesign standardIndustrial utility focusSanitary GMP designBetter cleanabilitySupports inspectionsSterile pharma systemMicrobial controlLimitedContinuous control strategyFewer excursionsHigher assuranceSterile pharma systemDocumentationBasic manualsDQ/IQ/OQ/PQ supportFaster qualificationAudit readinessSterile pharma systemDistribution loopOften static or low hygieneRecirculating sanitary loopStable water qualityLower contamination riskSterile pharma systemMonitoringPeriodic onlyOnline data-rich monitoringFaster troubleshootingBetter data integritySterile pharma systemLifecycle suitabilityLower initial cost onlyHigher long-term valueReduced downtimeLower deviation riskSterile pharma systemIn practice, traditional systems may still be appropriate for non-product-contact support functions outside GMP scope, but once water enters product, cleaning validation, aseptic support, or sterile processing, the decision should shift toward purpose-built pharmaceutical infrastructure.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var chartComp = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Compliance’, ‘Microbial Control’, ‘Validation Support’, ‘Operating Stability’, ‘Expandability’, ‘Lifecycle ROI’],datasets: [{label: ‘Traditional water treatment’,data: [35, 30, 20, 45, 40, 50],backgroundColor: ‘#dc3912’},{label: ‘Sterile pharma water system’,data: [92, 90, 94, 88, 84, 86],backgroundColor: ‘#3366cc’}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The U.S. market for pharmaceutical water treatment is supported by continued investment in sterile injectables, biologics, vaccine resilience, CDMO expansion, and domestic manufacturing initiatives. States such as Massachusetts, New Jersey, California, North Carolina, Indiana, and Maryland continue to attract pharma and biotech capital, while logistics hubs connected to ports in Los Angeles, Long Beach, Houston, Savannah, and New York/New Jersey support equipment importation and project execution.
Several drivers are shaping the market:
Looking toward 2026, future trends are likely to include smarter automation, remote diagnostics, predictive maintenance, lower-energy distillation, membrane optimization, more advanced sanitization strategies, and stronger emphasis on reclaiming process efficiency without compromising GMP compliance. Policy direction in the United States also continues to favor resilient domestic manufacturing for critical medicines, which indirectly supports investment in utility systems including pharmaceutical water generation.
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var chartLine = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. sterile pharma water system market index’,data: [100, 108, 117, 129, 141, 156],borderColor: ‘#109618’,backgroundColor: ‘rgba(16,150,24,0.1)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: false } }}});var ctxArea = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var chartArea = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Shift toward automated and sustainable systems’,data: [28, 35, 44, 56, 68, 79],borderColor: ‘#ff9900’,backgroundColor: ‘rgba(255,153,0,0.25)’,fill: true,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The line chart illustrates broad growth in demand, while the area chart shows the increasing share of projects prioritizing automation, utility efficiency, and sustainability features. This matters for U.S. buyers because systems purchased today should still be competitive and compliant several years from now.
Choosing the right supplier is often more important than choosing the lowest equipment price. The best manufacturers or suppliers combine engineering discipline, regulated manufacturing experience, validation knowledge, and service responsiveness. A strong water system vendor should understand not only purification technology but also pharmaceutical process integration, FDA expectations, and lifecycle support needs.
Key evaluation factors include:
Supplier Evaluation PointWhy It MattersWhat to AskGood SignWarning SignBuyer PriorityRegulatory knowledgeSupports compliant designHave you supplied FDA-oriented projects?Clear GMP referencesGeneric industrial answersVery HighEngineering depthReduces integration riskCan you design full loops and utilities?Process + mechanical + controls teamOnly skid sales focusHighManufacturing qualityAffects durability and hygieneHow are welds documented?Traceable fabrication recordsLimited QA visibilityVery HighValidation supportSaves startup timeDo you provide IQ/OQ packages?Structured qualification documentsBuyer must create everythingHighService networkMinimizes downtimeWhat is your response plan in the U.S.?Defined support pathwayUnclear service commitmentHighTotal solution capabilityImproves project deliveryCan you support turnkey integration?Multi-system project experienceFragmented vendor responsibilityMedium to HighFrom a manufacturing capability standpoint, many buyers prefer companies that build multiple categories of pharmaceutical equipment rather than only standalone utility skids. This often indicates stronger cross-functional design and integration experience. IVEN Pharmatech Engineering, for example, operates specialized manufacturing bases across pharmaceutical filling and packaging machinery, pharmaceutical water treatment systems, intelligent logistics systems, and blood collection tube equipment, which can be valuable for projects that need coordinated utilities and process lines.
For buyers comparing equipment or project options, it can also help to review available product ranges through a supplier’s pharmaceutical equipment portfolio before moving into formal technical discussion.
Capital investment for water treatment sterile manufacturing in the United States varies widely depending on capacity, water grade, automation level, utility integration, documentation scope, and installation complexity. A small Purified Water package for a development or pilot facility may cost far less than a fully redundant WFI generation and distribution system for a commercial injectable plant.
Budget planning should separate at least six cost categories: equipment, engineering, piping and installation, automation and software, validation, and operating utilities. Many buyers underestimate the cost of distribution loop design, commissioning, and qualification, even though these elements strongly influence final system performance.
Cost ElementLower Complexity RangeHigher Complexity RangeKey Cost DriverCan It Be Optimized?ROI ImpactPretreatment package$20,000-$80,000$100,000+Feed water qualityYesProtects core systemRO/EDI generation$80,000-$250,000$400,000+Flow rate and redundancyYesMajor operating valueWFI distillation$150,000-$400,000$700,000+Capacity and steam integrationPartlyCritical for sterile outputStorage and distribution loop$100,000-$300,000$800,000+Plant layout and loop sizeYesStrong quality effectAutomation and instrumentation$30,000-$120,000$250,000+Data and control complexityYesImproves reliabilityValidation and startup$25,000-$100,000$200,000+Documentation depthYesFaster release to productionThe table indicates that lifecycle thinking is more useful than focusing on first cost. For ROI, common gains come from reduced batch loss, lower downtime, fewer cleaning deviations, reduced chemical consumption, better energy efficiency, and smoother inspections. In high-value sterile manufacturing, one avoided contamination event may justify significant investment.
A realistic ROI model for a U.S. facility should include:
Service capability matters strongly here. A supplier that can support feasibility, design review, equipment customization, installation, commissioning, qualification, training, and optimization helps prevent hidden costs later. IVEN Pharmatech Engineering positions itself around this full-lifecycle approach, which is particularly relevant for overseas procurement projects entering the United States market or for investors building new facilities with broad utility and process scope.
Investment in pharmaceutical water infrastructure carries strategic value, but it also comes with technical and project risks. The most common failure point is not the core technology itself; it is poor alignment between the process requirement, the engineering design, and the operational reality of the plant.
Important considerations include source water variability, peak demand, redundancy expectations, heat load, sanitization philosophy, future expansion, and plant layout constraints. In coastal or industrial regions of the United States, incoming water chemistry may fluctuate seasonally, requiring more robust pretreatment. In dense urban facilities, utility room footprint and ceiling height can strongly influence the technology choice.
Potential risks include:
One practical mitigation strategy is to engage suppliers early and request a documented user requirement specification, utility balance, and phased implementation roadmap. Buyers should also confirm spare parts planning, local technical support, and long-term service communication. If you are evaluating project support or need direct consultation, a useful next step is to contact the engineering team for project discussion.
For companies building complete plants, risk also decreases when the water system is coordinated with filling lines, washing equipment, sterilization strategy, and material handling rather than designed in isolation. This integrated view is particularly important in sterile injectable and infusion projects.
1. What water grades are most important in sterile pharmaceutical manufacturing?Purified Water and Water for Injection are the most important. Pure Steam is also essential in many aseptic facilities for sterilization and SIP support.
2. Is RO + EDI enough for all sterile applications?No. RO + EDI is widely used for Purified Water, but WFI applications often require distillation or another validated approach acceptable for the intended regulatory and process context.
3. How often should a pharmaceutical water system be sanitized?The answer depends on design, use pattern, monitoring data, and sanitization method. A validated preventive schedule should be defined during qualification and adjusted based on trending.
4. What industries beyond injectable drugs use these systems?Biologics, vaccines, oral liquids, dialysis solutions, ophthalmics, medical consumables, and some device manufacturing segments all rely on pharmaceutical water systems.
5. What should U.S. buyers ask first when comparing suppliers?Ask for GMP project references, water quality guarantees, material specifications, validation document examples, and service support plans for the United States.
6. How long can a well-built system last?With proper maintenance, sanitary stainless steel construction and disciplined operation, core equipment can remain productive for many years, often well beyond a decade.
7. Why do turnkey capabilities matter?Turnkey capability reduces interface risk between utilities, process equipment, controls, installation, and qualification. This is especially useful for greenfield projects and fast-track expansions.
8. Are sustainability features becoming important in 2026 planning?Yes. U.S. manufacturers increasingly prioritize water recovery, lower-energy thermal systems, smarter controls, and optimized sanitization cycles to reduce resource consumption while maintaining GMP performance.
9. Can an international supplier serve the U.S. market effectively?Yes, if the supplier demonstrates strong compliance knowledge, proven export execution, robust documentation, and reliable service coordination. Experience with EU GMP, U.S. FDA cGMP, WHO GMP, and PIC/S expectations is a meaningful advantage.
10. What makes IVEN Pharmatech Engineering relevant for this market?The company combines pharmaceutical water treatment expertise with broader sterile manufacturing, filling, packaging, logistics, and turnkey project capability. For U.S. buyers, that can be valuable where integrated engineering, customized design, and lifecycle support are more important than buying a standalone utility skid at the lowest upfront price.
In summary, water treatment sterile manufacturing is a foundational investment for pharmaceutical production in the United States. It supports patient safety, regulatory compliance, stable operations, and long-term factory performance. The most successful projects align system type, plant demand, validation strategy, and supplier capability from the beginning. Buyers who evaluate technology, lifecycle cost, and integration quality together are far more likely to achieve a reliable and audit-ready result.
-
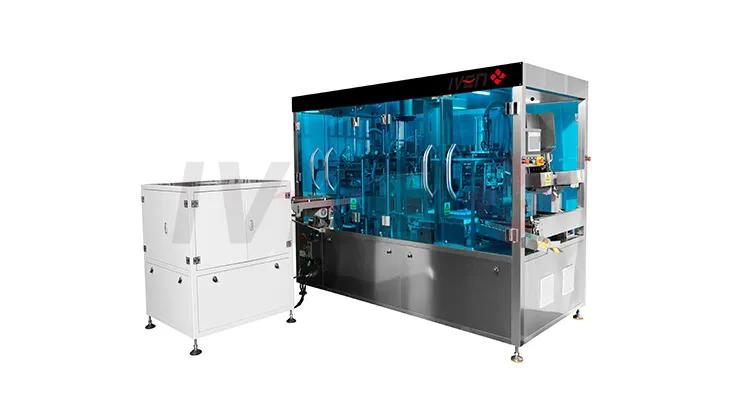
Micro Blood Tube Line Troubleshooting in the United States
For U.S. medical device companies, effective micro blood tube line troubleshooting is essential for maintaining high output, precise additive dosing, stable cap assembly, and reliable quality control. A well-designed automated production line helps hospitals, physician office labs, and diagnostic networks receive consistent micro blood collection tubes at scale while reducing downtime, labor dependence, and contamination risk.
In the United States, demand for capillary and micro blood collection products continues to rise across pediatric care, neonatal testing, outpatient diagnostics, home collection programs, and decentralized laboratory services. Manufacturers serving buyers in cities such as Boston, Chicago, Houston, San Diego, and Atlanta must balance FDA-focused quality expectations with speed, traceability, and cost discipline. That is why troubleshooting is no longer just a maintenance task. It has become a core production strategy tied directly to OEE, batch release confidence, and long-term profitability.
Whether a factory is located near major logistics corridors such as the Port of Los Angeles, Port of Long Beach, Port of Houston, Savannah, or Newark, uninterrupted tube line performance matters. Delays in tube molding transfer, chemical dosing, drying, capping, vacuum-related functions, tray loading, and labeling can ripple through the full plant and affect customer delivery commitments. For that reason, U.S. buyers increasingly prefer suppliers that can provide not only equipment, but also validation support, line integration, remote diagnostics, and lifecycle service.
Micro blood tube line troubleshooting is the structured process of identifying, correcting, and preventing production issues on automated lines that manufacture micro blood collection tubes. In practical terms, it covers diagnosis of feeder jams, inaccurate reagent filling, cap fitting errors, tube contamination, sensor faults, drying instability, printing defects, and packaging interruptions. When handled correctly, troubleshooting enables medical device companies to sustain large-volume output with stable quality for U.S. hospitals, clinics, and diagnostic laboratories.
The biggest benefit is not simply fixing a fault after it happens. The real advantage lies in building a line that can detect abnormal conditions early, isolate root causes, reduce scrap, and recover quickly. A mature troubleshooting system typically includes:
For U.S. manufacturers, troubleshooting also supports regulatory readiness. Better control over process deviations helps with documentation, CAPA workflows, audit response, and release consistency. This is especially important for suppliers serving large healthcare systems or laboratory chains that expect dependable product performance across every shipment.
Troubleshooting AreaTypical ProblemLikely CauseImmediate ActionLong-Term FixBusiness ImpactTube feedingFrequent jamMisaligned railsStop and re-center feederUpgrade guide designOutput lossAdditive dosingUnderfill or overfillPump drift or nozzle cloggingRecalibrate pumpScheduled verification planBatch rejection riskDrying stationIncomplete dryingAirflow imbalanceAdjust temperature and flowInstall zone monitoringClumping or residueCap assemblyLoose or tilted capsFeeder vibration mismatchReset cap trackServo-controlled cap placementSeal failureInspectionFalse rejectsVision sensitivity issueRe-teach image standardImprove lighting and algorithmYield reductionLabeling/packingWrong count or print issueSensor timing driftCheck encoderIntegrated line synchronizationShipment delaysThe table above shows why troubleshooting should be treated as an integrated quality and production discipline, not just a maintenance checklist. Each fault affects both technical performance and commercial reliability.
A micro blood tube production line is an automated or semi-automated system used to manufacture and assemble small-volume blood collection tubes, often designed for capillary sampling. The line may include tube unscrambling, conveying, additive spraying or filling, drying, cap feeding, capping, visual inspection, labeling, tray loading, and final packaging. Troubleshooting within this environment means evaluating each station in sequence and determining whether a process, equipment, material, or operator variable caused the deviation.
In most U.S.-oriented factories, the troubleshooting workflow follows five steps:
For example, if additive coating inside micro tubes appears inconsistent, the problem may not be the dosing pump alone. It could stem from viscosity variation, room humidity, nozzle wear, compressed air fluctuation, or conveyor indexing inconsistency. Good troubleshooting therefore depends on line integration and process understanding.
Advanced systems used by larger medical device companies often include PLC-based diagnostics, HMI alarm libraries, production trend dashboards, and camera inspection records. These digital tools help teams in the United States reduce dependence on tribal knowledge and create standardized responses across multiple shifts.
From a technology standpoint, a strong line supplier should understand more than standalone equipment. This is where an engineering-driven company matters. IVEN Pharmatech Engineering is known in the sector for combining pharmaceutical and medical consumable equipment expertise with compliance-focused engineering. Its technical capabilities are relevant because micro blood tube manufacturing requires precise dosing, controlled handling, clean design, and reliable automation logic rather than simple assembly alone.
Line ModuleMain FunctionCommon Fault SignalDiagnostic MethodCorrective MeasurePrevention MethodUnscramblerOrient tubesOrientation errorCheck bowl vibration and guide pathReset feed angleRoutine mechanical inspectionConveyorTransfer tubesPosition driftReview encoder and belt tensionAlign conveyorWeekly calibrationDosing unitApply additiveVolume varianceSample weigh testAdjust dosing headPump maintenance scheduleDrying stationStabilize additiveResidue or wet filmMeasure heat and airflowChange air distributionThermal mappingCapping unitPlace capsCap misfitInspect track and gripperRe-time placement motionCap feeder validationInspection systemReject defectsHigh false reject rateReview image settingsRecalibrate cameraGolden sample libraryThis table explains how troubleshooting is linked to each functional station. Faster diagnosis comes from designing the line so each module can be checked independently while still sharing data across the whole system.
Micro blood collection tubes are used across pediatric blood draws, neonatal screening, point-of-care support, outpatient testing, emergency departments, and low-volume laboratory applications. In the United States, these products are especially valuable where venous blood draw is difficult or sample volume must be minimized. Buyers include hospital systems, reference labs, physician group practices, community clinics, blood testing service networks, and contract medical product distributors.
For manufacturers, the production benefits of a stable and well-troubleshot line include:
Factories supplying U.S. customers often need to support mixed production, such as different tube sizes, cap colors, labeling formats, packaging counts, and private-label requirements. In that environment, troubleshooting becomes even more important because changeovers can introduce setup errors. The right production line should therefore support recipe management, quick format adjustment, and validation-friendly controls.
On the manufacturing side, supplier depth matters. IVEN has developed multiple generations of blood collection tube production equipment and combines that experience with broader clean utility, packaging, and logistics capabilities. That manufacturing base is useful for U.S. customers seeking a line partner with plant-scale understanding rather than a narrow machine-only provider. More details on broader integrated projects can be seen at turnkey engineering solutions.
var ctxBarIndustryDemand = document.getElementById(‘barIndustryDemand’).getContext(‘2d’);var chartBarIndustryDemand = new Chart(ctxBarIndustryDemand, { type: ‘bar’, data: { labels: [‘Pediatric Hospitals’, ‘Diagnostic Labs’, ‘Outpatient Clinics’, ‘Home Collection’, ‘Research Centers’, ‘Emergency Care’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [92, 88, 76, 61, 54, 67], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The bar chart above illustrates where demand pressure is strongest in the U.S. market. Pediatric hospitals and diagnostic laboratories typically place the highest emphasis on product consistency, while home collection and decentralized care are becoming important growth drivers.
Application SegmentTypical End UserWhy Micro Tubes MatterProduction PriorityTroubleshooting FocusCommercial BenefitPediatric testingChildren’s hospitalsLower blood volume neededConsistencyCap seal and additive accuracyPremium reliabilityNeonatal careNICUsVery small sample sizesClean handlingContamination controlClinical trustOutpatient diagnosticsClinic networksFast routine testingVolume outputLabeling and packing flowEfficient distributionReference laboratoriesCentral labsLarge batch procurementLot traceabilityInspection data integrityContract retentionHome collection programsTelehealth providersUser-friendly formatPackaging qualityKit completenessExpanding channel reachResearch useBiotech and universitiesControlled samplingCustomizationFormat changeoverHigher margin ordersThe explanation from this table is straightforward: each application has different production priorities, so troubleshooting plans should be aligned with actual buyer expectations rather than generic machine uptime alone.
Micro blood tube lines are available in several configurations depending on target output, automation level, additive chemistry, cleanroom requirement, and packaging style. U.S. buyers should evaluate not only throughput, but also the line architecture needed for validation, maintenance access, and future product expansion.
Common configurations include:
Selection should also consider whether the line processes EDTA, heparin, clot activator, gel-related, or customized additive solutions. Different formulations change the drying profile, dosing tolerance, nozzle design, and cleaning protocol.
For companies comparing equipment options, reviewing available configurations through a structured product catalog can help narrow choices. A starting point can be found at medical and pharmaceutical equipment solutions, especially for buyers seeking integrated production ecosystems rather than isolated machines.
Configuration TypeOutput RangeBest ForKey StrengthMain RiskRecommended U.S. Buyer ProfileSemi-automaticLowDevelopment or niche productsLower initial costHigher labor variabilityStartups and pilot facilitiesCompact automaticLow to mediumRegional supplySmaller footprintLimited expansionMid-size OEMsModular automaticMediumMulti-SKU productionFlexible changeoverControl complexityPrivate-label suppliersHigh-speed integratedHighNational volume supplyStrong productivityHigher capital demandLarge medical manufacturersCleanroom-optimizedMedium to highSensitive productsBetter contamination controlUtility costQuality-focused exportersTurnkey line with packagingMedium to highNew factory projectsFull process integrationProject coordination pressureInvestors building greenfield plantsThe table explains that the best line is not always the fastest one. For many U.S. companies, modularity, compliance support, and long-term service are just as important as nominal speed.
Manual or labor-heavy assembly remains an option for very small-scale operations, but it has serious limitations for U.S. medical device companies that need repeatability, documentation, and commercial scalability. Automated micro blood tube lines significantly outperform manual processes in consistency, labor efficiency, contamination control, and data collection. Troubleshooting on an automated line is also more systematic because fault patterns can be captured electronically.
Manual lines depend heavily on operator skill. That can create shift-to-shift variation, especially in dosing, cap fit, visual acceptance, and packaging counts. Automated systems reduce this variation by locking in process parameters and enabling routine verification. They also make CAPA investigations easier because the production record is more complete.
var ctxComparisonSupplierProduct = document.getElementById(‘comparisonSupplierProduct’).getContext(‘2d’);var chartComparisonSupplierProduct = new Chart(ctxComparisonSupplierProduct, { type: ‘bar’, data: { labels: [‘Consistency’, ‘Traceability’, ‘Labor Efficiency’, ‘Scale-Up Speed’, ‘Defect Control’, ‘Audit Readiness’], datasets: [ { label: ‘Automated Line’, data: [94, 96, 91, 89, 93, 95], backgroundColor: ‘#6f42c1’ }, { label: ‘Manual Assembly’, data: [58, 41, 44, 37, 52, 46], backgroundColor: ‘#adb5bd’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The comparison chart shows how automated lines create broad operational advantages beyond speed alone. In the United States, where customers expect robust documentation and dependable lot performance, those differences become commercially decisive.
FactorAutomated LineManual AssemblyWhy It MattersTroubleshooting EffectU.S. Market ImpactOutput stabilityHighLow to mediumSupports delivery schedulesAlarms aid fast responseBetter contract performanceQuality repeatabilityHighOperator dependentCritical for medical useData-based correctionFewer complaintsLabor costLower per unitHigher per unitImproves marginLess human errorMore competitive pricingTraceabilityDetailedLimitedImportant for auditsRoot cause easier to proveRegulatory confidenceScalabilityStrongWeakSupports national growthStandard SOPs possibleFaster expansionContamination controlBetterHarder to manageProtects product integrityControlled environmentReduced rejection riskThis table explains that troubleshooting in automated production creates cumulative business advantages. Better data means better decisions, and better decisions mean stronger margins and customer retention.
The U.S. market for blood collection consumables remains attractive due to aging demographics, chronic disease monitoring, decentralized testing growth, and expanding pediatric and outpatient diagnostics. Micro blood collection products are also gaining relevance as home sampling models develop and as health systems seek patient-friendly collection formats.
For manufacturers, the opportunity is not limited to tube sales alone. There is value in private-label manufacturing, custom cap colors, integrated packaging kits, OEM partnerships, and regional fulfillment models. Producers located close to distribution hubs such as Memphis, Dallas, Columbus, and New Jersey can gain logistical advantages in serving national accounts quickly.
In addition, reshoring and supply-chain resilience remain strategic themes in the United States. Buyers increasingly assess supplier stability, documentation quality, spare parts availability, and service responsiveness. This opens room for well-prepared international manufacturers that can support local expectations through strong engineering, validation files, and reliable after-sales coordination.
var ctxLineMarketGrowth = document.getElementById(‘lineMarketGrowth’).getContext(‘2d’);var chartLineMarketGrowth = new Chart(ctxLineMarketGrowth, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [{ label: ‘U.S. Micro Blood Tube Equipment Demand Index’, data: [68, 72, 77, 84, 91, 98, 106], borderColor: ‘#20c997’, backgroundColor: ‘rgba(32,201,151,0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});The line chart reflects realistic growth momentum based on stronger diagnostic demand, replacement of older lines, and greater interest in automation-ready manufacturing platforms.
Case studies in this market often show that U.S. manufacturers gain the most when they do three things together: automate core assembly, standardize troubleshooting, and plan service support before installation. Companies that delay maintenance strategy often face more expensive downtime later. For this reason, experienced engineering partners that can advise on equipment selection, layout logic, validation planning, and post-startup optimization offer a measurable advantage.
Choosing a micro blood tube line supplier for the United States requires more than comparing quotations. The right supplier should be evaluated on technical depth, compliance familiarity, customization ability, documentation quality, factory manufacturing capability, spare parts planning, and service responsiveness. U.S. buyers should also confirm whether the supplier can support IQ, OQ, PQ-style documentation and structured FAT/SAT processes where needed.
Key checkpoints include:
Service capability is especially important. A line may be mechanically strong, but if the supplier cannot support commissioning, operator training, spare parts forecasting, or process optimization, the ownership experience will suffer. IVEN’s service model is relevant here because it extends beyond delivery into installation, commissioning, validation support, documentation, training, and ongoing optimization. U.S. buyers seeking to discuss plant fit, service response, or project scope can connect through the contact page.
Selection CriterionWhy It MattersQuestions to AskStrong Supplier SignalWarning SignDecision ImpactTechnical specializationImproves process fitHow many similar lines delivered?Proven tube line portfolioOnly generic automation historyHigher performance confidenceCompliance awarenessSupports auditsWhat documents are included?Structured FAT/IQ/OQ supportMinimal documentationLower regulatory riskCustomization abilityFits product mixCan the line run multiple SKUs?Recipe-based designRigid fixed setupBetter expansion pathManufacturing strengthAffects quality and lead timeWhere are key modules made?Dedicated production plantsHeavy outsourcingMore stable deliveryAfter-sales serviceReduces downtimeWhat is the support plan?Training and remote supportOne-time shipment onlyLower lifecycle costReference credibilityShows real experienceAre there international projects?Global installationsNo verifiable casesSafer purchasing decisionThe explanation is clear: supplier quality determines how much troubleshooting effort your team will face after installation. A stronger supplier reduces both launch risk and long-term operational friction.
Investment in a micro blood tube line can vary widely based on automation level, speed, additive system complexity, cleanroom integration, inspection depth, packaging scope, and validation requirements. U.S. projects should budget not only for machine purchase, but also for utilities, room preparation, tooling, spare parts, training, FAT/SAT travel, software support, and ongoing maintenance.
Typical cost categories include:
ROI usually comes from labor reduction, lower defect rates, fewer customer complaints, higher batch throughput, shorter lead times, and improved contract win rates. For larger U.S. manufacturers, an automated line may justify itself in two to four years depending on utilization, margin, and quality savings. A robust troubleshooting framework accelerates ROI because it shortens the time needed to stabilize production after start-up.
var ctxAreaTrendShift = document.getElementById(‘areaTrendShift’).getContext(‘2d’);var chartAreaTrendShift = new Chart(ctxAreaTrendShift, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [{ label: ‘Shift from Labor-Heavy to Automated Production (%)’, data: [34, 39, 45, 52, 60, 67, 73], borderColor: ‘#0d6efd’, backgroundColor: ‘rgba(13,110,253,0.20)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The area chart highlights the industry trend toward automation and data-based process control. This shift is likely to continue through 2026 and beyond as labor costs, traceability expectations, and quality requirements keep rising.
Budget ItemRelative Cost LevelWhat Drives CostCan It Be Optimized?ROI RelevancePlanning AdviceBase equipmentHighSpeed and automation levelYesDirectMatch output to demand forecastInspection systemMedium to highCamera count and softwarePartlyStrong through scrap reductionDo not under-specifyUtilities integrationMediumRoom readiness and HVACYesIndirectAudit site conditions earlyTooling/change partsMediumSKU diversityYesImproves flexibilityPlan future formats nowTraining/serviceMediumSupport scopeNo major shortcut advisedVery highProtect start-up successSpare parts packageLow to mediumCritical component listYesStrong through downtime reductionPrioritize wear itemsThis table explains that the lowest upfront quote is rarely the lowest total cost. Smart budget planning looks at full lifecycle performance, not purchase price alone.
Before investing, U.S. manufacturers should evaluate product demand stability, line flexibility, room conditions, staffing capability, maintenance readiness, spare parts stocking, and regulatory documentation needs. A technically good machine can still perform poorly if facility design, utilities, operator training, or material consistency are weak.
Main investment risks include:
One practical way to reduce risk is to choose a supplier with both technological and project capability. IVEN’s background in pharmaceutical and medical device engineering, including equipment, water systems, logistics, and production integration, is relevant because blood tube projects often interact with broader factory workflows. For U.S. projects, this integrated thinking can reduce layout conflicts, schedule slippage, and qualification surprises.
Looking ahead to 2026, three trends are especially important in the United States:
Manufacturers that invest with these trends in mind will be in a stronger position to serve healthcare networks, distributors, and OEM buyers over the next several years.
1. What are the most common micro blood tube line troubleshooting problems?The most common issues include tube jams, inaccurate additive dosing, incomplete drying, cap misalignment, vision inspection false rejects, and packaging synchronization errors. Most are linked to setup drift, worn parts, sensor calibration, or material variation.
2. Is troubleshooting different for U.S. buyers?Yes. U.S. buyers typically expect stronger documentation, traceability, validation support, and quality records. Troubleshooting therefore needs to be documented in a way that supports audits, CAPA, and customer confidence.
3. How much automation is ideal?That depends on order volume, SKU complexity, labor cost, and quality requirements. For most commercial-scale U.S. operations, a fully automatic or modular automatic line offers the best balance of efficiency and control.
4. How can downtime be reduced after installation?Use structured FAT and SAT, train operators by station, stock critical spare parts, standardize alarm-response SOPs, and monitor recurring faults by shift and product type.
5. What should be included in a supplier quotation?Equipment scope, throughput, utility requirements, material specifications, validation documents, spare parts list, training plan, lead time, warranty terms, and post-installation support details.
6. Are turnkey projects better than standalone machine purchases?For greenfield or major expansion projects, yes. Turnkey planning can reduce interface problems between equipment, utilities, layout, and validation. For smaller upgrades, standalone equipment may still be practical.
7. What role does predictive maintenance play?A growing one. By 2026, more lines in the United States are expected to use predictive alerts based on cycle counts, vibration, temperature, and alarm history. This reduces unplanned stoppages.
8. How important is local or remote service support?It is critical. A strong service program shortens recovery time, improves operator confidence, and protects ROI. Remote diagnostics, multilingual support, and clear spare parts planning are major advantages.
9. Can a line be customized for multiple tube formats?Yes, but customization should be designed from the start. Recipe control, quick-change tooling, adaptable feeders, and validation-friendly software are important for multi-format production.
10. What kind of partner is best for a U.S. project?The best partner combines technical depth, manufacturing capability, and lifecycle service. That means more than machine supply. It includes engineering judgment, production experience, quality documentation, commissioning, training, and optimization support.
For medical device companies serving the United States, the most effective approach is to view micro blood tube line troubleshooting as part of a larger production excellence system. When equipment design, process control, operator training, documentation, and service support work together, manufacturers gain higher uptime, stronger quality confidence, and better commercial resilience. In a market shaped by strict customer expectations and rapid diagnostic demand, those advantages matter every day.