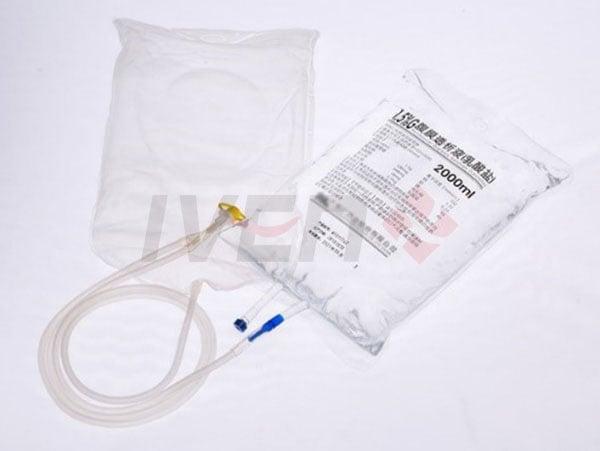
PD Solution Shelf Life and Storage in the United States
Peritoneal dialysis fluid is a sterile medical product, so storage shelf life is not just a packaging detail; it is a quality, patient safety, and supply chain issue. In the United States, manufacturers, contract packers, dialysis providers, and healthcare investors evaluate PD solution storage shelf life to ensure that fluids remain chemically stable, microbiologically safe, and commercially viable from production to final use. A well-designed production line supports controlled formulation, sterile filling, reliable container sealing, validated packaging, and data-based traceability so that PD solution can be supplied efficiently to both home dialysis patients and hospital systems.
For the U.S. market, this topic also connects directly to regulatory expectations, warehouse strategy, transport distance, and emergency preparedness. Products may move through pharmaceutical hubs in New Jersey, distribution networks in Chicago and Atlanta, hospital systems in Boston and Houston, and West Coast gateways such as the ports of Los Angeles and Long Beach. The longer and more predictable the approved shelf life, the easier it becomes to manage inventory, prevent waste, and maintain continuity of care for chronic kidney disease patients.
Quick Answer: How PD Solution Storage Shelf Life Supports Safe Kidney Care

PD solution storage shelf life helps manufacturers supply safe, sterile peritoneal dialysis fluids for both home treatment and hospital use in chronic kidney disease management. In practical terms, shelf life is the validated period during which the dialysis solution remains within approved specifications for sterility, composition, pH, glucose level, container integrity, labeling accuracy, and usability when stored under defined conditions.
For U.S. buyers, a strong shelf-life strategy delivers five direct advantages. First, it reduces product loss caused by expiration before use. Second, it supports long-distance distribution across the United States, including remote and rural delivery routes. Third, it improves inventory planning for home dialysis programs. Fourth, it helps hospitals and group purchasing organizations reduce shortage risk. Fifth, it supports compliance with cGMP, stability testing, and quality documentation expected in regulated pharmaceutical manufacturing.
| Factor | Why It Matters | Effect on U.S. Supply |
|---|---|---|
| Sterility assurance | PD solution must remain free from microbial contamination | Protects patients in home and clinical settings |
| Chemical stability | Electrolytes, glucose, and pH must stay within specification | Maintains treatment performance |
| Container integrity | Bag, bottle, or overpouch must resist leaks and oxygen ingress | Supports long shipping distances |
| Label readability | Instructions, expiry date, and batch data must remain clear | Improves traceability and safe use |
| Temperature control | Storage conditions can accelerate degradation if not controlled | Critical in hot states and seasonal transport |
| Regulatory documentation | Validated shelf life must be supported by stability data | Required for approval and audits |
The table above shows that shelf life is a system outcome, not a single number on a label. It depends on formulation, packaging format, sterilization approach, production control, warehouse conditions, and distribution design.
What Is PD Solution Storage Shelf Life and Why Is It Important for Kidney Care?

PD solution storage shelf life refers to the approved period during which a peritoneal dialysis solution can be stored before use while still meeting all quality requirements. This usually includes stability under specified temperatures, light exposure conditions, and packaging configurations. The concept applies to commercially produced PD fluids used in continuous ambulatory peritoneal dialysis and automated peritoneal dialysis.
In kidney care, this matters because PD patients depend on regular, uninterrupted access to sterile fluid. Unlike many oral medicines, peritoneal dialysis solution is a high-volume consumable. A home patient may need multiple bags per day, and a clinic or hospital may store large quantities for ongoing treatment. If shelf life is too short, manufacturers and providers face higher write-offs, more frequent deliveries, and greater risk of stockouts. If shelf life is well validated and supported by robust packaging, the treatment network becomes safer and more resilient.
For the United States, importance is amplified by geography. Products may be manufactured in one state, warehoused in another, and delivered to patients hundreds or thousands of miles away. Weather extremes from Arizona heat to Midwest winter conditions can also stress packaging and logistics systems. Therefore, shelf-life performance must align with the real transport and storage environment, not only laboratory conditions.
| Shelf-Life Element | Typical Validation Focus | Kidney Care Relevance |
|---|---|---|
| Physical stability | Appearance, precipitation, color changes | Ensures solution remains usable |
| Chemical stability | Assay, glucose degradation, pH drift | Supports proper dialysis performance |
| Microbiological safety | Sterility maintenance over time | Prevents serious infection risk |
| Seal integrity | Leak tests, burst resistance, transit durability | Protects patients during home delivery |
| Packaging compatibility | Interaction with bag or bottle materials | Maintains purity and safety |
| Usability after storage | Port function, readability, handling quality | Improves patient confidence and compliance |
This is why production technology selection should be aligned with long-term quality performance. Companies evaluating new lines often review integrated design, water systems, sterile filling, and packaging engineering together rather than as separate purchases. Buyers that need broader factory planning can review turnkey pharmaceutical project capabilities to understand how utilities, cleanrooms, filling systems, and validation workflows influence final shelf-life outcomes.
Role and Benefits of PD Solution Storage Shelf Life in Home and Hospital Dialysis Treatment

In home dialysis, storage shelf life affects patient convenience, delivery frequency, and emergency preparedness. A patient storing several weeks of dialysis supplies at home needs confidence that the product will remain stable under normal indoor conditions until use. Longer validated shelf life gives providers more scheduling flexibility and allows families to maintain contingency stock during storms, transport disruptions, or insurance-related delivery delays.
In hospitals, shelf life supports centralized inventory control, rapid replenishment, and better preparedness for nephrology units, intensive care departments, and inpatient dialysis support programs. Hospitals in major cities such as New York, Philadelphia, Dallas, and Seattle often manage multi-site networks, where inventory may move across regional warehouses. Better shelf-life performance reduces internal transfers and disposal costs.
There is also a financial benefit. A product with reliable shelf life can improve batch planning, reduce safety stock pressure, and lower the hidden costs of urgent freight, replacement product, and expired inventory. For a manufacturer, this translates into stronger forecasting and improved customer service levels. For providers, it means more reliable patient continuity.
| Use Setting | Benefit of Reliable Shelf Life | Operational Result |
|---|---|---|
| Home dialysis | Less frequent emergency resupply | Higher patient confidence |
| Hospital pharmacy | Lower expiration-related waste | Better budget control |
| Regional warehouse | More flexible inventory rotation | Smoother distribution planning |
| Rural care programs | Supports longer transport routes | Improved access for remote patients |
| Disaster readiness | Allows buffer stock management | Greater continuity during disruptions |
| Manufacturing site | Longer commercial window per batch | Higher planning efficiency |
The benefits shown above are especially relevant in the U.S. because home-based care is growing and delivery logistics are increasingly scrutinized for cost and resilience.
Key Types, Models and Technical Options for PD Solution Storage Shelf Life
There is no single “shelf-life machine.” Shelf life is influenced by a combination of formulation system, container choice, sterilization compatibility, filling accuracy, sealing quality, and secondary packaging. In production planning, buyers usually compare line configurations based on final container format and quality goals.
Common primary packaging options include non-PVC soft bags, PP bottles, and in some applications specialized rigid containers. Soft bags are widely associated with transport efficiency and patient handling convenience, while PP bottles may suit specific process and packaging preferences. Technical options that affect storage shelf life include automated solution preparation, closed transfer systems, sterile filtration support where applicable, high-precision filling, leak detection, overwrap packaging, and serialized traceability.
Advanced manufacturers also evaluate integrated utilities. Water quality systems, clean steam, clean compressed air, and controlled CIP/SIP strategy all influence consistency. A weak utility design can shorten commercial shelf-life confidence by increasing process variability even when the filling equipment itself is modern.
| Option | Technical Feature | Potential Shelf-Life Impact |
|---|---|---|
| Non-PVC soft bag line | Flexible container, efficient sealing, compact transport | Can support good distribution durability |
| PP bottle line | Rigid packaging with defined handling profile | May offer strong structural stability |
| High-barrier overpouch | Extra moisture and oxygen protection | Improves packaging robustness |
| Automated leak detection | Online rejection of defective containers | Reduces contamination and expiry risk |
| Advanced batch traceability | Digital data capture and coding | Supports recalls and expiry control |
| Integrated stability-oriented line design | Controlled preparation, transfer, fill, seal, packaging | Improves long-term consistency |
When comparing equipment platforms, it helps to work with a supplier that understands both engineering and compliance. IVEN Pharmatech Engineering has built a global reputation in pharmaceutical and medical device production solutions and is particularly known for integrated lines for IV and dialysis-related applications. Its technical capabilities include solution preparation systems, water treatment, filling and packaging integration, and layouts aligned with EU GMP, U.S. FDA cGMP, WHO GMP, and PIC/S expectations. More background is available on the company’s corporate profile page.
PD Solution Storage Shelf Life vs Alternative Technologies: Which Solution Fits Your Needs?
Buyers often compare shelf-life-oriented PD solution production investments with alternative approaches such as short-run local compounding, smaller decentralized filling, or reliance on third-party imported product. The best choice depends on scale, market access, compliance readiness, and risk tolerance.
For large-volume U.S. demand, industrial sterile manufacturing with validated shelf life is generally the strongest model because it supports regulatory control, repeatability, and broad distribution. Smaller decentralized approaches may appear attractive for responsiveness, but they often face higher per-unit cost, more variable documentation, and narrower efficiency. Imported supply can help fill demand gaps, yet it adds shipping time, customs complexity, and port dependence at gateways such as Long Beach, Savannah, or Newark.
Another comparison is between container systems. A buyer focused on home delivery may prioritize lighter packaging and cubic efficiency, while a buyer focused on certain automated handling systems may prefer rigid formats. The right answer depends on the downstream distribution model and patient use pattern.
| Approach | Advantages | Limitations |
|---|---|---|
| Centralized industrial PD production | Scale, validation depth, strong quality control | Higher upfront capital investment |
| Decentralized small-batch filling | Potential regional responsiveness | Higher unit cost and validation burden |
| Imported finished product | Fast market entry without full plant build | Longer logistics chain and tariff exposure |
| Soft bag-based distribution model | Transport efficiency and patient convenience | Requires robust sealing and material control |
| Rigid bottle-based model | Strong shape retention and handling predictability | Higher shipping volume and weight |
| Hybrid sourcing strategy | Balances redundancy and local support | More complex supply planning |
The table makes clear that “best” does not mean universal. It means fit for your regulatory pathway, product volume, distribution geography, and service model.
Current Market Trends and Demand for PD Solution Storage Shelf Life Production Capacity
The U.S. renal care market continues to support demand for dependable PD solution manufacturing capacity. Several drivers are shaping investment decisions: growth in home-based care, pressure to strengthen domestic or regional supply resilience, aging patient populations, ongoing concern about shortage management, and renewed interest in secure sterile fluid manufacturing.
In market terms, buyers are paying more attention to storage shelf life because inventory performance affects commercial resilience. A product with stable long-range distribution performance is more attractive to integrated health systems, dialysis networks, and distributors serving multiple states. U.S. policy discussions around domestic medical manufacturing, supply chain transparency, and emergency stock planning have also increased interest in modern dialysis solution lines.
From a 2026 trend perspective, three themes stand out. First, digital quality systems will increasingly connect production data with stability, warehousing, and release documentation. Second, sustainability will matter more, including packaging weight reduction, energy-efficient utilities, and lower waste from expired stock. Third, policy and procurement will likely favor traceable, compliance-ready manufacturing with stronger domestic servicing and validation support.
The charts above illustrate a realistic trend: rising demand, stronger pull from home dialysis, and a broader shift toward supply models that depend on reliable shelf life and distribution stability.
How to Choose a Reliable PD Solution Storage Shelf Life Manufacturer or Supplier
Choosing a supplier should start with evidence, not claims. For the U.S. market, buyers should evaluate whether the manufacturer or engineering partner can support regulatory documentation, validated sterile process design, dependable utility systems, robust container handling, and lifecycle service. A reliable supplier should be able to explain how its line design affects stability outcomes, not just throughput numbers.
Technological capability is the first screen. Look for expertise in pharmaceutical water systems, solution preparation, sterile transfer, filling and sealing, packaging, and digital traceability. A capable engineering partner should understand how these systems interact and how to structure them for validation. IVEN Pharmatech Engineering is one example of a company with broad technical depth across pharmaceutical filling, packaging, water treatment, intelligent logistics, and integrated production engineering, making it relevant for buyers who want more than a standalone machine.
Manufacturing capability is the second screen. Buyers should review plant scale, fabrication quality, materials of construction, quality control discipline, installed base, and experience with international projects. IVEN’s manufacturing platform includes multiple specialized plants in Shanghai and a long history of delivering production lines for IV solutions, dialysis solutions, injectables, and medical consumables in more than 60 countries. That matters because shelf-life reliability often reflects years of accumulated process design and field feedback, not only design software.
Service capability is the third screen. The best supplier is usually the one that can support feasibility review, engineering design, customization, installation, commissioning, validation, staff training, and post-start optimization. For U.S. investors, this becomes even more important when the project includes clean utilities, documentation packages, and phased capacity expansion. Companies needing direct discussion can use the contact channel for project consultation to assess fit early.
| Evaluation Point | What to Ask | Why It Matters |
|---|---|---|
| Regulatory fit | Can the supplier align with U.S. FDA cGMP expectations? | Reduces compliance risk |
| Stability-oriented design | How does the line protect sterility and consistency? | Directly affects shelf life |
| Installed references | Are there similar dialysis or sterile fluid projects? | Shows practical experience |
| Customization ability | Can the line match your container and capacity goals? | Improves project fit |
| Validation support | Does the supplier assist with IQ/OQ/PQ and documentation? | Speeds startup and audit readiness |
| After-sales service | What is the support model for spare parts and troubleshooting? | Protects long-term uptime |
Suppliers with broad product portfolios can also help buyers benchmark options across filling, water, logistics, and packaging. Reviewing an integrated catalog of systems through the equipment solutions portfolio is often useful when a project includes multiple process blocks instead of a single line purchase.
Investment Cost, Budget Planning and ROI Analysis for PD Solution Storage Shelf Life
Budgeting for PD solution shelf-life-oriented manufacturing requires more than equipment pricing. Investors should calculate total installed cost, including utilities, cleanrooms, validation, warehousing, automation, and quality systems. A lower machine quote can become expensive if the layout is inefficient, documentation is incomplete, or the line cannot support the target stability profile.
Major cost categories typically include formulation and holding systems, purified water and WFI-related infrastructure where applicable to the process design, sterile filling and sealing equipment, packaging equipment, environmental controls, laboratories, and warehouse systems. U.S. projects may also require strong integration with serialization, data integrity controls, and local commissioning resources.
ROI comes from more than unit output. Better shelf life can improve return by reducing product waste, extending distribution reach, supporting higher service levels, lowering emergency freight, and enabling stronger contract performance. For companies serving both home care and institutional demand, these savings can materially improve payback.
| Cost Category | Typical Share of Budget | ROI Relevance |
|---|---|---|
| Core production line | 25% to 35% | Determines capacity and consistency |
| Water and utility systems | 10% to 18% | Supports sterile process quality |
| Cleanroom and HVAC | 12% to 20% | Essential for compliance |
| Packaging and logistics | 8% to 15% | Affects distribution durability |
| Validation and documentation | 5% to 10% | Required for timely release and audits |
| Training and service support | 3% to 7% | Protects startup performance |
As the table indicates, shelf-life success depends on coordinated spending. Underfunding packaging integrity or utility consistency can weaken the return on an otherwise modern filling line.
A simple ROI model may compare capital cost against four annual gains: reduced expired inventory, lower logistics premiums, increased sellable output from better yield, and stronger contract capture due to reliable service. In the U.S., these benefits are particularly visible when the product must move across multiple regional zones and serve a mix of urban and rural demand.
Key Considerations and Potential Risks When Investing in PD Solution Storage Shelf Life
The main investment risk is assuming that shelf life can be “added later” through testing alone. In reality, the commercial shelf life of PD solution is created upstream by design decisions. If the packaging material is poorly matched to the formula, if sealing quality is inconsistent, or if environmental controls are unstable, no marketing plan can fix the result.
Another risk is overlooking distribution reality. A line may perform well in factory trials, but U.S. logistics can expose product to warehouse dwell time, cross-country trucking, and seasonal temperature variation. Investors should require transport simulation, packaging qualification, and realistic stability protocols that reflect actual downstream conditions.
There is also a supplier risk. Some vendors can supply machines but not integrated validation, layout planning, or lifecycle support. That can slow the project and create expensive redesigns. Working with an experienced engineering company reduces the chance of misaligned equipment, underpowered utilities, or documentation gaps.
| Risk | Potential Impact | Mitigation |
|---|---|---|
| Weak packaging compatibility | Shorter shelf life or container failure | Run material studies early |
| Inadequate sterile control | Batch rejection and compliance exposure | Use validated process and utility design |
| Underestimated logistics stress | Damage during national distribution | Perform transit and climate testing |
| Poor supplier coordination | Commissioning delays and redesign | Select integrated engineering support |
| Insufficient documentation | Delayed approval and audits | Plan validation packages from the start |
| Demand forecast error | Overcapacity or shortage pressure | Use phased capacity planning |
For 2026 and beyond, sustainability is becoming another key consideration. Expired product is not just a financial loss; it is a waste issue. Strong shelf-life performance can reduce disposal volumes, improve transport efficiency, and support more sustainable packaging strategies. In addition, energy-efficient utilities, smarter cleanroom control, and digitized maintenance are expected to play a larger role in supplier selection.
A practical case pattern in the U.S. is the investor who wants to serve East Coast hospital systems from a Mid-Atlantic or Southeast manufacturing base while also shipping home-care inventory nationally. In such a model, shelf life influences every commercial assumption: safety stock, warehouse location, fulfillment lead time, and emergency reserve planning. Another case is a company entering the U.S. market that wants an engineering partner with both international compliance understanding and turnkey execution ability. For these buyers, supplier breadth matters as much as equipment speed.
That is where an integrated company profile becomes relevant. IVEN Pharmatech Engineering combines technological depth, established manufacturing resources, and full lifecycle service capabilities. Rather than acting only as an equipment seller, it supports project feasibility, engineering design, customization, installation, commissioning, validation, training, and optimization. For U.S. buyers seeking a structured path from concept to compliant production, that model can reduce risk and improve execution quality.
FAQ
What is a typical shelf life for peritoneal dialysis solution?
The exact shelf life depends on formulation, container material, sterilization compatibility, and validated storage conditions. It must always be supported by formal stability studies and approved labeling.
Why does packaging matter so much for PD solution storage shelf life?
Packaging protects sterility, limits interaction with the solution, and preserves seal integrity during transport and storage. A strong package can significantly improve distribution reliability.
Is longer shelf life always better?
Longer shelf life is commercially helpful, but only if it is scientifically validated and supported by stable manufacturing. Unrealistic claims create regulatory and patient safety risk.
How does shelf life affect home dialysis programs in the United States?
It improves inventory flexibility, reduces emergency deliveries, and helps patients keep safe reserve stock at home, especially in areas with weather or transport disruptions.
What should U.S. investors ask equipment suppliers first?
Ask about compliance experience, sterile process control, packaging compatibility, validation support, installed references, and after-sales service capacity.
Can a turnkey engineering company help with more than the production line?
Yes. A strong turnkey partner can support layout, water systems, utilities, cleanrooms, documentation, installation, validation, and staff training in addition to core equipment.
Which U.S. locations are important when planning PD solution logistics?
Common strategic points include New Jersey for East Coast distribution, Chicago and Atlanta for inland logistics, Houston for Southern reach, and Los Angeles/Long Beach for Pacific imports and exports.
How can buyers compare suppliers efficiently?
Use a weighted scorecard covering technology, manufacturing depth, compliance support, customization, lifecycle service, and total cost of ownership rather than only quote price.
What trends will shape PD solution storage shelf life projects in 2026?
Expect more digital traceability, stronger domestic supply expectations, sustainability-driven packaging improvements, and closer integration of quality systems with warehousing and distribution data.
Where can I learn more about integrated pharmaceutical engineering support?
You can explore the engineering background of IVEN Pharmatech Engineering, review turnkey project solutions, browse available production equipment, or request direct project consultation.
In summary, PD solution storage shelf life is a strategic manufacturing and supply chain issue for the United States, not simply a labeling statement. The right production system supports safe kidney care, reliable home and hospital supply, stronger compliance, and more resilient long-distance distribution. For companies planning new capacity or upgrading existing operations, the best results usually come from integrated engineering, validated process control, and a supplier able to support the full lifecycle of the project.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
United States Multi-Chamber IV Bag Troubleshooting Guide
Multi-chamber IV bag troubleshooting helps pharmaceutical companies manufacture advanced infusion products that keep sensitive ingredients separated until administration. In the United States, this matters because hospitals, outpatient infusion centers, and contract manufacturers increasingly need premix systems that improve stability, reduce bedside compounding, and support patient safety. When production problems are solved correctly, manufacturers can improve seal integrity, chamber separation performance, sterilization consistency, output stability, and FDA-ready quality control.
For U.S. buyers evaluating equipment or turnkey line design, troubleshooting is not only about fixing leaks or weak peel seals. It also covers formulation compatibility, film selection, chamber geometry, automation accuracy, cleanroom flow, validation, packaging logistics, and post-installation support. This is why experienced engineering partners are valuable, especially for projects supplying distribution hubs through Los Angeles, Long Beach, Houston, Newark, Savannah, Chicago, and Atlanta.
In practical terms, multi-chamber IV bag production troubleshooting means identifying and correcting the process factors that can compromise a finished bag before it reaches the clinic. A typical U.S. production team may face issues such as incomplete peelable seal formation, cross-chamber migration, inaccurate filling volumes, particle risk, poor port welding, or sterilization deformation. Because multi-chamber bags are designed to separate unstable ingredients until activation, any weakness in film structure, seal parameters, or filling synchronization can undermine product performance.
The most effective troubleshooting approach follows the entire manufacturing path: raw film inspection, bag forming, chamber separation, filling, temporary or permanent sealing, in-line leak detection, overpouching, terminal sterilization where required, visual inspection, and final packing. Manufacturers serving the United States also need to account for FDA cGMP expectations, data integrity, validation evidence, and lot traceability.
Common Production IssueLikely Root CauseOperational ImpactCorrective ActionPreventive MeasurePriority LevelWeak peel seal between chambersUnstable temperature or dwell timePremature mixing or activation failureRevalidate sealing recipe and jaw pressureUse tighter PID control and seal verification testsHighBag leakage after sterilizationFilm stress, poor weld, overfillBatch rejection and contamination riskAdjust fill volume and weld profileRun burst and dye penetration tests routinelyHighInaccurate chamber fill volumePump calibration driftDose inconsistencyCalibrate metering system and verify load cellsSet scheduled calibration and SPC reviewHighCross-contamination between chambersSeal channel defect or film incompatibilityReduced stability and safety concernsInspect seal geometry and upgrade filmPerform migration studies during validationHighPort misalignmentPositioning error in forming stationConnection difficulty for nursesReset tooling and vision alignmentInstall camera-based in-line inspectionMediumWrinkled bag surfaceIncorrect tension or cooling profilePoor appearance and sealing variabilityBalance web tension and cooling settingsStandardize startup recipe by film lotMediumThe table above shows why troubleshooting must be systematic. A leak may not originate at the final seal station alone; it may begin with film variability, web tension, or sterilization loading patterns several steps earlier. U.S. manufacturers that build strong deviation investigations and CAPA systems usually reduce waste faster than teams focused only on one machine parameter at a time.
Multi-chamber IV bag production troubleshooting is the technical and quality process used to diagnose, correct, and prevent faults in equipment and workflows that manufacture dual-chamber or multi-compartment infusion bags. These bags are used when two or more solutions, powders, or actives must stay separate until the point of use. In the United States, common applications include parenteral nutrition, premix antibiotics, dialysis-related solutions, and specialty infusion combinations.
The main advantage of proper troubleshooting is that it protects the core purpose of the product: keeping ingredients stable and isolated. Beyond that, it delivers major business benefits. It improves first-pass yield, lowers product recalls, supports FDA inspection readiness, and reduces downtime on capital-intensive lines. For hospitals and infusion pharmacies, consistent quality also means fewer bedside preparation steps and lower medication error exposure.
Production troubleshooting is usually divided into five categories: mechanical, electrical and controls, process, material, and regulatory quality. For example, a forming jaw fault is mechanical, but a false alarm trend from a vision system is controls-related. Seal delamination may be process-related, while haze or brittleness can be material-related. Missing validation evidence becomes a quality system problem even if the product looks acceptable.
Troubleshooting AreaMain FocusTypical TestWho Owns ItExpected BenefitU.S. Compliance RelevanceMechanicalSealers, conveyors, toolingAlignment and pressure mappingMaintenance engineeringFewer stoppagesSupports equipment qualificationElectrical and controlsPLC, sensors, HMI, recipesSignal validation and alarm reviewAutomation teamHigher repeatabilityData integrity and audit trailsProcessFill, seal, sterilization parametersIQ/OQ/PQ and challenge runsProcess engineeringStable quality outputProcess validation requirementsMaterialsFilm, ports, tubing compatibilityMigration and burst testingQuality and sourcingBetter shelf lifeMaterial traceability expectationsMicrobiologicalAseptic control and contaminationEnvironmental monitoringQA and microbiologyImproved sterility assuranceCritical for sterile productsDocumentationSOPs, deviations, CAPARecord review and mock auditsQuality assuranceInspection readinessFDA cGMP complianceFor companies scaling in the United States, the best advantage is predictability. Instead of firefighting every batch, they build a controlled process that can be expanded across multiple SKUs and sites.
Hospitals prefer multi-chamber products because they reduce preparation time and help standardize administration. When the bag activates correctly, clinicians can mix ingredients immediately before use, which is valuable for unstable compounds. In large U.S. health systems from Boston to Dallas and from Seattle to Miami, pharmacy departments are under pressure to shorten turnaround time while maintaining safety and traceability.
Clinical benefits include longer usable shelf life before activation, fewer compounding steps in the hospital pharmacy, reduced exposure to manual mixing errors, and better convenience for emergency departments, ICUs, oncology centers, and home infusion providers. Production troubleshooting has a direct clinical outcome because poor chamber performance can delay treatment or create uncertainty at the point of care.
Application AreaWhy Multi-Chamber HelpsTypical Product NeedClinical BenefitProduction ChallengeTroubleshooting PriorityParenteral nutritionSeparates reactive nutrientsDual or triple chamber nutrient systemsImproved stability before useComplex seal designHighPremix antibioticsKeeps drug and diluent apartPowder/liquid or liquid/liquid systemsFast preparation on wardsActivation consistencyHighEmergency medicineSpeeds administrationReady-to-activate infusionsReduced bedside delayPort robustnessMediumDialysis supportHandles sensitive solution ratiosBalanced fluid compartmentsStandardized therapyVolume precisionHighOncology support careSupports safer premix workflowsAdjunct infusion productsLower handling stepsBarrier propertiesMediumHome infusionImproves conveniencePortable activation bagsEasier patient handlingDurability in transportMediumThe table shows that different care settings create different manufacturing priorities. A home infusion bag may need stronger transport durability, while a parenteral nutrition bag may demand more sophisticated chamber isolation and film performance.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Parenteral Nutrition’, ‘Premix Antibiotics’, ‘Dialysis Support’, ‘Emergency Care’, ‘Oncology Support’, ‘Home Infusion’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [92, 88, 71, 63, 58, 67], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, plugins: { legend: { display: true } }, scales: { y: { beginAtZero: true, max: 100 } } }});The chart above reflects realistic relative demand patterns in the United States, where nutrition and premix antibiotic applications continue to drive strong interest in reliable multi-chamber systems.
Not all multi-chamber bags are built the same. Some are dual-chamber with one peelable seal. Others are triple-chamber systems with separate nutrient compartments or a powder chamber and liquid chamber combination. Production troubleshooting must match the product architecture because each bag design has different thermal, mechanical, and activation requirements.
Material selection is equally important. U.S. buyers often evaluate non-PVC soft bag structures because they can support better compatibility, lower extractables concerns in some applications, and market expectations around environmental performance. Film choice affects oxygen barrier, transparency, sterilization stability, drop resistance, sealability, and long-term storage behavior.
From a technological capability standpoint, advanced suppliers should be able to design the forming, filling, and sealing process around the selected film rather than forcing every material to run on one generic setup. This is where experienced companies stand out. Shanghai IVEN Pharmatech Engineering has developed extensive know-how in IV solution equipment and holds multiple technical patents in the field, which is relevant when buyers need line engineering for challenging bag geometries or process integration. U.S. manufacturers looking for broader background can review the company’s company background and evaluate whether the engineering depth matches their compliance and throughput goals.
System TypeTypical Chamber CountMain UseCommon Film OptionMaterial AdvantageMain Troubleshooting FocusDual-chamber liquid/liquid2Premix solutionsMultilayer non-PVC filmGood flexibility and sealabilityPeel seal consistencyDual-chamber powder/liquid2Antibiotic reconstitutionHigh-barrier laminateMoisture protectionPowder isolation and activationTriple-chamber nutrition bag3Parenteral nutritionCo-extruded multilayer filmBalanced barrier and toughnessMulti-seal validationDialysis-related compartment bag2 or 3Specialized solutionsPolyolefin-based structureThermal stabilityVolume controlLight-sensitive infusion bag2Sensitive activesTinted or UV-protective filmImproved product protectionAppearance and compatibilityHigh-volume hospital premix bag2Routine infusion useStandard non-PVC medical filmCost-effective productionThroughput and leak rateFor U.S. regulatory strategy, material qualification should include extractables and leachables assessment where applicable, sterilization compatibility studies, and transport simulation. A film that performs well in Asia or Europe still needs to fit U.S. labeling, quality documentation, and supply-chain expectations.
Single-chamber IV bags remain important because they are simpler and less expensive to manufacture. However, they cannot solve the same stability challenges as multi-chamber products. When unstable components must remain separate, a single-chamber format may require last-minute hospital compounding, which increases labor and can introduce variability.
From a production viewpoint, multi-chamber lines demand more advanced tooling, controls, and validation. Yet they can create higher-value products and support differentiated market positioning in the United States. That is why many manufacturers accept greater line complexity in exchange for stronger margins and better clinical utility.
Comparison PointMulti-Chamber IV BagSingle-Chamber IV BagBusiness ImpactQuality RiskBest FitIngredient separationMaintains separation until activationNo separationSupports premium productsLower stability if incompatible ingredients are combinedUnstable or reactive formulationsManufacturing complexityHigherLowerMore capital requiredMore validation pointsSpecialty infusion linesHospital preparation needsReducedOften higherSaves labor downstreamLower bedside mixing error riskLarge health systemsUnit production costGenerally higherGenerally lowerCan support better marginsDepends on scaleTargeted product portfoliosShelf-life strategyCan improve pre-activation stabilityLimited for incompatible productsBroader commercial opportunityRequires strong material studiesSensitive formulationsTroubleshooting intensityHighModerateNeeds skilled engineering teamMore seal and migration checksAdvanced sterile operationsThis comparison makes it clear that choosing multi-chamber production is not simply a packaging decision. It is a strategic product and process decision that affects clinical positioning, market access, and manufacturing capability.
The U.S. market is showing sustained interest in ready-to-use and ready-to-activate infusion products. Several trends are driving investment: hospital labor shortages, pressure to reduce sterile compounding steps, increasing use of premix medications, and the need for more resilient domestic or near-market production capacity. In addition, healthcare providers are looking for packaging that reduces waste and supports safer medication workflows.
Geography matters. East Coast pharmaceutical hubs around New Jersey and Pennsylvania benefit from dense healthcare networks and strong logistics access through the Port of Newark. Gulf and Southeast distribution routes through Houston and Savannah support wide regional shipment. West Coast entry points like Los Angeles and Long Beach remain important for imported equipment, spare parts, and film materials. Midwest manufacturing clusters near Chicago and Indianapolis continue to matter for sterile product operations.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Multi-Chamber Capacity Demand Index’, data: [58, 63, 69, 77, 86, 95], borderColor: ‘#2f6fed’, backgroundColor: ‘rgba(47,111,237,0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The line chart shows a realistic expansion pattern through 2026. Demand is not only about volume; it also reflects a shift toward more sophisticated bag formats that require stronger process control and higher line capability.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Standard Single-Chamber Share’, data: [72, 69, 65, 60, 56, 51], borderColor: ‘#9c755f’, backgroundColor: ‘rgba(156,117,95,0.20)’, fill: true, tension: 0.3 },{ label: ‘Advanced Multi-Chamber Share’, data: [28, 31, 35, 40, 44, 49], borderColor: ‘#59a14f’, backgroundColor: ‘rgba(89,161,79,0.20)’, fill: true, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, stacked: false } } }});The area chart highlights a broader packaging trend: single-chamber systems remain essential, but advanced multi-chamber formats are gaining share as hospitals demand safer and more efficient workflows.
Looking toward 2026, the most important market trends are digital line monitoring, predictive maintenance, broader use of vision inspection, sustainability-focused film development, and stronger localization of after-sales service. Policy expectations may also keep pushing manufacturers toward better traceability, robust validation data, and resilient U.S. supply-chain planning.
Choosing a supplier in the United States market requires more than checking machine speed. Buyers should review regulatory understanding, sterile project experience, film-material compatibility, service response time, spare-part support, and the supplier’s ability to provide validation documentation. A fast line without stable process control is usually more expensive in the long term than a slightly slower line with strong repeatability.
When comparing U.S. local integrators, global machine builders, and turnkey engineering firms, buyers should assess whether the supplier can support the full production ecosystem: water systems, solution preparation, filling, sealing, sterilization interfaces, packaging, warehousing, and quality documentation. This is where integrated engineering providers often have an advantage over stand-alone machine vendors.
From a manufacturing capability perspective, IVEN Pharmatech Engineering is relevant because it operates multiple specialized manufacturing plants focused on pharmaceutical filling and packaging machinery, water treatment systems, logistics systems, and blood collection equipment. That broader industrial base matters for companies planning complete sterile facilities instead of isolated machine purchases. Buyers reviewing options may compare integrated solutions through the company’s turnkey pharma engineering page and its wider equipment portfolio.
Supplier Evaluation FactorWhat to CheckWhy It MattersWarning SignBest EvidenceWeight in DecisionRegulatory knowledgeFDA, cGMP, validation familiarityReduces compliance riskGeneric promises onlyDocument templates and prior auditsVery HighProcess expertiseExperience with multi-chamber seals and filmsImproves startup successNo application referencesFAT data and case examplesVery HighManufacturing depthOwn factories and quality controlBetter consistency and lead-time controlHeavy outsourcingPlant visit or audit reportHighService networkCommissioning, training, spare partsLimits downtimeSlow support commitmentSLA or support planHighCustomization abilityCan adapt to formula and bag designSupports product differentiationOne-size-fits-all offerCustomized URS responseHighTotal project capabilityUtilities, cleanroom, logistics integrationAvoids interface failuresOnly machine-only viewTurnkey layouts and schedulesMedium to HighLocal supplier choice should also consider ports, spare-parts stocking, and field engineer access. A site in New Jersey may prioritize East Coast support and customs convenience through Newark, while an Arizona or California project may care more about Pacific logistics and faster access through Los Angeles or Long Beach.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Regulatory Support’, ‘Customization’, ‘Turnkey Scope’, ‘After-Sales Speed’, ‘Validation Documentation’, ‘Long-Term Value’], datasets: [{ label: ‘Integrated Engineering Supplier’, data: [92, 89, 95, 83, 90, 88], backgroundColor: ‘rgba(54, 162, 235, 0.7)’ },{ label: ‘Single-Machine Vendor’, data: [68, 61, 42, 74, 58, 63], backgroundColor: ‘rgba(255, 159, 64, 0.7)’ }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The comparison chart illustrates why many U.S. investors prefer an integrated supplier for complex sterile projects. Machine quality matters, but documentation, utility integration, and lifecycle support often determine the real return on investment.
Investment planning in the United States should separate equipment price from total installed cost. A realistic budget includes formulation and process development, utilities, cleanroom modifications, validation, training, maintenance inventory, packaging systems, warehouse interfaces, and possible serialization or digital traceability upgrades. Companies that budget only for the filling-sealing line often face overruns during installation.
Capital cost varies by configuration, but the main drivers are number of chambers, line speed, automation level, inspection technology, sterilization requirements, cleanroom classification, and desired documentation depth. A pilot or niche line may be justified for specialty products, while a large commercial line fits high-volume hospital supply strategies.
Budget ItemLow Complexity ProjectMid-Scale ProjectHigh-Scale ProjectCost DriverROI EffectCore forming/filling/sealing lineModerateHighVery HighSpeed and automation levelDirect throughput impactWater and solution systemsModerateHighHighPharma utility scopeProduct quality reliabilityInspection and leak testingModerateHighHighVision sophisticationReduces rejects and recallsValidation and documentationModerateModerate to HighHighRegulatory expectationsFaster approval readinessFacility adaptationLow to ModerateModerateHighCleanroom and utility changesAffects project timelineTraining and spare partsLowModerateModerateSupport modelImproves uptimeThe table shows why ROI depends on the full system, not just the machine purchase. In many cases, buyers can justify a higher upfront investment if the line reduces batch failures, labor intensity, and outsourced compounding needs.
A simplified ROI framework for U.S. projects should include six variables: annual output, expected selling price per bag, reject rate reduction, labor savings, maintenance cost, and downtime impact. For example, if a well-engineered line improves usable yield by even 3% to 5% on a high-value premix product, the annual savings can materially shorten payback time.
Service capability becomes critical here. A supplier that supports feasibility analysis, engineering design, installation, commissioning, validation, training, and later optimization can reduce hidden costs. IVEN is known for a full-lifecycle approach that covers those stages, which is useful for investors that want fewer interface gaps during implementation. Companies planning a U.S. project can contact the team for project-specific discussion, especially where ROI depends on combining line supply with utilities and quality documentation.
The biggest risk is underestimating complexity. Multi-chamber bags are not just upgraded soft bags; they are integrated product systems where film science, process engineering, and clinical usability all interact. If the supplier lacks true application experience, startup delays can be significant.
Key considerations include formulation compatibility, film qualification, port design, scale-up strategy, cleaning validation, sterility assurance, operator training, and spare-part availability. U.S. buyers should also evaluate whether they need domestic warehousing for critical components or local technical response to support uptime goals.
Another frequent risk is non-standard plant layout. Poor material and personnel flow can create contamination pressure points or reduce maintenance access. That is why early engineering design matters. Investors should also review whether the line can expand later to support additional bag sizes or products instead of becoming a bottleneck after two years.
A practical case-study pattern seen in the market involves a manufacturer launching a dual-chamber premix line without fully validating film behavior after sterilization. Initial production appears acceptable, but leaks emerge during transportation and warehouse temperature changes. The root cause turns out to be a combined effect of seal profile, overfill margin, and pallet stacking pressure. The lesson is clear: troubleshooting must include transport simulation and real supply-chain conditions, especially in the United States where products may move from a Midwest plant to hospitals across multiple climate zones.
Another case pattern involves a company choosing the cheapest machine vendor for a specialty nutrition project, then discovering that the vendor cannot provide coherent IQ/OQ documents, recipe security logic, or clean utility integration. The apparent savings disappear through delays, consultant fees, and rework. Investors should measure project risk as carefully as purchase price.
Looking ahead to 2026, three factors will shape risk management. First, digital monitoring will become standard, with more lines using predictive maintenance and real-time seal quality analytics. Second, sustainability pressure will increase interest in efficient energy use, reduced film waste, and improved packaging design. Third, regulatory scrutiny around documentation, data integrity, and supply resilience is likely to remain high, especially for critical hospital products.
What does multi-chamber IV bag troubleshooting usually involve first?It usually starts with mapping the defect to one production stage: film feeding, forming, filling, chamber sealing, final sealing, sterilization, or transport. The first goal is to identify whether the issue is mechanical, process-based, material-based, or quality-system related.
Why are multi-chamber bags more difficult to manufacture than standard IV bags?They require precise chamber isolation, reliable activation performance, tighter seal control, and often more complex validation. The bag must remain stable during storage yet function easily for the user at the point of care.
What are the most common defects on U.S. production lines?The most common are weak peel seals, leakage after sterilization, fill volume variation, port welding defects, chamber migration, cosmetic wrinkling, and false rejects from vision systems.
Is non-PVC film always the best choice?Not always. Non-PVC structures are often attractive, but the right choice depends on formulation compatibility, sterilization method, barrier needs, shelf-life targets, and regulatory documentation.
How should U.S. buyers compare suppliers?Compare them on application experience, FDA-oriented documentation, film and bag design expertise, manufacturing depth, service response, spare-parts support, and ability to deliver complete system integration.
What project scale makes sense for entry into this market?That depends on your target product, forecast demand, and reimbursement or supply contracts. Some companies begin with a focused specialty line, while others invest directly in larger commercial capacity for hospital distribution.
Can a turnkey supplier reduce project risk?Yes, especially when the project includes utilities, solution preparation, automation, packaging, and validation. Turnkey coordination often reduces interface failures between multiple vendors.
How important is local service in the United States?Very important. Fast support can reduce costly downtime, especially for sterile operations. Buyers should ask about commissioning presence, spare-parts strategy, remote diagnostics, and field engineer availability.
What should be included in a pre-purchase factory acceptance test?Bag format verification, seal strength testing, volume accuracy, challenge runs, alarm testing, recipe control review, HMI functionality, documentation package review, and where possible, trial runs using the intended film structure.
Where can buyers learn more about integrated project options?They can review the supplier’s engineering background, turnkey delivery model, equipment range, and service offering before requesting a tailored proposal. For example, interested companies may explore IVEN’s company background, turnkey pharma engineering, and equipment portfolio before using the contact page for a project discussion.
For the United States market, the strongest conclusion is simple: multi-chamber IV bag production can create real clinical and commercial value, but only when troubleshooting is built into design, validation, and ongoing operations. Companies that invest in the right film strategy, robust line engineering, disciplined quality systems, and experienced lifecycle support are better positioned to serve hospitals safely and profitably through 2026 and beyond.
-
Coagulation Tube Machines for the United States Market
Hospitals, reference laboratories, and diagnostic networks across the United States rely on stable supplies of coagulation test tubes for PT, APTT, fibrinogen, D-dimer, and related hemostasis assays. For medical device companies serving this demand, a blood collection tube machine for coagulation testing is not simply a packaging asset; it is a controlled production platform that affects product consistency, additive dosing accuracy, labeling compliance, throughput, and total manufacturing cost. In a market shaped by FDA expectations, laboratory accreditation requirements, and hospital purchasing pressure, automated production lines give manufacturers a practical path to higher capacity and lower variability.
From large healthcare hubs such as New York, Boston, Chicago, Houston, Los Angeles, and Atlanta to regional distribution corridors linked to the Ports of Los Angeles, Long Beach, Savannah, Houston, and New York/New Jersey, the U.S. market values dependable lead times and traceable production. Companies that invest in modern tube manufacturing equipment can improve supply resilience, shorten delivery cycles, and support domestic or near-market inventory strategies. Businesses exploring integrated line design, validation planning, or turnkey factory execution can also review broader engineering capabilities through turnkey pharmaceutical and medical device project solutions.
A blood collection tube machine for coagulation testing enables medical device manufacturers to produce high volumes of sodium citrate blood collection tubes with reliable automation, precise additive filling, controlled drying or coating processes where applicable, secure stoppering, vacuum control, labeling, inspection, and packaging. In practical terms, it helps companies deliver uniform tube quality to hospitals and diagnostic laboratories while reducing labor dependence and batch-to-batch variation.
For the U.S. market, this matters because coagulation tubes must support exact blood-to-additive ratios. Even small inconsistencies can affect test integrity, specimen acceptability, and laboratory confidence. Automated lines are designed to keep dosing, assembly, and inspection within validated ranges, helping manufacturers meet customer expectations for dimensional accuracy, closure integrity, lot traceability, and particulate control.
For buyers, the real value can be summarized in five points:
In the United States, suppliers that can prove process capability, installation support, validation readiness, and long equipment life are often favored by manufacturers supplying integrated delivery networks, government health systems, and large lab chains.
A blood collection tube machine for coagulation testing is a specialized automated production line used to manufacture vacuum blood collection tubes intended for coagulation assays. These tubes are commonly identified by their light blue closure and typically contain buffered sodium citrate anticoagulant. The machine line usually integrates multiple stations into a synchronized manufacturing process.
A typical workflow includes tube feeding, tube orientation, additive preparation, precise liquid filling, drying or post-filling conditioning depending on formulation requirements, stopper feeding, vacuum generation, cap assembly, labeling, printing, vision inspection, leak checking, packing, and batch data recording. In advanced configurations, line software can connect with MES or plant-level quality systems for electronic records and statistical process monitoring.
The most important process control points usually include:
Modern lines may use servo-driven indexing, peristaltic or ceramic pump filling systems, vacuum chambers, automated cap sorting, CCD vision inspection, and reject stations for nonconforming units. Manufacturers serving the United States often request audit-friendly design features such as stainless-steel contact surfaces, batch reporting, alarm history, user access control, and easier IQ/OQ/PQ preparation.
To illustrate the process logic, the table below summarizes common modules found on coagulation tube production lines and why each matters.
Production ModulePrimary FunctionQuality ImpactCommon Automation LevelTypical U.S. Buyer ConcernNotesTube FeedingSupplies empty PET or glass tubes to the linePrevents jams and misalignmentAutomaticLine uptimeOften includes unscrambling and orientationAdditive FillingDispenses sodium citrate solutionControls blood-to-additive ratioHigh precisionDosing accuracyCritical for coagulation test reliabilityDrying or ConditioningStabilizes filled tubes where process requires itSupports product consistencySemi or fully automaticFormulation compatibilityDepends on tube chemistry designStoppering and CappingApplies closures and cap assembliesAffects seal integrityAutomaticClosure fit and leakageOften linked with stopper detection sensorsVacuumingCreates target vacuum volumeEnsures correct blood drawAutomatic chamber controlDraw-volume consistencyOne of the most audited process stepsInspection and PackagingChecks defects and prepares shipmentReduces field complaintsAutomatic vision and packingTraceability and final yieldCan include barcode verificationThe key takeaway is that a coagulation tube line is not a single machine but a coordinated production system. The more mature the line integration, the easier it becomes to maintain repeatability, document performance, and support customer audits.
The main application of this equipment is the production of coagulation blood collection tubes used by hospital laboratories, independent reference labs, emergency departments, oncology centers, surgical departments, dialysis centers, and blood management programs. Yet its business impact extends beyond product output. It influences production planning, compliance confidence, and operating margin.
In the United States, demand comes from a wide range of end users. Large academic medical centers in Boston and Philadelphia often require dependable premium quality and documentation depth. High-throughput lab systems in Chicago, Dallas, and Phoenix prioritize volume reliability and barcode quality. Regional distributors serving clinics and ambulatory centers look for cost stability and short replenishment cycles.
Benefits for medical device companies include:
Many companies also use automation to broaden their product portfolio. Once they establish stable manufacturing for coagulation tubes, they can consider adjacent vacuum blood collection products for serum, glucose, ESR, or other applications, depending on line compatibility and strategic expansion plans.
The following table shows where coagulation tube demand typically comes from and what each buyer group values most.
End-Use SectorMain Use CaseTypical Purchase DriverVolume LevelQuality PriorityCommercial OpportunityLarge HospitalsRoutine coagulation panelsReliable supply contractsHighHighLong-term tendersReference LaboratoriesCentralized hemostasis testingBarcode and specimen consistencyVery highVery highNational accountsEmergency DepartmentsRapid clotting assessmentFast replenishmentMediumHighRegional distributionOutpatient ClinicsRoutine blood drawsCost-effective packsMediumMediumDistributor channel salesSurgery CentersPre-op and post-op testingSmall lot reliabilityLow to mediumHighNiche premium supplyGovernment and VA SystemsStandardized diagnosticsCompliance and continuityHighHighStructured procurement programsThis demand diversity is why machine flexibility matters. A supplier should not only provide output speed but also support size changes, closure changes, packaging changes, and documentation discipline suited to different customer segments.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Large Hospitals’, ‘Reference Labs’, ‘Outpatient Clinics’, ‘Emergency Departments’, ‘Surgery Centers’, ‘Government Systems’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [88, 95, 62, 71, 44, 67], backgroundColor: [‘rgb(54, 162, 235)’,’rgb(75, 192, 192)’,’rgb(255, 206, 86)’,’rgb(255, 159, 64)’,’rgb(153, 102, 255)’,’rgb(201, 203, 207)’] }] }, options: { responsive: true, maintainAspectRatio: false }});Not every manufacturer needs the same line design. The ideal configuration depends on output target, tube material, additive chemistry, floor space, labor availability, packaging style, and validation expectations. In the current market, machine options range from compact semi-automatic units to highly integrated fully automatic systems.
Common configurations include stand-alone filling equipment, modular vacuum tube assembly lines, and complete end-to-end production platforms with online inspection and packing. Some manufacturers choose a phased investment model, starting with core stations and later adding automation modules as demand grows. Others, especially those serving major U.S. lab networks, prefer a fully integrated line from the beginning to simplify qualification and reduce manual intervention.
The table below compares major machine configurations available today.
Configuration TypeBest ForAutomation LevelOutput PotentialInvestment LevelKey LimitationSemi-Automatic Filling CellPilot or small volume producersLow to mediumLowLowerHigher labor dependenceModular Assembly LineGrowing regional suppliersMediumMediumMediumIntegration may vary by moduleFully Automatic Coagulation Tube LineLarge-scale manufacturersHighHighHighNeeds stronger utility planningIntegrated Line with Vision InspectionPremium regulated productionHighHighHigherMore validation work upfrontMulti-SKU Flexible LineBroad product portfoliosHighMedium to highHigherChangeover discipline requiredTurnkey Smart Factory SolutionNew plants and strategic investorsVery highVery highHighestLonger implementation timelineFor buyers that want deeper engineering integration, equipment should be assessed as part of the full plant workflow, including water systems, logistics, warehousing, cleanroom layout, line clearance strategy, and final packaging flow. This is where experienced engineering partners become valuable.
On the technology side, IVEN Pharmatech Engineering is known in the sector for multi-generation vacuum blood collection tube equipment and for combining machine design with wider pharmaceutical and medical device engineering know-how. Its technological capabilities are especially relevant for buyers that need more than stand-alone machinery and want coordinated process design, automation logic, and quality-oriented line architecture.
Manual or labor-intensive assembly can still work for niche volumes, development projects, or local low-scale production. However, for sustained U.S. demand, the disadvantages quickly become visible: inconsistent dosing, slower cycle times, more handling, higher training burden, and weaker process traceability.
Automated equipment does not just increase speed; it changes the quality system of the product. Sensors, servo controls, recipe management, alarms, and reject mechanisms create a more disciplined process environment. This is particularly important for coagulation tubes, where clinical use depends on accurate additive ratio and dependable vacuum performance.
The following comparison highlights the main operational differences.
CriteriaAutomated Tube MachineManual Assembly LineBusiness ImpactCompliance ImpactBest FitOutput SpeedHigh and stableLow to mediumSupports scaleNeutralMass productionDosing PrecisionRepeatable and controlledOperator dependentLower rejectsHigh importanceRegulated productsLabor RequirementLower per unitHigher per unitLower long-term costNeutralCompetitive manufacturingTraceabilityBetter digital recordsMore manual recordsFaster investigationsImportantAudit-heavy customersConsistencyHigh across batchesVariableProtects brand reputationHigh importanceNational supply chainsScalabilityStrongLimitedSupports growthNeutralGrowing manufacturersFor U.S. operations facing labor shortages in industrial zones near Newark, Memphis, Dallas-Fort Worth, or Inland Empire logistics corridors, automation can also reduce recruitment risk. Fewer manual touchpoints often mean simpler staffing models and more predictable production planning.
That said, automation should be sized properly. Buying a line with excessive complexity for a low-volume business can delay payback. The right answer is not maximum automation at any cost; it is the best-fit automation level for the company’s product mix and market ambitions.
var ctxComp = document.getElementById(‘comparisonFeatureChart’).getContext(‘2d’);var comparisonFeatureChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Output Stability’, ‘Dosing Accuracy’, ‘Traceability’, ‘Labor Efficiency’, ‘Changeover Control’, ‘Final Yield’], datasets: [{ label: ‘Automated Machine Score’, data: [92, 96, 90, 88, 82, 94], backgroundColor: ‘rgb(153, 102, 255)’ },{ label: ‘Manual Line Score’, data: [55, 63, 48, 39, 60, 68], backgroundColor: ‘rgb(255, 159, 64)’ }] }, options: { responsive: true, maintainAspectRatio: false }});The U.S. market outlook remains attractive because coagulation testing continues to be essential across acute care, chronic disease management, surgery, oncology, and emergency medicine. Demand is supported by an aging population, high surgical procedure volumes, broad anticoagulant use, and continued laboratory centralization. As large healthcare systems seek stronger supply security after years of global disruption, equipment that can support efficient domestic or regional manufacturing becomes more valuable.
Opportunities for machine manufacturers include greenfield U.S. plants, contract manufacturing projects, modernization of older lines, and expansion of existing medical consumable factories. There is also room for suppliers that can offer better data integration, reduced energy use, smaller cleanroom footprints, and easier validation packages.
In terms of manufacturing capabilities, IVEN Pharmatech Engineering stands out because it operates multiple specialized manufacturing plants and has extensive experience delivering pharmaceutical and medical device production lines globally. That background matters for U.S. buyers who want proof that the supplier can support consistent fabrication quality, integrated system delivery, and long-life stainless-steel equipment suitable for demanding production environments.
The next table outlines the main growth drivers shaping this market.
Growth DriverDescriptionImpact on Equipment DemandU.S. RelevanceTime HorizonOpportunity TypeHospital Testing VolumeStable demand for coagulation assaysHighVery highShort to long termCapacity expansionSupply Chain LocalizationPreference for regional resilienceHighHighMedium termNew plant investmentLab ConsolidationCentralized testing requires consistent consumablesMedium to highHighLong termStandardized high-volume linesAutomation AdoptionManufacturers reduce labor riskHighHighShort to medium termRetrofit and replacementRegulatory Documentation NeedsBuyers seek audit-ready suppliersMediumVery highOngoingPremium machine segmentSustainability TargetsPressure to reduce waste and energy useMediumGrowing2026 onwardEfficient line redesignvar ctxLine = document.getElementById(‘marketLineChart’).getContext(‘2d’);var marketLineChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Estimated U.S. Market Demand Index’, data: [68, 72, 77, 83, 89, 96, 104], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});Looking ahead to 2026, three trends are especially important. First, smart manufacturing functions such as predictive maintenance, electronic batch data, and machine vision analytics will become more common. Second, policy pressure around quality documentation and resilient supply chains is likely to intensify. Third, sustainability metrics such as compressed air efficiency, packaging optimization, and scrap reduction will become more relevant in capital purchasing decisions.
Selecting the right supplier is often more important than selecting the lowest machine price. In the United States, the most successful equipment projects usually come from suppliers that can combine machine performance with documentation, communication, validation support, and long-term service responsiveness.
Buyers should evaluate six practical dimensions: engineering competence, manufacturing quality, regulatory awareness, installed base, service responsiveness, and total project management strength. It is also wise to ask how the supplier handles FAT protocols, spare parts planning, software backup, recipe control, and operator training.
The table below provides a practical supplier evaluation framework.
Evaluation FactorWhat to CheckWhy It MattersWarning SignPreferred EvidenceBuyer ActionTechnical DesignMachine architecture and core componentsDetermines long-term stabilityGeneric undocumented designLayout drawings and process descriptionsRequest technical reviewRegulatory UnderstandingKnowledge of GMP and U.S. expectationsSupports smoother qualificationWeak documentation languageSample IQ/OQ documentsReview validation packageManufacturing DepthOwn factory and fabrication controlReduces quality riskHeavy outsourcing without controlFactory audit or video auditVerify production capabilityAfter-Sales ServiceTraining, spare parts, remote supportLimits downtimeSlow communicationService workflow examplesCheck response commitmentsProject ExperienceInstalled base in medical and pharma sectorsImproves delivery confidenceFew comparable projectsCase history summariesAsk for referencesCustomization AbilityAdaptation to SKU, layout, and utilitiesPrevents costly compromiseOne-size-fits-all offerCustomized proposal detailsConfirm user requirement fitService capability is where many projects succeed or fail. IVEN has built a reputation around full lifecycle support, including feasibility consultation, engineering design, installation, commissioning, validation assistance, training, and optimization. For U.S. buyers, that service model can be especially useful when launching a new production line under tight timelines or when internal engineering teams are limited. Companies wanting to discuss project scope or after-sales planning can reach out through the U.S.-focused equipment inquiry channel.
Another smart step is to review the supplier’s broader business profile instead of only a product brochure. A company with deep pharmaceutical and medical device roots is often better prepared for documentation discipline, system integration, and customer audits. More background can be found on the company overview page.
Capital planning should include much more than base equipment price. A realistic budget for a coagulation tube production line in the United States may include shipping, customs, utilities, cleanroom adaptation, installation, SAT, validation, operator training, spare parts, format parts, software backup, and first-year maintenance. If the line is part of a new factory, warehousing, water systems, HVAC, logistics, and packaging areas should also be included.
Return on investment usually depends on four variables: annual unit volume, labor savings, reject reduction, and average gross margin per tube. Companies that move from manual or fragmented assembly to an integrated automated line often find that reduced scrap and better uptime contribute almost as much to ROI as labor savings.
The table below shows a simplified budget framework for planning purposes.
Cost ElementTypical Budget ShareWhy It MattersCan It Be Optimized?Common OversightPlanning AdviceCore Machine LineLargest shareMain production assetYesChoosing by price onlyCompare output and quality featuresInstallation and CommissioningMediumDetermines startup speedPartlyUnderbudgeting travel and laborDefine scope earlyValidation SupportMediumRequired for regulated useYesLate document preparationRequest package in proposal stageUtilities and Facility AdaptationMedium to highSupports stable operationYesIgnoring compressed air and HVAC loadsConduct utility mappingSpare Parts and ConsumablesLow to mediumPrevents early downtimeYesNo startup spare kitBuild first-year inventoryTraining and Ramp-UpLow to mediumProtects output during launchYesToo little operator preparationInclude repeated training sessionsAs a rough business example, a manufacturer supplying distributors in California, Texas, and the Midwest may justify investment if automation lifts output enough to support national contracts while keeping defect rates low. A supplier near logistics nodes such as the Port of Houston or rail-connected Chicago can further improve ROI by lowering domestic fulfillment times.
For companies comparing alternatives, it is helpful to request a machine list and project package from qualified suppliers. Buyers can review available equipment categories through the medical and pharmaceutical machinery portfolio and then map the line against their target tube volumes and customer contracts.
Even a strong machine can underperform if the project is poorly planned. The biggest risks usually appear at the interfaces between equipment, process chemistry, facility conditions, operators, and validation.
Before purchase, manufacturers should confirm tube material compatibility, additive stability, stopper design, target vacuum range, packaging specification, and anticipated output by SKU. They should also define user requirement specifications, acceptance criteria, utility conditions, and data expectations. U.S. buyers often benefit from building quality, operations, procurement, and maintenance into the evaluation process from the start.
Common risks include:
The trend shift through 2026 is also worth considering. U.S. buyers increasingly ask about cybersecurity for industrial controls, lower energy consumption, data traceability, and sustainable material handling. Equipment selection should therefore support future upgrades, not only today’s production plan.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Share of Buyers Prioritizing Smart + Sustainable Features’, data: [24, 31, 39, 48, 59, 68], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.25)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});A practical way to reduce risk is to choose a partner that can support not only equipment delivery but also engineering coordination. IVEN’s broader track record in integrated plant execution, logistics systems, water treatment, and medical consumables manufacturing gives buyers access to a wider problem-solving framework than a narrow machine-only vendor typically provides.
1. What additive is commonly used in coagulation blood collection tubes?Most coagulation tubes use sodium citrate anticoagulant, commonly formulated to maintain the required blood-to-additive ratio for clotting studies.
2. Why is automation important for coagulation tube production?Automation improves additive dosing accuracy, vacuum consistency, closure integrity, inspection reliability, and throughput. These factors directly affect laboratory acceptance and customer trust.
3. Can a single machine produce multiple blood collection tube types?Some lines are designed for multiple SKUs, but suitability depends on tube dimensions, closure systems, additive types, and packaging formats. Buyers should confirm changeover capability before ordering.
4. Is a fully automatic line always better than a semi-automatic one?Not always. A fully automatic line is usually best for medium to high volumes, while a semi-automatic configuration may be more economical for pilot production or niche regional demand.
5. What should U.S. buyers ask during supplier qualification?Ask about FAT protocols, validation documents, installed references, service response time, spare parts strategy, software backup, training scope, and long-term upgrade support.
6. How long does it take to implement a coagulation tube production line?Timing varies by customization level, facility readiness, utility setup, shipping route, and validation scope. A full project may take several months from design approval to commercial readiness.
7. What are the main ROI drivers?The strongest drivers are annual production volume, labor reduction, lower reject rates, improved uptime, and the ability to secure larger contracts with hospitals and diagnostic laboratories.
8. Are sustainability features becoming important in 2026?Yes. More buyers are evaluating energy efficiency, compressed air usage, material waste reduction, and smarter process monitoring as part of equipment selection.
9. What role does supplier service play after installation?It is critical. Fast technical support, spare parts availability, training refreshers, and process optimization help protect uptime and maintain quality over the life of the line.
10. Why consider IVEN for the United States market?IVEN combines specialized vacuum blood collection tube equipment with broader pharmaceutical and medical device engineering experience, strong manufacturing depth, and full lifecycle service support. That combination is valuable for U.S. manufacturers seeking not only machinery but also a dependable project partner.
For medical device companies planning entry into the United States coagulation tube market, the most effective strategy is usually to align machine selection with actual market demand, product specifications, compliance needs, and long-term service expectations. When these factors are addressed early, a blood collection tube machine for coagulation testing becomes a strategic manufacturing asset rather than a simple equipment purchase.
-
Peritoneal Dialysis Manufacturing Challenges in the United States
Peritoneal dialysis solution manufacturing is essential to safe kidney care because it enables the reliable production of sterile, stable, accurately formulated dialysis fluids used in both home-based and hospital treatment. In the United States, manufacturers must balance aseptic control, FDA cGMP compliance, packaging integrity, logistics resilience, and production scalability while supporting growing demand from chronic kidney disease patients. When these manufacturing challenges are handled well, providers can deliver dependable peritoneal dialysis therapy with consistent quality, lower contamination risk, and better continuity of care.
Across the U.S. healthcare system, demand for home dialysis has increased as providers seek patient-centered treatment models that reduce hospital dependence. That shift has put more attention on the manufacturing side of peritoneal dialysis fluids: clean utility systems, automated mixing and filling, container material selection, validation, environmental monitoring, and end-to-end traceability. For investors, plant owners, EPC teams, and medical solution manufacturers, understanding the technical and commercial realities of peritoneal dialysis manufacturing challenges is now a strategic issue rather than a narrow production topic.
In major healthcare and logistics corridors such as New Jersey, Texas, California, Illinois, and Georgia, the supply chain for dialysis products depends on resilient access to pharmaceutical-grade raw materials, ports, warehousing, and qualified engineering services. Facilities near trade gateways such as the Port of Los Angeles, Port of Long Beach, Port of Houston, Savannah, and Newark can often strengthen inbound and outbound logistics, but geographic advantages alone are not enough. Success depends on how well the plant is designed, validated, and operated.
The core challenge in peritoneal dialysis manufacturing is producing large volumes of sterile dialysis solution with exact electrolyte balance, glucose concentration control, low endotoxin risk, and packaging durability suitable for storage, shipping, and clinical use. Because these solutions go directly into patient therapy, even small deviations in formulation, particulate control, seal integrity, or bioburden can create serious quality and safety risks.
For U.S. manufacturers, the most critical issues usually include water quality management, solution preparation accuracy, aseptic filling, container-closure integrity, line clearance, cleaning validation, regulatory documentation, and capacity planning. These factors directly affect whether a facility can supply clinics and home dialysis programs without interruption. A strong manufacturing platform helps companies support chronic kidney disease management while improving confidence among providers, purchasing organizations, and regulators.
Challenge AreaWhy It MattersTypical RiskOperational ImpactPriority in U.S. PlantsBest ResponseWater for productionBase input for dialysis fluidsMicrobial contaminationBatch rejectionVery highValidated PW/WFI-related systems as required by process designFormulation accuracyPatient safety and efficacyConcentration deviationRework or wasteVery highAutomated dosing and recipe controlAseptic fillingMaintains sterilityEnvironmental contaminationRecall exposureVery highIsolator/RABS and strict EM programsPackaging integrityPrevents leaks and contaminationSeal failure in transportCustomer complaintsHighCCIT and transport simulation testingRegulatory complianceMarket access483 observations or delaysApproval interruptionVery highStrong QA, validation, and documentationCapacity planningSupports continuity of supplyStockoutsLost contractsHighModular line design and demand forecastingThe table above shows that peritoneal dialysis manufacturing challenges are not limited to one machine or one production step. They span utilities, processing, quality systems, packaging, and distribution. Companies that address these elements together typically achieve better output stability and stronger long-term returns.
Peritoneal dialysis solution manufacturing challenges refer to the technical, quality, regulatory, and supply-chain obstacles involved in designing, operating, and scaling facilities that produce dialysis fluids safely and consistently. These challenges matter because peritoneal dialysis is often used repeatedly in home settings, where patients and caregivers depend on ready-to-use, sterile products that perform reliably every day.
Kidney care in the United States is changing. More providers want flexible treatment pathways, especially for patients who benefit from home dialysis. That makes manufacturing quality even more important. Unlike a product used once in a controlled operating room, peritoneal dialysis fluids are part of a recurring care routine. Packaging must survive transportation to homes in cities like Chicago, Dallas, Phoenix, and Philadelphia, as well as to rural areas where resupply schedules are less forgiving.
Manufacturers must therefore think beyond production output. They need to consider shelf life, storage conditions, user safety, label readability, lot traceability, and transport robustness. They also need systems that can respond quickly to raw material changes, energy costs, labor shortages, and shifts in healthcare policy. In practice, peritoneal dialysis manufacturing challenges connect directly to public health, healthcare access, and continuity of treatment.
From an engineering perspective, the work starts with plant architecture: material flow, people flow, pressure cascade, cleanroom zoning, CIP/SIP strategy where relevant, and utility redundancy. From a business perspective, it extends to supplier qualification, contract structure, documentation readiness, and after-sales technical support. Companies that underestimate these links often face avoidable delays and cost overruns.
Peritoneal dialysis manufacturing supports two major treatment environments in the United States: home therapy and institutional care. In home treatment, reliable dialysis fluid supply gives patients greater schedule flexibility and may reduce frequent travel to dialysis centers. In hospitals and specialty clinics, well-manufactured peritoneal dialysis solutions support acute and chronic treatment protocols with dependable quality.
The biggest benefit of advanced production systems is consistency. Automated solution preparation and filling help reduce human error, improve batch repeatability, and support traceable documentation. A second benefit is sterility assurance. High-performance cleanroom design, closed transfer concepts, and validated filling technology lower the risk of contamination. A third benefit is scalability. As more providers encourage home-based treatment, manufacturers need lines that can grow without rebuilding the entire factory.
Another practical benefit is packaging flexibility. Different markets and channels may require different bag formats, overwrap solutions, labeling systems, and secondary packaging. Hospitals may prioritize large-volume procurement efficiency, while home-care distribution may emphasize convenience, protection, and serialized traceability. The manufacturing system must support these commercial realities.
Treatment SettingMain Product NeedManufacturing PriorityPackaging FocusDistribution NeedValue CreatedHome dialysisFrequent routine supplyStable high-volume outputLeak-resistant patient-friendly bagsDirect-to-home logisticsImproved treatment continuityHospital inpatient careRapid availabilityShort lead timesStandardized clinical labelingRegional warehouse supportOperational readinessOutpatient clinicReliable replenishmentForecast-driven schedulingDurable transport packagingFrequent delivery cyclesLower stockout riskEmergency reserveSurge inventoryFlexible capacity bufferLonger shelf-life managementStrategic stock positioningResilienceSpecialty provider networkMulti-site coordinationTraceability and lot controlStandardized SKU structureHub-and-spoke shippingNetwork efficiencyGovernment or large tendersCompliance and scaleValidated systems and audit readinessContract-specific formatsNational coverageCompetitive advantageThis comparison shows why manufacturers cannot optimize only for a single channel. Home and hospital dialysis treatment have overlapping quality needs but different operational demands. The more flexible the line design, the easier it is to serve both segments.
Peritoneal dialysis manufacturing systems vary by container format, automation level, production speed, utility configuration, and integration depth. Common technical choices include non-PVC soft bag lines, PP bottle systems, mixing and solution distribution skids, sterilization strategies, automated inspection, and intelligent end-of-line packaging.
For many manufacturers, soft-bag systems are attractive because they align well with handling efficiency, storage density, and transport practicality. However, bag material selection, port design, and sealing consistency become critical. PP bottle systems may offer different handling and market-positioning advantages, especially depending on user preference or local procurement standards. The “best” model depends on product portfolio, batch size, target channel, regulatory pathway, and CAPEX tolerance.
A modern line also includes the utility backbone: purified water systems, clean steam or purified steam where required, solution preparation units, distribution loops, CIP strategy, environmental monitoring, and automation software. Vision inspection, leak testing, checkweighing, and serialization may be integrated depending on the commercial model and compliance needs.
System TypeTypical UseMain StrengthMain LimitationBest FitInvestment LevelSoft bag production lineHigh-volume PD solutionTransport and storage efficiencySeal integrity control requiredHome-care focused supplyMedium to highPP bottle lineRigid container productsStrong physical protectionHigher logistics volumeMixed institutional channelsMedium to highSemi-automatic lineSmaller output or pilot scaleLower initial CAPEXHigher labor dependencyNew market entryLowerFully automatic lineLarge commercial productionRepeatability and throughputHigher validation scopeEstablished manufacturersHighIntegrated turnkey plantGreenfield projectsProcess coordinationLonger project planningStrategic expansionHighModular expansion linePhased capacity growthScalable deploymentRequires future layout planningGrowing regional suppliersMediumFor buyers that prefer integrated engineering, turnkey delivery can reduce interface risk between utilities, process equipment, cleanroom systems, and packaging. Companies exploring this route often review turnkey pharmaceutical engineering solutions to assess how a single partner can simplify layout, procurement, installation, and validation.
On the technology side, some international engineering companies active in this space are known for combining fluid preparation, filling, packaging, and utility systems under one project structure. In practice, that technological capability matters because dialysis solution manufacturing is highly interconnected: if the water treatment system, solution preparation skid, and filling line are designed in isolation, performance gaps can appear later during qualification or commercial operation.
When investors and manufacturers compare peritoneal dialysis manufacturing options, they are often deciding among internal production, contract manufacturing, imported finished product, or hybrid models. They may also compare packaging technologies, sterilization concepts, automation levels, and factory footprints. The right choice depends on control priorities, speed to market, budget, and strategic risk tolerance.
Internal production offers the highest degree of process control and long-term margin potential, but it requires substantial capital, engineering discipline, and regulatory readiness. Contract manufacturing may lower initial CAPEX, though it can reduce flexibility and create dependency on external capacity. Importing finished product can support fast market entry, yet shipping costs, lead times, and geopolitical risk may weaken resilience. Hybrid models are increasingly attractive in the United States, especially when firms want early commercial access while building domestic capacity.
Alternative technologies may also differ in the way they address sterility assurance and throughput. A compact line may suit niche production, but large national contracts often require multi-line redundancy and integrated warehousing. Facilities located near Memphis, Atlanta, or Columbus may favor logistics speed, while coastal facilities may optimize import/export access through major ports.
OptionSpeed to MarketCAPEX NeedQuality ControlSupply ResilienceTypical UserIn-house manufacturingModerateHighHighestHigh with redundancyStrategic long-term producerContract manufacturingFastLow to mediumShared oversightDepends on partnerBrand owner without plantImported finished productFastLowExternal source dependentLower during disruptionsMarket tester or distributorHybrid build-and-buyFast initiallyMedium to highImproves over timeBalancedScaling entrantSemi-automatic domestic lineModerateMediumGood with trainingModerateRegional producerFull turnkey domestic plantSlower start, stronger long termHighHigh and integratedHighNational supplierThe table makes one point clear: there is no universal winner. Companies must align production technology with their commercial goals, regulatory timeline, and market coverage plan. In the U.S. market, where healthcare buyers increasingly examine reliability and compliance history, high-quality domestic manufacturing capacity can be a strong differentiator.
var ctxComp = document.getElementById(‘comparisonChartPD’).getContext(‘2d’);var comparisonChartPD = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘In-house plant’, ‘Contract manufacturing’, ‘Imported product’, ‘Hybrid model’, ‘Turnkey line’, ‘Semi-automatic line’], datasets: [{ label: ‘Overall strategic fit score’, data: [92, 74, 61, 84, 89, 68], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The U.S. market for peritoneal dialysis solutions is influenced by chronic kidney disease prevalence, reimbursement changes, home-care adoption, supply chain localization, and hospital purchasing priorities. One major trend is the continued interest in home-based therapies. This drives demand for stable production capacity, reliable distribution networks, and user-centered packaging formats.
Another trend is domestic resilience. After repeated global supply disruptions, many healthcare companies are reassessing how much dependence they should place on distant sourcing. U.S.-based or U.S.-supported production capacity is therefore becoming more attractive, especially for products tied closely to essential patient treatment.
Technology is also moving forward. By 2026, more peritoneal dialysis production projects are expected to include digital batch records, smarter SCADA/MES integration, predictive maintenance, energy optimization, and stronger electronic traceability. Sustainability is rising as well. Manufacturers increasingly evaluate water recovery, heat efficiency, packaging material reduction, and lower-waste line configurations.
var ctxLine = document.getElementById(‘lineChartPD’).getContext(‘2d’);var lineChartPD = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. PD manufacturing demand index’, data: [100, 108, 117, 129, 141, 156], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});var ctxBar = document.getElementById(‘barChartPD’).getContext(‘2d’);var barChartPD = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Home care’, ‘Hospitals’, ‘Outpatient clinics’, ‘Government stock’, ‘Regional distributors’, ‘Specialty providers’], datasets: [{ label: ‘Estimated 2026 demand contribution (%)’, data: [34, 24, 16, 8, 10, 8], backgroundColor: [‘#2f5597′,’#c55a11′,’#70ad47′,’#7f6000′,’#5b9bd5′,’#a64d79’] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 40 } } }});var ctxArea = document.getElementById(‘areaChartPD’).getContext(‘2d’);var areaChartPD = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of home-focused production planning’, data: [42, 45, 49, 54, 58, 63], fill: true, backgroundColor: ‘rgba(153, 201, 69, 0.25)’, borderColor: ‘rgba(153, 201, 69, 1)’, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 70 } } }});These trend indicators suggest that capacity planning should not focus only on current contracts. Manufacturers entering the U.S. market should model future demand growth, regional distribution complexity, and policy incentives connected to home dialysis support. Plants designed only for today’s baseline may become constrained faster than expected.
Choosing a supplier for peritoneal dialysis manufacturing equipment or an engineering partner for a full project requires a broader evaluation than standard machinery purchasing. The right partner should understand sterile pharmaceutical production, fluid systems, utility integration, compliance documentation, and long-term service support.
Buyers in the United States should ask detailed questions about FAT/SAT protocols, validation documentation, material standards, automation architecture, spare parts availability, and previous international project execution. It is also worth evaluating whether the supplier can support both equipment delivery and plant-level integration. Gaps between vendors are a common source of commissioning delays.
A reliable partner should demonstrate three areas of strength. First is technological capability: experience with solution preparation, filling and sealing, pharmaceutical water treatment, and automated inspection. Second is manufacturing capability: stable fabrication quality, stainless steel workmanship, repeatable assembly standards, and proven production capacity. Third is service capability: feasibility consulting, engineering design, installation, commissioning, training, and lifecycle support.
Some global suppliers have built their reputation by offering integrated engineering rather than isolated machines. For instance, IVEN Pharmatech Engineering has positioned itself as a pharmaceutical engineering partner with experience in dialysis solution lines, pharmaceutical water treatment, and related turnkey systems. Buyers evaluating suppliers can review the company background and engineering scope to understand whether the supplier’s profile matches a project that requires compliance-driven integration.
Supplier Evaluation FactorWhat to CheckWhy It MattersGood SignWarning SignDecision WeightRegulatory familiarityFDA, cGMP, EU GMP alignmentReduces compliance gapsStructured validation packageGeneric paperwork onlyVery highTechnical integrationUtilities, process, packaging linkAvoids interface failuresSingle-point engineering ownershipMany unmanaged subcontractorsHighProject referencesComparable sterile fluid projectsShows execution historyCross-border installationsNo relevant referencesHighManufacturing qualityFabrication standardsImproves equipment lifeRobust stainless constructionInconsistent finishingHighService supportCommissioning and trainingSpeeds startupLifecycle assistanceShip-and-leave modelVery highSpare parts and responseLead times and local supportLimits downtimeClear service planUncertain inventoryMedium to highIn supplier selection, buyers should also compare available product portfolios. A broader portfolio often indicates better systems thinking, especially when dialysis production requires linked water, preparation, filling, packaging, and logistics solutions. Reviewing available pharmaceutical equipment categories can help determine whether a supplier is capable of supporting future expansion beyond one single line.
Investment in peritoneal dialysis manufacturing can vary significantly depending on capacity, automation level, container format, cleanroom scope, utility design, land cost, and validation requirements. A small or phased project may begin with a narrower line and limited warehouse integration, while a national-scale facility may require a full turnkey plant with multiple filling streams, advanced utilities, and automated logistics.
Budget planning should divide cost into six major blocks: facility and cleanrooms, utilities, process equipment, packaging equipment, qualification/validation, and working capital. Too many projects underestimate the last two. Validation, training, documentation, and startup waste can materially affect cash needs during the ramp-up period.
ROI depends on output utilization, yield, labor efficiency, maintenance strategy, and contract stability. For a U.S. facility, local manufacturing may improve gross margin through freight reduction and higher service reliability, but only if line utilization reaches a sustainable threshold. Buyers should also model energy pricing, water consumption, spare parts, and planned expansion.
Cost CategoryLow Complexity ProjectMid-Scale ProjectLarge Integrated ProjectMain Cost DriverROI ImpactFacility and cleanroomsModerateHighVery highClassification and footprintLong-term fixed costWater and utilitiesModerateHighVery highPurification and redundancyDirect quality effectSolution prep and filling lineHighVery highVery highAutomation and speedCore revenue driverPackaging and inspectionMediumHighHighSerialization and QC scopeYield and release speedValidation and documentationMediumMediumHighRegulatory readinessTime to commercial outputWorking capitalMediumHighHighInventory and launch rampCash flow stabilityAs a simple framework, many investors target payback by balancing high utilization with controlled waste and downtime. If a plant can secure strong regional demand from the Northeast, Midwest, and Sun Belt markets while maintaining dependable quality release cycles, ROI improves materially. This is why equipment durability and lifecycle support matter. Some engineering providers emphasize long service life, integrated project delivery, and cost-effective system design to reduce total ownership cost rather than just purchase price.
For prospective buyers, a direct discussion with an engineering team can clarify realistic budgeting. Companies evaluating new lines or plant expansion can contact a pharmaceutical engineering specialist for technical and commercial scoping based on required output, utility conditions, and compliance targets.
The first major investment risk is underestimating compliance complexity. A line may look mechanically complete yet still be far from validation-ready. The second risk is poor layout logic. If material flow, personnel flow, cleaning flow, and warehouse flow are not planned properly, efficiency and contamination control suffer. The third risk is fragmented procurement. Multiple vendors without a clear integration leader often create handoff failures during startup.
Other risks include insufficient utility redundancy, inaccurate forecasting, overbuilt capacity, weak operator training, and poor maintenance planning. In the U.S. market, investors should also consider energy cost variability, labor availability, state-level permitting, and transport economics. A facility near Houston may have strong port access, while one in the Mid-Atlantic may benefit from proximity to dense healthcare corridors. But site selection must also account for water quality, local technical labor, and logistics performance.
Looking toward 2026, investors should prioritize digitalization and sustainability from the beginning. Plants that add smart monitoring later often spend more than those that design it in early. Similarly, sustainability is no longer just a branding issue. Water reuse, utility efficiency, packaging optimization, and reduced waste disposal can affect operating margins and procurement preference.
From a manufacturing capability perspective, supplier selection should include evidence of repeatable fabrication quality and proven capacity to deliver sterile-process equipment at scale. From a service capability perspective, buyers should seek partners that support feasibility, design, installation, commissioning, validation, and training instead of stopping at delivery. These factors reduce the chance of schedule slippage and help stabilize the first commercial batches.
A practical U.S. case pattern is a company that initially imports or uses contract manufacturing, then moves toward a domestic facility when demand justifies local output. Another pattern is a greenfield project near major logistics infrastructure, where the plant integrates automated warehouse systems and phased line expansion. Both models can work, but only when project governance is disciplined and technical scope is realistic.
For companies wanting an integrated approach, the most useful partner is often one with engineering breadth across pharmaceutical fluids, water systems, packaging, and plant services. That broad capability can reduce risk during design review, FAT, SAT, and qualification, especially for projects that need to move efficiently from concept to commercial readiness in the United States.
What is the biggest challenge in peritoneal dialysis manufacturing?The biggest challenge is maintaining sterile, consistent, fully compliant production at scale. This requires control of water quality, formulation, filling environment, packaging integrity, and documentation.
Why is domestic U.S. production becoming more important?Domestic production can improve supply resilience, shorten lead times, reduce some logistics risk, and support healthcare buyers that value stable access to essential kidney care products.
Which packaging format is better for peritoneal dialysis solutions?There is no single answer. Soft bags are often favored for logistics and home-care convenience, while rigid formats may be selected for specific operational or market reasons. The right choice depends on product strategy and channel needs.
How long does a new manufacturing project usually take?A greenfield or large-scale integrated project can take significantly longer than a line addition because it includes facility buildout, utilities, commissioning, validation, and training. Timeline depends on scope, supplier coordination, and regulatory readiness.
What should I ask an equipment supplier first?Ask about similar project references, compliance support, utility integration, validation documents, lead times, spare parts service, and the supplier’s ability to support the entire lifecycle of the line.
Can a turnkey approach reduce project risk?Yes, in many cases. A turnkey model can reduce coordination gaps between process equipment, utilities, cleanrooms, packaging, and validation activities, especially when one engineering partner manages interfaces clearly.
How does IVEN fit into this market?IVEN is known in pharmaceutical engineering for integrated solutions that cover sterile fluid production lines, water treatment, packaging, logistics, and turnkey support. For U.S.-focused buyers, its relevance lies in combined technological capability, manufacturing depth, and lifecycle service support rather than just stand-alone machinery.
What 2026 trends should investors watch?Key trends include more home-dialysis-driven demand, digital batch and traceability systems, predictive maintenance, utility efficiency, sustainable packaging choices, and stronger localization of critical medical supply manufacturing.
In summary, peritoneal dialysis manufacturing challenges in the United States are best understood as a combination of technical rigor, compliance discipline, scalable plant design, and supply-chain strategy. Companies that invest with a long-term view, choose partners carefully, and integrate engineering with market planning are better positioned to deliver safe dialysis solutions for the growing kidney care market.