Peritoneal Dialysis Manufacturing Challenges in the United States
Peritoneal dialysis solution manufacturing is essential to safe kidney care because it enables the reliable production of sterile, stable, accurately formulated dialysis fluids used in both home-based and hospital treatment. In the United States, manufacturers must balance aseptic control, FDA cGMP compliance, packaging integrity, logistics resilience, and production scalability while supporting growing demand from chronic kidney disease patients. When these manufacturing challenges are handled well, providers can deliver dependable peritoneal dialysis therapy with consistent quality, lower contamination risk, and better continuity of care.
Across the U.S. healthcare system, demand for home dialysis has increased as providers seek patient-centered treatment models that reduce hospital dependence. That shift has put more attention on the manufacturing side of peritoneal dialysis fluids: clean utility systems, automated mixing and filling, container material selection, validation, environmental monitoring, and end-to-end traceability. For investors, plant owners, EPC teams, and medical solution manufacturers, understanding the technical and commercial realities of peritoneal dialysis manufacturing challenges is now a strategic issue rather than a narrow production topic.
In major healthcare and logistics corridors such as New Jersey, Texas, California, Illinois, and Georgia, the supply chain for dialysis products depends on resilient access to pharmaceutical-grade raw materials, ports, warehousing, and qualified engineering services. Facilities near trade gateways such as the Port of Los Angeles, Port of Long Beach, Port of Houston, Savannah, and Newark can often strengthen inbound and outbound logistics, but geographic advantages alone are not enough. Success depends on how well the plant is designed, validated, and operated.
Quick Answer: How peritoneal dialysis manufacturing challenges affect safe supply

The core challenge in peritoneal dialysis manufacturing is producing large volumes of sterile dialysis solution with exact electrolyte balance, glucose concentration control, low endotoxin risk, and packaging durability suitable for storage, shipping, and clinical use. Because these solutions go directly into patient therapy, even small deviations in formulation, particulate control, seal integrity, or bioburden can create serious quality and safety risks.
For U.S. manufacturers, the most critical issues usually include water quality management, solution preparation accuracy, aseptic filling, container-closure integrity, line clearance, cleaning validation, regulatory documentation, and capacity planning. These factors directly affect whether a facility can supply clinics and home dialysis programs without interruption. A strong manufacturing platform helps companies support chronic kidney disease management while improving confidence among providers, purchasing organizations, and regulators.
| Challenge Area | Why It Matters | Typical Risk | Operational Impact | Priority in U.S. Plants | Best Response |
|---|---|---|---|---|---|
| Water for production | Base input for dialysis fluids | Microbial contamination | Batch rejection | Very high | Validated PW/WFI-related systems as required by process design |
| Formulation accuracy | Patient safety and efficacy | Concentration deviation | Rework or waste | Very high | Automated dosing and recipe control |
| Aseptic filling | Maintains sterility | Environmental contamination | Recall exposure | Very high | Isolator/RABS and strict EM programs |
| Packaging integrity | Prevents leaks and contamination | Seal failure in transport | Customer complaints | High | CCIT and transport simulation testing |
| Regulatory compliance | Market access | 483 observations or delays | Approval interruption | Very high | Strong QA, validation, and documentation |
| Capacity planning | Supports continuity of supply | Stockouts | Lost contracts | High | Modular line design and demand forecasting |
The table above shows that peritoneal dialysis manufacturing challenges are not limited to one machine or one production step. They span utilities, processing, quality systems, packaging, and distribution. Companies that address these elements together typically achieve better output stability and stronger long-term returns.
What peritoneal dialysis manufacturing challenges are and why they matter for kidney care

Peritoneal dialysis solution manufacturing challenges refer to the technical, quality, regulatory, and supply-chain obstacles involved in designing, operating, and scaling facilities that produce dialysis fluids safely and consistently. These challenges matter because peritoneal dialysis is often used repeatedly in home settings, where patients and caregivers depend on ready-to-use, sterile products that perform reliably every day.
Kidney care in the United States is changing. More providers want flexible treatment pathways, especially for patients who benefit from home dialysis. That makes manufacturing quality even more important. Unlike a product used once in a controlled operating room, peritoneal dialysis fluids are part of a recurring care routine. Packaging must survive transportation to homes in cities like Chicago, Dallas, Phoenix, and Philadelphia, as well as to rural areas where resupply schedules are less forgiving.
Manufacturers must therefore think beyond production output. They need to consider shelf life, storage conditions, user safety, label readability, lot traceability, and transport robustness. They also need systems that can respond quickly to raw material changes, energy costs, labor shortages, and shifts in healthcare policy. In practice, peritoneal dialysis manufacturing challenges connect directly to public health, healthcare access, and continuity of treatment.
From an engineering perspective, the work starts with plant architecture: material flow, people flow, pressure cascade, cleanroom zoning, CIP/SIP strategy where relevant, and utility redundancy. From a business perspective, it extends to supplier qualification, contract structure, documentation readiness, and after-sales technical support. Companies that underestimate these links often face avoidable delays and cost overruns.
Role and benefits of peritoneal dialysis manufacturing in home and hospital treatment

Peritoneal dialysis manufacturing supports two major treatment environments in the United States: home therapy and institutional care. In home treatment, reliable dialysis fluid supply gives patients greater schedule flexibility and may reduce frequent travel to dialysis centers. In hospitals and specialty clinics, well-manufactured peritoneal dialysis solutions support acute and chronic treatment protocols with dependable quality.
The biggest benefit of advanced production systems is consistency. Automated solution preparation and filling help reduce human error, improve batch repeatability, and support traceable documentation. A second benefit is sterility assurance. High-performance cleanroom design, closed transfer concepts, and validated filling technology lower the risk of contamination. A third benefit is scalability. As more providers encourage home-based treatment, manufacturers need lines that can grow without rebuilding the entire factory.
Another practical benefit is packaging flexibility. Different markets and channels may require different bag formats, overwrap solutions, labeling systems, and secondary packaging. Hospitals may prioritize large-volume procurement efficiency, while home-care distribution may emphasize convenience, protection, and serialized traceability. The manufacturing system must support these commercial realities.
| Treatment Setting | Main Product Need | Manufacturing Priority | Packaging Focus | Distribution Need | Value Created |
|---|---|---|---|---|---|
| Home dialysis | Frequent routine supply | Stable high-volume output | Leak-resistant patient-friendly bags | Direct-to-home logistics | Improved treatment continuity |
| Hospital inpatient care | Rapid availability | Short lead times | Standardized clinical labeling | Regional warehouse support | Operational readiness |
| Outpatient clinic | Reliable replenishment | Forecast-driven scheduling | Durable transport packaging | Frequent delivery cycles | Lower stockout risk |
| Emergency reserve | Surge inventory | Flexible capacity buffer | Longer shelf-life management | Strategic stock positioning | Resilience |
| Specialty provider network | Multi-site coordination | Traceability and lot control | Standardized SKU structure | Hub-and-spoke shipping | Network efficiency |
| Government or large tenders | Compliance and scale | Validated systems and audit readiness | Contract-specific formats | National coverage | Competitive advantage |
This comparison shows why manufacturers cannot optimize only for a single channel. Home and hospital dialysis treatment have overlapping quality needs but different operational demands. The more flexible the line design, the easier it is to serve both segments.
Key types, models, and technical options for peritoneal dialysis manufacturing
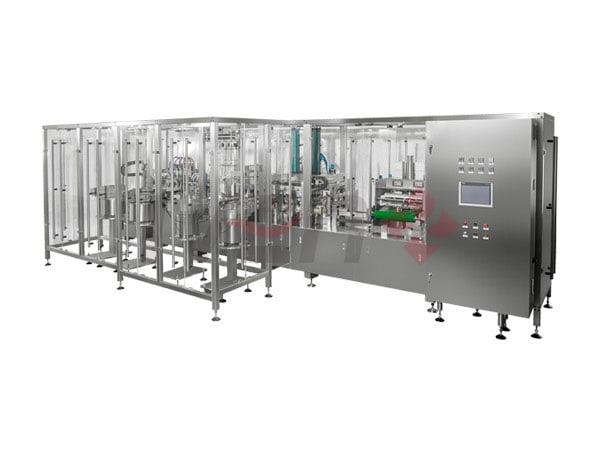
Peritoneal dialysis manufacturing systems vary by container format, automation level, production speed, utility configuration, and integration depth. Common technical choices include non-PVC soft bag lines, PP bottle systems, mixing and solution distribution skids, sterilization strategies, automated inspection, and intelligent end-of-line packaging.
For many manufacturers, soft-bag systems are attractive because they align well with handling efficiency, storage density, and transport practicality. However, bag material selection, port design, and sealing consistency become critical. PP bottle systems may offer different handling and market-positioning advantages, especially depending on user preference or local procurement standards. The “best” model depends on product portfolio, batch size, target channel, regulatory pathway, and CAPEX tolerance.
A modern line also includes the utility backbone: purified water systems, clean steam or purified steam where required, solution preparation units, distribution loops, CIP strategy, environmental monitoring, and automation software. Vision inspection, leak testing, checkweighing, and serialization may be integrated depending on the commercial model and compliance needs.
| System Type | Typical Use | Main Strength | Main Limitation | Best Fit | Investment Level |
|---|---|---|---|---|---|
| Soft bag production line | High-volume PD solution | Transport and storage efficiency | Seal integrity control required | Home-care focused supply | Medium to high |
| PP bottle line | Rigid container products | Strong physical protection | Higher logistics volume | Mixed institutional channels | Medium to high |
| Semi-automatic line | Smaller output or pilot scale | Lower initial CAPEX | Higher labor dependency | New market entry | Lower |
| Fully automatic line | Large commercial production | Repeatability and throughput | Higher validation scope | Established manufacturers | High |
| Integrated turnkey plant | Greenfield projects | Process coordination | Longer project planning | Strategic expansion | High |
| Modular expansion line | Phased capacity growth | Scalable deployment | Requires future layout planning | Growing regional suppliers | Medium |
For buyers that prefer integrated engineering, turnkey delivery can reduce interface risk between utilities, process equipment, cleanroom systems, and packaging. Companies exploring this route often review turnkey pharmaceutical engineering solutions to assess how a single partner can simplify layout, procurement, installation, and validation.
On the technology side, some international engineering companies active in this space are known for combining fluid preparation, filling, packaging, and utility systems under one project structure. In practice, that technological capability matters because dialysis solution manufacturing is highly interconnected: if the water treatment system, solution preparation skid, and filling line are designed in isolation, performance gaps can appear later during qualification or commercial operation.
Peritoneal dialysis manufacturing versus alternative technologies: which fits your needs?
When investors and manufacturers compare peritoneal dialysis manufacturing options, they are often deciding among internal production, contract manufacturing, imported finished product, or hybrid models. They may also compare packaging technologies, sterilization concepts, automation levels, and factory footprints. The right choice depends on control priorities, speed to market, budget, and strategic risk tolerance.
Internal production offers the highest degree of process control and long-term margin potential, but it requires substantial capital, engineering discipline, and regulatory readiness. Contract manufacturing may lower initial CAPEX, though it can reduce flexibility and create dependency on external capacity. Importing finished product can support fast market entry, yet shipping costs, lead times, and geopolitical risk may weaken resilience. Hybrid models are increasingly attractive in the United States, especially when firms want early commercial access while building domestic capacity.
Alternative technologies may also differ in the way they address sterility assurance and throughput. A compact line may suit niche production, but large national contracts often require multi-line redundancy and integrated warehousing. Facilities located near Memphis, Atlanta, or Columbus may favor logistics speed, while coastal facilities may optimize import/export access through major ports.
| Option | Speed to Market | CAPEX Need | Quality Control | Supply Resilience | Typical User |
|---|---|---|---|---|---|
| In-house manufacturing | Moderate | High | Highest | High with redundancy | Strategic long-term producer |
| Contract manufacturing | Fast | Low to medium | Shared oversight | Depends on partner | Brand owner without plant |
| Imported finished product | Fast | Low | External source dependent | Lower during disruptions | Market tester or distributor |
| Hybrid build-and-buy | Fast initially | Medium to high | Improves over time | Balanced | Scaling entrant |
| Semi-automatic domestic line | Moderate | Medium | Good with training | Moderate | Regional producer |
| Full turnkey domestic plant | Slower start, stronger long term | High | High and integrated | High | National supplier |
The table makes one point clear: there is no universal winner. Companies must align production technology with their commercial goals, regulatory timeline, and market coverage plan. In the U.S. market, where healthcare buyers increasingly examine reliability and compliance history, high-quality domestic manufacturing capacity can be a strong differentiator.
Current market trends and demand for peritoneal dialysis production capacity
The U.S. market for peritoneal dialysis solutions is influenced by chronic kidney disease prevalence, reimbursement changes, home-care adoption, supply chain localization, and hospital purchasing priorities. One major trend is the continued interest in home-based therapies. This drives demand for stable production capacity, reliable distribution networks, and user-centered packaging formats.
Another trend is domestic resilience. After repeated global supply disruptions, many healthcare companies are reassessing how much dependence they should place on distant sourcing. U.S.-based or U.S.-supported production capacity is therefore becoming more attractive, especially for products tied closely to essential patient treatment.
Technology is also moving forward. By 2026, more peritoneal dialysis production projects are expected to include digital batch records, smarter SCADA/MES integration, predictive maintenance, energy optimization, and stronger electronic traceability. Sustainability is rising as well. Manufacturers increasingly evaluate water recovery, heat efficiency, packaging material reduction, and lower-waste line configurations.
These trend indicators suggest that capacity planning should not focus only on current contracts. Manufacturers entering the U.S. market should model future demand growth, regional distribution complexity, and policy incentives connected to home dialysis support. Plants designed only for today’s baseline may become constrained faster than expected.
How to choose a reliable peritoneal dialysis manufacturing manufacturer or supplier
Choosing a supplier for peritoneal dialysis manufacturing equipment or an engineering partner for a full project requires a broader evaluation than standard machinery purchasing. The right partner should understand sterile pharmaceutical production, fluid systems, utility integration, compliance documentation, and long-term service support.
Buyers in the United States should ask detailed questions about FAT/SAT protocols, validation documentation, material standards, automation architecture, spare parts availability, and previous international project execution. It is also worth evaluating whether the supplier can support both equipment delivery and plant-level integration. Gaps between vendors are a common source of commissioning delays.
A reliable partner should demonstrate three areas of strength. First is technological capability: experience with solution preparation, filling and sealing, pharmaceutical water treatment, and automated inspection. Second is manufacturing capability: stable fabrication quality, stainless steel workmanship, repeatable assembly standards, and proven production capacity. Third is service capability: feasibility consulting, engineering design, installation, commissioning, training, and lifecycle support.
Some global suppliers have built their reputation by offering integrated engineering rather than isolated machines. For instance, IVEN Pharmatech Engineering has positioned itself as a pharmaceutical engineering partner with experience in dialysis solution lines, pharmaceutical water treatment, and related turnkey systems. Buyers evaluating suppliers can review the company background and engineering scope to understand whether the supplier’s profile matches a project that requires compliance-driven integration.
| Supplier Evaluation Factor | What to Check | Why It Matters | Good Sign | Warning Sign | Decision Weight |
|---|---|---|---|---|---|
| Regulatory familiarity | FDA, cGMP, EU GMP alignment | Reduces compliance gaps | Structured validation package | Generic paperwork only | Very high |
| Technical integration | Utilities, process, packaging link | Avoids interface failures | Single-point engineering ownership | Many unmanaged subcontractors | High |
| Project references | Comparable sterile fluid projects | Shows execution history | Cross-border installations | No relevant references | High |
| Manufacturing quality | Fabrication standards | Improves equipment life | Robust stainless construction | Inconsistent finishing | High |
| Service support | Commissioning and training | Speeds startup | Lifecycle assistance | Ship-and-leave model | Very high |
| Spare parts and response | Lead times and local support | Limits downtime | Clear service plan | Uncertain inventory | Medium to high |
In supplier selection, buyers should also compare available product portfolios. A broader portfolio often indicates better systems thinking, especially when dialysis production requires linked water, preparation, filling, packaging, and logistics solutions. Reviewing available pharmaceutical equipment categories can help determine whether a supplier is capable of supporting future expansion beyond one single line.
Investment cost, budget planning, and ROI analysis for peritoneal dialysis manufacturing
Investment in peritoneal dialysis manufacturing can vary significantly depending on capacity, automation level, container format, cleanroom scope, utility design, land cost, and validation requirements. A small or phased project may begin with a narrower line and limited warehouse integration, while a national-scale facility may require a full turnkey plant with multiple filling streams, advanced utilities, and automated logistics.
Budget planning should divide cost into six major blocks: facility and cleanrooms, utilities, process equipment, packaging equipment, qualification/validation, and working capital. Too many projects underestimate the last two. Validation, training, documentation, and startup waste can materially affect cash needs during the ramp-up period.
ROI depends on output utilization, yield, labor efficiency, maintenance strategy, and contract stability. For a U.S. facility, local manufacturing may improve gross margin through freight reduction and higher service reliability, but only if line utilization reaches a sustainable threshold. Buyers should also model energy pricing, water consumption, spare parts, and planned expansion.
| Cost Category | Low Complexity Project | Mid-Scale Project | Large Integrated Project | Main Cost Driver | ROI Impact |
|---|---|---|---|---|---|
| Facility and cleanrooms | Moderate | High | Very high | Classification and footprint | Long-term fixed cost |
| Water and utilities | Moderate | High | Very high | Purification and redundancy | Direct quality effect |
| Solution prep and filling line | High | Very high | Very high | Automation and speed | Core revenue driver |
| Packaging and inspection | Medium | High | High | Serialization and QC scope | Yield and release speed |
| Validation and documentation | Medium | Medium | High | Regulatory readiness | Time to commercial output |
| Working capital | Medium | High | High | Inventory and launch ramp | Cash flow stability |
As a simple framework, many investors target payback by balancing high utilization with controlled waste and downtime. If a plant can secure strong regional demand from the Northeast, Midwest, and Sun Belt markets while maintaining dependable quality release cycles, ROI improves materially. This is why equipment durability and lifecycle support matter. Some engineering providers emphasize long service life, integrated project delivery, and cost-effective system design to reduce total ownership cost rather than just purchase price.
For prospective buyers, a direct discussion with an engineering team can clarify realistic budgeting. Companies evaluating new lines or plant expansion can contact a pharmaceutical engineering specialist for technical and commercial scoping based on required output, utility conditions, and compliance targets.
Key considerations and potential risks when investing in peritoneal dialysis manufacturing
The first major investment risk is underestimating compliance complexity. A line may look mechanically complete yet still be far from validation-ready. The second risk is poor layout logic. If material flow, personnel flow, cleaning flow, and warehouse flow are not planned properly, efficiency and contamination control suffer. The third risk is fragmented procurement. Multiple vendors without a clear integration leader often create handoff failures during startup.
Other risks include insufficient utility redundancy, inaccurate forecasting, overbuilt capacity, weak operator training, and poor maintenance planning. In the U.S. market, investors should also consider energy cost variability, labor availability, state-level permitting, and transport economics. A facility near Houston may have strong port access, while one in the Mid-Atlantic may benefit from proximity to dense healthcare corridors. But site selection must also account for water quality, local technical labor, and logistics performance.
Looking toward 2026, investors should prioritize digitalization and sustainability from the beginning. Plants that add smart monitoring later often spend more than those that design it in early. Similarly, sustainability is no longer just a branding issue. Water reuse, utility efficiency, packaging optimization, and reduced waste disposal can affect operating margins and procurement preference.
From a manufacturing capability perspective, supplier selection should include evidence of repeatable fabrication quality and proven capacity to deliver sterile-process equipment at scale. From a service capability perspective, buyers should seek partners that support feasibility, design, installation, commissioning, validation, and training instead of stopping at delivery. These factors reduce the chance of schedule slippage and help stabilize the first commercial batches.
A practical U.S. case pattern is a company that initially imports or uses contract manufacturing, then moves toward a domestic facility when demand justifies local output. Another pattern is a greenfield project near major logistics infrastructure, where the plant integrates automated warehouse systems and phased line expansion. Both models can work, but only when project governance is disciplined and technical scope is realistic.
For companies wanting an integrated approach, the most useful partner is often one with engineering breadth across pharmaceutical fluids, water systems, packaging, and plant services. That broad capability can reduce risk during design review, FAT, SAT, and qualification, especially for projects that need to move efficiently from concept to commercial readiness in the United States.
FAQ
What is the biggest challenge in peritoneal dialysis manufacturing?
The biggest challenge is maintaining sterile, consistent, fully compliant production at scale. This requires control of water quality, formulation, filling environment, packaging integrity, and documentation.
Why is domestic U.S. production becoming more important?
Domestic production can improve supply resilience, shorten lead times, reduce some logistics risk, and support healthcare buyers that value stable access to essential kidney care products.
Which packaging format is better for peritoneal dialysis solutions?
There is no single answer. Soft bags are often favored for logistics and home-care convenience, while rigid formats may be selected for specific operational or market reasons. The right choice depends on product strategy and channel needs.
How long does a new manufacturing project usually take?
A greenfield or large-scale integrated project can take significantly longer than a line addition because it includes facility buildout, utilities, commissioning, validation, and training. Timeline depends on scope, supplier coordination, and regulatory readiness.
What should I ask an equipment supplier first?
Ask about similar project references, compliance support, utility integration, validation documents, lead times, spare parts service, and the supplier’s ability to support the entire lifecycle of the line.
Can a turnkey approach reduce project risk?
Yes, in many cases. A turnkey model can reduce coordination gaps between process equipment, utilities, cleanrooms, packaging, and validation activities, especially when one engineering partner manages interfaces clearly.
How does IVEN fit into this market?
IVEN is known in pharmaceutical engineering for integrated solutions that cover sterile fluid production lines, water treatment, packaging, logistics, and turnkey support. For U.S.-focused buyers, its relevance lies in combined technological capability, manufacturing depth, and lifecycle service support rather than just stand-alone machinery.
What 2026 trends should investors watch?
Key trends include more home-dialysis-driven demand, digital batch and traceability systems, predictive maintenance, utility efficiency, sustainable packaging choices, and stronger localization of critical medical supply manufacturing.
In summary, peritoneal dialysis manufacturing challenges in the United States are best understood as a combination of technical rigor, compliance discipline, scalable plant design, and supply-chain strategy. Companies that invest with a long-term view, choose partners carefully, and integrate engineering with market planning are better positioned to deliver safe dialysis solutions for the growing kidney care market.
About the Author
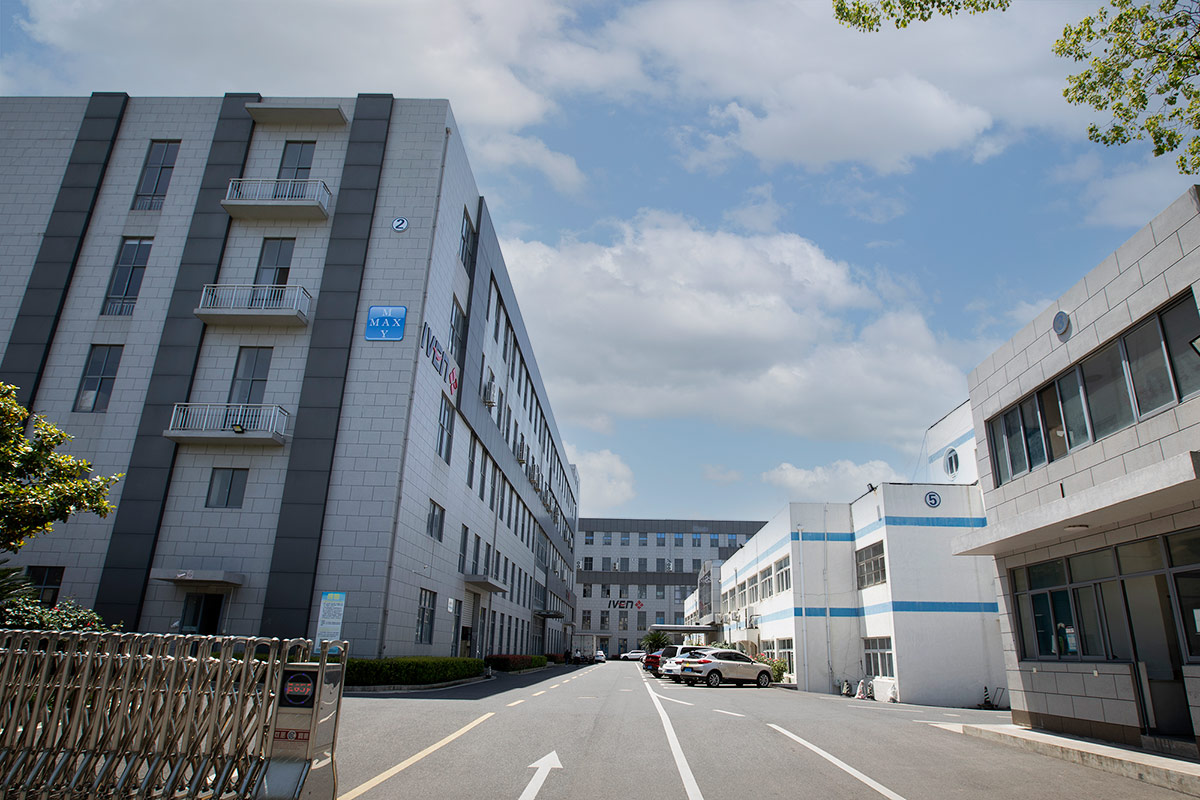
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Coagulation Tube Machines for the United States Market
Hospitals, reference laboratories, and diagnostic networks across the United States rely on stable supplies of coagulation test tubes for PT, APTT, fibrinogen, D-dimer, and related hemostasis assays. For medical device companies serving this demand, a blood collection tube machine for coagulation testing is not simply a packaging asset; it is a controlled production platform that affects product consistency, additive dosing accuracy, labeling compliance, throughput, and total manufacturing cost. In a market shaped by FDA expectations, laboratory accreditation requirements, and hospital purchasing pressure, automated production lines give manufacturers a practical path to higher capacity and lower variability.
From large healthcare hubs such as New York, Boston, Chicago, Houston, Los Angeles, and Atlanta to regional distribution corridors linked to the Ports of Los Angeles, Long Beach, Savannah, Houston, and New York/New Jersey, the U.S. market values dependable lead times and traceable production. Companies that invest in modern tube manufacturing equipment can improve supply resilience, shorten delivery cycles, and support domestic or near-market inventory strategies. Businesses exploring integrated line design, validation planning, or turnkey factory execution can also review broader engineering capabilities through turnkey pharmaceutical and medical device project solutions.
A blood collection tube machine for coagulation testing enables medical device manufacturers to produce high volumes of sodium citrate blood collection tubes with reliable automation, precise additive filling, controlled drying or coating processes where applicable, secure stoppering, vacuum control, labeling, inspection, and packaging. In practical terms, it helps companies deliver uniform tube quality to hospitals and diagnostic laboratories while reducing labor dependence and batch-to-batch variation.
For the U.S. market, this matters because coagulation tubes must support exact blood-to-additive ratios. Even small inconsistencies can affect test integrity, specimen acceptability, and laboratory confidence. Automated lines are designed to keep dosing, assembly, and inspection within validated ranges, helping manufacturers meet customer expectations for dimensional accuracy, closure integrity, lot traceability, and particulate control.
For buyers, the real value can be summarized in five points:
In the United States, suppliers that can prove process capability, installation support, validation readiness, and long equipment life are often favored by manufacturers supplying integrated delivery networks, government health systems, and large lab chains.
A blood collection tube machine for coagulation testing is a specialized automated production line used to manufacture vacuum blood collection tubes intended for coagulation assays. These tubes are commonly identified by their light blue closure and typically contain buffered sodium citrate anticoagulant. The machine line usually integrates multiple stations into a synchronized manufacturing process.
A typical workflow includes tube feeding, tube orientation, additive preparation, precise liquid filling, drying or post-filling conditioning depending on formulation requirements, stopper feeding, vacuum generation, cap assembly, labeling, printing, vision inspection, leak checking, packing, and batch data recording. In advanced configurations, line software can connect with MES or plant-level quality systems for electronic records and statistical process monitoring.
The most important process control points usually include:
Modern lines may use servo-driven indexing, peristaltic or ceramic pump filling systems, vacuum chambers, automated cap sorting, CCD vision inspection, and reject stations for nonconforming units. Manufacturers serving the United States often request audit-friendly design features such as stainless-steel contact surfaces, batch reporting, alarm history, user access control, and easier IQ/OQ/PQ preparation.
To illustrate the process logic, the table below summarizes common modules found on coagulation tube production lines and why each matters.
Production ModulePrimary FunctionQuality ImpactCommon Automation LevelTypical U.S. Buyer ConcernNotesTube FeedingSupplies empty PET or glass tubes to the linePrevents jams and misalignmentAutomaticLine uptimeOften includes unscrambling and orientationAdditive FillingDispenses sodium citrate solutionControls blood-to-additive ratioHigh precisionDosing accuracyCritical for coagulation test reliabilityDrying or ConditioningStabilizes filled tubes where process requires itSupports product consistencySemi or fully automaticFormulation compatibilityDepends on tube chemistry designStoppering and CappingApplies closures and cap assembliesAffects seal integrityAutomaticClosure fit and leakageOften linked with stopper detection sensorsVacuumingCreates target vacuum volumeEnsures correct blood drawAutomatic chamber controlDraw-volume consistencyOne of the most audited process stepsInspection and PackagingChecks defects and prepares shipmentReduces field complaintsAutomatic vision and packingTraceability and final yieldCan include barcode verificationThe key takeaway is that a coagulation tube line is not a single machine but a coordinated production system. The more mature the line integration, the easier it becomes to maintain repeatability, document performance, and support customer audits.
The main application of this equipment is the production of coagulation blood collection tubes used by hospital laboratories, independent reference labs, emergency departments, oncology centers, surgical departments, dialysis centers, and blood management programs. Yet its business impact extends beyond product output. It influences production planning, compliance confidence, and operating margin.
In the United States, demand comes from a wide range of end users. Large academic medical centers in Boston and Philadelphia often require dependable premium quality and documentation depth. High-throughput lab systems in Chicago, Dallas, and Phoenix prioritize volume reliability and barcode quality. Regional distributors serving clinics and ambulatory centers look for cost stability and short replenishment cycles.
Benefits for medical device companies include:
Many companies also use automation to broaden their product portfolio. Once they establish stable manufacturing for coagulation tubes, they can consider adjacent vacuum blood collection products for serum, glucose, ESR, or other applications, depending on line compatibility and strategic expansion plans.
The following table shows where coagulation tube demand typically comes from and what each buyer group values most.
End-Use SectorMain Use CaseTypical Purchase DriverVolume LevelQuality PriorityCommercial OpportunityLarge HospitalsRoutine coagulation panelsReliable supply contractsHighHighLong-term tendersReference LaboratoriesCentralized hemostasis testingBarcode and specimen consistencyVery highVery highNational accountsEmergency DepartmentsRapid clotting assessmentFast replenishmentMediumHighRegional distributionOutpatient ClinicsRoutine blood drawsCost-effective packsMediumMediumDistributor channel salesSurgery CentersPre-op and post-op testingSmall lot reliabilityLow to mediumHighNiche premium supplyGovernment and VA SystemsStandardized diagnosticsCompliance and continuityHighHighStructured procurement programsThis demand diversity is why machine flexibility matters. A supplier should not only provide output speed but also support size changes, closure changes, packaging changes, and documentation discipline suited to different customer segments.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Large Hospitals’, ‘Reference Labs’, ‘Outpatient Clinics’, ‘Emergency Departments’, ‘Surgery Centers’, ‘Government Systems’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [88, 95, 62, 71, 44, 67], backgroundColor: [‘rgb(54, 162, 235)’,’rgb(75, 192, 192)’,’rgb(255, 206, 86)’,’rgb(255, 159, 64)’,’rgb(153, 102, 255)’,’rgb(201, 203, 207)’] }] }, options: { responsive: true, maintainAspectRatio: false }});Not every manufacturer needs the same line design. The ideal configuration depends on output target, tube material, additive chemistry, floor space, labor availability, packaging style, and validation expectations. In the current market, machine options range from compact semi-automatic units to highly integrated fully automatic systems.
Common configurations include stand-alone filling equipment, modular vacuum tube assembly lines, and complete end-to-end production platforms with online inspection and packing. Some manufacturers choose a phased investment model, starting with core stations and later adding automation modules as demand grows. Others, especially those serving major U.S. lab networks, prefer a fully integrated line from the beginning to simplify qualification and reduce manual intervention.
The table below compares major machine configurations available today.
Configuration TypeBest ForAutomation LevelOutput PotentialInvestment LevelKey LimitationSemi-Automatic Filling CellPilot or small volume producersLow to mediumLowLowerHigher labor dependenceModular Assembly LineGrowing regional suppliersMediumMediumMediumIntegration may vary by moduleFully Automatic Coagulation Tube LineLarge-scale manufacturersHighHighHighNeeds stronger utility planningIntegrated Line with Vision InspectionPremium regulated productionHighHighHigherMore validation work upfrontMulti-SKU Flexible LineBroad product portfoliosHighMedium to highHigherChangeover discipline requiredTurnkey Smart Factory SolutionNew plants and strategic investorsVery highVery highHighestLonger implementation timelineFor buyers that want deeper engineering integration, equipment should be assessed as part of the full plant workflow, including water systems, logistics, warehousing, cleanroom layout, line clearance strategy, and final packaging flow. This is where experienced engineering partners become valuable.
On the technology side, IVEN Pharmatech Engineering is known in the sector for multi-generation vacuum blood collection tube equipment and for combining machine design with wider pharmaceutical and medical device engineering know-how. Its technological capabilities are especially relevant for buyers that need more than stand-alone machinery and want coordinated process design, automation logic, and quality-oriented line architecture.
Manual or labor-intensive assembly can still work for niche volumes, development projects, or local low-scale production. However, for sustained U.S. demand, the disadvantages quickly become visible: inconsistent dosing, slower cycle times, more handling, higher training burden, and weaker process traceability.
Automated equipment does not just increase speed; it changes the quality system of the product. Sensors, servo controls, recipe management, alarms, and reject mechanisms create a more disciplined process environment. This is particularly important for coagulation tubes, where clinical use depends on accurate additive ratio and dependable vacuum performance.
The following comparison highlights the main operational differences.
CriteriaAutomated Tube MachineManual Assembly LineBusiness ImpactCompliance ImpactBest FitOutput SpeedHigh and stableLow to mediumSupports scaleNeutralMass productionDosing PrecisionRepeatable and controlledOperator dependentLower rejectsHigh importanceRegulated productsLabor RequirementLower per unitHigher per unitLower long-term costNeutralCompetitive manufacturingTraceabilityBetter digital recordsMore manual recordsFaster investigationsImportantAudit-heavy customersConsistencyHigh across batchesVariableProtects brand reputationHigh importanceNational supply chainsScalabilityStrongLimitedSupports growthNeutralGrowing manufacturersFor U.S. operations facing labor shortages in industrial zones near Newark, Memphis, Dallas-Fort Worth, or Inland Empire logistics corridors, automation can also reduce recruitment risk. Fewer manual touchpoints often mean simpler staffing models and more predictable production planning.
That said, automation should be sized properly. Buying a line with excessive complexity for a low-volume business can delay payback. The right answer is not maximum automation at any cost; it is the best-fit automation level for the company’s product mix and market ambitions.
var ctxComp = document.getElementById(‘comparisonFeatureChart’).getContext(‘2d’);var comparisonFeatureChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Output Stability’, ‘Dosing Accuracy’, ‘Traceability’, ‘Labor Efficiency’, ‘Changeover Control’, ‘Final Yield’], datasets: [{ label: ‘Automated Machine Score’, data: [92, 96, 90, 88, 82, 94], backgroundColor: ‘rgb(153, 102, 255)’ },{ label: ‘Manual Line Score’, data: [55, 63, 48, 39, 60, 68], backgroundColor: ‘rgb(255, 159, 64)’ }] }, options: { responsive: true, maintainAspectRatio: false }});The U.S. market outlook remains attractive because coagulation testing continues to be essential across acute care, chronic disease management, surgery, oncology, and emergency medicine. Demand is supported by an aging population, high surgical procedure volumes, broad anticoagulant use, and continued laboratory centralization. As large healthcare systems seek stronger supply security after years of global disruption, equipment that can support efficient domestic or regional manufacturing becomes more valuable.
Opportunities for machine manufacturers include greenfield U.S. plants, contract manufacturing projects, modernization of older lines, and expansion of existing medical consumable factories. There is also room for suppliers that can offer better data integration, reduced energy use, smaller cleanroom footprints, and easier validation packages.
In terms of manufacturing capabilities, IVEN Pharmatech Engineering stands out because it operates multiple specialized manufacturing plants and has extensive experience delivering pharmaceutical and medical device production lines globally. That background matters for U.S. buyers who want proof that the supplier can support consistent fabrication quality, integrated system delivery, and long-life stainless-steel equipment suitable for demanding production environments.
The next table outlines the main growth drivers shaping this market.
Growth DriverDescriptionImpact on Equipment DemandU.S. RelevanceTime HorizonOpportunity TypeHospital Testing VolumeStable demand for coagulation assaysHighVery highShort to long termCapacity expansionSupply Chain LocalizationPreference for regional resilienceHighHighMedium termNew plant investmentLab ConsolidationCentralized testing requires consistent consumablesMedium to highHighLong termStandardized high-volume linesAutomation AdoptionManufacturers reduce labor riskHighHighShort to medium termRetrofit and replacementRegulatory Documentation NeedsBuyers seek audit-ready suppliersMediumVery highOngoingPremium machine segmentSustainability TargetsPressure to reduce waste and energy useMediumGrowing2026 onwardEfficient line redesignvar ctxLine = document.getElementById(‘marketLineChart’).getContext(‘2d’);var marketLineChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Estimated U.S. Market Demand Index’, data: [68, 72, 77, 83, 89, 96, 104], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});Looking ahead to 2026, three trends are especially important. First, smart manufacturing functions such as predictive maintenance, electronic batch data, and machine vision analytics will become more common. Second, policy pressure around quality documentation and resilient supply chains is likely to intensify. Third, sustainability metrics such as compressed air efficiency, packaging optimization, and scrap reduction will become more relevant in capital purchasing decisions.
Selecting the right supplier is often more important than selecting the lowest machine price. In the United States, the most successful equipment projects usually come from suppliers that can combine machine performance with documentation, communication, validation support, and long-term service responsiveness.
Buyers should evaluate six practical dimensions: engineering competence, manufacturing quality, regulatory awareness, installed base, service responsiveness, and total project management strength. It is also wise to ask how the supplier handles FAT protocols, spare parts planning, software backup, recipe control, and operator training.
The table below provides a practical supplier evaluation framework.
Evaluation FactorWhat to CheckWhy It MattersWarning SignPreferred EvidenceBuyer ActionTechnical DesignMachine architecture and core componentsDetermines long-term stabilityGeneric undocumented designLayout drawings and process descriptionsRequest technical reviewRegulatory UnderstandingKnowledge of GMP and U.S. expectationsSupports smoother qualificationWeak documentation languageSample IQ/OQ documentsReview validation packageManufacturing DepthOwn factory and fabrication controlReduces quality riskHeavy outsourcing without controlFactory audit or video auditVerify production capabilityAfter-Sales ServiceTraining, spare parts, remote supportLimits downtimeSlow communicationService workflow examplesCheck response commitmentsProject ExperienceInstalled base in medical and pharma sectorsImproves delivery confidenceFew comparable projectsCase history summariesAsk for referencesCustomization AbilityAdaptation to SKU, layout, and utilitiesPrevents costly compromiseOne-size-fits-all offerCustomized proposal detailsConfirm user requirement fitService capability is where many projects succeed or fail. IVEN has built a reputation around full lifecycle support, including feasibility consultation, engineering design, installation, commissioning, validation assistance, training, and optimization. For U.S. buyers, that service model can be especially useful when launching a new production line under tight timelines or when internal engineering teams are limited. Companies wanting to discuss project scope or after-sales planning can reach out through the U.S.-focused equipment inquiry channel.
Another smart step is to review the supplier’s broader business profile instead of only a product brochure. A company with deep pharmaceutical and medical device roots is often better prepared for documentation discipline, system integration, and customer audits. More background can be found on the company overview page.
Capital planning should include much more than base equipment price. A realistic budget for a coagulation tube production line in the United States may include shipping, customs, utilities, cleanroom adaptation, installation, SAT, validation, operator training, spare parts, format parts, software backup, and first-year maintenance. If the line is part of a new factory, warehousing, water systems, HVAC, logistics, and packaging areas should also be included.
Return on investment usually depends on four variables: annual unit volume, labor savings, reject reduction, and average gross margin per tube. Companies that move from manual or fragmented assembly to an integrated automated line often find that reduced scrap and better uptime contribute almost as much to ROI as labor savings.
The table below shows a simplified budget framework for planning purposes.
Cost ElementTypical Budget ShareWhy It MattersCan It Be Optimized?Common OversightPlanning AdviceCore Machine LineLargest shareMain production assetYesChoosing by price onlyCompare output and quality featuresInstallation and CommissioningMediumDetermines startup speedPartlyUnderbudgeting travel and laborDefine scope earlyValidation SupportMediumRequired for regulated useYesLate document preparationRequest package in proposal stageUtilities and Facility AdaptationMedium to highSupports stable operationYesIgnoring compressed air and HVAC loadsConduct utility mappingSpare Parts and ConsumablesLow to mediumPrevents early downtimeYesNo startup spare kitBuild first-year inventoryTraining and Ramp-UpLow to mediumProtects output during launchYesToo little operator preparationInclude repeated training sessionsAs a rough business example, a manufacturer supplying distributors in California, Texas, and the Midwest may justify investment if automation lifts output enough to support national contracts while keeping defect rates low. A supplier near logistics nodes such as the Port of Houston or rail-connected Chicago can further improve ROI by lowering domestic fulfillment times.
For companies comparing alternatives, it is helpful to request a machine list and project package from qualified suppliers. Buyers can review available equipment categories through the medical and pharmaceutical machinery portfolio and then map the line against their target tube volumes and customer contracts.
Even a strong machine can underperform if the project is poorly planned. The biggest risks usually appear at the interfaces between equipment, process chemistry, facility conditions, operators, and validation.
Before purchase, manufacturers should confirm tube material compatibility, additive stability, stopper design, target vacuum range, packaging specification, and anticipated output by SKU. They should also define user requirement specifications, acceptance criteria, utility conditions, and data expectations. U.S. buyers often benefit from building quality, operations, procurement, and maintenance into the evaluation process from the start.
Common risks include:
The trend shift through 2026 is also worth considering. U.S. buyers increasingly ask about cybersecurity for industrial controls, lower energy consumption, data traceability, and sustainable material handling. Equipment selection should therefore support future upgrades, not only today’s production plan.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Share of Buyers Prioritizing Smart + Sustainable Features’, data: [24, 31, 39, 48, 59, 68], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.25)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});A practical way to reduce risk is to choose a partner that can support not only equipment delivery but also engineering coordination. IVEN’s broader track record in integrated plant execution, logistics systems, water treatment, and medical consumables manufacturing gives buyers access to a wider problem-solving framework than a narrow machine-only vendor typically provides.
1. What additive is commonly used in coagulation blood collection tubes?Most coagulation tubes use sodium citrate anticoagulant, commonly formulated to maintain the required blood-to-additive ratio for clotting studies.
2. Why is automation important for coagulation tube production?Automation improves additive dosing accuracy, vacuum consistency, closure integrity, inspection reliability, and throughput. These factors directly affect laboratory acceptance and customer trust.
3. Can a single machine produce multiple blood collection tube types?Some lines are designed for multiple SKUs, but suitability depends on tube dimensions, closure systems, additive types, and packaging formats. Buyers should confirm changeover capability before ordering.
4. Is a fully automatic line always better than a semi-automatic one?Not always. A fully automatic line is usually best for medium to high volumes, while a semi-automatic configuration may be more economical for pilot production or niche regional demand.
5. What should U.S. buyers ask during supplier qualification?Ask about FAT protocols, validation documents, installed references, service response time, spare parts strategy, software backup, training scope, and long-term upgrade support.
6. How long does it take to implement a coagulation tube production line?Timing varies by customization level, facility readiness, utility setup, shipping route, and validation scope. A full project may take several months from design approval to commercial readiness.
7. What are the main ROI drivers?The strongest drivers are annual production volume, labor reduction, lower reject rates, improved uptime, and the ability to secure larger contracts with hospitals and diagnostic laboratories.
8. Are sustainability features becoming important in 2026?Yes. More buyers are evaluating energy efficiency, compressed air usage, material waste reduction, and smarter process monitoring as part of equipment selection.
9. What role does supplier service play after installation?It is critical. Fast technical support, spare parts availability, training refreshers, and process optimization help protect uptime and maintain quality over the life of the line.
10. Why consider IVEN for the United States market?IVEN combines specialized vacuum blood collection tube equipment with broader pharmaceutical and medical device engineering experience, strong manufacturing depth, and full lifecycle service support. That combination is valuable for U.S. manufacturers seeking not only machinery but also a dependable project partner.
For medical device companies planning entry into the United States coagulation tube market, the most effective strategy is usually to align machine selection with actual market demand, product specifications, compliance needs, and long-term service expectations. When these factors are addressed early, a blood collection tube machine for coagulation testing becomes a strategic manufacturing asset rather than a simple equipment purchase.
-
United States Guide to Multi-Chamber Lipid IV Bags
In the United States, multi-chamber IV bag lipid emulsion systems help pharmaceutical manufacturers produce sterile admixtures that keep unstable ingredients separated until activation, improving shelf life, compatibility control, transport flexibility, and patient safety in hospitals, infusion centers, and nutrition therapy programs.
A multi-chamber IV bag lipid emulsion is a sterile flexible container divided into two or more compartments by peelable or frangible seals. It is designed to keep lipid emulsions, amino acids, dextrose, electrolytes, vitamins, or specialty additives apart until the point of use. In the United States market, these systems are particularly important for parenteral nutrition, critical care, perioperative support, and certain ready-to-mix infusion therapies where formulation stability is a major concern.
Instead of filling all ingredients into one chamber and risking degradation, oxidation, precipitation, or emulsion instability during storage, manufacturers use compartmentalized packaging to preserve sensitive components until clinicians activate the bag. This approach supports longer usable shelf life, cleaner labeling, reduced bedside compounding, and lower contamination risk compared with open mixing processes inside hospital pharmacies.
For drug manufacturers serving healthcare networks in New York, Chicago, Houston, Los Angeles, Boston, and Atlanta, multi-chamber systems also align with broader supply chain priorities: ready-to-use format, reduced preparation time, improved emergency stock readiness, and lower waste. These advantages are increasingly relevant as U.S. hospitals seek standardized sterile products that reduce pharmacy workload and comply with strict aseptic handling expectations.
Companies that want to evaluate integrated line design, engineering support, and compliance planning can review the background of IVEN Pharmatech Engineering as part of their supplier research process for the U.S. market.
A multi-chamber lipid emulsion IV bag combines advanced packaging design with aseptic pharmaceutical processing. The bag is typically formed from high-barrier medical film, then separated into dedicated compartments. One chamber may contain a lipid phase, another amino acid solution, and a third dextrose or electrolyte phase. Before administration, the user breaks the internal seal and mixes the components to create the final infusion.
The main benefit is controlled separation. Lipid emulsions are particularly sensitive to oxygen exposure, temperature variation, droplet stability changes, and chemical interactions with minerals or vitamins. By isolating the ingredients, manufacturers can improve product integrity throughout storage, shipping, and hospital inventory cycles.
In U.S. practice, the strongest advantages include:
These bags are especially relevant when hospitals want safer ready-to-mix nutrition products or emergency stock that can be activated quickly. In areas with large tertiary care networks such as Philadelphia, San Diego, and Dallas, procurement teams often prioritize products that simplify workflow while maintaining cGMP-compliant manufacturing standards.
FeatureMulti-Chamber FunctionWhy It MattersU.S. Hospital ImpactSeparated formulationKeeps incompatible ingredients apartProtects stabilityLess pharmacy manipulationPeelable seal activationAllows mixing before infusionFresh final admixtureFaster preparation at bedsideBarrier film structureLimits oxygen and moisture transferHelps preserve lipid qualitySupports broader distributionReady-to-use formatReduces compounding stepsLowers contamination opportunitiesImproves nursing efficiencyStandardized fill volumesImproves consistencyAccurate product presentationSupports formulary controlFlexible packagingLightweight and shippableLower logistics burdenUseful for large hospital systemsThe table above shows why multi-chamber packaging is more than a container choice. It directly influences stability management, clinical workflow, and national distribution suitability.
Clinical use in the United States centers heavily on parenteral nutrition and specialized infusion support. Neonatal intensive care units, oncology departments, surgical recovery programs, trauma centers, and long-term critical care services all value products that minimize bedside compounding. Multi-chamber bags support this goal by arriving in a controlled, semi-finished format that is activated only when needed.
Hospitals in major healthcare corridors such as Baltimore, Cleveland, Phoenix, and Minneapolis often face staffing constraints in sterile compounding areas. A ready-to-mix multi-chamber bag can reduce manual steps, improve turnaround time, and lower the probability of preparation errors. This is particularly useful during weekends, night shifts, and emergency admissions.
Clinical advantages include reduced handling, more consistent admixture quality, and easier training for nursing or pharmacy staff. For home infusion and transitional care, the format can also support safer administration outside large academic hospitals, provided the formulation and instructions are suitable for the intended care setting.
Application AreaTypical UseWhy Multi-Chamber HelpsOperational BenefitParenteral nutritionLipids, amino acids, dextroseKeeps ingredients stable until activationReduces compounding timeNICU and pediatricsCareful nutrition supportSupports controlled preparationImproves workflow for small-volume critical careICURapid nutritional interventionReady-to-mix product availabilityShortens preparation delaysOncology supportNutrition during intensive treatmentLess manipulation for vulnerable patientsLower contamination exposureHome infusion transitionDischarge support for selected patientsSimple activation protocolBetter continuity of careDisaster and emergency stockPrepared reserve inventoryLonger usable storage structureImproves readiness planningThis table illustrates how production format translates into real care delivery value across hospital and alternate-site settings.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Parenteral Nutrition’, ‘ICU’, ‘Oncology’, ‘Pediatrics’, ‘Home Infusion’, ‘Emergency Stock’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [96, 78, 64, 71, 58, 67], backgroundColor: [‘#4e79a7′,’#59a14f’,’#f28e2b’,’#e15759′,’#76b7b2′,’#af7aa1′] }] }, options: { responsive: true, maintainAspectRatio: false }});Not all multi-chamber systems are identical. U.S. buyers should assess chamber count, seal design, sterilization compatibility, fill volume, and film chemistry before approving a project. Common designs include dual-chamber bags, triple-chamber bags, and custom multi-compartment structures used for more complex formulas. The most frequent pharmaceutical need is the separation of a lipid emulsion from aqueous phases until just before use.
Film selection is equally important. The material must provide suitable oxygen barrier performance, extractables and leachables control, seal integrity, transparency where needed, and compatibility with sterilization processes. In the American market, decision-making usually includes regulatory evaluation, shelf-life validation, and logistics suitability for nationwide temperature-managed distribution through hubs such as Los Angeles/Long Beach, Savannah, Houston, and New Jersey port systems.
Bag TypeTypical ChambersCommon UseKey ConsiderationDual-chamber bag2Separate lipid and aqueous baseSimpler activationTriple-chamber bag3Nutrition formulas with lipid, amino acid, dextroseHigher formulation flexibilityCustom multi-chamber bag3 or moreSpecialty admixture programsComplex validationLarge-volume bag2 or 3Adult clinical useWeight and mixing uniformityMedium-volume bag2 or 3General hospital applicationsEfficient storagePediatric-focused configuration2 or 3Specialized care pathwaysPrecise dose presentationThe table above helps procurement teams compare structural formats based on intended therapy rather than packaging alone.
Film Material OptionMain AdvantagePotential LimitationTypical Evaluation FocusMulti-layer non-PVC filmGood flexibility and broad market acceptanceNeeds full compatibility reviewExtractables, barrier, seal performanceEVA-based structureSoft handling and clarityBarrier level varies by structureStorage and drug compatibilityPP-based co-extruded filmThermal resistance potentialDesign complexity may riseSterilization suitabilityHigh-barrier multilayer filmImproved oxygen protectionHigher material costLipid stability and shelf lifeCustomized laminateTailored performanceLonger qualification timelineApplication-specific validationDEHP-free medical filmMeets sensitive market preferencesMay require supply qualificationRegulatory and purchasing acceptanceFilm choice affects product stability, transport durability, sterilization strategy, and long-term market approval. That is why material qualification should begin early in development.
Many investors and technical teams ask whether a single-chamber bag can still meet demand. The answer depends on the formulation. If ingredients are stable together for the entire shelf life, a single-chamber solution may remain practical. But for lipid-containing admixtures and multi-component nutrition products, multi-chamber packaging often offers a more robust answer to compatibility and storage challenges.
For the U.S. market, the comparison extends beyond product science. It also touches hospital labor, batch release strategy, cold chain exposure risk, and potential recall complexity. Multi-chamber products may cost more to manufacture, but they can offer savings through waste reduction and lower in-hospital preparation burden.
Comparison PointMulti-Chamber BagSingle-Chamber BagStrategic ImpactIngredient separationYesNoCritical for unstable formulasShelf-life flexibilityOften strongerLimited by mixed formula stabilityAffects distribution planningPreparation steps at useActivation then administrationUsually immediate useBoth simple, but multi-chamber reduces external mixingManufacturing complexityHigherLowerInfluences capexHospital compounding demandReducedMay remain higher for complex therapiesLabor savings potentialSuitability for lipid emulsion admixturesStrongLimited when compatibility is weakImportant for nutrition productsThe table highlights that multi-chamber lines make the most sense when formulation stability and workflow simplification justify the added engineering investment.
var ctxComp = document.getElementById(‘comparisonChartUs’).getContext(‘2d’);var comparisonChartUs = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Stability Support’, ‘Workflow Efficiency’, ‘Capex Need’, ‘Hospital Safety Benefit’, ‘Formulation Flexibility’, ‘Distribution Value’], datasets: [ { label: ‘Multi-Chamber’, data: [94, 88, 72, 91, 89, 86], backgroundColor: ‘#4e79a7’ }, { label: ‘Single-Chamber’, data: [61, 69, 48, 66, 55, 63], backgroundColor: ‘#f28e2b’ } ] }, options: { responsive: true, maintainAspectRatio: false }});Demand in the United States is being driven by three converging forces: a continuing focus on sterile ready-to-use products, supply chain resilience after years of healthcare disruption, and rising preference for closed-system preparation models. Large hospital groups, outsourced compounding networks, and nutrition-focused manufacturers are all exploring more scalable delivery formats.
Another trend is domestic and near-market supply planning. U.S. buyers increasingly evaluate how quickly a supplier can support validation, spare parts, technical documentation, and long-term production continuity. Manufacturing programs tied to East Coast and Gulf logistics routes often consider inbound equipment scheduling through New York/New Jersey, Charleston, Houston, or Miami, while West Coast projects may depend on Los Angeles/Long Beach or Oakland entries.
By 2026, the market is expected to place even more emphasis on automated visual inspection, digital batch records, barrier-film sustainability, and lower-energy sterilization strategies. Policy pressure around supply security and quality assurance may further reward manufacturers with stronger engineering controls and regulatory readiness.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Multi-Chamber Capacity Demand Index’, data: [58, 63, 70, 79, 88, 98], borderColor: ‘#59a14f’, backgroundColor: ‘rgba(89,161,79,0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});Market growth is not just volume-based. It also reflects a shift toward higher-quality packaging systems with more advanced automation, validation support, and data traceability.
var ctxArea = document.getElementById(‘areaShiftChart’).getContext(‘2d’);var areaShiftChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of Ready-to-Use and Ready-to-Mix Preference’, data: [41, 46, 52, 59, 65, 72], borderColor: ‘#e15759’, backgroundColor: ‘rgba(225,87,89,0.25)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});Choosing a supplier requires more than comparing machine prices. U.S. pharmaceutical investors should review regulatory understanding, equipment design quality, film and bag handling experience, sterilization knowledge, line integration ability, validation documentation, and after-sales service. A high-output line is only valuable if it consistently meets cGMP expectations and supports successful product registration.
Technological capability is one of the first checkpoints. A qualified engineering partner should understand chamber-forming precision, liquid preparation systems, aseptic filling, seal integrity verification, leak testing, automated conveying, and line data integration. Some suppliers can also support upstream purified water and water for injection systems, which improves project coordination. Businesses comparing turnkey paths can explore integrated pharmaceutical turnkey solutions to understand how equipment, utilities, and facility engineering can be aligned from the beginning.
Manufacturing capability matters as much as design. Buyers should ask whether the supplier has dedicated production plants for filling and packaging machinery, water treatment systems, logistics systems, and related medical packaging equipment. A company with multi-plant specialization is often better positioned to control lead time and component quality. This is relevant for American buyers facing project schedules tied to financing windows, construction milestones, or launch commitments.
Service capability should be evaluated in detail. Strong partners provide feasibility input, engineering design, factory acceptance testing, installation, commissioning, IQ/OQ/PQ support, operator training, spare parts planning, and long-term technical assistance. U.S. teams should also ask about English-language documentation, remote service response, and local coordination methods.
Supplier Evaluation PointWhat to CheckWhy It Matters in the U.S.Priority LevelRegulatory understandingEU GMP, U.S. FDA cGMP, WHO/PIC/S awarenessSupports validation and audit readinessVery highEngineering depthBag forming, filling, sealing, utilities integrationReduces project interface riskVery highManufacturing baseDedicated plants and stable production systemsImproves delivery confidenceHighDocumentation supportDQ/IQ/OQ/PQ materials and manualsSpeeds qualificationHighAfter-sales responseTraining, parts, remote diagnosticsCritical after startupHighReference experienceInstalled lines and turnkey projectsShows execution capabilityHighThis comparison framework helps buyers move from simple vendor selection to risk-based partner selection.
For companies seeking a broader view of available systems and production equipment, the product portfolio can provide a starting point for technical review before detailed RFQ discussions.
Capital budgeting for a multi-chamber IV bag lipid emulsion project in the United States should include much more than the filling line itself. Total investment usually covers cleanroom construction, utilities, solution preparation and distribution systems, purified water and WFI equipment, sterilization support, HVAC, automation, validation, packaging equipment, warehousing, and operator training. Imported equipment projects must also consider freight, insurance, customs handling, installation schedule buffers, and utility adaptation requirements.
The budget varies according to line speed, chamber design complexity, level of automation, inspection scope, and production volume targets. A pilot or niche-scale program may justify a compact line, while a national supply model for hospital groups requires larger throughput and stronger redundancy planning.
ROI depends on formulation margin, annual output, hospital adoption rate, labor savings for customers, and reduced waste. In many cases, the business case becomes strongest when the product replaces higher-risk compounding activities or fills a clear gap in stable ready-to-mix nutrition supply.
Cost ElementBudget RoleCommon RiskPlanning AdviceBag production and filling equipmentCore capexUnderspecification of outputMatch line speed to demand forecastCleanroom and facility worksMajor infrastructure costLayout changes during buildFinalize process flow earlyWater and utility systemsCritical support packageUtility mismatchIntegrate with process designAutomation and data systemsTraceability and controlSoftware integration delaysDefine URS clearlyValidation and qualificationNecessary launch requirementHidden timeline extensionsBudget for full lifecycle documentsTraining and after-sales supportStartup reliabilityOperator learning curveInclude extended support periodThe table above shows why realistic budget planning should include technical, regulatory, and operational factors rather than equipment invoice values alone.
For U.S. investors comparing project pathways, manufacturers with integrated engineering experience may reduce coordination cost. Shanghai IVEN Pharmatech Engineering, established in 2005, is known internationally for combining pharmaceutical equipment, water systems, logistics, and turnkey execution. Its experience across IV solution lines, packaging equipment, and validation-oriented project delivery can be relevant for companies seeking one engineering partner rather than multiple disconnected vendors.
Investment in this field can be attractive, but only when product science, regulatory planning, and plant execution are aligned. The biggest risk is underestimating formulation complexity. Lipid emulsions require careful control of droplet size distribution, oxidation protection, ingredient compatibility, and sterilization impact. Packaging innovation cannot compensate for unstable formulation design.
A second risk is choosing film or seal technology before completing full validation strategy. If barrier performance, leachables profile, or peel strength is not matched correctly to the formula, scale-up may stall. A third risk is project fragmentation. Using separate vendors for solution systems, bag handling, filling, inspection, and utilities can create interface failures that delay startup.
Policy and sustainability trends also matter. By 2026, more U.S. buyers are expected to assess packaging recyclability potential, material reduction, energy use per unit, and electronic batch traceability. State-level environmental attention in markets such as California and New York may indirectly influence packaging selection and supplier reputation.
Another concern is service continuity. A lower-cost supplier may become expensive if commissioning takes longer than expected or spare parts support is weak. This is where service capability becomes a decisive investment factor. Suppliers that offer installation, commissioning, validation support, training, and process optimization can significantly reduce total project risk. Companies wanting direct technical discussion can use the contact channel to request project-specific support.
Risk AreaDescriptionPossible EffectMitigationFormulation instabilityLipid and additives fail compatibility targetsShort shelf life or approval delayRun early stability studiesFilm mismatchBarrier or extractables profile unsuitableRevalidation or product redesignQualify material suppliers earlySeal reliability issuesActivation or transport failureProduct loss and complaintsExtensive seal integrity testingRegulatory gapsInsufficient documentation or design controlLonger launch timelineBuild cGMP compliance into projectFragmented project managementMultiple vendors with unclear interfacesCost overrun and delayUse integrated engineering managementWeak after-sales serviceSlow troubleshooting and parts deliveryExtended downtimeDefine service SLA before purchaseThis risk map can help finance, operations, and technical teams create a more durable investment plan.
For U.S. pharmaceutical manufacturers and investors exploring advanced IV packaging projects, Shanghai IVEN Pharmatech Engineering offers a profile worth considering. Its strengths can be viewed through three practical lenses relevant to American project teams.
Technological capabilities: the company has built expertise in IV solution equipment, pharmaceutical water treatment, solution preparation, intelligent conveying, and packaging-related systems. Its engineering approach is centered on compliance-oriented design and integration, which is useful when a multi-chamber lipid emulsion line must interact smoothly with utilities, preparation tanks, sterilization workflows, and downstream logistics.
Manufacturing capabilities: the organization operates multiple specialized plants in Shanghai focused on filling and packaging machinery, water treatment systems, logistics systems, and vacuum blood collection tube equipment. This manufacturing structure can be valuable for buyers who want better consistency, component control, and coordinated production schedules. It also has extensive experience delivering IV solution lines for soft bags, PP bottles, and glass bottles, supporting a broader understanding of sterile liquid manufacturing.
Service capabilities: for U.S.-facing projects, the important point is lifecycle support. The company provides consulting, engineering design, customization, installation, commissioning, validation assistance, quality documentation support, training, and after-sales service. This model can reduce the risk of layout errors, schedule delays, and unclear responsibilities during project execution. It has also participated in international projects in more than 60 countries and completed numerous turnkey works, giving buyers a stronger basis for evaluating execution maturity.
For American decision-makers, especially those building new capacity near pharmaceutical clusters in New Jersey, North Carolina, Indiana, Texas, or California, the value of such an integrated partner lies in reducing technical handoff points and strengthening launch predictability.
1. Is a multi-chamber bag always necessary for lipid emulsion products?No. It is most beneficial when ingredients are unstable or incompatible during long-term storage. If a formulation is proven stable in a single chamber, a simpler bag may still work.
2. What U.S. sectors create the strongest demand?Hospital nutrition programs, ICU support, pediatrics, oncology support services, and institutions that want to reduce sterile compounding workload are the main drivers.
3. What is the biggest technical challenge?Usually the combination of formulation stability, barrier film selection, and reliable internal seal design. These three factors strongly affect commercial viability.
4. How important is regulatory experience when choosing equipment?It is essential. Equipment design, documentation, validation support, and data integrity readiness all influence the success of FDA-facing projects in the United States.
5. Are multi-chamber IV bags only for parenteral nutrition?No. While parenteral nutrition is the most common use, the concept can support other multi-component sterile liquid applications that require separation until use.
6. How should buyers evaluate ROI?Look at product margin, annual volume, hospital workflow savings, reduced compounding needs, waste reduction, and the strategic value of a differentiated stable product format.
7. What future trends should investors watch for through 2026?Higher automation, digital batch traceability, sustainable film development, resilient domestic supply planning, and stronger readiness for quality audits and regulatory review.
8. What makes an engineering partner more reliable?A combination of proven manufacturing depth, integrated system capability, cGMP awareness, validation support, and responsive after-sales service.
9. Should U.S. buyers prefer turnkey execution?For many projects, yes. Turnkey planning can reduce interface risk among water systems, cleanrooms, filling equipment, logistics, validation, and startup management.
10. Where should a project start?Begin with market sizing, formulation strategy, target throughput, regulatory pathway, facility concept, and a qualified supplier shortlist. Then move into URS definition and budget validation.
In summary, multi-chamber IV bag lipid emulsion production is becoming an increasingly strategic capability in the United States. It supports better product stability, safer clinical handling, and more efficient hospital workflows. For pharmaceutical companies, CDMOs, and healthcare supply investors, success will depend on choosing the right bag architecture, validated materials, compliant production systems, and a partner with strong technological, manufacturing, and service capabilities.
-
Micro Blood Tube Machine Maintenance in United States
For medical device manufacturers in the United States, effective maintenance for micro blood tube machines is essential for producing high volumes of consistent, compliant, and high-quality blood collection tubes. These systems support automated tube feeding, cap assembly, additive dosing, drying, labeling, inspection, and packing with tighter process control than manual operations. In hospitals, physician office labs, central laboratories, and diagnostic networks across cities such as Boston, Houston, San Diego, and Chicago, demand for reliable micro blood collection products continues to rise. That is why maintenance planning is not simply a technical task; it is a core business strategy tied to uptime, sterility, precision, and regulatory readiness.
Well-maintained production equipment reduces scrap, improves additive accuracy, protects cap fit quality, lowers contamination risk, and extends asset life. For buyers evaluating new production lines or upgrading existing operations, machine maintenance should be reviewed alongside automation level, validation support, spare parts availability, and supplier responsiveness. Companies seeking broader engineering support can also review the manufacturer background, explore turnkey engineering capabilities, browse available equipment solutions, or contact a technical team for project discussions.
Micro blood tube machine maintenance enables medical device companies to achieve stable large-scale production of blood collection tubes for hospitals and diagnostic laboratories with dependable automation, repeatable quality, and lower operational risk. In the United States market, where FDA expectations, traceability standards, and customer audits are strict, maintenance directly influences whether a line can keep meeting throughput and quality targets month after month.
The most important maintenance goals are straightforward: prevent unexpected downtime, preserve dimensional consistency, keep dosing and insertion stations calibrated, maintain clean contact surfaces, and ensure sensors and vision systems continue to detect defects accurately. Maintenance also supports production economics. A line with fewer stoppages can protect labor utilization, reduce missed deliveries, and help manufacturers serve regional distribution hubs near Los Angeles, New York/New Jersey, Savannah, and Dallas more efficiently.
Maintenance Focus Main Objective Production Impact Quality Impact Risk if Ignored Recommended Frequency Lubrication Reduce wear on moving parts Stable cycle speed More consistent assembly Premature failure Daily to weekly Sensor cleaning Maintain accurate detection Fewer false stops Better reject sorting Missed defects Daily Calibration Preserve dosing and positioning accuracy Reduced scrap Correct additive fill Out-of-spec batches Weekly to monthly Wear-part replacement Avoid sudden breakdowns Higher uptime Stable sealing and fit Emergency shutdown By running hours Electrical inspection Protect control reliability Reduced faults Consistent automation logic Line trips Monthly Validation review Maintain compliance evidence Supports release timing Audit readiness Documentation gaps QuarterlyThe table above shows why maintenance should be treated as a production control system, not merely a repair function. Each routine activity contributes to both operating efficiency and compliance performance.
A micro blood tube machine maintenance program is a structured set of preventive, predictive, and corrective actions used to keep automated blood collection tube production lines operating within validated parameters. It covers mechanical assemblies, filling and dosing units, capping modules, conveyors, electrical cabinets, human-machine interfaces, compressed air systems, and vision inspection devices.
In practice, maintenance usually works through five layers. First, operators perform daily startup and shutdown checks. Second, technicians complete preventive tasks according to hours of operation. Third, calibration and qualification reviews are performed to confirm equipment remains within specification. Fourth, spare parts and consumables are managed to avoid stockouts. Fifth, service data is analyzed to identify root causes and improve long-term line reliability.
A typical micro blood collection tube line may include tube unscrambling, transfer, additive spraying or dosing, drying, cap or closure assembly, vacuum-related handling where relevant, leak checks, labeling, visual inspection, counting, and final packaging. Even minor drift at one station can affect downstream performance. For example, misaligned cap insertion can increase reject rates at inspection, while improper dosing can create customer complaints and regulatory exposure.
For U.S. buyers, the best maintenance programs are linked to documented SOPs, electronic records, line clearance procedures, and preventive maintenance schedules aligned with GMP practices. These programs are especially important for plants supplying large integrated delivery networks and nationwide distributors.
Micro blood tube systems are used primarily in the production of capillary and small-volume blood collection tubes for neonatal sampling, pediatric testing, point-of-care workflows, and specialized diagnostics. U.S. healthcare providers increasingly value products that minimize blood draw volume while preserving sample integrity. That trend supports continued investment in efficient automated production.
The application range includes hospital laboratories, reference labs, outpatient clinics, blood testing service providers, contract manufacturing organizations, and medical consumables companies. Facilities near research and healthcare clusters such as Minneapolis, Philadelphia, Raleigh-Durham, and the San Francisco Bay Area can particularly benefit from consistent small-volume collection products.
The production benefits are substantial. Automated lines improve throughput, reduce labor dependency, support lot traceability, and enable more stable quality control. They also make it easier to integrate in-line inspection and data collection. From a maintenance perspective, these benefits are fully realized only when machine reliability is sustained through disciplined servicing.
Application Area Typical End User Why Micro Tubes Are Used Benefit of Automation Maintenance Priority Business Value Neonatal testing Children’s hospitals Low sample volume Precise small-format handling High dosing accuracy Reduced sample waste Pediatric diagnostics Regional hospitals Patient comfort Fast, repeatable output Cap fit consistency Higher customer trust Specialty labs Reference laboratories Specific additive needs Controlled formulation application Calibration discipline Better product differentiation POC channels Clinics and urgent care Convenient collection Scalable production Inspection stability Market responsiveness OEM supply Medical consumables brands Private label demand Lot traceability Documentation control Supports contract business Export supply International distributors Cross-border compliance Repeatable quality records Validation upkeep Improved market accessThis table shows that maintenance requirements vary by end-market use. For higher-value and more regulated applications, service discipline becomes a larger contributor to profitability and customer retention.
var ctxBar = document.getElementById(‘barIndustryDemand’).getContext(‘2d’);var chartBar = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Hospital Labs’, ‘Reference Labs’, ‘Clinics’, ‘OEM Brands’, ‘Export Distributors’, ‘Research Centers’], datasets: [{ label: ‘Estimated U.S. Demand Index 2026’, data: [92, 88, 74, 69, 61, 57], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false }});Micro blood tube production equipment is available in several configurations, ranging from semi-automatic units to fully integrated high-speed lines. The right type depends on target output, tube design, additive format, packaging requirements, and validation expectations.
Semi-automatic machines are often chosen by smaller producers or new entrants that need flexibility and lower capital cost. Modular automatic systems allow expansion over time by adding inspection, labeling, or packing units. Fully integrated lines are best suited for high-volume U.S. manufacturers supplying national healthcare networks and private-label channels.
Configuration choices also affect maintenance. Simpler machines are easier to service but may depend more on operator skill. Highly automated lines can deliver superior repeatability, yet they require stronger technical support, spare parts planning, and software-aware maintenance practices.
Machine Type Automation Level Typical Output Best For Maintenance Complexity Key Strength Bench semi-automatic unit Low Small batches R&D and pilot use Low Affordable entry Standalone dosing machine Medium Medium batches Special additive lines Medium Dosing precision Cap assembly line Medium Mid-volume production Focused tube formats Medium Compact footprint Modular automatic line High Scalable output Growing manufacturers Medium to high Upgrade flexibility Integrated high-speed line Very high Large-scale output Major U.S. suppliers High Throughput and traceability Turnkey cleanroom solution Very high Plant-wide capacity New factory projects High Compliance integrationThe table highlights how configuration affects both output and service burden. Buyers should balance productivity gains against the technical resources needed to maintain the line.
From a technology standpoint, some international engineering companies have become competitive because they combine blood collection tube line design with broader pharmaceutical and medical device process expertise. IVEN Pharmatech Engineering, for example, is recognized for integrating automation, process engineering, and compliance-oriented design across multiple equipment categories. That technological capability can be attractive for U.S. projects requiring synchronization between utilities, production lines, and downstream packaging.
Comparing automated equipment maintenance with manual assembly may seem unusual, but it is highly relevant. Manual lines may appear simpler because they involve fewer machines. However, they often create hidden costs through labor variability, inconsistent output, lower traceability, and higher contamination exposure. Automated lines require planned maintenance, but they usually deliver better total process control.
In manual operations, quality often depends on operator attention and training stability. In automated operations, quality depends more on machine condition, setup accuracy, and validated controls. Therefore, maintenance becomes the bridge between design capability and actual production performance.
Factor Automated Line Manual Line Impact on Quality Impact on Cost Best Fit Output consistency High Variable Stronger lot uniformity Lower scrap long-term High-volume plants Labor dependence Lower High Less operator variation Lower cost per unit at scale National supply programs Traceability Strong Limited Better compliance support Less recall risk Regulated markets Maintenance need Structured Lower formal need Machine-based consistency Predictable service cost Serious manufacturers Scale-up potential Excellent Weak Supports stable growth Improves ROI as demand rises Growing firms Audit readiness Better Harder Documented control points Lower compliance disruption FDA-facing operationsThis comparison shows that automated lines convert maintenance spending into measurable production advantages. Manual lines may still suit very small operations, but they are harder to scale across the U.S. healthcare supply chain.
var ctxComp = document.getElementById(‘comparisonChartSuppliers’).getContext(‘2d’);var chartComp = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Uptime’, ‘Traceability’, ‘Labor Efficiency’, ‘Quality Control’, ‘Scale-Up’, ‘Audit Support’], datasets: [{ label: ‘Automated Line Advantage Score’, data: [94, 96, 91, 95, 93, 92], backgroundColor: ‘#7b61ff’ },{ label: ‘Manual Line Score’, data: [63, 48, 52, 61, 46, 55], backgroundColor: ‘#c9c9c9’ }] }, options: { responsive: true, maintainAspectRatio: false }});The United States remains one of the most attractive markets for blood collection consumables and associated production technology. Demand is supported by aging populations, higher testing volumes, preventive care trends, decentralized diagnostics, and continuous need for pediatric and specialty collection products. By 2026, manufacturers are expected to invest more in automation, digital maintenance tracking, and sustainable production systems.
Several factors create opportunity. First, domestic resilience and supply chain diversification are encouraging more local manufacturing discussions. Second, healthcare networks want dependable supply after experiencing disruptions in global logistics. Third, FDA-focused quality systems favor equipment with robust documentation and support. Fourth, plants located near major freight corridors such as Memphis, Atlanta, Long Beach, Newark, and Seattle can leverage efficient distribution once output is stabilized.
Machine suppliers that can support not just equipment sales but also factory planning, utility design, validation, and after-sales service have an advantage. This is where broader manufacturing capability matters. IVEN Pharmatech Engineering, for instance, has specialized production bases for filling and packaging systems, pharmaceutical water systems, logistics equipment, and vacuum blood collection tube equipment. That manufacturing depth can reduce integration risk for customers that want more than a standalone machine.
var ctxLine = document.getElementById(‘lineMarketGrowth’).getContext(‘2d’);var chartLine = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘U.S. Market Demand Index’, data: [68, 73, 79, 85, 92, 98], borderColor: ‘#2a9d8f’, backgroundColor: ‘rgba(42,157,143,0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart above reflects a realistic growth pattern driven by higher testing intensity and automation investment. While exact growth rates vary by segment, the trend direction remains favorable for reliable equipment suppliers and domestic or near-market producers.
Choosing a supplier for micro blood tube production equipment should go beyond comparing quotations. U.S. buyers should assess regulatory understanding, engineering depth, installed base, response speed, training capability, parts availability, and documentation quality. The lowest initial price rarely delivers the lowest lifecycle cost.
Start by reviewing whether the supplier understands U.S. compliance expectations, including documentation structure, validation support, material traceability, and quality records. Then confirm whether the line design matches your intended tube sizes, additives, throughput targets, packaging concept, and cleanroom level. A capable supplier should be willing to discuss FAT, SAT, IQ, OQ, and PQ planning early in the project.
Service capability is equally critical. Buyers should ask who handles installation, commissioning, training, remote support, and emergency troubleshooting. A supplier that offers lifecycle support, process transfer assistance, and optimization services can reduce the burden on in-house teams. IVEN’s service model is often noted by buyers because it extends from feasibility and engineering design through commissioning, validation support, documentation, staff training, and ongoing after-sales assistance.
Selection Criterion Why It Matters What to Ask Warning Sign Preferred Evidence Buyer Benefit Regulatory knowledge Supports compliance Have you supplied FDA-facing projects? Generic answers only Validation document samples Lower audit risk Customization ability Aligns line with product needs Can you adapt for our tube format? One-size-fits-all design Layout drawings Better process fit After-sales response Protects uptime What is your response timeline? Unclear support channels Service SOPs Faster recovery Spare parts support Avoids long stoppages Which parts should we stock locally? No spare list provided Recommended inventory plan Stable operations Factory acceptance testing Reduces startup issues Can we witness FAT with protocols? Limited test transparency FAT reports Lower commissioning risk Reference projects Shows real execution ability Can you share similar case experience? No relevant examples Installed base summary Higher confidenceThis evaluation framework helps buyers compare suppliers on lifecycle value, not just machine cost. In the U.S. market, that distinction can significantly affect long-term profitability.
Investment in a micro blood tube line varies depending on automation level, speed, tooling, cleanroom integration, inspection systems, and validation scope. Budgeting should include the machine itself, utilities, installation, packaging integration, operator training, spare parts, maintenance tools, and qualification activities. Many companies underestimate the importance of maintenance budget during the first two years after startup.
ROI is usually driven by labor savings, higher output, lower scrap, reduced rework, improved compliance, and stronger ability to win supply contracts. In the United States, additional ROI can come from shortened lead times for domestic customers and lower dependence on uncertain imported finished consumables.
Cost Item Low Automation Setup Mid-Level Automatic Line High-Speed Integrated Line Budgeting Note ROI Relevance Main equipment Lower Medium High Largest capital item Defines output scale Tooling and format parts Low Medium Medium to high Needed for tube variants Supports product flexibility Installation and commissioning Medium Medium High Often underestimated Faster time to production Validation package Low to medium Medium High Critical for regulated supply Enables market access Spare parts inventory Low Medium Medium to high Protects uptime Reduces downtime cost Annual maintenance Low Medium High Plan from day one Preserves long-term returnThe table above is useful because it separates visible capital expense from less visible lifecycle costs. Many failed equipment projects do not fail technically; they fail because owners budgeted for purchase but not for qualification, service, and maintenance discipline.
For ROI modeling, a mid-sized U.S. manufacturer may find that a well-maintained automatic line delivers payback faster than expected when customer demand is stable and labor costs are high. Savings can also come from fewer rejected batches, better additive accuracy, and stronger on-time delivery performance. Plants near major healthcare procurement centers such as New Jersey, Texas, and California may realize extra benefit because distribution efficiency supports faster order turnaround.
var ctxArea = document.getElementById(‘areaTrendShift’).getContext(‘2d’);var chartArea = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Shift from Manual to Automated Production’, data: [35, 42, 50, 59, 68, 76], borderColor: ‘#e76f51’, backgroundColor: ‘rgba(231,111,81,0.25)’, fill: true, tension: 0.35 }] }, options: { responsive: true, maintainAspectRatio: false }});Before purchasing a micro blood tube line, companies should review technical fit, utility requirements, cleanroom conditions, validation burden, staffing readiness, digital integration, and spare parts strategy. Maintenance risk should be considered during procurement, not after installation. The most common problem is buying a line whose complexity exceeds the site’s ability to operate and maintain it properly.
Other risks include inconsistent raw materials, inadequate change-part control, poor environmental control, insufficient training, and weak supplier communication. Import logistics can also affect delivery schedules, so buyers should plan carefully around U.S. port entry points and inland transport. For equipment arriving through Los Angeles/Long Beach, Houston, or New York/New Jersey, project managers should build in customs, inland trucking, and site readiness buffers.
Sustainability is becoming another strategic factor. By 2026, more buyers will ask about energy efficiency, compressed air consumption, material waste reduction, washable contact surfaces, and digital monitoring that helps prevent over-maintenance. Predictive maintenance using sensors and data analytics is expected to grow, especially in larger facilities that already use MES, ERP, or computerized maintenance management systems.
Policy trends also matter. Domestic manufacturing incentives, healthcare supply chain resilience initiatives, and stricter documentation expectations may shape procurement decisions. Equipment that can support clear traceability, efficient validation, and reduced waste will likely gain more attention.
A practical case scenario illustrates the point. Imagine a U.S. medical consumables company launching a pediatric tube line near Charlotte. It selects a modular automatic system with dosing, drying, capping, and labeling. In the first six months, output is strong, but unplanned downtime begins to rise because preventive maintenance intervals are missed and spare sensors are not stocked. After implementing a disciplined maintenance schedule, adding operator checklists, and using supplier remote support, uptime improves, scrap falls, and customer delivery performance stabilizes. The lesson is simple: the machine creates potential, but maintenance converts potential into business performance.
Another case may involve a company in the Midwest expanding from manual assembly to automated production. By choosing a supplier with strong engineering and training support, the firm reduces startup risk and builds internal technical confidence more quickly. This is where integrated project experience can be valuable. Suppliers with cross-functional engineering teams can help align layout, utilities, documentation, and training, not just ship equipment.
What is included in micro blood tube machine maintenance?It usually includes lubrication, cleaning, sensor inspection, electrical checks, calibration, wear-part replacement, software backups, and documentation review.
How often should these machines be serviced?Basic checks are often daily, preventive service is commonly weekly or monthly, and deeper inspection or validation review may be quarterly or based on operating hours.
Why is maintenance so important in the United States market?Because U.S. customers and regulators place high value on quality consistency, traceability, audit readiness, and reliable delivery performance.
Can small manufacturers invest in these lines?Yes. Semi-automatic or modular systems can provide a practical entry point, especially when future expansion is planned carefully.
What should buyers ask suppliers before purchase?Ask about validation support, spare parts plans, training, response times, customization, factory testing, and experience with regulated production environments.
Are turnkey solutions better than standalone machines?They can be, especially for new U.S. facilities that need layout design, utility planning, installation, commissioning, and validation support in one coordinated package.
How does IVEN fit into this market?IVEN Pharmatech Engineering is known internationally for combining engineering, manufacturing, and service capabilities across pharmaceutical and medical device equipment. For blood collection tube projects, that means customers can evaluate not only machine hardware but also broader project execution support, customized integration, and lifecycle service.
What future trends should buyers watch through 2026?Predictive maintenance, smarter vision inspection, digital traceability, energy-efficient automation, more sustainable production practices, and stronger localization of healthcare supply chains.
In summary, maintenance for micro blood tube machines is a strategic requirement for any company that wants reliable, scalable, and compliant production in the United States. The strongest projects combine suitable machine configuration, disciplined service planning, supplier partnership, and long-term operational readiness. Buyers that evaluate technology capability, manufacturing depth, and service responsiveness together are typically better positioned to protect uptime and achieve a stronger return on investment.