Prefilled Syringe Filling Systems in the United States
For pharmaceutical manufacturers in the United States, a prefilled syringe filling machine is a high-value aseptic production system used to fill, stop, plunger-place, and often label or nest-process syringes with sterile drug products under tightly controlled conditions. It is widely evaluated by large pharmaceutical companies, biotech firms, and medical device manufacturers that need higher product safety, precise dosing, better operator protection, and compliance with U.S. FDA cGMP requirements. In practical terms, this equipment supports the commercial production of vaccines, biologics, injectables, anticoagulants, ophthalmic products, and specialty therapies packaged in ready-to-use syringe formats for hospitals, clinics, and home-care markets.
Across major U.S. pharmaceutical hubs such as Boston, New Jersey, Philadelphia, Raleigh-Durham, Indianapolis, Chicago, Houston, and the San Francisco Bay Area, investment in advanced aseptic filling technology continues to rise. The shift is driven by biologics growth, demand for patient-friendly delivery devices, stricter quality expectations, and the need to modernize older vial-based lines. Buyers are not only comparing machine speed; they are also assessing isolator integration, container closure integrity, changeover flexibility, digital validation support, and lifecycle service. For companies planning a new line or expansion project, understanding the available equipment configurations and supplier capabilities is essential.
Quick Answer: Why Prefilled Syringe Filling Equipment Matters for U.S. Manufacturers

A prefilled syringe filling machine matters because it directly affects sterility assurance, dose accuracy, production efficiency, and regulatory readiness. In the United States, where injectable production is subject to rigorous FDA oversight, the equipment must support aseptic processing, repeatable performance, documentation integrity, and process validation. Compared with manual or semi-automatic approaches, modern automatic prefilled syringe lines reduce contamination risk, improve throughput, and create a more scalable path for commercial manufacturing.
It is especially important for firms expanding from clinical to commercial scale, converting a product from vial to syringe presentation, or building a greenfield facility near key logistics corridors such as Port Newark, Los Angeles/Long Beach, Savannah, or Memphis air cargo routes. Because prefilled syringe packaging is often used for high-value formulations, equipment selection also has a major financial effect on product loss, yield, and recall risk.
| Evaluation Factor | Why It Matters | Impact on U.S. Operations |
|---|---|---|
| Sterility assurance | Supports aseptic filling and minimizes contamination risk | Critical for FDA inspection readiness and patient safety |
| Dose accuracy | Ensures consistent fill volume per syringe | Reduces rejects, complaints, and batch deviations |
| Changeover flexibility | Allows multiple syringe sizes or formats | Useful for CMOs and multi-product facilities |
| Automation level | Reduces operator intervention | Improves consistency and labor efficiency |
| Validation support | Provides IQ/OQ/PQ and documentation structure | Speeds line qualification in regulated plants |
| Lifecycle service | Supports uptime and spare parts management | Important for long-term ROI in U.S. manufacturing |
The table above shows why this equipment is typically treated as a strategic investment rather than a simple machine purchase. A buyer is usually assessing total production performance, not just the initial output rate.
What Is a Prefilled Syringe Filling Machine and What Is It Used For in Pharmaceutical Production?

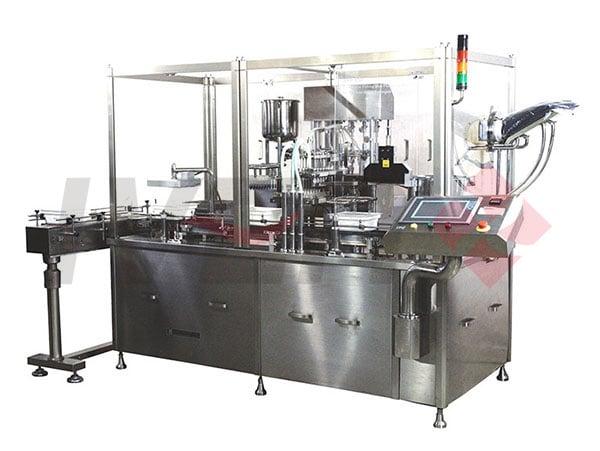
A prefilled syringe filling machine is specialized aseptic equipment designed to process empty syringes or ready-to-use nested syringes and fill them with sterile liquid drug products. Depending on the line design, the machine may perform de-nesting, syringe feeding, vacuum or time-pressure filling, nitrogen purging, stopper insertion, plunger rod placement, vision inspection, labeling, and tray or tub handling. Some systems are built for glass syringes, while others are optimized for polymer syringes or safety syringe assemblies.
In pharmaceutical production, these systems are used for products that benefit from unit-dose accuracy, user convenience, and reduced preparation steps at the point of care. This includes vaccines, low molecular weight heparin, monoclonal antibodies, emergency injectables, fertility drugs, and specialty hospital therapies. Prefilled formats are also increasingly attractive for self-administration, particularly in chronic disease treatment categories.
Unlike standard vial lines, syringe lines must manage delicate container handling and tight tolerance requirements. Plunger positioning, siliconization compatibility, residual volume control, and breakage prevention all become important. For highly potent or sensitive formulations, the machine may be integrated into a restricted access barrier system or isolator.
For manufacturers seeking broader plant planning support, integrated engineering partners can be valuable. Companies that combine equipment supply with turnkey pharmaceutical project services help reduce interface risk between filling systems, clean utilities, HVAC, cleanroom layouts, and material logistics.
Main Applications and Benefits of Prefilled Syringe Filling Equipment in Modern Pharmaceutical Manufacturing

Modern prefilled syringe filling equipment is used across multiple production environments, from biotech startups scaling an innovative injectable to established multinational pharmaceutical plants upgrading legacy packaging formats. In the United States, common users include branded drug manufacturers, CDMOs, vaccine producers, hospital injectable suppliers, and medical consumables companies entering combination product markets.
The primary benefit is patient-ready packaging. Prefilled syringes reduce bedside preparation steps, cut the risk of dosing errors, and support fast administration in hospitals, ambulatory care centers, and home settings. For manufacturers, the benefits include lower contamination risk, better line efficiency, improved ergonomics, stronger market differentiation, and reduced overfill versus some vial presentations.
| Application Area | Typical Products | Key Benefit |
|---|---|---|
| Vaccines | Seasonal and specialty immunizations | Fast administration and unit-dose control |
| Biologics | Monoclonal antibodies, proteins | High-value product protection |
| Anticoagulants | Heparin and related injectables | Ready-to-use convenience |
| Emergency medicine | Acute care injectables | Rapid deployment in clinical settings |
| Ophthalmics and specialty injectables | Small-volume sterile formulations | Precise fill control |
| Home-care therapies | Chronic disease and self-injection products | Patient usability and adherence support |
This table illustrates how the same core equipment can serve different therapeutic segments while delivering distinct operational and commercial benefits.
Another major advantage is compatibility with digital manufacturing strategies. Newer lines often include recipe management, electronic batch record interfaces, audit trails, predictive maintenance data, and camera-based process verification. These features are especially relevant for facilities in competitive U.S. clusters where quality and speed to market are critical.
The line chart reflects a realistic growth pattern in demand for syringe filling lines in the United States, driven by biologics expansion, reshoring interest, and ongoing capital investment in sterile manufacturing.
Key Types, Models and Technical Options for Prefilled Syringe Filling Machines
There is no single best machine for every facility. The right configuration depends on batch size, container format, viscosity, sterility strategy, available cleanroom classification, and whether the buyer is running clinical, pilot, or commercial volumes.
Broadly, the market includes semi-automatic units, fully automatic lines, nested syringe systems, bulk syringe systems, and integrated lines with isolators or RABS. Filling technology may include rotary piston pumps, peristaltic pumps, time-pressure systems, or mass-flow based control. Vision systems may inspect stopper placement, fill level, cosmetics, and component presence. Some lines also allow fast format changes for 0.5 mL, 1 mL, 2.25 mL, 3 mL, 5 mL, or custom syringe sizes.
| Machine Type | Best Use Case | Advantages |
|---|---|---|
| Semi-automatic syringe filler | R&D, pilot, low-volume specialty lines | Lower cost, flexible setup |
| Automatic nested syringe line | Sterile ready-to-use syringes | Low handling risk, strong aseptic profile |
| Automatic bulk syringe line | Higher-volume customized operations | Potentially lower container cost |
| Isolator-integrated line | High-potency or high-sterility assurance needs | Reduced intervention and contamination exposure |
| RABS-based line | Commercial aseptic filling with controlled access | Balance of access and containment |
| Multi-format flexible line | CMOs and multi-product plants | Faster changeover, broader customer fit |
The table shows how technical selection should match business model and process risk, not only output speed. For example, a CDMO serving multiple clients in New Jersey may prioritize flexibility and validation support, while a single-product biologics manufacturer in Massachusetts may prioritize containment and ultra-low product loss.
Common technical options requested by U.S. buyers include:
- 21 CFR Part 11-ready control architecture
- Automatic no-syringe-no-fill functions
- Inline weight check or vision fill verification
- Laminar airflow or isolator compatibility
- CIP/SIP options where applicable
- Nitrogen overlay for oxygen-sensitive products
- Robotic tub handling and de-nesting
- Data export for MES or plant SCADA systems
Manufacturers that provide broad equipment portfolios often offer better integration support across adjacent systems such as water for injection, purified steam, solution preparation, and packaging. For buyers reviewing supplier background, the company overview can help clarify engineering depth and project history.
Prefilled Syringe Filling Machine vs Alternative Technologies: Which Solution Fits Your Needs?
Many manufacturers ask whether they should invest in a syringe line or continue using vials, ampoules, cartridges, or contract filling. The answer depends on commercial strategy, product type, target patient population, and cost structure.
Vials remain highly versatile and are often favored for lyophilization, large batch production, and hospital distribution where bedside preparation is acceptable. Cartridges are common in pen injector systems. Ampoules are less common in some modern high-value biologic applications due to opening and handling limitations. Contract manufacturing can reduce initial capital outlay but may limit scheduling control and create tech transfer complexity.
| Format or Approach | Strengths | Limitations |
|---|---|---|
| Prefilled syringes | Ready to use, strong convenience, precise dose | Higher equipment and component complexity |
| Vials | Flexible, widely established, good for lyophilization | More preparation steps at use point |
| Ampoules | Simple container concept | Less user-friendly and more breakage risk |
| Cartridges | Well suited for pen systems | Application-specific and device-dependent |
| CMO outsourcing | Lower upfront capex | Less direct control over scheduling and know-how |
| Manual or semi-manual filling | Low initial cost for very small scale | Not ideal for commercial sterile scale-up |
This comparison makes clear that prefilled syringe technology is most attractive when convenience, premium presentation, dosing control, and market differentiation matter. It is less compelling when a product needs lyophilization first or when a company lacks sufficient forecast volume to justify capital spending.
The bar chart indicates where current U.S. demand is strongest. Biologics and home-care therapies are especially important demand drivers because syringe presentation aligns well with high-value, patient-administered therapies.
Market Overview and Future Trends for Prefilled Syringe Filling Equipment in Pharmaceutical Manufacturing
The U.S. market for prefilled syringe filling systems is supported by several structural factors: a large injectable drug market, strong biologics pipelines, active CDMO expansion, pressure to improve supply chain resilience, and increasing demand for patient-centric delivery formats. Domestic investments continue across East Coast, Midwest, and West Coast manufacturing centers, while Gulf Coast logistics hubs also remain relevant for imported components and finished-goods distribution.
By 2026, several trends are expected to shape equipment buying decisions:
- Higher adoption of isolator-based aseptic filling for premium sterile products
- More flexible lines designed for smaller, high-value batches
- Advanced vision inspection and digital batch traceability
- Greater focus on sustainable utilities and reduced product waste
- Integration with robotics, AGVs, and intelligent plant logistics
- Closer attention to supply chain localization and spare parts availability in North America
- Designs aligned with stricter data integrity and contamination control expectations
Policy and compliance will also matter. While exact regulatory priorities evolve, contamination control, documentation integrity, and lifecycle validation remain central. Buyers should expect future projects to emphasize not only machine qualification, but also environmental monitoring strategy, intervention reduction, and line clearance control.
The area chart shows the expected shift toward more advanced and highly automated sterile filling architecture in the United States through 2026.
Sustainability is becoming more visible in capital planning as well. Companies are comparing energy consumption, compressed air load, cleanroom footprint efficiency, reject rates, and packaging material optimization. Equipment suppliers that can help reduce product giveaway and cleaning burden may provide a stronger long-term value proposition.
How to Choose a Reliable Prefilled Syringe Filling Machine Manufacturer or Supplier
Selecting a supplier requires more than comparing brochures. U.S. buyers should evaluate technical competence, compliance track record, integration capability, after-sales support, and project execution discipline. The best supplier for one project may not be the best for another, especially when one plant needs a standalone machine and another needs a full sterile suite with utilities, conveyors, packaging, and validation deliverables.
A practical vendor assessment should cover the following areas:
| Supplier Checkpoint | Questions to Ask | Why It Matters |
|---|---|---|
| Regulatory familiarity | Can the supplier support FDA cGMP and global GMP expectations? | Reduces compliance risk during qualification and inspection |
| Engineering depth | Does the vendor understand filling, utilities, and facility interfaces? | Improves project coordination |
| Manufacturing capability | Are critical machine components produced under controlled standards? | Influences quality consistency and lead time |
| Reference projects | Has the vendor delivered similar lines to regulated markets? | Shows practical execution ability |
| Service network | How fast are spare parts, troubleshooting, and training support? | Protects uptime after startup |
| Validation documentation | Are FAT, SAT, IQ, OQ, and PQ support available? | Helps accelerate implementation |
This table functions as a working shortlist tool for procurement, engineering, and quality teams. It highlights the difference between buying a machine and selecting a qualified project partner.
When considering technology capabilities, IVEN Pharmatech Engineering is relevant to U.S. buyers because it focuses on integrated pharmaceutical engineering and sterile production solutions rather than only isolated equipment sales. Its technical strengths include pharmaceutical filling and packaging machinery, water treatment systems, logistics integration, and customized production line design aligned with international GMP expectations. For syringe filling projects, this broader process understanding can help reduce interface issues between the line and the rest of the sterile manufacturing environment.
On manufacturing capability, the company operates specialized production facilities focused on core pharmaceutical equipment categories. That matters because buyers often want consistency in fabrication quality, stainless steel workmanship, controls integration, and system durability over many years of operation. Large U.S. manufacturers comparing global suppliers usually look for evidence that the vendor can support both custom engineering and repeatable production standards.
On service capability, full lifecycle support is increasingly important. For example, U.S. project teams often need feasibility input, layout review, installation coordination, commissioning assistance, validation documentation, training, and post-startup troubleshooting. A supplier that can provide these services through the project cycle can reduce delays and change-order risks. Buyers ready to discuss a specific project scope can use the contact page to request a technical consultation.
Investment Cost, Budget Planning and ROI Analysis for Prefilled Syringe Filling Machines
Capital cost varies widely based on output speed, sterility architecture, automation level, inspection requirements, and the extent of line integration. A semi-automatic solution for development use may require a modest budget, while a commercial isolator-integrated line with de-nesting, stoppering, vision inspection, labeling, and robotic handling may require a multi-million-dollar investment.
In the United States, buyers should budget for more than the equipment invoice. True project cost often includes facility modifications, clean utilities, isolator testing, HVAC balancing, FAT and SAT travel, validation support, shipping, customs, installation, spare parts, operator training, and startup waste. If the site is in a high-cost metro region like Boston, San Diego, or the New York/New Jersey corridor, construction and integration costs can be significantly higher than equipment-only estimates suggest.
| Cost Element | Typical Budget Weight | Planning Note |
|---|---|---|
| Core filling machine | High | Main mechanical and control platform cost |
| Barrier system or isolator | High | Often needed for advanced aseptic strategy |
| Utilities and facility adaptation | Medium to high | Can rise sharply in retrofit projects |
| Inspection and ancillary modules | Medium | Depends on automation and product quality strategy |
| Validation and documentation | Medium | Essential in regulated U.S. deployment |
| Training, spares, service | Medium | Protects startup and long-term uptime |
This budget table helps decision-makers look beyond sticker price. For many projects, the hidden cost of poor planning is greater than the cost difference between two machine models.
ROI analysis should consider labor reduction, lower contamination risk, reduced product loss, higher yield, faster release readiness, greater market access, and strategic control over production. A line may also support higher-margin product launches that would be difficult in vial-only packaging. For a biologic with high product value per milliliter, even small reductions in overfill or reject rate can materially improve payback.
A typical ROI framework includes:
- Annual syringe output capacity
- Expected OEE after stabilization
- Reduction in labor per batch
- Decrease in rejects and interventions
- Estimated margin gain from syringe presentation
- Revenue protection from supply reliability
- Maintenance and consumables over 5 to 10 years
Key Considerations and Potential Risks When Investing in Prefilled Syringe Filling Equipment
Despite strong market potential, syringe filling projects come with real risks. One of the biggest is underestimating process complexity. Syringes are sensitive primary containers, and line performance depends on component quality, tub consistency, stopper compatibility, siliconization behavior, and environmental control. A machine that performs well at FAT may still face challenges during product-specific qualification if formulation viscosity, bubble behavior, or fill tolerance are not fully understood.
Another common risk is incomplete user requirement definition. If the URS does not clearly specify syringe formats, throughput targets, recipe management, barrier strategy, data integrity needs, and inspection criteria, expensive redesigns can occur. Retrofit projects are especially vulnerable when older cleanrooms in places like New Jersey or Puerto Rico need modern equipment with limited footprint flexibility.
Supply chain risk also deserves attention. Some buyers learned during recent disruptions that lead times for pumps, PLC components, servo systems, and sterile consumables can affect startup schedules. U.S. manufacturers should ask vendors about critical part sourcing, inventory planning, and field service response times.
Below is a practical risk matrix:
| Risk | Potential Consequence | Mitigation Approach |
|---|---|---|
| Poor URS definition | Scope gaps and change orders | Cross-functional design review before PO |
| Weak aseptic strategy | Qualification failure or contamination events | Use formal contamination control planning |
| Component incompatibility | Breakage, leaks, rejects | Run component trials early |
| Insufficient validation support | Delayed commercial launch | Confirm documentation package in contract |
| Limited service response | Extended downtime | Secure spares and service agreement |
| Underestimated total cost | Budget overruns | Model full project capex and opex |
This table is useful for project governance because it links each major risk to a practical control action. Mature buyers often include these items in supplier audits and internal capital approval packages.
The comparison chart demonstrates the type of weighted supplier evaluation many U.S. buyers use during formal procurement reviews. It reflects how broader project capability often matters as much as the machine itself.
If you are comparing available systems, a useful starting point is to review the wider pharmaceutical equipment portfolio and then narrow the discussion to product format, throughput, compliance, and facility integration needs.
FAQ:
1. What production speed is typical for a prefilled syringe filling machine?
Speed varies by machine design, syringe format, and product behavior. Development systems may run at low speeds for flexibility, while commercial automatic lines can process several thousand syringes per hour. However, actual qualified speed depends on sterility controls, reject strategy, and component handling stability.
2. Are prefilled syringe lines suitable for biologics?
Yes. They are widely used for biologics, especially when dose precision, patient convenience, and premium presentation are important. Buyers should confirm compatibility with protein sensitivity, shear concerns, oxygen exposure limits, and component materials.
3. What is the difference between nested and bulk syringe processing?
Nested processing handles ready-to-use syringes in tubs, usually reducing manual handling and contamination risk. Bulk processing may offer different cost or format advantages but often requires more extensive container handling. Nested systems are common in high-sterility modern applications.
4. Do U.S. manufacturers usually prefer isolators or RABS?
It depends on the product and risk strategy. Isolators are often favored for high-value sterile products and reduced intervention designs. RABS can still be appropriate for many commercial applications when well designed and properly operated.
5. How long does implementation usually take?
A full project timeline can range from several months to well over a year depending on customization, facility readiness, FAT scheduling, shipping, installation, validation, and local contractor performance. Retrofit projects often take longer than expected because of utility and layout constraints.
6. What documentation should buyers request?
Typical requests include URS alignment documents, DQ support, P&IDs where relevant, FAT protocols, calibration records, material certificates, software documentation, manuals, spare parts lists, and IQ/OQ templates or support packages.
7. Is a turnkey partner better than buying a standalone machine?
If your project includes clean utilities, facility coordination, HVAC interfaces, or multiple integrated systems, a turnkey-capable partner can reduce coordination risk. For simple line replacement in an established sterile suite, a standalone machine purchase may be sufficient.
8. What should U.S. buyers ask about after-sales support?
Ask about remote diagnostics, local service availability, emergency response time, critical spare parts stock, operator training, and support for requalification after upgrades. Strong service planning can prevent expensive downtime.
9. Can a supplier support broader factory development beyond the syringe line?
Some suppliers can. This is especially useful for companies building new injectable plants or expanding multi-product sites. Providers with experience in integrated sterile manufacturing can support equipment, utilities, logistics, validation, and training in a coordinated way.
10. Where can I learn more about integrated pharmaceutical project support?
Manufacturers evaluating a broader solution can review integrated turnkey capabilities, explore the engineering background, or reach out through the project inquiry channel for a more tailored discussion.
In summary, the right prefilled syringe filling machine for the United States market is the one that aligns product risk, regulatory expectations, plant infrastructure, and long-term commercial strategy. For large pharmaceutical and medical device companies, the decision should be based on validated performance, aseptic design, flexible engineering, service support, and lifecycle value rather than purchase price alone.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Liquid Vial Filling Machines for the United States
In the United States, a liquid vial filling machine is a mission-critical production asset for pharmaceutical and medical device manufacturers that need sterile, accurate, and regulator-ready filling of injectable products. It is typically evaluated when companies expand capacity, replace aging aseptic lines, launch new biologics, or modernize operations to meet strict FDA cGMP expectations while improving throughput, yield, and data integrity.
For buyers in major U.S. pharmaceutical corridors such as New Jersey, Boston, Raleigh-Durham, Indianapolis, and the San Francisco Bay Area, the right filling platform is not simply a packaging purchase. It is a strategic manufacturing decision that affects contamination control, line efficiency, validation timelines, labor planning, and total cost of ownership. Whether a plant sources components through the ports of Los Angeles/Long Beach, Savannah, Houston, or New York/New Jersey, supply chain stability and after-sales support also influence equipment selection.
This guide explains how to evaluate a liquid vial filling machine for the United States market, what technical options matter most, how it compares with alternatives, what trends are shaping 2026 planning, and how to screen manufacturers and suppliers with confidence.
A liquid vial filling machine is used to dose sterile liquid formulations into glass or polymer vials under tightly controlled aseptic or contained conditions. In U.S. pharmaceutical production, it commonly supports vaccines, antibiotics, oncology drugs, biologics, diagnostic reagents, and other injectables. The machine usually integrates with vial washing, depyrogenation, stopper placement, capping, in-process controls, environmental monitoring, and automated rejection systems.
Large manufacturers and contract development and manufacturing organizations in the United States assess these systems when they need to:
From a commercial perspective, the best system is the one that matches product characteristics, container format, batch size, sterility strategy, and expansion plans. A low-speed laboratory or pilot solution may fit a biotech startup in Cambridge, Massachusetts, while a high-speed integrated aseptic line may better suit a large injectable plant in New Jersey or North Carolina.
Decision FactorWhy It MattersImpact on U.S. OperationsFDA cGMP alignmentSupports audit readiness and documentation disciplineReduces compliance risk during inspectionsFill accuracyProtects dose consistency and product valueEssential for potent and expensive injectablesSterility assuranceControls contamination in aseptic processingCritical for parenteral products sold nationwideAutomation levelReduces manual intervention and errorImproves uptime and labor efficiencyChangeover flexibilitySupports multiple vial sizes and SKUsUseful for CDMOs and multi-product facilitiesService supportShortens downtime and validation delaysImportant across distributed U.S. plant networksThe table above shows that purchasing decisions are rarely based on speed alone. In practice, U.S. buyers compare compliance capability, validation documentation, maintenance access, spare parts availability, and long-term operational resilience before signing off on capital expenditure.
A liquid vial filling machine is designed to meter a defined volume of sterile or non-sterile liquid into vials, then close them with stoppers and caps for downstream inspection, labeling, and packaging. In sterile pharmaceutical production, the equipment often forms part of a larger line that includes ultrasonic vial washing, depyrogenation tunnel, filling station, stoppering, capping, visual inspection, leak testing, and secondary packaging.
Core filling technologies may include peristaltic pumps, piston pumps, time-pressure systems, or mass-flow-based filling modules. The choice depends on viscosity, foaming tendency, dose volume, cleaning requirements, and the sensitivity of the formulation. Biologics and high-value small batches often favor technologies that minimize product loss and support rapid product changeover. High-volume generics may prioritize speed, robust repeatability, and lower consumable cost.
In a typical U.S. injectable facility, the machine is used for several production scenarios:
Because every formulation behaves differently, user requirement specifications should define fill volume range, target line speed, product contact materials, oxygen control, nitrogen purging, container closure integrity objectives, and integration with SCADA or MES systems. For U.S. projects, it is also common to align equipment documentation with IQ, OQ, and PQ expectations before installation begins.
Companies seeking broader background on integrated projects often review a supplier’s engineering profile and prior regulated work. For example, buyers can examine company capabilities and compliance experience before progressing to technical discussions.
The main applications of a liquid vial filling machine stretch across sterile injectable pharmaceuticals, biotech products, laboratory reagents, and selected medical device liquids. In the United States, demand is particularly strong in biologics, specialty injectables, contract manufacturing, and hospital supply resilience projects.
Typical applications include:
The benefits go beyond output. A well-designed system improves dose consistency, lowers reject rates, supports electronic batch record integration, and helps reduce line intervention. In facilities near major life science clusters such as Philadelphia, Chicago, and San Diego, these advantages can translate into faster release cycles and better utilization of cleanroom assets.
Application AreaTypical ProductKey RequirementMain BenefitSterile injectablesAntibioticsAseptic filling accuracyConsistent dose and lower contamination riskBiologicsMonoclonal antibody solutionsGentle handlingProtects product integrityVaccinesMulti-dose or single-dose vialsHigh sterility assuranceReliable commercial outputOncologyPotent injectable drugsContainment and safetyOperator protectionClinical batchesInvestigational productsFlexible batch controlFaster scale-up and tech transferDiagnosticsReagents and assay liquidsPrecise low-volume dosingBetter test consistencyThe table highlights how application drives machine configuration. The ideal line for diagnostic reagents may be very different from the right line for an oncology injectable or a vaccine campaign. That is why upfront process mapping matters.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Biologics’, ‘Sterile Generics’, ‘Vaccines’, ‘CDMO Projects’, ‘Diagnostics’, ‘Clinical Supply’], datasets: [{ label: ‘Estimated U.S. demand index’, data: [92, 78, 85, 88, 61, 57], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The demand pattern above reflects strong U.S. investment in biologics, vaccine resilience, and outsourced sterile manufacturing capacity, especially among CDMOs serving both domestic and international launches.
Liquid vial filling machines can be grouped by speed, sterility concept, filling method, and line integration level. For U.S. buyers, the practical choice often comes down to matching batch profile, regulatory strategy, facility footprint, and future SKU expansion.
Common machine categories include monoblock fillers, linear indexing fillers, rotary fillers, and fully integrated aseptic lines. Smaller operations may choose semi-automatic or compact automatic systems for development work. High-output commercial plants usually prefer synchronized washing, depyrogenation, filling, stoppering, and capping lines with isolator or RABS protection.
Machine TypeTypical SpeedBest Use CaseKey AdvantageLimitationSemi-automatic fillerLowR&D and pilot workLow entry costHigher labor dependenceCompact automatic fillerLow to mediumClinical and specialty productsFlexible changeoverLimited large-scale throughputLinear aseptic fillerMediumMulti-SKU facilitiesGood accessibilityLarger footprintRotary high-speed fillerHighCommercial injectablesExcellent throughputMore complex validationIsolator-based fillerMedium to highHigh-value sterile productsLower contamination riskHigher capital costLyophilization-ready lineMediumFreeze-dried formulationsIntegrated process compatibilityRequires coordinated freeze-dryer interfaceImportant technical options include:
When reviewing equipment portfolios, buyers often look for suppliers with broad sterile processing competence, not only a single machine. IVEN Pharmatech Engineering, for example, is known for technological capabilities spanning filling and packaging systems, water treatment, intelligent logistics, and integrated pharmaceutical engineering. That broader process understanding can matter when a vial line must interact with purified water, WFI, clean utilities, and upstream preparation systems in a compliant plant design.
Not every product should be packed in a vial, and not every vial should be filled on the same type of machine. U.S. project teams often compare a liquid vial filling machine against ampoule filling lines, prefilled syringe systems, BFS platforms, cartridge fillers, and outsourcing to a CDMO.
The best choice depends on dosage form strategy, market channel, administration route, cold-chain handling, and lifecycle cost. For example, prefilled syringes may improve user convenience but can raise packaging complexity and component cost. Blow-fill-seal can offer integrated form-fill-seal efficiency for some liquid products, but it does not fit every biologic or premium sterile application. Vials remain highly versatile for hospital products, lyophilized products, and global distribution formats.
TechnologyBest ForStrengthTrade-OffLiquid vial filling machineSterile injectables, biologics, lyo-ready productsVersatility and broad market acceptanceRequires strong aseptic controlAmpoule lineSingle-dose sterile liquidsHermetic glass sealingLess flexible for some modern formatsPrefilled syringe lineConvenience products and self-administrationUser-friendly deliveryHigher component and line complexityBlow-fill-sealCertain sterile liquids at scaleIntegrated forming and fillingNot suitable for all product typesCartridge fillingPen injectors and specialty deliveryDevice compatibilityNarrower application rangeCDMO outsourcingEarly-stage or overflow productionLower initial capital outlayReduced direct process controlFor many United States manufacturers, vial filling remains the most balanced choice when flexibility, lyophilization compatibility, hospital use, and export readiness are priorities. The technology also scales well from clinical to commercial production if the line architecture is chosen carefully from the start.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Flexibility’, ‘Speed’, ‘Validation Ease’, ‘Operator Convenience’, ‘Format Versatility’, ‘Capital Efficiency’], datasets: [ { label: ‘Vial Filling’, data: [90, 82, 76, 72, 95, 80], backgroundColor: ‘#6f4e7c’ }, { label: ‘Prefilled Syringe’, data: [68, 74, 70, 93, 60, 58], backgroundColor: ‘#4c78a8’ }, { label: ‘BFS’, data: [55, 91, 65, 70, 50, 77], backgroundColor: ‘#f58518’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});This comparison chart shows why the vial format continues to hold strong appeal in regulated U.S. manufacturing: it offers a broad balance of flexibility, commercial practicality, and lifecycle fit.
The U.S. market for liquid vial filling equipment is supported by steady growth in biologics, sterile generics, vaccine preparedness, onshoring initiatives, and modernization of legacy injectable plants. Capital spending is being directed not only toward new greenfield facilities but also toward brownfield upgrades that improve line containment, digital integration, and cleanroom performance.
Several drivers are shaping the market:
In 2026, buyers are expected to put even more attention on robotics, machine vision, predictive maintenance, digital twins for FAT and SAT preparation, and modular line design. Policy and procurement trends in the United States also favor stronger domestic readiness, dual-source strategies, and systems that can demonstrate easier qualification and audit support. Environmental design is becoming a board-level topic as companies seek lower utility consumption and smarter cleanroom airflow management.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘U.S. market growth index’, data: [100, 108, 117, 128, 139, 151], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});The line chart illustrates a realistic upward trajectory as pharmaceutical manufacturers in hubs such as New Jersey, Texas, and the Midwest continue to add or refurbish sterile capacity.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [ { label: ‘Manual intervention dependent lines’, data: [62, 58, 52, 46, 40, 34], fill: true, backgroundColor: ‘rgba(225, 87, 89, 0.25)’, borderColor: ‘#e15759’, tension: 0.25 }, { label: ‘Automated barrier or isolator lines’, data: [38, 42, 48, 54, 60, 66], fill: true, backgroundColor: ‘rgba(118, 183, 178, 0.25)’, borderColor: ‘#76b7b2’, tension: 0.25 } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, stacked: false } } }});The area chart reflects a clear shift toward higher automation and stronger contamination control strategies, a trend likely to intensify through 2026 as labor efficiency and inspection readiness remain top priorities.
Choosing a supplier is as important as choosing the machine itself. In the United States, a reliable manufacturer should be able to demonstrate regulatory awareness, engineering depth, proven references, and practical after-sales responsiveness. This is especially important when installation schedules are tight and project teams must coordinate utility connections, FAT, SAT, validation protocols, and operator training across different time zones and functions.
Start with a structured qualification process. Review whether the supplier understands sterile process design, can provide documentation aligned with FDA expectations, and has experience with integrated projects rather than only stand-alone equipment shipments. Ask how they handle change control, spare parts planning, software backup, and long-term support.
Supplier Evaluation PointWhat to AskWhy It MattersCompliance knowledgeCan they support FDA cGMP-aligned documentation?Reduces validation and audit frictionReference projectsDo they have sterile line installations in regulated markets?Shows practical execution abilityCustomization depthCan they match your vial sizes, products, and layout?Avoids poor fit and expensive retrofitsFactory capabilityWhat manufacturing resources and testing systems exist?Indicates reliability and quality controlService responseHow do they handle commissioning and troubleshooting?Directly affects uptimeLifecycle supportCan they assist with training, spare parts, and upgrades?Protects long-term ROIManufacturing capability should also be reviewed carefully. IVEN Pharmatech Engineering, for instance, highlights multiple specialized manufacturing plants in Shanghai dedicated to filling and packaging machinery, water treatment systems, intelligent conveying and logistics, and blood collection tube equipment. For U.S. buyers, that kind of production depth can be meaningful because it suggests stronger vertical integration, broader technical coordination, and more consistent fabrication quality across a full line package.
If your project involves not only equipment procurement but also layout review, utility planning, and validation pathway design, it helps to assess whether the supplier can support turnkey work. Buyers can review turnkey pharmaceutical engineering solutions to understand how an integrated partner may reduce interface risk between machines, clean utilities, and facility systems.
Finally, evaluate communication discipline. A good supplier should provide clear URS feedback, layout drawings, FAT protocols, spare parts recommendations, software architecture notes, and escalation contacts. In a cross-border project serving the United States, communication speed often becomes a hidden differentiator.
The investment cost of a liquid vial filling machine varies widely based on output, sterility concept, line integration, isolator use, inspection automation, software scope, and validation deliverables. For a U.S. buyer, the budget should include much more than the machine base price. Freight, customs, installation, cleanroom modifications, utility tie-ins, FAT travel, SAT, validation support, spare parts, training, and first-year maintenance must all be included in the project model.
Brownfield upgrades in older injectable plants can cost more than expected because layout constraints, ceiling height, HVAC balance, and material flow changes add complexity. Greenfield projects may benefit from cleaner line design but usually involve broader capital planning.
Cost ElementLow Complexity ProjectHigher Complexity ProjectBudget NoteBase filling machineModerateHighDepends on speed and automationWashing and depyrogenation integrationOptionalCommonMajor line cost driverIsolator or RABSLower with open RABSHigher with isolatorImproves sterility assuranceValidation documentationBasic packageExpanded packageDo not underbudget documentationFacility modificationLimitedSubstantialOften underestimated in old plantsTraining and serviceStandardExtendedImportant for smooth startupROI typically comes from several areas:
In practical terms, a U.S. facility may justify investment if the new line replaces manual interventions, boosts OEE, supports higher-margin products, or shortens commercialization timelines. Companies comparing suppliers sometimes use a weighted scorecard including acquisition cost, expected uptime, validation burden, operating cost, and expansion capability. That approach often gives a truer picture than comparing quoted prices alone.
Prospective buyers can also review available equipment categories through the product catalog and machinery overview when building an early-stage budget range for sterile filling, utilities, and related systems.
The biggest purchasing mistakes usually happen when decision-makers focus on nominal speed while overlooking product-specific, regulatory, and site-specific realities. A liquid vial filling machine may look ideal on paper but become difficult to validate, clean, maintain, or integrate if the buying team does not assess the full lifecycle.
Risk AreaCommon ProblemPotential ConsequenceHow to Reduce RiskURS definitionIncomplete technical requirementsMismatch between machine and processBuild detailed cross-functional URSFacility fitPoor layout and utility alignmentInstallation delays and added costRun early layout and utility reviewsValidation scopeUnderestimated documentation needsDelayed startupDefine DQ, IQ, OQ, PQ package earlyOperator interventionToo much manual handlingHigher contamination riskPrioritize automation and barrier systemsSpare parts planningLimited stocking strategyLong downtimeOrder critical spare kits in advanceService coordinationWeak post-installation supportSlow troubleshootingSet response terms before purchaseOther risks include inaccurate assumptions about vial supply quality, stopper compatibility, particulate control, and environmental monitoring integration. U.S. plants importing equipment through coastal ports should also plan for logistics timing, inland transport, and site readiness to avoid costly idle periods after arrival.
Service capability can make a major difference after commissioning. IVEN Pharmatech Engineering positions itself around full lifecycle support, including project consulting, engineering design, equipment selection, installation, commissioning, validation assistance, staff training, documentation support, and optimization. For buyers in the United States, that service model can help reduce common project issues such as schedule slippage, layout inefficiency, and fragmented supplier accountability.
Before contract award, create a written checklist covering FAT criteria, acceptance sampling, alarm handling, batch reporting, recipe management, cyber access control, and preventive maintenance expectations. That level of detail pays off later.
1. What products are most commonly filled with a liquid vial filling machine in the United States?Common products include sterile injectables, antibiotics, biologics, vaccines, specialty hospital drugs, clinical trial materials, and diagnostic reagents.
2. Is an isolator always necessary?Not always. The need depends on product risk, sterility strategy, operator intervention profile, and site policy. However, isolator-based systems are increasingly favored for high-value sterile applications and future-oriented facilities.
3. Which filling method is best for sensitive biologics?Peristaltic or other gentle low-shear approaches are often selected, but the best method depends on viscosity, foaming behavior, hold-up volume, and cleaning strategy. Product trials are essential.
4. How long does a typical project take?Lead time varies by customization level and validation scope. A regulated U.S. project may include design review, fabrication, FAT, shipping, installation, SAT, and qualification, often stretching across several months to more than a year.
5. What documentation should a buyer request?Request layout drawings, P&ID where relevant, material certificates, component lists, software descriptions, FAT/SAT protocols, calibration records, manuals, and qualification support documentation aligned with your validation plan.
6. How important is integration with other systems?Very important. A vial filling machine should be assessed as part of the full process path, including washing, depyrogenation, stoppering, capping, inspection, clean utilities, and data systems.
7. Can one machine handle multiple vial sizes?Yes, many systems can. But change parts, recipe setup, format range, and changeover time should be reviewed carefully during supplier evaluation.
8. What should U.S. buyers look for in a manufacturer?Look for compliance expertise, proven sterile references, strong fabrication quality, clear validation support, responsive service, and the ability to customize around your facility and product requirements.
9. How does IVEN fit into this market?IVEN Pharmatech Engineering is active as an international pharmaceutical engineering partner with experience in filling and packaging machinery, utilities, logistics, and turnkey projects. Its profile is especially relevant for buyers who prefer integrated thinking across equipment, clean utility systems, and factory planning rather than a stand-alone machine-only transaction.
10. Where can a buyer start a discussion?If you are evaluating a line for a U.S. expansion, retrofit, or greenfield plant, you can begin by requesting project guidance through the contact page for technical consultation and then align the discussion around product type, throughput, facility conditions, and compliance objectives.
In summary, a liquid vial filling machine remains one of the most strategically important investments in sterile pharmaceutical manufacturing. For the United States market, the best buying decision comes from balancing compliance, product fit, automation, lifecycle service, and long-term expansion potential. Companies that take a disciplined, process-driven approach to supplier selection are better positioned to protect both regulatory performance and commercial return.
-
Syringe Assembly Machine Guide for the United States
In the United States, a syringe assembly machine is an automated production system used to assemble syringe components with speed, precision, traceability, and regulatory control. Large pharmaceutical manufacturers, contract development and manufacturing organizations, and medical device companies evaluate these systems when they expand capacity, launch prefilled products, reduce labor dependency, or upgrade aging equipment to meet stricter quality standards. For U.S. operations in Boston, New Jersey, Chicago, Houston, San Diego, and other major life sciences hubs, the decision is not just about buying a machine. It is about building a validated, scalable, FDA-ready production platform that supports product quality, operator safety, and long-term return on investment.
Syringe assembly equipment can serve multiple product strategies, from standard disposable syringes to prefilled syringe platforms used in biologics, vaccines, injectable generics, and specialty therapies. Depending on the project scope, buyers may require standalone assembly stations, semi-automatic lines, or high-speed fully integrated systems linked to washing, siliconization, needle insertion, plunger assembly, printing, vision inspection, labeling, packaging, and data collection. The right solution depends on format complexity, expected annual output, cleanroom class, validation expectations, available floor space, and the reliability of the engineering partner.
For companies planning new capacity in the United States, it is increasingly important to work with suppliers that understand not only mechanics and automation, but also documentation, installation qualification, operational qualification, performance qualification, and lifecycle service. This is where an experienced engineering company can add value beyond the machine itself. IVEN Pharmatech Engineering is known internationally for pharmaceutical and medical device engineering, combining equipment design with turnkey thinking, regulatory awareness, and practical factory execution. That combination matters when a syringe line must fit into a larger manufacturing strategy rather than operate as an isolated piece of equipment.
A syringe assembly machine matters because it directly affects throughput, dimensional accuracy, contamination control, and compliance. In U.S. manufacturing, especially under FDA cGMP expectations, assembly steps that were once manual are increasingly automated to lower variability and strengthen data integrity. Whether a company produces disposable medical consumables or prefilled delivery systems, automation reduces the risk of human error in critical operations such as barrel feeding, plunger insertion, needle mounting, cap placement, force control, leak-sensitive joining, vision inspection, and reject management.
In practical terms, a modern syringe assembly machine can help a plant in New Jersey or North Carolina move from labor-intensive production toward consistent, documentable output. It can also support reshoring strategies and improve resilience when labor markets are tight. U.S. buyers often compare total equipment effectiveness, changeover time, spare parts availability, electronic batch records compatibility, and ease of validation. The machine must work reliably inside a broader quality system.
Decision Factor Why It Matters U.S. Buyer Priority Regulatory compliance Supports cGMP, validation, and audit readiness Very high Automation level Reduces manual intervention and error risk High Output capacity Matches forecast demand and utilization goals High Product flexibility Allows multiple syringe sizes or formats High Traceability Improves quality records and deviation control Very high Service support Reduces downtime and speeds issue resolution Very highThe table above shows why U.S. procurement teams usually look beyond price. A lower-cost machine can become expensive if it lacks proper validation documents, stable software architecture, or long-term maintenance support.
A syringe assembly machine is a specialized automated system that brings together syringe parts in a controlled sequence. Depending on the application, these parts may include the barrel, plunger rod, stopper, needle, luer lock component, safety shield, finger flange, backstop, cap, and labeling or coding elements. In pharmaceutical production, the machine may also be integrated with upstream and downstream processes such as nest handling, clean air protection, sterile transfer logic, inspection, and secondary packaging.
In medical consumables manufacturing, the focus is often on high output and dimensional consistency. In pharmaceutical applications, especially with prefilled syringes, the focus expands to include particulate risk reduction, component compatibility, aseptic design, and container closure integrity. Assembly machines may operate in ISO-classified cleanroom environments and can be configured with servo systems, force monitoring, rejection stations, and machine vision to verify correct insertion depth, alignment, and component presence.
Typical users in the United States include:
At the engineering level, the best systems are designed for repeatability, cleanability, and digital integration. IVEN Pharmatech Engineering has built its reputation in pharmaceutical innovation by combining process equipment know-how with compliance-oriented design. Its broader experience in filling, packaging, purified water, logistics systems, and medical consumables is relevant because syringe assembly lines often need to connect with surrounding plant utilities, material flow, and qualification planning rather than stand alone.
The main applications of syringe assembly machines span both medical device and pharmaceutical sectors. In the United States, demand comes from vaccine delivery systems, insulin and GLP-1 related injection platforms, emergency medicine formats, flush syringes, diagnostic sampling products, and prefilled systems used in specialty biologics. Buyers also use these machines when they need to improve throughput after product approvals or when hospital contracts require more reliable domestic capacity.
Key benefits include:
For example, a manufacturer shipping to major U.S. distribution points such as Los Angeles, Savannah, Newark, and Houston can benefit from predictable output and lower deviation rates, especially when demand surges. Automation also supports business continuity planning because the plant is less exposed to manual labor shortages.
Application Segment Typical Product Main Benefit of Automation Disposable medical syringes Standard injection syringes High-speed production and lower labor cost Prefilled syringes Biologics and specialty injectables Better consistency and traceability Vaccine delivery Ready-to-use syringe formats Rapid scale-up capability Hospital flush products Saline or heparin flush systems Reliable batch output and packaging flow Diagnostic and sampling devices Specialized collection formats Precision assembly of multiple parts Safety syringe systems Needlestick protection formats Accurate insertion and functional testingThe benefits in the table are not theoretical. They affect scrap costs, complaint rates, maintenance schedules, and customer confidence. For heavily regulated products, consistent assembly quality is a strategic advantage, not just an operational improvement.
var ctx1 = document.getElementById(‘lineChartMarketGrowth’).getContext(‘2d’);var chart1 = new Chart(ctx1, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Syringe Assembly Market Growth Index’, data: [100, 108, 117, 129, 141, 156], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart indicates how investment interest has continued to rise. Growth is being driven by injectable therapies, domestic manufacturing initiatives, and the modernization of older assembly assets.
There is no single universal syringe assembly machine. U.S. buyers generally evaluate systems by automation level, sterility requirements, output range, format flexibility, and integration scope. A startup medical device company in Austin may need a compact semi-automatic machine for pilot volumes, while an established pharmaceutical plant near Philadelphia may need a fully automatic line integrated with inspection and packaging.
Common equipment categories include:
Technical options often include machine vision, force-displacement monitoring, robotic pick-and-place units, HEPA-protected enclosures, SCADA integration, MES connectivity, reject segregation, tool-less change parts, and recipe-driven changeover settings. These features become important when a company runs multiple SKUs or expects future line expansion.
Machine Type Output Range Best Fit Semi-automatic bench or compact system Low R&D, pilot, niche products Automatic linear assembly line Medium Flexible multi-format production Automatic rotary assembly line Medium to high Stable repetitive high-volume output Integrated prefilled syringe module Medium to high Pharmaceutical sterile applications Safety syringe assembly system Medium Advanced device configurations Turnkey line with packaging integration High Large plants and expansion projectsWhen buyers compare these options, they should focus on the target product first, then evaluate speed. A machine that runs extremely fast but cannot handle component variation, inspection requirements, or future format changes may not be the best long-term choice.
Alternative approaches include manual assembly, modular workstations, outsourced production, and retrofitted legacy equipment. Each has a place, but they serve different business cases. Manual assembly may work for very small volumes or prototyping. Outsourcing may reduce upfront capital but can increase supply chain dependency. Retrofitting a legacy machine can be cost-effective when the core platform is mechanically sound, but it may not solve limitations in data integrity, parts availability, or compliance documentation.
For United States buyers, the choice often depends on three questions: How fast must capacity come online? How strict are the quality and validation requirements? How likely is future product diversification?
Solution Capital Cost Scalability Compliance Readiness Labor Dependence Manual assembly Low Low Limited Very high Semi-automatic assembly Moderate Moderate Moderate Medium Fully automatic assembly machine High High High Low Outsourced production Low initial Depends on contractor Depends on contractor Low internal Legacy retrofit Moderate Limited to existing design Variable Medium Turnkey integrated line High Very high Very high LowThe table makes one point clear: the best fit is rarely the cheapest entry option. If your plant is shipping nationally through hubs such as Memphis, Chicago, or Atlanta, downtime and quality escapes can cost more than the difference between equipment classes.
var ctx2 = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, { type: ‘bar’, data: { labels: [‘Biologics’, ‘Vaccines’, ‘Hospital Supplies’, ‘Generics’, ‘Diagnostics’, ‘Safety Devices’], datasets: [{ label: ‘Estimated U.S. Demand Score’, data: [92, 84, 76, 68, 61, 73], backgroundColor: [ ‘rgba(255, 99, 132, 0.7)’, ‘rgba(54, 162, 235, 0.7)’, ‘rgba(255, 206, 86, 0.7)’, ‘rgba(75, 192, 192, 0.7)’, ‘rgba(153, 102, 255, 0.7)’, ‘rgba(255, 159, 64, 0.7)’ ] }] }, options: { responsive: true, maintainAspectRatio: false }});The bar chart highlights why biologics and vaccine-related formats are influencing machine design. Suppliers increasingly need to provide flexible, high-control systems that can support demanding injectable products.
The U.S. market for syringe assembly machinery is shaped by injectable drug growth, medtech innovation, domestic supply chain planning, and quality modernization. Pharmaceutical clusters in Massachusetts, California, New Jersey, Pennsylvania, North Carolina, and Indiana continue to invest in advanced manufacturing assets. At the same time, contract manufacturers are expanding to capture outsourced sterile and device-related production.
Several market forces are especially important:
Looking toward 2026, buyers should expect more interest in smart servo platforms, predictive maintenance, recipe management, remote diagnostics, and compact footprints for urban production sites. Policy trends may continue to favor resilient domestic manufacturing, while sustainability requirements will push manufacturers toward lower compressed air consumption, cleaner lubrication strategies, and more efficient reject reduction programs.
var ctx3 = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var chart3 = new Chart(ctx3, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Manual/Semi-Automatic Share’, data: [48, 44, 39, 34, 29, 25], borderColor: ‘rgb(201, 203, 207)’, backgroundColor: ‘rgba(201, 203, 207, 0.25)’, fill: true, tension: 0.3 }, { label: ‘Fully Automated Share’, data: [52, 56, 61, 66, 71, 75], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.25)’, fill: true, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The area chart shows the ongoing shift from manual and semi-automatic methods toward higher automation. That shift is not only about speed. It is tied to compliance, labor availability, and the need for reliable production data.
On the technology side, IVEN Pharmatech Engineering is relevant to this trend because it operates across multiple pharmaceutical equipment categories, not just a single machine type. Its engineering background in filling, packaging, water systems, intelligent logistics, and medical consumables supports projects where line integration and plant-wide coordination matter. Companies exploring broader capacity expansion can review turnkey pharmaceutical solutions when considering how syringe assembly fits into a larger factory investment.
Choosing a reliable supplier is one of the most important decisions in the project. U.S. buyers should evaluate more than the brochure. A strong supplier should demonstrate technical depth, manufacturing discipline, documentation capability, and after-sales responsiveness. If the line will be installed in a cGMP environment, the supplier must also understand qualification packages, FAT and SAT execution, and the level of detail expected by quality and validation teams.
Key selection criteria include:
A practical approach is to issue a detailed user requirement specification, compare supplier deviations carefully, and ask how each vendor manages component tolerances, rejects, line clearance, and preventive maintenance. Buyers should also assess factory capacity. A supplier with strong engineering but weak manufacturing discipline can create delivery delays or quality inconsistencies.
Supplier Evaluation Point What to Ask Why It Matters Application experience Have you built lines for similar syringe formats? Reduces design risk Compliance support What validation documents are standard? Speeds qualification Automation architecture Which PLC, HMI, and data options are offered? Improves integration Manufacturing capability How are critical parts produced and inspected? Supports machine reliability Service coverage What are response times and spare parts plans? Limits downtime Project management Who handles schedule, FAT, SAT, and training? Improves delivery successManufacturing capability is especially important. IVEN Pharmatech Engineering has developed specialized production resources through multiple manufacturing plants focused on pharmaceutical filling and packaging machinery, water treatment systems, intelligent conveying and logistics, and blood collection tube equipment. For U.S. buyers, that kind of industrial base can be meaningful because it suggests the supplier is not relying solely on outsourced assembly. It also supports broader customization and project coordination.
If you are comparing options, it is useful to review available equipment categories directly through the supplier’s pharmaceutical equipment portfolio and ask how each platform can be adapted for U.S. regulatory and utility requirements.
Investment cost varies widely based on automation level, speed, number of assembly stations, inspection scope, cleanroom design, validation package depth, and integration with upstream or downstream systems. In the United States, budgeting should include not only the base machine price but also freight, customs, installation, utility hookup, cleanroom modifications, software validation, training, spare parts, and startup losses during ramp-up.
Many projects underestimate indirect costs. A fully automatic syringe assembly line may need floor reinforcement review, controlled environmental upgrades, compressed air improvement, central monitoring connectivity, and additional quality resources for protocol execution. If the line is linked to packaging, material handling, or warehousing, interfaces must also be budgeted.
Typical ROI drivers include:
Cost Element Low Complexity Project High Complexity Project Base machine or line Moderate Very high Tooling and change parts Low to moderate Moderate Validation documentation Moderate High Installation and commissioning Moderate High Cleanroom or facility upgrades Low High Training and spare parts Moderate Moderate to highAs a rule, companies should model best case, expected case, and delayed ramp-up scenarios. A project with a longer qualification period may still outperform a cheaper option if the line reaches stable commercial output with fewer deviations. For buyers expanding in major trade corridors such as the Northeast, Gulf Coast, or Midwest, robust ROI should be linked to market access, not only labor savings.
var ctx4 = document.getElementById(‘comparisonChartSupplierFactors’).getContext(‘2d’);var chart4 = new Chart(ctx4, { type: ‘bar’, data: { labels: [‘Compliance Support’, ‘Customization’, ‘Factory Capacity’, ‘Lifecycle Service’, ‘Integration Ability’, ‘Cost Efficiency’], datasets: [{ label: ‘High-Value Supplier Score’, data: [95, 88, 90, 92, 89, 84], backgroundColor: ‘rgba(153, 102, 255, 0.75)’ }] }, options: { responsive: true, maintainAspectRatio: false }});The comparison chart shows how procurement teams often weigh supplier value. A vendor with balanced strength across compliance, customization, manufacturing, and service usually delivers better long-term results than one competing on price alone.
Every equipment project carries risk. The most common errors are under-specifying the product requirements, overestimating speed without confirming component quality, and underestimating qualification time. In U.S. pharmaceutical and medical device environments, line acceptance depends on more than speed at FAT. It depends on stable performance under real production conditions.
Major risks include:
To reduce these risks, buyers should conduct component studies early, define user requirements precisely, and involve engineering, QA, validation, production, and procurement from the start. Factory acceptance testing should use representative components and challenge scenarios, not just ideal conditions. Site acceptance should include operator training, maintenance routines, and clear escalation paths.
Service capability also deserves close attention. IVEN Pharmatech Engineering promotes a lifecycle approach that goes beyond equipment shipment, including project planning, installation support, commissioning, validation assistance, training, documentation, and optimization. For U.S. buyers, this matters because the real test of a supplier begins after the machine arrives. Fast troubleshooting and clear technical communication can protect the investment during startup and commercial scale-up. Companies needing direct discussion can use the U.S.-focused contact channel to review project scope, documentation expectations, and service arrangements.
Another important issue is future readiness. By 2026, investment decisions are likely to be influenced by sustainability metrics, digital traceability, and resilience planning. A machine that cannot support data connectivity, energy optimization, or future format expansion may age quickly. Buyers should therefore consider the line’s upgrade path, not just the initial configuration.
What production speed should a U.S. buyer target?The answer depends on product format, annual demand, and line utilization assumptions. It is better to choose a realistic validated speed with stable quality than a higher theoretical speed that is rarely achieved in practice.
Can one machine handle multiple syringe sizes?Yes, many modern systems can be configured for multiple sizes, but changeover design, tooling, recipes, and validation complexity should be reviewed carefully before purchase.
Is a syringe assembly machine only for pharmaceutical companies?No. Medical device manufacturers, hospital supply producers, contract manufacturers, and diagnostic product companies also use these systems.
What documents should be requested from the supplier?Common requirements include design documents, material certificates for critical contact parts, FAT protocols, operation manuals, wiring diagrams, spare parts lists, calibration records, and IQ/OQ support documentation.
How long does implementation usually take?Timing varies by customization level. A simpler project may move faster, while a fully integrated validated line can take significantly longer when facility modifications and QA approvals are included.
Should I buy a standalone machine or a turnkey line?If your process is narrow and existing utilities and packaging are already in place, a standalone system may be enough. If you are building or expanding a full production area, a turnkey approach often reduces interface risk.
How important is supplier manufacturing strength?Very important. Consistent machining, assembly quality, and testing discipline affect long-term reliability, spare parts fit, and maintenance performance.
What makes a supplier credible for the United States market?A credible supplier should understand FDA-oriented expectations, provide strong documentation, support qualification, communicate clearly in English, and demonstrate successful international project execution.
Can imported equipment still be a good fit for U.S. plants?Yes, if the supplier has solid compliance knowledge, dependable project management, and a practical service plan. Many U.S. buyers focus on total project value rather than country of origin alone.
Why do some companies choose IVEN Pharmatech Engineering?Because they want a partner that combines equipment capability with broader pharmaceutical engineering experience. The company is known for integrated solutions, customization, international compliance awareness, and a manufacturing base that supports not only machine supply but also larger factory planning.
In summary, a syringe assembly machine is a strategic investment for companies seeking quality, capacity, and regulatory confidence in the United States. The right choice depends on product requirements, supplier capability, validation needs, and future growth plans. Buyers that take a structured approach to specification, supplier assessment, and lifecycle planning usually achieve better technical and financial outcomes.
-
Cartridge Filling Machines for United States Pharma
For pharmaceutical and medical device manufacturers in the United States, a cartridge filling machine is not just a packaging asset. It is a regulated production platform that directly affects dose accuracy, sterility assurance, throughput, validation workload, and long-term operating cost. Companies in markets such as New Jersey, Massachusetts, California, Texas, and North Carolina often assess cartridge filling systems when launching injectable drugs, biologics, dental anesthetics, ophthalmic products, and device-drug combination products. In practice, the right system can help shorten scale-up time, support FDA expectations, reduce operator intervention, and prepare a plant for future automation.
A cartridge filling machine is specialized equipment designed to wash or prepare, fill, stopper, cap, inspect, and sometimes label cartridges used for sterile pharmaceutical products. In the United States, the machine is commonly evaluated by larger pharmaceutical companies, CDMOs, and medical device manufacturers that need high precision under US FDA cGMP requirements. It is especially important when a facility is expanding a sterile line, replacing labor-intensive manual filling, or converting to a more automated process that improves contamination control and batch consistency.
Compared with generic liquid filling equipment, cartridge-specific systems are engineered around the geometry, sealing behavior, and handling sensitivity of glass or polymer cartridges. This matters when dealing with high-value formulations, shear-sensitive biologics, viscous products, or products that must be delivered through pen injectors and related delivery systems. In major U.S. life-science corridors such as Boston, Philadelphia, Chicago, and the San Francisco Bay Area, companies increasingly favor integrated solutions that combine filling, stoppering, capping, in-process controls, and data collection.
For organizations planning a new line or a turnkey facility, the choice of supplier can be as important as the machine design. Many buyers look for partners able to support engineering, layout development, FAT/SAT, IQ/OQ/PQ documentation, training, and after-sales support. Companies reviewing international suppliers often compare technical depth, regulatory understanding, and lifecycle service. A useful starting point is to review a supplier’s corporate background and regulatory experience before moving into URS discussions.
A cartridge filling machine is a production system used to dose sterile liquid or semi-liquid pharmaceutical formulations into cartridges, followed by component placement and closure. These cartridges may later be assembled into pen injectors, dental syringes, or specialty drug-delivery systems. The machine is typically installed in aseptic processing areas, often integrated with isolators, RABS, laminar airflow systems, or other contamination control strategies.
Its core purpose is to fill a defined volume repeatedly and safely while protecting product quality. Depending on the line design, the process may include cartridge infeed, air cleaning or washing, depyrogenation interface handling, nitrogen purging, filling by peristaltic or piston pump, plunger insertion, capping, crimping, check weighing, visual inspection, reject handling, and batch data recording. Higher-end platforms also include no-container-no-fill logic, automatic format change support, recipe management, and 21 CFR Part 11-compatible data handling through upstream or supervisory systems.
In pharmaceutical production, cartridge filling machines are used for insulin products, GLP-1 therapies, hormonal drugs, local anesthetics, biologics, ophthalmic preparations, and selected veterinary injectables. They are also used in device combination manufacturing where the cartridge is part of the final administration system. This makes them particularly valuable for companies serving hospitals, retail pharmacy channels, specialty clinics, and home-use drug delivery markets across the United States.
Process StepFunctionWhy It MattersTypical U.S. ConcernCartridge feedingMoves empty cartridges into the linePrevents jams and breakageHigh OEE and reduced manual handlingCleaning or preparationRemoves particles or prepares containersSupports sterility and product safetyContamination control expectationsPrecision fillingDispenses accurate product volumeControls dose uniformityYield and batch release compliancePlunger insertionPlaces stopper or plunger correctlyEnsures container closure integrityLeak prevention and transport stabilityCapping/crimpingSecures final closureProtects product after fillingDownstream device compatibilityInspection and rejectionDetects fill, closure, or cosmetic defectsImproves final qualityLower deviation and recall riskThe table above shows why cartridge filling is more than a simple dosing task. Every process step affects compliance, throughput, and final product performance.
Cartridge filling technology has gained relevance as injectable therapy portfolios expand in the United States. The strongest growth is visible in chronic disease therapies, self-administration devices, and specialty biologics. Pharmaceutical plants near Newark, Raleigh-Durham, Indianapolis, and San Diego often consider cartridge systems when a product pipeline includes delivery devices or premium injectable formats.
The main applications include insulin and diabetes-related formulations, biologics for autoimmune disorders, fertility products, dental anesthetics, cosmetic medicine injectables, and niche hospital products. CDMOs are also investing in flexible cartridge lines because customers increasingly want smaller batch sizes in development followed by rapid commercial scale-up.
The benefits usually fall into five categories: precision, sterility, productivity, compatibility, and traceability. Precision reduces product giveaway and supports label claim. Sterility-focused design lowers contamination risk through enclosed processing and reduced touchpoints. Productivity improves through continuous motion or automated indexing systems. Compatibility supports different cartridge sizes and closure types. Traceability helps quality teams with audit readiness, batch review, and process investigation.
For companies that need broader plant integration, cartridge filling lines can be part of a larger sterile manufacturing strategy involving purified water, WFI systems, clean utilities, formulation, and final packaging. Buyers exploring full-factory planning sometimes review turnkey pharmaceutical engineering solutions rather than sourcing each subsystem separately.
Application AreaTypical ProductWhy Cartridges Are UsedMain BenefitDiabetes careInsulin and related therapiesDevice integration with pen systemsConvenient patient self-useBiologicsHigh-value sterile injectablesAccurate low-volume dosingReduced product lossDentalLocal anestheticsEstablished cartridge delivery formatReliable clinical administrationOphthalmicsSpecialized sterile liquidsControlled fill requirementsBetter process repeatabilityHormonal therapiesFertility and endocrine productsMulti-dose or device-linked useImproved dosage consistencyVeterinary pharmaceuticalsSelected injectable productsRobust packaging for field useOperational flexibilityThis table highlights why cartridge formats are favored where dosage reliability and delivery-system integration are important.
var ctx1 = document.getElementById(‘lineChartMarket’).getContext(‘2d’);var chart1 = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026’],datasets: [{label: ‘U.S. Cartridge Filling Equipment Demand Index’,data: [78, 84, 91, 102, 114, 128],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});Not every cartridge filling machine is built for the same production objective. In the U.S. market, buyers usually compare manual, semi-automatic, and fully automatic models first, then narrow their selection by sterility concept, speed, filling technology, container range, and digital integration level.
Entry-level or lab-scale units are suitable for R&D, clinical batches, and engineering trials. Semi-automatic systems can fit pilot plants or low-volume specialty manufacturing. Fully automatic lines are preferred for commercial aseptic production, especially where labor reduction, line clearance repeatability, and data integrity are major priorities.
Technical options often include:
For larger projects, it is also common to assess whether the line can be connected to upstream preparation systems, clean utilities, and downstream packaging automation. Suppliers with broad equipment portfolios may provide more standardized interfaces and fewer integration gaps across the plant.
Machine TypeOutput RangeBest ForAdvantagesManual bench unitVery lowR&D and trialsLow cost and fast setupSemi-automatic fillerLow to mediumPilot and niche productsMore control with modest investmentIntermittent automatic lineMediumCommercial specialty batchesGood balance of speed and flexibilityContinuous motion lineHighLarge-volume productionHigher throughput and efficiencyIsolator-integrated systemMedium to highHigh-sterility applicationsReduced human intervention riskMulti-format cartridge lineMedium to highCDMOs and mixed portfoliosFaster format adaptabilityThe right model depends less on headline speed than on your formulation, batch pattern, sterility strategy, and future expansion plan.
Many U.S. buyers compare cartridge filling machines with vial lines, prefilled syringe lines, ampoule lines, and flexible small-batch isolator fillers. The correct answer depends on the product presentation and commercial route to market.
Vials offer broad industry familiarity and strong flexibility, but they may not support the same patient-use convenience as cartridges in pen systems. Prefilled syringes are ideal for many single-dose products, though cartridges can be better for multi-dose or device-integrated applications. Ampoules remain relevant for some hospital markets but are less favored where breakage, opening steps, or device compatibility are concerns.
If a company expects strong growth in self-administration, adherence-focused drug delivery, or premium injectable formats, cartridge filling often becomes the better long-term choice. On the other hand, if the product is still in early development and packaging presentation is undecided, a highly flexible filling platform may offer lower near-term risk.
TechnologyStrengthLimitationBest FitCartridge filling machineDevice compatibility and dosing precisionSpecific component and format needsPen systems and premium injectablesVial filling lineWide market acceptanceLess patient-friendly final useHospitals and multi-purpose sterile linesPrefilled syringe lineReady-to-use convenienceMay be less suitable for some multi-dose usesSingle-dose self-injection productsAmpoule filling lineSimple container conceptOpening and breakage concernsTraditional injectable segmentsFlexible aseptic fillerDevelopment adaptabilityOften lower commercial speedClinical and early-stage productionOutsourced CDMO fillingReduced capital burdenLess internal control and scheduling dependenceCompanies without in-house sterile capacityThe table makes clear that cartridge technology is strongest when delivery format and long-term commercial positioning matter as much as filling itself.
var ctx2 = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Biologics’,’Diabetes Care’,’Dental’,’Ophthalmics’,’CDMO Projects’,’Veterinary’],datasets: [{label: ‘Estimated U.S. Demand by Segment’,data: [92, 110, 58, 49, 84, 36],backgroundColor: [‘#4dc9f6′,’#f67019′,’#f53794′,’#537bc4′,’#acc236′,’#166a8f’]}]},options: {responsive: true,maintainAspectRatio: false}});The U.S. market for cartridge filling equipment is supported by three structural drivers: growth in injectable therapies, expansion of device-based drug delivery, and modernization of domestic manufacturing capacity. Facilities near major ports and freight hubs such as Los Angeles, Houston, Savannah, New York/New Jersey, and Chicago increasingly consider equipment resilience, spare-parts planning, and dual-sourcing strategies as part of procurement decisions.
Large pharmaceutical companies, specialty manufacturers, and CDMOs are all active buyers. Domestic reshoring and supply chain diversification remain important themes, especially for firms seeking more control over sterile manufacturing. In addition, more projects now include digital monitoring, recipe management, predictive maintenance, and remote diagnostics.
Looking toward 2026, several trends are likely to shape buying decisions:
Policy expectations will also matter. Companies selling into the United States must continue aligning with FDA cGMP, data integrity practices, and evolving contamination control expectations. Buyers are increasingly asking suppliers not only for machine performance but also for documented support during qualification and ongoing lifecycle management.
var ctx3 = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var chart3 = new Chart(ctx3, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026’],datasets: [{label: ‘Shift Toward Automated and Isolator-Based Systems (%)’,data: [34, 39, 45, 53, 61, 69],borderColor: ‘rgb(153, 102, 255)’,backgroundColor: ‘rgba(153, 102, 255, 0.25)’,fill: true,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});Choosing a supplier in the United States market requires more than comparing quoted speed and price. Buyers should assess technical capabilities, manufacturing depth, quality systems, service organization, validation documentation, and actual experience with regulated projects.
Start with technical capabilities. A reliable supplier should demonstrate understanding of aseptic process design, filling accuracy, CIP/SIP or single-use options where relevant, alarm logic, reject handling, and line integration. They should also be able to discuss practical topics such as oxygen-sensitive formulations, viscosity range, plunger insertion force, and component feeding reliability.
Next, review manufacturing capabilities. Buyers should ask whether the supplier produces key modules in-house, what level of stainless-steel fabrication quality is used, how electrical and control cabinets are standardized, and whether FAT protocols reflect pharmaceutical expectations. Strong manufacturing control often translates into shorter debug cycles and more stable long-term performance.
Service capabilities are equally important. U.S. buyers often favor suppliers that can support feasibility review, layout planning, installation, commissioning, training, spare parts, remote troubleshooting, and qualification packages. A supplier with lifecycle support can reduce risk during both startup and commercial operations. If you are comparing options, it can help to explore available equipment categories through a supplier’s pharmaceutical machinery portfolio and then discuss the exact cartridge line configuration required.
Shanghai IVEN Pharmatech Engineering, for example, is often evaluated by global buyers because it combines engineering and equipment experience across pharmaceutical filling, water treatment, intelligent logistics, and medical device production systems. Its technological capabilities are relevant for regulated projects that require integrated thinking rather than stand-alone machine supply. Its manufacturing capabilities are supported by specialized production plants focused on core categories. Its service capabilities extend from design consultation and customization to commissioning, validation support, training, and after-sales assistance, which is particularly useful for companies trying to control schedule and compliance risk in the United States.
Evaluation PointWhat to AskGood SignRisk if WeakRegulatory understandingCan the supplier support FDA-focused documentation?Clear IQ/OQ/PQ and cGMP familiarityQualification delaysTechnical designHow is filling accuracy maintained?Validated dosing and stable controlsYield loss and deviationsManufacturing qualityWhich modules are built in-house?Strong fabrication and FAT controlInconsistent machine performanceProject executionWho manages installation and SAT?Defined milestones and experienced teamSchedule slippageSpare parts/serviceWhat is the support model for U.S. clients?Fast response and planned inventoryLong downtimeReference experienceHas the supplier served regulated global plants?Documented project track recordExecution uncertaintyThis framework helps purchasing, quality, engineering, and operations teams align around practical decision criteria.
Capital cost varies widely depending on output, sterility architecture, automation depth, component feeding complexity, and inspection requirements. A basic semi-automatic cartridge filler may fit a modest budget, while a fully integrated aseptic line with isolator, robotic handling, vision systems, and complete qualification support can require a multi-million-dollar investment.
In the United States, budget planning should include more than the machine invoice. Buyers need to account for shipping, import logistics, customs, line-side utilities, cleanroom modifications, FAT travel, SAT, commissioning, qualification, operator training, spare parts, consumables, and potential integration with SCADA or MES platforms. Sites near ports such as Long Beach, Newark, or Houston may have different freight timing and inland transport considerations than inland manufacturing campuses.
ROI should be measured against labor reduction, scrap reduction, higher throughput, lower deviation rates, better fill consistency, reduced contamination risk, and the ability to commercialize higher-value products. For some companies, the real payoff comes from faster regulatory readiness and improved launch timing rather than from labor savings alone.
Cost ElementLow Automation ProjectHigh Automation ProjectPlanning NoteCore equipmentModerateHighMain driver of budgetIsolator/RABSOptionalUsually includedMajor sterility-cost factorInstallation and SATModerateModerate to highDepends on site complexityQualification documentsBasicExtensiveImportant for FDA-regulated useTraining and serviceLimitedBroader lifecycle packageReduces startup riskSpare parts inventoryLowerHigherImportant for uptime assuranceThe table shows why initial machine price alone can be misleading. Total cost of ownership is a more accurate measure for investment decisions.
var ctx4 = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var chart4 = new Chart(ctx4, {type: ‘bar’,data: {labels: [‘Regulatory Support’,’Automation Depth’,’Customization’,’Lifecycle Service’,’Cost Efficiency’,’Integration Ability’],datasets: [{label: ‘Supplier Capability Comparison Index’,data: [90, 86, 88, 91, 84, 89],backgroundColor: ‘rgb(255, 159, 64)’}]},options: {responsive: true,maintainAspectRatio: false}});The biggest mistake buyers make is assuming a cartridge filling project is a simple equipment purchase. In reality, it is a process, compliance, and lifecycle decision. A machine can meet speed targets but still create issues if format parts are unstable, software access is poorly controlled, or validation support is incomplete.
Key considerations include product characteristics, batch size strategy, closure system reliability, line clearance design, operator ergonomics, changeover time, and environmental classification. If you manufacture sensitive biologics, pump selection and product-contact materials become critical. If you run multiple SKUs, format flexibility and recipe management may matter more than top-end speed.
Common risks include underestimated facility modifications, insufficient FAT scope, weak SAT planning, long lead times for components, lack of local support, and over-customization that complicates maintenance. Another risk is choosing a supplier without enough experience in regulated documentation, which can slow qualification and delay product launch.
For U.S. buyers, a prudent strategy is to define a detailed URS, align quality and engineering teams early, and insist on documented acceptance criteria. It also helps to involve a supplier that can support broader plant planning, especially if the cartridge line interfaces with clean utilities, formulation systems, logistics automation, or final packaging. When project teams need direct technical discussions, a practical next step is to contact an engineering and equipment specialist to review application requirements, production targets, and compliance expectations.
From a company perspective, IVEN’s value is usually strongest where buyers want a combination of technological capabilities, manufacturing capabilities, and service capabilities rather than a narrow machine-only transaction. Its engineering-based approach can be useful for U.S. manufacturers that need integrated planning, while its production background helps support durable machine construction. On the service side, training, installation, commissioning, and qualification support can lower operational risk during startup and scale-up.
1. What products are most commonly filled by a cartridge filling machine?Common products include insulin, biologics, hormonal injectables, dental anesthetics, ophthalmic solutions, and device-combination pharmaceuticals.
2. Is a cartridge filling machine always used for aseptic processing?Most pharmaceutical cartridge filling applications are sterile or aseptic, but the exact setup depends on the product and regulatory pathway. For U.S. pharmaceutical use, aseptic design and contamination control are usually central.
3. What output range should a United States manufacturer consider?It depends on batch size, market demand, and SKU count. High speed is valuable, but many facilities gain more from stable medium-speed production with fast changeovers and strong validation support.
4. How does cartridge filling compare with prefilled syringes?Cartridges are often preferred when the product is intended for pen systems or certain multi-dose/device-integrated applications. Prefilled syringes may be better for ready-to-inject single-dose presentations.
5. What documentation should buyers request from suppliers?Typical requirements include DQ support where applicable, FAT/SAT protocols, material certificates, calibration records, software and alarm descriptions, manuals, spare-parts lists, and IQ/OQ documentation packages.
6. Are imported cartridge filling machines suitable for U.S. compliance?Yes, if the supplier understands FDA expectations, follows good engineering practices, and provides proper documentation, validation support, and service. Compliance depends on execution, not nationality.
7. What are the main hidden costs in a project?Facility upgrades, cleanroom interfaces, utility connections, integration work, qualification effort, travel, spare parts, and operator training are often underestimated.
8. How important is local or remote after-sales support?Very important. Sterile production downtime is expensive. Fast technical support, available spare parts, and remote diagnostics can significantly improve lifecycle performance.
9. When should a company choose a turnkey partner instead of buying a stand-alone machine?A turnkey approach is often better when the project involves multiple systems such as sterile filling, water treatment, solution preparation, clean utilities, and packaging. It can reduce interface risk and simplify project coordination.
10. What should U.S. buyers look for in a long-term supplier relationship?Look for regulatory awareness, strong engineering, documented manufacturing quality, customization capability, training, service responsiveness, and a proven ability to support expansion as your portfolio grows.
In summary, a cartridge filling machine is a strategic investment for U.S. pharmaceutical and medical device manufacturers pursuing sterile precision, delivery-system compatibility, and scalable automation. The best decision comes from aligning product needs, regulatory requirements, plant infrastructure, and supplier capability. Companies that treat the purchase as part of a wider manufacturing strategy usually achieve stronger compliance, faster execution, and better long-term ROI.