United States Guide to IV Soft Bag Manufacturing
IV solution soft bag manufacturing is a strategic production technology used by pharmaceutical and medical device companies to produce sterile large-volume parenteral products in flexible containers. In the United States, it is especially relevant for manufacturers expanding hospital supply capacity, upgrading aging infusion packaging systems, improving compliance with US FDA cGMP requirements, and reducing logistics costs through lightweight non-PVC or multilayer bag formats. For companies serving markets such as New Jersey, North Carolina, Illinois, California, Texas, and Puerto Rico, a modern soft bag IV line can support scalable, automated, high-integrity sterile production while aligning with stricter expectations for validation, traceability, and efficiency.
When decision-makers assess a new line, they are usually not buying only one machine. They are evaluating a complete manufacturing system that may include film handling, bag forming, port insertion, solution preparation, sterile filling, sealing, leak detection, light inspection, overpouch packing, cartoning, intelligent conveying, and utility integration. This is why partner selection matters. Companies looking for an experienced engineering supplier often review firms with proven turnkey capability, regulatory familiarity, and installed projects across global pharmaceutical markets, such as IVEN Pharmatech Engineering, which is known in the industry for integrated pharmaceutical production solutions.
Quick Answer: Why IV solution soft bag manufacturing matters for pharmaceutical expansion

For pharmaceutical producers in the United States, IV solution soft bag manufacturing matters because it combines sterile packaging technology, automation, and compliance into one high-value production platform. Hospitals, infusion centers, dialysis providers, emergency stockpile programs, and contract manufacturers all rely on dependable supply of large-volume sterile solutions such as sodium chloride, dextrose, compound electrolyte solutions, irrigation fluids, and sometimes specialized formulations.
Soft bag systems are attractive because they are lightweight, efficient to ship, and often easier to store than glass bottles. They can also reduce breakage risk in distribution channels moving through major hubs like Los Angeles, Chicago, Savannah, Houston, and Newark. In modern production planning, the line is not judged only by output speed. It is also judged by sterility assurance level, sealing integrity, environmental monitoring compatibility, changeover efficiency, digital data capture, and lifecycle service support.
For large pharmaceutical manufacturers, the technology is usually evaluated in the context of capacity expansion, product diversification, replacement of legacy bottle lines, or development of a new sterile manufacturing site. For mid-sized companies and CDMOs, the main driver may be access to a profitable market segment with high recurring demand. In both cases, the business decision sits at the intersection of engineering, regulatory compliance, supply chain resilience, and return on investment.
| Decision Factor | Why It Matters | Impact on US Operations |
|---|---|---|
| Sterility assurance | Protects patient safety and supports validation | Critical for US FDA inspection readiness |
| Packaging flexibility | Supports multiple bag sizes and port designs | Useful for hospital and contract supply programs |
| Automation level | Reduces manual intervention and variability | Helps with labor constraints in US plants |
| Utility efficiency | Affects water, steam, HVAC, and energy use | Important in high-cost regions like California |
| Traceability | Supports batch records and audit trails | Needed for cGMP digital compliance trends |
| Service support | Limits downtime and speeds troubleshooting | Essential for nationwide distribution commitments |
The table above shows why soft bag production lines are considered board-level capital investments rather than routine packaging purchases. The right system influences quality, throughput, maintenance burden, and long-term competitiveness.
What IV solution soft bag manufacturing is and how it is used in pharmaceutical production

IV solution soft bag manufacturing refers to the integrated process and equipment used to produce sterile infusion solutions in flexible polymer bags. The line usually starts with pharmaceutical water generation and solution preparation, followed by filtration, bag forming or bag feeding, port welding or insertion, filling, sealing, terminal sterilization or aseptic processing depending on the product design, and final packaging.
In the United States, this technology is used for products that need consistent dosing accuracy, container closure integrity, visual cleanliness, and dependable shelf life. Common finished products include 100 mL, 250 mL, 500 mL, and 1000 mL infusion bags for saline, glucose, balanced electrolyte solutions, irrigation fluids, and dialysis-related solutions. Some lines are designed specifically for non-PVC bags to meet environmental or material compatibility goals, while others support multilayer films tailored to oxygen barrier and extractables performance.
The production workflow generally includes the following functions:
| Production Stage | Main Equipment | Purpose |
|---|---|---|
| Water and utility preparation | RO, purified water, WFI, pure steam systems | Provides compliant process media |
| Solution compounding | Mixing tanks, distribution loops | Prepares sterile formulation accurately |
| Bag formation | Film forming and sealing modules | Creates flexible primary container |
| Port insertion | Welding and insertion station | Adds administration and additive ports |
| Filling and sealing | Sterile filling heads and heat sealing units | Controls dose accuracy and closure |
| Inspection and packaging | Leak tester, vision system, overwrapper, cartoner | Confirms quality and prepares shipment |
This process can be deployed in greenfield plants, expansion modules, or retrofits of existing sterile facilities. Companies that require a broader integrated scope may seek a supplier with turnkey engineering experience in process design, clean utilities, logistics, validation, and documentation. More information on this type of integrated approach can be found in pharmaceutical turnkey project solutions.
From a technological capability standpoint, advanced suppliers are expected to provide automation architecture, recipe control, data collection, HMI design, alarm management, and compatibility with facility SCADA or MES layers. In the US market, buyers increasingly ask for CFR-ready electronic record architecture, robust IQ/OQ/PQ documentation, and compatibility with risk-based validation strategies.
Main applications and benefits in modern pharmaceutical manufacturing

The most important applications of IV solution soft bag manufacturing are found in hospital infusion products, emergency care fluids, ICU support solutions, surgical irrigation, renal care, and outsourced sterile manufacturing. Demand is driven by healthcare system scale, aging population trends, chronic disease management, and the need for secure domestic or near-domestic production capacity.
Benefits vary by producer type. A large branded pharmaceutical company may prioritize line reliability and regulatory confidence. A contract manufacturer may focus on format flexibility and fast campaign changeover. A public health supplier may prioritize output stability and packaging durability.
| Application Area | Typical Product | Main Benefit of Soft Bag Format |
|---|---|---|
| Hospital infusion therapy | 0.9% sodium chloride | Lightweight and easy handling |
| Emergency medicine | Dextrose solutions | Fast distribution and reduced breakage |
| Surgery and irrigation | Sterile irrigation fluids | Efficient storage and transport |
| Dialysis support | Specialized solution formats | Consistent sterile packaging |
| Contract manufacturing | Private label infusion products | Flexible size and SKU management |
| Government supply programs | Stockpile essential fluids | Scalable output for surge demand |
The table highlights how the same technology serves multiple commercial and public-health use cases. It is especially valuable in a market like the United States, where regional distribution efficiency matters. Shipping soft bags from production centers near Philadelphia, Indianapolis, Raleigh-Durham, or Dallas can lower handling complexity compared with heavier rigid containers.
Other important benefits include reduced packaging material weight, less breakage in transport, lower warehouse cube in some configurations, and better compatibility with automated secondary packaging. There are also sustainability advantages when film structures and process energy use are optimized. Looking ahead to 2026, environmental reporting and waste reduction targets are expected to influence material selection, line efficiency design, and packaging procurement strategy.
The line chart above illustrates a realistic growth pattern for the US IV soft bag market index, reflecting increasing demand, modernization investment, and resilience planning in sterile supply chains.
Key types, models, and technical options for IV solution soft bag manufacturing
There is no single universal line design. Equipment is selected according to product mix, planned output, sterilization strategy, film material, and facility layout. Buyers in the United States often compare semi-automatic expansion lines, fully automatic high-capacity lines, and turnkey plants with complete utilities and warehousing integration.
Typical technical options include single-chamber versus multi-chamber bag capability, non-PVC film processing, inline weight control, closed-loop filling accuracy correction, automatic rejection, 100% leak detection, machine vision inspection, robotic cartoning, and integration with warehouse logistics systems.
| Line Type | Typical Capacity | Best Fit |
|---|---|---|
| Pilot or development line | Low volume | R&D, validation batches, niche products |
| Mid-speed automatic line | Moderate volume | Regional supply and contract manufacturing |
| High-speed production line | Large volume | National hospital distribution |
| Multi-format line | Variable by SKU | Manufacturers with diverse portfolios |
| Turnkey integrated line | Scalable | Greenfield plants and major expansion |
| Smart factory line | Scalable with digital analytics | Companies pursuing Industry 4.0 goals |
From a manufacturing capability perspective, experienced suppliers stand out when they can deliver not just the core filling and sealing machine, but also upstream water treatment systems, solution preparation units, conveying systems, and downstream packing modules. Some engineering firms operate specialized manufacturing plants for different equipment families so they can control quality, consistency, and customization depth across the full project scope.
For US buyers, useful model options include:
- Bag sizes from 100 mL to 5000 mL depending on product and market
- Single or dual port configurations
- Inline CIP/SIP compatible design where appropriate
- Servo-controlled film transport for better dimensional consistency
- Particle-reducing mechanical layout with easy cleaning access
- Remote diagnostics and maintenance support
- Data export for electronic batch records
Companies comparing available systems may explore a broader equipment catalog through pharmaceutical equipment product offerings to understand configuration possibilities for sterile manufacturing facilities.
IV solution soft bag manufacturing compared with alternative technologies
Soft bag IV production is often compared with PP bottle lines, glass bottle lines, and outsourced fill-finish arrangements. Each option has strengths. The best solution depends on product profile, transport model, market expectations, and regulatory strategy.
| Technology | Advantages | Limitations |
|---|---|---|
| Soft bag IV line | Lightweight, lower breakage, efficient logistics | Film compatibility and seal integrity must be well managed |
| PP bottle line | Strong container structure, familiar format | Higher material bulk than soft bags |
| Glass bottle line | Excellent barrier and legacy acceptance | Heavy, fragile, higher transport burden |
| Outsourced production | Lower initial capital commitment | Less control over capacity and scheduling |
| Import-based sourcing | Can be quick to enter market | Supply chain disruption and tariff exposure |
| Hybrid model | Diversified risk | More complex quality oversight |
In the United States, manufacturers often keep more than one platform in operation. For example, a company may use soft bags for high-volume hospital products, PP bottles for selected formulations, and outsourced contracts for temporary demand peaks. The comparison should therefore focus on strategic fit rather than abstract superiority.
The comparison chart provides a practical view of how buyers may evaluate the main formats across major purchasing criteria. In many cases, soft bags score highest where shipping, storage, and hospital handling are central priorities.
Market overview and future trends in pharmaceutical manufacturing
The US market for IV solution packaging equipment is shaped by several forces: domestic pharmaceutical reshoring, pressure to stabilize essential medicine supply, growth in hospital demand, increasing contract manufacturing activity, and gradual modernization of sterile facilities. Regions with strong pharmaceutical footprints such as New Jersey, Massachusetts, Indiana, North Carolina, and Puerto Rico continue to be focal points for investment discussions.
Major ports and inland logistics hubs also matter. Equipment imported through Long Beach, Houston, Savannah, or Newark must be timed carefully with installation planning, site readiness, and factory acceptance or site acceptance milestones. This is one reason buyers increasingly prefer suppliers who can coordinate engineering, manufacturing, shipment, installation, validation, and operator training under one project structure.
Three future trends are especially important for 2026:
- Digital validation and data integrity expectations will rise. Systems with better audit trails, recipe security, and electronic documentation support will be favored.
- Sustainability pressures will increase. Material reduction, energy-efficient utilities, and lifecycle maintenance planning will become stronger buying criteria.
- Policy and resilience planning will influence sourcing. Domestic production expansion and diversified supply chains will remain major themes for essential sterile products.
The area chart shows the expected shift toward more automated and sustainability-oriented line designs. This trend is consistent with broader pharmaceutical capital planning across the United States.
How to choose a reliable manufacturer or supplier
Choosing a reliable IV solution soft bag manufacturing supplier requires more than checking machine speed. The best supplier is one that reduces project risk from feasibility through long-term operation. In the United States, the most successful projects are usually awarded to companies that demonstrate strong regulatory understanding, documented installation history, responsive service, and the ability to customize around process realities rather than only sell standard equipment.
Buyers should assess suppliers across technological capabilities, manufacturing capabilities, and service capabilities.
On the technology side, look for expertise in sterile process integration, automation, water systems, solution preparation, filling accuracy, sealing consistency, and inspection. On the manufacturing side, review plant specialization, quality control standards, materials of construction, traceability of components, and capacity to build custom modules. On the service side, evaluate documentation quality, installation support, training, spare parts planning, and post-startup optimization.
| Supplier Evaluation Item | What to Verify | Why It Reduces Risk |
|---|---|---|
| Regulatory experience | EU GMP, US FDA cGMP, WHO GMP familiarity | Improves compliance alignment |
| Installed references | Sterile lines in multiple countries | Shows practical execution ability |
| Customization depth | Bag format, utilities, line layout options | Ensures fit with site constraints |
| Documentation package | DQ, FAT, SAT, IQ/OQ/PQ support | Speeds validation process |
| Service responsiveness | Remote support, spares, training | Minimizes downtime |
| Turnkey capability | Engineering plus equipment integration | Controls interface risk across systems |
As one example of what buyers often seek, IVEN Pharmatech Engineering has built its reputation around international pharmaceutical engineering, with a long history in sterile production technologies, multiple specialized manufacturing bases, and broad experience delivering integrated projects across dozens of countries. Rather than acting only as a machine seller, this type of supplier can support feasibility review, design coordination, equipment selection, commissioning, and validation support. Companies interested in discussing requirements directly can use the contact channel for project consultation.
The bar chart suggests where demand is strongest in the United States. Hospitals and hospital-focused supply chains remain the key driver, followed by regional pharmaceutical producers and contract manufacturers.
Investment cost, budget planning, and ROI analysis
Capital investment in an IV solution soft bag manufacturing line can vary widely depending on speed, format range, utility scope, validation requirements, and whether the project is equipment-only or turnkey. In the United States, companies must also account for building adaptation, cleanroom modifications, HVAC balancing, utility generation, digital systems integration, local installation labor, and qualification costs.
Typical budgeting categories include core line equipment, water treatment and WFI systems, solution preparation, clean utilities, cleanroom construction interface, packaging equipment, automation, validation, spare parts, and training. Imported projects also require logistics planning, customs coordination, and contingency allowances.
| Budget Category | Relative Cost Weight | Planning Note |
|---|---|---|
| Core soft bag line | High | Main driver of capex |
| Water and steam systems | High | Essential for compliant sterile production |
| Solution preparation | Medium to high | Depends on batch complexity |
| Facility adaptation | Medium to high | Varies by site condition |
| Validation and documentation | Medium | Must not be underbudgeted |
| Training and after-sales support | Medium | Protects startup performance |
ROI is typically influenced by six measurable levers: throughput increase, scrap reduction, labor savings, packaging logistics efficiency, reduced downtime, and improved market access. For a producer supplying large hospital networks, the biggest return may come from dependable capacity and lower unit cost. For a company replacing obsolete equipment, the return may come from reduced maintenance burden and stronger inspection readiness.
A basic ROI model should include:
- Annual planned output by bag size and SKU
- Expected yield improvement from better seal and fill control
- Labor delta versus current line or outsourced model
- Distribution savings due to lower package weight
- Maintenance savings from modern design
- Incremental revenue from new contracts enabled by capacity
In many US projects, the payback period is improved when companies align the line purchase with broader sterile plant modernization, because utility and digital investments then serve multiple production areas instead of only one asset.
Key considerations and potential risks when investing
The main risks in soft bag IV line investment are not limited to machine quality. Many failures occur because of poor layout planning, weak utility design, underdefined user requirement specifications, unrealistic validation schedules, or insufficient operator preparation. In the United States, projects can also face delays due to permitting, contractor coordination, and supply chain timing for imported components.
To reduce these risks, companies should conduct an early gap assessment covering building flow, cleanroom classification, personnel and material segregation, WFI and pure steam loads, serialization or coding requirements, and expected future product extensions. They should also confirm material compatibility for the chosen bag film and ports, especially for products with sensitive formulations or longer shelf-life targets.
| Risk Area | Typical Problem | Mitigation Strategy |
|---|---|---|
| Project scope | Unclear interfaces between suppliers | Use integrated engineering management |
| Validation timeline | Documentation arrives too late | Define deliverables in contract early |
| Utility capacity | WFI or HVAC undersized | Perform detailed load analysis |
| Material compatibility | Film or port interaction concerns | Run compatibility and stability studies |
| Operator readiness | Startup errors and low yield | Provide structured training and SOP rollout |
| Service continuity | Slow spare parts response | Plan critical spare inventory in advance |
This table shows that the highest-value supplier is often the one that anticipates risk before it turns into delay or deviation. Service capability is especially important here. Buyers benefit from partners that offer lifecycle support, from feasibility and design through installation, commissioning, qualification support, training, troubleshooting, and later optimization. That service structure can significantly reduce cost overruns and startup uncertainty.
For multinational or growth-stage pharmaceutical companies, risk management should also include scenario planning for tariff changes, local content expectations, cybersecurity in connected equipment, and sustainability reporting requirements that may become more visible by 2026.
FAQ
What products can be made on an IV solution soft bag manufacturing line?
Typical products include normal saline, dextrose solutions, electrolyte solutions, irrigation fluids, and selected dialysis-related or specialty infusion products, depending on line design and regulatory strategy.
Is soft bag packaging accepted in the United States?
Yes. Soft bag infusion formats are widely used in the United States when produced under compliant, validated conditions and with suitable material and container closure integrity performance.
What is the difference between a machine supplier and a turnkey engineering partner?
A machine supplier may provide core equipment only. A turnkey engineering partner can support design, utilities, cleanroom interfaces, validation documentation, installation, training, and broader project coordination.
How long does implementation usually take?
It depends on scope. Equipment-only projects may move faster, while full turnkey sterile manufacturing projects can take considerably longer due to building work, utility installation, and qualification activities.
What are the most important compliance points for US buyers?
US buyers typically focus on cGMP compliance, documentation quality, material traceability, data integrity, validation support, and supplier responsiveness during FAT, SAT, IQ, OQ, and PQ stages.
How do companies choose between non-PVC bags and other materials?
The decision is based on formulation compatibility, market requirements, sustainability goals, cost, barrier properties, and procurement availability of the packaging film system.
Why do many buyers ask for integrated water treatment and solution preparation systems?
Because sterile IV production depends on upstream utility and formulation reliability. Integrated sourcing can simplify interface management and reduce project risk.
What should be included in a supplier RFQ?
Include product list, target output, bag sizes, film type, sterilization approach, utility conditions, layout constraints, automation requirements, documentation expectations, validation scope, and after-sales service needs.
What role does experience play in supplier selection?
Experience helps a supplier anticipate real sterile manufacturing challenges, customize accurately, and support compliance with international regulatory standards. This is why many buyers prioritize suppliers with broad installed bases and proven pharmaceutical references.
Why consider IVEN Pharmatech Engineering for the United States market?
Because buyers often value a partner that combines sterile line technology, specialized equipment manufacturing, and full lifecycle service. IVEN Pharmatech Engineering is recognized in the market for integrated pharmaceutical engineering solutions, strong compliance awareness, and experience across IV solution production systems, water treatment, intelligent logistics, and project execution for pharmaceutical and medical device facilities.
For pharmaceutical companies in the United States, IV solution soft bag manufacturing is no longer just a packaging choice. It is an infrastructure decision tied to compliance, resilience, cost, and long-term market access. Whether the project involves a new line in New Jersey, a facility expansion in Texas, a sterile plant upgrade in Indiana, or a broader turnkey strategy serving national hospital networks, the most successful investments are based on careful process design, strong supplier qualification, realistic validation planning, and dependable service support after startup.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
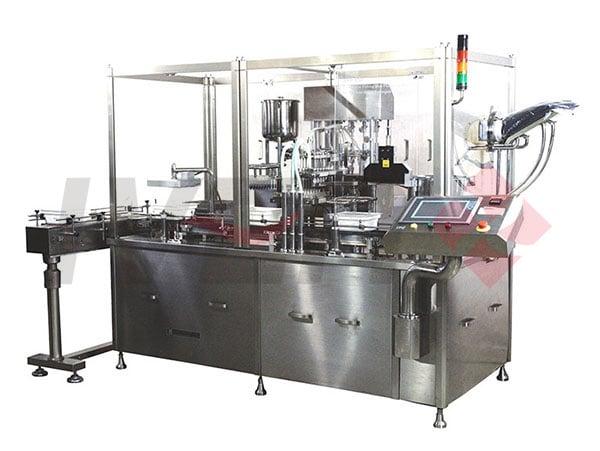
How Prefilled Syringe Filling Works in the United States
In the United States, understanding how prefilled syringe filling works is essential for pharmaceutical and medical device manufacturers planning new injectable capacity, upgrading legacy lines, or moving high-value biologics into safer and more efficient drug delivery formats. A prefilled syringe line is not just a filling machine. It is an integrated sterile production system that combines container handling, nest or bulk syringe feeding, washing or ready-to-use processing, filling, stoppering, plunger insertion, inspection, labeling, and packaging under tightly controlled aseptic conditions.
For U.S. manufacturers operating in markets such as Boston, New Jersey, Philadelphia, Indianapolis, Houston, and San Diego, the technology matters because it directly affects yield, sterility assurance, operator intervention, batch traceability, regulatory readiness, and total cost of ownership. Companies evaluating capacity near major logistics hubs like the Port of New York and New Jersey, Port of Los Angeles, or air freight corridors through Memphis and Chicago often prioritize prefilled syringe systems that support both domestic distribution and export requirements.
Modern prefilled syringe filling lines are widely used for vaccines, anticoagulants, biologics, ophthalmics, emergency drugs, and specialty injectables. They reduce dosing errors, shorten preparation time in hospitals, improve patient convenience, and support advanced self-administration programs. In the U.S. market, demand is especially strong where contract development and manufacturing organizations, hospital systems, and biologics producers require high precision, barrier isolation, and compliance with FDA cGMP expectations.
The short answer is that prefilled syringe filling works by moving sterile syringes through a highly controlled aseptic process where a precise dose of drug product is introduced, the syringe is closed with a stopper or plunger system, and the finished unit is inspected and packaged for safe clinical or commercial use. The process can be configured for glass or polymer syringes, ready-to-use nested formats, or bulk containers depending on product sensitivity, output target, and facility design.
A typical line includes syringe infeed, de-nesting or unscrambling, optional air or vacuum particle removal, filling pumps, stoppering, plunger rod insertion where required, weigh control, vision inspection, labeling, and downstream secondary packaging. For high-value biologics or highly potent injectables, the system is often paired with isolators, restricted access barrier systems, automated environmental monitoring, and electronic batch records.
In practical terms, large pharmaceutical companies assess this technology when they need to improve sterility assurance, lower operator intervention, reduce overfill, increase format flexibility, and meet growing demand from clinics, retail pharmacies, and home-use therapies across the United States.
Process StageWhat HappensMain EquipmentCritical Control PointTypical U.S. ConcernOperational BenefitSyringe InfeedNested tubs or bulk syringes enter the lineDe-nester or unscramblerContainer integrityDamage during transport from suppliersStable line flowPreparationContainers are presented for fillingAir cleaning or sterile transfer systemParticulate controlFDA inspection focus on contamination preventionCleaner product pathFillingPrecise liquid dose is dispensedPeristaltic, rotary piston, or time-pressure pumpVolume accuracyYield loss on expensive biologicsLower overfill and better consistencyStopperingClosure is inserted after fillingStoppering stationSeal integrityCCIT expectations for sterile productsReduced leakage riskPlunger InsertionPlunger or rod is positioned to specificationPlunger insertion moduleGlide force and positionDevice functionality verificationReliable administration performanceInspection & PackagingUnits are checked and packedVision inspection, labeler, cartonerDefect rejection and traceabilitySerialization and batch release speedHigher compliance and market readinessThe table above shows why the topic is broader than filling alone. Each step has a direct effect on product quality, compliance, and plant economics.
From an engineering perspective, how prefilled syringe filling works refers to the design logic, process flow, and equipment architecture used to fill sterile drug products into pre-assembled syringe containers. In pharmaceutical production, this technology is used when manufacturers want a final dosage form that is ready for injection with minimal preparation by nurses, physicians, patients, or emergency responders.
Its main uses include unit-dose delivery of injectable formulations, reduction of bedside compounding steps, improved dose accuracy, and support for sensitive products that benefit from low hold-up volume and tight filling precision. In U.S. production environments, prefilled syringe systems are especially common in facilities producing biologics, vaccines, anticoagulants, flushing solutions, anesthetics, fertility drugs, and ophthalmic injections.
Because many products are temperature-sensitive and high in value, line design typically emphasizes gentle product handling, low shear, short product paths, CIP/SIP strategies where applicable, and integration with cold-chain planning. Manufacturers in biotech clusters such as Cambridge, South San Francisco, and Research Triangle Park often favor modular lines that can scale from clinical batches to commercial volumes without redesigning the entire sterile suite.
For companies developing new facilities, the broader decision is often whether to build a dedicated prefilled syringe line or adopt a flexible injectable platform that supports vials and syringes. The right answer depends on portfolio mix, fill volume range, closure system, market forecasts, and reimbursement-driven packaging needs in the United States.
Prefilled syringe technology creates value across the pharmaceutical supply chain. In manufacturing, it can improve line efficiency, reduce operator contact, and support higher-value product presentation. In healthcare settings, it shortens preparation time and reduces dosing variation. In patient use, it helps enable self-injection and adherence programs.
The strongest applications in the United States include chronic disease biologics, emergency care products, hospital-administered injectables, vaccine campaigns, and specialized formulations supplied to ambulatory centers. Compared with many vial-based workflows, prefilled syringes can reduce wastage and simplify administration training.
Application AreaTypical Product ExamplesWhy Syringe Format Is ChosenKey Manufacturing BenefitEnd-User BenefitU.S. Market RelevanceBiologicsMonoclonal antibodiesConvenient self-administrationPrecise fill controlFaster home treatmentHigh growth in specialty pharmaVaccinesSingle-dose immunizationsReady-to-use formatReduced preparation stepsFaster throughput in clinicsPublic health distribution efficiencyHospital InjectablesAnticoagulants, flush syringesMedication safetyHigh repeatabilityLower dosing error riskCommon in acute care networksEmergency MedicineCritical rescue drugsRapid deploymentReliable closure performanceImmediate use under stressImportant for EMS and ER settingsOphthalmicsSpecialized sterile injectionsSmall-volume accuracyLow overfill lossBetter handling precisionNiche but high-value segmentClinical TrialsInvestigational injectablesPatient convenience and blinding supportFlexible batch size capabilityEasier protocol administrationGrowing in U.S. CDMO sectorThe benefits shown above explain why so many expansion projects now include syringe capability. Manufacturers are not only buying capacity; they are buying a format that can improve the commercial value of the product itself.
There are also environmental and labor benefits when the line is designed well. Ready-to-use nested syringes can reduce washing and depyrogenation requirements compared with bulk container preparation, though tradeoffs remain around packaging waste and supplier dependency. This is why lifecycle analysis and utility consumption should be part of the equipment review.
There is no single universal prefilled syringe line. Equipment selection depends on syringe material, output speed, drug viscosity, cleanroom concept, and level of automation. In the U.S. market, the most common distinction is between nested ready-to-use syringe systems and bulk syringe handling systems. Nested formats are often preferred for sterile assurance and simpler upstream processing, while bulk systems may support different economics at scale.
Technical options typically include servo-driven dosing, peristaltic or piston pumps, vacuum-assisted filling, in-process check weighing, no-bag-no-fill logic, automatic rejection, laminar airflow, isolator integration, robotic tub handling, and recipe-based changeover control. Manufacturers also compare line concepts based on compatibility with dual-chamber formats, safety devices, autoinjector assembly requirements, and future digital validation needs.
Equipment TypeBest ForSpeed RangeTechnical StrengthPossible LimitationTypical Buyer ProfileNested RTU Syringe LineBiologics and sterile high-value drugsLow to highLower contamination riskDependency on tub format suppliersBiotech plants and CDMOsBulk Syringe LineLarge repetitive campaignsMedium to highPotentially lower container costMore complex preparation stepsHigh-volume injectable producersIsolator-Based LineAseptic critical productsMedium to highExcellent sterility assuranceHigher capital costCommercial sterile facilitiesRABS-Based LineBalanced cost and controlMediumGood operator separationMore intervention planning neededMid-size pharmaceutical plantsClinical Batch Compact LineDevelopment and small lotsLowFlexibility and quick changeoverLower throughputR&D and pilot operationsHigh-Speed Commercial LineMass market productsHighAutomation and low labor per unitComplex validation effortLarge multinational producersThe table shows that the right model is driven by portfolio strategy, not just maximum speed. A plant in New Jersey serving multiple specialty products may need flexibility more than headline output, while a large Midwest facility supporting national hospital systems may favor a high-speed standardized platform.
On the technology side, some global suppliers emphasize high-end aseptic automation and digital batch integration, while others compete on cost-effective customization and complete utility support. For buyers seeking integrated project execution, it can be useful to work with engineering firms that can combine filling equipment with purified water, WFI, clean utilities, logistics automation, and packaging systems in one validated scope.
When choosing packaging for injectable products, U.S. manufacturers often compare prefilled syringes with vials, ampoules, cartridges, blow-fill-seal formats, and auto-injector compatible systems. Each option has advantages, and the best fit depends on product characteristics, market channel, administration setting, and long-term cost structure.
Prefilled syringes are strongest where ready-to-administer convenience, dose precision, and patient handling matter. Vials remain attractive for multipurpose lines, lyophilization, and lower initial equipment cost. Cartridges are useful for pen systems, while BFS may serve certain high-volume liquid applications but is not a direct substitute for many sensitive biologics. Ampoules still exist in selected markets but are less aligned with modern safety expectations for many U.S. use cases.
FormatBest Use CaseSterile Filling ComplexityUser ConvenienceCapital IntensityCommercial Fit in the U.S.Prefilled SyringeReady-to-use unit doseHigh but controlledVery highMedium to highStrong growth for biologics and hospitalsVialFlexible sterile portfolioModerate to highModerateMediumStill dominant in many injectablesCartridgePen injector systemsHighHighHighStrong in diabetes and specialty deliveryAmpouleCertain legacy productsModerateLowLowerLimited new investment focusBFS Unit DoseSome high-volume liquidsIntegrated forming and fillingModerateHighNiche relative to syringe applicationsAutoinjector AssemblyPatient self-injection programsDepends on syringe platformVery highHighFast-growing specialty segmentThe comparison above helps frame strategy. If your commercial pathway involves home administration, specialty pharmacy channels, or nurse time reduction, a prefilled syringe platform often delivers the best overall value. If your pipeline is broad and uncertain, a flexible vial line may still be a rational first investment. Many larger manufacturers eventually operate both.
var ctxComp = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var comparisonChartSupplier = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Flexibility’, ‘Aseptic Control’, ‘Patient Convenience’, ‘Changeover Speed’, ‘Scale Potential’, ‘Format Value’],datasets: [{label: ‘Prefilled Syringe Line’,data: [88, 93, 96, 78, 85, 94],backgroundColor: ‘rgba(153, 102, 255, 0.7)’},{label: ‘Standard Vial Line’,data: [91, 90, 65, 82, 92, 74],backgroundColor: ‘rgba(54, 162, 235, 0.7)’}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { position: ‘top’ } },scales: { y: { beginAtZero: true, max: 100 } }}});The U.S. market for prefilled syringe filling is supported by three major forces: the ongoing expansion of injectable biologics, healthcare demand for ready-to-administer products, and the need for more resilient domestic manufacturing capacity. Facilities in the Northeast corridor, the Midwest biomanufacturing belt, Texas, and California are all evaluating new sterile investments to reduce supply risk and improve market responsiveness.
Demand is also shaped by logistics and trade infrastructure. Components may move through the Port of Savannah, Port of Los Angeles, or Port of Houston; finished products may require rapid cold-chain distribution to hospital networks from Chicago, Atlanta, or Memphis. This makes equipment uptime, spare parts planning, and validation support especially important when choosing a supplier.
Looking toward 2026, several trends are clear. First, isolator adoption will continue to grow as contamination control strategies become more demanding. Second, digital manufacturing tools such as electronic batch review, predictive maintenance, and recipe analytics will become standard expectations. Third, sustainability will shift from a marketing point to a procurement criterion, with more attention to energy use, compressed air consumption, reject reduction, and recyclable secondary packaging. Fourth, policy attention on domestic capacity and supply-chain resilience is likely to support U.S.-based expansion projects.
var ctxLine = document.getElementById(‘lineChartMarketGrowth’).getContext(‘2d’);var lineChartMarketGrowth = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. Prefilled Syringe Line Market Index’,data: [100, 108, 117, 128, 141, 156],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { position: ‘top’ } },scales: { y: { beginAtZero: false } }}});var ctxBar = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var barChartIndustryDemand = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Biologics’, ‘Vaccines’, ‘Hospital Injectables’, ‘CDMO Services’, ‘Ophthalmics’, ‘Emergency Drugs’],datasets: [{label: ‘Projected 2026 U.S. Demand Score’,data: [94, 82, 76, 88, 61, 69],backgroundColor: [‘rgba(255, 99, 132, 0.7)’,’rgba(54, 162, 235, 0.7)’,’rgba(255, 206, 86, 0.7)’,’rgba(75, 192, 192, 0.7)’,’rgba(153, 102, 255, 0.7)’,’rgba(255, 159, 64, 0.7)’]}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: false } },scales: { y: { beginAtZero: true, max: 100 } }}});var ctxArea = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var areaChartTrendShift = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Share of New U.S. Projects Using Isolators (%)’,data: [34, 39, 45, 52, 58, 64],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,fill: true,tension: 0.3},{label: ‘Share of New U.S. Projects Using Basic Open RABS (%)’,data: [46, 43, 39, 35, 31, 27],borderColor: ‘rgb(255, 159, 64)’,backgroundColor: ‘rgba(255, 159, 64, 0.18)’,fill: true,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { position: ‘top’ } },scales: { y: { beginAtZero: true, max: 80 } }}});The charts above illustrate realistic market behavior: expanding investment, strong demand from biologics and CDMOs, and a clear shift toward higher-containment aseptic designs.
Supplier selection in the United States should go beyond brochure speed and container range. Buyers need to evaluate regulatory understanding, mechanical reliability, documentation depth, FAT/SAT discipline, spare parts strategy, validation support, and whether the supplier can execute the full project scope without creating interface risk.
For example, a line may perform well in a factory acceptance test but still underdeliver if the supplier cannot coordinate utilities, cleanroom interfaces, conveyors, serialization, or operator training. This is why many investors prefer partners that can support turnkey or semi-turnkey delivery. A useful starting point is reviewing a supplier’s engineering background, manufacturing footprint, and installed base. Buyers can also ask whether the company has experience aligning projects with EU GMP, U.S. FDA cGMP, WHO GMP, and PIC/S expectations, particularly when the facility may serve multiple markets.
Shanghai IVEN Pharmatech Engineering, for instance, is often considered by buyers looking for integrated sterile manufacturing solutions because its strengths are distributed across technology, manufacturing, and service rather than limited to a single machine. On the technology side, the company is known for combining filling and packaging equipment with pharmaceutical water treatment, solution preparation, intelligent conveying, and related plant systems. On the manufacturing side, it operates specialized production plants focused on distinct equipment categories, which can help with quality consistency and system integration. On the service side, its project teams support feasibility review, design, installation, commissioning, validation, training, and lifecycle optimization. Companies exploring integrated project support can review its company background, learn more about turnkey pharmaceutical engineering, browse selected equipment solutions, or contact the team for a project discussion.
Supplier Evaluation FactorWhy It MattersWhat to AskGood SignWarning SignImpact on ProjectRegulatory ExperienceSupports smoother inspectionsWhat standards have you delivered to?Strong cGMP documentation historyGeneric answers onlyLower compliance riskAseptic Engineering CapabilityProtects product sterilityIsolator, RABS, EM integration?Clear contamination control logicLimited barrier experienceHigher process confidenceCustomization AbilityMatches product portfolioCan you support multiple syringe formats?Recipe-driven flexible designOne-size-fits-all proposalBetter long-term utilityManufacturing DepthAffects quality and lead timeWhich modules are built in-house?Specialized production capabilityHeavy dependence on third partiesImproved schedule controlValidation SupportCritical for startupDo you provide IQ/OQ/PQ packages?Structured validation deliverablesMinimal documentationFaster qualificationAfter-Sales ServiceDetermines uptimeHow are parts and service handled in the U.S.?Defined support modelUnclear response timesBetter lifecycle ROIThe table emphasizes that supplier reliability is operational, not just reputational. A cheaper line with weak documentation or slow service can become much more expensive after startup.
Capital planning for prefilled syringe filling must include more than the base machine price. U.S. projects often require spending on isolators or RABS, cleanroom integration, utilities, inspection, packaging, digital systems, validation, spare parts, training, and line clearance tools. Facility modifications can be substantial, especially in older plants around New Jersey, Baltimore, or the Chicago area where legacy sterile suites may not be optimized for current barrier expectations.
Budget levels vary widely. A compact development line may be in a lower capital band, while a full commercial high-speed line with isolator, automated de-nesting, inspection, labeling, and downstream packaging can require a multi-million-dollar investment. ROI depends on product margin, expected utilization, labor reduction, reduced overfill, lower rejects, and the premium value of ready-to-administer presentation.
Cost CategoryTypical Share of BudgetWhat Is IncludedHidden Cost RiskControl StrategyROI EffectCore Filling Line25% to 40%Infeed, filling, closing modulesUnder-specification of change partsClear URS and format listDirect throughput impactBarrier System10% to 25%Isolator or RABSDecon cycle complexityEarly contamination control planningHigher sterility assuranceInspection & Packaging10% to 20%Vision, labeling, cartoningLate serialization integrationEnd-to-end line design reviewRelease and compliance efficiencyUtilities & Cleanroom Interface10% to 20%HVAC, gases, electrical, WFI supportRetrofit surprisesSite survey and 3D coordinationStartup reliabilityValidation & Documentation5% to 10%DQ, IQ, OQ, PQ supportRework from incomplete protocolsDocument review gatesFaster time to marketTraining, Parts, Service5% to 10%Spare kits, training, supportInsufficient first-year inventoryLifecycle service planBetter uptime and lower disruptionROI analysis should examine both hard and soft gains. Hard gains include reduced manual labor, improved yield on expensive formulations, lower rejection rates, and higher line speed. Soft gains include fewer administration errors in the market, better product positioning, and stronger customer preference among hospitals and specialty pharmacies. For many branded products, these soft gains can justify the investment as much as factory economics.
A disciplined U.S. budgeting process usually includes a user requirement specification, supplier comparison matrix, conceptual layout, utility load analysis, validation plan, and sensitivity model covering best-case and downside demand scenarios.
The largest risks in a prefilled syringe investment are usually not mechanical failure alone. They include poor format compatibility, inadequate barrier design, weak component supply planning, unrealistic output assumptions, and underestimating validation timelines. In addition, many companies fail to plan enough time for stability implications, extractables and leachables review, syringe-component interaction testing, and device functionality studies.
Supply-chain risk is especially important in the United States because syringe tubs, stoppers, plungers, needles, and safety device components may come from multiple regions. Freight delays through West Coast or East Coast ports can affect launch timing if sourcing is not diversified. Cold-chain projects add another layer of complexity because commissioning windows and product transfer planning must align.
Risk AreaWhat Can Go WrongEarly Warning SignMitigation MethodResponsible TeamBusiness ImpactContainer CompatibilityPlunger or closure mismatchFrequent setup adjustmentsRobust format trialsEngineering + QABatch loss and delaysAseptic DesignExcessive interventionsComplex manual access stepsIntervention minimization reviewOperations + validationHigher contamination riskComponent SupplyShortage of RTU syringes or stoppersLong vendor lead timesDual sourcing and safety stockSupply chainProduction interruptionValidation TimelineDelayed commercial startLate protocol approvalFront-load document planningQA + project managementMissed revenue windowOperator TrainingHigh reject rate at startupFrequent alarms and slow changeoversStructured FAT/SAT trainingOperationsLower efficiencyTotal Cost ControlBudget overrunsMany unpriced interfacesTurnkey scope clarityProcurement + PMOReduced project returnFor buyers who want to reduce these risks, it helps to involve engineering, QA, operations, supply chain, and commercial stakeholders early. The best projects define not only the line speed target but also the product roadmap, component strategy, utility envelope, maintenance philosophy, and future expansion path through 2026 and beyond.
What is the biggest reason U.S. pharma companies invest in prefilled syringe filling lines?The main reason is the combination of sterility control, dose accuracy, and market convenience. It is especially attractive for biologics, hospital injectables, and self-administration therapies.
Are prefilled syringe lines only for large pharmaceutical companies?No. Large companies buy high-speed commercial systems, but smaller biotech firms and CDMOs also invest in compact or modular lines for clinical and specialty products.
How does a nested ready-to-use syringe line differ from a bulk line?A nested RTU line handles syringes in tubs that arrive sterilized and ready for aseptic processing, which can reduce contamination risk and upstream preparation. A bulk line may suit larger repetitive production but typically requires more handling steps.
Which products are most suitable for this format in the United States?Biologics, vaccines, anticoagulants, flushing syringes, emergency injectables, and many specialty therapies are strong candidates, especially where ready-to-administer use is valued.
What regulatory issues matter most?FDA cGMP compliance, aseptic processing control, data integrity, validation completeness, container closure integrity, and traceability are all central.
How long does a project usually take?Timelines vary, but a full commercial project can take many months from URS to qualification. Existing facility constraints, utility upgrades, and validation requirements often shape the schedule more than machine assembly alone.
Can one supplier provide more than just the filling line?Yes. Many buyers prefer suppliers or engineering partners that can support utilities, water systems, preparation systems, packaging, logistics, and validation so there are fewer handoff risks. This is one reason integrated engineering companies are often shortlisted in larger U.S. projects.
How should we compare suppliers?Use a scorecard covering technical fit, regulatory documentation, installed base, service support, total project scope, lead time, parts availability, and lifecycle cost. The lowest purchase price is rarely the best long-term value.
What should be included in a request for proposal?Include syringe formats, fill volumes, product viscosity, target speed, sterility concept, batch size, inspection requirements, packaging scope, validation needs, utility conditions, and acceptance criteria.
What future trends should buyers prepare for by 2026?Expect more isolator-based systems, stronger digital integration, sustainability metrics in procurement, increasing domestic resilience requirements, and growing demand for flexible lines that can support evolving injectable portfolios.
For U.S. manufacturers, understanding how prefilled syringe filling works is ultimately about matching the right sterile technology to the right business model. When the equipment, barrier strategy, validation plan, and supplier support are aligned, prefilled syringe production can deliver both regulatory confidence and strong commercial value.
-
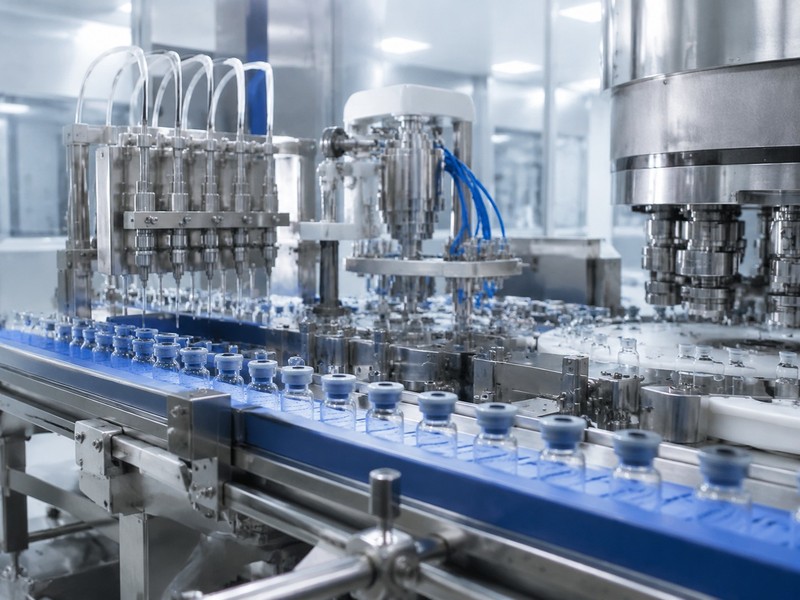
United States Guide to Cartridge and Vial Filling
For pharmaceutical manufacturers in the United States, the choice between cartridge filling and vial filling is not a minor equipment decision. It affects product strategy, regulatory planning, line flexibility, contamination control, market positioning, and long-term operating cost. Companies expanding injectable production in hubs such as New Jersey, Boston, Raleigh-Durham, Houston, and California often compare both formats when modernizing facilities under FDA cGMP expectations. In practical terms, cartridge filling is usually preferred for pen injectors, dental anesthetics, and other ready-to-use delivery systems, while vial filling remains the more versatile option for biologics, lyophilized products, hospital injectables, and multi-dose presentations. The best choice depends on dosage form, container closure system, throughput target, sterility strategy, device compatibility, and future pipeline plans.
As the U.S. market continues to invest in aseptic processing, isolator technology, robotics, digital batch management, and supply chain resilience, manufacturers increasingly want filling lines that are compliant, scalable, and easy to validate. This is where an experienced engineering partner matters. Companies evaluating complete solutions often look for suppliers that can support not only the machine itself, but also purified water systems, WFI generation, cleanroom integration, automated logistics, packaging, qualification, and lifecycle service. A global engineering company such as IVEN Pharmatech Engineering is often considered in such projects because it combines filling equipment know-how with broader pharmaceutical plant engineering capabilities for regulated markets including the United States.
Cartridge and vial filling systems are core aseptic manufacturing assets used to dose sterile liquid or powder drugs into primary packaging under controlled, validated conditions. Large pharmaceutical companies, CDMOs, biotech firms, and medical device manufacturers evaluate them when launching new injectable therapies, replacing aging lines, increasing batch capacity, or moving toward automated, higher-containment production.
In the United States, the decision usually comes down to six strategic questions:
For manufacturers serving hospital, specialty, biologics, and self-injection segments, the comparison is especially important because filling format influences everything from component supply to secondary packaging and cold chain design.
Decision AreaCartridge FillingVial FillingWhy It MattersPrimary usePen injectors, device-integrated dosingHospital injectables, biologics, multi-product linesDetermines market fit and packaging strategyFormat flexibilityModerateHighImportant for CDMOs and mixed portfoliosDevice compatibilityVery highLower unless transferred laterCritical for self-administration productsLyophilization compatibilityLimited in many projectsExcellentNeeded for unstable biologicsTypical contamination control levelHigh, often integrated with advanced containmentHigh, with broad isolator and RABS optionsSupports sterility assuranceBest fitTargeted, device-led productsFlexible sterile manufacturingGuides capex prioritiesThe table above shows why no single format is universally better. Cartridge lines typically create more value when the commercial model is tied directly to a delivery device. Vial lines usually win when flexibility, scale diversity, and broader sterile product compatibility are top priorities.
Cartridge filling is the aseptic process of filling sterile product into cylindrical cartridges, then stoppering and sealing them for use in pens, autoinjectors, dental systems, or specialized injector platforms. The line may include tub or tray handling, de-nesting, air management, filling, plunger insertion, crimping or closure application, inspection, and transfer to downstream assembly or packaging.
Vial filling is the aseptic process of filling sterile liquid or powder into glass or polymer vials, followed by stoppering, capping, and, when needed, transfer to lyophilization. Vials may be used as liquid ready-to-use presentations, reconstitution formats, or multi-dose products. The line often includes vial washing, depyrogenation tunnel, filling, stoppering, capping, inspection, labeling, and packaging.
In U.S. production environments, both technologies must fit stringent standards for particulate control, environmental monitoring, container closure integrity, cleaning validation, batch traceability, and operator intervention reduction. Whether the project is located near the Port of New York and New Jersey, in the biotech corridor around Cambridge, or in manufacturing zones around Chicago and Dallas, plant planners must align the filling line with utility systems, material flow, warehousing, and quality systems.
Manufacturers pursuing broader facility upgrades often evaluate equipment suppliers that can also support turnkey pharmaceutical engineering solutions. This matters because filling performance is linked to WFI supply, purified steam, clean compressed gases, solution preparation systems, and cleanroom logistics.
Production StepCartridge LineVial LineOperational NoteContainer preparationNesting, de-bagging, de-nesting or tray loadingWashing and depyrogenation or RTU handlingFormat affects upstream complexityFilling modeLiquid dosing, often precision-focusedLiquid or powder dosingVials support broader product typesClosure systemPlunger insertion and seal handlingRubber stopper and aluminum capDifferent closure validation needsDevice integrationOften direct downstream compatibilityUsually separate from device assemblyKey for user-ready productsLyophilization pathLess commonCommon and well establishedMajor factor for biologicsTypical usersMedical device and specialty pharma firmsPharma, biotech, hospitals, CDMOsDefines purchasing prioritiesThe table clarifies that the technologies overlap in aseptic fundamentals but differ significantly in packaging architecture and downstream use.
Cartridge filling is widely used for insulin delivery, GLP-1 therapies, fertility drugs, growth hormones, ophthalmic products, dental anesthetics, and other therapies requiring accurate, device-friendly dosing. Its biggest advantage is convenience: the filled unit is designed to work with a delivery platform that improves dose control and patient compliance.
Vial filling serves a broader cross-section of the market, including oncology injectables, vaccines, anti-infectives, monoclonal antibodies, emergency medicines, contract manufacturing programs, and clinical supplies. Because vials can support liquid or freeze-dried formats and multiple fill volumes, they remain a default choice for many U.S. sterile facilities.
Benefits shared by both line types include:
From a manufacturing strategy perspective, cartridge systems are often linked to premium drug-device business models, while vial systems support broader portfolio resilience. This is especially relevant in the United States, where hospital demand, specialty pharmacy channels, and home-care growth coexist.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Biologics’, ‘Hospital Injectables’, ‘Self-Injection Devices’, ‘Vaccines’, ‘CDMO Projects’, ‘Dental/Local Anesthesia’],datasets: [{label: ‘Estimated U.S. Demand Index’,data: [92, 88, 84, 76, 81, 54],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: {display: true}},scales: {y: {beginAtZero: true, max: 100}}}});The bar chart indicates where sterile filling investments are currently strongest in the U.S. market. Biologics, hospital injectables, and self-injection segments are major drivers of both cartridge and vial line upgrades.
When specifying a line, buyers should not think only in terms of “cartridge” versus “vial.” The real comparison includes automation level, speed range, dosing technology, sterility barrier system, component feed design, and changeover architecture.
Common technical options include time-pressure filling, peristaltic pumps, rotary piston pumps, mass-flow controlled filling, vacuum-assisted stoppering, in-process weight checking, 100% IPC systems, vision inspection, robotics, and isolator integration. U.S. buyers increasingly request recipe-driven control systems, audit trails, OPC connectivity, and remote diagnostics.
Equipment categories often include compact R&D or clinical lines, medium-speed commercial lines, and high-speed large-scale systems. Suppliers may also provide monoblock designs or modular units that fit phased expansion plans.
Line TypeTypical Speed RangeBest ForMain AdvantageClinical cartridge filling lineUp to 30 units/minR&D, pilot, niche launchesFlexible small batchesCommercial cartridge line30 to 180 units/minPen injector and device productsStable precision dosingHigh-speed cartridge line180+ units/minLarge-volume device programsScalable outputCompact vial filling line20 to 100 vials/minSpecialty products and CDMOsMulti-product adaptabilityIntegrated vial and lyophilization line50 to 400 vials/minBiologics and freeze-dried drugsSupports unstable formulationsRTU vial or cartridge lineVariesFast startup and reduced preparationLower upstream handling burdenThe explanation here is important: speed alone does not define value. A 60-unit-per-minute line with excellent changeover, low reject rates, and strong data integrity may deliver better ROI than a faster line that is difficult to validate or maintain.
On the technology side, engineering capability is equally important. IVEN Pharmatech Engineering is known in the market for integrating pharmaceutical filling and packaging machinery with supporting systems such as purified water, WFI, purified steam, intelligent conveying, and solution preparation. For U.S. companies comparing line concepts, this type of cross-system capability helps reduce interface risk between filling equipment and the wider plant.
Alternative technologies include prefilled syringe filling, BFS for certain liquid products, ampoule lines, flexible bag filling, and outsourcing to a CDMO. Each option serves a different business model.
Prefilled syringes can be ideal for user convenience and premium biologics, but they may involve higher component cost and different device compatibility. Blow-fill-seal can be cost-effective for some high-volume liquids, though it is not a direct substitute for many sensitive biologics. Ampoules remain useful in selected markets but have declined for some premium applications. Outsourcing is attractive for speed-to-market, yet companies may lose some process control and scheduling flexibility.
TechnologyBest ApplicationStrengthsLimitationsCartridge fillingPen systems, injector-compatible drugsDevice readiness, user convenienceLess flexible than vial formats for broad portfoliosVial fillingBiologics, hospital, multi-product plantsVery versatile, lyophilization friendlyLess direct for self-injection device integrationPrefilled syringe fillingReady-to-inject premium therapiesStrong patient convenienceHigher format sensitivity and costBFSHigh-volume sterile liquidsIntegrated forming and fillingNot ideal for all formulations or device ecosystemsAmpoule fillingCertain legacy or regional productsGood barrier propertiesBreakage and user handling concernsCDMO outsourcingFast market entry or low initial capexSpeed and lower upfront investmentLess operational controlFor a U.S. biotech launching a freeze-dried oncology product, a vial line usually makes more sense than a cartridge line. For a company building a self-injection chronic care portfolio, cartridges may be strategically stronger. For a diversified CDMO near Philadelphia or Indianapolis, flexible vial capabilities often deliver the widest customer appeal.
var ctxComp = document.getElementById(‘comparisonChartUS’).getContext(‘2d’);var comparisonChartUS = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Format Flexibility’, ‘Device Compatibility’, ‘Lyophilization Fit’, ‘Changeover Ease’, ‘Portfolio Breadth’, ‘Premium Patient Use’],datasets: [{label: ‘Cartridge Filling’,data: [68, 95, 35, 70, 62, 90],backgroundColor: ‘#6f4ef2’},{label: ‘Vial Filling’,data: [94, 52, 96, 78, 93, 60],backgroundColor: ‘#2ca58d’}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: {display: true}},scales: {y: {beginAtZero: true, max: 100}}}});This comparison chart helps buyers visualize the tradeoff. Cartridge lines score highest where device integration matters; vial lines dominate where process and portfolio flexibility are priorities.
The U.S. sterile manufacturing market remains one of the most active in the world. Demand is driven by biologics, obesity and diabetes therapies, specialty injectables, hospital preparedness programs, and domestic supply chain resilience. Investment activity is visible across New Jersey, Massachusetts, North Carolina, California, Indiana, and Texas, with many projects linked to modernization, capacity balancing, or reshoring strategies.
By 2026, several trends are expected to shape cartridge and vial filling decisions:
FDA expectations around contamination control strategy, visual inspection robustness, and lifecycle process validation will continue to influence equipment specification. At the same time, procurement teams are paying more attention to total cost of ownership and local service responsiveness, especially after global logistics disruptions through major trade gateways such as Los Angeles/Long Beach, Savannah, and Newark.
var ctxLine = document.getElementById(‘lineMarketChart’).getContext(‘2d’);var lineMarketChart = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘U.S. Sterile Filling Investment Index’,data: [100, 109, 121, 134, 148, 165],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: {display: true}},scales: {y: {beginAtZero: false}}}});The line chart reflects a realistic upward trend in capital investment for sterile filling in the United States, supported by biologics expansion and domestic manufacturing priorities.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Conventional Open Aseptic Share’,data: [42, 38, 34, 30, 27, 24],borderColor: ‘#d62728’,backgroundColor: ‘rgba(214,39,40,0.15)’,fill: true,tension: 0.25},{label: ‘Isolator/Advanced Containment Share’,data: [28, 33, 39, 45, 50, 56],borderColor: ‘#1f77b4’,backgroundColor: ‘rgba(31,119,180,0.15)’,fill: true,tension: 0.25},{label: ‘RTU Component Adoption Share’,data: [18, 22, 27, 31, 36, 41],borderColor: ‘#2ca02c’,backgroundColor: ‘rgba(44,160,44,0.15)’,fill: true,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: {display: true}},scales: {y: {beginAtZero: true, max: 70}}}});The area chart highlights the shift toward advanced containment and ready-to-use processing. This trend is especially relevant for new U.S. facilities designed with future audits, labor efficiency, and contamination control in mind.
Supplier selection should go far beyond catalog speed or headline pricing. In the United States, a good supplier must demonstrate regulatory understanding, documentation quality, installation discipline, and the ability to support FAT, SAT, IQ, OQ, PQ, and training. Strong suppliers are transparent about component sources, software architecture, spare parts strategy, and service response times.
Buyers should evaluate at least the following:
Manufacturing depth matters too. IVEN Pharmatech Engineering operates specialized manufacturing bases in Shanghai covering filling and packaging equipment, pharmaceutical water treatment, intelligent conveying and logistics, and blood collection tube machinery. For U.S. buyers, this kind of structured manufacturing footprint can be advantageous because it reduces dependence on fragmented subcontracting and supports more coordinated system delivery.
Companies that want to review available product categories can also explore the supplier’s pharmaceutical equipment portfolio during the early benchmarking phase.
Supplier CheckpointWhat to AskWhy It Matters in the U.S.Red FlagRegulatory documentationCan you provide DQ/IQ/OQ support and material traceability?Supports inspections and validationGeneric or incomplete documentationAseptic designHow are interventions minimized?Contamination control strategy alignmentToo much manual handlingService networkWhat is your response time for U.S. customers?Downtime is costlyNo clear support modelCustomization disciplineHow do you manage change control?Protects timeline and qualificationInformal engineering changesFactory testingWhat FAT protocols are included?Reduces startup riskMinimal FAT scopeLifecycle supportDo you offer training, optimization, and upgrades?Improves long-term ROISupport ends after installationThe table above should be used as a procurement checklist. It helps separate machine sellers from long-term project partners.
Capital expenditure for cartridge or vial filling lines in the United States varies widely depending on speed, containment level, automation degree, vision systems, lyophilization interface, environmental classification, and project scope. A compact line for clinical or specialty production may cost far less than a high-speed isolator line integrated into a full greenfield facility.
Budget planning should include not only the machine skid, but also format parts, spare parts, FAT/SAT, shipping, customs, installation, clean utilities, HVAC adaptation, validation support, training, serialization interfaces, and secondary packaging. For imported systems, project planners should also consider lead time exposure through ports and inland transportation networks.
Cost ElementCartridge Project ImpactVial Project ImpactBudget NoteMain filling lineHighHighCore capex driverBarrier system or isolatorHighHighMajor sterility investmentContainer/component handlingModerate to highModerateDepends on RTU vs bulkLyophilization integrationLow in most casesPotentially very highCan transform project economicsValidation and qualificationModerateModerateShould not be underestimatedTraining and serviceModerateModerateEssential for uptime and complianceROI depends on more than output rate. The best-performing projects usually improve yield, reduce rejects, shorten changeovers, lower contamination events, and support faster release through stronger in-process control. A line that enables a company to bring a high-margin drug-device product to market six months earlier may justify a premium initial investment.
From a service capability perspective, buyers often favor suppliers that can support feasibility review, engineering design, installation, commissioning, validation, documentation, staff training, and long-term optimization. IVEN Pharmatech Engineering is active in this full-lifecycle support model, which is useful for U.S. clients seeking both equipment and implementation discipline rather than standalone machinery only.
For project-specific budgeting or phased capacity planning, manufacturers can contact an engineering specialist to compare line architecture, utility impact, and validation scope before final procurement.
Even well-funded sterile projects can underperform if critical risks are missed early. The most common problems include over-specifying line speed, underestimating changeover complexity, choosing the wrong container format for the commercial pipeline, weak utility planning, poor FAT definition, and inadequate operator training.
Risk management should cover technical, regulatory, and business dimensions:
One of the most overlooked risks in the United States is misalignment between engineering and quality teams during URS development. A line that looks attractive from a production standpoint may become painful if the documentation package, audit trails, or intervention design do not satisfy quality expectations.
Another common issue is layout inflexibility. Space constraints in older East Coast facilities can complicate vial washing tunnels, isolator footprints, or material/personnel segregation. In newer Midwest and Southern plants, the challenge may be balancing future expansion with current budget discipline.
A practical way to reduce risk is to work with a supplier that has experience in integrated plant design, not just machine manufacturing. This is especially useful where filling lines must coordinate with water systems, warehouse automation, packaging, and clean utility networks.
Across the United States, cartridge and vial filling projects appear in several industry segments: big pharma, biotech startups moving from clinical to commercial scale, hospital injectable manufacturers, veterinary pharmaceutical firms, dental product companies, and CDMOs serving multiple sponsors.
For example, a biotech company near Boston might begin with a compact vial line and later add isolator-based expansion once a monoclonal antibody gains market traction. A diabetes care manufacturer in the Midwest may choose cartridge filling because the product is inseparable from a pen delivery ecosystem. A CDMO near Research Triangle Park may prioritize a modular vial line capable of frequent changeovers and mixed batch sizes.
Integrated engineering becomes valuable when projects move beyond equipment procurement into full manufacturing capability development. IVEN Pharmatech Engineering has built its reputation around this broader approach, combining customized engineering with line integration, utility systems, logistics, and compliance support. Its experience across injectable pharma, biological products, medical consumables, and turnkey facilities is especially relevant to buyers who want one accountable partner rather than multiple disconnected vendors.
For U.S. companies that are benchmarking international suppliers, what stands out is not just machine scope, but the ability to align projects with EU GMP, U.S. FDA cGMP, WHO GMP, and PIC/S expectations. That blend of technical and regulatory familiarity can materially reduce startup risk.
Which is better for biologics in the United States, cartridge or vial filling?For many biologics, vial filling is still the more common choice because it supports a broad range of fill volumes and freeze-drying workflows. Cartridge filling is strong when the product is intended for a pen or device-based administration format.
Are cartridge lines more expensive than vial lines?Not always. Cost depends on speed, automation, containment, component handling, and downstream integration. A high-speed isolator vial line with lyophilization interface can exceed the cost of a mid-speed cartridge line.
Can one supplier provide both equipment and full factory engineering?Yes. Some suppliers provide both line equipment and broader engineering scope, including clean utilities, water systems, layout design, qualification support, and turnkey execution. This can reduce interface risk.
What U.S. regulatory issues should buyers focus on first?Start with aseptic design, contamination control strategy, data integrity, documentation completeness, and validation deliverables. These factors shape both inspection readiness and startup efficiency.
Is RTU processing becoming standard?RTU components are becoming more common, especially in projects focused on contamination reduction and faster implementation. They are not mandatory, but they are increasingly attractive for advanced aseptic lines.
How long does ROI usually take?It varies by product value, utilization rate, line efficiency, and launch timing. For high-value injectable or device-linked therapies, payback can be significantly faster than for low-margin commodity products.
What should a U.S. buyer ask during FAT?Ask for dosing accuracy data, reject handling logic, intervention testing, alarm management review, recipe management demonstration, audit trail checks, and documentation package verification.
Is local after-sales support essential?Yes. For sterile production, downtime is expensive and compliance-sensitive. Buyers should confirm spare parts planning, remote diagnostics, service response commitments, and training coverage before purchase.
In summary, the cartridge versus vial filling decision should be based on product format, market channel, regulatory strategy, and long-term plant economics rather than a simple preference for one container type. U.S. manufacturers that perform a structured comparison and work with capable engineering partners are far more likely to achieve faster qualification, stronger compliance, and better lifecycle returns.
-
Sterile Vial Filling Process in the United States Guide
For pharmaceutical and medical device manufacturers in the United States, the sterile vial filling process is not simply a production step. It is a tightly controlled aseptic manufacturing system used to fill injectable drugs, biologics, vaccines, and specialty formulations into sterile vials while meeting FDA cGMP, data integrity, and contamination control requirements. Companies expanding capacity in New Jersey, Massachusetts, North Carolina, Texas, California, and the Midwest often evaluate this process when modernizing a facility, adding high-value parenteral products, or reducing operator intervention through isolators, RABS, robotics, and automated inspection.
In practice, a sterile vial filling line usually includes vial infeed, washing, depyrogenation, sterile transfer, dosing, stoppering, capping, in-process controls, and downstream inspection. The right design depends on product sensitivity, fill volume, batch size, required sterility assurance level, container closure integrity expectations, and the regulatory pathway for the product. In the United States market, decision-makers also weigh utility demand, cleanroom footprint, qualification timelines, cybersecurity, and long-term service support.
The sterile vial filling process matters because it directly affects product sterility, dosage accuracy, batch release reliability, and commercial scalability. For large pharmaceutical manufacturers, CDMOs, biotech firms, and advanced therapy producers, it is one of the most critical investments in sterile production. A well-designed line reduces contamination risk, supports audit readiness, improves OEE, and can shorten the path from development to commercial launch.
In the United States, the strongest demand comes from injectable generics, oncology products, vaccines, lyophilized drugs, biologics, and high-potency formulations. Facilities near major life science clusters such as Boston-Cambridge, Philadelphia, New Jersey, Raleigh-Durham, Indianapolis, Chicago, and San Diego often prioritize flexible lines that can handle multiple vial sizes, low dead volume filling, and rapid changeover. Manufacturers serving national distribution hubs through the ports of Newark, Savannah, Houston, and Los Angeles also value packaging integration and logistics planning.
Core Process StageMain PurposeTypical Risk ControlledCommon EquipmentU.S. Compliance FocusOperational ImpactVial washingRemove particles and residuesParticulate contaminationRotary or linear vial washerCleaning validationImproves final container cleanlinessDepyrogenationEliminate endotoxin riskPyrogen carryoverTunnel depyrogenation ovenThermal mapping and qualificationSupports injectable safetySterile fillingDeliver accurate product doseMicrobial and volumetric errorPeristaltic, piston, or time-pressure fillerAseptic process simulationDrives yield and batch consistencyStopperingSeal vial immediately after fillExposure to environmentRubber stopper placement systemIntervention controlProtects sterility assuranceCappingSecure closure integritySeal weaknessCrimping machineContainer closure integrityImproves transport robustnessInspection and release supportVerify filled units meet specsDefect escapeVision system, checkweigher, leak testData integrity and traceabilityReduces rejects and recallsThe table above shows why the sterile vial filling process is treated as a complete aseptic system rather than a standalone filler. Each step contributes to risk reduction, compliance, and commercial performance.
The sterile vial filling process is an aseptic manufacturing sequence used to transfer sterile liquid or sterile-filtered product into pre-cleaned, depyrogenated vials under controlled environmental conditions. It is used for injectable medicines that must remain free of viable contamination and foreign particles. Depending on formulation characteristics, the process may support ready-to-use liquid products, products that will later be lyophilized, or highly sensitive biologics requiring minimal shear and precise environmental control.
Its main use cases include small molecule injectables, anti-infectives, emergency drugs, anesthetics, monoclonal antibodies, peptides, cell and gene therapy support materials, diagnostic reagents, and specialty hospital products. In addition to large pharmaceutical plants, many U.S. contract development and manufacturing organizations adopt modular sterile filling lines to serve multiple sponsors with short runs and frequent product changeovers.
Modern systems can be configured for manual, semi-automatic, or fully automatic operation. The most advanced lines combine isolator technology, automatic glove leak testing, robotic handling, online weight verification, no-glass-to-glass transport, 21 CFR Part 11-compatible data capture, and recipe-driven changeover management. This is especially relevant in U.S. facilities where labor efficiency, deviation reduction, and digital batch documentation are strategic priorities.
Product CategoryTypical Vial FormatWhy Aseptic Filling Is NeededCommon Fill RangeProduction ChallengeRecommended Line FeatureInjectable generics2 mL to 20 mLHigh-volume sterile dosing1 mL to 10 mLThroughput pressureHigh-speed automatic lineVaccines2 mL to 10 mLSterility and cold-chain sensitivity0.5 mL to 5 mLStrict batch controlIsolator and precise dosingBiologics2 mL to 50 mLProtein stability protection1 mL to 20 mLFoaming or shearGentle peristaltic fillingOncology drugs2 mL to 100 mLHigh potency containment1 mL to 50 mLOperator exposureClosed barrier technologyLyophilized products10 mL to 50 mLSterile fill before freeze drying2 mL to 30 mLPartial stoppering precisionLyophilizer integrationDiagnostic reagents2 mL to 30 mLConsistency and contamination control0.5 mL to 15 mLMulti-SKU flexibilityFast changeover designThe table makes clear that the same sterile vial filling process can be used across very different therapeutic categories, but the optimal machine architecture changes significantly with product risk and commercial goals.
The main applications are broad. Hospitals and public health systems depend on sterile filled vials for emergency medicines, IV additives, antibiotics, vaccines, and anesthesia products. Biotech companies use them for clinical and commercial biologics. CDMOs use flexible systems to serve diverse customer portfolios. Medical device and diagnostic manufacturers also use vial filling for reagent kits and specialized sterile liquids.
The biggest benefits are contamination control, dosage precision, batch reproducibility, and scalability. When integrated with modern environmental monitoring and electronic records, a strong aseptic line also helps reduce investigations and supports smoother inspections. In U.S. operations facing rising labor costs, automation brings another advantage: fewer interventions in the critical zone.
Operationally, the sterile vial filling process can improve:
For companies planning integrated projects, it is often helpful to evaluate not only the filler, but also utilities, water systems, clean steam, formulation preparation, logistics, and packaging. Providers with broad engineering capability can reduce coordination gaps between process areas. This is one reason some international buyers reviewing turnkey pharmaceutical engineering solutions look for a partner that can connect aseptic filling with upstream and downstream systems from the start.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Injectable Generics’, ‘Biologics’, ‘Vaccines’, ‘Oncology’, ‘CDMO Multi-Product’, ‘Diagnostics’],datasets: [{label: ‘Estimated U.S. Demand Index 2026’,data: [82, 91, 74, 88, 95, 63],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The chart above illustrates realistic relative demand across key U.S. segments. CDMO and biologics demand remains particularly strong because these organizations value flexible sterile vial filling platforms that can support both development and commercial production.
Application AreaPrimary UserMain BenefitTypical Batch ProfileCommon U.S. RegionWhy It MattersHospital injectablesLarge pharmaHigh output consistencyMedium to largeNew Jersey and MidwestSupports essential medicine supplyClinical biologicsBiotech companiesFlexible low-volume fillingSmall to mediumBoston and San DiegoAccelerates development programsContract manufacturingCDMOsFast changeoversVariableNorth Carolina and IndianaImproves multi-client utilizationVaccinesPharma and public health suppliersStrong sterility controlMedium to largePennsylvania and MarylandSupports public health readinessPotent oncologySpecialty manufacturersContainment and safetySmall to mediumCalifornia and TexasProtects operators and productsDiagnostic liquidsMedical device firmsRepeatable dosingSmall to mediumIllinois and MinnesotaSupports kit performance and qualityThis application matrix helps buyers match sterile filling capability to real production needs instead of purchasing a line that is either oversized or too limited for future growth.
There is no single best sterile vial filling process for every manufacturer. Selection should be based on product characteristics, contamination control strategy, and production economics. The main equipment architectures include linear lines, rotary lines, nested vial handling systems, monoblock configurations, isolator-based systems, and integrated fill-finish lines connected to lyophilizers.
Filling technology options also differ. Peristaltic pumps are favored for gentle product handling and disposable fluid path flexibility, especially in biotech and early commercial production. Piston pumps may offer strong repeatability for certain liquids at higher speeds. Time-pressure filling can suit specific product profiles but requires careful validation. Barrier protection choices include open RABS, closed RABS, and isolators, with isolators typically preferred for the highest contamination-control performance.
Additional technical options include:
Companies reviewing available systems through a supplier’s pharmaceutical equipment portfolio should compare not just machine speed, but line clearance logic, cleaning access, spare parts standardization, and validation documentation quality.
System TypeBest ForTypical SpeedCapital LevelKey AdvantageKey LimitationSemi-automatic aseptic fillerR&D and small clinical lotsLowLowerAffordable and flexibleMore operator involvementLinear automatic lineMulti-product commercial useMediumMediumEasy format changesLarger footprintRotary high-speed lineLarge-volume injectablesHighHighExcellent throughputLess suited to frequent changeoversIsolator-based lineHigh sterility assuranceMedium to highHighMinimal intervention riskLonger upfront integrationLyophilization-ready lineFreeze-dried productsMediumHighIntegrated partial stopperingMore complex process coordinationNested vial platformHigh-value low-volume productsLow to mediumMedium to highReduced container prep burdenHigher consumable costThe table shows how the best model depends on whether your priority is flexibility, speed, sterility assurance, or low-volume premium product handling.
Pharmaceutical manufacturers often compare the sterile vial filling process with prefilled syringe lines, ampoule filling, blow-fill-seal, cartridge filling, or outsourcing to a CDMO. The correct choice depends on administration route, product presentation, healthcare setting, and total lifecycle cost.
Vials remain one of the most flexible container types. They support multiple fill volumes, can work for liquid or lyophilized products, and fit both hospital and specialty applications. Prefilled syringes may improve convenience and reduce bedside preparation, but require different containment, siliconization, and plunger system considerations. Blow-fill-seal can be efficient for some high-volume sterile liquids but is less universal for premium biologics and complex product portfolios.
For U.S. buyers, another major comparison is in-house installation versus outsourced fill-finish. Outsourcing reduces initial capex but may limit schedule control and capacity assurance. This becomes critical when demand is volatile or when launch readiness depends on secured domestic supply.
OptionBest Use CaseFlexibilityInitial InvestmentCompliance ComplexityCommercial ConsiderationSterile vial fillingBroad injectable portfolioHighMedium to highHighStrong long-term versatilityPrefilled syringe fillingReady-to-administer productsMediumHighHighPremium presentation valueAmpoule fillingCertain liquid injectablesMediumMediumMediumLess common for some modern portfoliosBlow-fill-sealHigh-volume sterile solutionsLow to mediumHighHighEfficient for selected productsCartridge fillingDevice-combination productsMediumHighHighDevice integration requiredOutsourced fill-finishEarly-stage or low-capex strategyMediumLower upfrontShared with partnerLess direct control of capacityAs the table shows, the sterile vial filling process remains the most versatile route for companies that need broad portfolio support, scalable capacity, and the option to serve both liquid and lyophilized drug programs.
var ctxComp = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var comparisonChartSupplier = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Format Flexibility’, ‘Sterility Control’, ‘Scale-Up Ease’, ‘Changeover Speed’, ‘Lifecycle Cost Efficiency’, ‘Hospital Market Fit’],datasets: [{label: ‘Sterile Vial Filling’,data: [94, 93, 90, 82, 85, 96],backgroundColor: ‘#6f4e7c’},{label: ‘Alternative Formats Average’,data: [72, 86, 77, 75, 73, 68],backgroundColor: ‘#b07aa1’}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});This comparison chart highlights why vial lines remain attractive for broad pharmaceutical manufacturing strategies in the United States, especially where hospitals, wholesalers, and specialty channels all need dependable supply.
The U.S. market for sterile fill-finish equipment continues to expand due to biologics growth, domestic supply chain diversification, capacity localization, and stronger resilience planning after years of disruption in global healthcare logistics. Major investment corridors include the Northeast, the Research Triangle, Texas, and selected Midwest hubs with strong labor and utility infrastructure.
By 2026 and beyond, several trends are shaping the sterile vial filling process:
Policy and compliance pressure will also remain strong. While U.S. manufacturers focus on FDA expectations, many export-oriented companies must align with international GMP frameworks too. This is pushing buyers to choose systems that are globally acceptable rather than narrowly compliant for one geography.
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var lineChartGrowth = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’],datasets: [{label: ‘U.S. Sterile Fill-Finish Equipment Market Index’,data: [100, 108, 117, 129, 141, 154, 168],borderColor: ‘#2a9d8f’,backgroundColor: ‘rgba(42,157,143,0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: false } }}});The line chart presents a realistic growth pattern for the U.S. sterile fill-finish equipment market, reflecting ongoing demand from biotech, generics, and outsourced manufacturing.
var ctxArea = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var areaChartTrend = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’],datasets: [{label: ‘Share of Advanced Aseptic Technologies’,data: [38, 42, 47, 53, 60, 67, 73],borderColor: ‘#e76f51’,backgroundColor: ‘rgba(231,111,81,0.25)’,fill: true,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The area chart shows the shift toward isolators, robotics, advanced monitoring, and digitally integrated aseptic platforms. This trend will likely continue as facilities in the United States seek stronger sterility assurance with lower manual intervention.
Choosing the right supplier requires more than comparing machine speed and quotation price. Buyers should evaluate the manufacturer’s regulatory understanding, engineering depth, quality systems, project execution discipline, and long-term support network. In the United States, qualification packages, FAT quality, SAT efficiency, IQ/OQ/PQ support, and documentation readiness are often just as important as the equipment itself.
Key buying criteria include proven aseptic references, the quality of barrier technology integration, software architecture, spare parts support, validation deliverables, and the ability to coordinate with utilities and building systems. It also helps to assess whether the supplier has experience shipping to U.S. ports and handling installation planning around local codes, customs timing, and on-site acceptance requirements.
From a technology standpoint, some buyers prefer working with a partner that has broad expertise beyond one machine category. IVEN Pharmatech Engineering, for example, is known internationally for integrated pharmaceutical engineering and can support projects involving filling and packaging machinery, water treatment, intelligent logistics, and production line customization. That type of technological capability can be valuable when the sterile vial filling process must operate as part of a larger compliant plant ecosystem rather than as an isolated purchase.
Supplier Evaluation PointWhat to AskWhy It MattersGood SignWarning SignImpact on ProjectRegulatory expertiseHave you supported FDA-oriented projects?Reduces compliance gapsStrong validation templatesGeneric documentation onlySmoother qualificationAseptic design qualityHow are interventions minimized?Lowers contamination riskBarrier strategy is clearToo much manual accessHigher sterility assuranceCustomization capabilityCan the line match our vial sizes and products?Prevents mismatchApplication engineering teamOne-size-fits-all proposalBetter operational fitManufacturing depthWhich components are built in-house?Improves control and consistencyDedicated production plantsHeavy outsourcing without oversightBetter delivery predictabilityService supportWhat is your commissioning and training model?Speeds startupLifecycle support planSupport ends after shipmentFewer startup delaysReference projectsCan you share similar installations?Validates real capabilityMultiple comparable casesNo relevant referencesLower project riskThe table above gives a practical supplier checklist. It helps procurement, engineering, QA, and operations teams align on a structured decision rather than choosing based only on headline price.
Manufacturing capability matters as well. Suppliers with specialized factories for filling, packaging, water systems, and logistics can often coordinate interfaces more efficiently and control quality more tightly. Buyers exploring the background of a potential partner can review a company overview such as this pharmaceutical engineering profile to understand whether the supplier has the scale, patents, and production specialization needed for a serious aseptic project.
Service capability is the third pillar. The best suppliers do not stop at delivery. They support feasibility review, layout design, customization, installation, commissioning, training, documentation, and optimization. For sterile operations, post-installation support can be decisive because startup delays are expensive and aseptic investigations can quickly disrupt production plans.
Investment cost varies widely based on speed, barrier type, automation level, lyophilizer integration, and facility readiness. A small semi-automatic setup may fit pilot or clinical work at a relatively modest level, while a high-speed isolator-based commercial line with automated loading, inspection, and packaging can require a major capital program. In the United States, project budgets should include not only equipment price but also HVAC modifications, cleanroom upgrades, utilities, qualification, shipping, duties, installation labor, digital integration, and operator training.
Typical budget categories include:
ROI should be measured against expected throughput, reduced rejects, lower labor intensity, better batch success rates, and strategic supply security. For many U.S. manufacturers, the strongest ROI case is not only direct margin improvement but also avoided outsourcing dependency, faster launch timing, and more reliable customer service to hospitals and distributors.
Cost ElementLow-Complexity ProjectMid-Range ProjectHigh-End ProjectBudget RiskCost Control StrategyFilling and stoppering lineModerateHighVery highSpecification creepFreeze URS earlyBarrier technologyLow or noneMediumHighDesign changesDecide contamination strategy upfrontWasher and tunnelMediumMediumHighCapacity mismatchBalance line speeds carefullyFacility modificationLowMediumHighHidden utility workComplete site survey firstQualification and validationMediumMediumHighIncomplete documentsConfirm deliverables contractuallyTraining and serviceLowMediumMediumInsufficient operator readinessInclude multi-phase training planThis cost table is useful because it highlights where aseptic projects most often go over budget. In many cases, the hidden costs are not in the filler itself, but in integration, qualification, and utility adaptation.
When evaluating proposals, ask suppliers for a phased capex and opex model. That should cover expected throughput, staffing assumptions, preventive maintenance, parts replacement, and energy usage. Sustainability is becoming more relevant in 2026 planning, so energy-efficient tunnel design, optimized compressed air use, and lower cleanroom burden through isolators can improve long-term economics.
The biggest risks in sterile vial filling investments are contamination events, design mismatch, inadequate qualification, poor utility integration, and weak supplier support. A line may look impressive during procurement but still fail commercially if interventions are awkward, changeovers are too slow, software is difficult to validate, or spare parts are hard to obtain in the United States.
Buyers should pay close attention to these issues:
A practical case study pattern seen in the market involves U.S. manufacturers adding sterile vial capacity to reduce dependence on overseas fill-finish. Plants near Newark and Philadelphia often prioritize access to East Coast logistics and skilled labor, while facilities in Texas and California may emphasize regional distribution resilience and proximity to growing biotech activity. In both scenarios, success usually depends on early layout planning, clear URS definition, and careful coordination between process equipment and cleanroom design.
For organizations seeking an integrated approach, IVEN’s manufacturing and service strengths can be relevant. The company operates specialized production bases for pharmaceutical equipment categories and offers lifecycle support covering design, customization, installation, commissioning, validation assistance, training, and optimization. That service model can reduce handoff risk in complex aseptic projects, particularly when buyers want one accountable partner across multiple systems. Companies ready to discuss project scope can use direct project contact options to begin specification review and planning.
Another risk factor is timeline pressure. Many U.S. projects underestimate how long URS approval, detailed design, FAT scheduling, factory remediation, shipping, installation, SAT, media fills, and PQ will take. A realistic schedule with built-in contingency is essential. So is local coordination for rigging, cleanroom readiness, and utility verification before equipment arrival.
1. What products most commonly use the sterile vial filling process in the United States?Injectable generics, vaccines, biologics, oncology drugs, anesthetics, anti-infectives, lyophilized medicines, and diagnostic reagents are among the most common.
2. Is an isolator always better than RABS?Not always, but isolators generally provide stronger contamination control and lower intervention risk. The right choice depends on product risk, batch size, facility strategy, and budget.
3. How long does it take to install and qualify a new sterile vial filling line?Timelines vary, but a full project can range from several months for a simple upgrade to well over a year for a highly integrated commercial aseptic line with facility modifications and extensive qualification.
4. What is the main difference between sterile vial filling and prefilled syringe filling?Vial filling offers broader format flexibility and is often better for diverse injectable portfolios, while prefilled syringe filling is optimized for ready-to-administer convenience and specific delivery formats.
5. What should be included in the supplier quotation review?Review speed, format range, barrier system, utility requirements, software scope, FAT/SAT protocols, documentation package, spare parts, training, service response, and validation support.
6. Can one line handle multiple vial sizes?Yes, many modern systems can manage multiple formats, but buyers should confirm change parts, changeover time, recipe management, and qualification boundaries in advance.
7. What are the top ROI drivers?Higher throughput, fewer rejects, reduced contamination events, lower labor dependency, better batch release success, and improved supply security are the main ROI drivers.
8. Why do U.S. manufacturers often prefer integrated engineering support?Because sterile filling projects affect utilities, cleanrooms, documentation, automation, and downstream packaging. Integrated support reduces interface risk and can accelerate startup.
9. How important is local service access?Very important. Downtime in aseptic production is expensive, so responsive technical support, spare parts planning, and operator training are essential for stable operation.
10. What should buyers look for in a long-term partner?Look for a supplier with strong regulatory understanding, robust manufacturing capability, documented aseptic experience, customization strength, and lifecycle service support.
In summary, the sterile vial filling process is a strategic investment for pharmaceutical production in the United States. The right system can strengthen sterility assurance, improve operational flexibility, support future regulatory expectations, and create a more resilient domestic supply chain. Buyers that combine clear technical requirements with disciplined supplier evaluation are far more likely to achieve strong long-term value.