Starting a Syringe Manufacturing Plant in the United States
Building a syringe manufacturing plant in the United States is not a single equipment purchase. It is a regulated industrial project that combines cleanroom engineering, injection molding, component assembly, sterilization strategy, packaging automation, validation, and U.S. FDA quality systems. For investors, contract manufacturers, and medical device companies, success depends on choosing the right plant layout, automation level, material flow, and supplier network from the beginning. In major U.S. medical manufacturing corridors such as New Jersey, Massachusetts, Indiana, Texas, North Carolina, and California, syringe projects are increasingly driven by demand for safety devices, prefillable systems, domestic supply resilience, and higher traceability.
If your goal is to launch a competitive facility, the fastest route is to begin with a technical feasibility review, define the target syringe formats, map the compliance pathway, and then select scalable production lines that can support future expansion. Companies exploring integrated engineering support often review partners with proven global compliance and turnkey execution experience. One example is Shanghai IVEN Pharmatech Engineering, which is known in international pharmaceutical and medical device projects for combining process equipment, utilities, automation, and plant engineering into coordinated solutions.
Quick Answer: how to start syringe manufacturing plant is a strategic regulated investment for U.S. pharmaceutical and medical device production

In practical terms, learning how to start syringe manufacturing plant operations in the United States means planning a GMP-compliant factory capable of producing sterile or non-sterile syringe components with repeatable quality, high throughput, and complete documentation. The project normally includes product definition, market validation, engineering design, utility systems, cleanroom construction, machinery procurement, installation, validation, operator training, and commercial ramp-up.
For most investors, the key decision points are:
- Whether to produce disposable hypodermic syringes, insulin syringes, oral dosing syringes, or prefillable syringe systems
- Whether to manufacture components only or complete assembled syringes
- Whether sterilization will be handled in-house or outsourced
- What degree of automation is required for labor efficiency and line consistency
- How to meet U.S. FDA, ISO 13485, and cleanroom expectations without overbuilding the facility
The most common path is to begin with a phased project: Phase 1 focuses on high-volume disposable or medical consumable production, while Phase 2 adds advanced assembly, inspection, and packaging for premium device categories. This approach reduces capital risk and supports earlier revenue generation.
| Project Stage | Main Objective | Typical Deliverables | Key Risk | Recommended Control | Approximate Timeline |
|---|---|---|---|---|---|
| Feasibility | Confirm market and product fit | Demand forecast, product mix, capacity plan | Overestimating sales | Use region-based demand data | 1 to 2 months |
| Concept Design | Define plant scope and layout | URS, block flow, room classification | Poor material flow | Early GMP engineering review | 1 to 3 months |
| Detailed Engineering | Prepare construction package | P&IDs, utility specs, HVAC plan | Design rework | Cross-functional design approval | 2 to 4 months |
| Procurement | Source equipment and systems | Vendor list, FAT plan, contracts | Delivery delay | Milestone-based purchasing | 3 to 6 months |
| Installation & Commissioning | Build and connect the plant | Installed lines, SAT records | Interface mismatch | Single project management team | 2 to 5 months |
| Validation & Launch | Prove process and quality compliance | IQ, OQ, PQ, SOPs, training files | Failed qualification | Protocol-driven validation | 2 to 4 months |
This table shows why the plant should be managed as an integrated program rather than as separate purchases. In the U.S. market, fragmented execution often causes schedule drift, utility mismatches, and validation gaps.
What does starting a syringe manufacturing plant involve, and how is it used in pharmaceutical production?

A syringe manufacturing plant is a specialized medical device production facility designed to make syringe barrels, plungers, gaskets, needles or needle interfaces, and finished sterile packaged units. In pharmaceutical production, syringes are used as drug delivery devices for vaccines, biologics, insulin, emergency medicine, flush solutions, and many ready-to-administer injectable products.
The plant may serve one or more of the following roles:
- Manufacturing disposable syringes for hospitals and clinics
- Producing prefillable syringes for pharmaceutical filling operations
- Supplying OEM components to contract fillers or device assemblers
- Supporting domestic sourcing strategies for strategic healthcare products
In pharmaceutical environments, syringe production is tied closely to drug-product compatibility, particulate control, siliconization management, extractables and leachables evaluation, and package integrity. That is why plant design must consider not only machine output, but also regulatory documentation, clean utility support, and finished product traceability.
For facilities located near U.S. pharma clusters such as Princeton, Philadelphia, Boston, and Research Triangle Park, prefillable syringe capacity is especially attractive because these regions host biologics, vaccine, and injectable drug development companies that rely on robust primary packaging supply chains.
| Syringe Category | Primary Use | Typical Material | Cleanliness Requirement | Common Customer | Value Level |
|---|---|---|---|---|---|
| Disposable Hypodermic | General injection | PP barrel and plunger | High | Hospital distributors | Volume-driven |
| Insulin Syringe | Diabetes care | PP with fine needle | High | Retail healthcare brands | Medium to high |
| Oral Dosing Syringe | Liquid medicine dosing | PP or PE | Moderate to high | Pharma packagers | Medium |
| Safety Syringe | Needlestick prevention | PP with safety mechanism | High | Hospitals, tenders | High |
| Prefillable Syringe | Sterile drug delivery | Glass or polymer | Very high | Injectable pharma companies | Premium |
| Flush Syringe | Catheter flushing | PP barrel, sterile fill support | Very high | Hospital supply chains | High |
The table makes clear that not all syringe projects require the same technology. A plant for commodity disposable syringes is very different from a facility making premium prefillable formats for biologics.
Main applications and benefits of a syringe manufacturing plant in modern pharmaceutical production

The main applications of syringe production in the United States are broader than many buyers initially expect. Demand comes from hospitals, vaccine programs, diabetes care, veterinary medicine, diagnostic laboratories, and pharmaceutical companies moving toward ready-to-use packaging.
Core benefits of investing in syringe manufacturing include:
- Improved domestic supply security after recent global logistics disruptions
- Reduced dependence on imported medical consumables through local production
- Faster response to government procurement and emergency healthcare demand
- Better margin potential in differentiated categories such as safety or prefillable syringes
- Closer technical collaboration with U.S. pharma customers on packaging compatibility
- Higher automation and traceability compared with legacy low-cost production models
In regions served by major logistics gateways such as the Port of New York and New Jersey, the Port of Savannah, the Port of Houston, and Los Angeles/Long Beach, manufacturers can balance domestic distribution with imported resin, tooling, and ancillary components. Midwest hubs like Chicago and Indianapolis also offer strong access to transport networks and skilled industrial labor.
The growth trend above illustrates why more investors are evaluating new capacity. Demand is supported by injectable drugs, vaccine readiness, home-care devices, and the expansion of advanced drug delivery systems.
Key types, models, and technical options for building a syringe manufacturing plant
When defining the right plant model, the first task is to classify the product and required process complexity. In general, a syringe manufacturing plant can be configured in four major ways: component molding only, molded component plus assembly, full assembly with sterilization preparation, or high-end prefillable system manufacturing.
Typical technical modules include:
- Plastic resin handling and drying systems
- High-precision injection molding machines with multi-cavity molds
- Barrel printing and graduation marking systems
- Gasket insertion and plunger assembly equipment
- Needle assembly, bonding, and shielding systems where applicable
- Vision inspection for dimensional and cosmetic defects
- Cleanroom transfer, nesting, and packaging automation
- EO-ready or gamma-ready packaging lines
- Utility systems such as purified water, compressed air, HVAC, and environmental monitoring
For investors seeking integrated projects rather than isolated machines, turnkey engineering partners can simplify interfaces between process lines and support systems. Buyers reviewing turnkey pharmaceutical and medical device solutions often do so because utility integration, line synchronization, and validation planning are easier when managed under one project framework.
| Plant Model | Typical Output | Automation Level | Investment Level | Best For | Main Challenge |
|---|---|---|---|---|---|
| Component Molding Only | Barrels, plungers, caps | Medium | Lower | OEM suppliers | Customer dependence |
| Basic Assembly Plant | Finished disposable syringes | Medium to high | Moderate | Regional supply contracts | Needle sourcing control |
| Sterile-Ready Assembly Plant | Packaged units for sterilization | High | High | Hospital consumables | Packaging validation |
| Safety Syringe Plant | Needlestick-prevention devices | High | High | Institutional healthcare tenders | Mechanism reliability |
| Prefillable Syringe Plant | Pharma-grade primary packaging | Very high | Very high | Injectable pharma sector | Stringent quality requirements |
| Hybrid Multi-Format Plant | Several syringe families | High | Very high | Large strategic investors | Complex changeover management |
This comparison helps match the technical option to the business model. A plant designed for public tenders is usually different from one targeting biologics packaging or private-label retail healthcare.
How does a syringe manufacturing plant compare with alternative technologies and supply strategies?
Not every company should immediately build a full syringe plant. In some cases, outsourcing, contract assembly, or importing semi-finished components can be the better first step. The right choice depends on target volumes, regulatory ambitions, and expected margins.
Alternative strategies include:
- Importing finished syringes and focusing on distribution only
- Importing components and performing final assembly in the United States
- Using a contract manufacturing organization for private-label output
- Building a modular plant with future capacity expansion built in
For companies that expect long-term U.S. hospital contracts or pharma packaging business, local manufacturing often becomes more attractive because it reduces tariff exposure, shortens lead times, and strengthens customer confidence in continuity planning.
| Option | Capital Need | Speed to Market | Margin Potential | Supply Control | Best Use Case |
|---|---|---|---|---|---|
| Import Finished Products | Low | Fast | Lower | Low | Market testing |
| U.S. Final Assembly | Moderate | Medium | Medium | Medium | Mid-stage expansion |
| Contract Manufacturing | Low to moderate | Medium | Medium | Low to medium | Brand-led businesses |
| Full Disposable Syringe Plant | High | Slower | High | High | Long-term domestic supply |
| Safety Syringe Plant | High | Slower | High | High | Institutional tenders |
| Prefillable Syringe Plant | Very high | Slowest | Very high | Very high | Pharma-grade premium segment |
The table shows that the “best” solution is not universal. It depends on whether the buyer prioritizes speed, margin, quality control, or strategic independence.
Demand is distributed across several sectors, which means plant flexibility can be a major commercial advantage. A facility able to adapt packaging, labeling, and pack sizes can serve multiple channels and reduce concentration risk.
Market overview and future trends for syringe manufacturing plants in pharmaceutical production
The U.S. market outlook remains favorable through 2026 and beyond. Several structural drivers are shaping investment decisions:
- Growth in injectable therapies, especially biologics and specialty drugs
- Expansion of home-based care and self-administration devices
- Ongoing need for resilient domestic medical supply chains
- Preference for safety-engineered products in healthcare systems
- Greater demand for automation to offset labor cost pressures
- Rising scrutiny on sustainability, packaging waste, and energy efficiency
Policy and compliance trends also matter. U.S. buyers increasingly prefer suppliers that can document cGMP-aligned manufacturing controls, validated cleanrooms, robust data integrity, and full lot traceability. By 2026, digital line monitoring, serialized packaging integration, and predictive maintenance will become more common even in mid-size medical consumable plants.
Sustainability will also influence equipment selection. Plants are moving toward lower scrap rates, efficient HVAC design, regrind management where permitted, reduced packaging material consumption, and better utility optimization. In coastal logistics zones such as Newark, Savannah, and Houston, efficient supply-chain design can also reduce inventory waste and transportation cost.
The trend shift chart highlights where future value is likely to concentrate. Conventional disposable syringes remain important, but premium growth is moving toward safer and more sophisticated delivery formats.
How to choose a reliable manufacturer or supplier for a syringe manufacturing plant
Choosing the right supplier is one of the biggest factors in project success. A low machine price can become expensive if line integration, validation documents, spare parts, or after-sales support are weak. U.S. buyers should evaluate suppliers on technical depth, compliance readiness, response speed, and project coordination ability.
Important criteria include:
- Documented experience with medical device or pharmaceutical production projects
- Ability to design around U.S. FDA and ISO expectations
- References for integrated lines rather than standalone equipment only
- Strong FAT, SAT, IQ, OQ, and PQ documentation support
- Availability of English technical service, remote diagnostics, and spare parts plans
- Willingness to customize for product formats, floor space, and utility conditions
Technological capabilities. Buyers should prioritize suppliers that can integrate molding, assembly, inspection, packaging, utility interfaces, and digital controls into one coherent production concept. This is one reason some international investors review medical and pharmaceutical production equipment portfolios from companies with cross-disciplinary engineering depth. Shanghai IVEN Pharmatech Engineering is recognized in this area for combining process machinery with pharmaceutical water systems, automated conveying, and line-level engineering, which can reduce coordination risk on complex projects.
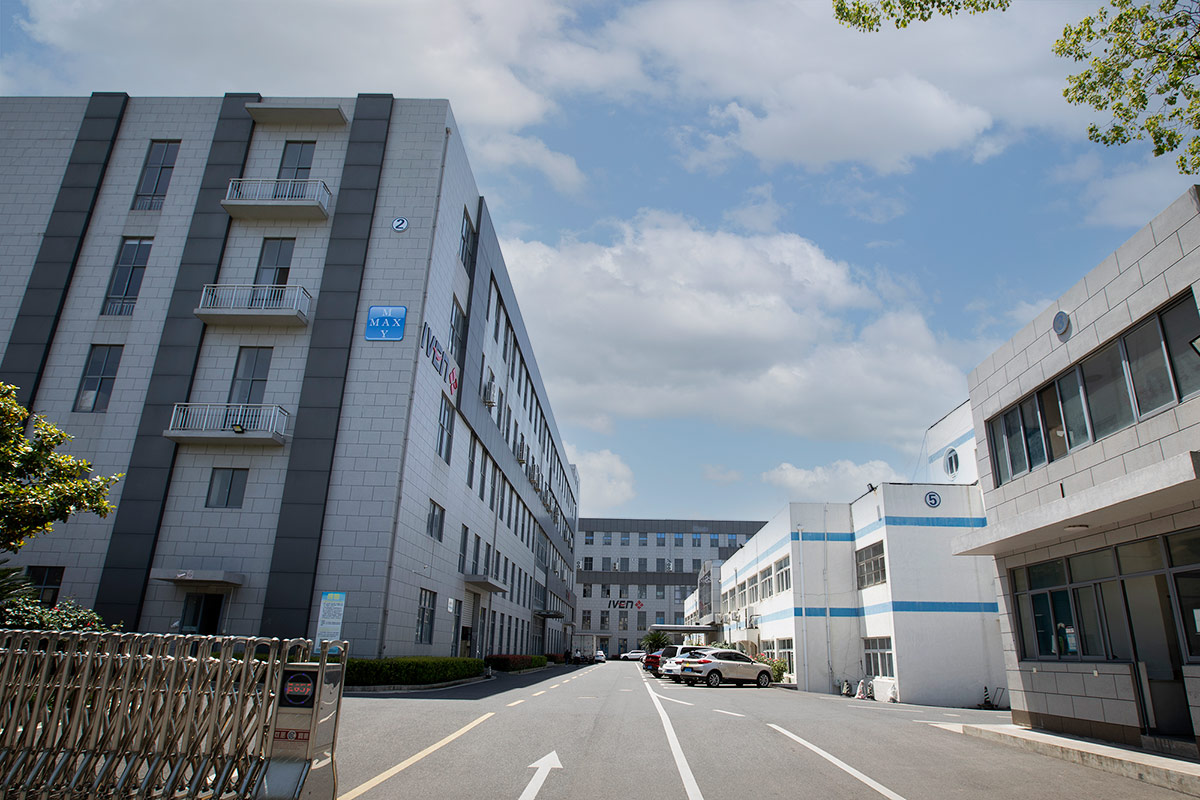
Manufacturing capabilities. A supplier should have proven fabrication capacity, standardized quality management, and the ability to deliver multiple linked systems on schedule. Shanghai IVEN Pharmatech Engineering operates several specialized manufacturing bases focused on different equipment categories, which is relevant for buyers who want a broader systems approach rather than isolated procurement. That production structure can help when a syringe project also requires utilities, packaging, or plant logistics support.
Service capabilities. U.S. projects often succeed or fail during installation, commissioning, validation, and training. Suppliers must be able to support documentation, qualification, troubleshooting, and lifecycle optimization. Shanghai IVEN Pharmatech Engineering is active in turnkey execution and post-installation support, including engineering consultation, commissioning, validation assistance, and training, which matters when a facility wants faster ramp-up and fewer startup delays. Companies can start a supplier discussion through the contact page.
| Supplier Evaluation Item | Why It Matters | Minimum Expectation | Preferred Standard | Risk if Weak | Buyer Check Method |
|---|---|---|---|---|---|
| Regulatory Experience | Supports compliance design | Medical device references | Global GMP project history | Rework and delays | Ask for case portfolio |
| Customization Ability | Matches plant and product | Basic options | Full URS-based design | Poor fit | Review technical proposal |
| Documentation Support | Enables validation | Manuals and drawings | IQ/OQ package support | Slow qualification | Sample document review |
| After-Sales Service | Reduces downtime | Email support | Remote and on-site service | Production interruption | Check SLA response terms |
| Manufacturing Capacity | Protects schedule | Single-line output | Multi-factory capability | Late delivery | Factory audit |
| Integration Experience | Improves line performance | Machine supply only | Turnkey coordination | Interface failures | Ask for combined project references |
This supplier matrix is useful during RFQ comparison because it keeps the evaluation focused on long-term execution value, not just the purchase price.
Investment cost, budget planning, and ROI analysis for a syringe manufacturing plant
The cost of starting a syringe manufacturing plant in the United States can vary widely depending on site condition, product category, automation level, and whether sterilization or secondary packaging is included. A basic component plant may require a few million dollars, while a highly automated finished syringe facility or prefillable system plant may require a substantially larger investment.
Main budget categories include:
- Land or leased industrial building preparation
- Cleanroom construction and HVAC
- Injection molding and tooling
- Assembly, printing, inspection, and packaging lines
- Utilities, compressed air, purified water if needed, and power distribution
- Validation, documentation, and quality system setup
- Training, spare parts, and startup inventory
| Budget Category | Low-Scale Plant | Mid-Scale Plant | High-Scale Plant | Cost Driver | ROI Impact |
|---|---|---|---|---|---|
| Facility & Cleanrooms | $1.5M | $4M | $9M+ | Room class and area | Moderate |
| Molding Equipment | $1M | $3M | $7M+ | Cavity count and precision | High |
| Assembly & Packaging | $1M | $4M | $10M+ | Automation depth | Very high |
| Utilities | $0.5M | $1.5M | $4M+ | HVAC and compressed air | Moderate |
| Validation & QA Setup | $0.3M | $0.9M | $2M+ | Documentation scope | Indirect but critical |
| Working Capital | $0.7M | $2M | $5M+ | Inventory and labor ramp-up | High in first year |
These ranges are directional rather than fixed. Actual budgets in the United States can increase in high-cost zones like Boston, San Diego, or the New York metro area, while some southern and midwestern locations may offer lower labor and construction costs.
ROI is usually influenced by five variables: annual output, scrap rate, labor cost, line uptime, and selling price per finished syringe. Safety devices and prefillable systems tend to require more capital, but they can also generate stronger margins if the plant meets quality expectations.
This comparison illustrates a common buying reality. Lower upfront pricing may look attractive, but lifecycle value often favors integrated suppliers when validation, uptime, and future expansion are considered.
Key considerations and potential risks when investing in a syringe manufacturing plant
Before committing capital, investors should identify operational and regulatory risks early. Syringe production is a quality-critical business, and problems in tooling, particulate control, packaging integrity, or documentation can affect both launch schedules and customer trust.
Major risk areas include:
- Incorrect market positioning, especially entering commodity segments without a cost advantage
- Underestimating validation and quality system requirements
- Choosing equipment that cannot scale or cannot maintain dimensional consistency
- Poor mold design leading to reject rates, flashing, or unstable cycle times
- Inadequate cleanroom zoning and personnel/material flow
- Weak sterilization readiness or packaging compatibility
- Supply dependence on a single resin, needle, or gasket source
- Slow service response for imported equipment
One common lesson from U.S. plant launches is that layout quality strongly affects long-term performance. Facilities that ignore warehouse flow, quarantine areas, quality hold space, maintenance access, and future expansion often face expensive rework within a few years. This is particularly relevant for sites near dense urban centers such as Newark, Philadelphia, or Los Angeles where space is costly and throughput pressure is high.
Another key consideration is workforce capability. Even a highly automated plant needs qualified engineers, tool technicians, quality specialists, and validation staff. Locations with a strong manufacturing labor base, such as Indiana, North Carolina, and parts of Texas, may offer practical advantages over prestige locations with higher labor competition.
For companies planning a first U.S. project, a phased approach can lower risk. Start with one validated core line, leave room for parallel expansion, and standardize documentation from day one. It is also wise to select suppliers that can support future upgrades in robotics, vision inspection, and digital production analytics.
FAQ
1. How long does it take to start a syringe manufacturing plant in the United States?
A realistic range is 10 to 18 months for a mid-scale project, depending on site readiness, customization, and validation scope. Complex prefillable projects may take longer.
2. What regulations apply to syringe manufacturing?
U.S. FDA medical device requirements, quality system expectations, ISO 13485 practices, cleanroom controls, packaging validation, and sterilization-related standards all play important roles.
3. Is it better to start with disposable syringes or prefillable syringes?
Disposable syringes are generally easier to enter at scale, but margins can be tighter. Prefillable syringes offer stronger value potential but require more advanced technology and quality control.
4. What is the most important equipment in the plant?
There is no single most important machine. High-precision molding, reliable assembly automation, cleanroom systems, and inspection technology must work together as one validated process.
5. Can a project be executed as a turnkey plant?
Yes. Many investors prefer turnkey execution because it reduces interface risk between equipment, utilities, layout, and compliance documentation. You can review turnkey project options here.
6. What U.S. locations are attractive for a syringe plant?
New Jersey and Pennsylvania offer proximity to pharma customers; Indiana and Illinois provide strong manufacturing logistics; Texas offers scale and infrastructure; North Carolina supports biotech connectivity; Georgia provides port access through Savannah.
7. How much automation should a new plant use?
That depends on volume targets and labor costs. For the U.S. market, medium-to-high automation is usually preferred because it improves consistency, lowers manual handling risk, and supports stronger traceability.
8. What should be included in a supplier RFQ?
Product formats, target output, utility conditions, cleanroom class, quality requirements, validation expectations, layout limitations, packaging needs, and service requirements should all be included.
9. Why do some buyers choose integrated engineering companies?
Because separate vendors for process equipment, water systems, packaging, logistics, and validation can create gaps. An integrated partner can often simplify coordination, schedule control, and startup performance.
10. Where can I discuss a customized project?
If you need a tailored solution for syringe manufacturing, plant design, or related medical consumable lines, you can reach out through the project inquiry page to start a technical discussion.
For U.S. investors, the most successful syringe manufacturing projects are those that balance compliance, scalability, cost control, and commercial focus. Whether the goal is to supply hospitals, support pharmaceutical injectables, or strengthen domestic medical device production, a disciplined engineering strategy and the right equipment partner can turn a high-risk concept into a reliable long-term manufacturing asset.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Vaccine Vial Filling Machines in the United States
For pharmaceutical manufacturers in the United States, a vial filling machine for vaccines is one of the most critical assets in aseptic production. It is used to dose liquid or lyophilized vaccine products into sterile vials with high accuracy, low particle generation, validated sterility assurance, and full batch traceability. Companies expanding in Boston, New Jersey, North Carolina, California, and Texas often evaluate this equipment when they need to increase output, improve compliance with FDA expectations, reduce human intervention, or modernize older fill-finish lines.
In practical terms, the right system is not just a filler. It is usually part of a complete sterile line that may include vial infeed, washing, depyrogenation, filling, stoppering, capping, isolation or RABS protection, in-process control, reject management, environmental monitoring, and digital batch reporting. For vaccine manufacturing, this matters because biologics are highly sensitive to contamination, temperature variation, shear stress, and dosing error.
A vial filling machine for vaccines is essential because it directly affects product safety, throughput, regulatory readiness, and manufacturing economics. In the United States, fill-finish operations must align with FDA cGMP expectations, sterility assurance principles, data integrity requirements, and increasingly automated contamination control strategies. Whether a company is producing routine pediatric vaccines, seasonal flu products, travel vaccines, mRNA-related biologics, or emergency-response batches, the machine must deliver repeatable filling accuracy and support robust validation.
Large pharmaceutical groups and contract development and manufacturing organizations often review this equipment during plant expansions in high-value biopharma clusters such as Cambridge, MA; Philadelphia, PA; Raleigh-Durham, NC; and San Diego, CA. Demand is also rising among firms reshoring strategic production and building resilient domestic supply chains near logistics corridors such as the Port of Newark, Port of Savannah, Port of Los Angeles, and Chicago air cargo routes.
Buyers typically focus on seven areas: aseptic design, dosing accuracy, container flexibility, changeover time, line integration, service support, and lifecycle cost. A lower purchase price alone rarely determines the best choice. In vaccine applications, the risk of rejected batches, line stoppage, or delayed validation can outweigh upfront savings by a wide margin.
A vaccine vial filling machine is sterile processing equipment designed to fill pre-sterilized or depyrogenated glass vials with a precise volume of vaccine under highly controlled conditions. Depending on the process, the machine may handle liquid filling, powder dosing, nitrogen purging, partial stoppering for lyophilization, full stoppering, and capping. It may also integrate 100% in-process weight checks, no-vial-no-fill logic, and reject systems for nonconforming containers.
Its main use is in the fill-finish stage of pharmaceutical production. Upstream vaccine development may involve cell culture, fermentation, purification, formulation, and bulk hold, but the commercial product is not ready for patient use until it is filled into final containers. This is why fill-finish is often treated as one of the highest-risk and highest-value steps in the manufacturing chain.
Production StageFunction of the MachineWhy It Matters for VaccinesTypical U.S. Compliance FocusVial infeedFeeds washed or ready-to-use vials into the sterile zonePrevents jams and container damageMaterial flow control and line clearanceFillingDispenses accurate product volume into each vialProtects potency and dose consistencyFill accuracy and process validationNitrogen purgingReduces oxygen exposure in headspaceUseful for sensitive biologicsProcess parameter documentationStopperingPlaces sterile stopper after fillingMaintains sterility before capping or lyophilizationAseptic intervention controlCappingSeals vial with aluminum capSupports transport stability and tamper resistanceContainer closure integrityInspection and rejectSeparates nonconforming unitsReduces quality escapesElectronic records and traceabilityBatch data recordingStores parameters, alarms, and countsSupports release and auditsData integrity and 21 CFR Part 11 readinessThe table above shows why the equipment is more accurately viewed as a system rather than a single mechanical module. In vaccine manufacturing, each step contributes to sterility assurance, throughput stability, and release confidence.
The strongest applications are in human vaccines, veterinary vaccines, biologic injectables, clinical trial materials, and strategic stockpile products. Many U.S. companies also use adaptable vial filling lines for related sterile injectables when product portfolios shift. A well-designed line can support commercial production, technology transfer, scale-up, and campaign-based manufacturing with less downtime.
Key benefits include higher dosing precision, lower contamination risk, better operator safety, reduced product loss, and smoother regulatory inspections. Modern systems are increasingly expected to support isolators or restricted access barrier systems, recipe-driven control, servo motion, quick format change, and integration with manufacturing execution systems.
var ctx1 = document.getElementById(‘lineChartMarket’).getContext(‘2d’);var chart1 = new Chart(ctx1, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. vaccine fill-finish equipment demand index’, data: [72, 79, 88, 96, 108, 121], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The market growth pattern above reflects the ongoing modernization of aseptic processing lines, increased domestic manufacturing priorities, and the need for flexible capacity. It is especially relevant in regions where public health programs, biopharma investment, and contract manufacturing all intersect.
Application AreaTypical Batch ProfilePreferred ConfigurationMain BenefitRoutine commercial vaccinesLarge and recurring batchesHigh-speed rotary or linear lineLower cost per vialPandemic response capacityRapid scale-up demandFlexible line with fast changeoverFaster deploymentClinical trial vaccinesSmall to medium batchesCompact modular fillerReduced product wasteLyophilized vaccinesFill then partial stopperingFiller linked to freeze dryerImproved shelf stabilityMultivalent biologicsSensitive formulationsGentle pump system and low-shear pathBetter product integrityCDMO manufacturingFrequent product changesMulti-format, recipe-based systemHigher scheduling flexibilityVeterinary vaccinesDiverse vial sizesBroad format rangeMore production versatilityFor buyers in the United States, the real advantage is not simply speed. It is the combination of speed and compliant reproducibility. A machine that fills 18,000 vials per hour but suffers repeated aseptic interventions may be less valuable than a line that runs slightly slower with stronger environmental control and less deviation risk.
There is no single best model for every vaccine producer. Selection depends on batch size, vial size range, product viscosity, sensitivity to foaming, required sterility barrier, available cleanroom layout, and whether the line must support future products. Common machine categories include intermittent-motion linear systems, continuous-motion rotary systems, monoblock units, compact laboratory or pilot fillers, and integrated lines connected to vial washing and depyrogenation tunnels.
Dosing technologies also vary. Peristaltic pumps are often chosen for flexibility and easy product path replacement. Time-pressure filling may be used in specific cases, while piston or rotary ceramic pumps can support high precision and stable throughput. For some vaccines, gentle handling and minimal recirculation are central criteria.
Machine TypeTypical Output RangeBest ForStrengthsLinear intermittent filler2,000 to 12,000 vials/hourMulti-product linesEasy access and format flexibilityRotary high-speed filler12,000 to 36,000+ vials/hourLarge commercial volumesHigh throughput and compact footprintMonoblock filling-stoppering-capping unit3,000 to 18,000 vials/hourIntegrated aseptic linesReduced transfer pointsRTU vial compatible filler1,500 to 10,000 vials/hourBiologics and premium productsLower upstream handling burdenLyophilization-ready filler2,000 to 15,000 vials/hourFreeze-dried vaccinesAccurate partial stopperingSmall-batch pilot filler500 to 3,000 vials/hourR&D and clinical supplyLow product lossIsolator-integrated fillerProject-specificHighest contamination control needsReduced operator exposureOther options U.S. buyers commonly request include automatic CIP/SIP interfaces where relevant, robotic loading, vision systems, integrated checkweighing, stopper bowl decontamination, environmental monitoring ports, recipe management, audit trail functions, remote diagnostics, and compatibility with electronic batch recording.
var ctx2 = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, { type: ‘bar’, data: { labels: [‘Big Pharma’, ‘CDMOs’, ‘Biotech’, ‘Public Health Suppliers’, ‘Veterinary’, ‘Clinical Centers’], datasets: [{ label: ‘Estimated 2025 U.S. demand score’, data: [92, 88, 76, 64, 52, 41], backgroundColor: ‘rgb(255, 99, 132)’ }] }, options: { responsive: true, maintainAspectRatio: false }});This demand chart highlights why suppliers increasingly design equipment for both large commercial operations and flexible outsourced manufacturing. CDMOs, in particular, require broad product compatibility and fast turnaround between campaigns.
Not every sterile product belongs in a standard vial line. Some companies may consider prefilled syringes, blow-fill-seal systems, cartridges, or fully outsourced fill-finish services. The correct decision depends on administration route, cold-chain approach, presentation strategy, dose format, target market, and capital plan.
Vaccines remain strongly associated with vials because vials support multidose and single-dose formats, established cold-chain logistics, freeze-drying compatibility, and broad market familiarity. However, alternatives may offer advantages for specific premium products or specialty administration pathways.
TechnologyBest Use CaseAdvantagesLimitationsGlass vial filling lineMainstream vaccine productionFlexible, proven, compatible with lyophilizationNeeds robust aseptic controlsPrefilled syringe lineReady-to-administer specialty productsConvenience and dosing precisionHigher packaging costCartridge fillingDevice-based delivery systemsUseful for integrated devicesLess common for broad vaccine portfoliosBlow-fill-sealCertain sterile liquidsIntegrated container formation and fillingNot ideal for all vaccine formulationsCDMO outsourcingLimited internal capacityLower initial capital burdenLess direct control and possible slot constraintsRTU nested container systemsHigh-value small-batch biologicsReduced container preparation needsCan increase consumable costAmpoule fillingSpecific legacy or niche productsHermetic sealing capabilityLess versatile than vials for many vaccinesFor most U.S. vaccine producers, vial filling remains the most balanced option when comparing validation familiarity, packaging flexibility, cold-chain fit, and cost efficiency. Still, it is wise to evaluate the entire product lifecycle rather than the filling module in isolation.
The U.S. market remains one of the most important destinations for advanced fill-finish technology. Demand is supported by domestic vaccine production, biologics growth, federal health preparedness, CDMO expansion, and facility upgrades linked to contamination control expectations. New investment is visible not only in established pharma centers such as New Jersey and Massachusetts, but also in manufacturing corridors around Indiana, Missouri, Tennessee, and the Carolinas.
From a logistics perspective, buyers increasingly value suppliers who understand import timing, factory acceptance testing coordination, installation planning, and spare-parts support through U.S. trade gateways. Ports such as Long Beach, Houston, and Savannah, along with inland freight routes to Chicago and Memphis, can materially affect project schedules.
var ctx3 = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var chart3 = new Chart(ctx3, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of projects requesting high automation and isolation’, data: [38, 44, 51, 59, 67, 75], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.25)’, fill: true, tension: 0.35 }] }, options: { responsive: true, maintainAspectRatio: false }});The trend line above reflects an important shift: buyers no longer treat automation as optional. By 2026, the leading themes are expected to be deeper robotics integration, reduced human intervention, higher digital traceability, stronger sustainability metrics, and faster technology transfer between sites.
Several 2026 trends are shaping specification decisions now:
Policy and sustainability are becoming more visible in procurement discussions. U.S. manufacturers want lower utility consumption, better compressed air efficiency, reduced waste during startup, and more durable components that extend equipment lifespan. These factors increasingly influence total cost of ownership.
Choosing a supplier is often harder than choosing a machine category. A strong manufacturer must be able to demonstrate more than catalog output speed. Buyers should review compliance knowledge, engineering depth, documentation quality, FAT and SAT discipline, local support, spare-parts responsiveness, and the ability to integrate the machine into a complete sterile process.
In the United States, the most successful projects usually involve suppliers that can communicate clearly with QA, validation, engineering, production, and procurement at the same time. This is especially important when the project includes water systems, solution preparation, logistics automation, and packaging interfaces rather than a single stand-alone filler.
Evaluation CriterionWhat to AskWhy It MattersWarning SignRegulatory understandingCan the supplier support FDA-oriented documentation?Reduces validation delaysGeneric answers without examplesAseptic design capabilityHow is intervention minimized?Supports sterility assurancePoor access and hard-to-clean zonesReference projectsHas the supplier completed similar vaccine or sterile lines?Shows practical execution abilityNo relevant installed baseCustomizationCan the line fit your vial range and future products?Improves long-term valueOne-size-fits-all approachDocumentation packageAre IQ/OQ/PQ support documents available?Speeds qualificationIncomplete or unclear templatesAfter-sales supportWhat are response times and spare-parts plans?Protects uptimeNo structured service processProject integrationCan the supplier coordinate utilities and upstream/downstream systems?Reduces interface riskOnly sells isolated equipmentWhen evaluating partners, some U.S. buyers prefer firms with experience beyond stand-alone machines. For example, IVEN Pharmatech Engineering is often considered by companies that want an engineering-led approach rather than only equipment supply. Its technological capabilities are relevant where sterile filling must connect with pharmaceutical water systems, solution preparation, conveying, and packaging automation. This kind of breadth can reduce interface issues during facility expansion or greenfield planning.
On the manufacturing side, suppliers with multiple specialized plants and long experience in sterile processing equipment can offer more control over component quality and system compatibility. For projects requiring broader factory planning, buyers may also review turnkey pharmaceutical engineering capabilities to judge whether the supplier can support layout, utilities, validation, and process flow from the beginning.
Investment cost varies widely. A compact semi-automatic or low-throughput aseptic unit may require a relatively modest budget, while a fully integrated high-speed vaccine vial line with washing, depyrogenation, isolator, capping, inspection interfaces, and validation support can represent a major capital program. In the United States, buyers should budget for much more than the machine purchase price.
Total project cost usually includes equipment, engineering, shipping, customs, site preparation, cleanroom modifications, utilities, installation, FAT/SAT, qualification, training, consumables, spare parts, and ongoing service. If the project is in a high-cost labor region such as the Boston area, the Bay Area, or central New Jersey, installation and validation costs may increase significantly.
Cost ElementTypical Share of BudgetCost DriverSavings OpportunityCore filling equipment30% to 45%Speed, automation, sterility barrierRight-size capacityUpstream/downstream integration10% to 20%Tunnel, capping, conveyance, controlsIntegrated supplier coordinationCleanroom and utilities10% to 18%HVAC, compressed air, WFI interfacesReuse existing infrastructure where feasibleValidation and documentation6% to 12%IQ/OQ/PQ, protocols, test executionStrong documentation from supplierInstallation and commissioning8% to 15%Site conditions and labor ratesDetailed pre-install planningTraining and startup support3% to 6%Operator and maintenance readinessStructured training programsSpare parts and service reserve4% to 8%Critical wear items and uptime protectionPhased stocking strategyROI is often driven by four measurable gains: more saleable vials, less batch loss, lower labor dependency, and reduced deviation or maintenance downtime. A line that improves yield by even a small percentage can recover capital quickly when the vaccine product has high per-batch value.
Typical payback periods can range from under three years for heavily utilized commercial lines to five years or more for specialized or lower-volume facilities. The most realistic business case compares the new line against current scrap rates, labor demand, outsourced fill-finish costs, and the revenue opportunity of increased capacity.
var ctx4 = document.getElementById(‘comparisonChartSuppliers’).getContext(‘2d’);var chart4 = new Chart(ctx4, { type: ‘bar’, data: { labels: [‘Compliance Support’, ‘Customization’, ‘Lifecycle Service’, ‘Integration Scope’, ‘Cost Efficiency’, ‘Lead Time Discipline’], datasets: [{ label: ‘Importance score in U.S. buying decisions’, data: [95, 86, 91, 88, 79, 83], backgroundColor: ‘rgb(153, 102, 255)’ }] }, options: { responsive: true, maintainAspectRatio: false }});This comparison chart illustrates a common U.S. procurement reality: supplier value is judged heavily on support and integration, not only on base price. Buyers increasingly want a partner that can stay involved from specification through validation and stable commercial operation.
For teams comparing options, a structured review of available pharmaceutical equipment solutions can help map line configuration, output level, and integration requirements before issuing a final RFQ.
The largest risks are usually not mechanical failure alone. More often, projects underperform because of weak URS definitions, underestimated validation effort, poor utility planning, inadequate operator training, or mismatched supplier capability. Vaccine products are especially sensitive because formulation behavior can change with temperature, hold time, agitation, and product-contact material selection.
Another risk is buying too little flexibility. A line that perfectly suits one vial size and one campaign profile may become restrictive if the site later adds new doses, secondary packaging formats, or higher throughput goals. Conversely, excessive over-specification can inflate capital cost and complexity without creating real operating value.
Risk AreaTypical ProblemImpactMitigation StrategyURS definitionUnclear performance expectationsDesign mismatch and change ordersDefine product, vial, and compliance needs earlyValidation timelineLate documentation readinessDelayed startupLock documentation deliverables into contractUtility mismatchInsufficient clean steam, WFI, or HVAC supportPerformance instabilityComplete utility audit before purchaseOperator dependenceToo many manual interventionsHigher contamination riskFavor automation and ergonomic designSupply chain delayLong lead components or shipping disruptionProject schedule slippageUse milestone tracking and early procurementFormat inflexibilityLimited vial range or difficult changeoverReduced future adaptabilityEvaluate full product roadmapService gapWeak spare parts and field supportLonger downtimeChoose suppliers with lifecycle service structureService capability is where many projects succeed or fail after installation. For U.S. manufacturers, it helps to work with partners that can support feasibility, engineering review, equipment customization, installation, commissioning, qualification assistance, training, and post-startup optimization. If a project requires broad coordination, early communication with a qualified supplier through a technical consultation channel can reduce avoidable risk.
A useful case pattern in the market involves companies modernizing older injectable plants rather than building entirely new sites. In such situations, a supplier with engineering, manufacturing, and service capability under one framework can often manage the interfaces more smoothly. This is where IVEN is frequently evaluated: not merely as a machine source, but as a partner able to contribute technological capabilities in sterile processing, manufacturing capabilities across specialized pharmaceutical equipment production, and service capabilities that extend from planning to validation and operational support. That model can be valuable for U.S. projects seeking lower integration risk.
1. What output speed is suitable for a vaccine vial filling line?It depends on batch size, campaign frequency, and shift model. Clinical and pilot lines may run at a few thousand vials per hour, while commercial lines can exceed 20,000 vials per hour. The best choice balances throughput with sterility assurance and changeover efficiency.
2. Are isolators always required for vaccine filling in the United States?Not always, but isolators are increasingly preferred for high-containment and advanced aseptic strategies. Some projects still use RABS, especially where existing facilities are being upgraded. The decision should be based on contamination control strategy, product risk, and facility design.
3. Can one machine handle multiple vial sizes?Yes, many modern systems are designed for multiple formats. Buyers should ask about change parts, recipe storage, changeover time, and whether performance remains stable across all planned vial sizes.
4. What level of documentation should a supplier provide?A reliable supplier should support design documents, FAT protocols, manuals, parts lists, electrical documentation, software descriptions, and qualification-related materials such as IQ/OQ support packages. Data integrity readiness is also important.
5. How important is product-contact material selection?Very important. Vaccine formulations can be sensitive to extractables, adsorption, and shear. Product path design, tubing choice, pump technology, and cleaning strategy all affect product quality.
6. Should U.S. buyers choose a stand-alone machine or a turnkey line?If the project only replaces one module and interfaces are stable, a stand-alone machine may work. If the plant is expanding, changing utilities, or integrating several systems, a turnkey-oriented approach often reduces coordination risk and saves time overall.
7. What are the most common hidden costs?Validation, cleanroom modifications, utility upgrades, shipping delays, spare parts, software customization, and extended commissioning are common hidden costs. These should be included in early budget planning.
8. Is importing pharmaceutical filling equipment into the United States practical?Yes, if the supplier understands documentation, schedule control, logistics planning, and on-site support. Port selection, inland transport, and customs timing should be planned early, especially for large integrated lines.
9. How long does a typical project take?For a high-spec aseptic vial line, total timeline from specification to qualification may range from around 10 to 18 months, depending on customization, facility readiness, and validation scope.
10. What should be included in a supplier comparison?Compare regulatory understanding, machine design, installed references, customization depth, documentation quality, lifecycle service, training, digital features, spare-parts strategy, and total cost of ownership.
In summary, a vial filling machine for vaccines is a strategic investment for U.S. pharmaceutical manufacturers seeking safe, compliant, and scalable sterile production. The best outcomes come from matching machine design to product needs, site conditions, and long-term capacity strategy while selecting a supplier with proven engineering, manufacturing, and service capabilities.
-
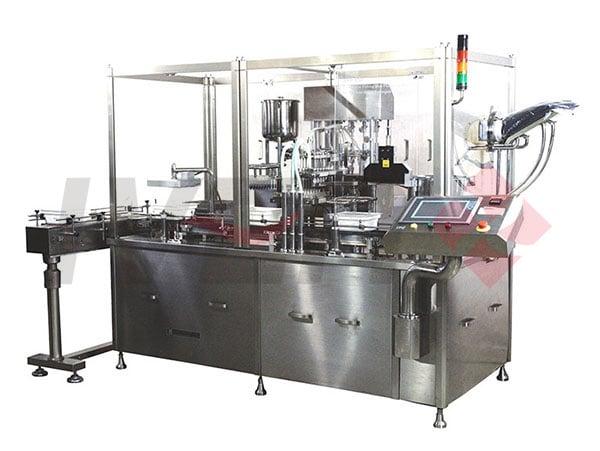
Prefilled Syringe vs Vial Filling in the United States
In the United States, the choice between prefilled syringe filling and vial filling is not just a packaging decision. It affects aseptic processing design, labor efficiency, regulatory strategy, patient safety, product loss, cold-chain handling, and long-term plant economics. Large pharmaceutical and medical device manufacturers evaluating new capacity in Boston, Raleigh-Durham, New Jersey, Chicago, Houston, and San Diego often compare these two formats during facility expansion or modernization because each one aligns differently with biologics, vaccines, hospital injectables, specialty drugs, and combination products.
For many drug developers, prefilled syringes offer strong advantages in dose accuracy, convenience, and reduced preparation steps at the point of care. Vials remain highly flexible, especially for multi-dose products, lyophilized formulations, early-stage commercial launches, and therapies requiring broader fill-volume options. In practice, the best choice depends on product viscosity, container-closure integrity, fill-finish speed targets, market positioning, and compliance with U.S. FDA cGMP expectations for sterile manufacturing.
Companies that want to reduce project risk usually assess the topic through engineering, quality, supply chain, and total lifecycle support. This is where an integrated partner can matter. IVEN Pharmatech Engineering is known in the industry for combining pharmaceutical engineering know-how with filling, packaging, water systems, logistics, and turnkey delivery experience for regulated factories worldwide. For U.S.-focused investment planning, that broader integration is often more valuable than buying a standalone machine without upstream and downstream coordination.
The short answer is simple: prefilled syringes generally improve user convenience, reduce dosing errors, and support premium injectable products, while vials provide greater manufacturing flexibility, broader product compatibility, and often lower initial packaging cost. U.S. manufacturers compare them because both formats remain essential under strict regulatory standards, but each drives a different operating model.
If the product is a ready-to-administer biologic for hospitals, specialty pharmacies, self-injection, or emergency care, prefilled syringe filling may create stronger commercial value. If the product requires lyophilization, multiple dose configurations, lower packaging complexity, or staged market introduction, vial filling may be the more practical path. For sterile injectable producers in the United States, the decision usually comes down to six core variables: formulation stability, annual volume, automation level, line changeover frequency, downstream device assembly requirements, and return on investment.
Decision FactorPrefilled SyringeVialU.S. Market ImpactPoint-of-care convenienceVery highModerateImportant for hospitals, clinics, and home useDose accuracyHigh, fixed presentationDepends on withdrawal stepRelevant for safety and training reductionPackaging flexibilityLowerHighUseful for diversified portfoliosSupport for lyophilizationLimited in standard formatsExcellentCritical for many biologics and vaccinesInitial line investmentUsually higherUsually lower to moderateKey for greenfield budgetingCommercial differentiationStrongModerateHigher value in specialty therapeuticsOperator interventionsPotentially lower on integrated linesCan be higher depending on processImpacts contamination control strategyThe table above shows why the debate is common in U.S. sterile projects. Prefilled syringes support premium delivery and workflow simplification, while vials preserve manufacturing range and process resilience.
The phrase “prefilled syringe vs vial” refers to a container and fill-finish strategy comparison within sterile pharmaceutical production. It is used during product development, process design, equipment procurement, facility planning, and technology transfer. The decision influences isolator design, washing and depyrogenation needs, stoppering systems, inspection systems, packaging architecture, cleanroom classification, and validation scope.
In a prefilled syringe process, the drug product is filled directly into a sterile syringe barrel, then closed with a plunger stopper and often integrated later with a needle safety device or final assembly platform. The result is a unit-dose presentation that minimizes handling before administration. In a vial process, the product is filled into glass or polymer vials, then stoppered and capped. Healthcare personnel or end users later withdraw the solution with a syringe, or the product may be reconstituted before use.
In pharmaceutical production, this comparison is used for:
U.S. manufacturers near major logistics corridors such as the Port of New York and New Jersey, the Port of Los Angeles, Houston, and Memphis air cargo hubs also factor in shipping resilience. Syringe components, elastomers, tubs, nests, vial glass, and caps all have different sourcing profiles and lead-time risks.
Both formats are deeply established in modern sterile manufacturing, but they serve different product and market needs. Prefilled syringes are increasingly favored for ready-to-use therapies, especially in therapeutic areas where reducing bedside preparation time matters. Vials still dominate in many hospital injectables, oncology products, generic injectables, and formulations requiring freeze-drying.
Application AreaBest-Fit FormatReasonOperational BenefitBiologic self-injectionPrefilled syringeConvenience and fixed doseSupports patient adherenceEmergency care drugsPrefilled syringeRapid administrationLower preparation timeLyophilized oncology productsVialBetter freeze-dry compatibilityImproved stabilityMulti-dose hospital productsVialAllows repeated accessInventory flexibilityHigh-value specialty injectablesPrefilled syringePremium presentationBrand differentiationEarly-stage commercial launchVialSimpler scale-up pathLower initial complexityAnticoagulants and vaccinesPrefilled syringe or vialDepends on dose and cold chainCustomized market strategyThe table above highlights application fit rather than absolute superiority. A format that is ideal for one injectable may be inefficient for another.
Benefits of prefilled syringes include:
Benefits of vials include:
From an engineering perspective, the selection also affects utility loads, line clearance procedures, machine footprint, reject handling, and visual inspection criteria. This is especially important for U.S. facilities trying to optimize expensive cleanroom space in major pharmaceutical regions such as Massachusetts and New Jersey.
var ctxBarDemand = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBarDemand, { type: ‘bar’, data: { labels: [‘Biologics’, ‘Vaccines’, ‘Hospital Injectables’, ‘Oncology’, ‘Emergency Drugs’, ‘Self-Administration’], datasets: [{ label: ‘Estimated U.S. Demand Intensity by Format Preference’, data: [88, 76, 68, 71, 79, 91], backgroundColor: [‘#4e79a7′,’#59a14f’,’#9c755f’,’#f28e2b’,’#e15759′,’#76b7b2′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});In the U.S. market, companies do not choose only between container formats. They also choose among machine architectures, automation levels, sterility barriers, component feeding methods, inspection technologies, and integration with packaging and warehouse systems.
Typical prefilled syringe line options include nested syringe processing, bulk syringe processing, servo-driven filling stations, in-process checkweighing, vacuum or peristaltic filling, plunger insertion modules, and automated tray or tub handling. Typical vial line options include rotary or linear washing machines, depyrogenation tunnels, aseptic fillers, stoppering units, capping systems, and optional lyophilizer loading solutions.
Technical OptionUsed for Prefilled SyringesUsed for VialsTypical U.S. Buying ConsiderationNested container formatCommonRareLower manual handling, useful for premium productsBulk container formatPossibleCommonMay lower packaging cost at scaleIsolator integrationVery commonVery commonSupports contamination control expectationsRABS configurationCommonCommonBalance between access and protectionLyophilizer interfaceLimitedCommonCritical for freeze-dried productsInline vision inspectionHigh importanceHigh importanceSupports cosmetic and particulate controlRobotic handlingIncreasingIncreasingReduces interventions and improves consistencyRecipe-driven changeoverHigh valueHigh valueImportant for multi-SKU plantsThe table shows that the technical decision is really a system decision. Companies expanding capacity often evaluate whether the new line should connect to purified water, WFI generation, solution preparation, inspection, carton packing, and intelligent logistics systems from a coordinated engineering source rather than separate vendors.
That is one area where IVEN’s technological capabilities stand out. The company is recognized for integrated sterile manufacturing platforms covering filling and packaging machinery, pharmaceutical water treatment systems, solution preparation, and intelligent conveying. For manufacturers seeking a broader project view instead of a single machine purchase, this integrated approach can simplify line harmonization and documentation alignment.
Comparing prefilled syringes with vials should also involve alternative formats such as cartridges, ampoules, blow-fill-seal containers, and auto-injector assemblies. Each serves different clinical and commercial objectives.
FormatBest Use CaseMain StrengthMain LimitationPrefilled syringeReady-to-administer and self-injection drugsUser convenience and dosing controlHigher packaging complexityVialHospital use, lyophilized products, flexible dosingVersatilityRequires preparation before useCartridgePen injectors and device-based deliveryDevice compatibilityNeeds dedicated delivery platformAmpouleSome legacy injectables and niche productsSimple sealed glass formatBreak risk and handling limitationsBFS containerHigh-volume sterile liquidsIntegrated forming and fillingNot ideal for all high-value biologicsAuto-injector assemblyPremium combination productsPatient-friendly administrationHigher total project costDual-chamber systemsReconstitution-required productsImproved end-user preparationComplex engineering and sourcingThe best solution depends on commercial route:
For U.S. buyers, it is also wise to evaluate the downstream ecosystem. Can the format move efficiently through labeling, aggregation, case packing, serialization, and warehouse automation? If not, a lower-cost container choice may create a higher total system cost.
The U.S. market remains one of the world’s most influential sterile fill-finish regions. Demand is supported by biologics growth, specialty drug launches, vaccine preparedness, domestic manufacturing policy discussions, hospital injectable resilience, and sustained investment in advanced aseptic processing. Prefilled syringes are seeing faster growth in many premium therapeutic segments, while vial filling continues to hold a large base due to its versatility and installed capacity.
Between 2024 and 2026, several forces are shaping the market:
var ctxLineGrowth = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var lineChartGrowth = new Chart(ctxLineGrowth, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Market Index for Prefilled Syringe Filling’, data: [100, 108, 118, 129, 141, 154], borderColor: ‘#2f6fed’, backgroundColor: ‘rgba(47,111,237,0.08)’, fill: false, tension: 0.25 },{ label: ‘Estimated U.S. Market Index for Vial Filling’, data: [100, 104, 109, 115, 121, 128], borderColor: ‘#f28e2b’, backgroundColor: ‘rgba(242,142,43,0.08)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});The line chart above illustrates realistic market direction rather than a fixed forecast. Prefilled syringe demand is rising faster, but vials remain fundamental to U.S. pharmaceutical infrastructure.
var ctxAreaShift = document.getElementById(‘areaChartShift’).getContext(‘2d’);var areaChartShift = new Chart(ctxAreaShift, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of New Premium Injectable Launches in Prefilled Formats’, data: [32, 36, 41, 47, 52, 58], borderColor: ‘#59a14f’, backgroundColor: ‘rgba(89,161,79,0.28)’, fill: true, tension: 0.25 },{ label: ‘Share of New Flexible or Lyophilized Launches in Vial Formats’, data: [68, 64, 59, 53, 48, 42], borderColor: ‘#9c755f’, backgroundColor: ‘rgba(156,117,95,0.18)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});By 2026, expected trends include more robotic handling, stronger use of ready-to-use sterile components, and closer integration between filling lines and digital manufacturing systems. Policy and sustainability trends will also matter. U.S. buyers increasingly ask about energy-efficient tunnel designs, reduced compressed air consumption, recipe-controlled cleaning, and lower reject rates. They also examine whether an equipment supplier can support qualification under U.S. FDA cGMP, EU GMP, WHO GMP, and PIC/S expectations to preserve export flexibility.
Choosing a supplier is often more important than choosing the format itself. A technically strong line can still fail as an investment if the supplier cannot support FAT, SAT, validation, spare parts, recipe optimization, operator training, and after-sales responsiveness in the United States.
Supplier Evaluation PointWhy It MattersWhat U.S. Buyers Should VerifyRisk if IgnoredRegulatory understandingSupports inspection readinessExperience with FDA-oriented documentation and cGMP designDelays in validation and approvalIntegrated engineering scopeReduces interface gapsAbility to connect utilities, filling, packaging, and logisticsCostly project fragmentationReference projectsProves practical delivery capabilityInstalled lines or turnkey projects in regulated marketsExecution uncertaintyCustomization abilityFits product-specific needsContainer range, format change parts, automation optionsOperational mismatchValidation supportSpeeds startupIQ, OQ, PQ documentation and test supportLonger commissioning periodAfter-sales serviceProtects uptimeTraining, remote support, spare parts planningExtended downtimeManufacturing strengthReflects reliability and consistencyOwn plants, quality controls, supply chain stabilityInconsistent delivery qualityThe table above can be used as a practical qualification checklist during vendor comparison. It helps procurement, engineering, and QA teams score suppliers on execution strength rather than brochure claims.
On manufacturing capability, IVEN brings a multi-plant production base focused on pharmaceutical filling and packaging machinery, water systems, intelligent logistics, and blood collection tube equipment. That breadth matters when projects require line integration instead of isolated equipment islands. On service capability, the company supports feasibility review, engineering design, equipment customization, installation, commissioning, validation, training, and lifecycle optimization. For U.S. buyers managing tight schedules and capital exposure, those services can reduce interface risk across the project timeline.
When evaluating alternatives, it is useful to review a supplier’s broader project portfolio through its turnkey pharmaceutical engineering solutions and compare whether the vendor can support a full facility roadmap rather than only a single filling module.
In the United States, capital budgeting for sterile fill-finish projects should include much more than the core machine price. The total cost model should cover cleanroom adaptation, barrier systems, HVAC implications, component preparation, utilities, validation, training, line integration, spare parts, and ramp-up losses.
Cost ElementPrefilled Syringe LineVial LineBudget NoteCore filling equipmentHighModerate to highDepends on speed and automationContainer/component handlingHighModerateNested or RTU formats can add costLyophilization interfaceUsually low or nonePotentially highMajor factor for vial projectsInspection and assemblyHighModerateSyringes may need more downstream stepsChange parts and format kitsModerateModeratePortfolio breadth drives costValidation and startupHighHighCritical regardless of formatLabor per finished doseOften lower long termCan be higherDepends on automation and outputOverfill and yield lossOften lowerCan be higherImportant for expensive biologicsThe table demonstrates why a higher initial cost for prefilled syringes may still generate better lifetime returns, especially for high-value formulations. On the other hand, vial lines can produce strong ROI when product flexibility, lyophilization, and lower entry cost are the main priorities.
A simple ROI framework should consider:
var ctxComparisonROI = document.getElementById(‘comparisonChartROI’).getContext(‘2d’);var comparisonChartROI = new Chart(ctxComparisonROI, { type: ‘bar’, data: { labels: [‘Initial CAPEX’, ‘Format Flexibility’, ‘Labor Efficiency’, ‘Yield Advantage’, ‘Point-of-Care Value’, ‘Lyophilization Fit’], datasets: [{ label: ‘Prefilled Syringe Score’, data: [62, 58, 84, 81, 92, 35], backgroundColor: ‘#7b61ff’ },{ label: ‘Vial Score’, data: [78, 91, 63, 60, 55, 95], backgroundColor: ‘#ff9da7’ }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});For a premium biologic with high drug substance cost, lower overfill and easier administration may justify a prefilled syringe investment relatively quickly. For a diversified injectable portfolio in a contract manufacturing environment, a vial line may produce better asset utilization because of broader product compatibility.
If your organization is comparing budgets across equipment categories, reviewing available sterile processing and packaging options in a structured equipment portfolio can help narrow specifications before tendering. A good starting point is the supplier’s pharmaceutical equipment range for line architecture and supporting systems.
The main investment risks are rarely limited to the machine itself. In the U.S. market, sterile projects can fail due to underestimated validation effort, weak supplier coordination, component shortages, improper line sizing, or poor compatibility between formulation and primary packaging.
Risk AreaHow It Affects SyringesHow It Affects VialsMitigation StrategyContainer compatibilityPlunger movement, siliconization, extractablesGlass interaction, stopper compatibilityEarly material studies and stability testingSupply chain disruptionRTU tubs, syringe components, safety devicesGlass vials, stoppers, capsDual sourcing and inventory planningValidation burdenDevice-related complexityLyophilization and stopper behaviorStructured IQ/OQ/PQ and media fill plansIncorrect line sizingUnderused premium assetBottlenecks in washing or cappingDemand modeling and OEE analysisChangeover inefficiencyComplex format partsMulti-size component variationRecipe-driven automation and SMED planningOperator intervention riskComponent handling sensitivityManual transfers around lyophilizationRobotics and barrier designLong-term service gapsDowntime on specialized assembliesDowntime across utility-linked systemsPreventive maintenance and supplier support contractsAmong U.S. operators, another major consideration is project location. A plant near Philadelphia, Newark, Baltimore, Savannah, or Long Beach may have better import and logistics flexibility for certain components and replacement parts. Likewise, a site in Indianapolis or Memphis may benefit from stronger inland distribution and air cargo access. These factors matter when lead times tighten.
Case studies in the industry repeatedly show that the best outcomes come from front-loaded engineering: selecting the right format early, verifying market demand, confirming packaging compatibility, and aligning utilities, cleanroom flow, serialization, warehouse design, and training before procurement. This is especially important for companies trying to avoid schedule drift or cost overruns on U.S. greenfield projects.
As a practical example, a specialty injectable producer launching a high-margin anticoagulant in the United States may choose prefilled syringes to gain nursing efficiency and commercial differentiation. A generic sterile manufacturer supplying hospital tenders may select vials because they support more SKU flexibility and lower launch complexity. Neither choice is universally better; the right answer depends on business model and product science.
For companies that want a deeper technical discussion, qualification planning, or a plant-level investment review, the most efficient next step is to contact a pharmaceutical engineering specialist with your expected product profile, annual volumes, and regulatory target.
1. Are prefilled syringes always better than vials?No. Prefilled syringes are often better for convenience, fixed dosing, and premium injectable positioning, but vials are usually better for flexible dosing, lyophilization, and some lower-cost or broader portfolio strategies.
2. Which format is more common in the United States?Both are common. Vials still hold a major position in hospital injectables and lyophilized drugs, while prefilled syringes are expanding rapidly in biologics, specialty therapies, and ready-to-administer applications.
3. Is prefilled syringe filling more expensive?Usually yes at the initial investment stage. However, the lifetime economics can be favorable when drug value is high, overfill reduction matters, and point-of-care convenience creates commercial advantages.
4. Can vial lines support more product types?In many cases, yes. Vial lines are generally more flexible for fill volumes, freeze-drying, and a broader range of sterile injectable products.
5. What regulatory issues matter most for U.S. buyers?FDA cGMP compliance, aseptic process control, container-closure integrity, validation documentation, media fills, data integrity, and robust change control are all critical.
6. What technical option is becoming more important by 2026?Robotic handling, isolator-based filling, digital batch data integration, and reduced-intervention line design are becoming increasingly important in both syringe and vial projects.
7. How do I compare suppliers effectively?Review regulatory experience, installed references, engineering integration capability, validation support, after-sales responsiveness, and the ability to customize around your product and facility constraints.
8. Can one supplier provide both line equipment and broader plant systems?Yes. Some engineering-focused suppliers provide not only filling lines but also water systems, solution preparation, packaging, logistics, validation support, and turnkey coordination, which can reduce project interface risk.
9. When should a company choose a turnkey approach?A turnkey approach is often valuable for greenfield factories, major expansions, or projects where schedule control, utility integration, and documentation consistency are as important as the filling machine itself.
10. What is the biggest mistake in this investment decision?The biggest mistake is choosing based only on machine price. The better approach is to evaluate total lifecycle cost, formulation fit, commercial strategy, regulatory burden, and long-term operational flexibility.
For U.S. pharmaceutical manufacturers, the decision between prefilled syringe and vial filling should be made at the intersection of science, engineering, market demand, and lifecycle economics. A premium biologic portfolio may justify syringe-focused investment, while a flexible sterile injectable operation may achieve better asset performance with vial technology. The strongest projects are built on integrated planning, clear validation strategy, and a supplier with proven technical, manufacturing, and service capabilities.
-
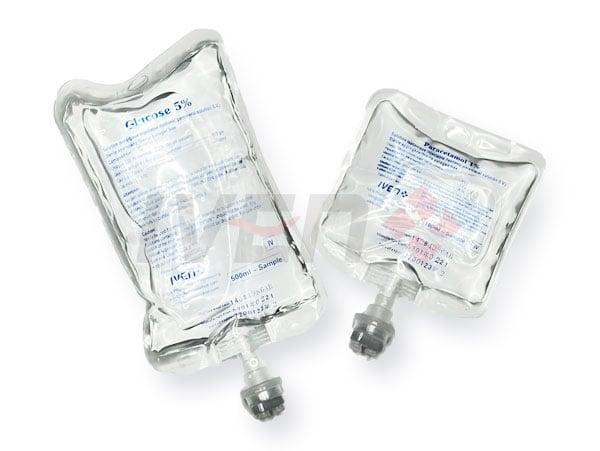
United States Guide to Non-PVC IV Bag Production Lines
For pharmaceutical manufacturers in the United States, a non-PVC IV bag production line is more than a packaging investment. It is a strategic manufacturing platform for producing safer, more stable, and more differentiated infusion products. By using multilayer non-PVC films and precise forming, filling, sealing, and sterilization systems, these lines help manufacturers create advanced IV solutions that may keep incompatible ingredients separated until use, reduce leachables concerns associated with traditional PVC, and support broader hospital demand for modern infusion packaging. In practical terms, this means better product stability, expanded formulation flexibility, and stronger positioning in a U.S. market shaped by FDA compliance, hospital purchasing standards, sustainability pressure, and ongoing drug shortage preparedness.
Across the United States, from New Jersey and Boston to Houston, Indianapolis, and the Research Triangle in North Carolina, interest in non-PVC IV bag production line capacity is rising. Buyers are evaluating not only machine speed, but also cleanroom integration, film compatibility, chamber design, validation support, and lifecycle service. For companies planning new sterile manufacturing projects or upgrading existing IV solution facilities near major logistics gateways such as the Port of Los Angeles, Port of Long Beach, Port of Savannah, and Port Newark, the right production line can improve both technical performance and supply chain resilience.
A non-PVC IV bag production line is a complete pharmaceutical manufacturing system used to produce soft infusion bags made from non-PVC medical films. Depending on the product design, the line may include film feeding, bag forming, port welding, filling, chamber separation, sealing, leak detection, visual inspection, overwrapping, sterilization compatibility, and final packing. Multi-chamber versions are especially valuable because they can keep active ingredients separate until mixing at the point of use. This supports better shelf stability for formulations that would otherwise degrade, precipitate, or react when stored together.
In the U.S. healthcare environment, this matters for several reasons. Hospitals are under pressure to reduce medication preparation steps, lower contamination risk, and standardize ready-to-use infusion products. Meanwhile, manufacturers need packaging formats that align with FDA expectations for quality systems, extractables and leachables assessment, container closure integrity, and robust process validation. A modern non-PVC IV bag production line helps address all of these concerns while also enabling premium formulations such as dual-chamber nutrition bags, unstable antibiotic combinations, and specialty critical care solutions.
Core BenefitWhy It MattersImpact on U.S. ManufacturersImproved chemical compatibilityNon-PVC films can reduce interaction with sensitive formulationsSupports broader product portfolios and regulatory confidenceMulti-chamber capabilityKeeps ingredients separate until activationEnables higher-value ready-to-mix productsBetter patient safety profileReduces handling steps in pharmacies and wardsHelps hospitals lower medication error riskModern hospital acceptanceMany buyers prefer lightweight, flexible, transport-efficient packsImproves commercial competitiveness in tendersHigh automationLess manual intervention in sterile productionImproves consistency and lowers contamination riskScalable productionCan be configured for regional or national supply needsUseful for U.S. network expansion and contract manufacturingThe table above shows why this technology is increasingly discussed in U.S. infusion manufacturing projects. The main value is not just replacing one bag material with another. It is enabling higher quality, better usability, and more advanced dosage forms.
A non-PVC IV bag production line typically combines several modules into one validated production workflow. At the front end, film is unwound, aligned, and thermoformed or heat formed into the required bag geometry. Ports are inserted and welded. Bags are then filled under controlled aseptic or clean conditions, sealed, checked for integrity, and transferred for downstream packaging. Depending on the manufacturer’s process design, the line may also integrate solution preparation, CIP/SIP interfaces, automatic loading, robotics, and serialization-ready secondary packing.
Compared with older infusion packaging methods, the main advantages are flexibility, process control, and product differentiation. Single-chamber bags remain important for standard saline, dextrose, and electrolyte solutions. However, multi-chamber systems add a strong commercial and clinical advantage by allowing unstable ingredients to remain isolated. This feature is especially relevant for parenteral nutrition, specialty anti-infective products, and formulations intended for emergency or critical care settings.
For U.S. buyers, there are also plant design considerations. A line selected for a facility in New Jersey or California may need different utility planning, labor assumptions, and automation priorities than a lower-cost greenfield site in the Midwest or Puerto Rico. Integration with FDA-compliant documentation, electronic batch recording, and validation packages can be just as important as output speed.
Production Line FunctionTypical Equipment RoleBusiness AdvantageFilm formingCreates precise bag shape and chamber layoutSupports consistent dimensions and packaging strengthPort insertion and weldingAttaches administration and additive portsImproves usability and leak resistanceLiquid fillingMeters sterile solution accuratelyReduces overfill loss and batch variationHeat sealingCloses bag perimeter and internal chambersEnsures container closure integrityInspection systemsDetect leaks, particles, and seal defectsSupports product release qualityAutomation and data loggingTracks process parameters and alarmsFacilitates validation and audit readinessIf your project requires a broader facility perspective, it is often useful to review a supplier’s experience in turnkey pharmaceutical engineering solutions rather than evaluating a stand-alone machine in isolation. In sterile manufacturing, utility systems, layout, material flow, and validation all influence the final return on investment.
From the hospital point of view, non-PVC IV bag formats support workflow simplification and help reduce bedside preparation. In large health systems across Chicago, Dallas, Philadelphia, and Atlanta, pharmacy teams increasingly value ready-to-use or ready-to-activate formats because labor shortages and medication safety initiatives continue to shape purchasing preferences. Multi-chamber bags can be activated close to administration time, reducing the need for compounding steps in some use cases.
Clinical benefits vary by product category. For example, nutrition formulations may require separation of amino acids, lipids, or electrolytes until just before infusion. Certain antibiotics or adjunctive agents benefit from delayed mixing to preserve potency. Emergency departments and military or disaster response stockpiles may also favor compact, easy-to-deploy infusion packs with reduced preparation time.
Application AreaHow Non-PVC Bags HelpCommon U.S. End UsersParenteral nutritionSupports multi-chamber storage of sensitive componentsAcute care hospitals and nutrition providersAntibiotic infusionImproves stability by separating diluent and drugHospital pharmacies and outpatient infusion centersEmergency careSpeeds activation and reduces prep burdenER departments and trauma centersOncology support solutionsEnables standardized supportive care infusion formatsCancer centers and specialty hospitalsRenal and metabolic careAllows specialized formulation packagingDialysis networks and tertiary hospitalsRoutine hydration and electrolytesProvides lightweight and efficient transport packagingCommunity hospitals and long-term care facilitiesThe value of this technology in U.S. clinical settings comes down to one principle: products that arrive closer to administration-ready status usually create better consistency and lower operational friction. Manufacturers capable of supplying such products gain a stronger position in hospital contracting.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chartBar = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Parenteral Nutrition’, ‘Antibiotic Infusion’, ‘Critical Care’, ‘General Hydration’, ‘Dialysis Support’, ‘Outpatient Infusion’], datasets: [{ label: ‘Estimated U.S. demand index for non-PVC IV bag products’, data: [92, 84, 79, 88, 61, 73], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The bar chart highlights where demand is strongest. General hydration remains large because of volume, while nutrition and antibiotic applications stand out because they carry higher complexity and value per unit.
Not every non-PVC IV bag production line is configured the same way. The most common categories include single-chamber standard infusion lines, dual-chamber mixing lines, three-chamber nutrition bag lines, and specialized formats for dialysis or custom hospital products. Selection depends on the intended formulation, sterilization method, fill volume range, target speed, and film structure.
Film selection is critical. In U.S. projects, buyers usually evaluate transparency, flexibility, weldability, sterilization tolerance, extractables profile, oxygen and moisture barrier performance, and compatibility with the planned drug formulation. Non-PVC films may include polypropylene-based blends, multilayer polyolefin structures, EVA-based systems, or custom coextruded materials engineered for infusion use.
Film Material OptionTypical StrengthPossible LimitationBest-Fit ApplicationMultilayer polyolefin filmGood chemical compatibility and flexibilityMay require precise sealing parameter controlGeneral infusion and premium sterile solutionsPP-based filmStrong heat resistance and clarityCan be stiffer than softer blendsHigh-temperature process compatibilityEVA-based filmSoft feel and good low-temperature flexibilityApplication suitability depends on formulationSelected specialty infusion productsCoextruded multi-layer filmBalanced barrier and mechanical propertiesHigher material qualification effortAdvanced multi-chamber bagsHigh-barrier custom filmImproved protection for sensitive ingredientsHigher material costStability-critical formulationsEco-optimized non-PVC structureSupports sustainability positioningMust still meet full performance validationFuture-oriented hospital and export programsThe table above shows that film choice should be led by formulation science and regulatory strategy, not only packaging cost. In many U.S. procurement reviews, the hidden cost of a poor material match appears later as seal issues, stability failures, or prolonged validation work.
When reviewing available equipment configurations, buyers often look at a supplier’s wider sterile processing portfolio. A company with experience in integrated systems listed through its pharmaceutical equipment portfolio can usually provide more practical guidance on material handling, utilities, and downstream packaging compatibility.
Single-chamber bags remain efficient and essential for commodity IV solutions. They are simpler, easier to validate, and usually lower in capital cost. Multi-chamber bags, however, are designed for products where timing of mixing changes product value. In the U.S. market, this difference is commercially important because hospitals increasingly prefer products that reduce compounding workload and preserve stability.
A decision between the two formats should include product portfolio planning. If a manufacturer intends to serve only standard saline or dextrose at very high volume, a single-chamber line may be enough. If the strategy includes nutrition, specialty anti-infectives, or differentiated ready-to-activate hospital products, a multi-chamber non-PVC IV bag production line becomes more attractive.
Comparison FactorSingle-Chamber BagsMulti-Chamber BagsProduct complexityLow to moderateModerate to highCapital investmentLowerHigherStability advantageLimited for incompatible ingredientsHigh for separated formulationsCommercial differentiationMore commodity-orientedHigher value and stronger product positioningChangeover complexityUsually easierRequires more process precisionHospital workflow benefitUseful for routine infusionStrong for ready-to-mix and ready-to-use workflowsRegulatory documentation burdenLower relative complexityGreater because of chamber function and activation designFor U.S. investors, the best choice is often not either-or. A phased capacity plan may begin with high-volume single-chamber products and expand into dual- or triple-chamber systems once market access is secured. This is particularly relevant in regions with strong hospital buying groups and compounding service demand, such as the Northeast corridor and large metropolitan health systems in Texas and California.
var ctxComp = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var chartComp = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Flexibility’, ‘Stability Support’, ‘CapEx Efficiency’, ‘Hospital Value’, ‘Validation Complexity’, ‘Portfolio Differentiation’], datasets: [ { label: ‘Single-Chamber Line’, data: [72, 58, 88, 67, 82, 54], backgroundColor: ‘#4e79a7’ }, { label: ‘Multi-Chamber Line’, data: [89, 94, 63, 91, 61, 96], backgroundColor: ‘#f28e2b’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});This comparison chart summarizes the trade-off clearly. Single-chamber lines win on simplicity and initial cost. Multi-chamber lines win on stability support and premium product strategy.
The U.S. infusion market is influenced by several simultaneous trends: hospital preference for ready-to-administer products, regulatory focus on supply continuity, expansion of specialty infusion, and the need to modernize aging domestic sterile manufacturing infrastructure. Drug shortage concerns have also strengthened interest in resilient local or regional production capacity. Buyers near major distribution centers such as Memphis, Louisville, and Columbus are increasingly designing facilities for fast national shipment rather than only local coverage.
Demand for non-PVC IV bag production line capacity is not limited to large multinational firms. Contract development and manufacturing organizations, regional sterile injectables companies, and health-system-affiliated production ventures are also evaluating non-PVC soft bag lines. The appeal is strongest where product differentiation and reliability matter more than commodity price alone.
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var chartLine = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [{ label: ‘Estimated U.S. demand index for non-PVC IV bag production lines’, data: [46, 51, 58, 66, 74, 82, 89, 97], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The line chart reflects a realistic growth scenario rather than an extreme projection. Demand is being pulled by a mix of replacement investment, hospital preference shifts, and portfolio upgrades.
var ctxArea = document.getElementById(‘areaChartShift’).getContext(‘2d’);var chartArea = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [{ label: ‘Share of new infusion packaging projects favoring non-PVC systems’, data: [39, 43, 48, 54, 61, 68, 73, 79], fill: true, backgroundColor: ‘rgba(153, 102, 255, 0.25)’, borderColor: ‘rgb(153, 102, 255)’, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The area chart shows the strategic shift underway. Even where current output is still dominated by traditional products, new capital projects are increasingly built around non-PVC concepts. Looking toward 2026 and beyond, three trends stand out. First, automation will deepen, including robotics, recipe management, machine vision, and predictive maintenance. Second, U.S. policy attention on domestic drug security will continue to favor dependable local supply. Third, sustainability will become more visible in purchasing decisions, including material efficiency, transport optimization, and packaging lifecycle analysis.
Choosing a supplier for the U.S. market requires more than comparing brochures. A serious buyer should assess regulatory understanding, sterile engineering depth, equipment durability, film and formulation experience, reference installations, documentation quality, and after-sales responsiveness. If a line is expected to support FDA-regulated commercial production, the supplier must be able to support design qualification, FAT/SAT planning, IQ/OQ/PQ structure, and change control discipline.
Technological capability matters. A supplier should demonstrate expertise in precision filling, stable thermal sealing, leak-proof chamber design, process monitoring, and compatibility with validation-oriented control systems. Manufacturing capability matters as well. It is important to confirm whether the supplier operates specialized plants, uses long-life stainless steel construction, and can scale output for large projects. Service capability matters just as much, especially for U.S. customers managing time zones, installation schedules, and audit pressure.
Shanghai IVEN Pharmatech Engineering Co Ltd, known in the market as IVEN Pharmatech Engineering, is often evaluated by buyers that want a combination of engineering depth and integrated project support. Its technical profile is built around pharmaceutical and medical device machinery development, with extensive know-how in IV solution systems, water treatment, intelligent logistics, and validation-oriented plant planning. On the manufacturing side, the company operates multiple specialized plants in Shanghai focused on different product categories, which helps maintain quality consistency across sterile production equipment. On the service side, it offers lifecycle support that can include engineering design, customization, commissioning, qualification support, training, and optimization. U.S. buyers interested in its background can review the company overview on the official company page.
Supplier Selection CriterionWhy It Is ImportantWhat to VerifyRegulatory knowledgeEssential for FDA-facing projectsExperience with cGMP documentation and validation packagesFilm and bag engineeringDrives product quality and yieldPast performance with non-PVC materials and chamber designsAutomation levelAffects labor, data integrity, and consistencyPLC architecture, alarms, recipe control, and traceabilityFactory manufacturing depthImpacts delivery and spare parts reliabilityDedicated plants, machining standards, QA processReference projectsReduces purchasing riskInstalled lines, product types, and country relevanceAfter-sales serviceCritical for startup and lifecycle uptimeRemote support, on-site support, training, and spare parts lead timeTurnkey capabilityUseful for greenfield sterile projectsUtility integration, layout design, and qualification supportThe table above shows a practical due-diligence checklist. In many cases, the best supplier is not the one with the lowest quoted price, but the one that can reliably bring a regulated sterile line into routine production without prolonged delays.
Capital planning for a non-PVC IV bag production line in the United States should include more than the machine price. Buyers must budget for cleanroom adaptation, utilities, WFI or purified water interfaces, solution preparation, sterilization compatibility, HVAC balancing, qualification, spare parts, operator training, and sometimes warehousing automation. Projects near high-cost labor markets such as Boston, San Diego, or the New York metro area may place a premium on automation and reduced manual intervention. Projects in lower-cost regions may choose a different balance.
ROI depends on product mix. Commodity infusion products generally require scale and operational efficiency to generate strong returns. Advanced multi-chamber products can deliver higher margins but require more sophisticated commercialization and regulatory planning. Capacity utilization is also crucial. A well-designed line that runs only sporadically rarely achieves an attractive payback.
Budget ItemTypical ImportanceROI ImpactMain production line equipmentVery highDetermines core throughput and product capabilityFilm qualification and trialsHighPrevents costly startup instabilityClean utilities integrationHighSupports compliance and uptimeValidation and documentationVery highDirectly affects launch timingTraining and SOP developmentMedium to highReduces operator errors and scrapSpare parts and maintenance strategyMediumImproves long-term availabilitySecondary packaging and logisticsMediumAffects distribution efficiency and labor costA realistic ROI model for U.S. investors should use at least three scenarios: a base case with moderate utilization, an upside case tied to premium hospital contracts, and a downside case that assumes slower validation or lower launch volume. Lead times for imported equipment, port handling at Long Beach or Savannah, inland transport, and commissioning schedules should all be built into the cash flow model. For project-specific budgeting or technical discussion, buyers can start through the contact channel for engineering consultation.
The biggest risk is underestimating complexity. A non-PVC IV bag production line is a pharmaceutical production system, not just a packaging machine. Problems can arise from film mismatch, seal weakness, chamber break-force inconsistency, filling accuracy drift, sterilization incompatibility, or weak validation planning. U.S. investors should also think about customs timing, site readiness, utility qualification, operator competency, cybersecurity for control systems, and spare parts stocking.
Another common risk is choosing equipment that matches today’s product but not tomorrow’s strategy. If your business plan includes only basic saline in year one but anticipates dual-chamber antibiotics in year three, the line architecture should be reviewed now. Retrofitting later can be expensive and disruptive.
Risk AreaTypical ProblemMitigation ApproachMaterial compatibilityFilm interacts poorly with formulation or processRun early compatibility and stability studiesSeal integrityLeaks or weak chamber separationOptimize sealing parameters and perform integrity validationProject timelineSite not ready when equipment arrivesUse integrated schedule management and FAT planningRegulatory readinessIncomplete qualification package delays launchDefine documentation scope before procurementOperational skill gapOperators struggle with advanced line controlsInvest in training, SOPs, and supervised startupSupply chain disruptionFilm or spare parts shortagesDual-source critical items and hold safety stockFuture product limitsLine cannot support planned premium formatsChoose scalable design with expansion optionsThe explanation behind this table is straightforward: most failures are avoidable when engineering, quality, procurement, and commercial teams plan together. In the U.S. market, where launch delays and supply gaps can be expensive, that cross-functional discipline is a major advantage.
A useful case pattern can be seen in greenfield or expansion projects that combine line procurement with full sterile plant planning. Suppliers with broad engineering capability can reduce the disconnect between machine delivery and plant readiness. IVEN Pharmatech Engineering is often considered in this category because it combines equipment design with integrated factory support, including utilities, layout planning, installation coordination, and qualification assistance rather than stopping at shipment alone.
What products can be made on a non-PVC IV bag production line?Common outputs include saline, dextrose, electrolyte solutions, specialty infusion products, parenteral nutrition bags, selected antibiotic systems, and some ready-to-mix hospital formulations depending on line design and regulatory approval strategy.
Is a multi-chamber line always better than a single-chamber line?No. Multi-chamber systems are better when formulation stability and point-of-use activation create real clinical or commercial value. For high-volume standard fluids, a single-chamber line may be more economical.
Why is non-PVC packaging attractive in the United States?U.S. buyers often value chemical compatibility, modern hospital usability, lower prep burden, and strategic alignment with updated infusion product expectations. Non-PVC also supports premium product development.
What should FDA-focused manufacturers prioritize when choosing a line?Prioritize documentation quality, process control, validation support, material compatibility, audit-ready data handling, and a supplier that understands sterile manufacturing and cGMP expectations.
How long does implementation usually take?Timing depends on project scope, customization, facility readiness, FAT/SAT scheduling, shipping, installation, validation, and staffing. A greenfield sterile project usually requires much more time than a line replacement in an existing qualified facility.
Where should U.S. companies locate new capacity?There is no single answer. Sites near established pharma hubs such as New Jersey, North Carolina, Massachusetts, Indiana, and Puerto Rico may offer talent and supply chain benefits. Sites near logistics corridors such as Houston, Savannah, Memphis, or Southern California may improve distribution efficiency.
What makes a supplier credible for this type of project?Credibility comes from installed references, engineering depth, specialized manufacturing capability, durable equipment design, strong service support, and the ability to help with validation and project execution, not just equipment shipment.
Can a supplier support both equipment and full plant development?Yes. Some suppliers provide both stand-alone machinery and broader factory solutions. For example, companies active in sterile engineering may support feasibility, design, equipment customization, commissioning, qualification, and training in one program.
In summary, the right non-PVC IV bag production line for the United States market should match your product strategy, regulatory pathway, hospital customer expectations, and long-term capacity plan. The strongest projects combine sound film selection, validation-ready engineering, scalable automation, and a supplier capable of supporting the full manufacturing lifecycle.