PD Solution Contamination Control in the United States
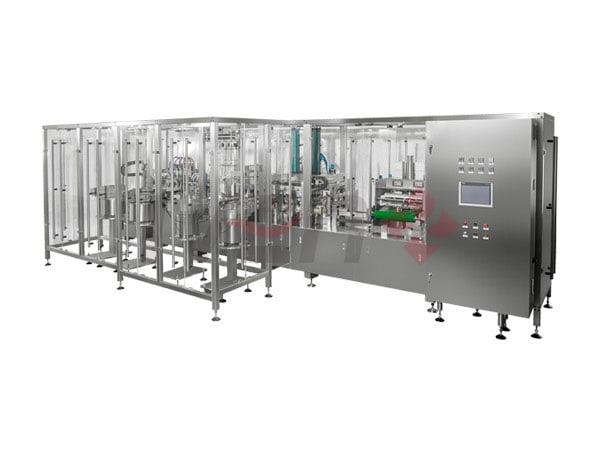
In the United States, PD solution production contamination prevention has become a strategic priority for manufacturers building or upgrading pharmaceutical facilities under FDA cGMP expectations. For peritoneal dialysis solution lines, contamination control is not one single machine. It is a coordinated production concept that combines water treatment, solution preparation, closed transfer, hygienic filling, environmental control, sterilization, inspection, packaging, validation, and digital monitoring. Large pharmaceutical and medical device companies evaluate these systems when launching new capacity in hubs such as New Jersey, Boston, Indianapolis, Houston, and San Diego, where regulatory pressure, product safety expectations, and supply chain resilience all matter.
For buyers in the United States market, the most effective approach is to evaluate contamination prevention not only by initial equipment price, but also by sterility assurance, batch consistency, cleaning validation, operator intervention reduction, utility efficiency, documentation quality, and lifecycle service support. Companies planning a new line often compare integrated systems from specialized engineering partners with piecemeal procurement from multiple vendors. A structured decision can reduce commissioning delays, deviation rates, and long-term operating costs.
Quick Answer: What PD Solution Production Contamination Prevention Means for U.S. Manufacturers

PD solution production contamination prevention refers to the full set of engineering controls, equipment design features, production procedures, and validation practices used to keep peritoneal dialysis solution free from microbial, particulate, chemical, and cross-product contamination during manufacturing. In U.S. pharmaceutical production, this includes purified water and WFI systems, sanitary solution mixing and holding tanks, aseptic or terminally sterilized filling lines, cleanroom zoning, CIP/SIP capability, container closure integrity, leak detection, automated transfer, and in-process monitoring.
The direct answer for procurement teams is simple: if a PD solution line cannot demonstrate reliable contamination prevention, it will struggle with FDA inspection readiness, product release consistency, and long-term operational economics. That is why contamination prevention is reviewed early in plant expansion plans, particularly for facilities near major logistics corridors such as the Port of Houston, Port Newark, Los Angeles/Long Beach, and Savannah, where imported equipment, stainless steel components, and packaging materials move through tightly scheduled projects.
In practical terms, contamination prevention protects patients, supports batch release, reduces recall exposure, and helps manufacturers maintain stable output. For dialysis-related products, this is especially important because end users are medically vulnerable and the product is often used frequently and in large volumes.
| Contamination Risk | Typical Source | Operational Impact | Preferred Control | Validation Focus | Why It Matters in the United States |
|---|---|---|---|---|---|
| Microbial contamination | Water, tanks, hoses, open handling | Batch rejection, sterility failure | Closed system design, SIP, environmental control | Bioburden trend and sterility assurance | Strong FDA emphasis on process hygiene and risk control |
| Particulate contamination | Container defects, component shedding | Visual inspection failures | Particle control, filtration, automated inspection | Particle counts and visual reject rates | Critical for patient safety and complaint reduction |
| Chemical residue | Cleaning agents, lubricants, cross-product carryover | Out-of-spec chemistry | Validated CIP, material compatibility | Cleaning validation and residue limits | Important for multi-product sites in contract manufacturing |
| Endotoxin risk | Water system biofilm, poor sanitation | Release delay or rejection | Hot water loops, hygienic dead-leg control | Endotoxin testing and loop mapping | High scrutiny for water-intensive sterile manufacturing |
| Cross-contamination | Shared vessels, transfer lines, operator error | Batch mix-up, regulatory finding | Dedicated circuits or validated changeover | Line clearance and traceability | Essential for facilities serving multiple formulations |
| Seal integrity failure | Poor filling, weak closure, damaged containers | Leaks and loss of sterility | Container closure integrity testing | Leak test and seal parameter qualification | Critical for distribution across long U.S. transport routes |
The table above shows why contamination prevention must be viewed as a system rather than a single point solution. U.S. buyers usually gain the best results when risk mapping is completed before equipment selection.
What Is PD Solution Production Contamination Prevention and What Is It Used For in Pharmaceutical Production?

In pharmaceutical manufacturing, PD solution production contamination prevention is used to ensure that every stage of the process preserves product quality from raw materials to final packed units. For peritoneal dialysis solutions, the process often includes water preparation, ingredient dissolution, pH and conductivity control, filtration, temporary storage, container filling, sealing, sterilization, cooling, leak testing, visual inspection, labeling, and secondary packaging.
Each stage introduces different contamination risks. Water systems can introduce endotoxins or microbes. Open mixing steps can invite airborne particles. Manual transfer raises operator-related risks. Filling and sealing defects can create post-process contamination. Contamination prevention technology reduces these vulnerabilities by using closed piping, sanitary pumps, orbital welding, automated recipe control, laminar airflow, isolated filling zones, and robust thermal sterilization profiles.
In the United States, this is commonly applied in:
- Large-volume parenteral and dialysis solution manufacturing plants
- Hospital supply and renal therapy product production
- New greenfield pharmaceutical facilities
- Brownfield modernization projects with legacy filling lines
- Contract development and manufacturing organizations handling sterile liquids
- Medical consumables plants that require integrated fluid preparation systems
When companies assess suppliers, they often seek partners that understand both process equipment and regulatory delivery. An international engineering company such as IVEN Pharmatech Engineering is relevant to this discussion because it combines pharmaceutical process knowledge with experience in integrated lines, water systems, packaging, and compliance-oriented project execution for global clients, including the U.S. market.
Main Applications and Benefits of PD Solution Production Contamination Prevention in Modern Pharmaceutical Manufacturing

The primary application is safe, repeatable production of peritoneal dialysis solution at commercial scale. However, the benefits extend far beyond contamination avoidance alone. U.S. manufacturers increasingly use contamination prevention investments to improve audit readiness, operator productivity, and total equipment effectiveness.
Main applications include sterile or low-bioburden solution preparation, hygienic transfer between unit operations, controlled filling of soft bags, bottles, or specialty containers, terminal sterilization compatibility, and integrated inspection before release. Modern lines also connect contamination control with MES or SCADA platforms so that alarms, recipes, trends, electronic batch records, and maintenance events can be traced in real time.
Key benefits for pharmaceutical plants in cities such as Raleigh-Durham, Philadelphia, St. Louis, and Minneapolis include:
- Lower contamination-related batch loss
- Higher process consistency across multiple shifts
- Reduced manual intervention and fewer human error events
- Stronger FDA inspection preparedness
- Better support for validation and deviation investigation
- Higher confidence in shelf-life and transport stability
- Improved utility efficiency through optimized CIP/SIP and heat recovery
| Application Area | Typical Equipment | Contamination Challenge | Benefit Achieved | KPI Often Used | U.S. Buyer Relevance |
|---|---|---|---|---|---|
| Water preparation | RO, purified water, WFI loop | Biofilm and endotoxin | Stable water quality | Conductivity, TOC, endotoxin | Supports cGMP utilities qualification |
| Solution compounding | Mixing tanks, transfer skids | Open exposure, carryover | Closed hygienic processing | Bioburden trend, batch consistency | Useful in multi-batch daily operations |
| Filling and sealing | Automated filling line | Particle and seal failure | Reduced intervention, stronger integrity | Reject rate, seal strength | Critical for large-volume product release |
| Sterilization | Autoclave or inline thermal system | Under-processing or over-processing | Reliable sterility assurance | F0 value, temperature mapping | Key in FDA validation packages |
| Inspection | Leak tester, vision system | Undetected defects | Higher outgoing quality | Detection sensitivity, false reject rate | Supports complaint reduction |
| Packaging and logistics | Cartoning, palletizing, warehouse system | Handling damage and mix-ups | Traceability and product protection | Serialization accuracy, damage rate | Important for nationwide distribution |
The table highlights that benefits are cumulative. If one stage is weak, the line can still underperform even when the filling machine itself is advanced.
The line chart above illustrates a realistic growth trajectory for U.S. demand as dialysis therapy volume, domestic manufacturing, and compliance upgrades continue to rise through 2030.
Key Types, Models and Technical Options for PD Solution Production Contamination Prevention
There is no universal line configuration. The right model depends on production scale, container format, sterility strategy, utility infrastructure, and available cleanroom space. U.S. buyers commonly evaluate the following technical options.
Closed compounding systems reduce operator contact and are favored when contamination control and batch reproducibility are both priorities. Automated CIP/SIP systems help plants standardize cleaning and sterilization between campaigns. Non-PVC soft bag lines may be attractive for flexible packaging, while PP bottle or glass bottle lines can fit different product and market requirements. Inline filtration and degassing support solution quality. Vision inspection and leak detection protect outgoing product integrity.
Technological capabilities matter here. IVEN Pharmatech Engineering is known in the market for integrated capabilities that cover IV solution lines, dialysis solution lines, water treatment, solution preparation and distribution, conveying, and end-of-line packaging. For U.S. buyers, this matters because contamination prevention is stronger when upstream and downstream interfaces are engineered together rather than assembled from disconnected modules.
| Type or Model | Best Fit | Main Technical Features | Contamination Control Strength | Possible Limitation | Typical U.S. Use Case |
|---|---|---|---|---|---|
| Manual-assisted semi-automatic line | Smaller capacity or pilot scale | Basic tanks, partial automation | Moderate | Higher operator dependence | R&D or specialty low-volume product |
| Fully automatic closed line | Commercial volume production | Automated transfer, CIP/SIP, recipe control | High | Higher capital cost | Large pharma expansion in New Jersey or Texas |
| Soft bag PD solution line | Flexible packaging strategy | Form-fill-seal or bag handling system | High | Film qualification required | Home-care focused supply programs |
| PP bottle line | Robust container preference | Bottle molding or integrated filling | High | Footprint and utility load | High-output sterile liquid plants |
| Glass bottle line | Specific compatibility or legacy format | Washing, depyrogenation, filling, sealing | High | Breakage management | Facilities upgrading older injectable lines |
| Modular skid-based system | Fast installation projects | Preassembled skids, digital controls | High if well integrated | Customization limits in some layouts | Accelerated projects near contract manufacturing hubs |
This comparison shows why model selection should be tied to lifecycle needs. A premium line may save money over time if it reduces manual cleaning, downtime, and deviation investigations.
PD Solution Production Contamination Prevention vs Alternative Technologies: Which Solution Fits Your Needs?
Many U.S. manufacturers compare a dedicated integrated PD solution line with alternative approaches such as adapting a general sterile liquid line, outsourcing filling to a CDMO, or using multiple stand-alone units from separate suppliers. The best option depends on batch size, internal expertise, launch speed, and long-term cost priorities.
An integrated dedicated line usually offers the best contamination prevention because interfaces are designed together. A retrofitted general liquid line may reduce upfront investment but often creates compromises in flow, cleaning, or documentation. Outsourcing can reduce immediate capital exposure, yet it may weaken supply control and make tech transfer more complex.
| Option | Upfront Cost | Compliance Readiness | Contamination Risk Profile | Scalability | Best For |
|---|---|---|---|---|---|
| Dedicated integrated PD line | High | Strong when supplied with documentation | Lowest among options | High | Long-term strategic manufacturing |
| Retrofitted sterile liquid line | Medium | Variable | Moderate to high | Medium | Brownfield site upgrades |
| Stand-alone multi-vendor units | Medium | Complex integration burden | Moderate | Medium | Experienced owner-led engineering teams |
| CDMO outsourcing | Low capex | Depends on partner | Process control outsourced | Medium | Short-term launch or uncertain demand |
| Manual-heavy local build | Low | Often weaker | Higher | Low | Not ideal for large U.S. sterile supply |
| Modular turnkey solution | Medium to high | Strong if validation package is complete | Low | High | Fast-track greenfield or expansion projects |
The table makes one point clear: the cheapest path rarely delivers the lowest total risk. Buyers should score alternatives against FDA documentation strength, utility compatibility, and changeover performance before deciding.
This bar chart shows where demand for contamination prevention investments is strongest. Dialysis and IV solution plants remain the leading segments due to volume, sterility expectations, and continuous supply obligations.
Market Overview and Future Trends for PD Solution Production Contamination Prevention in Pharmaceutical Manufacturing
The United States market is being driven by four forces: domestic pharmaceutical manufacturing expansion, pressure for more resilient healthcare supply chains, stricter quality oversight, and growing interest in automation that reduces intervention risk. The market includes greenfield projects, site modernization, utility upgrades, packaging line synchronization, and digital quality systems.
Buyers in coastal states often factor in import timing and commissioning logistics through the ports of Long Beach, Los Angeles, Newark, Charleston, and Houston. Midwest facilities may prioritize service response, spare parts warehousing, and factory acceptance planning to avoid long project delays. East Coast clusters around New Jersey and Massachusetts continue to see high demand for sophisticated compliance documentation and validation support.
Looking toward 2026 and beyond, the main trends are clear:
- More closed processing and reduced open handling
- Broader use of SCADA, historian data, and electronic batch records
- Greater emphasis on Annex 1 aligned contamination control strategies, even for companies selling globally from U.S. sites
- Energy-efficient sterilization and water systems
- Remote diagnostics and predictive maintenance
- Sustainable design with lower water, steam, and chemical consumption
- Supplier preference for integrated turnkey delivery instead of fragmented procurement
The area chart reflects the expected shift from conventional mixed-manual production toward more closed, automated, and data-rich contamination control strategies.
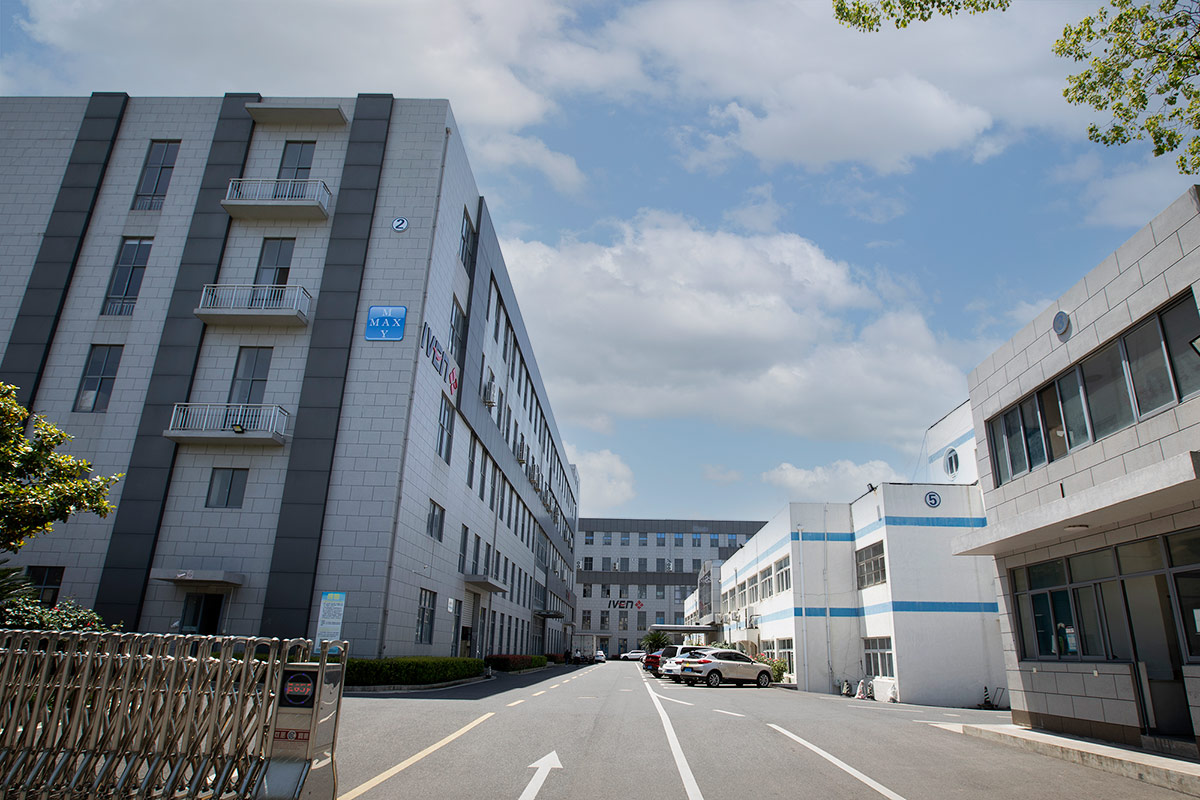
Manufacturing capabilities are becoming more important in supplier evaluation as well. Buyers increasingly favor companies with dedicated production plants for core equipment categories rather than trading-only organizations. IVEN Pharmatech Engineering, for example, operates specialized manufacturing facilities covering filling and packaging machinery, pharmaceutical water treatment, intelligent conveying and logistics, and blood collection tube equipment. For a U.S. buyer, this kind of manufacturing depth can improve consistency in fabrication, schedule coordination, and spare parts support for large integrated projects.
How to Choose a Reliable PD Solution Production Contamination Prevention Manufacturer or Supplier
Choosing the right supplier requires more than comparing quotations. In the United States, serious buyers evaluate technical fit, documentation quality, project management discipline, regulatory understanding, and post-installation support. A strong supplier should be able to discuss contamination control strategy at the system level, not only individual machine specifications.
Key questions include:
- Does the supplier understand PD solution process requirements, not just generic liquid filling?
- Can it provide IQ, OQ, and PQ support documentation?
- Does it design to recognized GMP expectations and U.S. project standards?
- Can it align water systems, solution preparation, filling, sterilization, inspection, and packaging in one project plan?
- Does it have reference installations, FAT procedures, and service response capability?
- Can it support scale-up, training, and troubleshooting after startup?
| Evaluation Criterion | Why It Matters | What Good Looks Like | Warning Sign | How to Verify | Relative Priority |
|---|---|---|---|---|---|
| Regulatory knowledge | Drives inspection readiness | Clear GMP-based design rationale | Generic claims without evidence | Review URS response and sample documents | Very high |
| Process integration ability | Prevents interface failures | One supplier manages critical interfaces | Owner must coordinate everything | P&ID and layout review | Very high |
| Fabrication quality | Affects hygiene and durability | High-grade stainless steel and weld quality | Inconsistent finish or weak documentation | Factory audit or FAT | High |
| Validation package | Speeds startup and release | IQ/OQ templates, FAT/SAT protocols | Minimal documentation only | Document sample review | High |
| Service responsiveness | Reduces downtime | Training, remote support, spare parts | Slow escalation path | Ask for SLA and references | High |
| Project delivery record | Reduces schedule risk | Documented installations and milestones | Few comparable projects | Reference checks | Medium to high |
The table should be used as a practical scoring sheet during supplier interviews. Many U.S. teams assign weighted values to each criterion and compare finalists side by side.
The comparison chart illustrates a common result in supplier evaluations: integrated specialists may not always be the lowest initial bidder, but they often score better on contamination control, documentation, and project coordination.
Service capabilities should also be weighed heavily. A supplier that can provide feasibility input, engineering design, equipment customization, installation, commissioning, validation support, quality documentation, staff training, and after-sales support reduces project fragmentation. Buyers seeking a more integrated route can review turnkey pharmaceutical project capabilities when considering how much scope to keep under a single accountable partner.
Investment Cost, Budget Planning and ROI Analysis for PD Solution Production Contamination Prevention
Investment cost varies widely by line speed, automation level, container type, cleanroom classification, sterilization method, utility scope, and validation depth. In the U.S. market, budget planning should include direct equipment cost and all associated project costs such as installation, piping, automation integration, FAT/SAT, qualification, operator training, and spare parts.
A typical budgeting mistake is to focus only on the line itself while underestimating utility and compliance expenses. Water systems, clean steam, HVAC balancing, electrical integration, data systems, and warehouse flow can significantly affect the final budget. Projects near major labor-cost centers such as Boston, San Francisco, and New York metro areas may also see higher installation and validation spending than projects in lower-cost regions.
| Cost Element | What It Includes | Typical Budget Impact | Risk If Underestimated | ROI Effect | Planning Tip |
|---|---|---|---|---|---|
| Core process equipment | Tanks, transfer, filling, sterilization | Highest | Scope gaps and redesign | Drives throughput and quality | Define URS clearly before quote comparison |
| Water and utility systems | PW/WFI, steam, compressed air | High | Commissioning delay | Strong impact on compliance and uptime | Model utility loads early |
| Cleanroom and HVAC interfaces | Zoning, air changes, pressure cascade | Medium to high | Environmental control weakness | Supports contamination reduction | Coordinate with layout design from day one |
| Automation and data systems | SCADA, historian, recipes, alarms | Medium | Weak traceability | Improves labor efficiency | Specify integration standards early |
| Validation and documentation | DQ, FAT, SAT, IQ/OQ support | Medium | Slow release readiness | Shortens startup curve | Request sample document sets before award |
| Training and lifecycle service | Operator training, spare parts, remote support | Low to medium | Higher downtime later | Protects long-term ROI | Include year-one support in contract |
ROI typically comes from lower batch rejection, reduced labor, faster line clearance, lower utility waste, fewer quality investigations, and improved uptime. For many U.S. plants, the payback horizon is influenced less by unit margin alone and more by the cost of supply interruption. If a contamination event stops a high-volume dialysis solution line, the financial impact can be substantial because of missed shipments, rework, testing costs, and market risk.
Buyers comparing suppliers can explore broader equipment categories through the pharmaceutical equipment portfolio to understand how contamination prevention ties into filling, water, logistics, and packaging systems rather than treating procurement as a single-machine purchase.
Key Considerations and Potential Risks When Investing in PD Solution Production Contamination Prevention
The biggest risk is assuming that any sterile liquid line can be adapted easily for PD solution without process-specific design work. In reality, contamination prevention depends on flow path geometry, material selection, sterilization logic, human-machine interfaces, cleaning coverage, and line layout. A line that looks adequate on paper may underperform during qualification if hold times, drainability, or seal consistency were not properly engineered.
Common investment risks include:
- Choosing a supplier with weak validation documentation
- Underestimating project management and owner-side coordination needs
- Ignoring utility bottlenecks that compromise hygiene performance
- Selecting over-complex automation that site staff cannot maintain
- Failing to secure spare parts and service plans in the United States
- Inadequate FAT leading to surprises during SAT and commissioning
- Layout constraints that increase manual intervention during operation
Service planning is where many projects succeed or fail. An effective partner should not disappear after shipment. U.S. manufacturers usually benefit from suppliers that can support installation, commissioning, qualification, training, troubleshooting, and performance optimization over time. IVEN Pharmatech Engineering positions itself as a lifecycle-oriented partner, which aligns well with buyers that need engineering plus operational continuity rather than equipment only.
Another point often overlooked is geographic logistics. If your site is in Memphis, Cleveland, or Salt Lake City, transit planning, customs timing, and field service mobilization can influence schedule risk as much as equipment fabrication itself. For imported systems, buyers should align port selection, inland transport, insurance, and installation sequencing well before SAT.
FAQ
1. Is PD solution production contamination prevention a single machine?
No. It is a system-level approach covering water treatment, solution preparation, transfer, filling, sterilization, inspection, packaging, environmental control, and validation.
2. What does PD usually refer to in this context?
In most pharmaceutical manufacturing discussions, PD solution refers to peritoneal dialysis solution, a high-safety fluid product that requires strong contamination control.
3. What is the most important contamination risk in PD solution lines?
There is no single risk, but microbial contamination, endotoxin control, particulate contamination, and seal integrity are typically the most critical.
4. Do U.S. manufacturers prefer integrated or multi-vendor systems?
Many prefer integrated solutions for critical sterile and dialysis-related production because it simplifies interface management, documentation, and accountability.
5. How important is water system quality?
Extremely important. Poor water quality can undermine the entire contamination prevention strategy, especially in high-volume sterile liquid and dialysis applications.
6. What documentation should a supplier provide?
At minimum, buyers often expect design documents, FAT/SAT protocols, material certificates, as-built records, manuals, and IQ/OQ support packages, with PQ assistance where agreed.
7. How do I compare suppliers fairly?
Use a weighted matrix covering regulatory fit, hygienic design, automation, validation support, project delivery, service responsiveness, and total cost of ownership.
8. What future trends should buyers watch in 2026?
Expect more closed systems, digital batch traceability, predictive maintenance, sustainability-focused utility design, and stronger contamination control strategies aligned with global GMP expectations.
9. Can one company supply the full line and supporting systems?
Yes, some engineering-driven manufacturers can provide integrated lines, water systems, conveying, packaging, and turnkey project support, which can reduce coordination risk.
10. Where can U.S. buyers start a discussion about project scope?
A practical first step is to contact an experienced engineering supplier with turnkey and validation capabilities through the project consultation contact page and share your intended capacity, container type, utility status, and compliance goals.
For pharmaceutical companies in the United States, the best contamination prevention strategy for PD solution production is the one that matches product risk, capacity targets, internal engineering resources, and regulatory expectations. A thoughtful investment can strengthen patient safety, improve operational reliability, and protect long-term manufacturing competitiveness.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Micro Blood Tube vs Capillary Tube in the United States
For manufacturers in the United States, the comparison between a micro blood tube and a capillary tube matters most in blood collection, diagnostics, and medical consumables production rather than in bulk drug processing. A micro blood tube is typically a small plastic collection tube designed to receive and store low-volume blood samples, while a capillary tube is a narrow glass or plastic tube mainly used to draw, transfer, or measure tiny blood volumes. In regulated production environments, companies evaluate both based on automation compatibility, specimen integrity, material selection, labeling, downstream testing workflow, and compliance with FDA, cGMP, ISO 13485, and CLSI-related expectations.
In the U.S. market, demand comes from diagnostic device makers, hospital supply chains, pediatric testing providers, point-of-care brands, central laboratories, and contract manufacturers serving healthcare systems in cities such as Boston, San Diego, Raleigh-Durham, Houston, and Minneapolis. Buyers also consider supply resilience through ports and logistics hubs such as Los Angeles, Long Beach, Savannah, New York/New Jersey, and Chicago. For companies planning line expansion, equipment decisions should focus on output stability, validation readiness, changeover efficiency, and total lifecycle cost rather than unit price alone.
The choice between micro blood tubes and capillary tubes is important because the two products support different clinical and manufacturing workflows. Micro blood tubes are usually better suited to labeled specimen collection, closed handling, additive integration, transport, centrifugation compatibility, and automated filling or packaging lines. Capillary tubes are preferred when the requirement is direct micro-volume collection, hematocrit testing, short-path sample transfer, or simple low-cost manual use.
For large pharmaceutical and medical device companies in the United States, this decision is rarely isolated. It affects line design, consumable sourcing, validation protocols, warehouse automation, kit assembly, sterility strategy, transportation stability, and customer usability. A pediatric diagnostics brand in Philadelphia may prioritize low draw volume and barcode traceability. A contract manufacturer in Indiana may focus on high-speed assembly, dimensional consistency, and reduced scrap. A laboratory supplier in California may care more about capillary precision, anticoagulant coating, and packaging density.
In practice, the better choice depends on the intended finished product. If the goal is a ready-to-use collection device for heel stick or finger stick blood collection, micro blood tubes often deliver stronger commercial value. If the goal is blood transfer or hematocrit measurement with minimal complexity, capillary tubes may be more appropriate.
Decision FactorMicro Blood TubeCapillary TubeTypical U.S. Buyer PriorityPrimary functionCollect, store, transport small blood samplesDraw or transfer very small blood volumesWorkflow fitMaterialMainly plastic, sometimes specialty polymersGlass or plasticBreakage risk and safetyAdditivesOften supports anticoagulants or clot activatorsMay be plain or coated depending on useTest compatibilityAutomation suitabilityHigh for filling, capping, labeling, packingLower to moderate depending on formatProduction efficiencyTransport readinessGood for organized sample logisticsLimited unless integrated into a kitDistribution securityTypical end marketDiagnostics, pediatrics, point-of-care, lab supplyHematocrit, transfer, specialty lab useCommercial scaleThe table above shows why many U.S. manufacturers treat micro blood tubes as a scalable finished consumable product, while capillary tubes are often treated as a simpler component or specialty accessory.
Strictly speaking, neither micro blood tubes nor capillary tubes are core process equipment for synthesizing active pharmaceutical ingredients or compressing tablets. However, they are highly relevant in pharmaceutical-adjacent production, especially where drug makers, biologics firms, and medical device companies support clinical testing, companion diagnostics, sample retention, or integrated healthcare kits. In modern regulated factories, they are part of the wider medical consumables and diagnostic device ecosystem.
A micro blood tube usually consists of a compact collection body, cap or closure system, labeling area, optional additive, and packaging configuration suitable for distribution. It is used in low-volume blood collection scenarios, especially for neonatal, pediatric, geriatric, and home-sampling applications. In some production systems, the tube is manufactured, assembled, dosed with additive, dried or conditioned, inspected, labeled, packed, and serialized.
A capillary tube is narrower and generally simpler. It relies on capillary action to draw blood or other fluids. Uses include hematocrit testing, specimen transfer, and niche diagnostic procedures. In manufacturing terms, capillary tube production often emphasizes tubing dimensional control, cutting precision, cleanliness, coating consistency, and safe packaging.
For pharmaceutical operations, their uses often include:
Companies expanding into these areas often require integrated line engineering, utility planning, cleanroom support, and validation services. Firms looking for broader project execution often review partners with turnkey capabilities; one example is turnkey pharmaceutical and medical device engineering solutions that combine process planning, equipment supply, installation, and commissioning.
ProductCore StructureMain UseCommon Additive OptionBest Production ContextMicro blood tubePlastic tube with capMicro-sample collection and storageEDTA, heparin, clot activatorHigh-volume medical consumablesCapillary tube, plainNarrow tubeSample transferNoneBasic lab supplyCapillary tube, heparinizedCoated narrow tubeBlood gas or specialty samplingHeparinSpecialized diagnostic packagingMicro hematocrit tubeCalibrated capillary formatHematocrit testingPlain or heparinizedLab-focused productionSafety micro collection tubeEnhanced closure designTransport and handling safetyMultiple optionsHospital and retail distributionKit-integrated micro tubeTube plus lancet/labelsHome or point-of-care collectionCase specificContract pack and kittingThe explanation here is practical: when a U.S. buyer asks about “production,” the real question is whether the intended line is for consumable manufacturing, diagnostic assembly, or integrated healthcare kit production. That distinction determines whether micro blood tubes or capillary tubes make more sense.
In the United States, applications are expanding because healthcare systems want lower blood draw volumes, more decentralized testing, and safer specimen handling. This is particularly relevant in pediatric hospitals, oncology monitoring, chronic disease management, and decentralized clinical trials.
Micro blood tubes provide several production and market benefits:
Capillary tubes remain important because they offer:
Modern applications extend across multiple sectors:
var ctxBarDemand = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBarDemand, {type: ‘bar’,data: {labels: [‘Pediatric Testing’, ‘Central Labs’, ‘Point-of-Care’, ‘Clinical Trials’, ‘Home Sampling’, ‘Hospital Supply’],datasets: [{label: ‘Estimated U.S. Demand Index’,data: [88, 76, 82, 68, 74, 91],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The chart highlights where demand is strongest. Hospital supply and pediatric testing are especially important for micro blood tubes, while central labs and specialty procedures continue to sustain capillary tube demand.
ApplicationPreferred FormatReasonOperational BenefitNeonatal screeningMicro blood tubeLow-volume retention and labelingSafer sample handlingHematocrit testingCapillary tubePrecise micro-volume drawEstablished lab workflowHome sample kitsMicro blood tubeTransport and closure securityLower leakage riskBlood gas collection supportCapillary tubeSpecialized coating optionsAnalytical suitabilityHospital distribution packsMicro blood tubePackaging and traceabilityProcurement efficiencyManual transfer tasksCapillary tubeSimplicity and low costReduced component complexityThe table demonstrates that the “better” choice is application specific. Micro blood tubes usually win when the process requires a finished commercial device. Capillary tubes remain strong in narrow, technical, or manual workflows.
U.S. buyers should separate product format from production-line configuration. The device type determines user value, but the line design determines yield, compliance, and profitability.
Common micro blood tube options include screw-cap and push-cap designs, multiple additive variants, color-coded closures, child-resistant or transport-secure formats, and kit-ready versions. Capacity ranges vary, but low-volume collection formats are usually optimized for fingerstick or heelstick workflows.
Capillary tube options include plain glass, heparinized glass, plastic capillary tubes, calibrated micro hematocrit tubes, and specialty formats with color coding or break protection. Technical decisions include internal diameter control, coating uniformity, static control, breakage resistance, and clean packaging.
On the machinery side, manufacturers may need:
Suppliers with stronger technological capabilities can tailor line architecture for output targets, cleanroom class, and validation requirements. Companies evaluating broader engineering support can review medical and pharmaceutical equipment portfolios to compare line categories and integrated systems.
Technical OptionMicro Blood Tube RelevanceCapillary Tube RelevanceBuyer ImpactAutomatic additive dosingHighModerateConsistency of test performanceVision inspectionHighHighReduced defects and rejectsClosure assemblyEssentialUsually not requiredTransport securityDimensional sortingHighEssentialPrecision and fitBreakage controlModerateEssential for glassSafety and scrap rateSerializationOften requiredLess commonTraceability and distributionThe main takeaway is that technical complexity tends to be higher for commercial micro blood tube products, while precision and material control are the central concerns for capillary tube production.
Many U.S. buyers compare micro blood tubes and capillary tubes not only against each other but also against alternative devices such as dried blood spot cards, microfluidic cartridges, small vacuum collection tubes, and integrated point-of-care sampling systems.
Each option has a different value proposition:
Selection depends on sample stability, required analytes, customer workflow, breakage tolerance, automation level, and reimbursement pathway. A retail health brand in the United States may prefer micro blood tubes or card-based systems. A lab instrument company may prefer capillary or cartridge formats. A medical device manufacturer supplying hospital networks may prioritize products that fit standard procurement and transport channels.
var ctxComparison = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComparison, {type: ‘bar’,data: {labels: [‘Automation Fit’, ‘Transport Safety’, ‘Labeling Space’, ‘Low Cost’, ‘Precision Transfer’, ‘Retail Readiness’],datasets: [{label: ‘Micro Blood Tube’,data: [90, 88, 92, 65, 70, 85],backgroundColor: ‘#4e79a7’},{label: ‘Capillary Tube’,data: [55, 50, 35, 88, 93, 48],backgroundColor: ‘#f28e2b’},{label: ‘Alternative Formats’,data: [72, 80, 60, 75, 78, 82],backgroundColor: ‘#59a14f’}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});This comparison shows why micro blood tubes often outperform in packaging, traceability, and market readiness, while capillary tubes still excel in precise transfer and low-cost simplicity.
TechnologyBest ForMain AdvantageMain LimitationMicro blood tubeCommercial collection productsTraceability and transportHigher production complexityCapillary tubeTransfer and specialty testingPrecision and simplicityLess suited to large retail formatsDried blood spot cardRemote samplingEasy shippingAnalyte limitationsMicrofluidic cartridgeAdvanced diagnosticsIntegrated testing workflowHigher development costMini vacuum tubeClinical collection settingsFamiliar user workflowMay require more infrastructureSampling kit systemDirect-to-patient useConvenienceAssembly and support complexityThe explanation is straightforward: choose the simplest technology that still satisfies regulatory, clinical, and commercial requirements in your target market.
The United States remains one of the most attractive markets for blood collection and diagnostic consumables because of high healthcare spending, strong clinical research activity, advanced hospital networks, and rising interest in decentralized testing. Demand is also influenced by aging demographics, chronic disease monitoring, and pressure to minimize blood volume draw in vulnerable populations.
Between now and 2026, several trends are shaping purchasing decisions:
Policy and compliance also matter. U.S. buyers increasingly expect suppliers to understand cGMP documentation, design qualification, IQ/OQ/PQ support, validation protocols, and change control. Sustainability is no longer a side issue; hospitals and procurement groups now ask about packaging reduction, material efficiency, logistics emissions, and machine energy consumption.
var ctxLineGrowth = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLineGrowth, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘U.S. Market Growth Index’,data: [100, 108, 117, 127, 138, 151],borderColor: ‘#76b7b2’,backgroundColor: ‘rgba(118,183,178,0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: false } }}});var ctxAreaTrend = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxAreaTrend, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Traditional Capillary Share’,data: [42, 40, 38, 35, 33, 31],borderColor: ‘#f28e2b’,backgroundColor: ‘rgba(242,142,43,0.20)’,fill: true,tension: 0.25},{label: ‘Micro Blood Tube and Advanced Formats’,data: [58, 60, 62, 65, 67, 69],borderColor: ‘#4e79a7’,backgroundColor: ‘rgba(78,121,167,0.20)’,fill: true,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The line chart suggests continued expansion of the U.S. market, while the area chart reflects a likely shift toward micro blood tube and more integrated sampling formats through 2026. Capillary tubes will remain relevant, but growth is expected to be stronger in products that fit automation, home sampling, and traceability requirements.
Choosing a reliable supplier in the United States market requires more than checking catalog specifications. Buyers should evaluate technical depth, manufacturing consistency, regulatory understanding, after-sales support, and the ability to scale with future demand.
Start with technological capabilities. Ask whether the supplier can support custom line design, additive handling, precision forming, automated inspection, digital traceability, and validation documentation. This is where experienced engineering companies stand out. Some international suppliers, including IVEN Pharmatech Engineering, are known for combining pharmaceutical and medical device engineering knowledge with specialized blood collection tube production equipment. That kind of cross-sector experience can be useful when a project spans consumables, utilities, packaging, and GMP-compliant factory planning.
Next, review manufacturing capabilities. A reliable partner should demonstrate stable fabrication quality, clean assembly standards, robust stainless-steel construction where applicable, repeatable output, and the ability to support both standard and customized lines. Suppliers with multiple specialized manufacturing bases and extensive project references often reduce execution risk for U.S. buyers needing high throughput or phased expansion.
Finally, assess service capabilities. Strong suppliers provide feasibility consulting, engineering design, installation, commissioning, staff training, spare parts planning, validation support, and lifecycle optimization. In the United States, response speed matters, especially when a line is tied to launch deadlines or contracted hospital demand.
Supplier Evaluation ItemWhat to CheckWhy It Matters in the U.S.Risk if WeakRegulatory familiarityFDA, cGMP, ISO 13485 supportSpeeds approval and auditsDocumentation gapsEngineering depthCustom design and integration abilitySupports expansion and upgradesPoor line fitManufacturing qualityMaterials, machining, consistencyImpacts uptime and rejectsHigh scrap rateValidation supportIQ, OQ, PQ readinessCritical for launch planningDelayed qualificationAfter-sales serviceTraining, spare parts, remote supportLimits downtimeLong service interruptionsProject referencesU.S. or global installationsConfirms practical capabilityExecution uncertaintyThe table shows that supplier quality is multidimensional. A lower upfront quote can become more expensive if the supplier cannot support validation, change parts, maintenance, or future line modifications. If you need project discussion or system matching, a direct consultation with an engineering team is often the fastest route to screening feasibility.
Investment ranges vary widely based on product complexity, output target, cleanroom classification, inspection level, and packaging scope. In the U.S. market, total project cost should include not only machine purchase price but also utilities, tooling, qualification, plant layout adaptation, operator training, validation, warehouse flow, and maintenance inventory.
Micro blood tube lines typically require a higher initial budget because they involve more assembly steps, closure systems, additive handling, labeling, and final packaging. Capillary tube production can be less expensive for simple formats, but cost rises quickly when precision cutting, coating, inspection, sterile or clean packaging, and specialty handling are added.
Budget categories often include:
Cost ElementMicro Blood Tube LineCapillary Tube LineROI RelevanceBase machineryMedium to highLow to mediumDefines entry thresholdTooling and change partsMediumMediumAffects product flexibilityInspection systemsHigh importanceHigh importanceReduces defects and recallsPackaging automationHighModerateLabor savingsValidation supportHighHighLaunch timing protectionMaintenance and sparesMediumMediumUptime and lifecycle costROI should be measured through more than direct labor reduction. Key drivers include:
A useful budgeting approach is to model three scenarios: pilot scale, mid-scale commercial, and high-volume strategic expansion. U.S. buyers with distribution through East Coast and West Coast hubs should also add freight, customs planning, domestic warehousing, and spare parts lead-time assumptions into the financial model.
The biggest investment mistakes usually come from underestimating product-market fit or overestimating the simplicity of validation and scale-up. Before finalizing a purchase, U.S. manufacturers should evaluate the following risk areas:
There is also a strategic risk in choosing a supplier that only sells standalone machinery without understanding facility integration. In many successful projects, especially in regulated sectors, buyers benefit from partners that can link production equipment with water systems, clean utilities, packaging flow, intelligent logistics, and documentation control. Companies with broad engineering and manufacturing resources can sometimes provide a more stable project pathway than vendors focused on a single machine module.
From a service perspective, experienced engineering firms can reduce risk through feasibility review, line balancing, qualification planning, production training, and post-startup optimization. These capabilities matter when entering the U.S. market with new blood collection or diagnostic consumable products, where time-to-commercialization can determine market share.
For example, a supplier with international project execution experience, multiple specialized manufacturing plants, and long equipment lifespan can be attractive to buyers who want durable systems and lower lifecycle replacement pressure. This is especially relevant where stainless-steel-intensive construction, patent-backed design, and multilingual technical support help smooth project delivery for American operations.
Practical buying advice includes:
What is the main difference between a micro blood tube and a capillary tube?A micro blood tube is usually a small finished collection tube designed for storage, transport, and traceability of low-volume blood samples. A capillary tube is a narrow tube used mainly for drawing or transferring tiny volumes, often in laboratory or specialty diagnostic tasks.
Which option is better for large-scale production in the United States?For commercial medical consumables and branded collection products, micro blood tubes are often better because they integrate more easily with automated assembly, labeling, and packaging. Capillary tubes are better for specialized or simpler transfer-based products.
Are these products relevant to pharmaceutical companies?Yes, especially for clinical trial supply, companion diagnostics, biologics support, laboratory operations, and medical device divisions. They are most relevant in pharmaceutical-adjacent manufacturing rather than in API or tablet production.
What regulations should U.S. buyers consider?FDA expectations, cGMP practices where applicable, ISO 13485 quality systems, validation requirements, labeling controls, and product-specific laboratory standards are all important. Buyers should also align equipment documentation with internal quality procedures.
Is plastic always better than glass?Not always. Plastic often reduces breakage and improves user safety, which is valuable for transport and home sampling. Glass may still be preferred in certain capillary applications where established analytical performance is critical.
How do I estimate ROI?Look at yield improvement, defect reduction, labor savings, product pricing power, throughput, and future SKU flexibility. Include utilities, qualification, logistics, and maintenance in the model rather than considering machine price alone.
What should I ask a supplier before buying?Ask about line capacity, validation support, additive handling, material compatibility, spare parts lead times, U.S. service approach, customization options, and reference projects in regulated industries.
Can one supplier handle both equipment and factory integration?Yes. Some engineering companies offer combined capabilities across equipment, utilities, packaging, logistics, commissioning, and training. This can reduce project coordination risk and improve launch speed.
Why do U.S. buyers care about service capability so much?Because downtime, delayed validation, or documentation gaps can disrupt launch schedules and customer commitments. Strong lifecycle service is often as important as the machine specification itself.
What is the 2026 outlook?The strongest trends point toward automation-ready micro collection formats, better traceability, safer materials, more decentralized testing, and stronger sustainability requirements. Capillary tubes will remain important, but growth is likely to concentrate in products aligned with integrated diagnostic workflows.
In summary, micro blood tubes and capillary tubes serve different but overlapping roles in the U.S. healthcare manufacturing landscape. The right investment depends on clinical use, product strategy, automation goals, and regulatory expectations. Buyers that combine detailed technical evaluation with strong supplier due diligence are more likely to achieve stable output, faster qualification, and better long-term returns.
-
Pharmaceutical Water Loop Design in the United States
Pharmaceutical water system loop design is a foundational utility for modern drug manufacturing in the United States. It creates, stores, circulates, sanitizes, and distributes high-purity water so that injectable products, vaccines, biologics, oral liquids, and medical consumables can be produced under controlled GMP conditions. In practical terms, a well-engineered loop protects product quality, reduces microbial risk, supports FDA inspection readiness, and helps manufacturers in hubs such as New Jersey, Boston, Raleigh-Durham, Houston, and San Diego maintain consistent operations. For U.S. facilities handling sterile production, a properly designed pharmaceutical water loop is not optional infrastructure; it is part of the quality system itself.
In the United States, pharmaceutical water is not treated as generic plant utility water. It is a critical process input governed by pharmacopeial expectations, cGMP discipline, validation standards, and site-specific risk management. A pharmaceutical water system loop design brings together pretreatment, reverse osmosis, electrodeionization or distillation, storage, hot or ambient recirculation, point-of-use distribution, instrumentation, sanitization strategy, and documentation into one validated system.
The goal is simple: deliver the right water quality, at the right temperature, flow, and pressure, to every user point without allowing stagnation, biofilm formation, conductivity drift, or total organic carbon excursions. For facilities producing injectables or vaccines, even minor design flaws such as dead legs, poor slope, undersized recirculation pumps, or weak sanitization strategy can create major compliance and product risks.
That is why U.S. owners increasingly evaluate loop design at the earliest concept phase, especially when building new lines near major logistics corridors like the Port of Newark, the Port of Houston, or air cargo centers serving Chicago and Atlanta. The water system must support not only startup, but also long-term expansion, validation efficiency, and reliable batch release.
A pharmaceutical water system loop design is the engineered architecture used to generate and continuously circulate purified water, water for injection, or other compendial water grades throughout a pharmaceutical plant. It includes source water assessment, pretreatment, primary purification, polishing, storage tank design, loop piping layout, point-of-use connections, automation, online monitoring, and sanitization controls.
Manufacturers need it because water is used everywhere in GMP production. It is used as a raw material, an excipient, a cleaning medium, a rinsing medium, a support utility for formulation, and an input to sterilization-related processes. In many U.S. plants, purified water and WFI touch product contact equipment more frequently than any other utility.
A proper loop design addresses several site realities:
For example, a manufacturer in Massachusetts may prioritize high data integrity and integration with a site SCADA system, while a plant in Texas may focus more strongly on feedwater variability, pretreatment robustness, and utility resilience under hot climate conditions. In both cases, the distribution loop must be engineered to prevent contamination while maintaining usability across the production schedule.
System ElementMain FunctionWhy It Matters in GMPTypical U.S. Design FocusPretreatmentRemoves chlorine, hardness, suspended solidsProtects downstream membranes and quality stabilityAdapted to municipal water variationRO UnitPrimary dissolved solids reductionDrives baseline purified water performanceHigh recovery, low fouling designEDI or DistillationFinal ionic polishing or WFI generationSupports pharmacopeial purity requirementsSelected by water grade and energy modelStorage TankBuffers demand and supports circulationImproper tank design can trigger contaminationSpray devices, vent filtration, drainabilityDistribution LoopRecirculates water to points of useControls stagnation and microbial riskVelocity, slope, dead-leg minimizationAutomation and MonitoringTracks conductivity, TOC, temperature, flowProvides data for release and investigations21 CFR Part 11 aligned systemsThe table above shows why the loop is more than piping. It is a controlled system whose design directly affects quality, maintenance, and regulatory confidence.
Pharmaceutical water loops serve different process zones depending on the plant profile. In oral solid dose sites, purified water may support granulation, coating prep, cleaning, and equipment rinsing. In sterile injectable facilities, WFI loops are often linked to compounding, final rinsing, autoclave feed, and aseptic process support. In biotech plants, high-purity water utilities are integrated with buffer prep, CIP skids, and single-use component handling.
The strongest benefit is consistency. A validated loop helps every department work with the same water quality baseline, whether the point of use is in formulation, washing, clean utilities, or microbiology support. This reduces batch variability and simplifies root cause analysis when deviations occur.
Other major benefits include:
Facilities in U.S. biotech clusters increasingly connect loop performance to overall equipment effectiveness. When water systems are unstable, cleaning delays, extended investigations, and hold-time disruptions can reduce production output significantly. By contrast, a stable loop supports operational rhythm and simpler quality release workflows.
Application AreaWater Grade Commonly UsedTypical User PointPrimary BenefitInjectable compoundingWFICompounding vesselsHigh purity and microbial controlEquipment final rinsePurified Water or WFIWasher outletsResidue reduction and repeatable cleaningBiologics buffer prepPurified WaterMixing tanksProcess consistencyOral liquid productionPurified WaterFormulation suitesStable product qualityCIP systemsPurified Water or WFICIP skid return and supplyValidated cleaning supportLaboratory and support usePurified WaterLab taps and prep roomsReliable internal utility supplyFor companies planning new facilities, the water loop often influences room zoning, pipe bridge routing, utility interstitial design, and future expansion corridors. That is one reason turnkey engineering partners are frequently engaged early in planning. A company such as IVEN Pharmatech Engineering typically supports owners by integrating clean utilities with process flow, building layout, and compliance strategy rather than treating water as an isolated equipment purchase.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Injectables’, ‘Biologics’, ‘Vaccines’, ‘Oral Liquids’, ‘Medical Consumables’, ‘CDMO Facilities’], datasets: [{ label: ‘Estimated U.S. demand index for high-purity water loops’, data: [95, 88, 82, 67, 61, 84], backgroundColor: [‘#4472C4′,’#5B9BD5′,’#70AD47′,’#FFC000′,’#A5A5A5′,’#ED7D31’] }] }, options: { responsive: true, maintainAspectRatio: false }});There is no universal system type for every U.S. plant. The correct design depends on required water grade, local feedwater condition, batch profile, sanitization preference, utility economics, and available floor space.
RO-based systems are common for purified water generation. They offer efficient dissolved solids reduction and can be paired with EDI, UV, degassing, and ultrafiltration for tighter control. EDI-based polishing is attractive where continuous operation, chemical reduction, and stable feed conditions align with site goals.
Distillation remains highly relevant for WFI and sterile applications. Multi-effect distillers and vapor compression systems are chosen where thermal robustness and established regulatory acceptance are priorities. Hybrid systems combine membrane and thermal technologies to balance purity, operating cost, and resilience.
Selection should always be tied to the distribution loop. An excellent generation skid cannot compensate for a poorly designed storage and recirculation network.
System TypeBest FitAdvantagesChallengesRO + EDIPurified Water systemsLower chemical use, continuous polishing, good automationRequires stable pretreatment and membrane careDouble-pass ROSites with variable feedwaterImproved conductivity control, robust baseline qualityHigher footprint and energy than single-passMulti-effect distillationWFI generationStrong microbial barrier, established sterile useHigher steam and capital demandsVapor compression distillationMedium to large WFI loadsEfficient thermal operation in some duty profilesMechanical complexity and maintenance skill needsRO + EDI + UF hybridBiotech and flexible facilitiesGood endotoxin and microbial strategy when designed wellRequires integrated control philosophyRO + Distillation hybridSites needing both PW and WFIShared pretreatment, optimized utility architectureNeeds careful load balancingWhen owners review equipment portfolios, they should also evaluate technology depth. IVEN Pharmatech Engineering has built capability in purified water units, multi-effect water distillers, purified steam generators, and solution preparation and distribution systems, which is relevant for facilities looking for coordinated clean utility planning rather than fragmented procurement. More information about the company background is available on its company profile page.
Traditional industrial water treatment methods focus on making water usable for boilers, cooling towers, or general process utility service. Pharmaceutical loop design, by contrast, is built for validated high-purity use. The difference is not just output quality; it is the total control strategy.
Conventional systems may use intermittent storage, low instrumentation density, non-sanitary piping, or unvalidated maintenance practice. That can work for non-GMP industrial operations, but not for drug manufacturing where microbial control, traceability, and documented performance are essential.
In the United States, the choice should be based on intended use. If the water touches product, product-contact equipment, sterile pathways, or validated cleaning surfaces, the system should be engineered as a pharmaceutical water system from day one.
Decision FactorPharmaceutical Loop DesignTraditional Water TreatmentPreferred for GMP?Piping standardSanitary design, drainable, minimal dead legsGeneral industrial pipingPharmaceutical loopMonitoringOnline conductivity, TOC, temp, flow, alarmsPeriodic utility checksPharmaceutical loopValidation supportIQ/OQ/PQ ready documentationLimited or nonePharmaceutical loopMicrobial controlContinuous recirculation and sanitization strategyOften intermittent, higher stagnation riskPharmaceutical loopRegulatory alignmentDesigned for cGMP expectationsIndustrial compliance focusPharmaceutical loopLifecycle costHigher upfront, lower compliance riskLower upfront, higher quality riskPharmaceutical loopThe table shows why apparent short-term savings from a basic utility system can become expensive once deviations, remediation work, or retrofit costs are considered. U.S. buyers increasingly compare not only capex, but also validation effort, water waste, downtime exposure, and inspection readiness.
var ctxComp = document.getElementById(‘comparisonChartUS’).getContext(‘2d’);var comparisonChartUS = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Compliance Readiness’, ‘Microbial Control’, ‘Data Visibility’, ‘Expansion Flexibility’, ‘Lifecycle Cost Efficiency’], datasets: [{ label: ‘Pharmaceutical loop design’, data: [95, 93, 90, 86, 82], backgroundColor: ‘#4472C4’ },{ label: ‘Traditional treatment’, data: [48, 44, 39, 51, 57], backgroundColor: ‘#C0504D’ }] }, options: { responsive: true, maintainAspectRatio: false }});The U.S. market for pharmaceutical water systems remains active due to biologics growth, domestic manufacturing investment, reshoring of strategic capacity, and upgrades to aging facilities. Demand is strongest in sterile injectables, vaccines, CDMO operations, and high-value biologics. States with strong life science investment, including New Jersey, Pennsylvania, North Carolina, California, and Massachusetts, continue to drive utility modernization projects.
Several trends are shaping the market through 2026 and beyond:
Policy pressure is also evolving. U.S. manufacturers face growing scrutiny around resilience, domestic capacity, and environmental performance. Water-intensive sites are paying more attention to reject recovery, pretreatment optimization, and clean utility heat management. Sustainability is now linked to both ESG reporting and operating margin.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. market index for pharmaceutical water loop projects’, data: [100, 108, 117, 129, 141, 156], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of projects emphasizing sustainability and digital control’, data: [22, 29, 37, 48, 58, 69], fill: true, backgroundColor: ‘rgba(112, 173, 71, 0.25)’, borderColor: ‘rgba(112, 173, 71, 1)’, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});For suppliers, this means that technical competence alone is no longer enough. U.S. buyers increasingly want integrated engineering, documentation discipline, FAT/SAT structure, and long-life equipment designed for future expansion. That is especially true in projects near major pharmaceutical clusters where production schedules are aggressive and utility downtime is expensive.
Supplier selection should start with engineering evidence, not brochure claims. The right manufacturer or engineering partner should understand U.S. compliance expectations, sanitary design principles, commissioning logic, validation documentation, and project execution under real plant constraints.
Look for three capability layers.
Technological capabilities: The supplier should be able to design complete systems covering RO, EDI, distillation, purified steam, storage and distribution, instrumentation, and automation. It should understand heat sanitization, chemical sanitization, ambient versus hot loops, and how loop hydraulics affect quality at the point of use.
Manufacturing capabilities: The supplier should have proven fabrication capacity for clean utility skids, sanitary components, and integrated equipment packages. Buyers should ask about shop standards, material traceability, welding quality, FAT procedures, and ability to coordinate adjacent systems. IVEN Pharmatech Engineering, for example, operates specialized manufacturing bases across areas such as pharmaceutical water treatment systems, filling and packaging equipment, logistics systems, and blood collection tube machinery, which can be attractive for owners seeking broader plant integration.
Service capabilities: The supplier should support feasibility consultation, design review, installation, commissioning, validation, training, and after-sales response. This matters because many water system problems emerge not at procurement, but during startup, PQ, or early production campaigns. A lifecycle partner can shorten that curve. Buyers can reach out through the contact page when evaluating project fit.
Evaluation ItemWhat to AskWhy It MattersStrong Supplier SignalRegulatory understandingCan you support FDA-aligned documentation?Reduces compliance gapsStructured URS, DQ, IQ/OQ/PQ packagesSanitary design skillHow do you control dead legs and drainability?Protects microbial performanceDetailed piping standards and examplesWater generation optionsWhich technologies do you integrate?Ensures right-fit designRO, EDI, distillation, hybrid competenceFabrication qualityHow are welds and materials documented?Supports long-term reliabilityTraceable sanitary manufacturing recordsService depthDo you assist with commissioning and validation?Improves startup successFull lifecycle support teamReference experienceHave you completed complex pharma projects?Shows execution credibilityMultiple production lines and turnkey projectsU.S. buyers should also consider local practicalities: spare parts lead time, field service availability, time zone responsiveness, and familiarity with American utility codes and contractor coordination. Ports and trade hubs can influence logistics planning, particularly for skid shipment, customs timing, and phased site delivery.
Investment cost depends on water grade, capacity, sanitization philosophy, automation level, material standard, and facility complexity. A small purified water loop for a localized process area can be relatively modest, while a full WFI generation and distribution system for a sterile injectable plant is a major capital utility.
In the United States, budget planning should account for far more than the generation skid. Owners often underestimate distribution piping, installation labor, orbital welding, passivation, automation integration, commissioning, validation, and documentation review. Renovation projects can cost more than greenfield work because shutdown windows are tighter and routing is more difficult.
ROI should be evaluated through avoided risk and operating performance, not only utility savings. A reliable loop can reduce batch delays, CAPA burden, out-of-spec investigations, and emergency maintenance. It can also support faster market expansion when new lines are added.
Cost CategoryTypical Share of Project BudgetMain Cost DriverBudget AdvicePretreatment and generation20%–30%Water grade, capacity, redundancySize for realistic peak and future loadStorage and distribution loop20%–25%Piping length, material, routingDo not underbudget field installationInstrumentation and automation10%–15%Online analyzers and control integrationPrioritize data visibility earlyInstallation and commissioning15%–20%Site labor, access, contractor coordinationLock schedule windows before procurementValidation and documentation8%–12%IQ/OQ/PQ, SOPs, turnover packageInclude quality review timeContingency and optimization8%–10%Retrofit surprises or utility changesHold contingency for startup learningA useful ROI framework is shown below:
Many owners also compare centralized versus decentralized architectures. A centralized validated loop often has higher upfront capex but better long-term control, simpler quality governance, and lower duplication of maintenance tasks. For product families that require common water grades across multiple suites, this tends to be the better strategic choice.
When sourcing equipment, buyers often review complete portfolios through a supplier equipment catalog to compare how water systems fit with filling, washing, packaging, and process support infrastructure.
The biggest risk is treating the water loop as a commodity. In reality, design mistakes can be expensive to correct after installation. Common issues include undersized recirculation flow, excessive dead legs, poor slope management, weak vent filter design, incompatible sanitization materials, and lack of reserve capacity for future points of use.
Another risk is misalignment between process demand and utility architecture. A loop may be technically compliant yet operationally frustrating if peak demand from washers, compounding vessels, and CIP events was not properly modeled. This can cause pressure dips, temperature instability, and production bottlenecks.
Control system design is another major factor. U.S. sites increasingly expect trendable alarms, audit-supportive data capture, secure user access, and integration with plant historians. Without that visibility, preventive action becomes difficult.
Risk AreaTypical CauseOperational ImpactMitigation StrategyMicrobial growthStagnation, poor sanitization, dead legsExcursions and shutdownsContinuous recirculation and hygienic designInsufficient capacityWeak demand forecastingProduction delaysPeak-load hydraulic modelingMembrane foulingInadequate pretreatmentQuality drift and higher OPEXFeedwater study and pretreatment reviewValidation delaysLate documentation planningStartup postponementDefine deliverables in contract stageEnergy overusePoor equipment selectionHigh utility costLifecycle cost comparison, not just capexFuture retrofit costNo expansion allowanceExpensive shutdown modificationsReserve tie-ins and spare I/O capacityCase experience across the industry shows that early coordination among process, quality, engineering, and validation teams is one of the best risk reducers. Owners should review not only P&IDs, but also point-of-use philosophy, loop balancing, sample plans, sanitization sequence, alarm setpoints, and maintenance access before fabrication begins.
On large integrated projects, engineering partners with experience in full pharmaceutical plant development can add value by resolving layout conflicts early. IVEN Pharmatech Engineering has positioned itself in this space by supporting customized integrated engineering and turnkey pharmaceutical projects, including clean utilities, production lines, and facility coordination for multiple dosage forms and medical device applications.
What water grades are most common in U.S. pharmaceutical plants?Purified Water and Water for Injection are the most common process grades. The right choice depends on the process application, product type, and cleaning requirement.
Does every pharmaceutical plant need a hot loop?No. Hot loops are common where thermal sanitization is preferred, especially for WFI or high-risk applications. Ambient loops can also perform well if designed with a strong microbial control strategy.
How often should a pharmaceutical water loop be sanitized?There is no single frequency for all plants. Sanitization frequency depends on system design, temperature regime, monitoring results, historical trends, and site SOPs.
Can RO-based systems replace distillation for all uses?Not always. RO-based approaches are excellent for many purified water applications, but WFI strategy must be selected based on current regulatory acceptance, risk profile, and operational needs.
What are the most important design details in the distribution loop?Velocity, drainability, dead-leg control, surface finish, valve selection, sampling points, temperature control, and point-of-use design are all critical.
How long does a typical project take in the United States?Depending on complexity, a project may take several months to more than a year when design, fabrication, shipping, installation, commissioning, and validation are included.
Should buyers choose a local supplier or an international engineering partner?The best choice depends on project complexity, internal engineering resources, and the supplier’s ability to support U.S. compliance, field execution, and after-sales service. International partners with proven turnkey experience can be strong options if they provide solid documentation and responsive support.
What makes IVEN Pharmatech Engineering relevant for U.S. buyers?The company combines pharmaceutical water treatment capability with broader plant engineering, production equipment integration, and lifecycle service support. For owners seeking one coordinated partner instead of multiple disconnected vendors, that can reduce interface risk.
What should be included in a supplier RFQ?Include required water grade, hourly and peak demand, source water data, sanitization preference, number of points of use, automation expectations, documentation scope, FAT/SAT requirements, and expansion assumptions.
What is the outlook for 2026?Expect more intelligent monitoring, stronger sustainability targets, higher use of hybrid clean utility systems, and continued investment in U.S. sterile, biotech, and CDMO capacity.
In summary, pharmaceutical water system loop design is a strategic infrastructure decision for manufacturers in the United States. It touches compliance, quality, operating cost, expansion planning, and production reliability. Companies that define user requirements clearly, select the right technology mix, and work with experienced engineering partners are usually best positioned to achieve long-term GMP performance.
-
Multi-Chamber IV Bag Sealing in the United States
Multi-chamber IV bag sealing technology helps pharmaceutical manufacturers produce infusion products that keep incompatible or unstable ingredients separated until activation. In the United States, this approach is increasingly important for premixed drugs, parenteral nutrition, emergency care products, and high-value hospital formulations where sterility, dosing accuracy, shelf life, and workflow efficiency matter. Compared with conventional single-chamber bags, multi-chamber systems can reduce compounding steps, lower medication preparation risk, and improve product differentiation for manufacturers serving acute care networks, group purchasing organizations, and specialized infusion markets.
For buyers in the United States, the topic is not just about the bag itself. It involves seal design, peelable or frangible partitions, film compatibility, aseptic filling, validation, line automation, container closure integrity, production throughput, and regulatory readiness under U.S. FDA cGMP expectations. It also involves supply chain practicality: resin sourcing, cleanroom layout, serialization compatibility, shipping from ports such as Los Angeles, Long Beach, Houston, Savannah, and New York/New Jersey, and technical support close to pharmaceutical hubs like New Jersey, Boston, Chicago, Raleigh-Durham, and San Diego.
In simple terms, a multi-chamber IV bag is a flexible infusion container divided into two or more separate chambers by engineered seals. Those seals are designed to keep drug components, electrolytes, amino acids, glucose, diluents, or other active ingredients apart during storage. At the point of use, the clinician activates the bag by breaking or opening the internal seal, allowing the contents to mix immediately before administration.
This technology matters because many formulations degrade when mixed too early. Vitamins may lose potency, certain antibiotics may have limited in-use stability, and nutrition formulas often require separation to protect sensitive components. By delaying contact between ingredients, manufacturers can offer longer shelf life, more stable drug performance, and safer preparation in hospital pharmacies and bedside settings.
The core advantages can be summarized in the following table.
Advantage How It Works Benefit for U.S. Manufacturers Benefit for Hospitals Ingredient separation Internal seals isolate unstable or incompatible components Supports more advanced product portfolios Improves safety and preparation consistency Longer shelf life Mixing occurs only before infusion Reduces inventory write-offs Improves stock management Reduced compounding Preconfigured bag replaces some manual pharmacy steps Creates higher-value finished products Lowers labor burden in sterile compounding areas Lower contamination risk Closed system minimizes handling Strengthens product quality positioning Supports aseptic administration practices Dose accuracy Precise chamber filling and validated mixing volume Improves batch consistency Reduces bedside preparation variability Better workflow Activation is fast and standardized Appeals to health systems seeking ready-to-use formats Speeds treatment in emergency and ICU settingsFor U.S. buyers, the strategic value is especially strong in shortages, labor-constrained pharmacy environments, and therapeutic categories where ready-to-activate infusion products can improve speed and compliance.
Multi-chamber IV bag sealing technology refers to the complete engineering system used to create separated chambers inside a soft infusion bag while maintaining sterile integrity, fill precision, and reliable activation. This is not only a packaging function. It combines film selection, bag forming, chamber welding, port integration, filling sequence control, sealing energy management, leak testing, visual inspection, overwrapping, and process validation.
The key technical element is the internal chamber seal. Depending on the product design, the seal may be frangible, peelable, or selectively breakable under controlled pressure. The activation force must be high enough to preserve transport safety, yet low enough for nurses or pharmacists to open predictably without damaging the outer container.
Main technical advantages include:
From a plant engineering perspective, manufacturers in the United States should evaluate the whole line, not only the final bag design. This includes sterile solution preparation, CIP/SIP compatibility, clean utilities, automated logistics, in-process controls, and validation documentation. Companies looking for integrated project support often review turnkey pharmaceutical engineering solutions because the filling line alone does not guarantee commercial readiness.
One area where supplier capability matters is technology depth. Shanghai IVEN Pharmatech Engineering has built its reputation around pharmaceutical process and packaging systems, including IV solution lines and related utility systems. From a technological capability standpoint, that matters because multi-chamber bag production depends on more than a single machine frame: it requires process integration between preparation, sterile handling, bag forming, filling, sealing, and downstream packaging.
The table below shows the main technical functions buyers should assess when comparing equipment.
Technical Function Why It Matters Typical Buyer Question Risk if Weak Internal seal consistency Controls separation and activation reliability What is the validated seal opening range? Premature mixing or difficult activation Filling accuracy Maintains chamber dose precision How is chamber volume verified? Off-spec product and batch loss Film handling Prevents wrinkles, weak welds, and defects Which film structures are supported? Leaks, cosmetic rejects, unstable quality Sterile process design Protects microbiological quality How are aseptic risks controlled? Compliance findings and recalls Inspection systems Detects seal, particulate, and fill anomalies Is 100% inspection available? Defects reaching market Validation support Accelerates U.S. qualification Are IQ/OQ/PQ documents included? Longer startup and approval delaysHospitals in the United States increasingly value multi-chamber IV systems because they support standardized therapy while reducing manual steps. The strongest demand tends to come from acute care hospitals, compounding centers, oncology networks, trauma centers, dialysis services, and home infusion programs seeking safer ready-to-use or ready-to-activate products.
Clinically, the biggest benefit is process simplification. Instead of drawing, transferring, or reconstituting multiple components under pressure, clinicians can activate a validated bag format designed for consistent mixing. This is particularly useful where labor is tight, medication turnaround must be fast, or sterile compounding exposure needs to be minimized.
Common U.S. application settings include emergency departments in large metro areas, ICU pharmacies in New York and Chicago, perioperative units in Houston, nutrition support teams in Boston, and regional health systems in the Southeast and Midwest where staffing efficiency is a recurring priority.
Application Typical Product Use Clinical Value Operational Value Parenteral nutrition Amino acids, dextrose, lipid-adjacent systems Protects stability before use Reduces pharmacy assembly steps Antibiotic infusion Drug powder or concentrate with diluent Supports fresher mixing Speeds treatment initiation Critical care Emergency hydration or combination support products Enables rapid bedside activation Improves workflow in ICU and ER Oncology support Adjunctive infusion preparations Helps standardize sensitive handling Less manual prep time Dialysis support Specialized fluid systems Improves consistency of formulation Supports high-volume routine use Home infusion Ready-to-activate therapy products Simplifies patient or caregiver use Improves convenience and logisticsThe chart below shows a realistic estimate of U.S. hospital demand growth for multi-chamber IV products by major application segment.
var ctxBarDemand = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBarDemand, { type: ‘bar’, data: { labels: [‘Parenteral Nutrition’, ‘Antibiotics’, ‘Critical Care’, ‘Dialysis’, ‘Oncology Support’, ‘Home Infusion’], datasets: [{ label: ‘Estimated U.S. Demand Index 2026’, data: [92, 81, 76, 58, 49, 67], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, title: { display: true, text: ‘Demand Index’ } } } }});When evaluating opportunities, manufacturers should also consider U.S. compounding reform and hospital procurement behavior. Ready-to-use and ready-to-activate products are often favored where they can support quality assurance and reduce labor-intensive sterile preparation.
Multi-chamber bags vary by chamber count, seal mechanism, sterilization compatibility, and film construction. In practice, the right design depends on product chemistry, target shelf life, oxygen sensitivity, steam resistance, puncture resistance, extractables profile, and downstream packaging conditions.
The most common product categories are two-chamber and three-chamber bags. Two-chamber versions are typically used for a drug and diluent or for binary nutrient systems. Three-chamber bags are common where more complex nutrient or combination formulations require additional separation.
Film selection is equally important. U.S. pharmaceutical buyers often evaluate non-PVC soft bag structures, multilayer coextruded films, and specialty formulations designed to balance flexibility, clarity, sealability, and barrier performance. Port design, overpouch requirements, and terminal sterilization exposure also affect the final decision.
Bag Type or Material Description Typical Use Main Advantage Two-chamber bag Two isolated compartments with breakable internal seal Drug + diluent systems Simple activation and broad applicability Three-chamber bag Three separated compartments Nutrition and complex admixtures Supports more advanced formulations Peelable seal design Controlled opening under applied pressure Products needing predictable activation force Reliable user experience Frangible seal design Seal ruptures when manipulated Fast-activation applications Clear chamber communication upon use Non-PVC multilayer film Flexible multilayer film with tailored performance Modern infusion packaging Good compliance with market preference trends High-barrier coextruded film Enhanced resistance to gas or moisture transmission Sensitive formulations Better product protectionSuppliers with strong product engineering can help match film structures to sealing process windows. On the manufacturing capability side, IVEN is notable for operating multiple specialized production facilities dedicated to pharmaceutical machinery and related systems. That matters for buyers because multi-chamber bag lines involve coordinated fabrication quality, repeatable welding performance, utility integration, and long-term spare parts support rather than one-off assembly.
If you want to review equipment categories relevant to IV production, it is useful to explore the broader pharmaceutical equipment portfolio to understand how line components, water systems, logistics, and packaging automation fit together.
The area chart below illustrates how U.S. preference is shifting from basic single-compartment solutions toward more specialized multi-chamber and high-barrier formats through 2026.
var ctxAreaShift = document.getElementById(‘areaShiftChart’).getContext(‘2d’);var areaShiftChart = new Chart(ctxAreaShift, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [ { label: ‘Standard Single-Chamber Share’, data: [74, 71, 68, 64, 60, 56], borderColor: ‘#9c755f’, backgroundColor: ‘rgba(156,117,95,0.25)’, fill: true, tension: 0.3 }, { label: ‘Multi-Chamber and High-Barrier Share’, data: [26, 29, 32, 36, 40, 44], borderColor: ‘#2ca02c’, backgroundColor: ‘rgba(44,160,44,0.25)’, fill: true, tension: 0.3 } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: ‘Estimated Share %’ } } } }});Single-chamber bags remain useful for stable, uncomplicated solutions with long-established manufacturing methods. They are generally easier to produce, cheaper to validate, and suitable for high-volume commodity fluids. However, they do not solve incompatibility or short in-use stability issues when multiple components must be combined close to administration.
Multi-chamber systems are more complex and require tighter control of seal design, line setup, and validation. Yet they provide product differentiation and workflow benefits that standard bags cannot easily match. In the U.S. market, this distinction is important because buyers increasingly evaluate total cost of care, not only unit purchase price.
Comparison Point Multi-Chamber IV Bag Single-Chamber IV Bag Commercial Impact Formulation flexibility High Limited Multi-chamber supports premium products Ingredient separation Yes No Key advantage for unstable combinations Manufacturing complexity Higher Lower Requires stronger process control Hospital preparation burden Lower Often higher Improves workflow for pharmacies and nurses Initial equipment investment Higher Lower Needs ROI planning Product differentiation Strong Modest Useful in competitive hospital marketsFor many U.S. manufacturers, the decision is not either-or. Commodity fluids may stay on single-chamber lines, while strategic, higher-margin therapies shift to multi-chamber formats. This hybrid portfolio approach is common among companies serving both broad hospital distribution and specialty channels.
The comparison chart below shows a simplified scoring model for key product selection factors.
var ctxComparison = document.getElementById(‘comparisonSupplierChart’).getContext(‘2d’);var comparisonSupplierChart = new Chart(ctxComparison, { type: ‘bar’, data: { labels: [‘Stability Support’, ‘Workflow Efficiency’, ‘Capex Simplicity’, ‘Product Differentiation’, ‘Scale-Up Flexibility’, ‘Hospital Appeal’], datasets: [ { label: ‘Multi-Chamber’, data: [94, 88, 54, 91, 79, 87], backgroundColor: ‘#6f42c1’ }, { label: ‘Single-Chamber’, data: [58, 61, 86, 52, 72, 63], backgroundColor: ‘#17a2b8’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100, title: { display: true, text: ‘Performance Score’ } } } }});The United States market is seeing steady interest in multi-chamber IV bag capacity for several reasons: hospital staffing pressure, more demand for ready-to-use sterile products, premiumization of infusion portfolios, and continued concern about drug shortages and compounding risk. Buyers are especially active in regions with concentrated pharmaceutical manufacturing and distribution infrastructure such as New Jersey, Pennsylvania, North Carolina, Texas, California, and the Midwest.
Growth is also supported by larger health systems seeking standardized products across multiple hospitals. When a network spans Boston, Philadelphia, Atlanta, Dallas, and Phoenix, simplifying pharmacy workflows and reducing bedside variation can create meaningful operational value.
From a supply chain standpoint, imported line equipment must fit realistic U.S. implementation timelines. Ports such as Long Beach, Los Angeles, Houston, Savannah, and New York/New Jersey remain important for inbound machinery and components. Inland commissioning then depends on local contractors, cleanroom coordination, and utility readiness.
The line chart below illustrates a realistic growth outlook for U.S. multi-chamber IV bag production demand through 2026.
var ctxLineGrowth = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLineGrowth, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Production Capacity Demand (Million Bags)’, data: [118, 126, 139, 154, 171, 189], borderColor: ‘#1f77b4’, backgroundColor: ‘rgba(31,119,180,0.12)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false, title: { display: true, text: ‘Million Bags’ } } } }});Another trend for 2026 is sustainability. More U.S. manufacturers are evaluating energy-efficient sealing systems, reduced scrap rates, better material utilization, and packaging formats with lower transport burden. Policy pressure around resilient domestic supply also encourages investment in flexible lines that can support both commercial and contingency production.
As a case example, companies developing premium hospital infusion portfolios often start with a mid-scale line for selected SKUs, then add more chamber configurations after market uptake is confirmed. This staged approach is usually more practical than overbuilding capacity on day one.
Choosing a supplier for multi-chamber IV bag sealing technology is a strategic decision. The right partner should understand pharmaceutical engineering, not just mechanical fabrication. In the United States, reliability is tied to documentation quality, validation support, regulatory familiarity, after-sales response, and the supplier’s ability to coordinate with local EPC firms, cleanroom contractors, and quality teams.
Start by screening suppliers across six dimensions: technical fit, regulatory competence, manufacturing depth, service capability, project references, and total lifecycle support. A lower upfront quote may become expensive if the supplier cannot deliver stable sealing, compliant documentation, or fast troubleshooting during SAT and PQ.
Selection Criterion What to Ask Good Sign Warning Sign Regulatory understanding Can the supplier support U.S. FDA cGMP documentation? Structured DQ/IQ/OQ/PQ package Only generic manuals Bag and seal expertise How many multi-chamber projects have been delivered? Clear performance data Concept-level answers only Manufacturing quality Are critical parts made in-house or tightly controlled? Traceable fabrication and QC Unclear sourcing chain Utilities integration Can the supplier align with WFI, clean steam, HVAC, and logistics? System-level engineering view Machine-only mindset U.S. project support How are FAT, shipping, installation, and training handled? Defined schedule and service plan Support starts after shipment only Long-term service What spare parts and remote support are available? Lifecycle support commitment Limited post-startup engagementService capability is often the deciding factor. IVEN, for example, positions itself around full lifecycle engineering support that can include feasibility advice, design coordination, equipment customization, installation, commissioning, qualification support, training, and optimization. For U.S. buyers building or upgrading lines, this service depth can reduce the common risks of layout mismatch, schedule slippage, and fragmented vendor accountability. You can learn more about the company background through its corporate overview.
It is also wise to request a supplier scorecard with measurable indicators such as seal defect rate, line availability, speed range, validation document turnaround, spare part lead time, and remote support response targets.
Investment levels vary significantly based on output volume, chamber count, aseptic design, automation level, utility scope, inspection requirements, and packaging integration. A pilot or lower-volume development line may serve niche products, while a fully integrated commercial line for a U.S. plant can require a much larger budget when clean utilities, sterile preparation, inspection, and secondary packaging are included.
Budget planning should cover both direct and indirect costs:
Cost Category Typical Share of Budget Main Variables Cost Control Tip Core production line 30% to 40% Speed, chamber count, automation Match capacity to launch plan Utilities and process systems 15% to 25% WFI, steam, HVAC, piping Audit existing plant capability first Facility adaptation 10% to 20% Layout, cleanroom, flooring, zoning Use 3D layout review early Inspection and packaging 10% to 15% Vision systems, leak test, cartoning Plan for future SKU expansion Validation and training 5% to 10% Protocols, execution, SOP readiness Include documentation in supplier scope Contingency 5% to 10% Schedule change, utilities, freight Reserve budget from the startROI usually depends on five drivers: premium pricing versus standard bags, lower compounding burden for customers, improved product shelf life, reduced waste, and stronger contract opportunities with hospital systems. Many manufacturers model payback in phases: initial launch volume, year-two SKU expansion, and year-three utilization improvement.
A realistic U.S. ROI model often works best when the line is tied to targeted therapeutic products rather than generic fluid production alone. Facilities near distribution corridors such as New Jersey, Memphis, Dallas-Fort Worth, or Columbus may also gain logistics efficiencies that improve delivered economics.
Despite the benefits, investment risk should be assessed carefully. The most common issue is underestimating formulation-packaging interaction. A strong bag design can still fail commercially if the film, seal, and product chemistry are not optimized together.
Key considerations include:
2026 will likely bring tighter expectations around digital traceability, sustainability reporting, and resilient sourcing. Buyers should ask whether the proposed line can support electronic batch record integration, vision-based quality monitoring, predictive maintenance, and energy optimization. These are no longer optional for many advanced pharmaceutical plants.
Another practical risk is service delay after installation. To reduce this, buyers should agree on spare parts strategy, remote diagnostics, and escalation contacts before shipment. If your project is still at evaluation stage, the fastest next step is usually a structured technical discussion through the supplier’s U.S. project inquiry channel.
For U.S. companies comparing local and overseas suppliers, the decision should be based on total project reliability, not geography alone. A supplier with deep pharmaceutical engineering, strong manufacturing control, and comprehensive lifecycle services may outperform a local vendor that offers faster meetings but weaker execution.
What products are best suited for multi-chamber IV bags?Products that benefit most are those with ingredients that should remain separate until use, including selected nutrition formulations, certain antibiotic systems, and specialty infusion combinations.
Are multi-chamber IV bag lines significantly more expensive than standard IV bag lines?Yes, they usually require higher capital investment because of added chamber sealing complexity, validation demands, and more precise process control. However, they can generate better margins and stronger differentiation.
Can non-PVC films be used for multi-chamber IV bags in the United States?Yes. Non-PVC and multilayer film structures are commonly evaluated for modern infusion products, especially where flexibility, compatibility, and barrier performance are important.
What is the biggest technical challenge in production?The most critical challenge is achieving stable internal seals that remain secure during storage and transport but open predictably during activation without damaging the bag.
How long does a typical project take?Depending on line scale and facility readiness, a commercial project may take many months from design review through FAT, shipment, installation, qualification, and performance verification. Utility and layout readiness often determine the pace.
Why do U.S. hospitals prefer these products?They can reduce manual preparation, support medication safety, improve consistency, and speed therapy initiation in busy pharmacy and nursing environments.
Should buyers choose a machine supplier or an integrated engineering partner?For simple expansions, a machine supplier may be enough. For larger U.S. projects involving utilities, cleanrooms, validation, and packaging integration, an engineering partner is usually the safer option.
What should be included in supplier due diligence?Review project references, seal performance data, film compatibility experience, manufacturing quality systems, validation documentation samples, service response plans, and spare parts support.
In summary, multi-chamber IV bag sealing technology is becoming a strategic manufacturing capability in the United States. It supports higher-value sterile products, aligns with hospital demand for safer and more efficient workflows, and offers strong long-term opportunity when paired with the right formulation strategy and engineering partner.