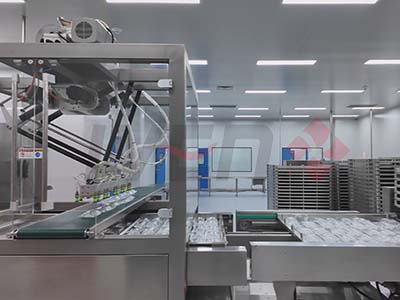
IV Bag Production Lines in the United States: 2026 Guide
An IV bag production line is the integrated manufacturing system used to form, fill, seal, inspect, and package intravenous solution bags for hospital and clinical use. In the United States, demand is rising for advanced lines that can produce multi-chamber IV bags, keep unstable ingredients separate until administration, and support higher standards for sterility, traceability, and regulatory compliance. For pharmaceutical manufacturers, CDMOs, and medical consumables investors, the right line can improve product stability, expand product portfolios, reduce contamination risk, and strengthen long-term competitiveness in a market shaped by FDA expectations, hospital safety goals, and resilient domestic supply planning.
Buyers in major U.S. pharma clusters such as New Jersey, Boston, the Research Triangle in North Carolina, Indianapolis, Texas, and Puerto Rico increasingly evaluate IV bag equipment not only on speed, but on validation support, film compatibility, clean utility integration, and lifecycle service. This guide explains what an IV bag production line does, compares common production formats, reviews 2026 market trends, and outlines how to choose a dependable supplier for the United States market.
Quick Answer: How an IV Bag Production Line Improves Stability and Safety

The quick answer is straightforward: an IV bag production line allows pharmaceutical companies to manufacture standard or multi-chamber infusion bags that separate active ingredients, diluents, electrolytes, or nutrition components until the point of use. That matters because many compounds lose potency, change color, precipitate, or degrade when mixed too early. By keeping ingredients apart and allowing activation before administration, manufacturers can extend shelf stability and help hospitals reduce medication preparation errors.
In practical U.S. hospital settings, this technology supports safer workflows in emergency departments, oncology centers, intensive care units, and large health systems that need ready-to-use sterile products. Compared with older manual admixture approaches, advanced production lines support more consistent dosing, lower risk of particulate contamination, improved batch traceability, and stronger compatibility with high-volume institutional procurement.
For buyers looking at long-term manufacturing strategy, the production line is not just a machine. It is part of a full sterile manufacturing ecosystem that includes formulation preparation, water systems, cleanroom design, container material selection, quality control, serialization, and documentation. That is why many manufacturers prefer experienced engineering partners that can support the full project lifecycle instead of supplying isolated equipment only.
| Production Stage | Main Function | Impact on Product Quality | Impact on Patient Safety |
|---|---|---|---|
| Film unwinding and forming | Shapes the IV bag body from medical-grade film | Ensures uniform bag dimensions | Reduces leakage and handling failure |
| Port insertion | Adds administration and additive ports | Improves connection consistency | Lowers risk of port-related contamination |
| Solution filling | Accurately doses sterile liquid into bag chambers | Protects dosage precision | Supports correct clinical administration |
| Sealing | Closes chambers and perimeter seams | Maintains container integrity | Prevents microbial ingress |
| Sterilization integration | Coordinates with terminal sterilization process | Improves sterility assurance | Supports hospital-ready safety standards |
| Inspection and leak test | Identifies cosmetic or functional defects | Rejects nonconforming units | Prevents unsafe bags from release |
| Overpouching and packaging | Protects finished product in distribution | Preserves shelf life | Maintains condition through transport |
The table above shows why buyers should evaluate the line as a process chain rather than a single filler or sealer. Every stage contributes to final sterility, dose accuracy, and product reliability.
What Is an IV Bag Production Line and What Are Its Main Advantages?

An IV bag production line is a specialized pharmaceutical manufacturing line designed to make intravenous solution bags from soft film materials, fill them with sterile formulations, and seal them for final sterilization and distribution. Depending on the design, the line may produce single-chamber bags for saline, dextrose, irrigation, or basic infusion solutions, or multi-chamber bags for products that require ingredient separation before use.
Main advantages include flexible product development, higher automation, lower manual intervention, and stronger process reproducibility. In the United States, these benefits are especially important because sterile manufacturing economics are driven by labor cost, compliance burden, and downtime risk. An automated line helps reduce operator dependency while improving digital recording, in-line monitoring, and batch consistency.
Another major advantage is supply chain resilience. U.S. healthcare systems have experienced repeated shortages in IV solutions and sterile injectables. A well-designed domestic or regional IV bag line can reduce exposure to long shipping routes through the ports of Los Angeles, Long Beach, Savannah, or Newark, especially when buyers align production with local demand forecasts.
From a technical perspective, advanced lines also support better compatibility with MES, SCADA, electronic batch records, and data integrity requirements. That makes them more attractive for companies planning greenfield facilities or expansion projects in regulated markets.
| Line Module | Typical Role | Why U.S. Buyers Value It | Common Upgrade Option |
|---|---|---|---|
| Bag forming unit | Creates the pouch structure | Supports consistent bag geometry | Quick changeover tooling |
| Port welding station | Attaches ports and connectors | Critical for closure integrity | Vision-guided alignment |
| Filling system | Dispenses sterile solution | Controls volume accuracy | Mass flow verification |
| Chamber separation unit | Creates breakable or permanent internal seals | Enables multi-chamber products | Enhanced seal monitoring |
| Inspection system | Checks leaks, seals, appearance | Reduces false release risk | AI-assisted defect recognition |
| Packaging section | Final packs products for shipment | Improves warehouse efficiency | Robotic case packing |
| Data and control system | Manages production parameters | Supports cGMP documentation | 21 CFR Part 11-ready interfaces |
This is also where supplier capability matters. Some vendors offer machine-only sales, while others provide process design and full plant integration. Buyers who need broader support often review a supplier’s engineering background and industry experience before shortlisting candidates.
Clinical Benefits and Hospital Applications of IV Bag Production Line Production

The clinical value of modern IV bag production is strongest where time-sensitive sterile delivery is essential. Hospitals in New York, Chicago, Houston, Phoenix, and Atlanta increasingly prefer ready-to-use or ready-to-activate containers that reduce bedside preparation steps. Multi-chamber technology is especially useful when ingredients are incompatible during long storage but must be combined immediately before infusion.
Examples include parenteral nutrition, antibiotics requiring reconstitution, electrolyte-balanced formulations, and specialty admixtures. In oncology and critical care, sterile accuracy and contamination control can directly affect patient outcomes. In home infusion and ambulatory care, bag durability and compact packaging improve logistics.
For hospital pharmacies, one of the biggest benefits is workflow simplification. Fewer manual mixing steps can lower compounding burden, shorten preparation time, and reduce human error. For group purchasing organizations and integrated delivery networks, standardized products can also improve procurement efficiency.
| Clinical Setting | Typical IV Bag Use | Why Advanced Production Helps | Operational Benefit |
|---|---|---|---|
| Emergency department | Rapid hydration and electrolyte correction | Reliable ready-to-use supply | Faster treatment initiation |
| ICU | Critical infusions and complex fluid therapy | Higher sterility assurance | Lower interruption risk |
| Oncology center | Specialty infusion support | Stable compartmentalized components | Safer preparation workflow |
| Neonatal care | Precise low-volume formulations | Improved dose consistency | Better batch reliability |
| Home infusion | Portable therapy products | Durable soft-bag packaging | Easier transport and storage |
| Dialysis center | Related sterile solution handling | High-volume production compatibility | Stable recurring supply |
| Hospital pharmacy | Reconstitution and admixture reduction | Multi-chamber convenience | Labor savings |
The table highlights that product design and production line capability are closely tied to end-use workflows. A line suitable for standard saline may not be sufficient for more advanced clinical applications.
This demand chart reflects why buyers often start with broad hospital solution products, then expand into higher-value specialty segments once validation and process control are established.
Common Types of IV Bag Production Line and Film Material Options
There is no single universal IV bag production line. The right configuration depends on container style, output requirement, sterilization method, compatibility target, and budget. In the U.S. market, soft-bag systems are commonly evaluated alongside PP bottle lines and glass bottle lines when product portfolios include multiple infusion categories. However, for this guide, the focus remains on IV bags.
Common production line categories include single-chamber soft-bag lines, multi-chamber bag lines, and specialty lines for high-barrier or customized pharmaceutical formulations. Film material choice is equally important. Buyers typically compare non-PVC materials, multilayer co-extruded films, and formulations optimized for sealability, transparency, flexibility, and sterilization resistance.
Material selection affects oxygen barrier performance, extractables and leachables profile, low-temperature flexibility, sterilization durability, and port welding quality. U.S. buyers must also think about sustainability pressure, especially from health systems pursuing reduced DEHP exposure, lower waste, and better material documentation.
| Bag or Material Type | Typical Use | Main Advantage | Main Limitation |
|---|---|---|---|
| Single-chamber soft bag | Saline, dextrose, irrigation | Simpler equipment and lower cost | Limited support for unstable combinations |
| Multi-chamber soft bag | Separated ingredients and specialty solutions | Improved stability before activation | Higher line complexity |
| Non-PVC film | Broad infusion applications | Reduced plasticizer concerns | Needs validated sealing parameters |
| Multilayer co-extruded film | Higher barrier applications | Better protection and strength balance | Higher material cost |
| Transparent medical film | Visual inspection priority | Easy fluid appearance check | May vary in barrier performance |
| High-temperature resistant film | Terminal sterilization conditions | Better process stability | Requires precise material qualification |
| Customized port-compatible film | Specialty bag formats | Better integration with accessories | Longer development timeline |
In many projects, material qualification takes longer than expected. That is why some buyers work with suppliers that can support line customization, sample validation, and broader plant engineering through a turnkey pharmaceutical project approach rather than piecing together separate contractors.
Multi-Chamber IV Bag Production Line vs Single-Chamber IV Bags: Detailed Comparison
Multi-chamber IV bag technology attracts strong interest because it combines pharmaceutical formulation strategy with container engineering. Instead of pre-mixing all ingredients in one space, the bag uses separate chambers divided by internal seals. These seals are opened or broken at the point of preparation, allowing the components to mix shortly before administration.
Single-chamber bags remain ideal for straightforward infusion products with proven stability and very large volume demand. They are easier to manufacture, easier to validate, and often deliver lower unit cost. But for sensitive products or differentiated product portfolios, multi-chamber systems offer clear commercial and clinical benefits.
| Comparison Factor | Multi-Chamber IV Bag | Single-Chamber IV Bag | Buyer Implication |
|---|---|---|---|
| Formulation stability | Keeps ingredients separate until use | All contents stored together | Multi-chamber suits unstable combinations |
| Line complexity | Higher | Lower | Single-chamber is easier for first projects |
| Capital cost | Higher | Lower | Budget planning differs significantly |
| Product differentiation | Strong | Moderate | Multi-chamber supports premium positioning |
| Validation workload | More extensive | More straightforward | Resource needs must be planned early |
| Hospital workflow value | High for reconstitution reduction | High for basic fluid needs | Choice depends on target customer segment |
| Unit manufacturing speed | Usually lower than simple bags | Usually higher | Output forecasts must be realistic |
For U.S. buyers, the key question is not which bag is universally better, but which one matches market strategy. A manufacturer serving broad med-surg demand in the Midwest may prioritize stable, high-output single-chamber lines. A company targeting value-added hospital products in California or Massachusetts may justify multi-chamber investment for differentiation.
The comparison chart makes the tradeoff visible: multi-chamber lines win on differentiation and stability, while single-chamber lines typically win on simplicity and throughput.
Current Market Trends and Demand for IV Bag Production Line Production Capacity
By 2026, the U.S. market for IV bag production equipment is being shaped by five forces: drug shortage mitigation, hospital preference for ready-to-use products, localization of sterile manufacturing, digital quality systems, and sustainability pressure. Demand is strongest among established infusion manufacturers, contract manufacturers entering sterile liquids, and investors building modern facilities near logistics and workforce hubs.
Regions around New Jersey and Pennsylvania benefit from dense pharmaceutical ecosystems. North Carolina offers strong life science expansion. Texas supports large healthcare demand and manufacturing space. Puerto Rico remains strategically important for regulated production. Proximity to ports such as Houston, Savannah, and Newark can also influence equipment import and spare parts planning.
2026 trends also include higher interest in modular factory design, predictive maintenance, robotics in secondary packaging, and enhanced container closure inspection. Environmentally, buyers are asking more questions about energy use, compressed air efficiency, water consumption, and recyclability of packaging materials.
The line chart illustrates a realistic upward trend rather than explosive growth. This is typical for regulated pharmaceutical equipment markets, where projects are large, capital-intensive, and approval-driven.
This area chart shows the shift many analysts expect through 2030: traditional high-volume formats remain important, but higher-value multi-chamber and automation-heavy projects gain share.
How to Choose a Reliable IV Bag Production Line Manufacturer or Supplier
Choosing a supplier is often more difficult than choosing a machine concept. Buyers in the United States should evaluate at least six categories: regulatory understanding, engineering depth, manufacturing quality, service responsiveness, spare parts strategy, and total project integration capability.
First, check whether the supplier understands FDA cGMP expectations, validation protocols, documentation structure, and data integrity needs. Second, review real manufacturing capability. Does the supplier build core modules in-house, or only assemble sourced components? Third, confirm lifecycle support. A low purchase price can become expensive if FAT preparation is weak, commissioning is delayed, or U.S. service coverage is limited.
Technological capability matters as much as price. Some established global engineering companies have accumulated significant patents in IV solution equipment, developed multiple container formats, and delivered thousands of lines across regulated markets. That depth can be important for challenging projects such as multi-chamber systems, utility integration, or complex acceptance testing.
Manufacturing capability should also be verified. Buyers should ask about fabrication standards, stainless steel quality, machining controls, electrical documentation, and whether the supplier has dedicated plants for filling and packaging machinery, water systems, intelligent logistics, or related medical production equipment. Broader manufacturing depth generally reduces coordination risk.
Service capability is the third pillar. Strong suppliers support feasibility studies, engineering design, installation, commissioning, IQ/OQ/PQ assistance, training, technology transfer, and after-sales optimization. For U.S. projects, time zone response and spare parts planning are especially important.
| Supplier Evaluation Item | What to Ask | Why It Matters | Warning Sign |
|---|---|---|---|
| Regulatory knowledge | Can you support FDA-oriented validation documents? | Reduces compliance gaps | Generic answers only |
| Reference projects | Do you have sterile infusion line examples? | Shows practical experience | No comparable installations |
| Engineering integration | Can you coordinate utilities and cleanroom interfaces? | Prevents layout conflicts | Machine-only scope with no support |
| Factory acceptance testing | What FAT protocol is included? | Improves commissioning readiness | Undefined FAT criteria |
| Service responsiveness | How quickly are critical issues handled? | Protects uptime | No clear escalation path |
| Spare parts availability | Which parts should be stocked in the U.S.? | Reduces downtime risk | No recommended inventory plan |
| Total cost transparency | What is included and excluded? | Avoids budget surprises | Large hidden change-order risk |
If you are comparing integrated suppliers, it is useful to review available pharmaceutical equipment portfolios to see whether the vendor can support upstream and downstream requirements beyond the IV bag line itself.
As one example of what buyers often look for, Shanghai IVEN Pharmatech Engineering has built its reputation around pharmaceutical engineering integration rather than single-equipment sales. Its technology capabilities include deep experience in IV solution systems, compliance-focused design, and a large patent base in IV and blood collection equipment. Its manufacturing capabilities extend across specialized plants covering filling and packaging machinery, pharmaceutical water treatment, intelligent conveying, and medical consumables equipment. Its service capabilities include feasibility consulting, design, customization, installation, commissioning, validation support, training, and long-term optimization. For U.S. buyers who need more than a standalone machine, that breadth can help reduce project coordination risk.
Investment Cost, Budget Planning and ROI Analysis for IV Bag Production Line
Investment cost depends on container type, automation level, output target, cleanroom scope, utility systems, validation package, and whether the project is a line addition or a new facility. A single-chamber line for standard infusion products can be far less expensive than a multi-chamber line that requires advanced seal control, more demanding qualification, and broader process development.
Budget planning should include much more than the machine price. U.S. investors commonly underestimate facility modifications, HVAC upgrades, purified water and WFI interfaces, clean steam, compressed air quality, EBR integration, and operator training. They may also overlook import logistics, customs timing, installation supervision, SAT planning, media fills, and local compliance consulting.
| Cost Category | Low Complexity Project | Higher Complexity Project | Budget Note |
|---|---|---|---|
| Core production line | $1.8M-$4.0M | $4.5M-$9.0M+ | Depends on speed and chamber design |
| Utilities integration | $250K-$800K | $800K-$2.0M | WFI, clean steam, HVAC interfaces matter |
| Cleanroom modifications | $300K-$1.2M | $1.0M-$3.5M | Higher if retrofitting an old site |
| Validation and documentation | $120K-$400K | $350K-$900K | Often under-budgeted |
| Training and start-up | $50K-$150K | $120K-$350K | Should include maintenance teams |
| Spare parts and contingencies | $80K-$250K | $200K-$600K | Important for year-one stability |
| Total indicative range | $2.6M-$6.8M | $6.9M-$16.4M+ | Project-specific and highly variable |
ROI depends on utilization rate, product mix, labor savings, waste reduction, and gross margin of the final IV portfolio. A line making commodity saline behaves very differently from one making premium multi-chamber clinical products. Buyers should model at least three scenarios: conservative, expected, and full-capacity.
A realistic ROI model should include revenue from avoided outsourcing, improved fill accuracy, lower reject rates, and faster launch of differentiated products. For many U.S. manufacturers, the strongest return is strategic rather than immediate: control over supply, less dependence on external sterile capacity, and stronger positioning with hospitals and distributors.
When planning capex, some companies also evaluate whether a supplier can support phased expansion. Starting with a validated base line and reserving space for future modules may improve cash flow and reduce early overbuilding.
Key Considerations and Potential Risks When Investing in IV Bag Production Line
The biggest investment risk is misalignment between product strategy and line design. A buyer may purchase a high-speed line optimized for standard bags, then later realize the target market wants multi-chamber or specialty packaging. Another common risk is assuming that successful operation in another country automatically translates to easy acceptance in the United States. Documentation, validation depth, software expectations, and quality unit requirements may be more demanding.
Project execution risk is also significant. Layout mistakes can cause material flow conflicts, maintenance access problems, and utility bottlenecks. This is especially true in brownfield sites around older manufacturing zones in the Northeast or Midwest. Early 3D layout review and utility mapping are essential.
Supply risk should not be ignored. Critical components, film materials, ports, and sterile-contact parts should be sourced with backup plans. Buyers should ask which components come from Europe, Asia, or the United States, and how lead times may be affected by freight through Long Beach, Houston, or East Coast ports.
There is also policy risk. In 2026 and beyond, buyers should expect more focus on domestic supply resilience, digital traceability, and sustainability reporting. Equipment that cannot support modern data collection or energy optimization may age quickly.
One practical way to reduce risk is to work with a supplier that can coordinate process equipment, water systems, logistics flow, and validation planning under a unified framework. For companies that want to discuss project scope directly, a supplier contact route such as technical consultation for IV solution projects can be useful early in feasibility.
| Risk Area | Example Problem | Business Impact | Mitigation Approach |
|---|---|---|---|
| Wrong product fit | Line cannot support target formulation design | Lost market opportunity | Define product roadmap before purchase |
| Validation delay | Incomplete IQ/OQ documents | Late commercial launch | Review documentation scope in contract |
| Material mismatch | Film performs poorly in sterilization | High reject rates | Run compatibility trials early |
| Service downtime | Slow technical response | Production interruption | Stock critical spares and define SLA |
| Layout issues | Poor maintenance access or flow design | Higher operating cost | Conduct detailed engineering review |
| Policy and sustainability gap | System lacks energy tracking or traceability | Future compliance pressure | Specify digital and ESG features upfront |
| Underestimated utilities | Insufficient clean steam or WFI capacity | Line underperformance | Integrate utilities with line design |
Case studies across the industry show that the most successful projects are not always the cheapest. They are the ones with realistic qualification timelines, clear URS definitions, reliable material trials, and strong after-sales engagement.
FAQ
What output range is common for an IV bag production line?
Output varies widely by bag size, chamber design, and automation level. Smaller specialty lines may target modest validated output, while standard single-chamber lines can be configured for large commercial volumes.
Is multi-chamber technology worth the extra cost?
It can be, especially if your product strategy depends on separating unstable ingredients, reducing bedside mixing, or offering differentiated clinical products with stronger margins.
What matters most for FDA-oriented projects?
Documentation quality, validation support, software and data integrity, material compatibility, and a supplier that understands sterile manufacturing expectations are all critical.
How long does implementation usually take?
For many U.S. projects, total timing from URS to commercial readiness can range from around 12 to 24 months or longer, depending on customization, facility readiness, FAT/SAT timing, validation scope, and utility work.
Should buyers choose a local U.S. supplier only?
Not necessarily. Many buyers combine local project management and service expectations with global technology sourcing. The better question is whether the supplier can support compliance, spare parts, response time, and full project delivery in the United States.
What future trends matter most for 2026 and beyond?
Expect more interest in digital batch records, predictive maintenance, robotics, energy-efficient line design, non-PVC and sustainable material strategies, and greater resilience in domestic sterile manufacturing supply.
Can one supplier handle the whole plant?
Some can. Integrated engineering companies may support IV bag lines, water systems, clean utilities, conveying, packaging, warehouse logistics, and validation. That can reduce interface risk in larger projects.
How should a first-time investor start?
Begin with market mapping, define target SKUs, build a realistic URS, compare single-chamber and multi-chamber economics, qualify film options, and evaluate suppliers on full lifecycle support rather than purchase price alone.
For the United States market, the best IV bag production line investment is the one that matches your therapeutic focus, plant capability, compliance strategy, and long-term service needs. Whether you are expanding commodity infusion capacity or launching advanced multi-chamber products, careful planning around equipment, materials, utilities, validation, and supplier strength will have a bigger impact than headline speed alone.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
IV Bag Filling Machine Guide for the United States
For pharmaceutical manufacturers in the United States, an IV bag filling machine is a core production asset used to form, fill, seal, and inspect infusion bags for sterile solutions. It supports large-volume parenteral manufacturing, improves dosage consistency, and enables advanced bag formats that can keep sensitive ingredients separate until administration. This is especially valuable for products with stability challenges, combination therapies, nutrition solutions, and hospital-ready sterile infusions. In a market shaped by FDA cGMP expectations, labor pressures, and growing demand for flexible manufacturing, the right machine can improve sterility assurance, reduce waste, raise throughput, and strengthen long-term supply reliability.
Across the United States, demand is expanding in major pharmaceutical corridors such as New Jersey, North Carolina, Illinois, Texas, California, and Massachusetts. Manufacturers supplying hospitals in New York, Chicago, Houston, Los Angeles, and Atlanta are looking for more efficient IV solution lines that support traceability, automated controls, and compliance-ready documentation. Whether a company is planning a greenfield sterile plant near the Port of Houston, upgrading an injectable facility in New Jersey, or evaluating contract manufacturing expansion near Memphis logistics hubs, selecting the right IV bag production system requires careful review of bag type, film compatibility, output targets, validation scope, and supplier capability.
An IV bag filling machine allows pharmaceutical companies to manufacture sterile infusion products with high precision and repeatability. More importantly, advanced configurations can support multi-chamber bag designs that keep active ingredients, electrolytes, or unstable compounds separated until use. That improves shelf stability, simplifies bedside preparation, and reduces medication handling risks in clinical settings. For U.S. manufacturers, these systems also help standardize production, lower contamination risk through closed processes, and support scale-up for hospital, clinic, and emergency care demand.
In practical terms, the machine usually performs several linked operations: film feeding, bag forming, port insertion, sterilizable sealing, volumetric or mass-based filling, leak testing, visual inspection support, and final discharge for downstream overwrapping or sterilization. Depending on the line design, it may also integrate clean utilities, CIP/SIP-compatible product paths, in-line printing, automatic rejects, and data capture for batch records.
FunctionWhat the Machine DoesOperational ValueQuality ImpactBag formingShapes flexible film into the final IV containerCreates consistent dimensionsSupports seal integrity and uniform packagingFillingDispenses sterile liquid at controlled volumeReduces product giveawayImproves dose accuracyPort insertionPlaces administration and additive portsEnables downstream use in hospitalsPrevents fit and leakage issuesSealingThermally seals the bag after fillingSupports line speed and consistencyCritical for sterility assuranceInspectionChecks weight, leaks, and visible defectsReduces rejects reaching packagingStrengthens release confidenceTraceabilityRecords batch and process parametersSupports audits and recalls if neededImportant for FDA complianceThe table above shows why the equipment is more than a filler. It is part of a validated sterile manufacturing system. In the United States, that systems perspective is essential because regulators and customers evaluate not just output, but also control strategy, documentation, and consistency over time.
An IV bag filling machine is specialized pharmaceutical equipment designed for the aseptic or terminally sterilized production of infusion bags. It is commonly used for saline, dextrose, irrigation solutions, parenteral nutrition bases, dialysis-related fluids, and other large-volume sterile liquids. The machine may be configured for non-PVC soft bags, PVC alternatives, multilayer films, or specialty chamber structures.
The main advantages are operational, clinical, and commercial. From an operations standpoint, automated bag filling lines reduce manual intervention, stabilize output, and lower labor dependence. From a product standpoint, they improve fill accuracy, seal consistency, and packaging integrity. From a business standpoint, they help manufacturers meet growing healthcare demand while improving batch reproducibility and cost control.
U.S. producers also value flexibility. A modern line can often be adapted for multiple bag sizes, such as 50 mL, 100 mL, 250 mL, 500 mL, and 1000 mL. That matters for contract manufacturers serving different hospital systems and wholesalers across the country. Facilities near pharmaceutical clusters in Newark, Raleigh-Durham, Indianapolis, and San Diego often look for fast changeover, digital recipe management, and compatibility with existing cleanroom layouts.
AdvantageDescriptionBenefit for U.S. PlantsTypical KPI InfluenceHigher automationLess manual contact during productionSupports sterile manufacturing controlLower labor hours per batchAccurate fillingPrecise liquid dosing systemsHelps reduce overfill and lossBetter fill-weight consistencyStable sealingControlled heat and pressure parametersImproves package reliabilityLower leak rateFormat versatilitySupports different bag volumes and structuresUseful for multi-product plantsShorter launch time for new SKUsIntegrated inspectionWeight, leak, and defect checksReduces quality escapesHigher first-pass yieldData collectionRecords process values and alarmsAssists with cGMP reviewImproved batch traceabilityWhen companies evaluate suppliers, they should examine not only machine speed but also cleaning concept, control software, component brand availability in the United States, and the supplier’s experience with validation. A lower-cost machine without robust documentation may become more expensive once FAT, SAT, IQ, OQ, PQ, and ongoing maintenance are considered.
The downstream impact of high-quality IV bag production is seen directly in hospitals, outpatient infusion centers, military medical systems, emergency care networks, and home infusion programs. Hospitals increasingly prefer ready-to-use sterile solutions that reduce compounding time and lower bedside preparation errors. For certain formulations, multi-chamber bags offer additional value because they allow nurses or pharmacists to activate the solution only when needed.
In U.S. healthcare environments, staffing shortages and medication safety programs are major drivers. Ready-to-use bags can reduce manipulations in the pharmacy cleanroom and help standardize administration protocols. During seasonal surges, natural disasters, or public health emergencies, consistent domestic or regional production capacity becomes especially important.
Common hospital applications include hydration therapy, electrolyte correction, glucose support, irrigation, dilution for injectable drugs, and nutrition-related sterile fluids. Some manufacturers also evaluate specialized bags for critical care or temperature-sensitive preparations. In large procurement markets such as the Northeast and Gulf Coast, hospitals focus not only on price but also on shelf life, supply continuity, and packaging durability during transport.
Application AreaTypical Product UseWhy Bag Quality MattersClinical BenefitEmergency medicineRapid hydration and electrolyte supportFast access and dependable sealsImproves treatment readinessICU and acute careContinuous sterile infusionsPrecise volume and compatibilitySupports patient safetyOncology supportDilution and supportive infusionsLow contamination riskReduces handling complexityHome infusionPortable sterile fluid administrationDurable packaging and longer stabilityImproves convenienceSurgery centersIrrigation and perioperative fluidsReliable sterility and easy storageSupports workflow efficiencyPharmacy outsourcingBatch-prepared ready-to-use solutionsTraceable and standardized productionImproves consistency across sitesThese clinical use cases explain why IV bag manufacturing decisions should not be made solely on machinery speed. The line must produce bags that maintain integrity from the plant to the hospital shelf to the bedside. Transport vibration, warehouse conditions, sterilization exposure, and user handling all matter.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Hospitals’, ‘Outpatient Infusion’, ‘Home Care’, ‘Emergency Stock’, ‘CDMOs’, ‘Government Supply’],datasets: [{label: ‘Estimated U.S. demand index for sterile IV bag output’,data: [96, 74, 58, 81, 69, 63],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});The chart highlights how hospital and emergency stock demand continue to anchor the U.S. market, while outpatient and home-based care are becoming more important secondary channels.
IV bag filling machines are not all built for the same product strategy. Some are optimized for high-volume, standardized single-solution output. Others are designed for more advanced multi-chamber structures, specialized films, and frequent product changes. The right line depends on capacity goals, film characteristics, sterilization method, and target market.
Single-lane systems are suitable for lower to medium capacity or pilot-to-commercial transitions. Multi-lane lines are used when manufacturers need higher throughput and more efficient footprint utilization. Form-fill-seal platforms can create bags directly from roll film, while some operations handle preformed bags for specific production models.
Film choice is equally critical. In the United States, buyers often seek non-PVC or low-extractable film options because of product compatibility, environmental positioning, and customer preferences. Multilayer films may improve barrier performance, durability, and sterilization tolerance, but they must be validated with the intended formulation.
Machine TypeBest Use CaseTypical StrengthPotential LimitationSingle-lane form-fill-sealModerate output and flexible product mixLower complexityLess total capacityMulti-lane form-fill-sealLarge commercial productionHigher throughputMore complex maintenancePreformed bag filling linePlants using external bag supplyFast product introductionDependent on bag supplier qualityMulti-chamber bag lineStability-sensitive formulationsSupports separated ingredientsHigher investment costPilot or R&D lineDevelopment and scale-up studiesUseful for validation trialsLower commercial outputIntegrated turnkey lineNew sterile factoriesBetter system coordinationLonger project planning phaseFilm Material OptionKey PropertySuitabilityImportant Review PointNon-PVC multilayer filmGood flexibility and compatibilityCommon for modern soft bagsSeal strength validationPVC-based filmEstablished historical useSome legacy applicationsExtractables and policy preferencesPP-compatible structureHeat resistanceSpecific product designsForming behaviorEVA-containing filmSoftness and clarityCertain infusion productsDrug compatibility testingCo-extruded barrier filmEnhanced oxygen/moisture barrierSensitive formulationsCost and sourcing consistencyCustom specialty laminateTailored performanceAdvanced or niche productsLead time and qualificationThe tables show that material and equipment decisions are linked. A machine with excellent speed but weak film adaptability may not serve a product pipeline well. For companies building new capacity, it is wise to test film, ports, sealing windows, and sterilization outcomes together rather than as isolated purchasing decisions.
Multi-chamber IV bag filling machine systems are designed to produce bags with two or more isolated compartments separated by peelable or breakable seals. This allows active ingredients to remain apart until the point of use. Single-chamber bags, by contrast, hold one mixed solution in a single space and are generally simpler to manufacture.
The choice depends on formulation stability, clinical workflow, and investment strategy. Multi-chamber systems often make sense for products that degrade after mixing, require bedside activation, or need extended shelf life before final combination. Single-chamber production remains highly efficient for standard saline, dextrose, and many established infusion products.
Comparison PointMulti-Chamber BagsSingle-Chamber BagsImplication for BuyersFormulation stabilityExcellent for separated ingredientsLimited if premixed stability is shortChoose based on product chemistryMachine complexityHigherLowerAffects maintenance and validationCapital costHigher initial investmentMore economical to startImportant for budget planningClinical convenienceActivation before use can simplify storageImmediate use if already premixedDepends on hospital workflowProduction speedOften lower for comparable line sizeTypically higherReview total annual demandProduct differentiationStronger market positioningMore commoditizedUseful for premium portfoliosvar ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Stability Benefit’, ‘Capex Efficiency’, ‘Line Complexity’, ‘Product Differentiation’, ‘Throughput Potential’, ‘Hospital Convenience’],datasets: [{label: ‘Multi-chamber’,data: [95, 52, 82, 91, 68, 84],backgroundColor: ‘#7b61ff’},{label: ‘Single-chamber’,data: [63, 86, 48, 58, 88, 79],backgroundColor: ‘#2ca02c’}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 100 } }}});For many U.S. manufacturers, the decision is strategic rather than purely technical. A company competing in high-volume commodity fluids may prioritize single-chamber speed and lower cost. A company targeting specialty sterile products may view multi-chamber capability as a way to defend margin and create differentiation.
The U.S. market for sterile infusion packaging equipment is influenced by healthcare utilization, domestic supply resilience efforts, outsourcing growth, and replacement of aging production lines. Drug shortage concerns have increased interest in modernized IV solution infrastructure, especially for plants serving hospitals, government programs, and regional emergency stockpiles.
There is also a broader shift toward automation, electronic batch recording support, energy efficiency, and lines designed for easier cleaning and faster validation. Buyers now ask more questions about SCADA integration, audit trail capability, remote diagnostics, spare part availability in North America, and the supplier’s installed base.
In logistics terms, the United States remains highly regional. Companies near the Port of New York and New Jersey may prioritize East Coast distribution; Gulf Coast operators may leverage Houston and New Orleans access; Midwest plants often value rail and interstate reach through Chicago and Indianapolis; West Coast facilities may support Pacific routes through Los Angeles and Long Beach. Machine capacity planning should match these distribution realities.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. demand index for IV bag filling machine capacity’,data: [72, 76, 83, 89, 96, 104],borderColor: ‘#1f77b4’,backgroundColor: ‘rgba(31,119,180,0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: false } }}});var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Shift toward advanced automation and multi-chamber capable lines’,data: [28, 34, 41, 49, 58, 68],borderColor: ‘#ff7f0e’,backgroundColor: ‘rgba(255,127,14,0.25)’,fill: true,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: { legend: { display: true } },scales: { y: { beginAtZero: true, max: 80 } }}});The charts suggest steady growth, with 2026 likely defined by three trends: stronger automation, greater resilience planning, and broader interest in advanced bag structures. Policy and procurement trends may also favor systems that support domestic or near-market supply continuity, lower material waste, and better documentation for regulated production.
Sustainability is another emerging factor. Buyers increasingly review film utilization efficiency, utility consumption, and machine design that reduces scrap. While sterile manufacturing will always require strict controls, better engineering can still improve energy use, changeover efficiency, and material yield.
Choosing a supplier is as important as choosing the machine itself. In the United States, buyers should compare regulatory understanding, real project execution history, technical depth, documentation quality, and after-sales responsiveness. A machine may perform well during a demonstration, but long-term value depends on validation support, spare parts access, and the supplier’s ability to troubleshoot under production pressure.
Start with five filters: compliance capability, engineering depth, manufacturing quality, service coverage, and commercial transparency. Ask for installed references, FAT protocols, software architecture, material compatibility data, and examples of IQ/OQ documentation. Review whether the supplier can coordinate with local utilities, cleanroom contractors, automation teams, and packaging partners.
From a technological capabilities perspective, buyers should seek suppliers with proven expertise in sterile liquid handling, filling accuracy control, sealing technology, leak prevention, multi-format changeover, and integrated automation. A company such as IVEN Pharmatech Engineering is often evaluated in this context because it combines pharmaceutical equipment know-how with broader engineering experience and has built solutions aligned with international GMP expectations, including U.S. compliance needs.
From a manufacturing capabilities perspective, it is important to assess whether the supplier has dedicated production infrastructure, stable component sourcing, and experience producing not only standalone machines but also coordinated line equipment. Manufacturers that operate specialized plants for filling and packaging, water systems, conveying, and related pharmaceutical equipment can often manage interfaces more effectively, especially in turnkey or semi-turnkey projects.
From a service capabilities perspective, buyers should confirm project management structure, installation support, commissioning plans, training, validation document delivery, and long-term service response. Suppliers that can support feasibility review, engineering design, equipment customization, SAT, IQ/OQ/PQ support, and staff training usually reduce project risk for U.S. investors.
Supplier Evaluation FactorWhat to AskWhy It MattersWarning SignRegulatory understandingCan they support FDA-aligned documentation?Reduces compliance gapsGeneric or incomplete documentsInstalled baseDo they have relevant IV line references?Shows practical experienceNo similar projectsFactory testingIs FAT detailed and data-driven?Finds issues before shipmentDemo-only acceptanceEngineering flexibilityCan they adapt to your layout and utilities?Improves project fitOne-size-fits-all designAfter-sales serviceWhat is the spare parts and response model?Protects uptimeSlow or unclear support pathTotal project scopeCan they coordinate related systems?Reduces interface riskMachine sold without integration planningIf you are comparing options for a new sterile plant or line upgrade, it is useful to review integrated project support rather than only equipment pricing. For example, companies exploring broader facility development can assess turnkey pharmaceutical engineering solutions alongside core filling line requirements.
Investment cost varies widely depending on capacity, chamber design, automation level, inspection integration, utility requirements, and validation scope. A basic line for standard bag output may be far less expensive than a fully integrated multi-chamber system with advanced controls, isolatable product paths, and extensive digital traceability. For U.S. projects, logistics, installation, local electrical adaptation, cleanroom modifications, and commissioning support can materially affect the total budget.
Budget planning should include much more than machine price. Decision-makers should estimate facility preparation, purified water and WFI interface needs, HVAC impact, compressed air quality, sterilization strategy, qualification costs, operator training, initial spare parts, and annual maintenance. The real measure is total cost of ownership over five to ten years.
Cost ElementTypical Share of Total ProjectWhy It Is ImportantCommon OversightMain machine and accessories35% to 50%Core production assetIgnoring format kits and optionsUtilities and integration10% to 18%Ensures stable operationUnderestimating clean utility tie-insInstallation and commissioning8% to 15%Turns equipment into a working lineWeak site readiness planningValidation and documentation6% to 12%Required for regulated productionLate document requestsTraining and startup support3% to 7%Improves operator performanceInsufficient shift coverageSpare parts and service reserve4% to 8%Protects uptime in early yearsBuying no startup inventoryROI depends on output volume, product margin, labor savings, scrap reduction, and the ability to capture new business. A line that supports one additional contract with a major hospital distributor may justify a higher upfront investment. Likewise, a machine that reduces leak-related rejects and overfill can create significant recurring savings.
For example, if a U.S. manufacturer replaces a semi-automated process with an advanced IV bag filling machine, the return may come from four areas: more saleable units per shift, reduced labor per thousand bags, fewer rejected bags after sterilization, and improved service level to customers. Specialty multi-chamber products can improve ROI further if they command better pricing or reduce competition.
Companies reviewing equipment portfolios can compare sterile production solutions through a supplier’s product catalog and equipment range, then refine budgets based on required speed, bag size, and compliance package.
The biggest investment mistakes usually come from incomplete scope definition. Buyers may focus on line speed while overlooking formulation sensitivity, film qualification, operator skill level, or the need for future expansion. In the United States, project delays can also result from permitting, utility upgrades, cleanroom bottlenecks, or insufficient coordination between equipment suppliers and local contractors.
Another risk is assuming that all compliant-looking documentation is equally useful. Validation packages differ widely in quality. Buyers should verify document structure early, including URS alignment, design review support, FAT/SAT coverage, component traceability, instrument calibration records, and software backup procedures.
Supply chain resilience matters too. Replacement parts should be accessible, and critical components should have acceptable lead times. If a plant in Ohio or California loses a key sealing component and waits weeks for shipment, production risk rises quickly. It is smart to identify long-lead wear parts and maintain a strategic inventory.
Risk AreaPotential ProblemImpactMitigation StrategyFilm incompatibilityWeak seals or product interactionBatch failurePerform full material qualificationUnderestimated validation scopeDelayed commercial releaseProject overrunDefine documentation earlyInsufficient service supportLong downtime during faultsRevenue lossSecure service terms and spare stockLayout mismatchPoor material and personnel flowOperational inefficiencyConduct detailed engineering reviewCapacity miscalculationLine too small or oversizedWeak ROIModel demand scenarios carefullyRegulatory gapsAudit observations or remediationCompliance riskChoose experienced, GMP-aware suppliersInvestors should also consider 2026 trends. These include more digital maintenance tools, broader adoption of data-driven quality monitoring, stronger sustainability pressure on packaging and utility use, and potential policy incentives tied to supply chain resilience. Equipment chosen today should remain viable under tomorrow’s expectations.
What production capacities are common for an IV bag filling machine?Capacities vary by bag size, machine configuration, and chamber design. High-output lines for standard single-chamber products can run much faster than specialty multi-chamber systems. Buyers should compare annual saleable output, not just nameplate speed.
Can one machine handle multiple bag volumes?Yes, many modern systems can support multiple volumes using format parts and recipe control. However, changeover time, operator training, and validation scope should be reviewed before assuming full flexibility.
Are non-PVC bags preferred in the United States?Many buyers favor non-PVC or alternative film structures for compatibility, sustainability positioning, and customer preference reasons. The best choice depends on the formulation, sterilization method, and commercial strategy.
When is a multi-chamber bag worth the extra cost?It is often worth the added investment when product stability improves significantly by keeping ingredients separate, when hospital workflow benefits from point-of-use activation, or when the product can command stronger market differentiation.
How long does a typical project take?Timelines depend on complexity. A straightforward line addition may move faster than a greenfield sterile facility. Engineering review, fabrication, FAT, shipping, installation, SAT, and qualification all need to be planned in sequence.
What should U.S. buyers ask during FAT?They should review filling accuracy, sealing consistency, alarm logic, control access levels, recipe management, reject handling, documentation completeness, and material-specific test results. It is better to resolve issues before shipment.
Why do some buyers prefer integrated engineering partners?Because sterile projects involve more than one machine. Water systems, solution preparation, logistics, packaging, layout design, and validation must work together. Integrated support often lowers interface risk and helps schedule control.
Where can I discuss a customized project requirement?For project consultation, layout review, or supplier communication, you can reach out through the contact page for IVEN Pharmatech Engineering to discuss line capacity, film type, chamber design, and compliance expectations for the United States market.
In summary, the best IV bag filling machine for the United States market is not simply the fastest or cheapest option. It is the one that aligns with your formulation needs, plant strategy, compliance roadmap, and long-term service requirements. Buyers that evaluate technology, manufacturing strength, and lifecycle support together are more likely to secure stable production, sound ROI, and dependable market supply.
-
U.S. Vial Filling Production Line Buying Guide
For pharmaceutical manufacturers in the United States, a vial filling production line is a core aseptic manufacturing system used to wash, sterilize, fill, stop, and cap vials under tightly controlled conditions. It is commonly evaluated when companies expand sterile injectable capacity, launch biologics, modernize legacy facilities, or build compliant operations that must meet FDA cGMP, data integrity, contamination control, and high-throughput production goals.
In the U.S. market, interest in vial filling systems is especially strong in established pharmaceutical corridors such as New Jersey, Pennsylvania, Massachusetts, North Carolina, Texas, and California. Companies operating near logistics centers like the Port of Los Angeles, Port of New York and New Jersey, Houston, Chicago, and Atlanta often prioritize not only machine performance, but also validation support, spare parts planning, clean utility integration, and lifecycle service. As a result, selecting the right line is not just an equipment purchase. It is a strategic manufacturing decision linked to regulatory readiness, product quality, staffing efficiency, and long-term return on investment.
A vial filling production line is a specialized automated system for sterile liquid drug manufacturing. In most U.S. pharmaceutical plants, it handles a sequence that may include vial infeed, washing, depyrogenation tunnel transfer, aseptic filling, stopper insertion, capping, inspection interface, and downstream packaging connectivity. These lines are used for injectables such as antibiotics, oncology drugs, vaccines, biologics, lyophilized products, and other high-value sterile formulations.
Large pharmaceutical and medical device companies evaluate these lines when they need to:
For buyers in the United States, the strongest value often comes from choosing a line that balances compliance, flexibility, throughput, and serviceability. This means the best system is not always the fastest one; it is the one that fits the product portfolio, plant utilities, available space, staffing model, and validation strategy.
A vial filling production line is a coordinated set of machines and control systems designed to prepare sterile containers and accurately fill them with pharmaceutical product under aseptic conditions. Depending on plant design, the line may include upstream utility systems, cleanroom interfaces, environmental controls, robotics, automatic reject systems, weight checking, and electronic batch recording.
In a typical U.S. injectable facility, the process flow may look like this:
This equipment is used across branded pharma, generic injectables, CDMOs, biotech startups, hospital supply manufacturers, and government-facing production programs. In areas such as Boston, Raleigh-Durham, Indianapolis, and the greater New York region, new sterile manufacturing investments are often focused on flexible systems that can support both clinical and commercial scales.
Line StageMain FunctionTypical U.S. RequirementCommon Risk ControlledOptional UpgradeBusiness BenefitVial washingRemove particulates and residuesValidated cleaning cycleContainer contaminationRecipe managementMore consistent preparationDepyrogenationSterilize and dry vialsTemperature mappingEndotoxin carryoverEnergy recovery designLower utility costAseptic fillingMeter exact liquid volumeFilling accuracy validationUnderfill or overfill100% in-process weight checkHigher yieldStopperingProtect sterile productSterile parts pathSeal integrity issuesRobotic parts handlingLess manual interventionCappingSecure closureTorque consistencyCap defectsVision inspectionFewer rejectsData captureRecord process values21 CFR Part 11 readinessData integrity gapsMES integrationFaster review and releaseThe table above shows why buyers should view a vial filling line as a complete validated process rather than a single filler machine. Every stage contributes to sterility assurance, container closure integrity, and release quality.
Modern vial filling lines are used for a broad range of sterile products. In the United States, their applications continue to expand because injectable therapies remain central in hospitals, specialty clinics, oncology centers, emergency medicine, and biologics distribution networks.
Main applications include:
Benefits typically include better dose accuracy, lower contamination risk, stronger batch reproducibility, reduced operator dependence, and easier scale-up. For U.S. plants facing labor shortages and tighter inspection expectations, automation also improves operational resilience.
ApplicationTypical Fill RangeLine PriorityWhy It Matters in the U.S.Recommended ConfigurationExpected BenefitGeneric injectables2 mL to 50 mLHigh throughputCost pressure and volume demandRotary filling with automationLower unit costBiologics1 mL to 20 mLGentle handlingProduct sensitivityPeristaltic pump with isolatorBetter product integrityVaccines1 mL to 10 mLSterility assurancePublic health requirementsRABS or isolator lineReduced contamination riskLyophilized drugs2 mL to 30 mLPartial stopperingComplex process integrationFilling line linked to lyophilizerEfficient transferClinical batchesSmall batchesFlexibilityFast development timelinesModular lineQuicker campaign changeoverCDMO multi-product plantsMixed sizesFast change partsContract scheduling complexityRecipe-driven line controlsHigher asset utilizationThe above table highlights that the right configuration depends heavily on product category. A vaccine line and a generic injectable line may both fill vials, but their priorities are different: one focuses more on contamination control and product sensitivity, while the other may emphasize speed and operating cost.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chartBar = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Generic Injectables’, ‘Biologics’, ‘Vaccines’, ‘Oncology’, ‘CDMO Services’, ‘Clinical Production’],datasets: [{label: ‘Estimated U.S. Demand Index’,data: [82, 91, 76, 88, 84, 63],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: { display: true }},scales: {y: { beginAtZero: true, max: 100 }}}});This demand comparison shows that biologics, oncology, and CDMO-driven manufacturing are some of the strongest drivers for vial filling investment in the U.S. market. These segments favor highly controlled, flexible production lines.
There is no single best vial filling production line for every manufacturer. U.S. buyers generally compare systems based on speed, sterility concept, batch size, container format, and integration requirements.
Common types include:
Key technical options often evaluated by procurement and engineering teams include nitrogen purging, no-vial-no-fill logic, CIP/SIP capability, in-line weight checking, machine vision inspection, robotic tub handling for nested formats, and digital recipe management.
Line TypeBest ForSpeed RangeCleanroom ApproachStrengthLimitationLinear lineFlexible multi-product plantsLow to mediumOpen RABS or isolatorEasy format changeLower top speedRotary lineLarge commercial outputMedium to highRABS or isolatorHigh efficiencyMore complex changeoverMonoblock systemSpace-constrained facilitiesMediumCompact aseptic zoneSmaller footprintLess modularityIsolator lineHigh-value sterile productsLow to highClosed barrierBest contamination controlHigher initial costRABS lineBalanced compliance and accessMedium to highRestricted access barrierGood operational flexibilityMore operator discipline neededLyophilization-ready lineFreeze-dried productsLow to mediumTransfer to lyophilizerProcess compatibilityBroader project scopeThe table makes clear that the right model depends on business reality. A startup in Cambridge or San Diego developing a biologic may prefer an isolator-based, lower-speed flexible system. A high-volume generic plant in New Jersey may favor a faster rotary line optimized for campaign production.
Not every sterile product should be filled on a traditional vial line. U.S. manufacturers frequently compare vial lines with ampoule lines, prefilled syringe systems, BFS technology, and outsourced fill-finish services.
Vials remain attractive because they support a wide product range, work well with both liquid and lyophilized dosage forms, and fit established hospital and distribution workflows. They also offer relatively broad compatibility with development-to-commercial scale strategies. However, alternatives may outperform vials in some use cases.
TechnologyBest Use CaseCapital IntensityFlexibilityRegulatory ComplexityStrategic NoteVial filling lineInjectables and biologicsMedium to highHighHighMost versatile for sterile drugsPrefilled syringe lineReady-to-use administrationHighMediumHighStrong for convenience productsAmpoule lineSealed glass dose unitsMediumLowerModerateLess common for some modern biologicsBFS systemHigh-volume aseptic packagingHighLow to mediumHighEfficient for selected productsCDMO outsourcingLow initial volumeLow upfrontHigh initiallySharedGood for market entryManual or semi-auto fillingR&D or very small batchesLowMediumHigh operational burdenNot ideal for scaleIf your U.S. operation expects multiple SKUs, lyophilization, or both clinical and commercial production, vial filling often remains the best fit. If patient convenience and self-administration are the top priorities, prefilled syringes may deserve stronger consideration. Buyers should compare product strategy before they compare equipment speed.
var ctxComp = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var chartComp = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Flexibility’, ‘Throughput’, ‘CAPEX Efficiency’, ‘Lyophilization Fit’, ‘Multi-SKU Support’, ‘Upgrade Potential’],datasets: [{label: ‘Vial Filling Line Score’,data: [91, 85, 78, 93, 89, 87],backgroundColor: ‘#8e63ce’},{label: ‘Alternative Average Score’,data: [74, 81, 71, 62, 68, 73],backgroundColor: ‘#c7b0e3’}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: { display: true }},scales: {y: { beginAtZero: true, max: 100 }}}});This comparison indicates why vial-based fill-finish remains a preferred platform in many U.S. sterile manufacturing strategies: strong flexibility, good compatibility with lyophilized products, and solid support for multi-SKU production planning.
The U.S. market for vial filling production lines is supported by continued investment in sterile injectables, biologics, vaccine readiness, and domestic supply chain resilience. Expansion projects are active in both large pharma hubs and emerging biotech regions. Buyers are also responding to aging installed equipment, the need for modernization, and pressure to reduce operator interventions in aseptic areas.
Several market drivers stand out:
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var chartLine = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. Market Growth Index’,data: [100, 108, 117, 128, 139, 151],borderColor: ‘#2a9d8f’,backgroundColor: ‘rgba(42,157,143,0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: { display: true }},scales: {y: { beginAtZero: false }}}});The growth trend above reflects steady U.S. investment momentum. Growth is not limited to mega-sites; mid-sized plants and CDMOs are also expanding capacity, especially where clients need redundancy and rapid launch support.
var ctxArea = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var chartArea = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Traditional Open Access Systems’,data: [48, 43, 37, 31, 26, 21],fill: true,backgroundColor: ‘rgba(231,111,81,0.25)’,borderColor: ‘#e76f51’,tension: 0.3},{label: ‘RABS and Isolator-Based Systems’,data: [52, 57, 63, 69, 74, 79],fill: true,backgroundColor: ‘rgba(38,70,83,0.20)’,borderColor: ‘#264653’,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false,plugins: {legend: { display: true }},scales: {y: { beginAtZero: true, max: 100 }}}});The area chart shows a clear shift toward barrier technologies. By 2026, the U.S. market is expected to favor RABS and isolator-based installations even more strongly as manufacturers respond to contamination control expectations, labor optimization, and high-value product protection.
Future trends through 2026 include:
In the United States, supplier selection should go beyond machine brochures. Buyers should assess technical depth, regulatory understanding, after-sales capability, project execution discipline, and the supplier’s ability to support qualification and documentation.
Important evaluation criteria include:
Some U.S. buyers prefer a supplier that can also support broader facility planning. That approach often reduces project interface risk, especially when the project includes WFI, clean steam, solution preparation, logistics, and packaging integration. Companies looking for that model may review turnkey pharmaceutical engineering solutions rather than only buying standalone machinery.
From a technological capability perspective, IVEN Pharmatech Engineering has built its reputation around integrated pharmaceutical systems rather than isolated equipment only. Its portfolio includes sterile filling and packaging machinery, water treatment systems, solution preparation and distribution systems, and intelligent logistics platforms. For U.S. buyers, that breadth is useful because a vial filling line rarely succeeds in isolation; it depends on upstream clean utilities, validated process design, and downstream material flow.
From a manufacturing capability perspective, the company operates multiple specialized production plants in Shanghai focused on different categories of pharmaceutical and medical device equipment. This structure supports customization, component specialization, and production coordination across filling, water systems, logistics, and medical consumable equipment. Buyers wanting to review the broader corporate background can visit the company overview page to understand its manufacturing base and project scope.
From a service capability perspective, many U.S. project teams value lifecycle support just as much as equipment design. IVEN emphasizes feasibility consultation, engineering design, equipment selection, installation, commissioning, validation documentation support, training, and after-sales optimization. For regulated sterile projects, that service layer can help reduce schedule risk and improve startup readiness.
Supplier CheckpointWhat to AskWhy It MattersWarning SignPreferred EvidenceImpact on ProjectRegulatory competenceCan you support FDA-style documentation?Speeds compliance readinessVague validation answersSample protocols and URS traceabilityLower audit riskAseptic designHow is intervention minimized?Protects sterility assuranceToo much manual accessIntervention study recordsBetter contamination controlCustomization abilityCan the line fit our vial sizes and products?Prevents mismatchOne-size-fits-all proposalLayout drawings and change part plansSmoother startupProject executionWho manages interfaces?Reduces delay riskUnclear responsibilitiesProject schedule and RACI chartMore predictable deliveryAfter-sales supportHow are U.S. service issues handled?Limits downtimeSlow response modelService SLA or support structureHigher equipment uptimeInstalled experienceDo you have regulated market references?Shows practical capabilityNo comparable projectsCase studies and acceptance historyMore buyer confidenceThe best suppliers are transparent about project limits, qualification responsibilities, and integration interfaces. If you need a quotation, technical discussion, or feasibility review for a U.S. project, a direct inquiry through the contact page is often the fastest way to compare configurations.
The cost of a vial filling production line in the United States can vary widely based on speed, barrier technology, level of automation, utility scope, and validation requirements. Buyers should budget not only for the machine itself, but also for facility modifications, cleanroom work, utilities, engineering, shipping, commissioning, training, and spare parts.
Major cost categories include:
Budget ItemLow Complexity LineMid Complexity LineHigh Complexity LineTypical U.S. ConsiderationROI EffectCore equipment$1.2M-$2.0M$2.0M-$4.5M$4.5M-$8.0M+Depends on speed and dosing systemMain capital driverBarrier technology$0.3M-$0.8M$0.8M-$1.8M$1.8M-$3.5M+Isolators cost more than RABSImproves risk profileUtilities and integration$0.4M-$1.0M$1.0M-$2.5M$2.5M-$5.0M+Site-specific clean utility needsAffects startup speedValidation package$0.1M-$0.3M$0.3M-$0.7M$0.7M-$1.5M+Documentation depth mattersReduces compliance delayFacility modification$0.5M-$1.5M$1.5M-$4.0M$4.0M-$10M+Can exceed machine costCritical but often underestimatedTraining and startup spares$0.05M-$0.2M$0.2M-$0.5M$0.5M-$1.0MImportant for early uptimeImproves ramp-up performanceThe table above shows why early budget planning is essential. A vial filling line project is often a total-facility investment rather than just a purchase order for equipment. In many U.S. cases, the cost of modifying the sterile suite, utilities, and material flow can equal or exceed the cost of the line itself.
ROI is usually driven by one or more of the following:
A high-value biologic line can often justify faster payback even with lower throughput because product value per vial is high. By contrast, commodity injectable lines usually rely on operational efficiency and large volume output to achieve acceptable returns.
Investment risk is manageable, but only when identified early. The most common mistake in the U.S. market is underestimating the interface between equipment, facility design, qualification, and production planning.
Main considerations include:
Potential risks include poor line layout, insufficient environmental control, incomplete FAT criteria, weak change part design, utility mismatches, and overly optimistic startup schedules. U.S. facilities in regions with high construction demand such as Boston, New Jersey, and the Bay Area may also face project timing pressure from labor availability and contractor scheduling.
Another important risk factor is selecting a machine that works for today’s product but not tomorrow’s pipeline. A line sized only for current demand may become a constraint when a second shift or new SKU is added. Conversely, oversizing the line can create avoidable capital burden and inefficient campaign planning.
For buyers comparing options, browsing available equipment categories through a supplier’s product catalog can help identify whether the vendor supports only one machine type or a broader integrated solution set. That difference matters when the project includes utilities, preparation systems, or packaging interfaces.
What throughput should a U.S. pharmaceutical company target?It depends on product demand, batch size, shift pattern, and changeover frequency. A lower-speed flexible line may outperform a high-speed line if your portfolio includes many SKUs and short campaigns.
Should we choose an isolator or RABS?Isolators generally provide stronger separation and lower intervention risk, while RABS can offer easier access and lower capital cost. The right choice depends on contamination control strategy, staffing, and product risk.
Can a vial filling line support lyophilized products?Yes, but the line must be designed for partial stoppering and transfer to the freeze dryer. Integration details should be defined early in the project.
How long does a typical project take?For a regulated U.S. installation, total project duration can range from around 12 to 24 months or more, depending on customization, facility work, FAT/SAT planning, and qualification scope.
What documents should we request from suppliers?Request URS response, P&ID where relevant, layout drawings, component lists, material certificates, FAT protocol samples, software documentation expectations, and qualification support scope.
Is a turnkey approach better than buying separate machines?For many sterile projects, yes. Turnkey coordination can reduce interface risk between equipment, utilities, layout, and validation. It is especially helpful for new facilities or major expansions.
How important is U.S. service support?Very important. Sterile lines are critical assets, and downtime is expensive. Buyers should define spare parts strategy, remote support methods, and escalation paths before contract award.
What makes IVEN relevant for U.S. buyers?IVEN is known for integrated pharmaceutical engineering, customized line design, and experience with regulated production requirements. Its strengths are especially relevant for companies seeking more than a single machine and looking for broader project coordination.
Will sustainability matter more by 2026?Yes. U.S. projects are increasingly evaluating energy use, heat recovery, digital monitoring, lower-intervention barrier systems, and utility optimization as part of total cost of ownership.
How do we start supplier comparison efficiently?Prepare a clear URS covering product type, vial sizes, speed targets, cleanroom concept, validation expectations, and future expansion needs. Then request technical proposals from qualified suppliers and compare total lifecycle fit, not just purchase price.
For U.S. manufacturers planning expansion, modernization, or a new sterile facility, a vial filling production line remains one of the most strategic investments in injectable manufacturing. The best outcomes come from aligning product needs, facility design, compliance goals, and supplier capability from the earliest planning stage. Whether the project is in New Jersey, Chicago, Houston, Philadelphia, Boston, or Los Angeles, the same principle applies: choose a line that supports validated performance over many years, not simply the lowest upfront price.
-
United States Guide to Blow-Fill-Seal Pharma Lines
In sterile pharmaceutical manufacturing, blow-fill-seal technology is widely preferred because it forms the container, fills the product, and seals the package in one enclosed aseptic sequence. For manufacturers in the United States, that means fewer human interventions, lower contamination exposure, faster output, and a practical route to consistent quality for unit-dose and multidose liquid products.
For U.S. drug makers expanding in New Jersey, Boston, Chicago, Houston, Raleigh-Durham, and Southern California, blow-fill-seal systems are increasingly evaluated not only as packaging equipment, but as a complete sterile production strategy. They matter most where contamination control, labor efficiency, validation discipline, and supply continuity are central to commercial success. In this guide, you will find how the technology works, where it fits best, how it compares with vial and ampoule lines, what budgets typically look like, and how to assess a supplier for long-term performance in the United States market.
Blow-fill-seal, often shortened to BFS, is an advanced aseptic packaging process used mainly for sterile liquids. A plastic container is formed from polymer resin, immediately filled with sterile product, and then hermetically sealed inside the same machine cycle. Because the package is created and closed without being transported through multiple open handling stages, contamination opportunities are reduced dramatically compared with many traditional filling approaches.
U.S. manufacturers choose BFS when they need dependable high-volume production of ophthalmic solutions, inhalation products, saline, respiratory therapies, unit-dose liquids, and some biologic-supporting applications. The strongest advantages are process integration, reduced operator dependence, compact line flow, and strong economics for certain product formats. This is why BFS is now part of capacity planning discussions from East Coast sterile hubs near the Port of New York and New Jersey to Gulf Coast distribution corridors serving Houston and beyond.
Key FactorBlow-Fill-Seal ImpactWhy It Matters in the United StatesContainer formingDone inside the machineReduces dependence on external container supply chainsAseptic controlIntegrated process pathSupports contamination control and audit readinessLabor requirementLower manual handlingUseful where skilled labor costs are highThroughputHigh-speed continuous cyclesHelps meet large commercial demandPackaging formatFlexible for plastic unit dosesFits respiratory and ophthalmic marketsOperating efficiencyFewer transfer pointsImproves line simplicity and maintenance planningThe table above summarizes the business case at a high level. BFS is not ideal for every sterile product, but when the dosage form, volume range, polymer compatibility, and market forecast align, it can be one of the most efficient sterile packaging investments available.
BFS technology uses thermoplastic resin, commonly polyethylene or polypropylene, to create a container directly on the machine. The resin is melted and extruded into a parison. A mold closes around the parison and compressed sterile air shapes it into the desired bottle or ampoule-like container. Once formed, sterile filling nozzles enter the open container and deliver the product. The top is then sealed before the finished unit exits the machine.
The process is continuous and enclosed, which is one reason BFS is often associated with advanced aseptic manufacturing. Although media fills, environmental controls, sterilization strategy, filter integrity, and validation requirements still remain critical, the design inherently reduces open exposure versus systems that depend on separately supplied containers moving through multiple stations.
From a technical perspective, a well-designed BFS line includes resin handling, extrusion, mold systems, sterile air management, product filling, sealing, reject management, leak testing options, process controls, and in many cases downstream inspection and secondary packaging integration. For companies considering large-scale U.S. deployment, compatibility with plant utilities, HVAC strategy, cleanroom zoning, and data integrity architecture should be evaluated at the same time.
Process StepWhat HappensMain Control PointResin feedingPolymer enters extrusion systemMaterial quality and traceabilityExtrusionMolten parison is formedTemperature and melt consistencyBlowingContainer shape is created in moldAir pressure and mold accuracyFillingSterile liquid is dosed into the containerFill precision and aseptic integritySealingContainer top is fused shutSeal strength and closure designDischargeFinished units move out for inspectionReject control and visual qualityThis workflow explains why BFS is often viewed as a platform rather than a single machine. Suppliers with stronger technological depth can provide not only the core filling block but also integrated water systems, solution preparation, sterile utility design, logistics interfaces, and validation support. For example, IVEN Pharmatech Engineering positions its capabilities around pharmaceutical process integration, with experience in filling machinery, pharmaceutical water systems, intelligent conveying, and full factory engineering. That combination matters when a BFS project must fit within wider sterile manufacturing architecture rather than operate as a standalone purchase.
Manufacturers do not adopt BFS simply because it is modern. They adopt it because it can solve recurring operational problems. The most common drivers are contamination reduction, lower total handling, reliable high-volume output, and lower packaging component complexity. BFS also supports unit-dose convenience, which remains important across ophthalmic products, inhalation therapy, and hospital-use sterile liquids.
In the United States, labor and compliance costs are high enough that process simplification has direct financial value. Every reduced intervention can lower deviation risk, training burden, gowning complexity, and line stoppage probability. When paired with robust maintenance planning, BFS can help stabilize production in facilities that serve national wholesalers, hospital systems, or retail pharmacy networks.
There are also supply-chain benefits. Traditional sterile lines often depend on glass vials, rubber stoppers, seals, trays, and multiple preparation steps. BFS, while still demanding strong resin and utility management, consolidates the packaging path. This can be attractive to plants operating near logistics hubs such as Savannah, Long Beach, or Chicago, where inbound coordination and lead-time variability affect working capital.
Reason for AdoptionOperational BenefitCommercial ResultReduced human interventionFewer contamination opportunitiesBetter batch reliabilitySingle-step container creationLess component handlingLower packaging complexityHigh-speed productionMore units per shiftImproved output economicsUnit-dose suitabilityConvenient patient useStronger product differentiationCompact process flowSimpler line layoutMore efficient plant space useAutomation compatibilityBetter data and control integrationImproved compliance managementThe table shows why BFS is especially compelling for products with stable demand and well-defined fill volumes. It is less about replacing every sterile line and more about choosing the right platform for the right dosage form.
var ctxLine = document.getElementById(‘lineChart’).getContext(‘2d’);var lineChart = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’],datasets: [{label: ‘Estimated U.S. BFS Market Index’,data: [100, 108, 117, 129, 141, 156, 172, 189],borderColor: ‘rgb(54, 162, 235)’,backgroundColor: ‘rgba(54, 162, 235, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart illustrates a realistic market growth trajectory for BFS investment in the United States. Expansion is being pushed by respiratory care demand, reshoring of sterile manufacturing, and greater interest in efficient single-dose packaging.
BFS machines are not all the same. Their differences usually relate to container size range, mold design, output speed, product viscosity, and whether the line is intended for unit-dose or larger bottle formats. Some systems are optimized for small-volume respiratory and ophthalmic products, while others focus on infusion-related solutions or specialty liquid applications.
Typical application industries include pharmaceutical injectables, inhalation therapy, ophthalmology, hospital care products, veterinary liquids, and certain medical consumables. Product designers should evaluate not only fill volume but also oxygen sensitivity, light protection requirements, extractables and leachables considerations, shipping conditions, and end-user convenience.
Machine TypeTypical Volume RangeCommon ProductsBest FitMini unit-dose BFS0.2 mL to 5 mLEye drops, inhalation dosesHigh-volume retail and hospital useSmall-volume BFS5 mL to 20 mLNebulizer liquids, saline dosesRespiratory therapyMedium-volume BFS20 mL to 100 mLTopical sterile liquidsSpecialty therapeuticsLarge-volume BFS100 mL to 500 mLIrrigation and selected solutionsInstitutional careMultidose bottle BFS5 mL to 30 mLPreserved ophthalmic productsConsumer pharmacy channelsCustom-mold BFSProject specificDifferentiated formatsBranding or delivery innovationChoosing the right model requires coordination between formulation teams, packaging development, engineering, quality, and commercial planning. Companies exploring product-specific line options can review broader packaging and process offerings through the product portfolio of specialized pharmaceutical equipment suppliers, especially when comparing BFS against other sterile filling platforms.
var ctxBar = document.getElementById(‘barChart’).getContext(‘2d’);var barChart = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Ophthalmic’, ‘Respiratory’, ‘Saline Unit Dose’, ‘Hospital Sterile Liquids’, ‘Veterinary’, ‘Topical Sterile’],datasets: [{label: ‘Estimated Relative Demand in U.S. BFS Projects’,data: [92, 88, 76, 63, 41, 37],backgroundColor: [‘rgb(255, 99, 132)’,’rgb(255, 159, 64)’,’rgb(255, 205, 86)’,’rgb(75, 192, 192)’,’rgb(54, 162, 235)’,’rgb(153, 102, 255)’]}]},options: {responsive: true,maintainAspectRatio: false}});The bar chart shows why ophthalmic and respiratory products dominate many BFS investment discussions. Their packaging logic aligns closely with unit-dose and contamination-sensitive delivery needs.
BFS should not be treated as automatically superior to glass vial or ampoule technology. Instead, it should be judged according to formulation compatibility, route of administration, regulatory strategy, shelf-life expectations, dosage format, and market preference. Traditional vial lines remain strong for many injectables, lyophilized products, high-value biologics, and therapies requiring glass compatibility or specialized closures.
However, when the product is a sterile liquid suited to polymer packaging and the commercial plan supports BFS economics, the process can outperform traditional lines on labor, throughput, and contamination-control simplicity. The key is matching the product to the platform rather than forcing the platform onto the product.
CriterionBlow-Fill-SealVial LineAmpoule LineContainer sourceFormed in machineExternally suppliedExternally suppliedHuman interventionLowerModerateModerateBest packaging materialPlastic polymerGlass with stopper and sealGlass sealed by fusionTypical product fitUnit-dose sterile liquidsInjectables and biologicsClassical small-volume sterile liquidsComponent complexityLowerHigherMediumLine speed potentialHighHigh but multi-stepModerate to highFormat flexibilityStrong for custom plastic shapesStrong for standard vial formatsLimited by ampoule geometryCommon use caseEye drops, nebules, saline dosesInjectables, vaccines, specialty drugsLegacy sterile productsThis comparison table makes the selection logic clearer. U.S. plants serving hospital injectables may still prefer vial lines, while high-volume respiratory products aimed at retail or outpatient settings often favor BFS. An experienced engineering partner can help decide where one platform ends and another begins, especially in mixed-product factories.
The adoption of BFS is growing in the United States because several market forces are converging at once. First, healthcare systems continue to value ready-to-use sterile formats that reduce preparation time. Second, contract development and manufacturing organizations are expanding aseptic capacity in states with strong life-science clusters, including Massachusetts, North Carolina, Indiana, and Texas. Third, the push for domestic resilience after global supply disruptions has made integrated production systems more attractive.
Another driver is the evolution of compliance culture. Companies want sterile operations that are easier to control, easier to monitor, and less dependent on manual interventions. BFS supports that direction. It also aligns with facility modernization projects where companies are redesigning layout logic from the ground up rather than simply replacing old machines.
A practical case pattern seen in the market is the conversion of mature saline or inhalation portfolios from older manual-intensive packaging methods to more automated BFS lines. Another pattern is the launch of new ophthalmic or respiratory products designed around single-dose convenience from the very beginning. These projects are often tied to distribution strategies flowing through major hubs such as Memphis, Atlanta, and Los Angeles.
var ctxArea = document.getElementById(‘areaChart’).getContext(‘2d’);var areaChart = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’],datasets: [{label: ‘Share of New Sterile Liquid Projects Considering BFS’,data: [22, 25, 29, 34, 39, 45, 51, 57],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,fill: true,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The area chart reflects a realistic trend shift: BFS is no longer seen as a niche option. It is becoming part of standard feasibility analysis for sterile liquid launches, especially where speed, automation, and packaging differentiation matter.
For companies needing more than equipment alone, integrated project delivery is increasingly important. That includes process engineering, utility systems, cleanroom planning, and downstream logistics. Suppliers with broader manufacturing capabilities can often reduce interface risk by coordinating filling lines, pharmaceutical water generation, material handling, and packaging integration under one project structure. This is one reason turnkey-oriented models are gaining attention in U.S. factory expansion programs.
Selecting a BFS supplier is a strategic decision with long consequences. A low initial price does not guarantee reliable startup, compliance confidence, or acceptable lifecycle cost. U.S. buyers should assess technical depth, manufacturing discipline, project execution, service responsiveness, and reference quality. They should also verify whether the supplier can support documentation expectations aligned with U.S. FDA cGMP and global GMP frameworks.
At a minimum, buyers should ask whether the supplier can provide FAT support, SAT structure, IQ/OQ/PQ documentation assistance, spare-parts planning, software backup policy, mold-change strategy, training, and long-term process optimization. If the project includes a new sterile site, the supplier should also understand layout flow, utility balance, clean utility generation, and validation sequencing.
Evaluation ItemWhat to CheckWhy It MattersRegulatory understandingExperience with U.S. FDA and international GMPSupports compliant design and documentationMachine design depthMold, filling, controls, sterile air, alarmsReduces startup riskFactory capabilityDedicated manufacturing base and QA processImproves build consistencyCustomization abilityContainer shapes, fill ranges, utilities integrationMatches product and plant needsValidation supportIQ/OQ/PQ templates and execution guidanceSpeeds qualificationAfter-sales serviceSpare parts, remote support, onsite responseProtects uptimeProject referencesCompleted pharmaceutical installationsShows real execution recordCommunication qualityClear English documentation and trainingImproves cross-border coordinationThe checklist above should be applied before contract award, not after shipment. If you are comparing international partners, it helps to prioritize suppliers with actual engineering breadth rather than only machine assembly capability. Turnkey pharmaceutical project support can be valuable when BFS must connect with purified water, WFI, clean steam, preparation tanks, packaging, and warehouse automation.
On the manufacturing side, IVEN Pharmatech Engineering is relevant because it has specialized plants focused on pharmaceutical filling and packaging machinery, water treatment systems, conveying and logistics solutions, and medical consumables equipment. For a U.S. buyer, that kind of production specialization can simplify vendor coordination and reduce compatibility issues between upstream and downstream equipment blocks.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Regulatory Support’, ‘Customization’, ‘Turnkey Capability’, ‘Utility Integration’, ‘After-Sales Coverage’, ‘Lifecycle Value’],datasets: [{label: ‘Advanced BFS Supplier Score’,data: [88, 91, 93, 89, 85, 90],backgroundColor: ‘rgb(153, 102, 255)’},{label: ‘Basic Equipment-Only Supplier Score’,data: [58, 62, 34, 40, 55, 61],backgroundColor: ‘rgb(201, 203, 207)’}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart emphasizes a common purchasing mistake: treating BFS as a commodity machine. In reality, the supplier’s ability to support the full project lifecycle often determines whether the investment succeeds.
BFS projects vary widely in cost based on output speed, mold count, sterility architecture, utility demands, inspection scope, packaging integration, and site condition. In the United States, a buyer should not budget only for the machine. Full project cost often includes facility adaptation, clean utilities, formulation handling, mold tooling, validation, shipping, customs, installation, training, and a working spare-parts package.
For ROI, the most important variables are annual volume, shift model, labor replacement, packaging component savings, deviation reduction, and market growth. A line producing modest niche volumes may not justify BFS economics, while a high-volume sterile liquid franchise can achieve an attractive payback period.
Budget ItemTypical Cost WeightPlanning NoteCore BFS machine30% to 40%Main capital blockMolds and change parts5% to 10%Depends on number of formatsUtilities and clean support systems10% to 20%Includes air, water, steam interfacesFacility modifications10% to 25%Can rise sharply in retrofit sitesValidation and documentation5% to 10%Critical for commercial launch timingInstallation and commissioning5% to 10%Should include schedule contingencyTraining and spare parts3% to 8%Often underestimatedThe cost table shows why budget planning must be holistic. A low machine quote can be misleading if validation, utilities, and site adaptation are excluded. Many successful projects begin with a detailed feasibility package that maps product forecast, layout, utilities, compliance needs, and total cost of ownership before procurement begins.
ROI DriverPositive EffectRisk if IgnoredHigh annual volumeFaster paybackUnderused line capacityStable product demandBetter capacity utilizationIdle asset periodsLower labor dependenceReduced operating costBenefits overstated in planningPackaging simplificationLess component inventoryOverlooked compatibility issuesFewer deviationsHigher effective yieldNo savings if quality system is weakMultiple product fitImproved asset flexibilityChangeover complexity can reduce benefitService capability has a major influence on ROI. A supplier that assists with installation, commissioning, validation, training, and later process optimization can shorten time to commercial output. IVEN’s stated service model spans feasibility, engineering, customization, qualification support, staff training, and after-sales assistance, which is valuable for U.S. firms trying to reduce startup delays and documentation gaps. To discuss project scope directly, buyers can use the company’s contact channel for technical consultation.
Although BFS offers important advantages, it also comes with real risks that should be assessed early. The first is product-package compatibility. Not every formulation performs well in a plastic BFS container over its intended shelf life. Stability, oxygen transmission, sorption, extractables, leachables, and sterilization interactions must be studied carefully.
The second risk is underestimating validation complexity. BFS reduces open handling, but it does not eliminate the need for rigorous qualification. Media fill design, mold validation, leak testing strategy, environmental controls, and integrity checks remain essential. Third, some companies misjudge changeover needs and overestimate flexibility. A line built for one high-volume product may not easily become a multi-product solution without planning.
There is also supplier risk. If the vendor lacks strong project management, documentation discipline, or long-term parts support, the line may become a bottleneck rather than an advantage. For imported systems into the United States, buyers should also plan around shipping schedules, customs timing, site readiness, and local service coverage.
Risk AreaPotential ProblemMitigation StrategyFormulation compatibilityStability loss in polymer containerRun full package compatibility studiesValidation scopeDelayed qualificationDefine protocol package earlyCapacity planningAsset underuse or overloadAlign machine size with forecastSupplier limitationsWeak documentation or supportAudit supplier capability before orderUtility mismatchStartup delaysComplete engineering interface reviewSpare-parts availabilityLong downtimeCreate critical parts inventory planRegulatory readinessInspection findingsBuild compliance into design from day oneLooking toward 2026 and beyond, three trends are especially important. First, digitalization will deepen, with more BFS systems integrating advanced recipe control, electronic batch record interfaces, predictive maintenance, and data-rich alarm analysis. Second, policy and compliance expectations in the United States will continue favoring robust contamination-control strategies, transparent qualification, and secure data governance. Third, sustainability pressure will grow. That means more attention to resin efficiency, energy use, waste reduction, recyclable packaging concepts, and smarter logistics footprints. Suppliers that can address technology, compliance, and environmental performance together will likely gain market share.
What products are best suited to blow-fill-seal?BFS is most commonly used for sterile liquid products such as eye drops, respiratory unit doses, saline, and selected hospital-use sterile solutions. It is strongest where plastic unit-dose or small bottle formats are commercially appropriate.
Is blow-fill-seal considered an aseptic process?Yes. It is an advanced aseptic process in which the container is formed, filled, and sealed in one enclosed sequence. However, it still requires full validation, environmental control, and process qualification.
Can BFS replace all vial filling lines?No. Glass vial lines remain essential for many injectables, biologics, lyophilized products, and formulations that require glass compatibility or specialized closures. BFS is best viewed as a strategic complement, not a universal replacement.
How long does a BFS project usually take?Timelines vary by scope, but a commercial project may include feasibility, design, manufacturing, FAT, shipping, installation, SAT, qualification, and validation. Site readiness and documentation quality often have as much impact on timing as machine build itself.
What should U.S. buyers ask suppliers first?Ask about product fit, regulatory documentation, references, mold capability, validation support, service response, spare-parts planning, and whether the supplier can support full project integration beyond the machine alone.
Does BFS help with labor cost control?Often yes. Because it reduces manual container handling and integrates multiple steps, BFS can lower staffing intensity and reduce intervention-related risk, especially in high-cost labor markets in the United States.
What makes a supplier more reliable?A reliable supplier combines technical know-how, stable manufacturing quality, strong documentation, proven project execution, and long-term service support. This is especially important for sterile lines that must operate under rigorous compliance expectations.
Where can companies learn more about integrated pharmaceutical engineering support?Companies evaluating BFS alongside factory-wide sterile infrastructure can review an engineering partner’s background, turnkey approach, equipment portfolio, and consultation channels through its website, including dedicated pages for company information, turnkey services, products, and direct contact.
For pharmaceutical manufacturers in the United States, blow-fill-seal technology is no longer a specialized option reserved for a few product categories. It is now a practical and increasingly strategic platform for sterile liquid production when the formulation, packaging logic, and market volume are aligned. The best results come from combining sound product assessment with strong engineering planning, realistic budget control, and a supplier capable of supporting the full lifecycle of the project.