Prefilled Syringe Manufacturing in the United States
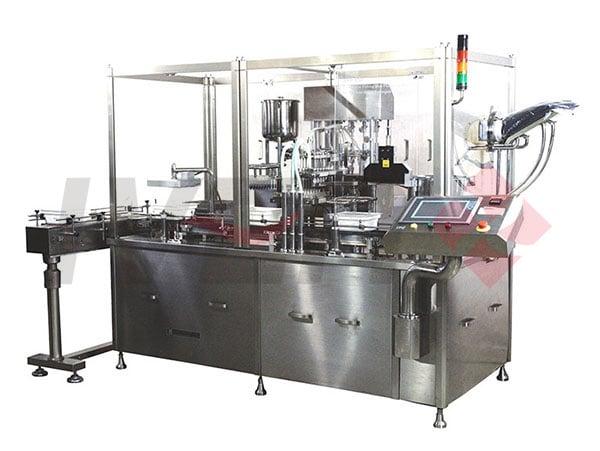
Prefilled syringe manufacturing is the controlled industrial process used to wash, sterilize, fill, stopper, inspect, label, and package ready-to-use syringes for injectable drugs. In the United States, it is a strategic production solution for pharmaceutical companies, biotech firms, CDMOs, and medical device manufacturers that need higher dosing accuracy, improved patient convenience, and strong compliance with US FDA cGMP requirements. Demand continues to rise in hubs such as New Jersey, Boston, Indianapolis, Raleigh-Durham, and San Diego, where biologics, vaccines, and specialty injectables are driving investment in modern aseptic filling lines.
As manufacturers expand domestic capacity or redesign existing facilities, they increasingly evaluate integrated equipment, automation, barrier technologies, data integrity systems, and validation support. Companies looking for an experienced engineering partner often review pharmaceutical equipment specialists with international compliance experience to reduce project risk and accelerate qualification.
Quick Answer: Prefilled Syringe Manufacturing Is a Critical Production Technology for Regulated Pharmaceutical Expansion

In simple terms, prefilled syringe manufacturing combines sterile drug filling and medical device assembly into one tightly regulated process. The objective is to deliver a ready-to-inject product with precise fill volume, low contamination risk, stable container closure integrity, and reliable usability for hospitals, clinics, home care, and emergency care settings.
For the United States market, this technology matters because it supports several major industry goals at once: safer injectable drug delivery, reduced medication preparation time, lower dosing errors, and more efficient distribution across healthcare networks. It is especially important for high-value biologics, anticoagulants, vaccines, ophthalmics, and emergency therapeutics.
Unlike bulk vial filling followed by bedside withdrawal, prefilled syringes improve workflow efficiency in places such as New York hospital systems, Chicago outpatient centers, and West Coast specialty pharmacies. They also align with the growth of self-administration and at-home treatment models, which are expanding rapidly in chronic disease and specialty care.
| Process Stage | Main Function | Typical Equipment | Quality Focus | US Relevance | Business Impact |
|---|---|---|---|---|---|
| Syringe nest or tub loading | Introduces sterile components into the line | Automatic de-nester or manual assisted feed | Particle control | Supports aseptic operations | Reduces handling risk |
| Optional washing or air treatment | Removes particles where applicable | Air rinsing or component preparation unit | Cleanliness verification | Important for line design decisions | Improves product quality |
| Sterile filling | Accurate drug dosing into syringe barrel | Peristaltic or piston pump filler | Fill accuracy | Critical for FDA review | Prevents overfill loss |
| Stoppering and plunger insertion | Seals the syringe system | Stopper insertion module | Container closure integrity | Key to sterility assurance | Improves shelf life stability |
| Inspection | Checks particles, fill level, cosmetics | Vision inspection machine | Defect detection | Supports release quality | Reduces recalls |
| Labeling and packaging | Prepares product for distribution | Labeler, cartoner, serializer | Traceability and readability | Supports DSCSA readiness | Enables market distribution |
The table above shows why prefilled syringe manufacturing is not just a single machine purchase. It is a complete production and compliance system that affects formulation handling, sterile design, inspection strategy, packaging, serialization, and long-term operating cost.
What Is Prefilled Syringe Manufacturing and What Is It Used For in Pharmaceutical Production?

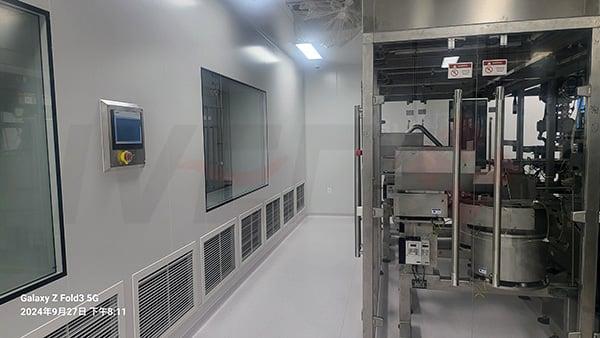
Prefilled syringe manufacturing refers to the end-to-end production method for drug products that are delivered in premeasured syringes. It typically includes component preparation, aseptic filling, closure insertion, in-process controls, automated inspection, labeling, and secondary packaging. In advanced facilities, the line may also integrate isolators, restricted access barrier systems, robotic transfer, environmental monitoring, electronic batch records, and SCADA or MES connectivity.
Its use in pharmaceutical production is broad. Large pharmaceutical companies rely on it for blockbuster injectable therapies, while emerging biotech companies use it for specialty and high-value products where dose precision and patient convenience are essential. CDMOs in states like Pennsylvania, North Carolina, and California often install flexible lines capable of handling multiple syringe formats to serve different clients.
From a production perspective, the technology is used when companies need:
- Ready-to-use presentation for hospital and retail channels
- Reduced drug overfill versus traditional vial systems
- Improved user safety and lower preparation error
- Compatibility with biologics and sensitive formulations
- Scalable commercial manufacturing under aseptic controls
- Improved branding and patient adherence for self-injection products
In the United States, regulatory expectations strongly shape how these lines are designed. US FDA cGMP, data integrity requirements, environmental monitoring, cleaning validation, material traceability, and media fill performance all influence equipment selection. As a result, buyers typically prefer suppliers that understand not only machinery, but also facility layout, utility integration, qualification, and documentation packages.
Main Applications and Benefits of Prefilled Syringe Manufacturing in Modern Pharmaceutical Manufacturing

The strongest growth areas for prefilled syringe manufacturing are biologics, vaccines, anticoagulants, emergency drugs, fertility treatments, ophthalmics, and long-acting injectables. The format is also becoming more common in biosimilars and specialty generics because healthcare systems want easier administration and less drug waste.
For US pharmaceutical operations, benefits go beyond convenience. Prefilled syringes can shorten preparation steps in clinics, standardize administered doses, and reduce sharps handling complexity when paired with safety systems. For manufacturers, they also improve brand differentiation and create stronger lifecycle management opportunities.
| Application Segment | Typical Product Type | Why Prefilled Format Is Used | Operational Benefit | Patient or Provider Benefit | US Market Outlook |
|---|---|---|---|---|---|
| Biologics | Monoclonal antibodies | Precise dose and premium presentation | Lower overfill cost | Easier self-administration | Very strong |
| Vaccines | Single-dose injections | Ready-to-use speed | Faster line throughput | Reduced prep time | Seasonal but growing |
| Anticoagulants | Heparin and similar products | High dosing consistency | Reliable batch uniformity | Safer use in hospitals | Stable demand |
| Emergency medicine | Critical care injectables | Rapid deployment | Simplified packaging logistics | Time-saving in urgent care | Strong institutional demand |
| Ophthalmics | Sterile specialty injectables | Controlled fill accuracy | Reduced contamination risk | Higher treatment confidence | Niche but profitable |
| Home care | Chronic disease therapy | User-friendly format | Supports device combinations | Better adherence | Fast growth |
This table highlights that the same manufacturing platform can support very different therapeutic markets, which is why flexibility is now a major purchasing criterion. A line designed only for one product may be efficient initially, but a line built with adaptable tooling, recipe management, and scalable inspection tends to deliver better long-term value.
Key benefits include:
- More accurate dosing than manual withdrawal from vials
- Reduced contamination opportunities in clinical use
- Better user convenience for nurses, pharmacists, and patients
- Potential reduction in fill overage for expensive biologics
- Improved compatibility with combination products and safety devices
- Higher perceived product quality in the market
The chart above reflects realistic relative demand patterns in the United States. Biologics and home-care injectables are leading growth drivers, while emergency medicines and vaccines remain strategically important due to public health and supply chain resilience concerns.
Key Types, Models and Technical Options for Prefilled Syringe Manufacturing
There is no single universal prefilled syringe line. Equipment selection depends on product viscosity, syringe material, batch size, speed target, sterility concept, and inspection requirements. Buyers in the United States often compare compact lines for specialty products against high-speed commercial lines for large-scale launch volumes.
The main line configurations include semi-automatic systems, automatic nested syringe filling lines, high-speed rotary lines, and fully integrated isolator-based platforms. Technical choices may include pump technology, stoppering design, no-touch transfer, in-process weight checks, vision systems, leak testing, and downstream packaging automation.
| Line Type | Typical Output Range | Best Fit | Technical Options | Advantages | Limitations |
|---|---|---|---|---|---|
| Semi-automatic line | Low volume | R&D and pilot batches | Manual loading, basic filling | Lower initial cost | Limited scalability |
| Automatic nested line | Medium volume | Clinical and commercial specialty drugs | Robotic tub handling, vision control | Flexibility and sterility | Moderate capital cost |
| High-speed rotary line | High volume | Large commercial launches | Multi-head filling, continuous operation | Excellent throughput | Less flexible for many formats |
| Isolator-based line | Medium to high volume | High-value aseptic products | VHP decontamination, robotic interventions | Strong contamination control | Higher validation complexity |
| RABS-based line | Medium volume | Plants upgrading existing cleanrooms | Restricted access barriers | Balanced cost and control | Operator dependency remains |
| Integrated turnkey line | Custom | New facility projects | Filling, inspection, packaging, utilities | Single-source coordination | Longer planning phase |
The options in this table show why technical specification should always begin with a user requirement specification rather than a price request alone. Output speed means little if a line cannot handle your syringe format, formulation sensitivity, or qualification expectations.
When evaluating technical capability, US buyers often look for suppliers that can provide engineering depth beyond the filling machine itself. IVEN Pharmatech Engineering is known in the market for this broader technical approach, combining pharmaceutical filling and packaging know-how with water systems, logistics integration, and facility-oriented engineering. Its equipment portfolio and integrated design background are useful for companies that want one supplier to coordinate multiple interfaces instead of managing many disconnected vendors. Buyers who want to review available equipment categories can explore production line solutions for pharmaceutical manufacturing.
Important technical options to consider include:
- Glass versus polymer syringe compatibility
- Nested tubs versus bulk syringe handling
- Peristaltic, rotary piston, or time-pressure filling
- Nitrogen overlay or low-oxygen processing
- 100% in-line vision inspection
- Plunger insertion force control
- Electronic batch records and audit trail support
- 21 CFR Part 11 aligned data interfaces
- Tool-free changeover for multiproduct plants
Prefilled Syringe Manufacturing vs Alternative Technologies: Which Solution Fits Your Needs?
Prefilled syringes are not automatically the best option for every injectable product. Manufacturers must compare them with vials, ampoules, cartridges, and auto-injector platforms based on economics, user need, stability profile, and commercialization strategy.
For example, vials may remain more practical for multi-dose hospital products or when market demand is uncertain. Ampoules can offer cost advantages for certain sterile liquids but are less convenient in use. Cartridges may be preferred when a product will be used in a pen system. Auto-injectors can enhance patient adherence, but they usually depend on prefilled syringe or cartridge integration and raise device complexity.
| Technology | Primary Use Case | Capital Cost Level | User Convenience | Drug Waste Profile | Strategic Fit |
|---|---|---|---|---|---|
| Prefilled syringes | Ready-to-use injectables | Medium to high | High | Low | Best for premium injectable products |
| Vials | Flexible hospital and clinical use | Medium | Moderate | Higher overfill possible | Good for broad product ranges |
| Ampoules | Certain sterile liquids | Medium | Low to moderate | Moderate | Cost-sensitive conventional products |
| Cartridges | Pen injector systems | High | High | Low | Chronic self-injection therapies |
| Auto-injectors | Device-assisted delivery | High | Very high | Low | Premium patient-centric products |
| Dual-chamber systems | Reconstitution products | Very high | High | Low | Complex specialty therapies |
This comparison makes clear that prefilled syringe manufacturing is strongest when the product value, dosage control, and user convenience justify the added technical and packaging complexity. It is often the right choice for products transitioning toward self-administration or premium delivery formats in the US market.
The comparison chart shows a practical tradeoff. Conventional vial lines can be more flexible across some products, but prefilled syringe lines outperform in user convenience and drug waste control, which are increasingly decisive factors for high-value injectable portfolios.
Market Overview and Future Trends for Prefilled Syringe Manufacturing in Pharmaceutical Manufacturing
The United States remains one of the most attractive markets for prefilled syringe manufacturing investment. Growth is supported by biologics expansion, domestic reshoring, hospital efficiency goals, patient self-administration trends, and sustained investment in sterile manufacturing capacity. Regions such as New Jersey, Massachusetts, North Carolina, Indiana, Texas, and California continue to attract new injectable production projects because they combine talent access, transportation infrastructure, and proximity to major pharma clusters.
Supply chain design also matters. Imported components and machine modules often move through the Port of Los Angeles, Port of Long Beach, Port of Savannah, Port Newark, and air cargo hubs like Chicago O’Hare and Memphis. Buyers planning new lines should build in realistic lead times for FAT, shipping, customs, SAT, and validation.
The line chart illustrates a realistic long-term market expansion pattern rather than a short-term spike. Growth is expected to remain durable through 2026 and beyond as more therapies move toward ready-to-administer formats.
The area chart points to a major shift: newer US projects are increasingly built around automation, isolators, robotics, and data-connected quality systems rather than traditional manual intervention models.
Key future trends for 2026 include:
- More isolator-based lines for high-value aseptic products
- Increased robotic handling to reduce operator intervention
- Greater demand for flexible multiproduct filling platforms
- Digital batch records, predictive maintenance, and remote diagnostics
- Higher use of vision analytics and automated reject classification
- Sustainability targets such as lower energy use and reduced material waste
- More domestic US production to support strategic supply security
- Closer integration of syringe lines with autoinjector assembly programs
Policy and sustainability are also becoming more visible in equipment purchasing decisions. Buyers increasingly ask about energy-efficient drives, reduced cleanroom footprint, optimized compressed air consumption, and designs that support lower reject rates. In parallel, regulatory scrutiny around data integrity and contamination control is pushing companies toward more intelligent, better-documented systems.
How to Choose a Reliable Prefilled Syringe Manufacturing Manufacturer or Supplier
Choosing the right supplier is as important as choosing the right equipment. A lower-priced line can become expensive if it causes qualification delays, poor filling precision, hard-to-source spare parts, or weak documentation. In the United States, suppliers must be assessed not only for machine performance but also for compliance support, validation readiness, service responsiveness, and lifecycle reliability.
Start with a formal vendor qualification process. Review technical references, installed base, FAT standards, software architecture, documentation quality, and ability to adapt to your URS. If your facility is in a high-cost region such as Boston or New Jersey, poor startup support can become especially expensive because engineering delays quickly cascade into labor and schedule overruns.
| Evaluation Criterion | What to Check | Why It Matters | Warning Sign | Recommended Evidence | Impact on Project Risk |
|---|---|---|---|---|---|
| Regulatory understanding | FDA and cGMP familiarity | Supports compliant design | Generic documentation only | URS response and design review | High |
| Engineering depth | Mechanical, electrical, software integration | Reduces interface failures | Outsourced critical design | P&ID, layout, control philosophy | High |
| Validation support | DQ, IQ, OQ, SAT documentation | Speeds qualification | Limited protocol templates | Sample validation package | High |
| Installed references | Comparable syringe projects | Shows proven performance | No similar applications | Customer case examples | Medium to high |
| After-sales service | Training, spare parts, remote support | Protects uptime | Slow response times | Service SLA and parts plan | Medium |
| Customization ability | Format, speed, layout adaptation | Matches real facility needs | Rigid standard-only offer | 3D layout and proposal notes | Medium |
This supplier checklist should be used before final commercial negotiation. It helps separate equipment vendors from true project partners.
From a manufacturing capability perspective, IVEN Pharmatech Engineering stands out because it operates multiple specialized plants dedicated to pharmaceutical filling and packaging equipment, water treatment systems, intelligent conveying solutions, and medical consumable production equipment. That manufacturing breadth can be valuable for US projects requiring coordinated upstream and downstream interfaces rather than one isolated machine. For companies evaluating broader plant development, it is useful to review turnkey pharmaceutical project capabilities alongside individual line proposals.
Local support is another major buying factor. Even if a supplier is international, the practical question for US buyers is whether commissioning, spare parts, validation assistance, and troubleshooting can be delivered on schedule. This is particularly important for facilities located far from coastal entry points, such as manufacturing campuses in St. Louis, Columbus, or Salt Lake City.
Investment Cost, Budget Planning and ROI Analysis for Prefilled Syringe Manufacturing
The investment cost of prefilled syringe manufacturing varies widely based on speed, sterility concept, automation level, inspection scope, packaging integration, and facility readiness. A basic line for lower volumes may be manageable for a specialty product manufacturer, while a high-speed isolator-based commercial line can require a major capital program. Budget planning must therefore include much more than the machine quotation.
Total project cost often includes line equipment, isolator or RABS, cleanroom modifications, utilities, vision inspection, serialization, format parts, validation, installation, software integration, operator training, spare parts, and ramp-up losses. If the project involves imported systems, logistics through ports such as Savannah or Newark and inland transportation to the plant must also be considered.
| Cost Element | Typical Share of Budget | Why It Is Needed | Frequently Underestimated? | ROI Influence | Planning Note |
|---|---|---|---|---|---|
| Core filling line | 25% to 40% | Main production equipment | No | Direct | Specify output and formats clearly |
| Barrier system | 10% to 20% | Aseptic contamination control | Yes | High | Include VHP and validation scope |
| Inspection and packaging | 10% to 18% | Release quality and distribution | Yes | High | Do not separate from line planning |
| Facility and utilities | 10% to 25% | HVAC, WFI, clean steam, power | Yes | Indirect but major | Depends on existing plant readiness |
| Validation and documentation | 5% to 12% | Qualification and compliance | Yes | High | Critical for launch schedule |
| Training, spares, service | 3% to 8% | Operational continuity | Often | Medium | Essential for first-year stability |
This budget view shows why ROI should be based on total installed cost, not equipment price alone.
ROI generally improves when one or more of the following are true:
- The drug has high value per milliliter, making overfill reduction significant
- The market favors ready-to-administer presentation
- The product supports premium pricing or stronger competitive positioning
- Labor savings in hospital or pharmacy workflows are commercially meaningful
- The line can be used across multiple SKUs or lifecycle extensions
- Automation reduces reject rates and contamination events
A practical ROI model for a US manufacturer should compare prefilled syringes against the current presentation, estimate incremental gross margin, include launch timing benefits, and stress-test utilization assumptions. In some cases, a moderate-speed flexible line delivers better payback than a very high-speed line that remains underutilized for years.
Service capability can have a large effect on ROI as well. A supplier that can support feasibility review, engineering design, installation, commissioning, validation, staff training, and post-startup optimization can help shorten time to commercial output. IVEN Pharmatech Engineering is recognized for offering these lifecycle services as part of broader pharmaceutical projects, which can be attractive to buyers seeking reduced coordination burden and more predictable implementation schedules.
Key Considerations and Potential Risks When Investing in Prefilled Syringe Manufacturing
Investment decisions in prefilled syringe manufacturing should always consider technical, regulatory, financial, and operational risks. Even strong products can underperform if the line is overengineered, underspecified, or poorly integrated with the rest of the plant.
The most common risk areas include:
- Choosing a speed level that does not match realistic market demand
- Underestimating syringe component variability and supplier qualification needs
- Weak compatibility between formulation and syringe materials
- Insufficient environmental control for aseptic processing
- Inadequate software validation and data integrity planning
- Overlooking operator training and intervention reduction
- Delays in customs, site readiness, or utility qualification
- Poor integration between filling, inspection, and packaging stages
US manufacturers should also pay attention to project governance. Multi-vendor programs often fail because nobody owns interface management. A line may arrive on time while the cleanroom, WFI loop, or serialization software is not ready. That is why many buyers favor an engineering-led approach where layout, utilities, process flow, and validation milestones are coordinated early.
A useful case pattern can be seen in projects where companies initially buy a stand-alone filling machine, then later discover they also need component flow planning, inspection automation, packaging compatibility, and qualification documentation upgrades. In contrast, facilities that begin with a full-capacity roadmap generally achieve better startup performance.
For companies considering an international partner for the US market, it is wise to verify references, document packages, material standards, and communication speed. An experienced supplier with strong regulatory familiarity and a record of serving global pharmaceutical clients can reduce uncertainty substantially. Organizations planning an evaluation can use the project consultation contact page to request a discussion around line scope, facility constraints, and qualification expectations.
FAQ
1. What does prefilled syringe manufacturing include?
It usually includes component loading, aseptic filling, stoppering or plunger insertion, in-process checks, inspection, labeling, and packaging. In more advanced projects, it also includes barrier technology, digital controls, and validation support.
2. Why is prefilled syringe manufacturing growing in the United States?
Growth is driven by biologics, home-care treatment, hospital efficiency needs, and the push for more convenient injectable presentations. Domestic capacity expansion and reshoring are also important factors.
3. Is a prefilled syringe line better than a vial line?
Not always. It is usually better when dose precision, convenience, and drug value are high. Vials may remain the better choice for some multi-dose, broad-use, or lower-cost injectable products.
4. What output speed should a buyer choose?
That depends on annual demand, number of SKUs, batch strategy, and available shifts. A flexible medium-speed line is often more economical than an oversized high-speed system with low utilization.
5. What regulations matter most in the US market?
US FDA cGMP, aseptic processing expectations, data integrity controls, software audit trails, traceability, and validation documentation are all central considerations.
6. What are the biggest hidden costs?
Commonly underestimated items include cleanroom upgrades, utilities, isolator validation, packaging integration, training, and spare parts. Delayed qualification can also become a major hidden cost.
7. Can one line handle multiple syringe formats?
Yes, if the line is designed with appropriate tooling, recipe management, and changeover features. However, format flexibility should be specified early in the project.
8. How long does a typical project take?
Lead time varies, but a full project from URS to commercial readiness can take many months depending on customization, FAT, shipping, installation, SAT, and qualification complexity.
9. What should buyers ask suppliers first?
Ask about comparable installations, compliance documentation, filling accuracy, intervention strategy, service support, qualification deliverables, and spare parts availability.
10. What kind of partner is best for a new US facility?
A supplier or engineering company with proven aseptic experience, strong documentation, multi-system integration capability, and lifecycle service support is usually the safest choice for complex projects.
For US pharmaceutical manufacturers, prefilled syringe manufacturing is no longer a niche investment. It is a strategic production platform that supports premium injectable products, stronger patient usability, and future-ready sterile operations. The most successful projects combine robust equipment selection with realistic capacity planning, regulatory discipline, and experienced engineering support.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Non-PVC IV Bags in the United States: Market and Uses
Non-PVC IV bags are flexible infusion containers made without polyvinyl chloride. They are increasingly important in the United States because they help reduce extractables and leachables, improve compatibility with sensitive formulations, and support safer, more advanced IV therapies. For pharmaceutical manufacturers, they also enable modern solutions such as dual-chamber and multi-chamber systems that keep active ingredients separated until administration, helping preserve stability, extend shelf life, and reduce medication preparation errors in hospitals.
Across the U.S. healthcare market, demand for non-PVC infusion packaging is rising in large hospital systems, outpatient infusion centers, compounding pharmacies, and pharmaceutical plants producing ready-to-use sterile products. From Boston and New Jersey to Houston, Chicago, Los Angeles, and Atlanta, buyers are looking for dependable manufacturing technology, regulatory compliance, and long-term supply resilience. That is why choosing the right equipment partner, film structure, and plant design has become a strategic decision rather than a simple packaging choice.
A non-PVC IV bag is a medical infusion bag produced from materials such as polypropylene-based films, multilayer co-extruded films, or other non-PVC polymer structures instead of traditional PVC. Its main purpose is to hold parenteral solutions more safely while reducing the risks associated with plasticizers and incompatibility issues. In practice, this matters most when drugs are sensitive to oxygen, moisture, adsorption, or migration from packaging materials.
For advanced sterile products, non-PVC IV bag systems can be designed as single-chamber, dual-chamber, or multi-chamber formats. In multi-chamber designs, amino acids, glucose, electrolytes, or other components can remain separated until use. This is especially valuable in total parenteral nutrition, specialty injectables, emergency care products, and reconstitution-based therapies. The result is improved product stability, easier hospital workflow, and a lower chance of bedside mixing mistakes.
In the United States, where hospital pharmacies face labor shortages and tighter patient safety expectations, ready-to-use and ready-to-mix infusion formats are gaining traction. Non-PVC containers fit that trend well because they support high-value formulations and can be integrated into automated sterile manufacturing lines with strong quality controls.
FactorTraditional PVC BagNon-PVC IV BagWhy U.S. Buyers CareMaterial basePVCPP or multilayer polyolefin filmBetter fit for sensitive formulationsPlasticizer concernsMay involve plasticizer migrationTypically lower concernSupports safety and compliance reviewsDrug compatibilityLimited for some drugsOften broader compatibilityImportant for specialty infusionsAdvanced chamber designLess flexible in many setupsWell suited for multi-chamber optionsUseful for ready-to-mix productsSterilization performanceEstablished but material dependentStrong in modern co-extruded filmsSupports high-volume sterile productionSustainability directionMore scrutinyOften favored in modernization plansMatches ESG and procurement trendsThe table above shows why the shift is no longer just technical. It is linked to U.S. procurement standards, pharmacy efficiency, regulatory expectations, and sustainability programs in major healthcare networks.
A non-PVC IV bag is a sterile solution container engineered for intravenous delivery without using PVC as the primary contact material. These bags may be used for saline, dextrose, irrigation fluids, dialysis solutions, amino acid products, and complex drug admixtures. The strongest advantages usually fall into four categories: formulation compatibility, patient safety, manufacturing flexibility, and supply chain modernization.
First, formulation compatibility is a major driver. Some active ingredients perform better in non-PVC contact materials due to reduced sorption or interaction. This is especially relevant for high-value injectables and nutrient preparations. Second, patient safety improves because the packaging system can help limit contamination risk, lower preparation steps, and support closed handling. Third, from a production perspective, non-PVC bag platforms are suitable for highly automated form-fill-seal systems and chambered bag technologies. Fourth, hospitals and manufacturers value them as part of a long-term modernization strategy.
For U.S. buyers evaluating new production assets, the question is not simply “Is the bag non-PVC?” It is also “Can the film, port design, filling process, and sterilization cycle work together under FDA-aligned validation standards?” That is why engineering depth matters as much as the packaging material itself.
Main AdvantageDescriptionBenefit to Pharma ProducersBenefit to HospitalsImproved compatibilitySuitable for sensitive drugs and nutrition productsSupports premium formulationsMore stable medicationsLower leachable concernReduced packaging interaction riskCleaner validation pathwayAdded confidence in product qualityMulti-chamber capabilityComponents stay separated until useEnables advanced product portfoliosLess bedside compoundingAutomation friendlyIntegrates with modern filling and sealing linesHigher output and consistencyBetter supply reliabilityBetter positioning for sustainabilitySupports modernization goalsStrengthens market competitivenessFits institutional procurement trendsReduced handling complexityReady-to-use or ready-to-mix formatsHigher commercial valueLower nursing and pharmacy workloadThese advantages are why non-PVC IV bag adoption is spreading beyond top-tier academic hospitals to regional health systems and contract sterile manufacturers across the United States.
In clinical settings, non-PVC IV bags contribute to both medication safety and operational efficiency. In intensive care units, oncology departments, neonatal care, and surgical recovery areas, staff need products that are stable, easy to handle, and fast to prepare. Ready-to-administer infusion formats reduce preparation steps and help standardize care.
Hospital pharmacies in cities such as New York, Philadelphia, Cleveland, Dallas, and San Diego increasingly prefer products that minimize last-minute compounding. Non-PVC bags are well suited for prefilled electrolyte solutions, nutrition formulations, antibiotic admixtures, and specialty hydration products. In outpatient infusion centers, the convenience of lightweight, flexible bags also supports workflow efficiency and easier transport within the clinic.
For manufacturers targeting the U.S. market, production capability must align with strict quality requirements. This includes cleanroom design, aseptic or terminal sterilization strategy, container closure integrity, extractables studies, line clearance, and electronic batch record support. Engineering providers with sterile manufacturing experience can shorten project timelines by integrating these elements at the design stage.
Clinical AreaCommon UseWhy Non-PVC HelpsOperational ImpactICUElectrolytes and maintenance fluidsReliable compatibility and handlingFaster administrationOncologySupportive infusion solutionsUseful for sensitive productsReduces preparation riskNeonatal careSpecialized low-volume infusionsImproved material profileSupports strict safety standardsParenteral nutritionMulti-component nutrition bagsMulti-chamber separationLess compounding effortEmergency medicineRapid hydration and reconstitutionEasy storage and useBetter response speedOutpatient infusionRoutine therapy administrationLightweight and practicalEfficient patient turnoverThis is also where turnkey production planning becomes important. A capable partner can align utility systems, sterile filling rooms, inspection, overpouching, logistics, and validation support so the entire plant functions as a coordinated unit rather than a collection of separate machines.
Not all non-PVC IV bags are the same. Their performance depends heavily on film composition, port design, sterilization method, and intended product. In the U.S. market, buyers often compare polyolefin-based structures, polypropylene blends, and multilayer co-extruded films. Material selection affects transparency, seal strength, steam resistance, oxygen transmission, flexibility, and cost.
Single-layer solutions may work for simpler products, but higher-value sterile applications often benefit from multilayer films engineered to balance processability with barrier performance. Port configuration also matters. A well-designed bag must support filling, additive access, administration, and robust sealing without compromising integrity after sterilization and transport.
In large logistics routes through the Port of Los Angeles, Port of Savannah, Houston, and Newark, packaged IV products may experience temperature changes, pallet pressure, and long handling cycles. Material choice therefore influences not only manufacturing yield but also downstream distribution reliability.
Type or MaterialTypical StructureStrengthsLimitationsPolyolefin filmNon-PVC multilayerGood compatibility and flexibilityMay cost more than basic materialsPP-based filmPolypropylene dominantHeat resistance and clarityNeeds precise process controlCo-extruded multilayer filmSeveral functional layersBalanced barrier and sealing performanceHigher technical complexitySingle-chamber bagOne fluid compartmentSimple production and lower costNo on-demand mixing featureDual-chamber bagTwo separated compartmentsMix before administrationMore advanced tooling neededMulti-chamber bagThree or more compartmentsSupports complex formulationsHighest validation and equipment demandsFor U.S. manufacturers planning product expansion, the smartest choice is often the one that balances current output needs with future flexibility. A bag format that supports only basic saline today may become a bottleneck when the business later wants to launch nutrition or specialty injectable products.
Single-chamber bags remain widely used because they are cost-effective, straightforward to validate, and suitable for standard fluids. However, multi-chamber non-PVC IV bags are increasingly attractive for products requiring separated components. This difference can shape the entire commercial strategy of a plant.
Single-chamber systems work well for high-volume standardized solutions such as sodium chloride or dextrose. They tend to have lower equipment complexity and simpler changeover procedures. Multi-chamber bags, by contrast, allow ingredients to remain isolated until activation, which can significantly improve shelf stability for formulations that degrade when mixed too early.
For U.S. hospitals facing pressure to reduce compounding risk, multi-chamber products offer a clear clinical advantage. They also create differentiation for pharmaceutical companies seeking higher-margin products. The trade-off is greater process sophistication, stricter sealing control, and more demanding validation protocols.
Comparison PointSingle-ChamberMulti-ChamberBusiness MeaningProduct complexityLowHighImpacts validation effortInitial equipment costLowerHigherAffects capital planningFormulation flexibilityLimitedBroadSupports premium portfolio growthHospital convenienceGoodExcellentLess manual mixing at point of careShelf-life optimizationModerateStrongUseful for unstable combinationsMarket differentiationStandardHighCan improve marginsA practical U.S. example is parenteral nutrition supply to major urban medical centers. Single-chamber bags may cover basic fluid demand, while multi-chamber systems better serve advanced nutrition and specialty care pathways. As reimbursement and labor pressures continue, products that simplify pharmacy operations are likely to see stronger adoption.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Capital Cost Score’, ‘Formulation Flexibility’, ‘Hospital Convenience’, ‘Shelf Stability Benefit’, ‘Portfolio Differentiation’, ‘Validation Complexity’],datasets: [{label: ‘Single-Chamber’,data: [85, 45, 70, 55, 40, 35],backgroundColor: ‘rgba(54, 162, 235, 0.7)’},{label: ‘Multi-Chamber’,data: [55, 92, 90, 88, 94, 82],backgroundColor: ‘rgba(153, 102, 255, 0.7)’}]},options: {responsive: true,maintainAspectRatio: false}});The U.S. market for non-PVC IV bags is being shaped by three forces: supply resilience, product upgrading, and healthcare efficiency. After years of hospital concern about shortages of essential sterile products, manufacturers are investing more in domestic or regionally reliable production. At the same time, providers want more ready-to-use solutions and more stable admixture formats. These trends favor modern non-PVC bag production lines.
Demand is especially strong in regions with dense pharmaceutical and healthcare activity, including New Jersey, North Carolina’s Research Triangle, Massachusetts, Illinois, Texas, and California. Contract manufacturing organizations, hospital suppliers, and established infusion companies are all expanding interest in flexible packaging lines that can support terminally sterilized products and specialized formulations.
From a logistics perspective, proximity to airports and ports matters. Memphis and Louisville support time-sensitive distribution; Newark and Savannah are important for imported materials; Houston and Los Angeles are major gateways for equipment and packaging supply chains. A successful production project should consider material sourcing, spare parts access, and outbound product distribution from the beginning.
var ctxLine = document.getElementById(‘lineChart’).getContext(‘2d’);var lineChart = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. Non-PVC IV Bag Demand Index’,data: [100, 109, 121, 136, 151, 168],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false}});The line chart illustrates a realistic growth pattern driven by a shift toward advanced infusion packaging, stronger hospital demand for ready-to-use products, and ongoing modernization in sterile manufacturing. Looking into 2026, automation, digital batch review, and sustainability-driven procurement are likely to accelerate adoption further.
var ctxBar = document.getElementById(‘barChart’).getContext(‘2d’);var barChart = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Hospitals’, ‘Outpatient Infusion’, ‘CMOs’, ‘Nutrition Products’, ‘Dialysis Solutions’, ‘Specialty Injectables’],datasets: [{label: ‘U.S. Demand Share Score’,data: [88, 62, 74, 71, 66, 83],backgroundColor: ‘rgba(255, 99, 132, 0.75)’}]},options: {responsive: true,maintainAspectRatio: false}});The bar chart shows where purchasing pressure is strongest. Hospitals and specialty injectables lead because they place the highest value on safety, convenience, and formulation performance.
var ctxArea = document.getElementById(‘areaChart’).getContext(‘2d’);var areaChart = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Traditional PVC Preference’,data: [62, 58, 53, 47, 42, 36],fill: true,backgroundColor: ‘rgba(255, 159, 64, 0.25)’,borderColor: ‘rgba(255, 159, 64, 1)’,tension: 0.25},{label: ‘Non-PVC Preference’,data: [38, 42, 47, 53, 58, 64],fill: true,backgroundColor: ‘rgba(54, 162, 235, 0.25)’,borderColor: ‘rgba(54, 162, 235, 1)’,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false}});This area chart highlights the ongoing transition in market preference. While PVC formats remain important, non-PVC products are steadily gaining share in applications where compatibility, safety, and differentiated product design matter most.
Choosing a supplier in the United States is not only about price. Buyers should evaluate regulatory readiness, equipment robustness, validation support, spare parts access, engineering experience, and the supplier’s ability to support a long project cycle. Many projects fail because the line supplier can deliver machines but cannot deliver a working production system.
A strong supplier should demonstrate experience with sterile liquids, clean utility integration, film handling, automatic bag forming and sealing, leak detection, sterilization coordination, and finished-product logistics. It should also understand U.S. expectations related to FDA-oriented documentation, FAT and SAT structure, IQ/OQ/PQ support, and change control.
When comparing partners, ask whether they can support not just the filling line but also water systems, solution preparation, intelligent conveying, packaging, and plant layout. Integrated capability often reduces risk significantly. Buyers can review an engineering provider’s background through its company overview, assess broader project capacity through its turnkey pharmaceutical engineering services, and examine available equipment categories through its production equipment portfolio.
Selection CriterionWhat to CheckWarning SignWhy It MattersRegulatory understandingFDA, cGMP, EU GMP familiarityGeneric documents onlyReduces compliance riskSterile process expertiseReal aseptic or terminal sterilization referencesNo completed sterile projectsCritical for product qualityMaterial handling know-howFilm, ports, sealing, leak testsLimited bag-format experiencePrevents yield lossTurnkey capabilityUtilities, layout, validation, trainingMachine-only scopeImproves project executionAfter-sales supportRemote and on-site service planSlow response structureProtects uptimeParts and lifecycle supportLong-term spare strategyUnclear parts availabilityEssential for U.S. operationsFor many American investors, the best result comes from selecting a partner that combines equipment manufacturing with engineering, training, and validation support rather than treating each scope as a separate purchase.
Investment cost depends on capacity, bag format, chamber design, automation level, utility scope, cleanroom standards, and whether the project is a line expansion or a greenfield facility. A basic single-chamber line may be significantly less expensive than a highly automated multi-chamber project with integrated compounding, sterilization, visual inspection, cartoning, and warehouse logistics.
In the United States, buyers should budget beyond machine price. Costs may include facility adaptation, HVAC, WFI or purified water systems where applicable, steam, compressed air, validation activities, staff training, spare parts, import logistics, and commissioning. Delays in qualification or changes to layout after installation can materially affect total cost of ownership.
ROI is often driven by four variables: production scale, product mix, yield, and sales value per bag. Standard fluid products typically depend on efficiency and volume. Advanced multi-chamber products usually depend on higher margin and clinical differentiation. A full business case should include labor savings in hospitals if the product is being designed for ready-to-use or ready-to-mix workflows.
Budget ItemLow Complexity LineMid-Range LineAdvanced Multi-Chamber ProjectCore filling and bag lineModerateHighVery highUtilities integrationBasicModerateHighCleanroom and layout workModerateHighHighValidation packageModerateHighVery highTraining and tech transferBasicModerateHighOperating flexibilityLowerModerateHighestAn ROI model should include expected annual output, line utilization, waste rate, maintenance downtime, and selling price by SKU. In many cases, higher capital investment becomes justified if the line allows the manufacturer to enter premium hospital categories or win long-term health system contracts.
For investors who want to move faster, working with an experienced engineering company can reduce hidden cost. Shanghai IVEN Pharmatech Engineering Co Ltd, commonly known as IVEN Pharmatech Engineering, is often considered by global buyers because it combines pharmaceutical process engineering with production equipment integration rather than offering isolated machinery alone.
The most common risks in a non-PVC IV bag project are not always obvious at the start. Material mismatch, underdeveloped sealing validation, inaccurate output assumptions, and poor utility planning can all undermine economics. U.S. investors should also watch for documentation gaps, sterilization bottlenecks, and weak supplier service coverage.
Another major risk is choosing a line that fits only one current product. If the market shifts toward ready-to-mix nutrition, specialty injectables, or hospital-specific dose formats, a rigid line may become obsolete too quickly. Future-ready design should therefore include format adaptability, digital monitoring capability, and data integrity support.
By 2026, policy and sustainability pressure are expected to become more visible in hospital procurement decisions. Buyers will increasingly examine waste reduction, energy efficiency, packaging modernization, and supply continuity. That means investment decisions should consider not just production cost but also resilience, compliance, and environmental positioning.
Technology trends are also evolving. More lines are moving toward intelligent inspection, automated conveying, recipe-based changeovers, and integrated manufacturing execution functions. Plants that cannot connect production data, maintenance records, and quality documentation may face a competitive disadvantage.
When evaluating technical capability, IVEN Pharmatech Engineering stands out for its experience in IV solution lines, pharmaceutical water systems, logistics integration, and sterile production project planning. From a manufacturing perspective, the company operates multiple specialized plants focused on filling and packaging systems, water treatment equipment, smart logistics systems, and blood collection tube machinery, which supports deeper control over quality and lead time. From a service perspective, it provides feasibility support, engineering design, customization, installation, commissioning, validation assistance, documentation, training, and lifecycle support. Buyers interested in discussing project scope can use the U.S. project contact page to begin a technical conversation.
var ctxSup = document.getElementById(‘supplierChart’).getContext(‘2d’);var supplierChart = new Chart(ctxSup, {type: ‘bar’,data: {labels: [‘Regulatory Support’, ‘Turnkey Scope’, ‘Sterile Line Experience’, ‘Lifecycle Service’, ‘Automation Depth’, ‘Cost Efficiency’],datasets: [{label: ‘Integrated Engineering Supplier Score’,data: [91, 94, 89, 92, 88, 84],backgroundColor: ‘rgba(46, 204, 113, 0.75)’},{label: ‘Machine-Only Supplier Score’,data: [58, 42, 61, 47, 55, 79],backgroundColor: ‘rgba(231, 76, 60, 0.75)’}]},options: {responsive: true,maintainAspectRatio: false}});The supplier comparison chart shows why some U.S. buyers prefer integrated engineering partners. While machine-only vendors may appear cheaper initially, the broader support model can reduce project risk and improve long-term performance.
What is the biggest reason U.S. hospitals prefer non-PVC IV bags?The biggest reason is the combination of safety, compatibility, and workflow efficiency. Non-PVC bags can support more stable formulations and reduce bedside preparation steps.
Are non-PVC IV bags only for premium products?No. They are used in both standard and advanced applications. However, they are particularly valuable for sensitive drugs, nutrition products, and multi-component therapies.
Is a multi-chamber bag always better than a single-chamber bag?Not always. Multi-chamber designs are better for unstable combinations and hospital convenience, but single-chamber bags remain highly practical for standard fluids and lower-cost production.
What should a U.S. manufacturer check before buying a line?Check regulatory documentation, material compatibility experience, production references, sterilization strategy, validation support, spare parts planning, and service responsiveness.
How long does a non-PVC IV bag project usually take?Timelines vary by scope. A line expansion may move faster, while a greenfield facility with utilities, cleanrooms, validation, and product development takes much longer. Early engineering planning reduces delays.
Can one supplier handle the full project?Yes, if the supplier has turnkey capability. This often includes process design, equipment, water systems, logistics, installation, commissioning, and qualification support.
Why does service capability matter so much?Sterile production lines need reliable uptime. Training, remote support, spare parts, and technical troubleshooting all affect output and compliance.
What future trends will shape this market in 2026?The main trends are smart automation, digital quality systems, greater use of multi-chamber products, more sustainability focus, and stronger demand for secure U.S.-aligned supply chains.
In summary, non-PVC IV bags are becoming a central part of sterile pharmaceutical strategy in the United States. They help manufacturers build higher-value infusion products, help hospitals simplify administration, and help healthcare systems move toward safer, more efficient care. For companies planning new capacity, the winning approach is to think beyond the bag itself and invest in materials, line design, validation, and service support as one integrated system.
-
Syringe Packaging Machines for the United States Market
In the United States, a syringe packaging machine is a critical production asset for pharmaceutical and medical device companies that need sterile, traceable, and regulation-ready packaging for disposable syringes and prefilled syringes. It is used to place syringes into blister packs, pouches, trays, or secondary cartons while controlling cleanliness, labeling accuracy, sealing quality, and line efficiency. For manufacturers expanding capacity in New Jersey, Massachusetts, North Carolina, Indiana, Texas, or California, the right packaging system can directly affect FDA readiness, labor utilization, product protection during transport, and total cost per unit.
Demand in the U.S. market is being driven by biologics, injectable generics, vaccine supply chains, contract manufacturing expansion, and the continuing shift toward automation. Buyers are no longer evaluating only machine speed. They are also looking at line integration, digital batch records, validation support, cleanroom suitability, spare parts availability, and whether a supplier can support long-term factory upgrades. For firms planning new facilities or modernization projects, it is often valuable to compare standalone packaging equipment with broader line integration and turnkey engineering approaches. Companies seeking this broader view can review pharmaceutical engineering capabilities to understand how equipment choice fits into full production strategy.
A syringe packaging machine matters because it protects a sensitive sterile product at the last critical stage before distribution. In U.S. pharmaceutical and medical device operations, packaging is not just an appearance issue; it is a compliance, quality, and commercial issue. A weak seal, mislabeled lot code, or poorly designed infeed can trigger rejects, recalls, distribution delays, or failed audits. For that reason, large manufacturers and fast-growing CDMOs increasingly treat syringe packaging technology as a strategic investment rather than a simple end-of-line purchase.
In practice, these machines are used to package empty disposable syringes, sterile syringes, safety syringes, and prefilled syringes for injectable drugs. Depending on the product, the machine may perform automatic feeding, orientation, blister forming, pouch loading, heat sealing, printing, vision inspection, leaflet insertion, cartoning, serialization, and case packing. U.S. facilities operating under FDA cGMP expectations also require strong documentation, repeatable process control, changeover procedures, and validation support.
The packaging format depends on product sensitivity, target channel, and distribution model. Hospital products may prioritize robust protection and efficient secondary packaging. Specialty biologic products may prioritize barrier performance, tamper evidence, and traceability. High-volume commodity syringes may prioritize output speed and packaging cost. These differences explain why buyers in cities such as Newark, Philadelphia, Boston, Chicago, Indianapolis, and San Diego often request customized machine layouts rather than off-the-shelf solutions.
Decision AreaWhy It MattersTypical U.S. Buyer PriorityBusiness ImpactSeal IntegrityProtects sterile barrier and transport stabilityVery highLower risk of product damage and complaintsValidation SupportSupports IQ, OQ, and PQ activitiesVery highFaster qualification and audit readinessSerialization IntegrationImproves traceability and data captureHighBetter compliance and supply chain visibilityChangeover TimeImportant for multi-SKU productionHighHigher OEE and lower downtimeCleanroom CompatibilityNeeded for controlled production zonesVery highReduced contamination riskAfter-Sales ResponseEssential for uptime in busy plantsHighLower maintenance-related delaysThe table above shows why procurement teams in the United States often use cross-functional reviews involving engineering, quality assurance, operations, validation, and supply chain management before selecting a machine.
A syringe packaging machine is automated equipment designed to package syringes into a protective, saleable, and traceable format. In pharmaceutical production, it typically sits downstream from syringe forming, assembly, sterilization, washing, filling, stoppering, labeling, or inspection systems, depending on whether the syringes are empty medical consumables or prefilled drug products.
Its core functions include product handling, orientation, loading, primary packaging formation, sealing, coding, inspection, and transfer to secondary packaging. In blister applications, the machine may thermoform or cold-form cavities, place syringes into defined pockets, add lids or backing material, and seal under controlled parameters. In pouch applications, it may feed syringes into medical-grade pouches or peelable packaging and then heat-seal them for sterile presentation. More advanced lines include robotic loading, camera-based defect detection, leak testing, and automated cartoning.
In the U.S. market, common use cases include:
The machine is also used to improve consistency. Manual handling increases contamination risk, label errors, and operator fatigue. Automated packaging reduces variability and produces more predictable output, especially where product demand fluctuates. For U.S. manufacturers under pressure to shorten lead times and reduce labor dependency, this consistency is a major advantage.
FunctionDescriptionTypical Modules InvolvedOperational BenefitFeedingMoves syringes into the machine in correct orientationUnscrambler, conveyor, robotic pickerStable throughputFormingCreates blister cavities or pouch dimensionsThermoforming or pouch forming stationConsistent package shapeLoadingPlaces syringes into package safelyPick-and-place, servo loaderLower breakage and rejectsSealingSeals package materials under controlled heat and pressureHeat sealer, pressure stationReliable package integrityCodingAdds batch, date, and traceability dataPrinter, laser coderRegulatory and supply chain complianceInspectionChecks package presence, print quality, and defectsVision system, reject stationImproved quality assuranceThis table reflects the typical packaging workflow. For FDA-facing operations, each function must be designed not only for output but also for documented control and repeatability.
The main applications of syringe packaging machines in modern U.S. pharmaceutical manufacturing extend across medical consumables, biotech injectables, combination products, and contract packaging operations. Although the exact format varies, the objective is always the same: preserve product quality while enabling efficient logistics and market access.
One major application is prefilled syringe packaging for higher-value drug products. These products often require careful positioning, gentle transport inside the machine, and compatibility with labels, safety devices, and nested trays. Another application is sterile disposable syringe packaging for hospital, laboratory, and outpatient settings. In this segment, line speed and packaging cost matter more, but suppliers still need dependable seal integrity and consistent print quality.
Benefits go beyond automation. A well-selected machine can reduce product contact, improve visual presentation, lower the frequency of rework, support UDI or serialization programs, and simplify downstream packing. This is particularly important for manufacturers distributing across the wide U.S. geography, from East Coast life science corridors to West Coast biotech hubs and central logistics routes through Chicago, Memphis, and Dallas-Fort Worth.
Modern benefits usually include:
ApplicationTypical ProductBest Packaging FormatPrimary BenefitBiologicsPrefilled sterile syringesHigh-barrier blister or trayStrong product protectionVaccinesSingle-dose syringe packsBlister with cartonTraceability and transport stabilityHospital SupplyDisposable syringesPouch or bulk trayLower unit packaging costContract PackagingMulti-brand syringe productsFlexible blister and pouch formatsFast changeoversDiagnostic UseSpecialty syringes and kitsPouch with insertsAccessory integrationRetail Medical ChannelsConsumer-facing syringe productsBlister plus cartonShelf appearance and tamper evidenceThe table shows that the best machine design depends on the final market channel. A line optimized for bulk hospital distribution may not fit the needs of a high-value specialty injectable product sold through specialty pharmacy or cold-chain networks.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Biologics’, ‘Vaccines’, ‘Hospital Supply’, ‘CDMO Packaging’, ‘Diagnostics’, ‘Retail Medical’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [92, 84, 76, 88, 61, 57], backgroundColor: [‘#4e79a7′,’#59a14f’,’#f28e2b’,’#e15759′,’#76b7b2′,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The demand chart highlights how biologics, CDMO packaging, and vaccine-related applications continue to support stronger investment in syringe packaging equipment across the United States.
The two most common categories are blister pack machines and pouch packaging machines, but within those categories there are major technical differences. U.S. buyers should evaluate not only the package style but also indexing method, product handling system, sealing technology, material compatibility, and integration scope.
Blister machines are often selected where precise positioning, strong visibility, and high-quality presentation are required. They can be configured for rigid or semi-rigid cavities and may support lidding foils, medical papers, or plastic films. Pouch machines are often chosen for sterile disposable products, simpler line architectures, or lower initial capital budgets. Tray-based and nested packaging options are also common for prefilled syringe lines.
Important technical options include servo-driven transport, robotic loading, vision inspection, online printing, leak testing, reject tracking, recipe management, 21 CFR Part 11-compatible data handling, and integration with cartoners or case packers. In addition, suppliers may offer custom line layouts to fit restricted cleanroom footprints often found in retrofit projects around older pharmaceutical campuses in New Jersey and Pennsylvania.
Machine TypeBest ForTypical Speed RangeKey StrengthThermoform Blister MachineVisible retail or hospital packs60 to 300 packs/minPresentation and protectionCold-Form Blister MachineHigher barrier applications40 to 180 packs/minEnhanced barrier performanceMedical Pouch MachineSterile disposable syringes30 to 220 packs/minCost-effective sterile packagingTray Packing SystemPrefilled syringe nests or specialty packs20 to 120 trays/minGentle product handlingRobotic Flexible LineMulti-SKU operationsVariable by formatFast changeover flexibilityIntegrated Packaging LineLarge-scale automated plantsHigh throughputEnd-to-end control and traceabilityWhen comparing models, buyers should ask whether the quoted speed is a mechanical maximum or a validated production speed with actual syringe formats. This distinction often affects ROI calculations significantly.
Technical capability is especially important when machines must connect with broader production systems. Some suppliers offer only standalone equipment, while others support integrated factory engineering. Shanghai IVEN Pharmatech Engineering, for example, is known in the industry for combining packaging equipment with water systems, filling lines, intelligent conveying, and plant-wide engineering concepts. Organizations evaluating full production expansion can review turnkey pharmaceutical project solutions when the objective goes beyond a single machine purchase.
Choosing between a syringe packaging machine and alternative methods depends on volume, sterility needs, packaging appearance, labor cost, and regulatory expectations. Alternatives include semi-automatic pouch sealers, manual tray loading, bulk bagging systems, outsourced contract packaging, and older non-servo blister systems. Each has a place, but not every method is suitable for modern U.S. pharmaceutical manufacturing.
Semi-automatic or manual methods may work for pilot batches, low-volume specialty products, or early-stage development. However, they often struggle to maintain consistency at commercial scale. Bulk packaging can reduce packaging costs for internal transfers, yet it may not be acceptable for final distribution where traceability and presentation matter. Outsourcing can preserve capital, but it reduces direct control and may create scheduling constraints.
Automated syringe packaging machines typically make the most sense when a company has medium to high volume, multiple SKUs, or strict audit requirements. They are also valuable when labor markets are tight, as seen in many U.S. manufacturing centers where skilled operators and technicians remain difficult to recruit.
OptionCapex LevelLabor NeedCompliance StrengthBest FitAutomatic Blister LineHighLowVery strongCommercial pharma scaleAutomatic Pouch LineMedium to highLowStrongDisposable syringe productionSemi-Automatic SealerLow to mediumMedium to highModerateSmall batches and pilot workManual Tray LoadingLowHighWeak to moderateTemporary or niche useBulk BaggingLowLow to mediumLimitedInternal transfer or non-retail useOutsourced Contract PackagingLow direct capexVery low onsiteDepends on providerDemand uncertainty or launch phaseThe comparison table makes clear that the “best” solution depends on context. For a fast-growing CDMO near Raleigh-Durham or Indianapolis, flexible automated packaging may be ideal. For a startup launching a limited-volume specialty product, outsourcing or semi-automatic packaging may be more realistic initially.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Output Speed’, ‘Format Flexibility’, ‘Validation Readiness’, ‘Labor Savings’, ‘Unit Cost Efficiency’, ‘Scalability’], datasets: [ { label: ‘Automatic Blister’, data: [90, 72, 93, 88, 85, 91], backgroundColor: ‘#4e79a7’ }, { label: ‘Automatic Pouch’, data: [82, 79, 86, 84, 88, 83], backgroundColor: ‘#59a14f’ }, { label: ‘Semi-Automatic’, data: [38, 64, 51, 35, 48, 40], backgroundColor: ‘#f28e2b’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});This comparison chart shows why automatic blister and pouch systems remain the preferred commercial solutions for most regulated U.S. production environments.
The U.S. market for syringe packaging machines is supported by several long-term factors: expanding injectable drug pipelines, growth in biologics, increased domestic manufacturing attention, stronger supply chain resilience planning, and the need to replace aging packaging assets. States with major pharmaceutical and medical device activity, including New Jersey, California, Massachusetts, North Carolina, Illinois, Indiana, and Texas, continue to generate demand for both new lines and modernization projects.
Import logistics also influence buying decisions. Equipment shipped through the Port of Los Angeles, Port of Long Beach, Port of Savannah, Port Houston, or Port Newark may require different installation planning, spare parts stocking, and commissioning schedules. U.S. buyers increasingly want suppliers that can coordinate documentation, FAT/SAT planning, remote diagnostics, and on-site technical support efficiently.
Looking toward 2026 and beyond, several trends stand out:
Sustainability is becoming a more practical buying criterion. U.S. manufacturers are asking about material waste, compressed air usage, electricity consumption, change-part efficiency, and recyclable packaging options. Policy pressure and customer expectations are both pushing the market in this direction.
var ctxLine = document.getElementById(‘lineMarketChart’).getContext(‘2d’);var lineMarketChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [{ label: ‘Estimated U.S. Market Index for Syringe Packaging Equipment’, data: [100, 108, 117, 126, 138, 151, 165, 179], borderColor: ‘#e15759’, backgroundColor: ‘rgba(225,87,89,0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’], datasets: [ { label: ‘Manual or Legacy Packaging Share’, data: [42, 37, 32, 27, 22, 18, 14], fill: true, backgroundColor: ‘rgba(242,142,43,0.25)’, borderColor: ‘#f28e2b’, tension: 0.25 }, { label: ‘Automated Smart Packaging Share’, data: [58, 63, 68, 73, 78, 82, 86], fill: true, backgroundColor: ‘rgba(89,161,79,0.20)’, borderColor: ‘#59a14f’, tension: 0.25 } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The line and area charts illustrate the expected market direction: steady growth in overall demand and a continued shift from labor-heavy packaging methods toward automated, data-enabled systems.
A reliable supplier should be judged by more than brochure speed or price. In the United States, buyers should assess regulatory understanding, machine durability, integration capability, documentation quality, service responsiveness, and proof of successful installations. A strong supplier should be able to explain material compatibility, sealing validation, cleanroom design, spare parts strategy, FAT protocol, SAT support, and operator training in clear terms.
Technological capability is the first major filter. Look for suppliers that can offer servo control, stable product handling, inspection integration, and traceability features rather than basic mechanical movement alone. Manufacturing capability is the second filter. Suppliers with specialized production plants and established quality systems usually provide better consistency in fabrication, assembly, and testing. Service capability is the third filter. U.S. projects often succeed or fail based on installation planning, validation support, training, and post-startup troubleshooting.
Shanghai IVEN Pharmatech Engineering is one example of a supplier that positions itself around integrated pharmaceutical and medical device engineering rather than isolated machine sales. Its broader portfolio includes packaging, filling, water treatment, intelligent conveying, and blood collection tube equipment, which can be relevant when a buyer plans a larger plant upgrade. For product and equipment scope, buyers can review the company’s pharmaceutical equipment portfolio in relation to their own line strategy.
Supplier Evaluation PointWhat to AskWhy It MattersGood SignRegulatory ExperienceDo you support FDA-oriented projects?Ensures documentation and compliance fitClear validation and cGMP referencesEngineering DepthCan you customize layouts and interfaces?Important for retrofit plantsStrong design team and examplesManufacturing BaseHow are machines built and tested?Indicates quality consistencyDedicated factories and FAT processAfter-Sales SupportWhat is your response time and spare parts plan?Protects uptimeStructured service systemProject ReferencesCan you show similar syringe projects?Reduces execution riskRelevant installations and case historyTotal Integration AbilityCan you support upstream and downstream systems?Useful for expansion projectsTurnkey or line-integration capabilityFor U.S. buyers, local representation or responsive remote support can also be decisive. Time zone differences, spare parts lead times, and training needs should be addressed before purchase order signing, not after the machine arrives at site.
Case-study thinking helps. A pharmaceutical company upgrading an injectable line in New Jersey may prioritize documentation, footprint optimization, and serialization integration. A medical consumables producer near Houston may focus more on throughput and packaging cost. A new biotech facility in the Boston-Cambridge corridor may value validation readiness and gentle robotic handling above all else. The best supplier is the one whose capabilities match your plant’s real constraints.
The investment cost for a syringe packaging machine in the United States varies widely based on format, speed, automation level, inspection scope, data systems, and facility requirements. A basic semi-automatic configuration may involve a relatively low capital commitment, while a fully integrated high-speed blister line with robotic loading, vision inspection, cartoning, and serialization can require a significant multi-million-dollar investment.
Budget planning should cover more than the machine price. Buyers should include tooling, factory acceptance testing, shipping, import handling, installation, cleanroom preparation, validation, spare parts, training, utility connections, and any integration work with MES, printers, labelers, or cartoners. Costs can also be affected by plant location. Facilities in high-cost regions such as Greater Boston, the San Francisco Bay Area, or parts of New Jersey may face higher installation and qualification expenses than sites in some central states.
Cost ElementLow Complexity LineMid Complexity LineHigh Complexity LineBase Machine$120,000 to $300,000$300,000 to $850,000$850,000 to $2,500,000+Tooling and Format Parts$10,000 to $25,000$25,000 to $80,000$80,000 to $200,000Inspection and Coding$15,000 to $40,000$40,000 to $120,000$120,000 to $300,000Installation and Commissioning$20,000 to $50,000$50,000 to $150,000$150,000 to $400,000Validation Support$10,000 to $35,000$35,000 to $100,000$100,000 to $250,000Annual Spare Parts and Service Reserve$8,000 to $20,000$20,000 to $60,000$60,000 to $150,000The table provides directional budgeting rather than fixed pricing. Actual project values depend on configuration, supplier, compliance scope, and installation model.
ROI is usually driven by labor savings, reduced reject rates, lower rework, improved packaging speed, and increased line availability. If a plant replaces a manual or semi-automatic process with a properly sized automatic line, payback may be achieved in two to five years depending on volume and product mix. For prefilled syringe products with high unit value, the ROI can be even faster if the machine materially lowers packaging defects or protects launch timelines.
ROI DriverExample ImpactHow to MeasureStrategic ValueLabor Reduction2 to 6 fewer operators per shiftAnnual wage savingsHighHigher Throughput20% to 80% more outputUnits per hourHighLower RejectsFewer seal and coding errorsScrap and rework rateHighAudit ReadinessStronger data and traceabilityDeviation reductionMedium to highProduct ProtectionLess transit damageComplaint and return rateMediumCapacity ExpansionSupports new contracts or SKUsRevenue growth potentialVery highTo improve investment confidence, companies often model best-case, base-case, and conservative scenarios. This is especially useful when demand forecasts depend on future product approvals, CDMO contracts, or public procurement volumes.
The biggest investment risks usually come from specification gaps, underestimating validation demands, poor format compatibility, and weak service planning. A machine that looks efficient on paper may become a bottleneck if it cannot reliably handle real syringe tolerances, safety devices, labels, or future packaging materials.
Another common risk is choosing for speed alone. High output matters, but only if the line remains stable across normal operating conditions. A slightly slower machine with better OEE, easier maintenance, and faster changeovers may outperform a faster but unstable system over the course of a year.
Buyers should also consider cleanroom logistics, operator ergonomics, line clearance procedures, and spare parts stocking. U.S. plants operating around the clock cannot afford long waits for critical components. Projects importing equipment through coastal ports should include realistic time buffers for inland transport, customs coordination, and utility readiness.
Service capability is where many projects succeed. Suppliers that provide installation, commissioning, training, documentation, and lifecycle optimization reduce launch risk substantially. IVEN is recognized by many buyers for emphasizing this broader service approach, including engineering support, equipment customization, commissioning, qualification assistance, and operator training across pharmaceutical projects. Companies that want to discuss plant-specific requirements can use the supplier’s project consultation contact channel to evaluate fit early.
RiskTypical CausePossible ConsequenceMitigationFormat MismatchInsufficient sample testingFrequent jams and rejectsRun FAT with real productsWeak DocumentationSupplier lacks regulated project depthValidation delaysReview document list before contractHidden Installation CostsIncomplete scope definitionBudget overrunsBuild full landed-cost modelService DelaysNo spare parts or poor support planExtended downtimeDefine service SLA and parts listMaterial IncompatibilityUnverified film or pouch specsPoor sealing or wasteConduct sealing trials earlyFuture InflexibilityMachine sized for only one formatEarly obsolescenceChoose modular design and recipesThis table underscores a simple principle: the purchase decision should be based on total project readiness, not machine headline speed alone.
From an operational perspective, it is wise to involve production, QA, validation, maintenance, and supply chain teams in the buying process. That cross-functional approach usually reveals issues earlier, such as packaging material approvals, code verification standards, or pallet configuration requirements for U.S. distributors and healthcare networks.
What is the difference between a blister syringe packaging machine and a pouch syringe packaging machine?A blister machine forms a cavity that holds the syringe in a defined shape, offering strong presentation and protection. A pouch machine seals the syringe inside flexible material, often with lower packaging cost and a simpler line configuration. The best choice depends on the product, sterility presentation, and distribution channel.
Is a syringe packaging machine used only for prefilled syringes?No. It can be used for empty disposable syringes, sterile syringes, safety syringes, and prefilled syringes. The product type affects handling design, packaging material, and compliance requirements.
How important is FDA-related documentation when buying equipment in the United States?It is very important. Even if the machine itself is not “FDA approved,” the supplier should support cGMP-oriented documentation, validation activities, traceability, and repeatable process control suitable for U.S. regulated environments.
What throughput should a buyer expect?That depends on the package format, syringe dimensions, loading method, and inspection scope. Commercial lines can range from tens of packs per minute to several hundred. Always ask for proven production speed with your actual product configuration.
How long does implementation usually take?A simple machine may be delivered and started within several months, while a fully integrated custom line may require a longer engineering, FAT, shipping, installation, SAT, and validation schedule. For U.S. facilities, utility readiness and internal qualification timelines often influence the total project duration as much as machine manufacturing does.
Should U.S. companies buy a standalone machine or a wider integrated system?If the need is limited to replacing one packaging asset, a standalone machine may be enough. If the project involves a new injectable plant, broader automation, utilities, or multiple connected processes, an integrated solution can reduce coordination risk and improve long-term consistency.
What should I ask a supplier before requesting a quotation?Prepare information on syringe size, material, sterility level, packaging format, target speed, coding needs, cleanroom classification, utility conditions, validation expectations, and planned future SKUs. The better the input, the more accurate and useful the quotation.
Why do large companies often evaluate suppliers with engineering depth?Because packaging equipment rarely operates in isolation. It must fit plant layout, utility planning, data systems, QA procedures, operator flow, and future expansion. Suppliers with strong engineering depth can reduce integration mistakes and support smoother project delivery.
For companies serving the United States market, the best syringe packaging machine is the one that balances product protection, compliance, operational efficiency, and lifecycle support. Whether the requirement is a pouch line for disposable syringes or a more advanced blister system for prefilled injectables, careful supplier evaluation and realistic project planning remain the keys to a successful investment.
-
Automatic Cartridge Filling Lines in the United States
For pharmaceutical and medical device manufacturers in the United States, an automatic cartridge filling line is a high-value production system used to fill, stopper, inspect, and package cartridges with tight dosing accuracy under regulated cleanroom conditions. It is commonly evaluated when companies expand sterile production, launch dental or injectable products, improve throughput, or upgrade facilities to align with US FDA cGMP expectations, data integrity requirements, and long-term automation goals.
In practice, these lines are most relevant for organizations producing injectable drugs, dental anesthetic cartridges, biologics, high-value specialty formulations, and combination products that require repeatable filling, low product loss, traceability, and validated performance. In U.S. markets such as New Jersey, Massachusetts, North Carolina, California, Illinois, and Texas, investment decisions are often tied to capacity planning, contract manufacturing demand, and facility modernization near major logistics gateways including the Port of Los Angeles, Port of Long Beach, Port of New York and New Jersey, and the Port of Savannah.
An automatic cartridge filling line is a fully or semi-automated production line designed to process empty cartridges through a sequence of operations that may include feeding, washing or decontamination where applicable, siliconization if needed, sterile filling, stopper insertion, capping, visual inspection, labeling, tray loading, and final packaging. In pharmaceutical settings, it supports high-speed, highly controlled filling of liquid or semi-liquid products into cartridge formats used for injection systems, pen injectors, dental applications, and selected medical device assemblies.
For large manufacturers in the United States, the technology matters because it directly affects batch consistency, labor efficiency, contamination control, validation workload, and product release speed. Compared with more manual or fragmented workflows, a modern automatic cartridge filling line can improve overall equipment effectiveness, reduce operator intervention, and create a more robust path to compliance with US FDA cGMP, 21 CFR Part 11 expectations for electronic records where implemented, and broader global standards when exports are planned.
Buyers typically assess the equipment not only as a machine, but as part of an integrated sterile manufacturing strategy. That is why facility layout, HVAC interaction, isolator or RABS configuration, CIP/SIP requirements, batch documentation, line clearance procedures, changeover time, and downstream packaging compatibility all influence the final procurement decision.
Decision FactorWhy It MattersTypical U.S. Buyer PriorityRegulatory fitSupports validation, audit readiness, and documentationVery highFilling accuracyProtects dosage consistency and yieldVery highSterility assuranceReduces contamination risk in aseptic operationsVery highScalabilityAllows future capacity expansionHighChangeover speedImportant for multi-product facilities and CDMOsHighService supportReduces downtime and speeds qualificationHighThe table above shows why U.S. buyers rarely choose on purchase price alone. Long-term operational fit usually outweighs the lowest upfront bid.
An automatic cartridge filling line is a specialized filling and finishing solution engineered for cartridge-based drug delivery or medical use. Depending on the product and regulatory classification, the line may handle glass cartridges, polymer cartridges, nested formats, bulk-fed formats, and ready-to-fill components. It is used when manufacturers need precise fill volumes, protected aseptic handling, minimal human contact, and repeatable downstream processing.
Common uses include dental anesthetic production, injectable therapies for pen systems, biologic formulations, hormone products, local anesthetics, and specialty formulations used in controlled-dose delivery systems. In U.S. production environments, it may also be considered for contract manufacturing organizations serving multiple brand owners that want flexible lot sizes and documented repeatability.
The line is usually composed of several modules. A basic system may include cartridge feeding, orientation, filling, stopper placement, crimping or sealing, reject handling, and outfeed. More advanced configurations add in-line weight checks, nitrogen purging, vacuum filling, camera inspection, robotic transfer, serialization integration, and automatic packaging interfaces.
Line ModuleMain FunctionOperational BenefitInfeed and orientationFeeds empty cartridges in controlled sequenceReduces jams and supports stable cycle timesFilling stationDispenses exact liquid volumeImproves dose accuracy and yieldStopperingPlaces plunger or stopper correctlySupports closure integrityCapping or sealingSecures the final closureProtects product during storage and transportInspectionDetects fill, cosmetic, or closure defectsImproves quality assurancePackaging interfaceTransfers accepted units downstreamCreates continuous line flowFor companies planning a broader sterile project, the cartridge line often connects with utilities, purified water systems, solution preparation, logistics, and packaging automation. Manufacturers looking for integrated project support often review turnkey engineering capabilities alongside the equipment itself. This is one reason some buyers study partners that can combine process equipment, utility systems, and plant planning under one scope, as described on integrated turnkey pharmaceutical engineering solutions.
The main applications of automatic cartridge filling lines center on sterile and high-value filling operations where precision and containment are critical. In the United States, the strongest demand often comes from injectable drug producers, biologics developers, dental pharmaceutical manufacturers, and medical device firms commercializing cartridge-compatible delivery systems.
Operationally, the benefits can be significant. Automated filling reduces dependency on manual intervention, improves batch reproducibility, and supports cleaner, more auditable processes. This is especially valuable in regions with high labor costs and strict compliance oversight, such as Boston, Philadelphia, Raleigh-Durham, Indianapolis, and the San Francisco Bay Area. Companies in these clusters also tend to value data capture, recipe control, and integration with MES or plant-level digital systems.
Another major advantage is reduced product loss. Many cartridge-filled drugs are expensive, sensitive, or both. Accurate pumps, low dead volume design, and optimized product path geometry help preserve yield. For high-potency or specialized formulations, that can materially improve cost per batch.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Injectables’, ‘Dental Pharma’, ‘Biologics’, ‘CDMO Services’, ‘Medical Devices’, ‘Specialty Drugs’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [92, 71, 88, 80, 67, 76], backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});Application AreaTypical Product TypePrimary BenefitDental cartridgesLocal anestheticsFast, repeatable filling at commercial scalePen injector cartridgesHormones or specialty injectablesDosing precision and compatibility with device assemblyBiologicsSensitive formulationsGentle product handling and controlled environmentContract manufacturingMulti-client productionFlexible formats and batch traceabilityHospital supply productsSterile injectablesReliable throughput and quality consistencyCombination productsDrug-device systemsIntegration with downstream medical assemblyThe chart and table together show that demand is not limited to one niche. Cartridge filling is increasingly linked to device-enabled drug delivery, which makes automation more strategic than a simple packaging upgrade.
There is no single best automatic cartridge filling line for every plant. Selection depends on product characteristics, batch sizes, sterility strategy, container format, and expansion plans. Broadly, systems can be grouped into semi-automatic, fully automatic, compact modular, high-speed integrated, and isolator-based lines.
Semi-automatic models are often used for development, pilot, or low-volume specialty production. Fully automatic lines are preferred for commercial pharmaceutical manufacturing where throughput and traceability matter most. Modular systems are attractive for U.S. companies that want phased investment, while high-speed lines suit established manufacturers with strong forecast volume.
Technical options also vary widely. Buyers may select peristaltic pumps for easy product path changeover, piston pumps for high repeatability in certain applications, or time-pressure systems for specific formulation behavior. Other options include vacuum stoppering, no-container-no-fill logic, vision systems, servo control, robotic loading, isolators, RABS, nitrogen overlay, and automated rejection stations.
Type or OptionBest FitStrengthSemi-automatic lineR&D, pilot, niche batchesLower entry cost and flexibilityFully automatic lineCommercial manufacturingHigher throughput and lower labor dependencyIsolator-based lineHigh sterility assurance needsReduced contamination riskRABS configurationControlled aseptic operationsBalanced access and protectionServo-driven fillingPrecision applicationsBetter repeatability and recipe controlVision inspection integrationQuality-focused plantsAutomated defect detectionRobotic handlingAdvanced facilitiesImproved transfer consistencyOne useful buying principle is to match line complexity to the plant’s real needs. Over-specifying a line can increase validation burden, spare part inventory, and training time. Under-specifying it may create bottlenecks or compliance gaps within two to three years.
Before purchasing, many U.S. manufacturers compare cartridge filling lines with vial filling lines, prefilled syringe lines, manual or bench-scale fillers, and outsourced contract filling. The right answer depends on your delivery platform, commercial model, and regulatory strategy.
If your product is intended for cartridge-based delivery devices or dental systems, a dedicated automatic cartridge filling line usually offers the best process fit. Vial lines provide broader market flexibility but do not directly support cartridge closure and downstream compatibility. Prefilled syringe lines are ideal for ready-to-inject presentations but come with their own component and device requirements. Outsourcing may be practical for early-stage launches, though it can reduce process control and limit scheduling flexibility.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Format Compatibility’, ‘Throughput’, ‘Flexibility’, ‘CAPEX Efficiency’, ‘Sterile Control’, ‘Device Integration’], datasets: [ { label: ‘Automatic Cartridge Line’, data: [95, 84, 76, 72, 90, 96], backgroundColor: ‘#6f42c1’ }, { label: ‘Vial Filling Line’, data: [48, 86, 88, 70, 89, 42], backgroundColor: ‘#17a2b8’ }, { label: ‘Contract Filling’, data: [65, 60, 82, 90, 68, 58], backgroundColor: ‘#fd7e14’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});SolutionBest Use CaseMain LimitationAutomatic cartridge filling lineDedicated cartridge products at scaleHigher initial capital investmentVial filling lineBroad injectable portfolioNot optimized for cartridge formatPrefilled syringe lineReady-to-administer productsDifferent component and device ecosystemManual or semi-manual fillerDevelopment or very small batchesLimited throughput and consistencyContract manufacturingFast market entry with low CAPEXLess direct control over schedule and processHybrid internal plus outsourced modelTransition phase during ramp-upMore complex supply coordinationThis comparison shows that the “best” technology is tied to business model. For companies building long-term U.S. supply capacity, owning a validated cartridge line often becomes more attractive once forecast demand stabilizes.
The U.S. market for automatic cartridge filling line technology is supported by several structural drivers: growth in injectable therapies, increased use of device-based drug delivery, reshoring and nearshoring interest, modernization of legacy sterile facilities, and stronger demand for digital manufacturing controls. Pharmaceutical clusters in New Jersey, Maryland, Indiana, and North Carolina continue to attract expansion projects, while West Coast innovation hubs contribute new biologic and specialty delivery formats.
Market competition includes established European suppliers, selected North American integrators, and international engineering companies that compete on technical customization and project value. Buyers are increasingly asking for more than equipment. They want line integration, validation support, documentation packages, FAT/SAT planning, and the ability to align the equipment with utility systems and cleanroom design.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Market Index’, data: [100, 108, 119, 131, 145, 161], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [ { label: ‘Legacy Standalone Systems’, data: [64, 59, 53, 46, 40, 34], fill: true, backgroundColor: ‘rgba(220, 53, 69, 0.20)’, borderColor: ‘rgba(220, 53, 69, 1)’, tension: 0.25 }, { label: ‘Integrated Smart Aseptic Lines’, data: [36, 41, 47, 54, 60, 66], fill: true, backgroundColor: ‘rgba(40, 167, 69, 0.20)’, borderColor: ‘rgba(40, 167, 69, 1)’, tension: 0.25 } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});Looking toward 2026, future trends are clear. First, smart automation will grow through servo control, recipe management, machine vision, and predictive maintenance. Second, policy pressure around supply chain resilience may encourage more domestic capacity in the United States. Third, sustainability will matter more, pushing buyers toward lower utility consumption, efficient compressed air design, reduced reject rates, and longer-life stainless steel equipment. Fourth, modular manufacturing concepts will expand because they shorten project timelines and simplify phased capacity growth.
These trends also favor suppliers that can align equipment with broader plant engineering. U.S. buyers increasingly ask whether a manufacturer can support not just the filler, but process water, layout optimization, warehousing links, and packaging connectivity.
Choosing a supplier for an automatic cartridge filling line in the United States should begin with technical fit, but it must end with lifecycle reliability. A line that performs well during factory acceptance testing but lacks documentation quality, spare support, or commissioning depth can create expensive delays during qualification.
Start by reviewing the supplier’s track record in regulated pharma and medical device environments. Ask for examples of cartridge, aseptic, or filling projects comparable to your product. Verify whether the company understands US FDA cGMP expectations and whether its documentation package supports IQ, OQ, and PQ execution. Review component brands, software architecture, alarm management, and access control logic.
It is also useful to examine three capability areas: technological capabilities, manufacturing capabilities, and service capabilities. On the technology side, some engineering companies offer strong experience in filling, packaging, process utilities, and automated logistics, allowing better line-to-plant coordination. On the manufacturing side, multi-plant production capacity and standardized fabrication can improve lead-time control and customization quality. On the service side, the best partners provide feasibility consulting, engineering design, installation, commissioning, validation support, operator training, and long-term after-sales response.
For buyers exploring suppliers with broad pharmaceutical project experience, it can be helpful to review a company background page such as the pharmaceutical engineering profile here and then compare that information against your own URS, FAT criteria, and compliance priorities.
Supplier Evaluation ItemWhat to CheckWarning SignRegulatory experienceExperience with cGMP and validation documentsGeneric documents not tailored to pharmaEngineering depthAbility to customize around process needsOnly offers standard machine catalog modelsManufacturing qualityMaterial finish, welding, assembly consistencyPoor finish records or unclear QA processAutomation architectureUser access, data capture, alarm historyLimited software transparencyAfter-sales supportRemote help, parts, field service, trainingSlow response or no U.S.-oriented support planProject managementClear milestones and communication structureUncertain delivery dates and weak coordinationIf you are narrowing down vendors, request a detailed proposal with throughput assumptions, utility requirements, change parts list, FAT scope, documentation list, and estimated spare parts package. You may also want to contact the supplier directly through its project consultation channel to clarify lead times, service response, and application fit for the U.S. market.
Investment cost varies significantly based on speed, sterility concept, automation level, inspection modules, and line integration scope. In the United States, a compact semi-automatic solution may fit a lower budget, while a fully integrated aseptic automatic cartridge filling line with isolator, robotic handling, inspection, and packaging interface can represent a major capital project.
Budget planning should include more than machine price. Companies often underestimate facility modifications, cleanroom adaptation, utilities, validation labor, training, spare parts, shipping, customs, and startup batches. For imported systems entering through U.S. gateways such as Los Angeles, Houston, Newark, or Savannah, freight planning and on-site installation sequencing also affect total cost.
Cost CategoryTypical Share of Project BudgetNotesCore equipment45% to 60%Main line modules, controls, format partsIsolator or RABS10% to 20%Depends on sterility strategyInspection and automation upgrades5% to 12%Vision systems, data integration, checkweighingInstallation and commissioning6% to 10%On-site mechanical and electrical workValidation and documentation5% to 10%IQ/OQ support, protocol adaptation, recordsSpares and training3% to 6%Recommended for first-year stabilityFacility adaptation8% to 18%Utilities, cleanroom changes, layout revisionsROI usually comes from five channels: higher throughput, reduced labor, lower reject rates, reduced product loss, and stronger compliance readiness. For a manufacturer moving from semi-manual filling to a validated automatic line, payback can be accelerated if existing demand is constrained by labor or if the product has high margin.
ROI DriverImpact on Financial PerformanceTypical Time HorizonThroughput increaseMore saleable units per shiftImmediate to 12 monthsLabor reductionLower direct operating cost6 to 24 monthsReject reductionLess wasted material and reworkImmediate to 18 monthsYield improvementBetter recovery of expensive productImmediate to 12 monthsDowntime controlHigher line availability6 to 24 monthsCompliance confidenceLower risk of delays and deviationsLong-term strategic valueAs a rough rule, U.S. buyers should model best-case, base-case, and conservative scenarios. Include utilization rate, staffing assumptions, changeover frequency, market demand volatility, and maintenance costs. That produces a more realistic business case than a simple units-per-minute comparison.
The main risks in purchasing an automatic cartridge filling line are rarely mechanical alone. The bigger problems are often scope gaps, poor format compatibility, weak validation preparation, unrealistic lead times, and insufficient service planning. For a U.S. buyer, the most costly mistake is choosing a line that technically runs but operationally does not fit the product, facility, or compliance model.
First, confirm product compatibility. Viscosity, foaming, oxygen sensitivity, and closure behavior all affect filling performance. Second, confirm container and component tolerances. Cartridge variation can create jams, rejects, or closure issues. Third, assess utility and cleanroom interfaces early. Fourth, validate software expectations, especially where electronic records or line data must integrate into existing plant systems.
It is also smart to review spare parts strategy and local service responsiveness. If your plant runs in a high-demand market like New Jersey or California, even a short unplanned shutdown can disrupt supply commitments. Ask whether critical parts can be stocked in the United States and how quickly field engineers or remote specialists can respond.
From a broader project perspective, some buyers prefer suppliers that can support multiple systems beyond the filler itself. Companies that also work in pharmaceutical water treatment, intelligent conveying, packaging, and plant engineering may reduce coordination risk during expansion. If you want to compare equipment categories beyond cartridges, a broader equipment listing such as pharmaceutical machinery solutions can help frame line integration decisions.
A practical case example is a mid-sized sterile manufacturer expanding into cartridge-based specialty products in the Midwest. The company initially planned to retrofit a vial area with minimal changes. During design review, it discovered that HVAC pressure cascades, material flow, and line clearance space would compromise operations. After revising the layout and selecting a modular line with future inspection expansion, the plant avoided a costly revalidation cycle and preserved room for growth. The lesson is simple: equipment purchasing should be tied to facility engineering from the start.
What production speed is considered normal for an automatic cartridge filling line?Normal speed depends on cartridge size, filling accuracy requirements, product behavior, and line design. Pilot and specialty lines may run at lower speeds, while commercial systems can achieve much higher output with stable upstream and downstream integration.
Is an automatic cartridge filling line always required for U.S. FDA-regulated production?Not always. Smaller operations may begin with lower automation. However, once output, consistency, and aseptic control become critical, automation is often the more sustainable choice for commercial manufacturing.
Can one line handle multiple cartridge sizes?Yes, many systems are designed for multiple formats through change parts and recipe settings. The key is to confirm validated changeover procedures and expected downtime between formats.
How long does qualification usually take?The timeline varies with project scope, documentation readiness, FAT quality, and facility preparation. Buyers should plan for engineering review, installation, SAT, IQ, OQ, training, and process validation activities rather than focusing on machine delivery date alone.
What should U.S. buyers ask during supplier audits?Ask about material traceability, software control, quality inspection, spare parts policy, documentation standards, prior regulated projects, and post-installation support structure.
How important is turnkey capability?It can be very important when the cartridge line is part of a larger sterile or medical device expansion. Turnkey coordination may reduce interface risk among utilities, cleanrooms, logistics, and packaging.
What role does our company play in this market?For U.S. buyers seeking a partner rather than only a machine builder, Shanghai IVEN Pharmatech Engineering Co Ltd brings relevant strengths in three areas. In technological capabilities, it has long experience in pharmaceutical filling and packaging systems, water treatment, intelligent conveying, and integrated engineering under international compliance frameworks. In manufacturing capabilities, it operates specialized production plants dedicated to core equipment categories and has supplied thousands of production lines globally. In service capabilities, it supports feasibility analysis, engineering design, customization, installation, commissioning, validation assistance, training, and lifecycle support. This combination can be valuable for companies planning a cartridge filling project as part of a larger plant modernization or new facility build.
How should a U.S. company start the buying process?Start with a detailed user requirement specification covering product, cartridge format, speed, sterility approach, utilities, compliance needs, and expansion goals. Then compare suppliers on lifecycle value, not just quote price.
In summary, an automatic cartridge filling line is no longer a narrow specialty purchase. In the United States, it is increasingly a strategic manufacturing asset for regulated producers that need speed, precision, traceability, and long-term flexibility. The best investment decisions align product requirements, facility design, digital controls, and supplier support into one clear expansion roadmap.