Syringe Production Lines in the United States Market
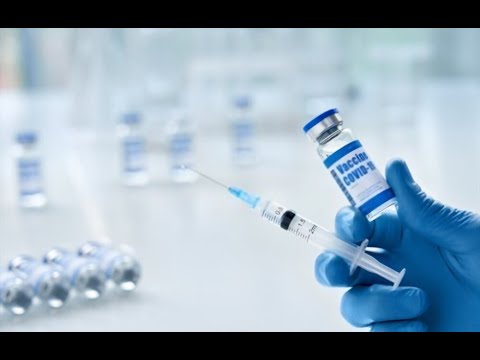
For large pharmaceutical and medical device manufacturers, a syringe production line for medical use is a strategic investment used to expand output, improve sterility assurance, automate traceability, and meet strict regulatory expectations in the United States. It is not just a machine set; it is a complete manufacturing system that supports molding, assembly, needle integration, printing, siliconization, inspection, packaging, and validated quality control under cGMP-driven operations.
In the U.S. market, this type of production line is increasingly evaluated by companies operating in injectable drugs, contract manufacturing, vaccination programs, hospital supply chains, and disposable medical consumables. Buyers in Boston, New Jersey, Chicago, Houston, San Diego, and the broader life sciences corridors often compare throughput, cleanroom compatibility, automation level, data integrity, and long-term service support before making a purchasing decision.
When planning a new plant or modernization project, manufacturers also look beyond single equipment performance. They assess line integration, utility consumption, changeover flexibility, validation readiness, supplier credibility, and how the line fits future demand for safety syringes, prefillable systems, and smart manufacturing. Companies that need broader project support often prefer suppliers capable of integrated engineering and turnkey execution. For example, IVEN Pharmatech Engineering presents itself as a pharmaceutical and medical device engineering partner with experience in complete production lines and factory-wide solutions. Buyers researching full-project support can review its company background and broader engineering approach as part of supplier comparison.
Quick Answer: Why a Syringe Production Line for Medical Use Matters

A syringe production line for medical use is a specialized manufacturing system designed to produce sterile or non-sterile disposable syringes and related components at industrial scale. In pharmaceutical production and medical device manufacturing, it helps companies maintain consistent product quality, reduce manual handling, increase throughput, and strengthen compliance with FDA expectations, ISO standards, and audit requirements.
In practical terms, these lines are used to produce insulin syringes, standard disposable syringes, safety syringes, irrigation syringes, and prefilled syringe components. Depending on the project scope, a line may include injection molding interfaces, barrel and plunger assembly, gasket insertion, needle attachment, lubrication or siliconization, automatic visual inspection, leak testing, blister packing, carton packing, serialization, and warehouse logistics connectivity.
In the United States, demand is shaped by hospital procurement pressure, public health preparedness, domestic supply chain resilience, and the need for high-precision drug delivery systems. As a result, many manufacturers prefer production lines that can support 21 CFR Part 11-compliant records, electronic batch traceability, vision inspection, and modular expansion.
| Production Area | Main Function | Typical Equipment | Compliance Focus | Business Value |
|---|---|---|---|---|
| Component Feeding | Automatic supply of barrels, plungers, gaskets, and needles | Hoppers, bowl feeders, conveyors | Material identification | Reduces manual errors |
| Assembly | Combines syringe parts in correct sequence | Assembly stations, servo modules | Process consistency | Improves output uniformity |
| Needle Integration | Attaches fixed or detachable needles | Needle mounting modules | Dimensional accuracy | Ensures patient safety |
| Lubrication | Applies silicone where needed | Micro-dosing units | Validated dosing control | Supports smooth plunger movement |
| Inspection | Checks defects, leakage, print quality | Vision systems, leak testers | Data integrity | Lowers rejection risk |
| Packaging | Protects and identifies final product | Blister packers, cartoners | Labeling accuracy | Supports distribution readiness |
The table above shows why buyers should see the line as a complete process chain rather than isolated machines. A weak inspection or packaging stage can undermine the value of a high-speed assembly section.
What Is a Syringe Production Line for Medical Use and What Is It Used For in Pharmaceutical Production?

A syringe production line for medical use is a coordinated set of machines and controls used to manufacture disposable syringes or prefillable syringe-related products under regulated conditions. It may serve pharmaceutical companies, device manufacturers, or contract manufacturers producing products for hospitals, clinics, diagnostics firms, and vaccination networks.
Its uses in pharmaceutical production depend on the product type. Some lines are focused on empty sterile syringes for later filling. Others are part of a prefilled syringe platform, where the syringe becomes a primary drug container for biologics, vaccines, anticoagulants, or emergency injectables. In this case, dimensional precision, low particulate generation, and packaging integrity become especially important.
In the United States, applications often align with regional industry strengths. New Jersey and Pennsylvania support major injectable and packaging operations. Massachusetts and California drive innovation in biotech delivery formats. Texas and the Midwest provide logistics advantages and growing domestic manufacturing footprints. Ports such as Los Angeles, Long Beach, Savannah, and New York/New Jersey also influence how imported equipment is installed and serviced across national supply chains.
For companies planning expansion, the line is commonly linked with clean utilities, compressed air, purified water systems, HVAC, cleanroom design, and digital manufacturing software. Suppliers with cross-disciplinary engineering capability can simplify this integration. IVEN, for instance, is known not only for product-line equipment but also for water treatment, distribution systems, filling and packaging technologies, and intelligent logistics. That matters when a syringe line must connect to broader factory systems rather than operate as a stand-alone asset.
| Use Case | End Product | Typical Buyer | Key Requirement | Risk if Under-Specified |
|---|---|---|---|---|
| Disposable syringe production | Standard sterile syringes | Medical consumables factory | High-speed assembly | Low throughput |
| Safety syringe production | Needlestick protection devices | Hospital supply manufacturer | Precise mechanism assembly | Safety failure |
| Insulin syringe production | Fine-dose syringes | Diabetes device company | Dimensional precision | Dosing inconsistency |
| Prefillable components | Drug-ready syringe bodies | Pharma packaging supplier | Particle control | Container closure issues |
| Irrigation syringes | Larger-volume devices | Procedure supply firm | Format flexibility | Frequent changeover losses |
| OEM contract production | Private-label syringes | CDMO or OEM | Traceability and fast changeover | Audit exposure |
This breakdown helps U.S. buyers define whether they need a line optimized for volume, versatility, sterility, or premium device performance.
Main Applications and Benefits of Syringe Production Lines in Modern Pharmaceutical Manufacturing

The primary applications of a syringe production line for medical use include large-scale output of disposable syringes, support for pharmaceutical packaging platforms, and secure production of medical consumables used in hospital and public health systems. The benefits, however, go beyond production speed.
First, automation improves consistency. A validated line minimizes variation in assembly force, needle position, gasket fit, and lubrication quantity. Second, it improves compliance readiness through automatic counting, alarm history, recipe management, and digital records. Third, it reduces labor dependence, which is important in U.S. regions facing skilled operator shortages. Fourth, integrated vision inspection can identify cosmetic and functional defects earlier, reducing downstream waste.
There is also a strategic supply-chain benefit. Since 2020, many U.S. manufacturers and healthcare buyers have prioritized resilient local production over sole dependence on imported consumables. A domestic syringe manufacturing line can support federal contracting opportunities, state emergency stockpiles, and long-term agreements with group purchasing organizations.
From a technical capability perspective, advanced suppliers stand out by offering automation integration, process customization, and regulatory-oriented design. IVEN’s engineering positioning is relevant here: it has experience in pharmaceutical filling, packaging, water treatment, logistics systems, and medical consumables equipment, which suggests a broader ability to support plant-level coordination rather than only machine shipment. For firms comparing technology depth, that wider engineering scope is often a deciding factor.
| Benefit | Operational Impact | Quality Impact | Financial Impact | Best Fit Scenario |
|---|---|---|---|---|
| Higher automation | Less manual intervention | Lower human error | Reduced labor cost per unit | High-volume production |
| Integrated inspection | Inline defect detection | Better release confidence | Less scrap and complaint cost | FDA-regulated products |
| Recipe-based control | Faster format switching | Repeatable settings | More uptime | Multi-SKU factories |
| Traceability | Batch and lot tracking | Audit support | Lower compliance risk | OEM and export supply |
| Cleanroom compatibility | Stable environmental control | Less contamination risk | Avoids costly rework | Sterile components |
| Scalable architecture | Future module additions | Consistent expansion path | Protects capital investment | Growing U.S. demand |
The most successful projects align these benefits with actual business goals: market entry, contract wins, cost reduction, or compliance upgrades.
The line chart illustrates a realistic upward trend in U.S. demand, driven by vaccination infrastructure, biologics packaging, and domestic manufacturing initiatives.
Key Types, Models and Technical Options for Syringe Production Lines
Not all syringe production lines are built the same. The right model depends on product design, speed expectations, cleanliness class, automation needs, and packaging method. Buyers should first define whether they need a line for conventional disposable syringes, safety syringes, insulin syringes, or prefillable systems.
Entry-level lines may focus on semi-automatic or lower-speed assembly for niche production. Mid-range lines typically combine automated feeding, assembly, and basic inspection. High-end lines integrate servo motion control, advanced vision systems, robotic handling, leak testing, cleanroom enclosure design, and MES or ERP connectivity.
Important technical options include:
- Fixed needle versus luer-lock or luer-slip design support
- Single-cavity or multi-format handling
- Automatic needle bonding or insertion modules
- Inline printing, scale marking, and camera verification
- Siliconization with precise dosing control
- Automatic packaging with blister, pouch, or carton formats
- Electronic batch records and remote diagnostics
| Line Type | Typical Speed | Main Products | Automation Level | Ideal Buyer |
|---|---|---|---|---|
| Basic disposable syringe line | 6,000-10,000 pcs/hour | 2 ml to 10 ml syringes | Medium | Regional medical consumables producer |
| High-speed syringe line | 12,000-24,000 pcs/hour | Mass-market standard syringes | High | Large-scale U.S. supplier |
| Safety syringe line | 5,000-12,000 pcs/hour | Retractable or shielded designs | High | Hospital-focused manufacturer |
| Insulin syringe line | 8,000-15,000 pcs/hour | Fine graduation syringes | High precision | Diabetes device producer |
| Prefillable syringe component line | 4,000-10,000 pcs/hour | Drug container systems | Very high | Pharma packaging partner |
| Custom multi-format line | Project-specific | Mixed sizes and mechanisms | Configurable | OEM or CDMO |
This table shows why technical fit matters more than headline speed. A lower-speed line with stronger inspection and changeover capability may outperform a faster but less flexible system in multi-SKU U.S. operations.
The bar chart highlights where end-user demand is strongest, helping manufacturers decide whether to prioritize standard hospital syringes, biologics-compatible formats, or government preparedness volumes.
Syringe Production Lines vs Alternative Technologies: Which Solution Fits Your Needs?
Some manufacturers hesitate between building a dedicated syringe production line, outsourcing to a contract producer, purchasing semi-automatic equipment, or adapting a broader medical consumables line. The best solution depends on strategic control, compliance risk, and expected demand stability.
A dedicated line is usually best for companies with medium-to-high volume forecasts, strict quality ownership, and long-term domestic supply commitments. Contract manufacturing is more flexible for market testing, but it can create dependency on third-party scheduling and quality systems. Semi-automatic solutions may lower upfront cost, yet they often lead to higher labor costs, slower output, and weaker repeatability. Multi-purpose consumables lines are useful for diverse portfolios but may compromise optimization for syringe-specific tolerances.
| Option | Capital Cost | Scalability | Quality Control | Speed | Best Use Case |
|---|---|---|---|---|---|
| Dedicated syringe production line | High | Excellent | Strong | High | Long-term U.S. manufacturing |
| Contract manufacturing | Low initial | Medium | Shared with partner | Variable | Market entry or overflow |
| Semi-automatic line | Medium | Limited | Moderate | Low to medium | Smaller batch needs |
| Multi-purpose consumables line | Medium to high | Good | Moderate | Medium | Diverse product portfolio |
| Imported finished syringes only | Low initial | Low control | Supplier-dependent | Not applicable | Short-term supply only |
| Hybrid build-and-outsource model | Balanced | Good | Improving over time | Balanced | Phased scale-up strategy |
For many U.S. firms, the hybrid model works well: outsource first, then invest in a domestic production line once customer contracts and demand visibility improve.
Market Overview and Future Trends for Syringe Production Lines in Pharmaceutical Manufacturing
The U.S. market for syringe manufacturing equipment is supported by several forces: growth in injectable therapies, public health inventory planning, biologics expansion, and policy interest in resilient domestic healthcare manufacturing. Demand is no longer tied only to traditional hospitals. It is increasingly influenced by specialty pharmacies, self-injection therapies, biosimilars, and vaccine infrastructure.
From a 2026 outlook, three trend areas stand out. First is technology: smart vision inspection, robotics, predictive maintenance, and digital twin simulation are becoming more relevant for buyers seeking uptime and electronic compliance records. Second is policy: U.S. procurement and industrial policy continue to favor secure, auditable, and geographically diverse supply chains. Third is sustainability: energy-efficient drives, reduced compressed air use, recyclable packaging formats, and lower scrap generation are increasingly considered in capital approval decisions.
Buyers should also watch the shift toward modular line design. Instead of installing one oversized system, many manufacturers now prefer scalable modules that can expand in phases as orders grow. This approach is especially useful in industrial zones around Atlanta, Raleigh-Durham, Minneapolis, and Phoenix, where facility growth can happen in stages.
The area chart shows how rapidly smart and modular equipment preferences are rising, especially among manufacturers planning expansion in high-compliance sectors.
Another future trend is closer integration between equipment suppliers and full-factory engineering partners. Instead of buying isolated machines, U.S. investors increasingly ask for support with layouts, clean utilities, validation, training, and startup. This is where service capability matters. IVEN’s market positioning includes not only equipment supply but also feasibility support, design coordination, installation, commissioning, validation assistance, staff training, and lifecycle optimization. For buyers seeking broader project execution rather than a single machine transaction, that service structure can reduce schedule and integration risk. Companies exploring complete project models can examine its turnkey solution capabilities as part of due diligence.
How to Choose a Reliable Syringe Production Line Manufacturer or Supplier
Choosing a supplier in the United States market requires more than checking a price sheet. A reliable manufacturer or supplier should demonstrate strong design competence, quality system maturity, regulatory understanding, and after-sales responsiveness. Buyers should ask for user references, FAT protocols, validation documents, spare parts plans, and proof of past high-compliance installations.
Start with technical compatibility. Can the supplier meet your syringe size range, speed target, packaging format, and cleanliness class? Then review manufacturing capability. Does the supplier actually build critical modules in-house or mainly assemble sourced parts? In complex projects, in-house manufacturing often improves consistency and service accountability.
Manufacturing capability is especially important when evaluating international suppliers. IVEN, for example, emphasizes specialized manufacturing plants covering filling and packaging machinery, water treatment systems, intelligent conveying and logistics, and blood collection tube equipment. That indicates a stronger industrial base than a pure trading company. In the U.S. market, where spare parts access and technical reliability matter, this distinction can be significant.
| Evaluation Factor | What to Verify | Why It Matters | Warning Sign | Recommended Action |
|---|---|---|---|---|
| Regulatory knowledge | FDA, cGMP, ISO familiarity | Supports compliance | Generic answers only | Request documentation samples |
| Engineering depth | Line layout and integration skill | Reduces project risk | No utility interface detail | Review P&ID and line concept |
| Manufacturing base | Own plants and machining ability | Improves consistency | Mostly outsourced core modules | Ask for factory audit |
| Validation support | IQ/OQ/PQ document readiness | Speeds qualification | No structured protocol package | Include in contract scope |
| Service network | Response time and training plan | Protects uptime | Unclear support contacts | Define SLA before purchase |
| Reference projects | Similar installed lines | Shows proven capability | Only prototype or demo claims | Speak with actual users |
For practical sourcing, buyers often compare U.S.-based integrators, European specialists, and established Asian manufacturers. Supplier selection should balance compliance confidence, total project scope, and long-term support rather than origin alone. If you want to review available product categories and equipment families, browsing a supplier’s equipment portfolio can provide a helpful starting point.
This comparison chart reflects what many U.S. buyers prioritize when selecting a production line supplier: compliance and service are nearly as important as raw throughput.
Investment Cost, Budget Planning and ROI Analysis for Syringe Production Lines
The investment cost for a syringe production line for medical use can vary widely depending on speed, product complexity, cleanroom requirements, inspection level, packaging scope, and utility integration. A basic line may fit a smaller capital budget, while a high-speed automated line with full inspection and serialization can require a substantially larger investment.
Budget planning should include far more than equipment purchase price. U.S. buyers must consider facility preparation, utility systems, installation, validation, operator training, spare parts, customs logistics, and inventory buildup. Port entry planning is also relevant for imported systems, especially through Los Angeles/Long Beach, Houston, or Newark, where timing and inland transport can affect startup schedules.
| Cost Element | Typical Share of Budget | Why It Is Included | Often Overlooked? | ROI Impact |
|---|---|---|---|---|
| Main equipment line | 35%-50% | Core production asset | No | Direct throughput driver |
| Inspection systems | 8%-15% | Quality assurance | Sometimes | Reduces defect costs |
| Packaging modules | 8%-12% | Saleable final format | Yes | Improves market readiness |
| Facility and cleanroom work | 10%-20% | Installation environment | Often | Affects compliance approval |
| Validation and documentation | 3%-8% | Qualification support | Yes | Speeds commercial launch |
| Training, spares, and service | 5%-10% | Operational continuity | Often | Protects uptime |
ROI usually depends on unit cost reduction, contract wins, import substitution, and improved output reliability. In a high-demand U.S. market, companies may justify investment if the line reduces lead time, captures hospital or government business, or replaces expensive outsourced production. Projects often become more attractive when one supplier can cover engineering, installation, and commissioning instead of leaving the buyer to coordinate multiple contractors.
Service capability plays a major role in ROI realization. Even a technically strong line underperforms if startup is delayed or training is weak. IVEN’s service approach is notable because it emphasizes lifecycle support from feasibility and design through commissioning, validation, documentation, training, and optimization. For investors, that can mean faster ramp-up and fewer hidden coordination costs.
Key Considerations and Potential Risks When Investing in a Syringe Production Line
The biggest mistake in this market is underestimating project complexity. A syringe production line is not only a machine purchase; it is a regulated manufacturing project. Risks can appear in design mismatches, insufficient utility planning, contamination control gaps, poor packaging integration, or weak validation support.
One common risk is buying based on speed claims alone. If the line cannot maintain stable output under your actual product specification, uptime will suffer. Another risk is failing to define the user requirement specification in enough detail. Small differences in needle type, barrel dimensions, print requirements, or package style can dramatically affect line design.
Supply-chain and service risks also matter. Buyers should review spare parts strategy, remote support capability, on-site technician availability, and commissioning lead times. This is especially important for equipment crossing international shipping lanes and customs processes before installation in the United States.
| Risk Area | Description | Potential Consequence | Mitigation Method | Priority Level |
|---|---|---|---|---|
| URS not detailed enough | Requirements are unclear | Wrong line configuration | Build a full technical URS | High |
| Weak validation package | Incomplete IQ/OQ/PQ support | Delayed release | Contract documentation scope early | High |
| Utility mismatch | Plant utilities do not align | Startup delays | Perform utility audit | High |
| Limited spare parts planning | Critical items unavailable | Extended downtime | Stock key components locally | Medium |
| Operator skill gap | Insufficient training | Low OEE and more rejects | Schedule phased training | Medium |
| Regulatory under-preparation | Audit readiness is weak | Compliance findings | Use experienced compliance advisors | High |
A useful way to reduce these risks is to choose a supplier with strong regulatory awareness, documentation discipline, and enough project experience to anticipate pitfalls before FAT and SAT. If you need to discuss a specific U.S. expansion or modernization project, requesting direct technical consultation through a supplier’s contact channel is often the fastest route to a realistic proposal.
FAQ
1. What output speed should a U.S. manufacturer target?
That depends on contract volume, SKU count, and labor strategy. Many medium-to-large buyers look for lines between 8,000 and 24,000 pieces per hour, but precision, inspection depth, and uptime matter as much as headline speed.
2. Can one line produce multiple syringe sizes?
Yes, many modern lines support multiple formats, but change parts, recipe management, and changeover time should be reviewed carefully before purchase.
3. Is a syringe production line different from a prefilled syringe filling line?
Yes. A syringe production line makes the syringe or its components, while a prefilled syringe filling line washes, fills, stopples, and packages drug product into compatible syringes.
4. What regulations matter in the United States?
FDA cGMP expectations, quality system requirements, ISO-related standards, documentation control, traceability, and packaging integrity are all highly relevant depending on product classification.
5. How long does installation and qualification usually take?
It varies by scope, but full projects can take several months from delivery to commercial readiness, especially when facility work, FAT, SAT, and IQ/OQ/PQ are involved.
6. Should buyers choose a local or international supplier?
Either can work if the supplier provides strong compliance support, fast service response, spare parts access, and proven project execution. Total capability matters more than geography alone.
7. What is the biggest hidden cost?
Many buyers underestimate facility adaptation, packaging integration, validation effort, and startup training. These can materially affect total investment and launch timing.
8. Are sustainability features becoming important?
Yes. By 2026, energy efficiency, reduced waste, smart diagnostics, and scalable modular design are expected to become more important in capital approval decisions across the U.S. market.
9. How can a buyer compare suppliers effectively?
Use a structured matrix covering throughput, compliance documentation, validation support, customization, service network, spare parts availability, and total lifecycle cost.
10. Why consider a supplier with broader pharmaceutical engineering expertise?
Because syringe manufacturing often connects with utilities, packaging, logistics, and cleanroom systems. Suppliers with wider engineering capability can reduce integration risk and simplify project delivery.
For U.S. manufacturers, the right syringe production line for medical use can support long-term compliance, stronger domestic supply resilience, and better cost control. The most successful investments are usually made by companies that define their product and regulatory needs clearly, compare suppliers on full lifecycle value, and choose a line that fits both current contracts and future 2026 market trends.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Pharma Cartridge Filling Systems in the United States
Cartridge filling in pharmaceutical production refers to the sterile dosing and closing of drug product into cylindrical cartridges, most commonly glass cartridges used in pen injectors, autoinjectors, and other combination drug-device formats. In the United States, it is a strategic manufacturing technology because it affects dose accuracy, aseptic assurance, line efficiency, container closure integrity, and readiness for FDA inspection. Companies expanding capacity in Boston, New Jersey, San Diego, Chicago, Houston, and North Carolina’s Research Triangle often evaluate cartridge filling lines when launching biologics, insulin products, hormone therapies, emergency injectables, and high-value specialty medicines.
Unlike simple liquid packaging, cartridge filling is a tightly controlled sterile process that usually includes washing or ready-to-use handling, depyrogenation when applicable, filling, stoppering, capping, in-process check weighing or vision inspection, and integration with downstream labeling and final packaging. It sits at the intersection of pharmaceutical engineering and medical device assembly because the finished cartridge often becomes part of a delivery platform. For this reason, buyers in the United States usually assess not only filling speed, but also changeover validation, particle control, 21 CFR compliance, data integrity, and compatibility with future automation goals.
For manufacturers seeking a scalable project approach, companies such as IVEN Pharmatech Engineering are often evaluated for integrated pharmaceutical engineering support, especially when a project requires more than a stand-alone machine and instead needs process utilities, cleanroom coordination, packaging interfaces, and compliance-oriented documentation.
In practical terms, cartridge filling in pharma is the process and equipment set used to aseptically fill medicinal solutions or suspensions into cartridges that will later be used directly by patients or assembled into injection devices. It matters because it reduces manual handling, supports unit-dose or multi-dose precision, and helps pharmaceutical companies commercialize patient-friendly drug delivery systems.
In the United States market, cartridge filling is especially important for three reasons. First, drug-device combination products continue to grow, particularly in diabetes care, fertility treatment, oncology supportive care, and self-administered biologics. Second, pharmaceutical manufacturers want flexible lines that can shift between batch sizes without sacrificing sterile control. Third, regulatory expectations remain strict, so investing in a well-designed cartridge filling line can reduce long-term compliance risk.
For buyers, the technology is not just a machine purchase. It is a production strategy decision involving filling accuracy, product loss, batch traceability, operator intervention levels, line clearance, and future expansion. A modern cartridge line can support ready-to-use components, restricted access barrier systems, isolators, recipe-driven automation, and electronic batch records. That combination is why cartridge filling is often reviewed during capacity upgrades, facility modernization, and greenfield sterile plant planning in the United States.
Pharmaceutical cartridge filling is used to place sterile drug product into cartridges under controlled aseptic conditions. The container may be a 1.5 mL, 3 mL, or custom-format glass cartridge, though the exact size depends on the therapy and delivery device. After filling, the cartridge is closed with plungers or stoppers and secured for downstream assembly or final packaging.
Common uses in U.S. pharmaceutical production include insulin cartridges for pen systems, anesthetic cartridges for dental applications, emergency medication cartridges, contrast media formats, and biologic products that benefit from precise delivery. Cartridge systems are also used when patient convenience and dose reproducibility are key market drivers.
The process usually includes the following stages: component infeed, washing or handling of nested ready-to-use parts, sterilization or depyrogenation where required, sterile filling, stoppering, capping or sealing, in-process control, visual inspection, labeling, and cartoning. In advanced installations, these steps are digitally connected to manufacturing execution systems for stronger audit trails.
Process StageMain FunctionTypical Control PointWhy It MattersCommon U.S. Buyer ConcernOperational ImpactComponent preparationReceives cartridges, plungers, caps, nests, or tubsParticulate cleanlinessPrevents contamination at line startSupplier quality consistencyReduces reject ratesWashing or RTU handlingCleans bulk components or manages ready-to-use partsBioburden and endotoxin controlSupports aseptic assuranceLine flexibility between formatsImproves changeover planningFillingDispenses precise drug volumeDose accuracyProtects product quality and label claimYield loss on high-value biologicsDirect effect on cost per batchStoppering/plunger insertionCloses the cartridgePlacement consistencyMaintains sterility and functionalityContainer closure integrityMinimizes leakage riskInspectionChecks fill level, particles, defects, and presenceVision system sensitivitySupports release qualityFalse rejects vs true detectionImproves acceptable yieldPackaging interfaceTransfers to labeling, cartoning, and device assemblyTraceability codingSupports serialization and distributionIntegration complexitySpeeds market releaseThis workflow shows why cartridge filling is more than volumetric dosing alone. Each stage influences both product quality and line economics. U.S. facilities that ship through trade corridors such as the Port of New York and New Jersey, Port of Savannah, Port of Los Angeles, and Memphis air cargo network often prioritize packaging robustness and supply continuity because cartridge products may move through temperature-controlled distribution networks after filling.
Modern pharmaceutical manufacturing increasingly favors delivery formats that are easier for patients to use, simpler for healthcare providers to administer, and more compatible with home care models. Cartridge filling supports these goals by enabling compact, precise, and device-ready dosage formats.
The main applications include endocrine therapies, biologics, vaccines in selected device concepts, reproductive medicine, dental anesthetics, and specialty hospital products. A cartridge line can also support contract development and manufacturing organizations that need to serve multiple clients with different batch sizes.
Benefits usually include strong dose repeatability, reduced manual transfer steps, lower contamination exposure versus open handling approaches, and good compatibility with pen systems and other injection devices. For manufacturers, there are also operational advantages such as reduced labor intensity, more structured in-process controls, and easier scale-up into commercial production.
Application AreaTypical Product TypeWhy Cartridge Format Is ChosenKey Manufacturing BenefitPatient or Market BenefitGrowth Outlook in the U.S.Diabetes careInsulin and analogsCompatible with pen injectorsStable repeatable fillingConvenient self-administrationHighBiologicsSpecialty injectable therapiesSupports combination productsHigh-value product protectionImproved adherenceHighFertility medicineHormone injectionsMulti-dose and device-friendly usePrecise batch controlEase of use at homeModerate to highDental applicationsAnesthetic cartridgesEstablished clinical formatEfficient high-speed outputReliable chairside handlingStableEmergency therapiesRapid-use injectablesFast device integrationReliable closure controlReadiness in critical situationsModerateCDMO servicesMulti-client sterile fillsFlexible commercial offeringShorter product onboarding timeFaster access to outsourced capacityHighThe table highlights that the cartridge format is selected for both technical and commercial reasons. In cities such as Boston and San Diego, where biologics innovation is concentrated, device-compatible sterile filling is often viewed as a route to differentiated product delivery rather than just a packaging choice.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBar, {type: ‘bar’,data: {labels: [‘Diabetes’, ‘Biologics’, ‘Fertility’, ‘Dental’, ‘Emergency Care’, ‘CDMO Projects’],datasets: [{label: ‘Estimated U.S. Demand Index 2026’,data: [92, 88, 63, 54, 58, 79],backgroundColor: [‘#4e79a7′,’#f28e2b’,’#e15759′,’#76b7b2′,’#59a14f’,’#edc948′]}]},options: {responsive: true,maintainAspectRatio: false,scales: {y: { beginAtZero: true, max: 100 }}}});The bar chart reflects a realistic demand pattern: diabetes and biologics remain the strongest cartridge-driven segments, while CDMO demand continues rising as U.S. manufacturers seek flexible outsourcing and dual-source risk reduction.
Cartridge filling systems vary by throughput, sterility architecture, component presentation, filling technology, and level of automation. The right model depends on product sensitivity, target output, and facility strategy.
Entry-level or pilot lines may suit clinical batches and product development. Mid-speed lines often meet regional commercial needs. High-speed integrated lines are selected by large pharmaceutical companies when launching widely distributed products across the United States. Technically, buyers often choose between peristaltic pumps, rotary piston systems, or time-pressure filling depending on viscosity, accuracy requirements, and cleaning strategy.
Another major decision is whether to run bulk components or ready-to-use nested cartridges. Ready-to-use formats can simplify sterile preparation and reduce upstream handling, while bulk processing may support lower component cost at larger volumes. Barrier systems are equally important: open RABS, closed RABS, and isolator-based solutions offer different balances of accessibility, aseptic risk reduction, and capital cost.
On the technology side, integrated suppliers are attractive because cartridge filling rarely stands alone. A successful project may also require purified water systems, clean utilities, conveying, packaging, and warehouse automation. IVEN’s technical positioning is strongest in this integrated engineering area, where sterile filling lines can be coordinated with utility systems and plant-wide process design through a broader turnkey pharmaceutical project approach.
System TypeTypical ThroughputBest ForMain Technical OptionAdvantageTrade-OffLab or pilot fillerLowR&D and clinical lotsSmall-batch peristaltic fillFast development flexibilityLimited commercial outputSemi-automatic lineLow to mediumNiche productsManual-assisted loadingLower upfront costHigher operator dependenceAutomatic monoblockMediumCommercial productionIntegrated fill and closeCompact layoutLess modular expansionHigh-speed lineHighLarge-scale launchesMultiple filling stationsHigh output and lower unit costHigher validation complexityNested RTU systemLow to mediumSensitive biologicsTub or nest handlingReduced component preparation burdenHigher component costIsolator-based lineMedium to highHigh sterility assuranceClosed aseptic barrierReduced intervention riskHigher capital and maintenance costThese choices should be evaluated together, not separately. A high-speed line may look attractive on paper, but if the product portfolio is diverse and batch sizes vary widely, a more flexible mid-speed system may produce a better return. Likewise, nested components can improve sterility handling but may increase long-term consumable expense.
For manufacturing capability, experienced suppliers with dedicated production plants often provide more confidence than machine brokers. IVEN, for example, presents itself as a multi-plant manufacturer covering filling and packaging machinery, pharmaceutical water treatment, intelligent conveying, logistics systems, and blood collection tube equipment. That wider manufacturing base matters when buyers want interface control across multiple systems rather than managing separate vendors for every utility and transfer step.
Cartridge filling should be compared with vials, prefilled syringes, ampoules, and blow-fill-seal depending on the intended therapy, delivery method, and commercialization model. No format is universally best. The right choice depends on product sensitivity, patient use, distribution model, and reimbursement strategy.
Vials remain highly flexible and familiar, especially for hospital administration. Prefilled syringes offer direct injection readiness and are strong in single-dose markets. Ampoules are cost-effective in some conventional applications but less aligned with modern device platforms. Blow-fill-seal is highly efficient for selected sterile liquid formats, though it is usually aimed at different packaging concepts than cartridge-device assemblies.
FormatBest Use CaseStrengthLimitationDevice CompatibilityTypical Buyer ProfileCartridgesPen injectors and device-based dosingPrecise repeated use and compact formatMore complex assembly interfaceExcellentCombination product manufacturersVialsHospital and flexible fill volumesBroad industry acceptanceExtra preparation before administrationLimitedSterile injectable plantsPrefilled syringesReady-to-inject therapiesHigh convenienceDifferent device pathway and cost profileVery goodSpecialty injectable brandsAmpoulesTraditional small-volume liquidsSimple sealed glass formatLower convenience and break riskPoorLegacy productsBFS containersHigh-volume sterile liquidsIntegrated forming and fillingNot ideal for pen systemsPoorLarge commodity producersDual-chamber systemsReconstitution needsAdvanced product presentationHigher complexity and costGoodPremium specialty therapiesIf the product strategy revolves around self-administration, adherence, and device-enabled differentiation, cartridge filling is often the stronger choice. If the focus is hospital versatility or broad generic manufacturing, vials may remain more practical. Many U.S. companies in New Jersey and the Midwest evaluate both cartridges and prefilled syringes at the same time because they compete for overlapping therapy categories.
var ctxComp = document.getElementById(‘comparisonChartOptions’).getContext(‘2d’);var comparisonChartOptions = new Chart(ctxComp, {type: ‘bar’,data: {labels: [‘Dose Precision’, ‘Device Fit’, ‘Speed to Patient Use’, ‘Format Flexibility’, ‘CapEx Efficiency’, ‘Commercial Differentiation’],datasets: [{label: ‘Cartridge Filling’,data: [90, 96, 82, 68, 70, 92],backgroundColor: ‘#7b61ff’},{label: ‘Vial Filling’,data: [86, 32, 55, 94, 78, 58],backgroundColor: ‘#2ca02c’},{label: ‘Prefilled Syringe Filling’,data: [92, 84, 95, 60, 66, 88],backgroundColor: ‘#ff9d00’}]},options: {responsive: true,maintainAspectRatio: false,scales: {y: { beginAtZero: true, max: 100 }}}});The comparison chart shows why cartridge lines are typically selected when device compatibility and brand differentiation are strategic priorities, even if another format might appear simpler from a legacy manufacturing perspective.
The U.S. market for cartridge filling is supported by ongoing biologics growth, expansion of self-injection platforms, and investment in domestic sterile capacity. New plant activity around Greater Boston, Philadelphia, Indianapolis, Raleigh-Durham, and California continues to shape demand for modern aseptic processing equipment.
Several market forces are driving demand. Pharmaceutical companies want more resilient domestic production footprints. CDMOs want flexible lines to attract small and mid-size innovators. Established manufacturers are replacing older equipment to improve data integrity and reduce intervention risk. Meanwhile, procurement teams are under pressure to balance compliance, speed, and total cost of ownership.
Looking toward 2026 and beyond, the strongest trends include isolator adoption, robot-assisted handling, real-time digital monitoring, predictive maintenance, and energy-conscious facility design. Sustainability is becoming more visible as U.S. manufacturers assess water use, compressed air efficiency, line cleaning burden, and packaging waste. Policy expectations are also evolving around quality systems maturity, cybersecurity for connected equipment, and tighter documentation discipline.
var ctxLine = document.getElementById(‘lineChartGrowth’).getContext(‘2d’);var lineChartGrowth = new Chart(ctxLine, {type: ‘line’,data: {labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’],datasets: [{label: ‘Estimated U.S. Market Index for Cartridge Filling Equipment’,data: [100, 108, 118, 131, 146, 161, 177],borderColor: ‘#1f77b4’,backgroundColor: ‘rgba(31,119,180,0.15)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,scales: {y: { beginAtZero: false }}}});var ctxArea = document.getElementById(‘areaChartShift’).getContext(‘2d’);var areaChartShift = new Chart(ctxArea, {type: ‘line’,data: {labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’, ‘2028’],datasets: [{label: ‘Automated/Isolator-Based Share’,data: [34, 39, 45, 52, 59, 66, 72],borderColor: ‘#d62728’,backgroundColor: ‘rgba(214,39,40,0.22)’,fill: true,tension: 0.25},{label: ‘Conventional Open Handling Share’,data: [66, 61, 55, 48, 41, 34, 28],borderColor: ‘#8c8c8c’,backgroundColor: ‘rgba(140,140,140,0.12)’,fill: true,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false,scales: {y: { beginAtZero: true, max: 100 }}}});The charts illustrate two realistic developments: overall market expansion and a clear shift toward more closed, automated aseptic processing. This is especially relevant in the United States, where labor costs, audit readiness, and business continuity planning increasingly support higher automation levels.
Another trend involves supply chain strategy. Buyers now look beyond machine shipment price. They ask where critical components are sourced, how quickly spare parts can reach U.S. sites through Los Angeles, Long Beach, Houston, Savannah, or Newark, and whether remote diagnostics can reduce downtime. In short, future competitiveness depends on the full support ecosystem around the line.
Choosing a supplier requires evaluating technical fit, compliance depth, manufacturing consistency, and service strength. A low purchase price is rarely the decisive factor for sterile filling projects because downtime, failed FAT/SAT performance, or poor documentation can cost far more than the original discount.
Start by defining your user requirement specification. Include product viscosity, target throughput, acceptable fill tolerance, component format, sterility architecture, automation level, inspection needs, and digital connectivity. Then review supplier experience with similar products and container formats. Ask for examples of installations that passed demanding qualification processes.
Selection CriterionWhat to CheckWhy It MattersWarning SignStrong Supplier IndicatorBuyer ActionRegulatory understandingFDA, cGMP, data integrity familiarityReduces compliance riskGeneric answers without examplesStructured validation document setReview sample documentsApplication experienceCartridge and sterile line referencesImproves project predictabilityNo comparable case historyRelevant multi-project recordRequest reference scenariosEngineering integrationUtilities, packaging, logistics interfacesAvoids layout conflictsScope gaps between vendorsSingle-point coordination abilityConduct interface workshopsManufacturing qualityFactory controls and component traceabilityAffects reliability and lifespanHeavy outsourcing without controlDedicated production plantsAudit the manufacturing siteService responseInstallation, training, spare parts, remote supportShortens downtimeSlow or unclear support structureLifecycle support planDefine SLA termsCustomization abilityAdaptation to product and facility needsImproves fit and ROIOne-size-fits-all proposalFlexible engineering optionsChallenge the supplier with a real URSThis evaluation process is where service capabilities become critical. IVEN’s value proposition is usually strongest when buyers need more than equipment delivery, including consulting, engineering design, installation, commissioning, validation support, training, and after-sales continuity. That broader capability is relevant to U.S. buyers managing compressed schedules, especially those launching new sterile lines under investor or commercial pressure. Companies comparing sources can review available systems through the supplier’s equipment portfolio and move quickly to technical discussion via the contact channel.
It is also wise to examine how the supplier organizes spare parts and field support for the United States. A machine that is affordable to buy but difficult to maintain can become expensive during the first major unplanned shutdown. Ask about commissioning engineers, remote troubleshooting, control system backups, critical wear parts, and training for local maintenance teams.
Capital investment in cartridge filling varies widely depending on throughput, sterility barrier type, component presentation, digital controls, and downstream integration. A simple semi-automatic setup may fit a smaller budget, while a high-speed isolator-based line with integrated inspection and packaging can require a major multi-million-dollar program.
Budget planning should include far more than the base machine. U.S. buyers should account for factory acceptance testing, shipping, customs, installation, cleanroom adaptation, utilities, software validation, IQ/OQ/PQ support, training, spare parts, and line integration. Import logistics through ports such as Newark, Savannah, Houston, or Los Angeles can influence timing and landed cost, especially for oversized equipment skids.
Cost ElementLow Complexity ProjectMid Complexity ProjectHigh Complexity ProjectBudget Risk LevelPlanning NoteCore filling equipmentModerateHighVery highMediumDepends on automation and speedBarrier technologyLowModerateHighHighIsolators significantly change capexInspection systemsBasicModerateAdvancedMediumVision capability affects yieldFacility modificationsLowModerateHighHighLayout and HVAC may require reworkValidation/documentationModerateModerateHighMediumMust align with internal QA expectationsLifecycle service and sparesLowModerateModerateLow to mediumEssential for uptime protectionROI should be measured across at least five dimensions: labor reduction, lower reject rate, better yield on expensive drug product, faster release cycles, and increased commercial flexibility. For high-value biologics, even modest improvements in fill accuracy and product loss can significantly change the economics. For contract manufacturers, the return may come from faster onboarding of new customer projects and the ability to attract higher-margin device-related work.
In many cases, the best ROI comes not from buying the fastest line, but from buying the line that matches the forecasted product mix. Overcapacity can create unnecessary depreciation and validation burden. Undercapacity can choke growth and force expensive outsourcing. A credible supplier should help model both scenarios rather than pushing only the highest-ticket configuration.
The main risks in cartridge filling projects are usually not hidden in the brochure. They emerge during integration, qualification, scale-up, and routine operation. Buyers in the United States should review these areas carefully before issuing a purchase order.
First, product compatibility risk: the same machine may behave differently depending on viscosity, foaming tendency, shear sensitivity, silicone interaction, or oxygen sensitivity. Second, component quality risk: cartridge dimensional variability can affect feeding and stoppering. Third, sterility assurance risk: every intervention point should be challenged during design review. Fourth, data and control risk: recipe management, alarm history, and user access must support cGMP expectations. Fifth, schedule risk: utility readiness and room completion often delay line startup more than the equipment itself.
Risk AreaTypical ProblemOperational ConsequenceSeverityMitigation StrategyOwnerProduct behaviorFoaming or inaccurate fillsYield loss and batch deviationHighRun early filling trialsProcess developmentComponent variabilityFeeding jams or stopper mismatchDowntime and rejectsHighQualify component suppliersProcurement and QAAseptic interventionsToo much operator accessContamination riskVery highUse barrier design and intervention studiesEngineering and QASoftware/data integrityWeak audit trailsCompliance findingsHighValidate controls architectureAutomation and QAProject coordinationFacility and line mismatchStartup delayMedium to highIntegrated project planningProject managementService continuitySlow spare parts supportExtended downtimeMediumStock critical parts and train local staffMaintenanceThese risks explain why many large buyers prefer suppliers that can support project planning from concept through validation. A broader engineering partner can often reduce conflicts between clean utilities, line layout, material flow, and packaging logic. This is particularly important for greenfield or major retrofit projects where the filling line is only one part of a wider sterile manufacturing ecosystem.
Another consideration is sustainability. By 2026, more U.S. projects will evaluate not only throughput and sterility, but also energy load, compressed air use, material waste, and cleaning efficiency. Buyers should ask for utility consumption data, expected wear parts, and maintenance intervals. Sustainable operation increasingly supports both ESG reporting and cost control.
What is the difference between cartridge filling and vial filling?Cartridge filling prepares drug product for use in cartridges that typically integrate with injection devices, while vial filling produces more general-purpose sterile containers often used in hospitals or for reconstitution.
Which industries use pharmaceutical cartridge filling systems?Biopharma, diabetes care, fertility medicine, dental anesthetics, hospital injectable producers, and CDMOs are the main users.
Are cartridge filling lines suitable for biologics?Yes, especially when designed with gentle product handling, low hold-up volume, barrier protection, and robust in-process controls.
What throughput is considered commercial scale?That depends on the product and market, but commercial lines generally range from moderate to very high output, with configuration chosen according to annual demand and batch strategy.
Should a U.S. buyer choose RTU nested components or bulk cartridges?RTU formats are often preferred for sensitive products and lower contamination exposure, while bulk formats may offer lower component cost for large stable-volume programs.
What documents should be requested from a supplier?Typical requests include URS response, DQ support, FAT protocol, material certificates, software documentation, manuals, spare parts list, and IQ/OQ support packages.
How long does implementation usually take?For a new project, timelines can range from several months to well over a year depending on customization, facility readiness, qualification scope, and shipping logistics.
Can one supplier handle more than the filling line?Yes. Many buyers prefer suppliers that can support utilities, packaging, logistics, and validation coordination alongside the core equipment, especially for turnkey or expansion projects.
Why do large companies evaluate integrated engineering suppliers?Because sterile manufacturing performance depends on layout, utilities, controls, and documentation as much as on the filling machine itself. Integrated engineering can reduce interface risk.
How should a buyer begin?Start with a clear process and business requirement, compare technical options, validate supplier experience, and schedule a detailed discussion with shortlisted partners. If your project involves broader sterile plant planning, a conversation with an integrated provider such as IVEN Pharmatech Engineering can help define the right scope before procurement advances.
In summary, cartridge filling in pharma is a high-value aseptic manufacturing solution that supports the United States market’s shift toward patient-friendly drug delivery, stronger domestic sterile capacity, and more automated compliant production. The right investment depends on product profile, device strategy, validation expectations, and supplier support model. When those elements are aligned, cartridge filling can deliver both operational resilience and long-term commercial advantage.
-
IV Bag Production Line Cost Guide for the United States
For buyers in the United States, the cost of an IV bag production line usually depends on output, bag format, automation level, cleanroom scope, validation requirements, and whether the project includes turnkey engineering. In practical terms, an entry-level line for standard soft-bag infusion products may require a moderate capital budget, while a high-speed multi-chamber line with advanced inspection, robotics, water systems, and full FDA-aligned documentation can move into a much larger investment range. The key point is that the purchase price of the machinery is only one part of the total project cost. Utilities, cleanroom construction, quality systems, validation, training, spare parts, and long-term maintenance often determine the true lifetime value.
For many pharmaceutical manufacturers, especially those serving hospitals and compounding networks in cities such as New York, Chicago, Houston, Los Angeles, and Philadelphia, modern IV bag production lines create more than manufacturing capacity. They make it possible to produce advanced infusion products, including multi-chamber bags that keep active ingredients separate until use. That improves stability, extends shelf life for selected formulations, reduces compatibility risks, and supports safer bedside preparation. In the U.S. market, where reliability, sterility assurance, and traceability are essential, those benefits directly affect commercial competitiveness.
When executives ask, “How much does an IV bag production line actually cost?” the better question is often, “What production model, compliance scope, and product mix will justify the investment?” A plant focused on 50 mL to 500 mL saline bags for regional distribution has a very different capital profile than a facility making amino acid solutions, parenteral nutrition, dialysis solutions, or dual-chamber specialty formulations for nationwide healthcare systems. This guide explains the major cost drivers, compares line options, outlines U.S. demand trends, and shows how to evaluate suppliers for a stable long-term return.
The shortest answer is this: in the United States, the cost of an IV bag production line is driven by six main variables: product type, line speed, packaging format, regulatory scope, utility integration, and lifecycle service. A simple single-chamber soft-bag line for basic infusion products costs far less than a multi-chamber system designed for advanced formulations with strict aseptic controls and fully automated inspection.
Typical budgeting usually includes:
Companies entering the market often underestimate indirect cost. A line may appear competitively priced at the equipment stage, yet become expensive after layout redesign, FAT and SAT delays, installation inefficiencies, or incomplete qualification support. That is why many U.S. buyers prefer suppliers able to support both machinery and integrated plant engineering. Manufacturers comparing options can review an IV manufacturing equipment portfolio early in the process to understand how different machine platforms affect production economics.
Line ConfigurationTypical Output RangeRelative Capital CostMain UseComplexityBest FitBasic single-chamber soft-bag lineLow to mediumLowerSaline, glucoseModerateRegional suppliersHigh-speed single-chamber lineMedium to highMediumLarge-volume infusionsHighNational volume productionPP bottle infusion lineMediumMedium to highProducts requiring rigid packagingHighDiversified packaging strategyGlass bottle IV lineMediumMedium to highLegacy and specialty formulationsHighEstablished pharmaceutical plantsDual-chamber bag lineMediumHighUnstable or separated formulationsVery highSpecialty infusion makersTurnkey multi-chamber facilityMedium to very highHighestAdvanced hospital productsVery highStrategic long-term investmentThe table above shows why there is no universal answer to pricing. The true cost is linked to the business model. A plant near the Port of Houston may optimize for high-volume domestic distribution and low unit cost, while a facility in New Jersey may prioritize flexible specialty batches with shorter release cycles for East Coast healthcare networks.
An IV bag production line is a coordinated manufacturing system used to produce sterile infusion containers and fill them with pharmaceutical solutions under controlled conditions. Depending on the product format, the line may include film unwinding, bag forming, port welding, filling, sealing, printing, leak testing, sterilization support, visual inspection, overwrapping, cartoning, and palletizing. In more advanced projects, it also connects with solution preparation tanks, CIP/SIP systems, purified water generation, and manufacturing execution software.
The main advantages of investing in this type of line are operational, regulatory, and commercial:
For U.S. pharmaceutical companies, the largest advantage is often supply resilience. Domestic healthcare systems have become more sensitive to shortages of basic infusion products, especially after disruptions affecting procurement channels through Los Angeles, Long Beach, Savannah, and Newark. A local or regional IV bag plant can reduce reliance on external supply while improving responsiveness to hospital demand.
Another advantage is formulation flexibility. Single-chamber bags remain standard for many routine products, but multi-chamber technology allows separate storage of ingredients that may degrade, react, or precipitate if pre-mixed too early. This is especially useful in nutrition and specialty infusion therapy. In economic terms, that flexibility can support premium product positioning and better plant utilization.
Some buyers also prefer suppliers with broader engineering expertise rather than machine-only sales. For example, Shanghai IVEN Pharmatech Engineering, which you can learn more about here, is known in the market for combining pharmaceutical equipment knowledge with factory engineering experience, which is relevant when U.S. projects must align machinery, utilities, process flow, and qualification milestones.
From a hospital perspective, IV bag quality affects far more than packaging appearance. It influences sterility assurance, dosage accuracy, storage stability, nursing efficiency, and medication safety. Advanced production lines help pharmaceutical manufacturers supply infusion products that are easier to transport, safer to administer, and less prone to handling errors.
Hospitals in major U.S. medical hubs such as Boston, Cleveland, Baltimore, Dallas, and San Diego increasingly value infusion products that reduce compounding time and lower contamination exposure. Ready-to-use or partially separated formulations can support pharmacy workflow and improve bedside efficiency. For health systems under staffing pressure, those clinical benefits create purchasing preference.
Clinical ApplicationTypical ProductWhy Bag Quality MattersHospital BenefitProduction RequirementCommercial ValueEmergency careNormal salineRapid availability and seal integrityFaster patient stabilizationHigh output consistencyStable bulk demandCritical careDextrose infusionAccurate fill volumeSafer dose controlPrecise meteringHigh repeat useParenteral nutritionMulti-component solutionsIngredient separation and stabilityReduced bedside mixingMulti-chamber capabilityHigher-margin specialty marketDialysis supportDialysis solutionsLow contamination riskReliable routine treatmentRobust sterile processingStrong institutional demandPediatricsSmall-volume infusionsFlexible sizes and safetyBetter dose suitabilityFormat adaptabilityNiche but valuable marketOncology supportAdjunctive infusion productsLeak resistance and compatibilitySafer pharmacy handlingEnhanced inspection systemsPremium quality positioningThe table shows that bag production line quality directly supports end-user clinical performance. For buyers selling into integrated delivery networks, Veterans Health Administration facilities, and major group purchasing organization channels, reliability can matter as much as price.
Another important application is disaster readiness. U.S. states exposed to hurricanes, wildfires, and winter infrastructure disruption need resilient medical supply. Facilities located near inland transport hubs such as Memphis, Indianapolis, or Kansas City may gain an advantage by serving multiple regions quickly. A modern production line can therefore become part of a broader healthcare continuity strategy, not only a packaging investment.
Not all IV bag lines use the same container system. The chosen format affects machine design, sterilization approach, line efficiency, and product shelf-life profile. In the United States, non-PVC soft bags continue to attract attention because they align with hospital preferences around material performance, environmental concerns, and product compatibility. However, PP bottles and glass bottles still retain value for certain applications.
The most common production formats include:
Material / FormatKey FeaturesAdvantagesLimitationsTypical U.S. UseCost ImpactNon-PVC filmFlexible, modern multilayer structureGood compatibility, lighter logisticsMaterial qualification neededMainstream soft-bag infusionsModeratePVC filmTraditional soft-bag materialEstablished process know-howEnvironmental and compatibility concernsSelective legacy useLower to moderatePP bottleRigid containerStrong physical protectionHigher packaging massProducts needing rigidityModerate to highGlass bottleExcellent barrier propertiesLong-established pharmaceutical useFragility and transport costSpecialty or legacy product linesModerate to highDual-chamber bag filmSegregated compartmentsSupports unstable formulationsMore complex sealing designNutrition and specialty drugsHighCustomized multilayer filmTailored barrier and weld propertiesProduct-specific performanceLonger development cyclePremium branded productsHighMaterial choice can influence line cost in several ways. Specialized films may require tighter temperature control during sealing, upgraded leak testing, or more extensive qualification runs. Ports, fitments, and peelable interfaces may also change component costs. For U.S. buyers that source raw materials through Gulf Coast or West Coast ports, lead-time planning is critical because film supply continuity can affect plant utilization more than machine speed.
Below is a realistic view of how the U.S. IV bag equipment market has expanded with the rise of flexible packaging and specialty formulations.
var ctxLine = document.getElementById(‘lineChartMarket’).getContext(‘2d’);var lineChartMarket = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘U.S. IV Bag Line Market Growth Index’, data: [100, 108, 119, 131, 145, 160], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart illustrates a sustained increase in U.S. market demand for IV bag manufacturing capability, driven by domestic supply security, specialty infusion products, and modernization of hospital procurement standards.
This is one of the most important decisions for capital planning. Single-chamber bags are simpler, faster to deploy, and highly suitable for standard saline, dextrose, and routine infusion products. Multi-chamber lines are more expensive and more technically demanding, but they unlock formulations that benefit from ingredient separation until activation or use.
Single-chamber lines generally offer:
Multi-chamber lines generally offer:
FactorSingle-Chamber LineMulti-Chamber LineOperational EffectCost EffectBest Use CaseMachine complexityLowerHigherEasier startup vs longer commissioningLower vs higher capexStandard vs specialty productsProduct rangeRoutine infusionsAdvanced separated formulationsLimited vs expanded portfolioBasic vs premium revenueCommodity vs value-added marketsValidation burdenModerateHighFaster qualification vs more testingLower vs higher indirect costFast launch vs strategic launchLine speedOften higherOften moderateBulk output vs controlled specialty runsBetter unit cost vs premium priceHigh volume vs niche marginMaterial demandsStandard film structuresAdvanced barrier and seal designSimpler sourcing vs tighter sourcingLower vs higher consumable costStable procurement vs engineered supplyMarket positioningBroad essential-care supplyDifferentiated clinical offeringVolume competition vs specialty brandingPrice-sensitive vs value-driven salesRegional contracts vs advanced care networksIn the U.S. market, a single-chamber line often makes sense for new entrants trying to secure hospital tenders for basic fluids. A multi-chamber line may be justified for firms with formulation expertise, stronger QA resources, and access to specialty clinical accounts. The investment decision should therefore match both commercial strategy and internal manufacturing maturity.
Demand in the United States is shaped by three intersecting trends: healthcare supply resilience, product diversification, and domestic manufacturing strategy. Basic infusion products remain essential, but purchasers increasingly favor dependable suppliers with transparent quality systems and robust delivery capability. At the same time, specialty therapies and nutrition products are pushing demand toward higher-value packaging formats.
Market growth is also affected by geography. East Coast projects often benefit from proximity to dense hospital networks and import gateways such as Newark and Savannah. Gulf Coast sites can leverage chemical and materials supply ecosystems around Houston. Midwest locations such as Columbus, St. Louis, and Indianapolis can support efficient national distribution. West Coast operations may align with Pacific trade flows and biotech clusters in California.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Basic Infusions’, ‘Nutrition’, ‘Dialysis’, ‘Critical Care’, ‘Pediatrics’, ‘Specialty Multi-Chamber’], datasets: [{ label: ‘Estimated U.S. Demand Index 2026’, data: [95, 68, 61, 72, 49, 77], backgroundColor: [ ‘rgb(54, 162, 235)’, ‘rgb(255, 159, 64)’, ‘rgb(75, 192, 192)’, ‘rgb(153, 102, 255)’, ‘rgb(255, 99, 132)’, ‘rgb(201, 203, 207)’ ] }] }, options: { responsive: true, maintainAspectRatio: false }});The bar chart suggests that while standard infusions still dominate total volume, specialty multi-chamber products are gaining strategic importance because they create stronger margins and support differentiated clinical value.
Another trend is digitalization. U.S. pharmaceutical plants are moving toward electronic batch records, machine vision analytics, predictive maintenance, and real-time quality monitoring. Buyers planning a 2026 or later project should evaluate whether the supplier can support data integration, audit trails, and future expansion. A line that looks cost-effective today but cannot connect to plant-wide digital systems may become a limiting asset.
var ctxArea = document.getElementById(‘areaChartShift’).getContext(‘2d’);var areaChartShift = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of Standard Single-Chamber Projects’, data: [78, 75, 72, 69, 66, 62], borderColor: ‘rgb(255, 99, 132)’, backgroundColor: ‘rgba(255, 99, 132, 0.25)’, fill: true, tension: 0.25 }, { label: ‘Share of Advanced Multi-Chamber Projects’, data: [22, 25, 28, 31, 34, 38], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.25)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});The area chart reflects a realistic trend shift: standard lines continue to lead, but advanced multi-chamber projects are steadily taking a larger share of new investment planning.
Sustainability is also becoming a stronger buying factor. Hospitals and pharmaceutical manufacturers are paying closer attention to material reduction, energy use, waste segregation, and water consumption. Future procurement may increasingly favor lines that reduce scrap, support lighter packaging, and improve utility efficiency without compromising sterility assurance.
Choosing the right supplier is often more important than negotiating the lowest headline price. In the United States, buyers should assess four dimensions: regulatory competence, machine quality, delivery capability, and after-sales support. A supplier that understands FDA expectations, cGMP documentation, and qualification workflows can save months of delay and significant hidden cost.
Important questions to ask include:
Evaluation PointWhy It MattersWhat Good Looks LikeWarning SignImpact on CostBuyer ActionRegulatory experienceReduces compliance riskDocumented GMP project historyGeneric claims onlyAvoids rework and delayRequest validation referencesEngineering depthImproves project integrationProcess, utility, and layout supportMachine-only sales approachLowers hidden installation costReview P&IDs and layoutsManufacturing qualityDetermines equipment lifeRobust stainless constructionInconsistent finishingReduces downtime costInspect fabrication standardsDocumentationSupports qualificationComplete manuals and protocolsLate or incomplete filesSpeeds commissioningDefine deliverables in contractService responseProtects production uptimeTraining and remote supportSlow escalation pathwayLowers operating lossAsk for SLA detailsCustomization abilityMatches product strategyFlexible design adaptationRigid standard package onlyPrevents future retrofit expenseMap product roadmap earlyThis table is useful during supplier shortlisting because it shifts the conversation from purchase price to total project success. A lower-cost line that arrives with incomplete qualification documentation can become more expensive than a higher-priced system with strong engineering support.
From a technology standpoint, buyers should pay attention to sealing consistency, filling accuracy, visual inspection systems, automation architecture, and compatibility with pharmaceutical water and solution preparation modules. Some established suppliers offer wider pharmaceutical process capability rather than isolated machine packages. IVEN, for instance, is known for technological strengths in IV solution equipment, pharmaceutical water systems, and intelligent logistics, which can benefit projects requiring integrated plant design rather than standalone equipment.
Manufacturing capability matters too. Buyers often prefer equipment suppliers with dedicated production facilities and experience across multiple container formats such as soft bags, PP bottles, and glass bottles. That breadth reduces the risk of design shortcuts. If your project involves a broad factory buildout, it can be useful to explore turnkey pharmaceutical engineering options alongside the core line itself.
A complete budget should separate direct equipment cost from total installed project cost. In many U.S. projects, the total installed cost can be significantly higher than the machinery quotation alone. Finance teams should model the project in phases: core line, process utilities, cleanroom construction, validation, startup inventory, and working capital.
Budget ItemWhat It CoversRelative Cost WeightCommon OversightROI EffectPlanning TipMain production lineForming, filling, sealing, inspectionHighIgnoring format change needsCore throughput driverMatch with 5-year demand planWater and solution systemsPW/WFI, preparation, distributionHighUnderestimating utility scaleAffects batch qualitySize for peak operationCleanroom and HVACControlled manufacturing environmentHighLate design coordinationImpacts compliance and OPEXIntegrate layout earlyValidation and documentationIQ/OQ/PQ protocols, recordsMediumBudgeted too lowImpacts launch timingInclude consultant supportTraining and startupOperator qualification and ramp-upMediumToo little production trial timeImpacts yield and scrapPlan staged commercializationSpare parts and serviceWear parts, technical supportMediumBuying only minimum kitImpacts uptimeStock critical parts locallyA practical ROI model should include:
For example, a plant serving southeastern U.S. hospital networks may justify investment through freight savings, local service reliability, and reduced stockout risk. A specialty line near Boston or Raleigh-Durham may justify higher capex through premium formulations and clinical differentiation. In both cases, the speed of qualification and time to market often has as much impact on ROI as nominal production speed.
Service capability can materially improve payback. Suppliers able to support feasibility review, equipment customization, installation, commissioning, qualification, training, and lifecycle optimization may reduce the risk of startup losses. IVEN is often positioned in that category because its service model extends beyond equipment sales into consulting, engineering, validation support, and long-term operational assistance. Buyers wanting a project-specific estimate can contact the engineering team to compare machinery scope with total investment needs.
var ctxComp = document.getElementById(‘comparisonChartSuppliers’).getContext(‘2d’);var comparisonChartSuppliers = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Regulatory Support’, ‘Customization’, ‘Integration’, ‘Lifecycle Service’, ‘Lead Time Control’, ‘Format Flexibility’], datasets: [{ label: ‘Integrated Engineering Supplier Score’, data: [92, 88, 94, 91, 84, 89], backgroundColor: ‘rgb(153, 102, 255)’ }, { label: ‘Machine-Only Supplier Score’, data: [68, 61, 55, 49, 72, 58], backgroundColor: ‘rgb(255, 159, 64)’ }] }, options: { responsive: true, maintainAspectRatio: false }});The comparison chart shows why integrated suppliers often produce lower total project risk even if the upfront quotation is not the lowest. Better integration generally reduces schedule slippage, redesign, and qualification friction.
Every major pharmaceutical capital project carries risk, and IV bag lines are no exception. The most common investment mistakes in the U.S. market are under-specifying compliance needs, overestimating initial demand, selecting the wrong packaging format, and ignoring material supply chain constraints.
Key risks include:
There is also a location risk factor. Sites heavily dependent on one port or one shipping lane may face disruption during congestion, labor actions, or severe weather events. U.S. buyers should model supplier lead times through Long Beach, Houston, Savannah, and Newark, and consider domestic warehousing for critical parts. For plants in inland manufacturing corridors, transport links to Memphis air freight, Chicago rail, or Dallas trucking can be strategic advantages.
Looking toward 2026, three trends deserve attention:
Investors should also assess whether the supplier can support future upgrades. Many U.S. projects start with single-chamber products and later add advanced formats. A scalable controls architecture, modular layout, and utility headroom can prevent costly reconstruction later. The best line is not merely the one that fits today’s SKU list; it is the one that still fits the plant strategy in five to ten years.
1. What is the average cost range for an IV bag production line in the United States?There is no single national average because project scope varies widely. A basic line for standard soft bags may require a far smaller investment than a fully integrated multi-chamber facility with water systems, cleanroom construction, and validation support. Buyers should budget for total installed cost, not machine price alone.
2. What has the biggest effect on total project cost?The largest cost drivers are output capacity, bag format, automation level, cleanroom and utility scope, validation requirements, and whether the supplier provides turnkey engineering.
3. Is a multi-chamber line worth the extra investment?It can be, especially if your strategy includes parenteral nutrition, specialty infusions, or unstable formulations that benefit from ingredient separation. For basic saline or dextrose, single-chamber lines are often more economical.
4. How long does it usually take to install and qualify a new line?Lead time depends on customization, plant readiness, utility integration, and qualification depth. For U.S. projects, timelines often extend when documentation, HVAC coordination, or operator training is underestimated.
5. Should we buy equipment only or a turnkey solution?If your internal engineering team is strong and the plant infrastructure already exists, equipment-only procurement may work. If the project involves new utilities, cleanrooms, water systems, or process layout design, a turnkey or integrated engineering approach often reduces risk.
6. What certifications or compliance support should we ask for?Request documentation aligned with pharmaceutical GMP expectations, including FAT/SAT records, IQ/OQ support, material certificates where relevant, software documentation, and maintenance manuals. U.S. buyers should verify whether the supplier understands FDA cGMP expectations.
7. How do we compare suppliers fairly?Use a weighted scorecard covering regulatory experience, engineering depth, machine quality, documentation, service response, and total lifecycle cost. Avoid comparing quotations only on initial purchase price.
8. What industries beyond standard pharma use these lines?Besides mainstream infusion manufacturers, demand may come from nutrition therapy producers, dialysis solution manufacturers, specialty hospital product suppliers, and contract manufacturers serving institutional healthcare channels.
9. What should we ask about spare parts?Ask which components are critical, expected wear intervals, local stocking options, software backup procedures, and response time for emergency support. In the U.S., downtime cost can quickly exceed the savings from buying a cheaper spare-parts package.
10. Why do some buyers consider IVEN for these projects?Because some projects need more than a single machine. Buyers may look at IVEN when they want a supplier with pharmaceutical engineering know-how, manufacturing experience across multiple IV solution formats, and lifecycle service support from design through commissioning and optimization.
In summary, the real cost of an IV bag production line in the United States is determined by strategy, not just specification. Standard single-chamber capacity, advanced multi-chamber capability, domestic supply resilience, compliance readiness, and long-term service all shape the final investment outcome. The most successful buyers define the product roadmap first, then choose a supplier and line configuration that support both current production goals and 2026 market realities.