Biologics Prefilled Syringe Machines in the United States
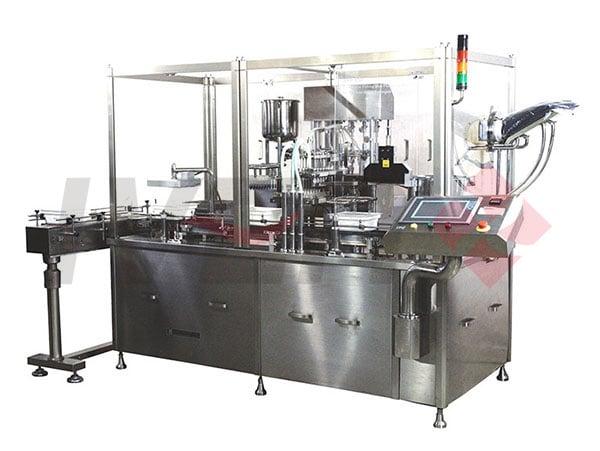
For pharmaceutical manufacturers in the United States, a prefilled syringe machine for biologics is a specialized aseptic filling and packaging system designed to handle high-value injectable products with strict control over sterility, dosing accuracy, product loss, and container integrity. It is widely evaluated by biologics developers, CDMOs, vaccine producers, and medical device companies when expanding capacity, launching new injectable therapies, or upgrading facilities to meet U.S. FDA cGMP expectations. In practical terms, these systems support the filling, stoppering, plunger insertion, inspection, labeling, and downstream packaging of sensitive biologic formulations in ready-to-use syringes for hospital, specialty pharmacy, and self-injection markets.
Demand in the U.S. continues to grow because biologics pipelines are expanding in hubs such as Boston, Cambridge, New Jersey, Philadelphia, Research Triangle Park, San Diego, and the San Francisco Bay Area. At the same time, procurement teams are under pressure to reduce contamination risk, improve batch traceability, shorten changeover time, and support flexible manufacturing for multiple SKUs. A modern biologics syringe filling line is therefore not just packaging equipment; it is part of a broader compliance, quality, and commercialization strategy that affects product launch timelines, total cost of ownership, and long-term plant competitiveness.
When companies compare solutions, they typically assess machine speed, line compatibility, fill accuracy, isolator or RABS integration, nested or bulk syringe handling, ready-to-use component support, environmental monitoring, CIP/SIP strategy, digital data collection, and validation burden. They also look carefully at whether the supplier can support installation, FAT/SAT, IQ/OQ/PQ, spare parts, operator training, and long-term service in the U.S. market.
Quick Answer: Why U.S. Manufacturers Evaluate Biologics Prefilled Syringe Machines

A prefilled syringe machine for biologics is considered a strategic investment because biologic drugs are expensive, sensitive to shear and contamination, and often intended for precise subcutaneous or intravenous administration. In the United States, where regulatory oversight is intense and commercialization timelines matter, the right equipment helps manufacturers protect product value while improving compliance and throughput.
Large pharmaceutical companies and fast-growing biotech firms alike evaluate these systems when launching monoclonal antibodies, biosimilars, vaccines, cell-derived injectables, peptide products, and other sterile therapies. Compared with traditional vial-only operations, prefilled syringe packaging can improve patient convenience, reduce dosing steps at the point of care, and support the shift toward self-administration. This is especially relevant for products distributed through specialty pharmacy networks in cities such as Chicago, Atlanta, Dallas, Seattle, and Miami.
From an operations perspective, a well-designed line can reduce overfill, minimize operator intervention, and streamline visual inspection and final packaging. From a commercial perspective, it can support premium product presentation, lifecycle management, and stronger differentiation in crowded therapeutic categories.
| Decision Factor | Why It Matters | U.S. Buyer Priority |
|---|---|---|
| Sterility assurance | Biologics are highly contamination-sensitive and require robust aseptic controls | Very high |
| Fill accuracy | Helps reduce batch loss and supports consistent delivered dose | Very high |
| Container compatibility | Supports glass or polymer syringes, nested tubs, and multiple formats | High |
| Regulatory readiness | Simplifies qualification under FDA cGMP and data integrity expectations | Very high |
| Flexibility | Enables multiple products or batch sizes on one line | High |
| Service support | Reduces downtime and validation delays after installation | High |
| Total cost of ownership | Affects long-term budget, spare parts, labor, utilities, and upgrades | High |
The table above shows why U.S. purchasing decisions are rarely based on speed alone. The most successful projects balance sterility, flexibility, serviceability, and regulatory confidence.
What Is a Biologics Prefilled Syringe Machine and What Is It Used For in Pharmaceutical Production?

A biologics prefilled syringe machine is an integrated filling and finishing system built for sterile injectable products that are filled directly into syringes rather than into vials or ampoules. The machine typically performs container infeed, de-nesting or unscrambling, nitrogen purging where required, filling, stopper insertion, plunger rod placement, in-process checks, reject management, and transfer to inspection and packaging stations.
In biologics production, the machine is used for products that require gentle handling, low product hold-up, and high precision. Since many biologics have high viscosity, are protein-based, or are sensitive to agitation, equipment design must account for pump selection, product path materials, and filling profile. Single-use product paths are increasingly considered by U.S. manufacturers that want faster changeovers and lower cleaning validation burden.
These systems are commonly deployed in:
- Commercial biologics plants in New Jersey and Massachusetts
- Clinical and small-batch facilities serving early-stage biotech programs
- CDMOs that support multi-client sterile fill-finish operations
- Medical device-drug combination product lines
- Vaccine and specialty injectable manufacturing sites
They are also used alongside isolators, restricted access barrier systems, automatic loading systems, leak testing equipment, visual inspection machines, and secondary packaging cells. In a modern facility, the prefilled syringe line forms part of a connected manufacturing ecosystem that includes purified water, WFI, clean utilities, environmental monitoring, logistics automation, and warehouse control.
| Process Stage | Function | Biologics-Specific Concern |
|---|---|---|
| Syringe infeed | Feeds nested or bulk syringes into the line | Minimize particulate generation and handling damage |
| Container preparation | Positions components for aseptic filling | Maintain sterility and alignment accuracy |
| Filling | Dispenses exact biologic volume into each syringe | Low shear, low hold-up, tight tolerance |
| Stoppering | Places stopper to protect the sterile product | Container closure integrity |
| Plunger insertion | Completes syringe assembly for final use | Consistent force and positioning |
| Inspection and rejection | Removes defective or out-of-spec units | Critical for quality release |
| Labeling and packaging | Prepares product for distribution | Traceability and cold-chain identification |
The table clarifies that a prefilled syringe machine is not a single filler alone. It is a coordinated system that protects sterile product quality from the first component feed through final pack-out.
Main Applications and Benefits of Biologics Prefilled Syringe Machines in Modern Pharmaceutical Manufacturing

The most common application is packaging high-value sterile biologic drugs in unit-dose presentation. In the U.S. market, this format is especially important for therapies used in oncology supportive care, immunology, endocrinology, ophthalmology, rare disease treatment, and long-term chronic disease management.
One major benefit is dosing convenience. Hospitals and clinics in cities like New York, Los Angeles, Houston, and Philadelphia increasingly prefer ready-to-administer formats that reduce manual preparation steps. For home-use products, prefilled syringes support better patient adherence and a more straightforward injection experience.
Another benefit is product economy. Since biologics can be costly per milliliter, reducing overfill and startup loss has direct financial value. Equipment with precise pumps, optimized product path geometry, and recipe-driven controls can significantly improve yield.
A third benefit is quality assurance. Automated filling, stoppering, and inspection help reduce the variability associated with manual intervention. This aligns with U.S. industry efforts to strengthen data integrity, batch traceability, and electronic records management.
| Application Area | Typical Product Type | Primary Benefit |
|---|---|---|
| Monoclonal antibodies | Autoimmune and oncology biologics | Precise dosing and premium presentation |
| Biosimilars | Reference biologic alternatives | Efficient scale-up and market competitiveness |
| Vaccines | Specialty and ready-dose injectables | Faster administration workflow |
| Peptides and hormones | Chronic therapy products | Patient convenience and self-injection support |
| Combination products | Syringe plus safety device or injector | Better downstream integration |
| Clinical biologics | Smaller development batches | Flexible batch sizing and quick changeover |
| High-potency injectables | Specialized niche therapies | Lower operator exposure risk |
This application map shows why syringe filling lines are no longer limited to one therapy segment. Their use spans both large-scale commercial output and flexible development manufacturing.
The chart highlights that monoclonal antibodies and biosimilars currently drive a large share of U.S. demand, while combination products continue to grow as delivery systems become more patient-centric.
Key Types, Models and Technical Options for Biologics Prefilled Syringe Machines
Buyers in the United States usually compare machines by throughput, aseptic design, syringe format, and automation depth. The main technical distinction is whether the system is designed for nested ready-to-use syringes, bulk syringes, or a hybrid approach. Nested systems are especially popular in biologics because they reduce direct component handling and can simplify contamination control.
Another important distinction is line speed. Small clinical lines may run at lower speeds with high flexibility, while commercial lines can reach several thousand units per hour depending on format and process complexity. However, for biologics, the best choice is often not the fastest line, but the line that best protects product quality and supports reproducible validation.
Key options include peristaltic pumps, rotary piston pumps, time-pressure systems, single-use product manifolds, vacuum stoppering, in-line weight checks, camera inspection, plunger insertion modules, and robotic transfer. U.S. buyers should also assess the control platform, audit trail capability, SCADA or MES integration, and remote diagnostic support.
| Machine Type | Best Fit | Advantages |
|---|---|---|
| Nested syringe filling line | Biologics, premium sterile products | Lower handling risk, strong aseptic control |
| Bulk syringe filling line | Higher volume standardized production | Potentially higher output and lower container cost |
| Clinical or small-batch model | R&D and early commercial use | Flexibility, small footprints, easier product changeover |
| Commercial high-speed model | Established biologics brands | Scalable output and automation |
| Isolator-integrated line | High sterility assurance needs | Reduced intervention risk |
| RABS-based line | Balanced cost and aseptic protection | Strong containment with easier access than full isolators |
| Single-use path system | Multi-product biologic facilities | Faster changeover and less cleaning validation |
The table shows that no single model suits every plant. A Boston biotech launching a niche specialty product may require very different features than a large New Jersey CDMO serving multiple commercial clients.
Biologics Prefilled Syringe Machines vs Alternative Technologies: Which Solution Fits Your Needs?
Many U.S. manufacturers compare prefilled syringe filling lines against vial filling, cartridge filling, blow-fill-seal for some applications, and outsourced fill-finish services. The right choice depends on product strategy, lifecycle stage, patient delivery model, and capital budget.
Vials remain highly flexible and are often preferred in early clinical development or for hospital compounding workflows. Cartridges are attractive when products will be used in pens or injector systems. Outsourcing can reduce upfront capital expenditure, but it may limit scheduling control and create dependence on external capacity in busy market periods.
Prefilled syringes stand out when convenience, dosing control, and direct administration are priorities. They are especially effective for biologics aimed at long-term therapy and self-injection channels. In the U.S. reimbursement environment, user-friendly presentation can also support market differentiation.
| Technology | Strengths | Limitations |
|---|---|---|
| Prefilled syringes | Ready-to-use, precise dose, strong patient convenience | Higher equipment complexity and component cost |
| Vials | Flexible formats, familiar process, broad supplier base | Extra preparation step at administration |
| Cartridges | Excellent for pens and advanced delivery systems | Requires compatible device strategy |
| Ampoules | Simple presentation for some products | Less suitable for many modern biologics |
| Outsourced fill-finish | Lower initial capex and faster start | Less control over timing and scheduling |
| Blow-fill-seal | Efficient for selected liquid products | Not typical for many premium biologic syringe formats |
| Manual or semi-automatic filling | Useful for very small volumes | Limited scalability and higher intervention risk |
For many U.S. biologics companies, the decision comes down to whether the product is moving toward patient-centric delivery and whether long-term commercial volumes justify dedicated in-house capacity.
This comparison illustrates why prefilled syringes are frequently chosen for premium biologics, even though the capital and technical requirements may be higher than for a vial line.
Market Overview and Future Trends for Biologics Prefilled Syringe Machines in Pharmaceutical Manufacturing
The U.S. market is being shaped by three powerful forces: rapid biologics growth, stronger focus on flexible sterile manufacturing, and rising interest in patient-friendly injectable delivery formats. Capital investment remains concentrated around established life science corridors such as Boston-Cambridge, New Jersey, Philadelphia, Raleigh-Durham, and San Diego, but expansion projects are also appearing in Texas, Indiana, and the Midwest.
By 2026, several trends are expected to influence equipment selection:
- More adoption of nested ready-to-use syringes for contamination control
- Greater use of robotics for de-nesting, transfer, and packaging
- Single-use fluid paths in multi-product biologics plants
- Digital batch data integration with MES, ERP, and maintenance systems
- Energy-efficient isolators and utility optimization to support sustainability goals
- Increased scrutiny on supply chain resilience for stoppers, syringes, and elastomer components entering via ports such as Los Angeles, Long Beach, Savannah, and Port Newark
Policy and compliance trends also matter. U.S. buyers are paying closer attention to Annex 1 implications for global operations, FDA inspection readiness, data integrity expectations, and contamination control strategy documentation. Sustainability is becoming a procurement factor as companies evaluate compressed air demand, cleanroom energy load, water use, and material waste.
The line chart reflects a realistic growth pattern driven by the expanding biologics pipeline, biosimilar launches, and continued investment in domestic fill-finish capabilities.
The area chart shows the ongoing shift toward nested formats, which are particularly attractive for high-value biologics requiring stronger contamination control and easier format management.
How to Choose a Reliable Biologics Prefilled Syringe Machine Manufacturer or Supplier
Choosing a supplier in the United States market requires more than comparing quotations. Buyers should evaluate regulatory competence, engineering depth, installation experience, service infrastructure, documentation quality, and willingness to customize. A low upfront price can become expensive if FAT preparation is weak, change parts are poorly engineered, or validation documents are incomplete.
Start with technical capability. The supplier should understand aseptic filling, biologics handling, clean utility integration, and component compatibility. It is also important that the supplier can support line integration with upstream and downstream systems, including inspection, labeling, cartoning, and intelligent logistics. Companies seeking broader factory development can review integrated project capabilities through pages such as turnkey pharmaceutical engineering solutions.
Next, review manufacturing capability. Strong suppliers usually have dedicated production resources for filling and packaging machinery, utilities, and handling systems rather than relying entirely on outsourced fabrication. This matters for schedule reliability, quality consistency, spare parts availability, and long-term upgrades. Buyers often request proof of previous deliveries, factory acceptance procedures, and examples of successful export projects to regulated markets.
Finally, assess service capability. U.S. projects move faster when the supplier can support feasibility review, equipment selection, layout optimization, installation, commissioning, validation documentation, and staff training. For a closer look at supplier background, procurement teams often examine the manufacturer’s profile, such as this overview of pharmaceutical engineering and equipment expertise, and then move to direct technical discussions through the contact team for project consultation.
| Supplier Evaluation Point | What to Verify | Why It Reduces Risk |
|---|---|---|
| Regulatory knowledge | FDA cGMP, EU GMP, WHO GMP understanding | Improves design compliance and validation readiness |
| Biologics handling experience | Low-shear filling and aseptic design references | Protects product quality |
| Manufacturing strength | In-house plants, machining, assembly, QA controls | Supports delivery reliability |
| Documentation package | DQ, FAT, SAT, IQ/OQ support, manuals, traceability | Shortens qualification timeline |
| U.S. service responsiveness | Remote support, parts strategy, training plan | Limits downtime after startup |
| Customization capability | Format changes, line integration, footprint adaptation | Ensures better fit for site constraints |
| Lifecycle support | Upgrades, optimization, audits, spare parts | Extends equipment value over time |
The checklist above is especially useful for teams managing greenfield or brownfield projects where equipment must fit existing utility corridors, material flows, and cleanroom zoning.
Investment Cost, Budget Planning and ROI Analysis for Biologics Prefilled Syringe Machines
Investment cost can vary widely depending on speed, automation level, aseptic barrier design, format range, inspection requirements, and site integration complexity. In the United States, budgeting should include not only the machine purchase price but also import logistics, rigging, facility modifications, isolator integration, validation, utilities, HVAC impact, packaging line interfaces, and operator training.
Projects near major logistics gateways such as Port Newark, the Port of Houston, Los Angeles/Long Beach, or Savannah may benefit from clearer equipment import planning, but inland delivery, specialized unloading, and controlled storage still need close coordination. Brownfield retrofits in older facilities around New Jersey or Pennsylvania may also require more hidden spending on cleanroom modifications, ceiling utilities, and material transfer redesign.
ROI typically depends on four variables: product value, annual production volume, reduction in overfill or rejects, and whether in-house filling improves launch timing or supply assurance versus outsourcing. For premium biologics, even small yield gains can have a strong financial impact.
| Budget Item | Typical Cost Impact | Planning Note |
|---|---|---|
| Core filling line | Highest capital component | Depends on speed, format, and aseptic level |
| Isolator or RABS | High | Critical for sterility strategy |
| Inspection and packaging integration | Moderate to high | Often underestimated during early budgeting |
| Facility retrofit | Moderate to high | Can increase sharply in older plants |
| Validation and documentation | Moderate | Essential for regulated startup |
| Training and commissioning | Moderate | Affects ramp-up speed and error reduction |
| Spare parts and service plan | Low to moderate | Helps prevent costly downtime later |
The table shows why machine price alone is not a reliable basis for procurement decisions. A complete lifecycle budget provides a more accurate investment picture.
For companies evaluating available platforms and modular options, it is useful to review a broader equipment portfolio through a supplier’s pharmaceutical machinery product catalog. This helps determine whether the vendor can support both the syringe line and related water, preparation, transfer, or packaging systems.
Key Considerations and Potential Risks When Investing in Biologics Prefilled Syringe Machines
The first risk is underestimating process development needs. Biologics are not standard water-like liquids, and fill behavior can change with viscosity, temperature, protein concentration, and sensitivity to agitation. A machine may perform well during a generic demo but still require further tuning for a specific formulation.
The second risk is incomplete component strategy. Syringes, stoppers, plungers, and nests must be compatible not only with the machine but also with the drug product and downstream use conditions. Any mismatch can affect closure integrity, cosmetic quality, or line efficiency.
The third risk is weak project management. Delays commonly come from late user requirement definitions, poor cleanroom coordination, incomplete FAT criteria, or documentation gaps. This is why many buyers prefer suppliers that can support design review, project planning, commissioning, and qualification as part of a structured lifecycle approach.
Regarding technology capability, some international suppliers stand out because they combine filling and packaging machinery with utility systems, conveying, and plant engineering know-how. Shanghai IVEN Pharmatech Engineering, for example, is known in the industry for integrated pharmaceutical engineering, sterile processing equipment, and compliance-oriented customization. Its technology base covers filling and packaging systems, purified water and WFI equipment, and intelligent logistics support, which is valuable when syringe filling lines must connect with wider facility infrastructure.
In manufacturing capability terms, the company operates specialized production resources in Shanghai focused on pharmaceutical filling and packaging equipment, water treatment systems, conveying and logistics, and blood collection tube machinery. That breadth can be relevant to U.S. buyers seeking coordinated sourcing rather than fragmented vendor management across several process packages.
From a service capability perspective, buyers often look for suppliers that can assist with feasibility review, equipment customization, installation, commissioning, validation activities, operator training, and post-startup optimization. A supplier with full-project support can reduce misalignment between design, delivery, and qualification. This matters particularly for U.S. facilities pursuing fast launch timelines or complex brownfield upgrades.
| Potential Risk | Typical Cause | Mitigation Approach |
|---|---|---|
| Low yield or excess overfill | Poor fill parameter matching | Run formulation-specific trials and optimize pump selection |
| Validation delay | Incomplete documentation package | Define FAT/SAT and IQ/OQ deliverables early |
| Container defects | Component incompatibility or handling damage | Qualify suppliers and run line compatibility tests |
| Downtime after startup | Weak training or spare parts planning | Build service and critical parts strategy in advance |
| Contamination event | Inadequate aseptic design or interventions | Use isolator/RABS and strong contamination control strategy |
| Expansion limitations | Machine too narrow in format or throughput range | Choose scalable and modular architecture |
| Unexpected retrofit cost | Facility constraints discovered late | Complete detailed layout and utility survey upfront |
These risks are manageable when process, engineering, quality, and procurement teams work from a common project roadmap rather than treating the machine as a stand-alone purchase.
FAQ
What speed should a U.S. biologics manufacturer look for?
It depends on batch size, product value, and commercialization stage. Many biologics projects prioritize filling accuracy, aseptic assurance, and flexibility over maximum speed.
Are nested syringe lines better for biologics?
In many cases, yes. Nested ready-to-use syringes reduce direct handling and are often preferred for sensitive sterile products, although bulk systems may still be appropriate for certain high-volume operations.
Can one line handle multiple syringe sizes?
Yes, many modern systems support multiple formats through change parts and recipe controls. Buyers should confirm actual changeover time, validation requirements, and operator complexity.
Is isolator integration necessary?
Not always, but it is increasingly common for high-value biologics because it improves contamination control and can reduce intervention risk. Some plants choose RABS when balancing protection and budget.
How important is single-use technology?
Very important for multi-product biologics facilities. Single-use fluid paths can reduce cleaning validation burden, shorten campaign changeover, and improve operational flexibility.
What documentation should be required from the supplier?
At a minimum, buyers should request design documents, material certificates, FAT protocol and records, SAT support, manuals, spare parts lists, traceability files, and IQ/OQ-related documentation aligned with the validation plan.
Should U.S. companies buy a stand-alone machine or a wider integrated solution?
If the project includes utilities, solution preparation, conveying, inspection, or packaging expansion, an integrated solution can reduce interface risk. This is especially relevant for greenfield projects or major modernization programs.
How long does ROI usually take?
It varies based on product value, line utilization, and whether the investment replaces outsourcing. For high-value biologics, improved yield and better launch control can shorten payback significantly.
What should buyers ask during factory acceptance testing?
They should verify fill accuracy, reject handling, component feeding stability, intervention procedures, alarm logic, recipe security, audit trails, and cleaning or changeover performance under realistic operating conditions.
How can a supplier support a U.S. project beyond equipment delivery?
The best suppliers contribute during concept planning, layout design, utility matching, commissioning, training, qualification support, and after-sales optimization. This broader support often has a major impact on project success.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Polypropylene IV Infusion Lines in the United States
For pharmaceutical manufacturers in the United States, a polypropylene bottle IV infusion line is a strategic production asset used to form, fill, seal, inspect, and package sterile infusion containers under tightly controlled GMP conditions. It is especially relevant for companies expanding hospital fluid capacity, replacing older glass or semi-rigid packaging systems, or building modern sterile plants that must align with US FDA cGMP, data integrity, validation, and sustainability expectations.
Demand for advanced IV solution equipment continues to rise in key pharmaceutical hubs such as New Jersey, North Carolina, California, Texas, Illinois, and Puerto Rico. Buyers in these regions often evaluate not only line speed and container format, but also sterility assurance, automation level, integration with purified water and WFI systems, cleanroom compatibility, and long-term lifecycle support. In practical terms, choosing the right polypropylene bottle IV infusion line can influence product quality, operating cost, labor efficiency, export readiness, and the speed of commercial launch.
Companies looking for fully integrated sterile production projects often prefer suppliers that can support more than standalone machinery. This is why many buyers review turnkey pharmaceutical engineering solutions, compare available production equipment portfolios, examine supplier backgrounds through their company capabilities, and request direct technical discussions through a project consultation channel.
A polypropylene bottle IV infusion line is a complete automated production system designed for sterile large-volume parenteral products such as sodium chloride, dextrose, balanced electrolyte solutions, irrigation solutions, and certain specialty infusions. The line typically includes bottle molding or bottle handling, air cleaning, filling, stopper or cap placement, sealing, leak testing, visual inspection, labeling, and final packaging. In many modern projects, it also connects with solution preparation systems, CIP/SIP modules, water treatment, sterilization support, and intelligent conveying systems.
In the United States, these lines are evaluated not only as machines but as compliance-critical systems. A successful project must support process validation, IQ/OQ/PQ documentation, batch traceability, electronic control reliability, alarm management, and clean utility compatibility. Buyers in Boston, Philadelphia, Raleigh-Durham, Houston, and Indianapolis often prioritize robust documentation packages because a sterile line purchase affects both pre-approval inspections and long-term audit performance.
Compared with legacy container formats, polypropylene bottles offer practical benefits including lower breakage risk than glass, strong chemical resistance, lighter transport weight, and suitability for automated handling. These features help manufacturers reduce product loss, improve warehouse efficiency, and streamline distribution to hospitals, wholesalers, and emergency stockpile programs. For health systems under pressure to secure domestic or nearshore supply resilience, modern PP bottle lines can also support faster capacity ramp-up.
Decision FactorWhy It MattersUS Buyer PrioritySterility assuranceDirectly affects patient safety and regulatory approvalVery highContainer integrityPrevents leakage, contamination, and transport failureVery highValidation packageSupports IQ/OQ/PQ and inspection readinessVery highAutomation levelReduces labor dependency and operator errorHighLine flexibilityEnables multiple bottle sizes and productsHighTotal lifecycle supportImproves uptime and long-term ROIHighThe table above shows why US pharmaceutical investors increasingly treat the line as part of a full sterile manufacturing strategy rather than a single equipment purchase.
A polypropylene bottle IV infusion line is a dedicated sterile manufacturing line for producing infusion solutions in PP bottles, usually in volumes such as 100 ml, 250 ml, 500 ml, and 1000 ml. Depending on the design, the line may use injection-blow or extrusion-based bottle forming, or it may process preformed bottles supplied from an upstream source. Its core purpose is to package sterile liquid drugs safely and consistently for intravenous administration.
These lines are used primarily for large-volume parenteral manufacturing. Common products include saline, glucose solutions, Ringer’s lactate, metronidazole infusion, mannitol, irrigation fluids, dialysis-related liquids, and other sterile hospital-use products. In the United States, such products are essential for acute care hospitals, outpatient infusion centers, long-term care networks, military and disaster preparedness programs, and regional drug distributors serving metropolitan areas like New York, Los Angeles, Chicago, Miami, and Atlanta.
A modern line usually works within a broader process architecture:
From a technical viewpoint, the system must deliver repeatability in fill volume, container geometry, seal quality, particulate control, and microbiological safety. Even small weaknesses in bottle stability, cap torque, thermal control, or airflow management can create deviations that become expensive during qualification or commercial production.
Production StageTypical FunctionMain Quality FocusResin handling or bottle inputFeeds PP material or preformed containersMaterial consistencyContainer formingCreates bottle body and neck finishDimensional accuracyWashing or air cleaningRemoves particles from the bottle interiorParticulate controlFillingDispenses sterile solutionFill accuracySealing or cappingCloses the container securelyContainer closure integrityInspection and packagingVerifies defects and prepares shipmentRelease qualityThis staged view helps buyers understand that a polypropylene bottle IV infusion line is best assessed as a complete process flow, not just a filler.
The main application of PP bottle infusion lines is the manufacture of sterile, ready-to-use infusion products at industrial scale. They are especially useful for high-volume products with stable demand patterns, including standard hospital fluids and emergency medical stock. In the United States, where supply interruptions can quickly affect hospital purchasing groups, production reliability is often as important as speed.
Key benefits include better transport performance than glass, lower breakage, reduced shipping weight, and strong compatibility with automated downstream packaging. Polypropylene bottles can also support attractive packaging designs with practical ergonomic handling for nurses and pharmacists. For manufacturers serving nationwide distribution centers near ports such as Los Angeles/Long Beach, Savannah, Newark, and Houston, lower packaging weight can contribute to freight efficiency.
Another major benefit is process standardization. Automated PP bottle lines can reduce variability in filling, sealing, and inspection compared with fragmented or older semi-automatic systems. This supports batch consistency and helps quality teams maintain tighter control over deviations, CAPA trends, and line clearance procedures.
For companies entering or expanding in contract manufacturing, infusion lines can also open access to new customer segments. Hospitals, group purchasing organizations, and government procurement programs usually prefer reliable suppliers with scalable sterile output. A line designed for fast changeover and multiple SKUs can help manufacturers balance large commodity runs with higher-margin specialty contracts.
Application AreaTypical ProductOperational BenefitHospital basic fluids0.9% sodium chlorideHigh-volume stable productionNutrition supportDextrose solutionsBroad market demandElectrolyte therapyRinger’s lactateFlexible product mixIrrigation solutionsSterile irrigation fluidsStrong institutional demandSpecialty infusionsMannitol or drug premix solutionsHigher value per batchEmergency reserve supplyCritical care fluidsSupports resilience planningThe broad application range above explains why many sterile manufacturers view PP bottle technology as a practical bridge between commodity scale and premium regulated production.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Hospital Fluids’, ‘Electrolytes’, ‘Irrigation’, ‘Dialysis Support’, ‘Specialty Infusions’, ‘Emergency Stock’], datasets: [{ label: ‘Estimated US demand index’, data: [92, 78, 64, 58, 51, 73], backgroundColor: [‘#4e79a7′,’#59a14f’,’#f28e2b’,’#e15759′,’#76b7b2′,’#9c755f’] }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});Not all polypropylene bottle IV infusion lines are built the same. The right configuration depends on output target, container range, cleanroom concept, utility availability, and the degree of upstream and downstream integration required. US buyers usually compare equipment on the basis of bottle size compatibility, automation level, filling technology, control system architecture, and validation readiness.
At the most basic level, there are mid-speed lines designed for regional production needs and high-speed lines suitable for large national supply programs. Some lines prioritize compact footprint for constrained facilities in urban locations like New Jersey or Southern California, while others are optimized for high-capacity greenfield plants in lower-cost industrial zones such as Texas or the Southeast.
Technical options commonly reviewed during procurement include:
Line TypeTypical OutputBest Use CaseCompact regional line3,000 to 6,000 bottles/hourSmaller market entry or hospital network supplyMid-speed flexible line6,000 to 12,000 bottles/hourMulti-SKU manufacturersHigh-speed commodity line12,000 to 18,000 bottles/hourNational volume productionIntegrated turnkey lineProject-specificNew sterile plant constructionSpecialty infusion lineLower to medium outputHigher-value formulationsExport-oriented lineFlexible by marketMulti-region compliance strategyThe technical choice should be tied to the commercial model. A high-output line is not always the best purchase if product variety, validation complexity, or local labor constraints make a flexible mid-speed platform more profitable.
The main alternatives to PP bottle IV infusion lines are glass bottle lines, non-PVC soft bag lines, and in some cases other semi-rigid plastic container systems. Each has specific strengths. The right choice depends on product sensitivity, hospital preferences, capital budget, logistics profile, and brand positioning.
Glass bottles remain relevant where chemical compatibility, premium perception, or legacy market expectations are important. However, they are heavier, more fragile, and usually more demanding in transport and warehousing. Soft bags are attractive for low weight and efficient storage, but some buyers prefer bottles for handling familiarity, standability, and certain application profiles.
For many US manufacturers, the PP bottle format strikes a balance between durability, automation compatibility, and practical distribution economics. This is especially attractive when serving large geographies from centralized production sites. Shipping from Midwest or Gulf Coast manufacturing centers to nationwide hospital networks can highlight the advantage of lighter, less fragile packaging.
TechnologyStrengthsLimitationsPP bottle lineLightweight, strong, scalable automationRequires precise molding and sealing controlGlass bottle lineHigh barrier confidence, established formatBreakage risk, heavier logistics costNon-PVC soft bag lineLow material weight, good storage efficiencyDifferent handling and presentation needsPVC bag lineLegacy familiarity in some marketsEnvironmental and material preference concernsSemi-rigid alternate plasticCustom design optionsLower standardization in some applicationsCMO outsourced supplyLow initial capexLess control over capacity and marginsThe comparison above is most useful when linked to business goals. If your priority is domestic capacity security and a balanced operating model, polypropylene often offers a compelling middle path.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Capital Efficiency’, ‘Transport Safety’, ‘Automation Fit’, ‘Weight Advantage’, ‘Format Familiarity’, ‘Scalability’], datasets: [ { label: ‘PP Bottle Line’, data: [82, 90, 88, 86, 78, 89], backgroundColor: ‘#6f42c1’ }, { label: ‘Glass Bottle Line’, data: [61, 48, 76, 32, 85, 72], backgroundColor: ‘#adb5bd’ }, { label: ‘Soft Bag Line’, data: [79, 84, 81, 93, 69, 85], backgroundColor: ‘#20c997’ } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});The US market for sterile infusion production equipment is shaped by several overlapping drivers: healthcare demand growth, the need to localize critical drug supply, FDA scrutiny of sterile operations, and the gradual replacement of aging production lines installed years ago. Buyers are increasingly interested in equipment that can support both current production and future digitalization.
Large-volume parenteral shortages have made resilience a board-level topic. As a result, many investors now consider not just the machine purchase price but also the strategic value of having flexible domestic or North America-oriented capacity. This is visible in project activity around established pharma corridors in New Jersey, Pennsylvania, North Carolina, Indiana, and manufacturing expansion zones in Texas and the Midwest.
For 2026 and beyond, three trends stand out. First, automation will continue moving from isolated line control toward integrated data environments with MES connectivity, predictive maintenance, and electronic batch support. Second, sustainability metrics will matter more, with focus on lighter packaging, lower utility consumption, and more efficient plant layout. Third, policy and procurement pressure will favor suppliers that can document compliance readiness, service responsiveness, and supply chain transparency.
There is also a clear trend toward integrated projects. Buyers increasingly prefer suppliers that can combine filling lines with purified water systems, WFI generation, clean utilities, logistics automation, and validation support. This reduces interface risk during fast-track projects.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [{ label: ‘Estimated US market demand index’, data: [68, 72, 79, 84, 91, 98, 106], borderColor: ‘rgb(75, 192, 192)’, backgroundColor: ‘rgba(75, 192, 192, 0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: false } } }});var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’, ‘2027’], datasets: [ { label: ‘Standalone line preference’, data: [62, 58, 52, 46, 39, 34], borderColor: ‘#dc3545’, backgroundColor: ‘rgba(220,53,69,0.15)’, fill: true, tension: 0.3 }, { label: ‘Integrated turnkey preference’, data: [38, 42, 48, 54, 61, 66], borderColor: ‘#198754’, backgroundColor: ‘rgba(25,135,84,0.15)’, fill: true, tension: 0.3 } ] }, options: { responsive: true, maintainAspectRatio: false, scales: { y: { beginAtZero: true, max: 100 } } }});These market patterns indicate that future winners will likely be suppliers able to combine equipment quality with project execution, documentation discipline, and service depth.
Supplier selection should begin with regulatory fit, not sales presentation. In the United States, buyers should verify whether the manufacturer can support cGMP-oriented design review, material traceability, FAT/SAT structure, and qualification documentation suitable for internal validation teams. A supplier experienced only in low-regulation markets may struggle with the level of detail expected by US quality and engineering departments.
Technological capability is the first screening layer. A credible supplier should demonstrate competence in sterile filling, bottle handling stability, control system architecture, and integration of line-level quality checks. In this area, IVEN Pharmatech Engineering is often evaluated for its long-standing involvement in IV solution equipment, pharmaceutical water systems, and plant-wide integration for regulated manufacturing projects. Its portfolio is relevant for buyers that prefer an engineering-led partner rather than a single-machine vendor.
Manufacturing capability is equally important. Buyers should review whether the supplier has specialized production facilities, durable fabrication standards, proven references, and the capacity to deliver complex projects on schedule. A supplier with dedicated manufacturing resources for filling and packaging machinery, water treatment systems, intelligent logistics, and related sterile equipment can often reduce coordination risk in larger projects.
Service capability is the third pillar. For US projects, the supplier should be able to support feasibility review, layout planning, documentation, commissioning, training, validation coordination, and after-sales response. This becomes critical during line start-up, where schedule delays can affect facility qualification, staffing, inventory planning, and customer commitments.
Supplier Evaluation ItemWhat to AskIdeal AnswerRegulatory experienceCan you support US FDA cGMP-oriented documentation?Yes, with validation package and audit-friendly recordsTechnical referencesHave you delivered sterile infusion projects before?Multiple comparable referencesManufacturing depthDo you build key systems in-house?Strong in-house production capabilityIntegration abilityCan you link utilities, filling, and packaging?Turnkey or high-level integration supportService responseHow do you handle commissioning and troubleshooting?Structured onsite and remote supportLifecycle partnershipCan you support upgrades and optimization later?Yes, with long-term service planWhen buyers compare international suppliers, they should look beyond list price. Documentation quality, parts availability, engineering communication, and realistic implementation schedules often determine the true success of the investment.
The investment cost of a polypropylene bottle IV infusion line depends heavily on scope. A standalone filling and sealing line may require a very different budget than a fully integrated sterile project with bottle forming, water treatment, cleanroom interfaces, automatic packaging, and validation services. In the United States, project cost is also affected by local installation labor, utility standards, building modifications, and compliance expectations.
Budget planning should include more than equipment purchase. Buyers frequently underestimate engineering design adaptation, clean utility connections, FAT travel, shipping, customs handling, SAT, training, spare parts, and initial validation runs. For projects landing through ports like Newark, Houston, or Los Angeles, logistics and inland transportation can also influence final cost.
A useful ROI model should estimate revenue gain from added production capacity, savings from reduced breakage or labor intensity, and margin benefits from bringing outsourced products in-house. Companies should also quantify the risk cost of supply interruptions. In hospital-facing markets, the ability to secure contracts through reliable domestic manufacturing can justify a faster payback than a simple capex spreadsheet suggests.
Cost ComponentTypical Share of Project BudgetBudget NoteCore production line30% to 40%Main capex driverUtilities and water systems12% to 20%Essential for sterile readinessCleanroom and installation15% to 25%Can vary widely by siteAutomation and data integration5% to 12%Important for modern complianceValidation and documentation4% to 8%Often underbudgetedTraining, spares, and support3% to 7%Improves start-up reliabilityFor many projects, payback is shaped by three levers: line utilization, product mix, and distribution footprint. A plant serving several regional hospitals from a central site may recover investment faster than a low-utilization facility producing too many small batches.
As a simplified example, a manufacturer replacing outsourced infusion supply with an in-house mid-speed PP bottle line may improve gross margin, reduce freight losses from glass breakage, and shorten lead times. If the line also supports secondary packaging automation and lower operator intervention, labor savings can further strengthen ROI. In many cases, buyers target a payback window of roughly three to six years, depending on portfolio and utilization assumptions.
The biggest mistake in sterile equipment investment is treating the project as a standard packaging purchase. A polypropylene bottle IV infusion line affects product quality, regulatory posture, staffing, utilities, and plant layout. The risk profile therefore includes both technical and organizational factors.
One major risk is under-specification. If bottle size changes, future product plans, or downstream packaging needs are not fully defined during URS development, the installed line may become restrictive within a few years. Another risk is over-customization, which can increase debug time and complicate future maintenance.
Validation risk is also significant. Equipment that performs well mechanically may still create delays if documents, software logic, alarms, or data records do not align with site quality requirements. This is why experienced buyers involve quality assurance, engineering, production, and validation teams early in the purchasing process.
Utility mismatch is another frequent problem. Sterile lines depend on stable compressed air, clean steam where applicable, purified water systems, temperature control, and environmental classification. If these are not aligned before installation, commissioning timelines can slip.
Risk AreaTypical ProblemMitigation StrategyURS definitionMissing future format requirementsBuild flexibility into specificationValidation readinessIncomplete documentationRequire document list before FATUtility integrationSite services not matched to line needsRun early engineering reviewOperator trainingSlow ramp-up and higher deviation ratePlan structured multilingual trainingSupply chainDelayed parts or resin variabilityMaintain critical spare inventoryProject timingLate installation affects launchUse milestone-based project controlFor 2026 and beyond, sustainability will become a larger decision factor. Buyers should assess resin efficiency, energy use, reject rate, waste management, and packaging optimization. Policy trends in the United States increasingly reward manufacturers that can demonstrate responsible production, better resource use, and stronger domestic supply resilience.
1. What products can be made on a polypropylene bottle IV infusion line?Common products include saline, dextrose, balanced electrolyte solutions, irrigation fluids, and selected specialty infusions. Final suitability depends on formulation, compatibility studies, and regulatory strategy.
2. Is a PP bottle line better than a glass bottle line?Not universally. PP bottle lines usually offer lower breakage risk and lighter logistics, while glass may remain preferred for some product or market situations. The best choice depends on your portfolio and supply model.
3. What output should a US manufacturer target?That depends on annual volume, SKU count, and customer contracts. Regional producers may choose mid-speed lines, while national suppliers often justify higher-capacity integrated systems.
4. What compliance standards matter most in the United States?US FDA cGMP expectations, validation discipline, documentation integrity, traceability, and cleanroom-compatible design are all critical. Buyers should also align with internal corporate quality systems.
5. How important is turnkey capability?Very important for greenfield or major expansion projects. If the supplier can coordinate utilities, process systems, logistics, and validation support, interface risk is often reduced substantially.
6. What should be included in a supplier proposal?URS response, technical layout, utility requirements, output assumptions, FAT/SAT scope, document list, training plan, spare parts recommendation, and project schedule.
7. Can one line handle multiple bottle sizes?Yes, many lines can, but changeover design should be reviewed carefully. Too much flexibility can reduce output or increase validation workload if not engineered well.
8. What makes IVEN Pharmatech Engineering relevant to this market?For US buyers seeking integrated sterile manufacturing support, the company is often considered because of its experience in IV solution equipment, pharmaceutical utility systems, intelligent logistics, and end-to-end project services. Its value is strongest when a project needs coordinated engineering rather than isolated machine supply.
9. How can buyers evaluate long-term service quality?Ask about commissioning structure, response times, spare parts planning, training, remote diagnostics, lifecycle upgrades, and previous international project support.
10. What is the best first step before requesting quotations?Prepare a detailed user requirement specification covering products, batch sizes, bottle formats, compliance expectations, utility conditions, plant layout constraints, and launch timeline. This leads to more accurate proposals and fewer surprises later.
In summary, a polypropylene bottle IV infusion line is not simply a packaging line but a core sterile manufacturing platform. For pharmaceutical companies in the United States, the best investment decision comes from balancing compliance, productivity, lifecycle cost, and strategic supply resilience. Buyers that combine clear URS development with careful supplier evaluation and realistic project planning are in the strongest position to achieve reliable, scalable production.
Whether the project involves a new plant, modernization of an older facility, or expansion of hospital fluid capacity, the most successful outcomes usually come from partners that can combine technology, manufacturing discipline, and service support. That is why many regulated-market buyers prefer to assess not only equipment performance but also the engineering depth, fabrication capability, and lifecycle services behind the line itself.
-
United States Guide to Auto-Disable Syringe Production
An auto-disable syringe production line is a specialized medical consumables manufacturing system used to produce syringes that mechanically prevent reuse after a single injection. In the United States, this type of line is increasingly relevant for companies serving public health programs, vaccination campaigns, export markets, humanitarian procurement, and safety-focused healthcare systems. For pharmaceutical and medical device investors, it is not simply a machine purchase; it is a strategic manufacturing decision tied to patient safety, regulatory compliance, throughput, traceability, and long-term cost control.
In practical terms, a complete auto-disable syringe line can cover molding integration, component feeding, printing, needle assembly, plunger and gasket insertion, auto-disable mechanism assembly, lubrication, inspection, sterile barrier packaging support, labeling, cartoning, and data traceability. Depending on product scope, manufacturers may also connect it with clean utilities, environmental control, warehouse automation, and validation documentation workflows.
For U.S. buyers, the evaluation usually centers on five core questions: Can the line meet FDA and cGMP expectations? Can it produce at stable speed with low reject rates? Can it support device design verification and process validation? Can the supplier provide long-term service in North America? And does the total investment make sense compared with importing finished syringes?
Large healthcare manufacturing projects in hubs such as Boston, New Jersey, Chicago, Houston, San Diego, and the Research Triangle often treat this equipment as part of broader capacity planning rather than a stand-alone asset. Buyers also consider port access through Los Angeles, Long Beach, Savannah, and Newark for imported components and export distribution. When the goal is resilient domestic supply, an auto-disable syringe production line can become a cornerstone of a safer and more localized medical device manufacturing strategy.
An auto-disable syringe production line is designed to manufacture syringes with a built-in mechanism that blocks reuse after the first administration. The mechanism can be based on plunger breakage, locking features, ring structures, or retraction-related design principles, depending on the product standard and target market. While these syringes are primarily medical devices, they are closely linked to pharmaceutical production because they are used to administer vaccines, biologics, injectables, and other sterile drug products.
In pharmaceutical ecosystems, the line serves several roles. First, it supports public health supply chains where injection safety is critical. Second, it enables contract manufacturers and medical consumables producers to align device output with drug delivery demand. Third, it provides a platform for integrated manufacturing projects where syringe production, packaging, warehousing, and quality systems are coordinated under one compliance framework.
Typical process stages include raw material handling, precision assembly of barrel and plunger components, integration of the auto-disable mechanism, vision inspection, leak testing, force testing, counting, packaging support, and batch data recording. If the project is configured at a higher automation level, robotic transfer, intelligent conveyors, and warehouse systems may also be included to reduce human intervention and contamination risk.
For companies expanding in the United States, the line is often evaluated together with plant layout, HVAC zoning, compressed air quality, cleanroom class, utility redundancy, and packaging material availability. This is especially important for facilities near major medical corridors such as Minneapolis, Indianapolis, and Philadelphia, where labor efficiency and validation readiness can significantly affect project timelines.
Production StageMain FunctionTypical Quality FocusAutomation OpportunityComponent feedingFeeds barrels, plungers, gaskets, and safety partsPart orientation and contamination controlAutomatic bowl feeders and robotic pick-and-placeMechanism assemblyBuilds the auto-disable feature into the syringeLock integrity and dimensional fitServo-controlled assembly stationsNeedle or nozzle integrationConnects delivery end structureLeak tightness and alignmentVision-guided insertion modulesLubrication and insertionOptimizes plunger movementForce consistency and material compatibilityMetered dosing controlsInspection and testingChecks visual and functional conformityReject detection and traceabilityCamera systems and automated rejectionPackaging interfaceTransfers accepted products for packingCount accuracy and batch codingCartoning and serialization integrationThe table above shows why buyers should view the line as a process chain rather than one machine. Every stage influences downstream validation, yield, and market acceptance.
The main application of an auto-disable syringe production line is the manufacture of single-use syringes intended to reduce reuse-related infection risk. This matters in immunization programs, emergency response procurement, export supply contracts, and healthcare systems requiring stronger sharps safety controls. In the U.S. market, these lines can also support manufacturers that supply federal, state, NGO, and international aid channels.
One major benefit is patient safety. By physically preventing reuse, the product lowers the risk of cross-contamination and unsafe injection practices. Another is regulatory and procurement alignment. Many institutional buyers prefer or require safety-enhanced disposable devices, particularly where high-volume vaccination or outreach programs are involved.
From an operations perspective, a modern line improves consistency. Automated assembly and inspection can reduce manual variability, improve dimensional control, and support electronic batch records. This is especially valuable when supplying high-volume distribution centers near Atlanta, Dallas, Columbus, and Memphis, where reliable outbound logistics depend on predictable production.
There is also a supply chain benefit. Domestic or regionalized manufacturing can reduce overreliance on imported finished syringes and shorten replenishment cycles. In periods of disruption, U.S. producers with local assembly and packaging capabilities may respond faster to hospital systems and public health agencies.
Another advantage is brand positioning. Medical device firms investing in safer injection technology often strengthen their standing with global tenders, donor-funded programs, and health systems emphasizing infection prevention. When a producer combines product safety with validated manufacturing, it becomes easier to compete on more than price alone.
Application AreaTypical Demand DriverBenefit to ManufacturerBenefit to End UserVaccination programsHigh-volume public health campaignsStable recurring demandReduced reuse riskHospital procurementSafety-focused clinical protocolsPremium positioningImproved injection safetyExport supplyGlobal tender requirementsAccess to broader marketsStandardized qualityHumanitarian responseEmergency medical deploymentRapid contract opportunitiesSafer field useContract manufacturingOutsourced device productionAsset utilization improvementReliable commercial supplyIntegrated pharma-device projectsDrug delivery ecosystem expansionCross-segment growthCoordinated supply continuityThis benefit profile explains why the line appeals not only to syringe manufacturers but also to broader pharmaceutical and medical consumables investors.
var ctx1 = document.getElementById(‘lineChartMarketGrowth’).getContext(‘2d’);var chart1 = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘U.S. market interest index’,data: [62, 68, 74, 83, 91, 101],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.1)’,fill: false,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false}});There is no single standard configuration for every project. In the United States, buyers typically compare lines by product size range, mechanism design compatibility, speed class, level of integration, cleanroom requirements, inspection depth, and packaging interface. A pilot-scale or mid-speed line may fit a company entering the segment, while a fully integrated high-speed line may suit established medical device plants.
Common model distinctions include low-output development lines, medium-speed commercial lines, and high-speed mass production lines. Product ranges may cover 0.05 mL, 0.5 mL, 1 mL, 2 mL, 3 mL, 5 mL, and selected specialized sizes depending on target use. Technical options can include in-line vision inspection, automatic needle bonding stations, force-displacement testing, rejection analytics, MES connectivity, servo motion control, and data collection for validation support.
Some buyers prioritize flexibility, especially if they expect mixed production or future product upgrades. Others prioritize dedicated efficiency for one high-volume SKU. The right balance depends on forecast demand, procurement commitments, staffing model, and facility space.
Technology depth also matters. Companies with broader engineering experience in pharmaceutical filling, water systems, smart logistics, and medical consumables often provide better integration support because they understand how equipment behaves in regulated factories, not only on a test floor. That can make a difference when the line must connect to packaging, warehouse automation, or documentation workflows.
Line TypeTypical Output RangeBest ForMain Trade-OffDevelopment line20 to 60 units per minuteR&D, validation, small batch launchesHigher unit cost at scaleMid-speed line60 to 180 units per minuteGrowing regional suppliersModerate expansion ceilingHigh-speed line180 to 350+ units per minuteLarge-scale commercial productionHigher upfront investmentDedicated single-size lineVaries by designOne major SKU with stable demandLower product flexibilityMulti-format lineVaries by change partsDiverse product portfolioLonger changeover and setupIntegrated turnkey lineVaries by scopeNew factory or full expansion projectGreater project coordination needThe table highlights a core buying principle: speed alone should not drive selection. Format flexibility, validation effort, staffing, and utility demands matter just as much.
Many U.S. manufacturers compare auto-disable syringe lines with standard disposable syringe lines, safety syringe assembly lines, or outsourced finished product sourcing. The best option depends on the intended market, regulatory profile, and commercial strategy.
A standard disposable syringe line may have lower capital cost but does not provide the same anti-reuse safety function. For commodity-focused markets, that may be acceptable. However, for public health programs or international tenders, the lack of an auto-disable feature may limit eligibility. Safety syringe lines focused on needlestick prevention can overlap in some use cases, but they solve a different problem. One centers on post-use sharps exposure; the other centers on reuse prevention.
Outsourcing finished syringes may reduce capital burden in the short term. Yet it can expose buyers to import volatility, longer replenishment cycles, and less control over validation, packaging, and quality data. This is a notable concern for firms serving U.S. healthcare networks that value domestic responsiveness.
Manufacturers in coastal states often also analyze freight economics. Importing finished devices through Long Beach, Oakland, or Newark can look attractive initially, but container swings, customs delays, and finished goods storage costs can change the equation. Local assembly or full production may offer stronger long-term resilience.
OptionCapital RequirementSafety LevelControl Over QualitySpeed to StartAuto-disable syringe lineMedium to highHigh for reuse preventionHighMediumStandard syringe lineMediumBasic single-use intentHighMediumSafety syringe lineMedium to highHigh for sharps protectionHighMediumContract manufacturingLow to mediumDepends on supplierMediumFastImported finished productLow upfrontDepends on product specLow to mediumFast initiallyHybrid modelMediumFlexibleMedium to highMediumFor firms that want strategic control and differentiation, an auto-disable syringe production line is usually strongest when demand volume is stable and compliance expectations are high.
var ctx2 = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Public health’, ‘Hospitals’, ‘Export tenders’, ‘NGO supply’, ‘CMO projects’, ‘Emergency stockpile’],datasets: [{label: ‘Estimated demand score’,data: [94, 79, 86, 72, 68, 88],backgroundColor: [‘rgb(255, 99, 132)’,’rgb(54, 162, 235)’,’rgb(255, 206, 86)’,’rgb(75, 192, 192)’,’rgb(153, 102, 255)’,’rgb(255, 159, 64)’]}]},options: {responsive: true,maintainAspectRatio: false}});The market outlook in the United States is shaped by three broad forces: healthcare safety requirements, supply chain localization, and automation-driven manufacturing upgrades. Interest in safer injection consumables has remained strong because providers, procurement agencies, and public health systems continue to prioritize risk reduction and dependable supply.
On the demand side, projects are influenced by vaccination readiness, emergency preparedness, and diversified sourcing strategies. Medical device producers are also watching global opportunities, since U.S.-based manufacturing can support export credibility if quality systems are robust. Regions with strong life sciences clusters, such as Massachusetts, North Carolina, Indiana, and California, are natural locations for related investments because they already have talent pools, cleanroom contractors, and validation specialists.
On the technology side, 2026 trends point to higher use of digital monitoring, machine vision, servo motion control, predictive maintenance, and electronic batch data integration. Sustainability is also becoming more relevant. Buyers are asking about compressed air consumption, reject reduction, recyclable packaging compatibility, and efficient factory logistics.
Policy trends matter as well. Projects increasingly factor in U.S. regulatory readiness, domestic manufacturing resilience, and audit transparency. Even when finished product regulations vary by market, investors prefer equipment suppliers that understand documentation discipline, change control, and global GMP culture.
Another visible trend is the move toward turnkey coordination. Instead of buying one stand-alone assembly machine, some investors want a broader package covering process layout, utility engineering, cleanroom interface, warehouse flow, and validation support. This is particularly important when launching in cities with high construction and labor costs, such as San Francisco, Seattle, and the New York metropolitan area, where design mistakes become expensive very quickly.
var ctx3 = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var chart3 = new Chart(ctx3, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Imported finished syringes share’,data: [72, 69, 65, 61, 57, 53],fill: true,backgroundColor: ‘rgba(255, 99, 132, 0.2)’,borderColor: ‘rgb(255, 99, 132)’,tension: 0.25},{label: ‘Localized production interest share’,data: [28, 31, 35, 39, 43, 47],fill: true,backgroundColor: ‘rgba(54, 162, 235, 0.2)’,borderColor: ‘rgb(54, 162, 235)’,tension: 0.25}]},options: {responsive: true,maintainAspectRatio: false}});Supplier selection should begin with compliance capability, not brochure speed. U.S. buyers need to know whether the manufacturer can support documentation, FAT structure, SAT execution, IQ/OQ/PQ alignment, spare parts continuity, and process risk assessment. Experience in regulated pharmaceutical and medical device environments is a major advantage because it reduces the chance of integration problems later.
Technology capability should be reviewed in detail. Ask whether the supplier can provide servo-controlled assembly, validated inspection logic, material handling coordination, data traceability, and compatibility with cleanroom operation. A strong engineering supplier should also be able to discuss line balancing, reject logic, preventive maintenance intervals, and change-part management. This is where broader know-how in pharmaceutical engineering becomes valuable. Companies with experience beyond a single machine category often understand water systems, filling equipment, intelligent conveying, and process layout in a more practical way.
Manufacturing capability is equally important. Buyers should ask about factory size, in-house machining, assembly quality standards, trial capacity, and delivery record. A supplier with multiple specialized plants and a large installed base generally offers better production control than a purely outsourced assembler. For example, a manufacturer that supports not only medical consumables equipment but also packaging, logistics, and utility-related solutions may be better prepared for complex turnkey work.
Service capability can determine the real success of the investment. Installation support, commissioning, operator training, validation documentation, after-sales response, and long-term optimization all affect uptime. In the U.S. market, time zone responsiveness and English technical communication are especially important. Buyers should also ask whether the supplier can support remote diagnostics, parts planning, and documentation review for audits.
Learn more about IVEN Pharmatech Engineering if you want to evaluate a supplier with international pharmaceutical engineering experience, specialized manufacturing resources, and project delivery exposure across multiple regulated markets. For investors considering broader factory development rather than equipment alone, it is wise to review whether the provider can also support turnkey pharmaceutical and medical device project execution from layout to validation.
Selection CriterionWhy It MattersWhat to AskWarning SignRegulatory understandingSupports audit readinessCan you align with FDA-style documentation expectations?Vague answers on validationEngineering depthImproves line stabilityHow do you control assembly force and reject logic?Only generic technical specsManufacturing baseAffects build quality and deliveryWhat is made in-house?Heavy dependence on unverified outsourcingInstalled referencesReduces execution riskWhat similar lines have you delivered?No comparable projectsService networkProtects uptime after start-upWhat is your support model for U.S. customers?No clear spare parts planLifecycle supportImproves ROI over timeDo you provide training, optimization, and upgrades?Support ends after shipmentThis table can be used as a supplier interview checklist during RFQ and technical clarification stages.
The cost of an auto-disable syringe production line varies widely depending on speed, level of automation, tooling complexity, inspection requirements, utility scope, and packaging integration. In the U.S. context, buyers should budget beyond machine price alone. Freight, installation, cleanroom adaptation, utilities, qualification, packaging development, local taxes, training, and spare parts can significantly change project economics.
A practical budget model includes capital expenditure, commissioning cost, validation cost, initial consumables, staffing, maintenance, and working capital for raw materials. In many projects, the difference between a “cheap” line and a “bankable” line becomes clear only after qualification planning begins. A lower initial quote can become more expensive if reject rates are high or documentation is weak.
ROI depends on annual throughput, selling price per syringe, line uptime, labor structure, scrap rate, and utilization. It also depends on the alternative. If the benchmark is importing finished product through major ports like Newark or Long Beach, domestic production may deliver value through shorter lead times, better supply assurance, and stronger contract positioning, even if unit manufacturing cost is not the absolute lowest on day one.
Buyers should run at least three scenarios: conservative, base case, and high-demand. The conservative case should assume slower market penetration and lower utilization during the first year. The high-demand case should test whether downstream packaging and warehouse systems can keep pace if demand surges.
Budget ItemLow Complexity ProjectMid Complexity ProjectHigh Complexity ProjectCore line equipmentModerateHighVery highTooling and change partsLowModerateHighInspection systemsBasic camera setupAdvanced vision and testingComprehensive in-line analyticsInstallation and commissioningModerateModerate to highHighValidation and documentationModerateHighHighPackaging and logistics integrationLow to moderateModerateHighAs the table suggests, total investment rises sharply once advanced inspection, data integration, and full factory coordination are added. Still, these features often protect long-term profitability.
var ctx4 = document.getElementById(‘comparisonChartSupplierFit’).getContext(‘2d’);var chart4 = new Chart(ctx4, {type: ‘bar’,data: {labels: [‘Compliance support’, ‘Customization’, ‘Manufacturing depth’, ‘Turnkey ability’, ‘After-sales service’, ‘Cost efficiency’],datasets: [{label: ‘Integrated engineering supplier score’,data: [92, 88, 90, 94, 86, 84],backgroundColor: ‘rgb(153, 102, 255)’},{label: ‘Basic machine-only supplier score’,data: [63, 58, 55, 40, 52, 78],backgroundColor: ‘rgb(201, 203, 207)’}]},options: {responsive: true,maintainAspectRatio: false}});The most common investment mistake is focusing on nominal speed instead of validated output. A line rated at high speed on paper may underperform if the product design is not mature, material consistency is poor, or inspection logic is unstable. Buyers should therefore review sustained output, not just peak mechanical speed.
Another risk is weak design transfer. If the syringe geometry and auto-disable mechanism are not fully compatible with the assembly system, startup can be delayed by repeated tuning. Early DFM and process reviews are essential. U.S. project teams should involve QA, operations, procurement, packaging, and maintenance from the start, not only engineering.
Supply chain risk is also important. Some projects assume all molded components, needles, packaging films, and elastomer parts will remain easily available. In reality, qualification of secondary suppliers is often necessary. Facilities located far from major logistics corridors may also face longer inbound lead times unless inventory planning is disciplined.
Utility and layout risk should not be underestimated. Compressed air quality, electrostatic control, environmental monitoring, and product flow all influence line performance. Plants near humid coastal climates or hot inland regions such as Florida, Texas, and Arizona may need specific environmental strategies to maintain consistent operation.
Service continuity is another risk area. If spare parts, remote diagnostics, and troubleshooting support are unclear, downtime can become expensive. For this reason, buyers should request recommended spare parts lists, response commitments, and training plans before signing.
For investors looking at a broader equipment portfolio, it can be useful to review available pharmaceutical and medical device machinery options to ensure future expansion, packaging, and utility systems can be aligned under a common technical philosophy.
Risk AreaTypical CauseImpactMitigationUnderperformanceOverstated speed claimsLow actual outputRequest FAT throughput evidenceValidation delaysWeak documentation packageLate commercial startDefine document list in contractProduct mismatchUnstable component toleranceHigh reject rateRun design and material trials earlySupply disruptionSingle-source componentsProduction stoppageQualify alternate suppliersService gapsLimited technical supportExtended downtimeSecure spare parts and SLA termsBudget overrunMissing utility and cleanroom costsProject stressUse full lifecycle budgetingThis risk framework is especially useful for board-level investment reviews and internal capital approval memos.
In real-world projects, outcomes often depend on how well the line fits the broader factory plan. A Midwestern medical consumables company may need a medium-speed line with fast changeover to serve hospital and distributor channels. A Gulf Coast exporter may care more about volume and port access through Houston. A Northeast project near Newark or Philadelphia may prioritize warehouse automation and regulatory documentation because labor and floor space are expensive.
One common case structure in the U.S. is phased localization. A company begins with packaging or final assembly, validates market demand, and then adds higher automation or upstream component integration later. Another is greenfield expansion, where the investor wants a more complete platform from day one, including intelligent conveying, quality documentation, and layout coordination.
Local supplier evaluation should include machine integrators, cleanroom contractors, packaging material vendors, test fixture providers, and warehouse automation partners. Domestic support capability is valuable, but international engineering breadth can also be a strength when the supplier has extensive regulated project experience and strong delivery systems.
From a technology standpoint, IVEN Pharmatech Engineering is often relevant for buyers who want more than a stand-alone machine. The company is known for integrated pharmaceutical and medical device engineering, including filling and packaging machinery, water treatment systems, intelligent conveying and logistics systems, and specialized production equipment for medical consumables. That broader technical base can help when a syringe line must operate within a larger regulated manufacturing ecosystem.
From a manufacturing perspective, IVEN has specialized production resources in Shanghai and long-term experience building equipment for global customers. Its background in multiple equipment categories and large installed project volume can be useful for customers who care about customization, durability, and coordinated factory solutions rather than only basic assembly hardware.
From a service perspective, IVEN supports customers through feasibility analysis, engineering design, equipment selection, installation, commissioning, validation-oriented assistance, training, and lifecycle optimization. For U.S. investors, that service depth matters because project risk often comes from execution gaps between equipment supply and production readiness. If you are planning a line or a full factory program, you can contact the team for a technical consultation and compare options based on your product, capacity, and compliance goals.
1. Is an auto-disable syringe production line only for vaccine projects?No. Vaccination is a major application, but the line can also support public health distribution, humanitarian supply, institutional procurement, and export-oriented medical consumables production.
2. Does the line fall under pharmaceutical equipment or medical device equipment?It is primarily medical device manufacturing equipment, but it is often evaluated within pharmaceutical investment plans because syringes are critical drug delivery consumables and must operate under strict quality systems.
3. What capacity should a first-time U.S. investor choose?That depends on annual demand, product mix, and contract visibility. Many first-time investors start with a mid-speed configuration that allows commercial output without overcommitting capital.
4. How important is validation support from the supplier?Very important. Documentation quality, FAT/SAT execution, and IQ/OQ/PQ support can strongly affect startup timing, compliance confidence, and audit readiness.
5. What is the difference between auto-disable and standard disposable syringes?A standard disposable syringe is intended for single use, but an auto-disable syringe includes a mechanical feature that actively prevents reuse after injection.
6. Can this type of line be integrated with packaging and warehouse automation?Yes. Many advanced projects connect the line with cartoning, logistics systems, and warehouse controls to improve flow, reduce manual handling, and support traceability.
7. What are the biggest hidden costs?Common hidden costs include cleanroom modifications, utility upgrades, validation activities, spare parts, operator training, packaging development, and reject reduction during ramp-up.
8. What future trends should buyers watch in 2026?Key trends include more digital monitoring, stronger documentation expectations, energy efficiency, better reject analytics, sustainability-focused design, and broader interest in localized supply resilience.
-
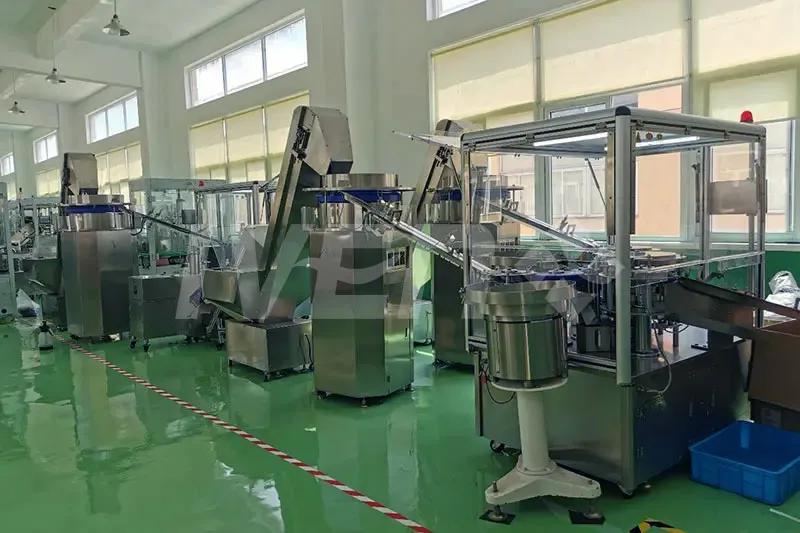
United States Guide to Syringe Barrel Molding Machines
In the United States, a syringe barrel molding machine is a specialized production system used to manufacture high-precision plastic syringe barrels for medical and pharmaceutical applications. It is a critical investment for companies expanding sterile injectables, prefilled syringe platforms, and medical consumables production under FDA and cGMP expectations. For large manufacturers, contract development and manufacturing organizations, and medical device plants, the machine is not just molding equipment; it is part of a validated quality system that affects dimensional consistency, particulate control, output efficiency, and downstream assembly performance.
Demand is increasing across major U.S. pharmaceutical corridors such as New Jersey, Massachusetts, California, Texas, and North Carolina. Facilities near logistics hubs including Los Angeles, Chicago, Houston, Savannah, and the Port of New York and New Jersey often evaluate syringe barrel molding technology as part of broader factory modernization programs. Buyers usually compare machine stability, cavity count, cleanroom compatibility, automation level, resin suitability, energy performance, traceability, and supplier validation support before making a purchase decision.
A syringe barrel molding machine matters because it directly determines whether a producer can achieve high-volume, repeatable, and compliant manufacturing of syringe components used in sterile drug delivery. In U.S. pharmaceutical production, syringe barrels must meet strict tolerances for inner diameter, flange geometry, transparency, and mechanical integrity. Even small molding deviations can create problems in siliconization, plunger movement, graduation printing, needle bonding, packaging, and final drug filling.
For that reason, large manufacturers in the United States usually evaluate this equipment during capacity expansion, line replacement, or greenfield project planning. The decision often sits at the intersection of engineering, quality assurance, regulatory affairs, operations, procurement, and finance. A good system reduces scrap, stabilizes cycle time, simplifies maintenance, and supports compliance documentation. A poor system may increase validation delays, operator intervention, and downstream rejection rates.
From a business perspective, the best syringe barrel molding machine can shorten lead times for domestic supply, reduce dependence on imported consumables, and improve resilience against freight disruptions through ports such as Long Beach or Newark. It also helps companies respond to rising U.S. demand for vaccine delivery systems, biologic injections, and self-administration devices.
Why U.S. Buyers Prioritize Syringe Barrel Molding Equipment Decision Factor Why It Matters Operational Impact Dimensional precision Essential for smooth plunger movement and leak integrity Lower reject rates in assembly and filling Cleanroom suitability Supports medical and pharmaceutical contamination control Reduced particulate risk High output stability Required for large-volume healthcare supply contracts Predictable planning and lower downtime Validation support Needed for IQ, OQ, PQ and documentation readiness Faster regulatory acceptance Automation integration Improves transfer to inspection, printing, and packaging Less labor dependency Resin compatibility Different drug delivery formats require different materials Broader product flexibility Energy efficiency Utility costs are significant in U.S. manufacturing plants Better long-term operating economicsThe table above shows that the investment case goes well beyond molding speed. U.S. buyers increasingly focus on the total manufacturing ecosystem around the machine, especially when building domestic medical supply capacity.
A syringe barrel molding machine is typically an injection molding system designed to produce syringe barrels from medical-grade polymer materials such as polypropylene or cyclic olefin-based plastics, depending on the application. The system may include resin drying, precision injection, mold temperature control, hot runner systems, robotic take-out, in-line visual inspection, conveying, and automated packing interfaces.
In pharmaceutical production, the machine is used to manufacture the barrel body of disposable syringes or prefilled syringe components. These barrels are then transferred to downstream processes such as tip forming, needle attachment, printing, siliconization, plunger assembly, sterilization preparation, and final packaging. In integrated projects, the molding equipment may be only one section of a broader medical consumables line.
Its most common uses include standard disposable syringes, insulin syringes, vaccine syringes, irrigation syringes, oral dosing syringes, and prefilled syringe platforms used in biologics and specialty injectables. In every case, consistency is vital. Barrel wall thickness, tip structure, graduation clarity, and flash control all affect final product quality.
Companies assessing factory-wide development can review integrated engineering and facility planning support through turnkey pharmaceutical project solutions when syringe component production is part of a new plant or expansion program.
Common Uses of Syringe Barrel Molding Machines in Pharmaceutical Manufacturing Application Typical End Market Key Quality Requirement Disposable medical syringes Hospitals and clinics Leak-tight performance and transparency Vaccination syringes Public health programs High-volume consistency Insulin syringes Diabetes care Fine graduation accuracy Prefilled syringe barrels Biologics and specialty drugs Tight dimensional tolerances Oral dosing syringes Pediatrics and home care Smooth plunger action Irrigation syringes Surgical and wound care Mechanical strength Custom diagnostic syringes Laboratories and device makers Tailored geometry and reliable molding repeatabilityThis table illustrates how the same core molding technology supports several product categories, but each use case shifts the quality priorities. That is why the equipment specification should always reflect the intended product portfolio.
The main application of a syringe barrel molding machine is efficient component production at scale, but the strategic benefits are broader. In modern pharmaceutical manufacturing, buyers want output, traceability, flexibility, and compliance together. This is particularly true in the United States, where shortages of medical consumables can quickly become national procurement issues.
Key benefits include lower unit cost at higher output volumes, stable product quality, lower contamination risk with automated handling, and easier integration with MES, SCADA, and electronic batch record environments. When connected to robotic extraction and closed conveying, the machine can reduce manual contact and improve line hygiene. It can also support serialized pallet or box handling for warehouse automation in larger plants.
Another benefit is manufacturing localization. With pressure to increase U.S.-based medical supply production, companies in regions like Dallas-Fort Worth, Raleigh-Durham, and greater Philadelphia increasingly examine how local molding capacity can support hospital systems, federal programs, and private-label device supply chains.
On the technology side, experienced engineering providers can help match molding output with purified utilities, cleanroom zoning, material logistics, and downstream assembly. IVEN Pharmatech Engineering is active in this type of technical coordination, combining pharmaceutical engineering know-how with equipment customization for regulated production environments. More about the company’s background can be found on its company overview page.
var ctx1 = document.getElementById(‘lineChartMarketGrowth’).getContext(‘2d’);var chart1 = new Chart(ctx1, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘U.S. market demand index for syringe barrel molding equipment’, data: [68, 74, 81, 89, 97, 108], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.1)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart above reflects a realistic demand trend seen in U.S. capacity planning: growth is being pushed by biologics, vaccine readiness, reshoring, and medical consumables security. Buyers should interpret this as a sign that supplier lead time and early engineering engagement are becoming more important.
There is no single best syringe barrel molding machine for every plant. The right choice depends on production scale, barrel size range, automation strategy, and regulatory expectations. Broadly, machines are differentiated by clamp force, number of cavities, all-electric versus hybrid drive, hot runner design, cycle time, automation level, and compatibility with cleanroom production.
For standard disposable syringes, high-cavitation systems are common because the economics favor large-volume production. For specialty barrels or prefilled syringe formats, manufacturers may prefer lower cavitation with higher precision control. All-electric systems are often selected for cleaner operation, energy efficiency, and repeatability, while hybrid systems may offer a balance between cost and performance.
Technical options often include automatic dehumidifying dryers, mold cavity pressure monitoring, robot take-out arms, camera inspection, sprue separation, anti-static handling, in-line counting, and traceability modules. Some plants also specify remote diagnostics, spare parts digitization, and predictive maintenance software.
Main Machine Types and Technical Options Machine Type Best For Main Advantage All-electric injection molding machine High-precision medical barrels Excellent repeatability and low energy use Hybrid molding machine Balanced capex and performance needs Good output with moderate investment High-cavitation system Mass-market disposable syringes Lower unit cost at scale Low-cavitation precision system Specialty or custom syringe formats Better process control for complex geometry Cleanroom-integrated machine Strict contamination-sensitive production Improved environmental control Robot-assisted take-out configuration Automated downstream transfer Reduced manual handling Vision-inspection-enabled line Quality-focused premium production Early defect detectionThis comparison helps buyers frame the machine selection process. The right model should be chosen based on the actual production objective rather than headline speed alone.
In most medical consumables scenarios, injection molding remains the dominant technology for syringe barrel production. However, some buyers also compare alternative methods or supply models such as outsourced barrel procurement, contract molding, glass-based systems for certain prefilled formats, or different plastic forming technologies for niche applications.
Injection molding is usually preferred because it offers high precision, fast cycles, and scalable economics. Outsourcing may reduce initial capex but can increase supply risk, dependence on external quality systems, and lead-time variability. Glass barrels can be suitable for some sensitive drug products, but they involve different breakage, handling, and cost considerations. For many disposable syringe applications, precision polymer molding remains the most practical route.
U.S. buyers should also compare domestic ownership of tooling and molds, intellectual property protection, maintenance support location, and spare part response time. For plants supplying federal or healthcare network contracts, control over the production chain can be a major advantage.
var ctx2 = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, { type: ‘bar’, data: { labels: [‘Hospitals’, ‘Vaccines’, ‘Biologics’, ‘Diagnostics’, ‘Home Care’, ‘OEM Devices’], datasets: [{ label: ‘Estimated demand index for syringe components in the U.S.’, data: [88, 95, 91, 72, 84, 77], backgroundColor: [ ‘rgb(255, 99, 132)’, ‘rgb(54, 162, 235)’, ‘rgb(255, 206, 86)’, ‘rgb(75, 192, 192)’, ‘rgb(153, 102, 255)’, ‘rgb(255, 159, 64)’ ] }] }, options: { responsive: true, maintainAspectRatio: false }}); Injection Molding Compared with Alternative Approaches Option Strength Limitation In-house injection molding Control, speed, quality integration Higher upfront investment Contract molding Lower immediate capex Less control over capacity and priorities Imported finished barrels Simple procurement model Exposure to freight and trade disruptions Glass barrel sourcing Suitable for select drug products Higher fragility and different handling needs Hybrid local sourcing plus molding Flexible risk management More complex supply planning Legacy manual production Low automation cost Poor consistency and labor intensity Fully automated molding cell Best for scale and traceability Requires careful integration and validationThe chart and table show that technology choice is ultimately a risk-and-control decision. For most U.S. pharmaceutical and medical device investors, in-house automated injection molding offers the strongest long-term position when volume justifies the capital spend.
The U.S. market for syringe barrel molding machine investments is supported by several structural drivers: growth in injectable therapies, expansion of self-administration drug delivery, emergency preparedness programs, and reshoring of essential medical consumables. CDMOs and medical device manufacturers are also increasing interest, especially where domestic production improves customer confidence and procurement resilience.
From a geographic perspective, activity is especially visible around Boston, San Diego, Minneapolis, Indianapolis, and New Jersey, where pharmaceutical, biotech, and medical device ecosystems overlap. Logistics considerations matter too. Proximity to ports such as Houston or Savannah can help imported machinery projects, while inland hubs like Chicago and Memphis strengthen domestic distribution planning.
Looking toward 2026, three trends stand out. First, smarter automation will continue to expand, including vision systems, digital mold monitoring, and predictive maintenance. Second, regulatory expectations around data integrity, process traceability, and quality-by-design will deepen. Third, sustainability will move from a marketing topic to an engineering requirement, influencing servo systems, resin waste reduction, cooling optimization, and packaging efficiency.
var ctx3 = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var chart3 = new Chart(ctx3, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Shift toward automated and compliant molding lines’, data: [42, 49, 57, 66, 76, 87], fill: true, backgroundColor: ‘rgba(75, 192, 192, 0.25)’, borderColor: ‘rgb(75, 192, 192)’, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});Policy also plays a role. In the United States, public discussions around supply chain security, domestic manufacturing incentives, and critical healthcare product availability are likely to support continued capital investment. That does not guarantee every project will be successful, but it does increase the strategic relevance of selecting robust molding technology.
Choosing a supplier requires more than comparing quotations. U.S. buyers should assess technical depth, regulatory familiarity, customization ability, manufacturing capacity, after-sales support, and proven references. A supplier that understands medical-grade production and validation will usually be more valuable than a low-price provider with limited life sciences experience.
One effective evaluation method is to divide your review into three areas: technological capabilities, manufacturing capabilities, and service capabilities. On the technology side, examine molding precision, automation integration, cleanroom design awareness, and support for validation documentation. On the manufacturing side, ask about factory scale, machining quality, component sourcing, and consistency across builds. On the service side, review installation, commissioning, training, spare parts support, and responsiveness for U.S. customers.
IVEN Pharmatech Engineering is known for integrating equipment supply with broader pharmaceutical engineering expertise. Its strengths include customized line design, regulated project understanding, and international compliance orientation for standards such as EU GMP, FDA cGMP, WHO GMP, and PIC/S-aligned projects. The company also operates specialized manufacturing plants and provides integrated project support rather than only stand-alone machine shipment. Buyers looking for tailored equipment can review available solutions through the equipment portfolio.
Supplier Evaluation Checklist for U.S. Buyers Evaluation Area What to Ask Why It Matters Regulatory understanding Can the supplier support IQ/OQ/PQ documentation? Reduces compliance risk Medical molding expertise How many similar syringe projects have been delivered? Shows process maturity Customization ability Can the line match your barrel sizes and automation plan? Improves fit for actual production Manufacturing quality What is the factory’s machining and assembly standard? Affects long-term reliability Support in the United States How are spare parts and technical response handled? Minimizes downtime Project management Is there a clear schedule, FAT, and installation plan? Prevents delays and cost overruns Lifecycle service Does the supplier offer training and optimization later? Improves ROI after startupThe table above provides a practical buying framework. It is especially useful for teams involving procurement, engineering, validation, and executive leadership, because each group can score the supplier from a different perspective.
The cost of a syringe barrel molding machine varies significantly depending on clamp size, cavitation, automation, tooling complexity, cleanroom compatibility, and downstream integration. A basic machine package may appear affordable at first glance, but a true project budget should also include mold sets, robotics, utility connections, environmental control, qualification, shipping, site preparation, operator training, and spare parts.
For U.S. buyers, freight, customs handling, insurance, and installation labor can materially affect total project cost. Plants near major coastal ports may benefit from smoother inbound logistics, while inland sites may need additional transport planning. Budgeting should also include production ramp-up losses, resin qualification runs, and initial maintenance inventory.
ROI depends on utilization rate, labor reduction, scrap reduction, margin on finished syringe components, and replacement of external procurement. If a company currently imports barrels or buys them from a contract supplier, in-house molding can create a strong return once throughput is high enough. However, underutilized machines can weaken payback.
var ctx4 = document.getElementById(‘comparisonChartSupplierProduct’).getContext(‘2d’);var chart4 = new Chart(ctx4, { type: ‘bar’, data: { labels: [‘Precision’, ‘Automation’, ‘Validation Support’, ‘Energy Use’, ‘Service’, ‘Scalability’], datasets: [{ label: ‘Typical premium medical-grade system score’, data: [92, 89, 94, 83, 87, 91], backgroundColor: ‘rgb(153, 102, 255)’ },{ label: ‘Typical economy industrial system score’, data: [71, 58, 49, 64, 52, 68], backgroundColor: ‘rgb(201, 203, 207)’ }] }, options: { responsive: true, maintainAspectRatio: false }}); Typical Budget Categories for a Syringe Barrel Molding Project Budget Item Cost Influence Planning Note Main molding machine High Core equipment cost varies by precision and tonnage Mold and hot runner system High Often the most quality-sensitive element Robotics and automation Medium to high Important for labor savings and contamination control Cleanroom and utilities integration Medium Can increase sharply in brownfield retrofits Validation and documentation Medium Must not be underestimated in pharma settings Training and commissioning Medium Directly affects startup speed Spare parts and maintenance stock Low to medium Improves uptime during first yearIn practical terms, a well-planned U.S. project usually evaluates both direct financial ROI and strategic ROI. Strategic ROI may include domestic supply assurance, reduced dependence on volatile shipping routes, improved customer confidence, and readiness for future product launches.
The biggest risks are usually not visible in the first quotation. One common issue is under-specifying the line. A machine may meet nominal output targets but fail to deliver the repeatability, cleanliness, or automation needed for pharmaceutical-grade performance. Another risk is poor integration between molding, inspection, and packaging, which causes bottlenecks and unplanned labor dependence.
Validation delay is another major concern. If user requirement specifications, FAT criteria, and documentation expectations are not aligned early, startup can slip by months. Mold quality is also critical. Even a good injection unit cannot compensate for poor mold design, uneven cooling, or unstable cavity performance.
Buyers should also consider future product flexibility. A system optimized only for one barrel size may not support new commercial opportunities. Finally, supplier support matters. If a critical part fails and technical response is slow, production losses can outweigh the original savings from choosing a cheaper machine.
From a manufacturing capability perspective, IVEN has built its reputation around specialized production facilities, durable stainless-steel equipment design, and large-scale line delivery experience across global pharmaceutical and medical device projects. From a service capability perspective, it supports customers through feasibility, engineering design, equipment customization, installation, commissioning, validation assistance, documentation, training, and ongoing optimization. U.S. companies considering direct discussion can use the contact page to start a technical inquiry.
Major Investment Risks and How to Reduce Them Risk Likely Consequence Mitigation Incorrect machine sizing Low efficiency or wasted capital Use realistic volume forecasting Weak mold design Quality instability and scrap Audit mold engineering before approval Insufficient validation planning Delayed startup Define URS, FAT, IQ/OQ/PQ scope early Poor automation integration Manual bottlenecks and contamination risk Map full process flow before purchase Inadequate supplier support Long downtime Secure parts and service commitments Regulatory mismatch Non-compliance findings Choose experienced life science suppliers Utility underestimation Installation overrun and performance issues Perform full site utility assessmentThe table makes clear that capital risk can be controlled if engineering and procurement teams treat the project as a full production system, not just a machine purchase.
What is the typical output of a syringe barrel molding machine?Output depends on cavity count, cycle time, and product size. High-cavitation systems for standard disposable syringes can achieve very high hourly output, while specialty barrels prioritize precision over absolute volume.
Is an all-electric machine better for pharmaceutical use?In many cases, yes. All-electric systems often offer cleaner operation, better repeatability, and lower energy consumption. However, the best choice still depends on your product format, budget, and utility profile.
Can a syringe barrel molding machine be used for prefilled syringe production?It can be used to produce the barrel component for certain polymer-based prefilled syringe systems. The full prefilled syringe program also requires compatibility with downstream assembly, sterilization strategy, and final filling operations.
How important is cleanroom installation?Very important for medical and pharmaceutical applications. The required room classification depends on product type and process design, but contamination control should be considered from the start.
What materials are commonly used?Medical-grade polypropylene is common for many disposable syringes. Some advanced applications may use cyclic olefin polymers or other engineered materials depending on clarity, barrier, and drug compatibility needs.
How long does implementation usually take?Lead time varies based on customization, mold complexity, FAT scheduling, shipment, site readiness, and validation scope. For U.S. projects, planning should include logistics through ports or inland routes plus commissioning and qualification time.
What should U.S. buyers ask suppliers first?Ask about similar delivered projects, mold design capability, validation documentation, automation integration, spare parts support, and expected service response for the United States.
Does turnkey support make a difference?Yes. When the syringe barrel molding machine is part of a broader manufacturing buildout, turnkey coordination can reduce layout mistakes, schedule conflicts, and integration problems across utilities, cleanrooms, and downstream lines.
What 2026 trends should investors watch?Watch for higher automation, stronger digital traceability, energy-efficient servo systems, smarter mold monitoring, sustainability-driven resin waste reduction, and policy pressure for resilient domestic manufacturing.
How should a buyer shortlist suppliers?Use a cross-functional scorecard covering technology, manufacturing quality, lifecycle service, compliance understanding, U.S. support, and total cost of ownership rather than only purchase price.
For companies in the United States evaluating syringe barrel molding machine investments, the strongest results usually come from a disciplined approach: define the product roadmap, align engineering and quality requirements early, compare supplier capabilities in depth, and select a partner able to support the full lifecycle of the project. That is especially important in a market where compliance, speed, and supply assurance are all strategic priorities.