Syringe Production Line Guide for the United States
In the United States, a syringe production line is a high-value manufacturing system used to produce sterile syringes, syringe components, or prefilled syringe formats at industrial scale under strict FDA, cGMP, and quality assurance requirements. For pharmaceutical companies, CDMOs, and medical device manufacturers, it is not just a machine purchase. It is a strategic investment that affects regulatory readiness, production capacity, labor efficiency, product integrity, and long-term cost control. As U.S. facilities in Boston, New Jersey, Chicago, Houston, and San Diego continue expanding injectable capacity, the demand for advanced syringe manufacturing and prefilled syringe lines is rising alongside biologics, vaccines, and specialty drug delivery.
Companies evaluating a syringe production line usually want to answer five core questions quickly: what the line actually includes, whether it fits sterile drug or device manufacturing, how it compares with alternative packaging technologies, what budget is realistic, and which supplier can support validation and long-term operation in the United States. The answers depend on production speed, barrel format, nest or bulk handling, filling accuracy, automation level, cleanroom integration, and the expected regulatory pathway. Buyers also need to factor in utilities, layout, qualification, digital traceability, and service response.
For organizations planning new capacity or modernization, it is useful to review both standalone equipment and broader factory integration. Many projects succeed when equipment selection is aligned early with water systems, clean utilities, logistics flow, isolator strategy, and secondary packaging. Companies that need a broader plant perspective can review turnkey pharmaceutical engineering solutions alongside equipment planning rather than treating the syringe line as an isolated purchase.
Quick Answer: Why a Syringe Production Line Matters in the United States

A syringe production line is a coordinated manufacturing platform that can include barrel feeding, washing, siliconization, sterilization interface, filling, stoppering, plunger insertion, needle assembly, inspection, labeling, and packaging. In some projects, the term refers specifically to a prefilled syringe filling line; in others, it covers upstream syringe component production for medical consumables. In the United States market, the strongest demand comes from injectable drug manufacturers, biologics producers, vaccine plants, hospital supply chains, and contract manufacturers serving national distribution networks through hubs such as Newark, Los Angeles, Savannah, and Houston.
The line matters because U.S. buyers are under pressure to achieve higher throughput without compromising sterility assurance. Manual or semi-automatic production may be acceptable for pilot runs, but commercial-scale injectable production requires tighter process control, lower particulate risk, more complete batch data, and repeatable output. A properly specified line can reduce operator intervention, improve fill-weight consistency, support annex-style contamination control strategies, and make plant expansion more predictable.
| Decision Area | Why It Matters | Typical U.S. Buyer Concern | Impact on Production |
|---|---|---|---|
| Regulatory compliance | Supports FDA inspection readiness | cGMP, data integrity, validation documentation | Lower audit risk |
| Sterility assurance | Protects drug and device safety | Intervention reduction, isolator integration | Fewer contamination events |
| Automation level | Reduces labor dependency | Operator shortages in major U.S. markets | Higher consistency |
| Format flexibility | Handles multiple syringe sizes | Need to support varied product portfolios | Faster product changeover |
| Speed and output | Determines commercial viability | Meeting hospital and retail demand | Better capacity utilization |
| Lifecycle service | Keeps uptime stable after installation | Spare parts and remote support in the United States | Lower downtime |
The table above shows why procurement teams cannot evaluate a syringe production line only by nameplate speed. A lower-priced line that lacks validation depth, spare part planning, or reliable in-process control can become more expensive after startup.
What Is a Syringe Production Line and What Is It Used For in Pharmaceutical Production?

In pharmaceutical production, a syringe production line is used to manufacture or process syringes in a controlled sequence. The exact configuration depends on whether the buyer makes disposable empty syringes, safety syringes, luer-lock or luer-slip formats, or prefilled syringes containing injectable drug products. For pharmaceutical plants, the most common meaning is a prefilled syringe line that prepares sterile syringes for filling, dispenses precise drug volumes, closes the container, and transfers units to inspection and packaging.
These lines are widely used for biologics, anticoagulants, vaccines, ophthalmic injectables, emergency drugs, and specialty therapies that benefit from accurate unit dosing and ready-to-use administration. Compared with vials, prefilled syringes can improve user convenience, reduce dosing errors, and enhance hospital workflow. This is particularly relevant in U.S. health systems where medication safety, nurse efficiency, and outpatient self-administration are growing priorities.
A modern line may include recipe management, servo-controlled filling, no-container-no-fill logic, vision inspection, reject segregation, environmental monitoring interface, and electronic batch record connectivity. In regulated environments, the line also needs to support installation qualification, operational qualification, and performance qualification, plus documentation that can satisfy both internal QA teams and external inspectors.
| Production Stage | Main Function | Common Equipment | Quality Focus |
|---|---|---|---|
| Component infeed | Feeds barrels, plungers, stoppers, needles | Feeders, trays, de-nesters | Orientation accuracy |
| Cleaning or preparation | Removes particles or prepares surfaces | Washer, air rinse, siliconization unit | Particulate control |
| Sterile transfer | Moves components into aseptic zone | RABS, isolator, sterile tunnel interface | Contamination prevention |
| Filling | Dispenses drug product | Peristaltic or piston filler | Dose accuracy |
| Closing and assembly | Stoppering, plunger insertion, needle shielding | Closure stations, insertion systems | Container closure integrity |
| Inspection and packaging | Checks defects and prepares saleable output | Vision systems, labelers, cartoners | Defect detection and traceability |
This process structure explains why syringe production lines often involve both drug product engineering and medical device handling expertise. Facilities in New Jersey and North Carolina often evaluate them as part of broader injectable expansion plans rather than as standalone line items.
Main Applications and Benefits of Syringe Production Line in Modern Pharmaceutical Manufacturing

The main applications of a syringe production line in the United States span commercial injectable pharmaceuticals, contract manufacturing, emergency stockpiles, biologic therapies, and medical consumables. Hospitals, outpatient clinics, military supply channels, and retail specialty pharmacies all influence demand. High-growth therapeutic areas include autoimmune biologics, GLP-1 related injectable delivery formats, anticoagulants, fertility medications, and vaccines.
The benefits are operational and commercial. First, prefilled syringe manufacturing supports ready-to-use dosing, which is valuable in hospitals and ambulatory care settings. Second, automated lines reduce handling and may lower contamination risk relative to more manual processes. Third, product differentiation is often stronger with prefilled syringes, especially when combined with safety devices, needle shields, or patient-friendly packaging. Fourth, lines with flexible format changeover help manufacturers serve both clinical and commercial runs.
From a finance perspective, the line can also reduce hidden costs tied to waste, rejects, overtime labor, and line clearance complexity. In markets with high labor costs such as California, Massachusetts, and Illinois, automation can materially affect cost per unit. For organizations exploring available systems, reviewing the equipment portfolio can help compare line configurations and upstream/downstream integration options.
| Application | Typical Product | Why Syringe Format Is Chosen | Operational Benefit |
|---|---|---|---|
| Biologics | Monoclonal antibody injections | Precise unit dose and patient convenience | Higher value-added packaging |
| Vaccines | Ready-to-administer doses | Fast clinical use and reduced preparation time | Improved throughput in care settings |
| Hospital injectables | Emergency and anesthesia products | Lower bedside preparation burden | Safer workflow |
| Anticoagulants | Heparin or similar products | Routine self-administration suitability | Better patient adherence |
| Ophthalmic and specialty care | Small-volume sterile injectables | High dosing precision | Reduced waste |
| Medical consumables | Empty disposable syringes | Large-volume supply for healthcare systems | Scalable manufacturing |
The benefit pattern shown above is why many U.S. producers no longer compare syringes only against container cost. They evaluate the total delivery model, including administration speed, end-user safety, and reimbursement-driven packaging preferences.
Key Types, Models and Technical Options for Syringe Production Line
Syringe production lines vary widely by end use, output level, and sterility strategy. In the U.S. market, the most common categories are disposable syringe assembly lines, prefilled syringe filling lines, nest-based lines for high-value biologics, bulk syringe lines for larger throughput, and integrated lines that connect to inspection and packaging cells. The right model depends on whether the plant prioritizes speed, flexibility, low intervention, or lower capital intensity.
Technical options usually include filling technology, closure system, infeed style, cleanroom architecture, and digital control depth. Peristaltic pumps are often favored for gentle product handling and easier cleaning in some applications, while rotary piston systems may be selected for high repeatability depending on viscosity and formulation needs. For barrels, glass remains common in many applications, but polymer formats are increasingly evaluated for break resistance and logistics efficiency.
On the technology side, some international suppliers stand out because they combine pharmaceutical engineering with adjacent utility and logistics systems rather than supplying only one machine. IVEN Pharmatech Engineering, for example, is known in the industry for integrating pharmaceutical filling, water systems, logistics, and medical consumables equipment into broader compliant production solutions. Its technological capabilities are particularly relevant when buyers need not just a filler, but a coordinated system that aligns with cGMP layout logic, aseptic process design, and validation documentation. More background is available on the company overview page.
| Line Type | Best For | Typical Speed Range | Main Advantage |
|---|---|---|---|
| Semi-automatic syringe line | R&D, pilot, low-volume specialty runs | 1,000 to 6,000 units/hour | Lower entry cost |
| Automatic bulk syringe filling line | Commercial generic injectables | 6,000 to 18,000 units/hour | High throughput |
| Nest-based prefilled syringe line | Biologics and sensitive formulations | 3,000 to 12,000 units/hour | Lower handling stress |
| Integrated isolator line | High aseptic assurance environments | 4,000 to 15,000 units/hour | Reduced contamination risk |
| Disposable syringe assembly line | Medical consumables manufacturing | 10,000 to 40,000 units/hour | Scale for device output |
| Turnkey syringe plant line | New factories or full modernization | Project dependent | Unified engineering and validation |
The technical options in this table should always be considered together with format requirements. A line for 1 mL long glass syringes used in biologics will differ significantly from a line designed for larger disposable medical syringes. U.S. buyers also increasingly request MES connectivity, audit trail functions, and recipe protection as standard, not premium, features.
Syringe Production Line vs Alternative Technologies: Which Solution Fits Your Needs?
A syringe production line is not automatically the best answer for every injectable product. Many companies compare it with vial filling, ampoule filling, cartridges, BFS formats, or outsourced contract packaging. The right choice depends on product sensitivity, shelf-life data, dosing model, intended user, logistics chain, and commercial strategy.
Vials remain attractive for multi-dose products, lyophilization workflows, and some flexible fill-finish operations. Ampoules are still used in selected markets but are less preferred where convenience and breakage concerns matter. Cartridges are important for pens and autoinjectors. Prefilled syringes, however, often win when ready-to-use delivery, patient convenience, and premium product positioning are priorities. In the United States, that advantage is especially visible in specialty pharmacy and self-injection therapies.
| Technology | Strength | Limitation | Best Fit |
|---|---|---|---|
| Prefilled syringe line | Ready-to-use, accurate unit dose | Higher capital and component complexity | Biologics, specialty injectables |
| Vial filling line | Flexible and widely established | More end-user preparation | Hospitals, lyophilized products |
| Ampoule line | Strong container integrity in some uses | Breakage and handling limitations | Selected sterile liquids |
| Cartridge line | Suitable for pens and devices | Device ecosystem dependency | Diabetes and self-injection platforms |
| BFS technology | Integrated forming and filling | Not ideal for all formulations or syringe needs | High-volume sterile unit doses |
| Outsourced fill-finish | Lower initial capex | Less control and capacity dependence | Early-stage or bridge manufacturing |
For a company launching a specialty injectable in the United States, the practical question is often not “which technology is best in theory” but “which technology matches our forecast, quality system, and commercialization timeline.” If the product will move through national distribution from East Coast warehousing near Newark or Philadelphia to West Coast networks through Los Angeles, a robust and user-friendly final presentation may justify the added investment of prefilled syringes.
Market Overview and Future Trends for Syringe Production Line in Pharmaceutical Manufacturing
The U.S. market for syringe production lines is being driven by multiple factors at once: growing demand for injectable biologics, reshoring and supply-chain resilience initiatives, hospital preference for ready-to-administer formats, and modernization of aging pharmaceutical infrastructure. The strongest investment activity is often concentrated in the Northeast corridor, the Mid-Atlantic, Texas, the Midwest biotech belt, and California. Buyers in these regions are also influenced by local labor costs, utility availability, and proximity to airports and seaports such as the Port of New York and New Jersey, Port of Houston, Port of Long Beach, and Savannah.
Looking toward 2026, three trend groups matter most. First is technology: more isolated filling environments, robotics, machine vision, predictive maintenance, and data integration with MES and ERP systems. Second is policy and compliance: stronger expectations around contamination control, electronic records, cybersecurity, and traceable batch history. Third is sustainability: lower energy consumption, reduced compressed air loss, better cleanroom zoning efficiency, recyclable packaging considerations, and more responsible water use in related utility systems.
Another major trend is integration. Buyers no longer want separate islands of automation that require multiple vendors to coordinate after purchase. Instead, they prefer suppliers that can align line equipment with purified water systems, clean steam, warehousing, and end-of-line packing. This is especially important for larger U.S. capital projects where delays in engineering interfaces can cost millions.
These trend lines reflect a clear U.S. shift toward higher automation and stronger contamination control. By 2026, buyers will increasingly expect remote diagnostics, digital maintenance logs, and energy-aware designs as baseline features rather than optional upgrades.
How to Choose a Reliable Syringe Production Line Manufacturer or Supplier
Choosing a reliable supplier in the United States market requires more than comparing quotations. A credible manufacturer or engineering partner should demonstrate regulatory understanding, stable manufacturing quality, installation references, process customization capability, and responsive after-sales support. Procurement teams should ask for FAT structure, SAT planning, validation document samples, spare parts philosophy, software access policy, and evidence of long-term service support.
Manufacturing capability is one of the most overlooked evaluation areas. A supplier that operates specialized production plants, controls critical fabrication standards, and can coordinate multiple equipment categories usually has better schedule control and quality consistency. IVEN Pharmatech Engineering is often considered by buyers seeking this broader capability because it combines dedicated manufacturing bases for pharmaceutical filling and packaging systems, water treatment, intelligent conveying, and blood collection tube equipment. That manufacturing depth can be valuable for syringe projects requiring coordinated interfaces rather than a single machine delivered without plant context.
U.S. buyers should also consider whether the supplier understands local expectations such as FDA-oriented documentation, cGMP training, SAT execution, and practical communication across time zones. If a project is intended for a new plant in states such as New Jersey, Indiana, or Texas, the best supplier is usually the one that can support design review early, not the one that simply ships equipment fastest.
| Supplier Checkpoint | What to Verify | Why It Matters | Red Flag |
|---|---|---|---|
| Regulatory experience | FDA/cGMP project references | Reduces compliance gaps | No validation examples |
| Engineering depth | Ability to customize line layout and utilities | Prevents interface failures | Only standard catalog answers |
| Manufacturing control | Own plants and fabrication oversight | Improves consistency and lead time | Heavy subcontract dependence |
| Service network | Remote support, training, parts plan | Protects uptime | Unclear response commitments |
| Documentation quality | DQ, FAT, IQ/OQ templates, manuals | Speeds qualification | Incomplete document list |
| Reference projects | Comparable syringe or aseptic lines | Confirms practical experience | No verifiable installations |
The table above should be used as a practical purchasing checklist. If you need direct discussions on project scope, layout, or qualification support, the most efficient next step is to contact the engineering team with your target output, syringe format, cleanroom class, and expected launch schedule.
Investment Cost, Budget Planning and ROI Analysis for Syringe Production Line
The investment cost for a syringe production line in the United States can vary sharply based on throughput, sterility strategy, line scope, and building readiness. A smaller semi-automatic or pilot-oriented system may represent a moderate capital outlay, while a fully integrated high-speed prefilled syringe line with isolator, inspection, and packaging can require a multi-million-dollar budget. The biggest mistake in budgeting is focusing only on the purchase price of the core machine.
Total project cost usually includes equipment, format parts, isolator or RABS, utility integration, HVAC impact, cleanroom modifications, software integration, shipping, customs, installation, SAT, validation, training, spare parts, and startup inventory. In the United States, site-specific costs can be significant due to labor, contractor rates, and compliance documentation demands. Projects in high-cost regions such as Boston or the San Francisco Bay Area may face noticeably higher installation and qualification expense than projects in some Southern manufacturing corridors.
ROI depends on more than annual unit output. Buyers should model reduced labor, lower rejects, lower contamination risk, avoided outsourcing fees, improved product presentation, and revenue acceleration from faster commercial launch. Service capability also matters here. Suppliers that provide lifecycle support, training, commissioning, technology transfer, and optimization after startup can materially improve payback because the line reaches stable performance faster. This type of end-to-end service approach is one reason some buyers choose partners with integrated engineering backgrounds rather than equipment traders.
| Cost Element | Typical Budget Weight | Why It Is Often Underestimated | Planning Note |
|---|---|---|---|
| Core line equipment | 30% to 45% | Visible price gets all the attention | Compare by scope, not headline cost |
| Aseptic enclosure | 10% to 20% | Isolation strategy changes total design | Define intervention philosophy early |
| Utilities and integration | 8% to 15% | Depends on existing plant readiness | Audit current infrastructure first |
| Installation and commissioning | 8% to 12% | Labor rates vary by state | Use local contractor assumptions |
| Validation and documentation | 6% to 12% | QA requirements expand late | Request document matrix upfront |
| Training and spare parts | 3% to 8% | Often postponed until startup | Budget for year-one support package |
A well-run ROI analysis should also estimate utilization ramp-up. Many new lines do not operate at full design speed in the first months, so realistic models should include staged performance assumptions.
| ROI Driver | Low Impact Scenario | High Impact Scenario | Resulting Benefit |
|---|---|---|---|
| Labor reduction | 10% fewer operators | 35% fewer operators | Lower annual operating cost |
| Reject reduction | 0.5% improvement | 2.0% improvement | Higher saleable output |
| Outsourcing replacement | Partial in-house production | Full internalization | Better margin control |
| Launch acceleration | 1 month faster | 4 months faster | Earlier revenue capture |
| Format flexibility | One syringe size | Multiple commercial sizes | Portfolio expansion |
| Downtime reduction | Basic service support | Preventive support and diagnostics | Improved OEE |
Key Considerations and Potential Risks When Investing in Syringe Production Line
The most important consideration is fit between product strategy and line design. If the line is oversized, capital is tied up in underutilized assets. If it is undersized, expansion arrives too soon and disrupts validated operations. U.S. buyers should also assess whether the selected format is aligned with future commercial plans such as autoinjector compatibility, cold-chain requirements, or hospital presentation preferences.
Regulatory and operational risks are equally important. Common issues include inadequate cleanroom layout, poor material-personnel flow, software validation gaps, weak vendor FAT execution, uncertain spare parts lead times, and limited local technical support. Another risk is treating utilities as an afterthought. Water quality, clean steam, compressed air, and environmental control can directly affect line performance and compliance outcomes.
Logistics risk matters too. For equipment imported into the United States, buyers should plan around customs timing, inland transport, rigging, and delivery routes to sites near ports or inland manufacturing campuses. A project destined for Houston, Memphis, or Columbus may require a different logistics strategy than one entering through Newark or Long Beach.
| Risk Area | Example Problem | Potential Consequence | Mitigation |
|---|---|---|---|
| Regulatory mismatch | Insufficient documentation | Delayed qualification | Review validation package before PO |
| Layout failure | Operator flow conflicts | Contamination and inefficiency | Perform early 3D layout review |
| Utility shortfall | Unstable compressed air or HVAC load | Line stoppage or quality deviations | Complete utility gap assessment |
| Changeover complexity | Too many manual adjustments | Low uptime and training burden | Request recipe-driven design |
| Supplier support gap | Slow troubleshooting response | Extended downtime | Define SLA and spare parts stock |
| Budget creep | Missing installation scope | Capex overrun | Use total cost model from day one |
For larger investments, many U.S. teams now run cross-functional review boards involving engineering, QA, operations, procurement, finance, and EHS before final approval. This is the most effective way to surface hidden risks early.
Case studies in the market repeatedly show that the best outcomes come when buyers define user requirement specifications clearly, select a supplier with proven integration experience, and keep qualification planning active from the first technical discussion. Projects that wait until late-stage FAT to address data integrity, recipe management, or intervention design often lose time and money.
In practical terms, “our company” value should also be measured by execution maturity. IVEN Pharmatech Engineering is frequently evaluated not only for equipment itself but for its ability to support broader project delivery through consulting, engineering design, equipment customization, installation, commissioning, validation support, training, and production optimization. For U.S. buyers seeking a partner rather than a single vendor, that service-oriented model can reduce interface risk across the full project lifecycle.
FAQ
What is included in a typical syringe production line?
A typical line may include syringe infeed, de-nesting or feeding, washing or preparation, sterile transfer, filling, stoppering, plunger insertion, inspection, labeling, cartoning, and supporting automation software. The exact scope depends on whether the project is for empty syringes or prefilled syringes.
Is a syringe production line mainly for pharmaceuticals or medical devices?
It can serve both. In pharmaceuticals, it is commonly used for prefilled sterile drug products. In medical devices, it may be used for disposable syringe assembly and packaging.
What U.S. regulations are most relevant?
FDA cGMP expectations, data integrity practices, cleanroom and aseptic processing requirements, and device-related standards where applicable are central. Validation documentation and traceability are especially important.
How much does a syringe production line cost?
Cost varies widely based on output, automation, enclosure type, and line scope. A full commercial aseptic line with isolation, inspection, and packaging can represent a major capital project, especially after installation and qualification are included.
How long does implementation take?
A realistic timeline often includes user requirement definition, design review, fabrication, FAT, shipping, installation, SAT, IQ/OQ, and ramp-up. Depending on scope, projects may take many months and should not be planned around equipment delivery alone.
Should we choose a standalone machine supplier or a turnkey partner?
If your project affects layout, utilities, warehousing, packaging, or regulatory qualification across multiple systems, a broader engineering or turnkey partner can lower coordination risk. Smaller expansions may work well with a focused standalone supplier.
What production speeds are common?
Speeds vary from low-volume pilot lines to high-speed commercial systems. The right speed should match demand forecast, product value, batch size, and available staffing rather than simply maximizing nameplate output.
Are prefilled syringes better than vials?
Not always. Prefilled syringes are often better for convenience, dosing accuracy, and user readiness, while vials may remain preferable for some formulations, lyophilized products, or more flexible fill-finish needs.
What are the most common buying mistakes in the United States?
Underestimating validation scope, ignoring total installed cost, choosing a line without enough format flexibility, and not checking service responsiveness are among the most common mistakes.
How can we compare suppliers efficiently?
Use a weighted matrix covering compliance experience, engineering depth, manufacturing capability, service model, lead time, references, and total lifecycle cost. Then request clear evidence for each score, not only sales claims.
For companies preparing expansion in the United States, the strongest purchasing strategy is to align product roadmap, facility design, and supplier capability from the beginning. Whether the goal is a single prefilled syringe filling line or a broader injectable plant modernization program, a disciplined evaluation process will produce better regulatory, financial, and operational outcomes.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
Blow Fill Seal Systems for Sterile Pharma in the United States
In the United States, blow fill seal technology is widely preferred for sterile pharmaceutical production because it forms the container, fills it, and seals it within one continuous aseptic cycle. That integrated process reduces human intervention, lowers particulate and microbial contamination risk, and supports efficient high-volume manufacturing for respiratory products, ophthalmics, injectables, and unit-dose packaging.
For U.S. manufacturers facing FDA scrutiny, rising labor costs, and demand for reliable sterile capacity, BFS equipment has become more than a niche packaging method. It is now a strategic platform for companies producing preservative-free formulations, single-dose therapies, and sensitive liquid products. Facilities in pharmaceutical hubs such as New Jersey, Boston, Raleigh-Durham, Indianapolis, Houston, and the greater Chicago region are increasingly evaluating BFS lines as part of modernization plans, especially when they need scalable aseptic output and a lower contamination profile than conventional open-container handling.
Buyers also evaluate BFS from a supply chain perspective. Ports such as Los Angeles, Long Beach, Savannah, Houston, and New York/New Jersey remain central to imported equipment logistics, spare parts planning, and factory project schedules. Whether the project is a greenfield sterile plant or a line expansion inside an existing cGMP facility, the real question is not only “What does the machine cost?” but “How will BFS affect validation, throughput, labor, utility demand, and long-term return on investment in the United States market?”
Blow fill seal technology is favored because it combines three critical steps into one enclosed process: container formation from polymer resin, sterile filling of the product, and immediate hermetic sealing. In practice, this means fewer transfers, fewer exposed surfaces, fewer operators in the critical zone, and better batch consistency. Compared with traditional vial or ampoule lines, BFS often delivers stronger contamination control, faster line speeds for unit-dose packaging, reduced dependence on preformed containers, and easier integration with modern environmental monitoring and data recording systems.
For U.S. pharmaceutical companies, this matters in several ways:
Decision FactorWhy It Matters in the United StatesBFS AdvantagePotential LimitationSterility assuranceFDA inspections focus heavily on contamination controlClosed, integrated process with less manual handlingRequires robust process validationLabor costSkilled operators and aseptic staff are expensiveLower direct intervention in critical operationsHigher automation dependenceSupply chain stabilityPreformed vial supply may fluctuateContainers are formed in-line from resinPolymer qualification is essentialProduction speedDemand spikes for inhalation and ophthalmic productsHigh output for unit-dose formatsNot ideal for every formulation typeFacility footprintU.S. expansion projects often face space constraintsIntegrated line can simplify process flowUtility and HVAC planning still criticalTotal cost of ownershipCapital planning is tightly reviewedMay lower long-term operating cost per unitInitial CAPEX can be highThe table above shows why BFS is often discussed not only by process engineers but also by quality leaders, finance teams, and plant managers. The technology solves multiple operational problems at once, which is why its business case can be compelling in U.S. sterile manufacturing.
Blow fill seal technology is an advanced aseptic packaging process primarily used for liquid pharmaceuticals and medical solutions. The machine extrudes molten polymer, usually polyethylene or polypropylene depending on the application, into a parison. A mold closes around that parison to form the container body. The newly formed container is then filled immediately with sterile product through specialized fill nozzles, and the top is sealed while the package remains inside the controlled machine environment.
The sequence generally includes:
Because the package is created just before filling, BFS avoids many contamination vectors associated with separate container manufacturing and transport. This is one reason the technology is especially suitable for inhalation solutions, ophthalmic preparations, saline, oral liquids in unit-dose containers, and certain sterile injectables.
From an engineering standpoint, the system depends on precise synchronization between thermal control, mold performance, fill accuracy, sterile air management, and in-process monitoring. Modern BFS equipment used in the United States often includes recipe management, batch records, alarm history, access controls, electronic data capture, and compatibility with plant-level SCADA or MES systems.
Process StageMain FunctionCritical Control PointTypical RiskResin meltingPrepare polymer for extrusionTemperature stabilityMaterial inconsistencyParison extrusionCreate container precursorExtrusion uniformityWall thickness variationContainer formingBlow and shape packageMold alignmentDimensional defectsSterile fillingDose product into formed containerFill volume accuracyUnderfill or overfillSealingCreate final closureSeal integrityLeakageDischarge and inspectionRelease acceptable unitsVision or leak testingUndetected rejectThis process discipline is one reason supplier capability matters so much. A BFS machine is not simply a packaging machine; it is a sterile process platform. Buyers evaluating suppliers often look closely at machine design quality, validation support, materials traceability, software architecture, and long-term spare parts availability.
Sterile drug manufacturers choose BFS for both regulatory and commercial reasons. In the United States, contamination control is increasingly viewed through a lifecycle lens: equipment design, operator activity, intervention frequency, cleaning validation, environmental control, and ongoing process verification all matter. BFS aligns well with that mindset because it reduces the number of open handling steps between container creation and final closure.
Manufacturers also value BFS when launching products that benefit from single-use packaging. Unit-dose respiratory products distributed through national pharmacy networks, preservative-free eye drops sold across major retail chains, and hospital-use solutions moving through healthcare systems all require repeatable packaging integrity and high output. BFS helps support those needs.
Key reasons U.S. manufacturers adopt BFS include:
The U.S. market is also influenced by outsourcing trends. CMOs and CDMOs in states such as New Jersey, Pennsylvania, North Carolina, and California are expanding sterile packaging options to attract pharmaceutical innovators. BFS can serve as a commercial-scale platform for these providers when they want to offer high-volume aseptic filling without relying entirely on traditional glass lines.
var ctx1 = document.getElementById(‘lineChartBfsGrowth’).getContext(‘2d’);var chart1 = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. BFS Project Growth Index’,data: [68, 74, 81, 89, 98, 109],borderColor: ‘rgb(54, 162, 235)’,backgroundColor: ‘rgba(54, 162, 235, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart above illustrates a realistic upward trend in U.S. BFS project activity. Growth is being driven by sterile capacity expansion, resilience planning after supply disruptions, and demand for automated aseptic systems.
BFS machines are not one-size-fits-all. Equipment is selected based on container volume, product viscosity, sterility class, output target, polymer type, and downstream packaging requirements. In the United States, buyers usually compare compact development systems, mid-scale production lines, and large industrial BFS platforms built for multi-shift operation.
Common machine categories include single-dose BFS lines for ampoule-style plastic containers, bottle-type BFS systems for larger liquid volumes, and specialized models for respiratory or ophthalmic packaging. Some projects require integrated leak detection, in-line weight control, vision inspection, and serialization compatibility depending on product distribution and regulatory expectations.
Machine Model TypeTypical Fill RangeCommon ProductsBest-Fit UsersUnit-dose ampoule BFS0.2 mL to 20 mLEye drops, inhalation solutionsOphthalmic and respiratory manufacturersSmall bottle BFS5 mL to 100 mLOral liquids, topical sterile solutionsMid-sized pharma plantsLarge bottle BFS100 mL to 1,000 mLInfusion and irrigation solutionsHigh-volume sterile fluid producersMulticavity high-speed BFS0.5 mL to 50 mLSingle-dose packsCMOs and mass-market producersCustomized specialty BFSApplication-specificDiagnostic reagents, niche liquidsSpecialty medical manufacturersR&D and pilot BFSLow to medium batch sizesScale-up and validation runsDevelopment labs and innovatorsThese machine categories serve diverse industries. Beyond mainstream pharmaceuticals, BFS is used in medical consumables, diagnostics, veterinary sterile liquids, and selected healthcare products. Applications can extend into contract packaging, hospital supply manufacturing, and export-focused production serving North America and Latin America.
var ctx2 = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Ophthalmic’, ‘Respiratory’, ‘Injectable Support Liquids’, ‘Oral Unit Dose’, ‘Hospital Solutions’, ‘Diagnostics’],datasets: [{label: ‘Estimated U.S. Demand Score’,data: [92, 96, 70, 78, 83, 61],backgroundColor: [‘rgb(255, 99, 132)’,’rgb(255, 159, 64)’,’rgb(255, 205, 86)’,’rgb(75, 192, 192)’,’rgb(54, 162, 235)’,’rgb(153, 102, 255)’]}]},options: {responsive: true,maintainAspectRatio: false}});The bar chart shows where demand is strongest. Respiratory and ophthalmic products continue to lead because unit-dose sterile packaging is central to those markets.
U.S. manufacturers rarely choose BFS in isolation. They compare it against vial lines, glass ampoule lines, and other aseptic filling methods. Traditional lines may still be the right choice for lyophilized products, formulations incompatible with BFS polymers, or products requiring established glass-container market acceptance. However, BFS often wins in applications where single-dose liquids, speed, and contamination reduction are the priority.
Comparison PointBFS TechnologyTraditional Vial LineTraditional Glass Ampoule LineContainer sourceFormed in-linePreformed vials supplied externallyPreformed glass ampoules supplied externallyCritical interventionsLowerHigherModerate to highBreakage riskLowModerateHighSingle-dose suitabilityExcellentGoodGoodFormat flexibilityStrong in polymer formatsStrong in vial sizesLimited relative to BFSIdeal use caseHigh-volume sterile liquidsInjectables, biologics, lyophilization workflowsLegacy or specialized liquid productsThe table clarifies that the decision should be application-based rather than trend-based. A company producing monoclonal antibody formulations in glass vials may not replace that line with BFS. But a company scaling preservative-free eye drops for nationwide distribution may find BFS far superior.
Another key difference is the facility workflow. Traditional vial lines usually require container receipt, storage, washing, depyrogenation, filling, stoppering, capping, and often more complex material movement. BFS condenses much of that chain. The simplification can reduce bottlenecks, especially in plants where space is expensive or workflow redesign is part of a broader digital transformation effort.
var ctx3 = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var chart3 = new Chart(ctx3, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Shift Toward Integrated Sterile Packaging’,data: [34, 39, 45, 52, 58, 65],fill: true,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,borderColor: ‘rgb(75, 192, 192)’,tension: 0.35}]},options: {responsive: true,maintainAspectRatio: false}});This area chart reflects the steady movement toward integrated sterile packaging platforms in the United States, especially where labor efficiency and contamination control are top priorities.
Adoption of BFS in the United States is expanding for structural reasons, not just temporary market fashion. First, pharmaceutical manufacturers want stronger contamination control strategies after years of heightened scrutiny around aseptic processing. Second, healthcare demand for unit-dose and preservative-free products continues to rise. Third, companies are trying to build domestic resilience and reduce supply dependency on fragile packaging chains.
From New Jersey and Pennsylvania to Texas and California, sterile manufacturers are reassessing asset strategies. Some are replacing aging equipment. Others are creating parallel capacity for BFS-friendly products while keeping conventional vial lines for biologics or high-value specialty injectables. Contract manufacturers are also investing in differentiated capabilities to win long-term client contracts.
Three important 2026 trends are shaping future adoption:
Ports and distribution networks also matter. Imported sterile machinery entering through Houston, Savannah, Newark, or Long Beach must be matched with realistic installation schedules, customs planning, and spare parts strategy. For U.S. buyers, strong adoption is often tied to supplier ability to execute—not only to machine specifications.
Choosing a supplier is one of the most consequential parts of a BFS investment. A low purchase price means little if the machine is difficult to validate, lacks local service, or cannot maintain fill accuracy over long production campaigns. U.S. buyers should assess not only the equipment but also the supplier’s engineering depth, manufacturing discipline, and project execution history.
A practical supplier evaluation framework includes the following criteria:
Supplier Selection CriterionWhat to VerifyWhy It MattersTypical U.S. Buyer QuestionRegulatory understandingExperience with FDA and global GMP projectsSupports smoother qualificationCan you support cGMP documentation and validation?Machine design qualityMaterials, controls, mold precision, aseptic designAffects reliability and sterility assuranceWhat is your design approach for critical zones?Manufacturing capabilityFactory scale, quality systems, testing methodsReduces build and acceptance riskCan we witness FAT at your plant?Service supportInstallation, commissioning, training, spare partsCritical after equipment arrivalHow quickly can you support a U.S. site?Customization abilityFormat flexibility and utility adaptationReal projects rarely match standard templatesCan you tailor the line to our product and layout?Project track recordInstalled lines and turnkey referencesShows execution credibilityWhat similar sterile projects have you completed?When reviewing suppliers, it is useful to look for a company that can support more than equipment delivery. For example, IVEN Pharmatech Engineering has built its reputation around pharmaceutical engineering and integrated manufacturing solutions rather than only single-machine sales. That matters in BFS projects, because line performance depends on utility design, cleanroom coordination, validation planning, and downstream logistics as much as on the forming and filling module itself.
From a technological capability perspective, buyers should value suppliers that understand sterile process integration, automation architecture, pharmaceutical water systems, and solution preparation. A vendor with competence beyond the BFS machine itself is often better positioned to solve performance issues during scale-up and site acceptance.
From a manufacturing capability perspective, it helps when the supplier operates specialized production facilities and has deep experience in pharmaceutical filling and packaging machinery. A company with broad manufacturing depth can usually manage precision fabrication, factory acceptance testing, and cross-system consistency more effectively than a trading intermediary.
From a service capability perspective, lifecycle support is crucial. U.S. projects benefit from suppliers who provide feasibility input, engineering design, installation, commissioning, validation assistance, training, documentation, and after-sales support. For plants evaluating larger sterile expansion programs, exploring turnkey pharmaceutical engineering solutions can reduce interface risk between utilities, process equipment, and packaging systems.
var ctx4 = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var chart4 = new Chart(ctx4, {type: ‘bar’,data: {labels: [‘Regulatory Support’, ‘Customization’, ‘Factory Testing’, ‘Lifecycle Service’, ‘Integrated Engineering’, ‘Cost Efficiency’],datasets: [{label: ‘Supplier Capability Comparison Score’,data: [88, 91, 86, 90, 94, 89],backgroundColor: ‘rgb(153, 102, 255)’}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart shows the capability profile U.S. buyers typically seek in a strong BFS partner. Integrated engineering and customization usually rank especially high because project success depends on alignment with the actual plant, product, and compliance strategy.
BFS projects require careful budgeting. The headline machine price is only one part of the investment. U.S. companies should budget for molds, utilities, HVAC interfaces, cleanroom modifications, installation, shipping, tariffs or import charges where applicable, validation, training, spare parts, and possible downstream packaging upgrades.
Costs vary widely depending on fill range, output speed, sterility level, automation scope, and whether the purchase is a standalone machine or part of a complete sterile line. A pilot or lower-speed BFS line may fit smaller market-entry strategies, while a high-capacity commercial platform demands a much larger capital commitment. Still, the ROI can be attractive when product volumes are high and manual interventions are expensive.
Budget ItemLow Complexity ProjectMid-Range ProjectHigh-Capacity ProjectCore BFS machine$1.5M-$3M$3M-$6M$6M-$12M+Molds and format parts$100K-$250K$250K-$500K$500K-$1MUtilities and installation$300K-$700K$700K-$1.5M$1.5M-$3MValidation and documentation$150K-$350K$350K-$800K$800K-$1.5MTraining and startup support$50K-$150K$150K-$300K$300K-$600KInitial spare parts package$50K-$120K$120K-$250K$250K-$500KThe ranges above are planning estimates, not quotations, but they help frame realistic capital discussions. U.S. companies in major biotech and pharmaceutical clusters often underestimate qualification cost and project management overhead. Those hidden costs can materially affect payback calculations.
A basic ROI model should examine:
In many cases, ROI becomes strongest when the line runs a stable, high-volume product family. If the product mix is too fragmented, changeover complexity can weaken the financial case. For this reason, many U.S. plants assign BFS to selected product platforms rather than using it as a universal sterile filling solution.
Companies comparing suppliers can review integrated system options through the supplier’s equipment portfolio to understand whether the BFS investment fits within a broader facility strategy that includes water systems, solution preparation, and automated packaging support.
Despite its advantages, BFS is not risk-free. The technology must match the product, the regulatory strategy, and the operational reality of the plant. One common mistake is assuming BFS automatically solves all contamination concerns. In fact, poor mold maintenance, weak resin control, inadequate media fills, or poor intervention procedures can still create serious compliance risk.
Another issue is product compatibility. Not every formulation works well in polymer containers. Oxygen sensitivity, sorption behavior, extractables and leachables, container-closure integrity expectations, and market acceptance all need careful review. U.S. buyers must also assess whether physicians, hospitals, pharmacies, or patients expect the product in a glass or polymer format.
Key risk areas include:
Risk mitigation starts early. Conduct thorough URS development, FAT and SAT planning, media fill strategy alignment, and extractables/leachables assessment. Build the project around cross-functional ownership: engineering, QA, QC, validation, procurement, regulatory affairs, and operations.
For U.S. sites that want to reduce execution risk, it is often wise to choose a supplier able to support layout optimization, documentation, qualification, and operator training. If your team is beginning a sourcing process, use the supplier’s contact channel to discuss the product profile, target output, and facility conditions before asking for a final proposal. Early technical alignment usually saves months later.
Is blow fill seal technology accepted in the United States?Yes. BFS is well established in the United States for suitable sterile and non-sterile liquid applications. Acceptance depends on proper validation, cGMP compliance, product suitability, and robust contamination control.
What products are best suited for BFS?Common products include unit-dose eye drops, inhalation solutions, saline, certain oral liquids, and selected sterile liquids where polymer packaging is appropriate and high throughput is needed.
Is BFS better than vial filling?Not universally. BFS is often better for high-volume sterile liquids and unit-dose packaging, while vial filling may remain preferable for biologics, lyophilized products, or formulations that require glass compatibility.
How long does a BFS project take in the United States?A full project can take roughly 12 to 24 months depending on machine complexity, import logistics, facility readiness, validation scope, and staffing availability. Greenfield projects can take longer.
What should U.S. buyers ask suppliers first?Ask about regulatory experience, installed references, FAT scope, automation standards, validation documentation, spare parts, lead time, and local or remote service support.
Can BFS support sustainability goals?Yes, in many cases. BFS can reduce container transport complexity and may improve process efficiency, though the sustainability outcome depends on resin choice, energy use, packaging design, and recycling pathways.
What makes a supplier more reliable for BFS projects?A reliable supplier combines strong aseptic technology, robust manufacturing quality, and full lifecycle service. This includes design support, custom engineering, commissioning, validation assistance, training, and long-term parts support.
Why do some U.S. companies choose integrated engineering partners?Because BFS performance is closely linked to utilities, water systems, layout, cleanroom coordination, and downstream packaging. An integrated engineering partner can reduce interface issues and shorten ramp-up time.
For many U.S. pharmaceutical and medical manufacturers, blow fill seal technology is no longer just an alternative packaging format. It is a strategic investment in sterile assurance, operational efficiency, and future-ready production. The best results come from matching the right product family with the right machine platform and the right engineering partner.
-
Vial Filling Machines in the United States Guide
For pharmaceutical manufacturers in the United States, a vial filling machine is a core production asset used to dose sterile liquid or powder products into glass or polymer vials with high precision, repeatability, and regulatory control. It is commonly evaluated when companies expand aseptic manufacturing, replace aging lines, launch injectable products, or upgrade plants to meet current FDA cGMP expectations. In practical terms, the right system helps improve filling accuracy, reduce contamination risk, support validation, and scale production for clinical, commercial, or contract manufacturing operations.
In the U.S. market, demand is especially strong in injectable drugs, biologics, vaccines, lyophilized products, diagnostic reagents, and specialty therapies. Buyers in Boston, San Diego, Raleigh-Durham, New Jersey, Houston, and Chicago often compare equipment not only on throughput, but also on cleanroom integration, container closure integrity, isolator or RABS compatibility, data integrity, spare parts support, and long-term total cost of ownership. This guide explains how vial filling equipment works, where it fits in modern pharmaceutical production, what technical configurations matter most, and how to choose a reliable partner for a compliant investment.
A vial filling machine matters because sterile injectable manufacturing is one of the most tightly controlled areas in pharmaceutical production. In the United States, companies expanding capacity in biologics, generic injectables, oncology drugs, emergency medicines, and hospital products must satisfy demanding standards for aseptic processing, environmental control, batch traceability, and process validation. A modern vial filler supports these goals by combining accurate filling, stopper placement, capping integration, clean transfer, and recipe-driven automation in a single production flow.
For large pharmaceutical companies and CDMOs, the equipment is often part of a larger strategic decision. A new line may be linked to facility expansion near major life science clusters such as Philadelphia, Indianapolis, or the San Francisco Bay Area, or near logistics corridors such as the Port of New York and New Jersey, the Port of Los Angeles, or Memphis air cargo routes. Faster product release, flexible batch sizes, and reduced operator intervention can directly affect plant economics and supply reliability. That is why vial filling systems are not simply packaging machines; they are critical process assets tied to compliance, quality assurance, and commercial readiness.
Business GoalWhy It Drives InvestmentTypical U.S. Buyer FocusOperational ImpactCapacity expansionMeet rising injectable demandHigher throughput with validated controlMore batches per yearRegulatory modernizationAlign with FDA cGMP expectationsAudit trails, alarms, and documentationLower compliance riskProduct diversificationSupport biologics, small molecules, and diagnosticsMulti-format flexibilityFaster product launchesContamination controlReduce human interventionIsolator or RABS integrationImproved sterility assuranceLabor efficiencyAddress skilled workforce constraintsAutomation and easier changeoverLower operating costLifecycle valueProtect long-term capital investmentService support and spare parts availabilityLonger usable asset lifeThe table above shows that buyers in the United States rarely evaluate a vial filling machine on speed alone. They balance regulatory, technical, labor, and financial factors to ensure the line remains useful across multiple product cycles.
A vial filling machine is specialized equipment designed to fill sterile or non-sterile product into vials in controlled volumes, usually followed by stoppering and sealing. In pharmaceutical settings, it is most often used for injectable liquids, suspension products, diagnostic preparations, biotech formulations, and powder filling applications. Depending on the process design, the system may be installed as a stand-alone machine or as part of a complete line including vial washing, depyrogenation, filling, stoppering, capping, inspection, labeling, and secondary packaging.
The machine typically includes a vial infeed, transport system, filling station, stopper feeder, stoppering station, and discharge. In aseptic lines, the system is frequently paired with laminar airflow, restricted access barrier systems, or isolators. Filling can be performed with peristaltic pumps, piston pumps, time-pressure systems, or net-weight technology depending on the viscosity, foaming behavior, dose range, and product sensitivity. Additional features may include nitrogen purging, vacuum stoppering, no-vial-no-fill logic, reject systems, and integrated SCADA or MES connectivity.
In U.S. pharmaceutical production, vial fillers are widely used in several scenarios:
Companies comparing integrated engineering partners may also look beyond the machine itself. For example, firms reviewing turnkey pharmaceutical project capabilities often prefer suppliers that understand how filling lines connect to utilities, cleanrooms, water systems, validation, and production logistics rather than treating the machine as an isolated purchase.
The main application of vial filling equipment is the safe and accurate transfer of product into sterile containers. Yet its value is broader than dosing. In modern pharmaceutical manufacturing, the machine directly influences yield, line clearance efficiency, environmental exposure, and lot consistency. This makes it essential in both high-volume generic operations and lower-volume specialty pharma settings.
One major benefit is filling precision. Injectable products often carry strict dose tolerances, especially for high-potency or expensive biologic formulations. Accurate pumps and servo controls reduce giveaway and batch deviation. Another major benefit is contamination control. Automated feeding and stoppering reduce manual intervention within critical zones, which supports aseptic assurance. A third benefit is scalability. Manufacturers can choose compact systems for development batches or high-speed rotary platforms for commercial volume.
Across the United States, application demand tends to vary by region. New Jersey and Pennsylvania have strong ties to established pharmaceutical manufacturing. Massachusetts and California generate strong demand from biotech and advanced therapy developers. North Carolina and Indiana remain important for large-scale sterile and injectable production. Texas and Florida increasingly attract healthcare and life science investment due to logistics access and population growth.
Application AreaTypical ProductKey Machine RequirementMain BenefitSterile injectablesAntibiotics, analgesics, hospital drugsHigh aseptic controlReliable commercial outputBiologicsMonoclonal antibodies, peptidesGentle filling and low product lossBetter yield protectionVaccinesSingle-dose or multi-dose fillsAccurate dosing and traceabilityConsistent batch releaseLyophilized drugsFreeze-dried injectablesPartial stoppering compatibilitySmooth integration with lyophilizersDiagnosticsReagents and test kitsSmall-volume precisionStable product presentationClinical productionPilot and trial lotsFast changeover and flexibilitySupports development timelinesThe chart below illustrates a realistic view of U.S. market growth interest for vial filling machinery, reflecting how injectable expansion has accelerated as supply resilience and domestic manufacturing have become stronger priorities.
var ctxLine = document.getElementById(‘lineChartMarket’).getContext(‘2d’);var lineChartMarket = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Market Demand Index’, data: [72, 78, 86, 95, 106, 118], borderColor: ‘rgb(54, 162, 235)’, backgroundColor: ‘rgba(54, 162, 235, 0.15)’, fill: false, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});From an engineering perspective, benefits increase when the filler is part of a well-planned line. The strongest results usually come from aligning the machine with vial format, formulation behavior, sterilization strategy, HVAC classification, and future capacity plans instead of buying strictly on initial price.
There is no single best vial filling machine for every U.S. facility. Selection depends on container size, target speed, sterility level, batch frequency, and product characteristics. Broadly, buyers evaluate linear and rotary systems, liquid and powder fillers, manual to fully automatic models, and cleanroom-open versus barrier-protected designs.
Linear machines are often preferred for flexibility, moderate output, and easier access during changeover. Rotary machines are better suited to high-volume, repeatable production with compact footprint efficiency. Peristaltic pump systems are valued for gentle handling and sterile fluid path replacement, especially in biotech applications. Piston pumps can deliver strong repeatability for certain liquid products, while auger or vacuum-based systems may be selected for powder filling. If lyophilization is involved, the machine must allow consistent partial stoppering and transfer to freeze dryers.
Machine TypeBest ForTypical Speed RangeAdvantagesLinear liquid fillerFlexible multi-product plants20 to 200 vials/minEasier changeover and accessRotary liquid fillerHigh-volume commercial lines150 to 600+ vials/minCompact high-speed operationPeristaltic pump systemBiologics and sensitive liquidsLow to medium speedLow shear and easy sterile tubing replacementPiston pump systemStable liquid fillsMedium to high speedStrong volumetric repeatabilityPowder vial fillerSterile powders and specialty drugsLower to medium speedSupports dry formulationsIsolator-integrated fillerHigh aseptic assurance operationsVaries by configurationReduced operator exposure and contamination riskImportant technical options to assess include:
For manufacturers seeking broader production assets, it can be useful to review an equipment portfolio rather than a single filler. A structured look at pharmaceutical equipment solutions helps buyers compare line compatibility, utility requirements, and expansion pathways across multiple dosage forms.
Vial filling is not the only container-based solution in pharmaceutical manufacturing. Some products may be better suited to ampoules, prefilled syringes, cartridges, BFS systems, or flexible IV containers. The best choice depends on dosage form, end use, shelf life, product sensitivity, administration method, and target market.
Vials remain highly versatile. They support liquid fills, powders, and lyophilized products, and they can be used for single-dose or multi-dose presentations. They are also familiar to hospitals and contract manufacturers. By contrast, prefilled syringes provide convenience and dosing accuracy for self-administration but involve more complex container systems and often higher packaging costs. Blow-fill-seal can be highly efficient for some liquids, but it is not ideal for every formulation or market segment. Ampoules offer strong hermetic sealing but are less favored when ease of opening and safety considerations dominate.
TechnologyBest Use CaseStrengthLimitationVial fillingInjectables, biologics, lyophilized productsHigh flexibilityRequires stopper and cap process controlAmpoule fillingSmall-volume sterile liquidsSealed glass presentationLess user-friendly openingPrefilled syringe fillingReady-to-administer therapiesConvenient dosingHigher packaging complexityCartridge fillingPens and injector systemsDevice compatibilityNarrower application rangeBlow-fill-sealCertain sterile liquidsIntegrated forming and fillingNot ideal for every product formatFlexible IV bag linesLarge-volume parenteralsHigh output for infusion productsDifferent market and package profileThe comparison chart below highlights common buyer priorities when evaluating container technologies for U.S. pharmaceutical applications.
var ctxComp = document.getElementById(‘comparisonChartTech’).getContext(‘2d’);var comparisonChartTech = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Flexibility’, ‘Aseptic Suitability’, ‘Format Range’, ‘Scale Potential’, ‘Hospital Acceptance’, ‘Changeover Ease’], datasets: [{ label: ‘Vial Filling Score’, data: [94, 92, 95, 88, 96, 82], backgroundColor: ‘rgb(153, 102, 255)’ },{ label: ‘Alternative Average Score’, data: [72, 85, 68, 84, 78, 70], backgroundColor: ‘rgb(255, 159, 64)’ }] }, options: { responsive: true, maintainAspectRatio: false }});For companies unsure which platform fits their product roadmap, the answer often lies in forecasting not just the first commercial launch, but also future line utilization. If multiple injectable products with different fill volumes are planned, a vial line typically offers the broadest long-term utility.
The U.S. market for vial filling machinery remains supported by three overlapping forces: continued demand for sterile injectables, reshoring and supply security efforts, and high investment in biologics and specialty medicines. Contract development and manufacturing organizations are also increasing their purchasing activity because sponsor companies want flexible domestic capacity without building every line in-house.
Current buying patterns show interest in medium-speed, flexible aseptic lines for CDMO and biotech use, alongside high-speed systems for generic injectable and hospital supply production. Renovation projects are common in legacy pharmaceutical corridors such as New Jersey and the Midwest, while greenfield opportunities continue to emerge in Southern states with growing industrial development and favorable logistics access.
By 2026, several trends are likely to shape investment decisions:
The area chart below shows how buyer preference is shifting from basic open cleanroom filling toward higher-containment, digitally integrated solutions.
var ctxArea = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var areaChartTrend = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Advanced Aseptic and Digital Line Adoption’, data: [28, 34, 43, 53, 64, 76], fill: true, backgroundColor: ‘rgba(75, 192, 192, 0.25)’, borderColor: ‘rgb(75, 192, 192)’, tension: 0.3 }] }, options: { responsive: true, maintainAspectRatio: false }});One practical trend in the United States is that buyers increasingly expect an equipment partner to understand the full project environment. That includes HVAC coordination, purified water and WFI interfaces, documentation packages, FAT/SAT expectations, and operator training. This is why engineering-oriented suppliers can stand out in larger projects.
For example, IVEN Pharmatech Engineering has built its reputation not only around individual equipment units but around integrated pharmaceutical engineering. On the technology side, the company offers sterile filling and packaging machinery, water treatment systems, logistics integration, and specialized manufacturing equipment developed through years of industry experience and patented design work. This kind of technical breadth is relevant for U.S. buyers who want to reduce interface risk across a larger factory project rather than source disconnected systems from multiple parties.
Choosing a supplier is often more important than choosing a model. Two machines with similar speed ratings can produce very different outcomes depending on design quality, documentation, validation support, and responsiveness after installation. In the United States, buyers should screen suppliers against both compliance readiness and long-term support capacity.
Start with regulatory alignment. Ask whether the machine design, materials, software, alarms, and data handling support U.S. FDA cGMP expectations and recognized global GMP frameworks. Then review engineering depth. Can the supplier adapt the line to your vial range, product behavior, and cleanroom constraints? Next, look at manufacturing capability. Does the company have sufficient fabrication capacity, quality control discipline, and supply chain stability to deliver consistently?
Service capability is equally important. Spare parts availability, remote troubleshooting, site installation, SAT, training, and documentation can determine whether startup goes smoothly or becomes delayed. U.S. buyers should also examine whether the supplier has experience supporting projects across time zones and whether English-language manuals, protocols, and qualification packages are professionally prepared.
Selection CriterionWhat to AskWhy It MattersWarning SignCompliance fitIs the system designed for FDA cGMP operations?Supports audit readinessVague documentation claimsEngineering abilityCan the supplier customize for product and facility needs?Reduces integration problemsOne-size-fits-all proposalManufacturing strengthHow are fabrication and QC managed?Improves consistency and durabilityNo evidence of production controlsValidation supportAre IQ/OQ/PQ documents and FAT/SAT support included?Speeds qualificationDocumentation sold as an afterthoughtAfter-sales serviceWhat are spare parts and response times?Protects uptimeUnclear support structureProject referencesHas the supplier delivered comparable lines?Shows practical capabilityNo relevant case historyOn manufacturing capability, IVEN is relevant to buyers seeking scale and specialization. The company operates multiple specialized manufacturing plants focused on areas such as filling and packaging equipment, pharmaceutical water treatment, intelligent conveying, and blood collection tube systems. For U.S. project teams, this matters because specialized production structures often support better process control, broader equipment compatibility, and more stable delivery performance.
On service capability, IVEN positions itself as a lifecycle partner rather than only an exporter of machinery. Its services span feasibility review, engineering design, equipment customization, installation, commissioning, validation support, documentation, staff training, and optimization. For U.S. firms planning large sterile projects, this fuller support model can reduce the coordination burden on internal engineering teams. Buyers wanting to review the company background can visit the company overview page to assess fit before moving to technical discussions.
Capital cost can vary widely depending on speed, sterility strategy, filling range, automation level, and line scope. A compact semi-automatic or lower-speed automatic system may suit clinical or specialty applications, while a fully integrated aseptic line with washing, depyrogenation tunnel, filler, capping, isolator, and inspection can represent a major capital program. In U.S. budgeting, it is critical to separate machine price from project cost.
Project cost usually includes the equipment itself, format parts, FAT, shipping, import and logistics, utility connections, installation, cleanroom adaptation, qualification, training, spare parts, and sometimes local contractor support. Depending on the project, civil or MEP changes may cost nearly as much as the filling line if the facility must be upgraded substantially.
Cost ElementLow Complexity ProjectHigher Complexity ProjectNotesBase filling machineModerateHighDepends on speed and automationBarrier technologyLow or noneHighIsolators increase sterility assurance and costUpstream/downstream integrationLimitedExtensiveWashers, tunnels, cappers, inspection unitsValidation packageBasicComprehensiveCritical for regulated startupFacility modificationsMinimalSubstantialHVAC and room layout drive major changesTraining and supportStandardAdvancedImportant for efficient ramp-upROI should be assessed on a multi-year basis. U.S. manufacturers often justify investment through increased capacity, reduced product giveaway, lower labor dependency, fewer deviations, less downtime, and access to new contract or commercial business. For CDMOs, line flexibility can create additional revenue by enabling more client programs. For brand owners, domestic filling capacity can lower supply chain risk and shorten response time to hospital or government demand.
The bar chart below shows a realistic ranking of demand by customer segment in the U.S. market, which often influences purchasing economics.
var ctxBar = document.getElementById(‘barChartDemand’).getContext(‘2d’);var barChartDemand = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Big Pharma’, ‘Biotech’, ‘CDMOs’, ‘Generic Injectables’, ‘Diagnostics’, ‘Hospital Supply’], datasets: [{ label: ‘Estimated 2025 Equipment Demand Index’, data: [88, 84, 96, 79, 67, 73], backgroundColor: ‘rgb(255, 99, 132)’ }] }, options: { responsive: true, maintainAspectRatio: false }});A disciplined ROI model should include the following variables:
If your team is beginning cost planning or supplier conversations, a direct discussion through the contact channel can help clarify machine scope, line configuration, and total project assumptions before budget approval.
The biggest investment mistake is underestimating the system context. A vial filling machine cannot perform well if the surrounding process, utilities, environmental control, and qualification strategy are poorly designed. Many disappointing projects do not fail because the machine concept was wrong, but because layout planning, user requirement specification quality, and cross-functional coordination were weak.
One major risk is mismatch between product and filling technology. Highly foaming, viscous, shear-sensitive, or high-value products may require different pump choices, nozzle designs, and line speeds. Another risk is overbuying speed without securing enough downstream capacity or demand. A third is inadequate documentation; without proper drawings, manuals, software records, and qualification protocols, startup in the U.S. can slow dramatically.
Supply support is another issue. A low-price machine may become expensive if spare parts are difficult to obtain or if remote troubleshooting is slow. Cybersecurity and data integrity also deserve attention where digital systems connect with plant networks. Finally, sustainability should not be ignored. Utility consumption, compressed air demand, and waste reduction increasingly influence long-term operating cost and ESG reporting.
Risk AreaCommon ProblemPotential ConsequenceMitigationProcess fitWrong pump or nozzle choicePoor accuracy or product lossRun product trials and technical reviewFacility integrationLayout conflicts with HVAC or material flowDelays and redesign costPerform early engineering coordinationCompliance packageIncomplete documentationQualification delaysDefine deliverables in contractSupplier serviceWeak spare parts supportLong downtimeCheck support model and inventory planningChangeover complexityToo many manual adjustmentsLost production timeRequest ergonomic and tool-less optionsFuture capacityEquipment cannot scale with demandPremature reinvestmentModel 3 to 5 year demand scenariosCase experience in the market shows that the best outcomes often come from suppliers who can bridge equipment and project execution. That is where engineering-led providers can add value. IVEN, for instance, has experience with integrated pharmaceutical projects and compliance-oriented system design, which can be helpful when a U.S. buyer needs coordination across machinery, utilities, validation, and plant workflow rather than a stand-alone transaction.
What production speeds are typical for a vial filling machine?Typical speeds range from about 20 vials per minute for compact or highly specialized applications up to several hundred vials per minute for commercial rotary systems. Actual speed depends on fill volume, product behavior, stoppering style, and sterility configuration.
Can one vial filling machine handle multiple vial sizes?Yes, many systems are designed for multiple vial formats. However, change parts, recipe management, and line clearance procedures should be reviewed carefully. The broader the format range, the more important ergonomic design becomes.
Is an isolator always necessary in the United States?Not always, but it is increasingly favored for high-value aseptic operations because it reduces operator intervention and can strengthen contamination control. The best choice depends on product risk, facility strategy, and budget.
What documentation should U.S. buyers request?At minimum, buyers should request material certificates, as-built drawings, electrical and software documentation, FAT protocols, calibration records, manuals, spare parts lists, and qualification support documents such as IQ/OQ templates where applicable.
How long does installation and validation usually take?This varies by scope. A stand-alone machine may move faster, while a full aseptic line with room modifications, utilities, and qualification can take many months. Early planning is essential to avoid delays.
Can a vial filling machine be integrated into a turnkey plant project?Yes. In fact, many larger U.S. investments benefit from integrated design. Buyers evaluating full-factory coordination can explore turnkey pharmaceutical engineering solutions when the filling line is only one part of a broader sterile manufacturing program.
How do I compare suppliers from a risk perspective?Look at technical fit, compliance understanding, manufacturing depth, installed base, qualification support, responsiveness, and the ability to provide lifecycle service. The lowest quote is not always the lowest total cost.
What makes IVEN relevant for the U.S. market?IVEN combines equipment manufacturing with pharmaceutical engineering capability, offering support across system design, customization, installation, validation, and training. For U.S. buyers seeking a partner that understands compliant production environments and integrated project delivery, this broader capability can reduce execution risk.
Should I buy only for current demand or future expansion?Usually both. The best practice is to size for realistic current demand while ensuring the line can support future products, higher utilization, or modular upgrades. Overly narrow specifications can limit long-term ROI.
In summary, a vial filling machine is one of the most consequential investments in modern injectable production. For manufacturers in the United States, the right decision balances compliance, flexibility, process accuracy, service support, and future readiness. Whether the need is a compact line for clinical batches, a robust commercial aseptic platform, or an integrated sterile plant expansion, careful supplier evaluation and project planning will shape the ultimate return on investment.
-
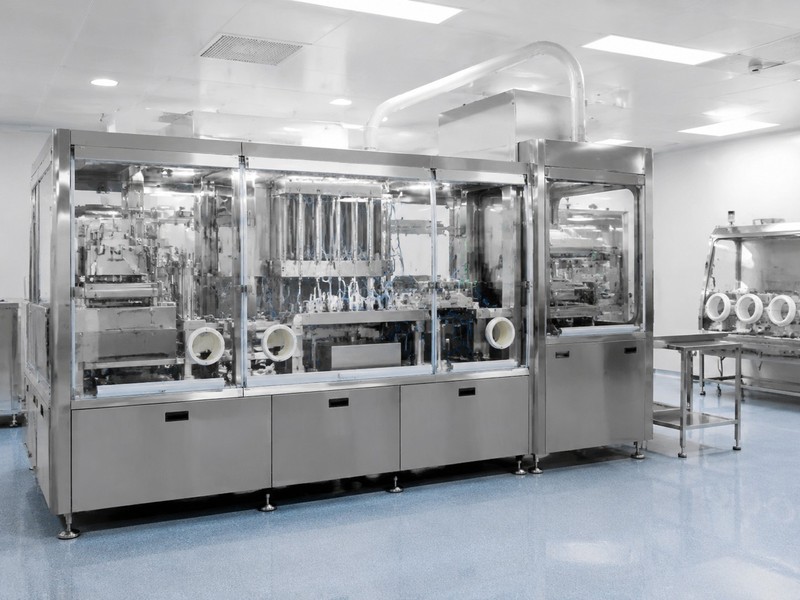
BFS Machines for Sterile Pharma in the United States
Blow-Fill-Seal equipment is preferred by many sterile product manufacturers because it forms the container, fills the product, and seals the package in one continuous aseptic cycle. For pharmaceutical plants in the United States, this integrated process can lower operator intervention, reduce contamination risk, improve line efficiency, and support compliance goals for high-value sterile liquids.
As sterile manufacturing standards continue to tighten across major U.S. hubs such as New Jersey, Boston, Philadelphia, Raleigh-Durham, Houston, and Southern California, interest in BFS machine systems has grown beyond traditional respiratory and ophthalmic products. Today, U.S. buyers are evaluating BFS platforms for preservative-free unit doses, biologics support liquids, diagnostic reagents, inhalation therapies, and contract manufacturing expansion projects. For companies planning capacity upgrades near ports such as Los Angeles, Houston, Savannah, or New York/New Jersey, BFS also offers packaging efficiency advantages that may simplify logistics, warehousing, and line integration.
For organizations comparing equipment partners, IVEN Pharmatech Engineering is known internationally for pharmaceutical engineering, filling and packaging systems, water treatment units, and integrated project execution. Its experience in regulated pharmaceutical environments, including projects aligned with U.S. FDA cGMP expectations, makes it relevant to buyers seeking both machinery and broader plant support.
A BFS machine is often chosen because it minimizes human intervention at the most contamination-sensitive stages of sterile packaging. Instead of separately sourcing containers, washing them, depyrogenating them, moving them into a filling zone, and then sealing them, the BFS process creates the plastic container from resin, immediately fills it with sterile product, and seals it in the same enclosed machine cycle. That single-flow design can reduce open exposure time, decrease transfer points, and streamline aseptic control.
In the United States market, the preference for BFS machines is especially strong among companies producing unit-dose pharmaceuticals, inhalation products, eye drops, irrigation solutions, and certain specialty liquids. The technology supports high output, repeatable quality, flexible container formats, and strong economics at medium to large production volumes. It is also attractive for plants that want to lower cleanroom labor dependency or expand sterile manufacturing without duplicating traditional vial infrastructure.
Decision FactorWhy It MattersBFS AdvantageTypical U.S. Buyer ConcernOperational ImpactCommentsContamination controlCritical for sterile productsClosed, integrated processFDA inspection readinessLower exposure riskMajor reason buyers switchLabor efficiencyRising labor costsLess manual handlingSkilled operator availabilityLower staffing pressureUseful in high-cost regionsOutput speedSupports scaleContinuous operationDemand surgesHigher throughputStrong for contract manufacturersPackaging integrationReduces process stepsForm, fill, seal togetherLine simplificationShorter process pathLess transfer complexityContainer flexibilityDifferent dose formatsCustom molds possibleProduct differentiationBroader portfolio optionsImportant in OTC and Rx segmentsCost per unitAffects profitabilityCompetitive at scaleROI justificationBetter long-run economicsDepends on utilization rateThe table above shows why BFS is often evaluated not only as a machine purchase, but as a contamination control and operating model decision. For many U.S. sterile drug makers, the biggest value is not the machine alone; it is the reduction in process complexity across the entire filling workflow.
BFS stands for Blow-Fill-Seal. In a typical BFS cycle, polymer resin is extruded into a hollow parison, the mold closes around it, sterile air blows the parison into a container shape, the product is filled through sterile nozzles, and the container is hermetically sealed before leaving the machine. The process occurs within a controlled environment designed to maintain aseptic conditions.
Most pharmaceutical BFS systems use polyethylene or polypropylene resins depending on the product, compatibility requirements, barrier expectations, and terminal sterilization strategy. Container sizes can range from very small unit-dose ampoules to larger bottles used for oral liquids or irrigation applications. Machine design varies by output target, mold configuration, automation level, and the required degree of integration with downstream leak testing, visual inspection, labeling, cartoning, and serialization.
Technologically, buyers in the United States often look for systems with validated clean-in-place or sterilize-in-place support where applicable, recipe management, electronic batch records, 21 CFR Part 11-friendly data management, alarm history, trend monitoring, and remote diagnostics. These features are increasingly important for multi-site operations and CDMOs managing diverse client audits.
Process StepWhat HappensMain Equipment AreaQuality FocusCommon RiskControl MethodResin feedingPolymer enters extruderFeeding and drying unitMaterial consistencyResin contaminationSupplier qualification and handling SOPsExtrusionParison is formedExtruder headWall thickness stabilityShape variationTemperature and pressure controlMoldingContainer shape is blownMold stationDimensional accuracyDefect formationMold design and maintenanceFillingSterile product dosed insideFilling stationVolume accuracy and sterilityUnderfill or contaminationCalibrated pumps and aseptic controlsSealingContainer closedSealing zoneClosure integrityLeakageSeal parameter validationDischarge and inspectionFinished units leave machineOutfeed and QA systemsAppearance and integrityHidden defectsLeak testing and vision inspectionThe process table helps explain why BFS is highly valued in sterile production. Every step can be engineered to reduce open handling, which is one of the main contamination pathways in traditional fill-finish operations.
var ctx1 = document.getElementById(‘lineChartBfsGrowth’).getContext(‘2d’);var chart1 = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Estimated U.S. BFS Market Growth Index’,data: [68, 74, 82, 91, 103, 118],borderColor: ‘rgb(54, 162, 235)’,backgroundColor: ‘rgba(54, 162, 235, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart reflects a realistic growth pattern driven by sterile capacity investment, domestic supply resilience, respiratory product demand, and modernization of aging fill-finish assets across the U.S. market.
Sterile drug manufacturers choose BFS technology for both technical and commercial reasons. On the technical side, BFS supports contamination control, dosage repeatability, and efficient high-volume output. On the commercial side, it can reduce dependence on preformed container supply chains, lower handling steps, and create strong economics for unit-dose packaging.
In the United States, regulatory pressure has pushed manufacturers to design processes that are easier to validate and monitor. BFS aligns well with quality-by-design thinking because the process is integrated and repeatable. Manufacturers can also use customized container shapes to improve dosing convenience, product differentiation, and patient adherence.
BFS is especially attractive for:
From a technological capability perspective, IVEN Pharmatech Engineering is relevant for companies seeking more than a standalone machine. Its strengths include pharmaceutical filling and packaging engineering, water treatment systems such as purified water and WFI support infrastructure, logistics integration, and full-factory solution planning. For U.S. manufacturers, that matters because BFS performance often depends on the quality of utilities, cleanroom layout, material flow, and downstream packaging design just as much as on the forming and filling machine itself.
BFS machines are not one-size-fits-all. Selection depends on product viscosity, output volume, container shape, regulatory strategy, and downstream packaging goals. Some machines are optimized for small-volume unit-dose containers, while others are designed for larger bottles used in oral liquids or irrigation products. Multi-cavity molds, single-row or multi-row systems, intermittent versus continuous motion configurations, and specialized dosing technologies all affect suitability.
BFS Model TypeTypical Fill RangeMain ApplicationCommon Container MaterialSuitable U.S. SegmentKey BenefitUnit-dose BFS0.2 mL to 10 mLEye drops, inhalationLDPERespiratory and ophthalmicHigh-speed small-dose outputMid-volume BFS10 mL to 100 mLTopical and specialty liquidsLDPE or PPRx and OTCFlexible product rangeLarge-volume BFS100 mL to 1000 mLIrrigation and solutionsPPHospital supplyIntegrated sterile packagingTwin-chamber BFSCustomCombination or activation productsSpecial polymersAdvanced therapy supportProduct separation until useStrip-pack BFS0.5 mL to 20 mLUnit-dose stripsLDPEConsumer-friendly formatsConvenient secondary packagingCustom molded BFSProject-specificDiagnostics and specialty useCustom resin selectionNiche manufacturersBrand and functional differentiationThis table shows that product fit is central to machine choice. A buyer producing 3 mL preservative-free eye drops in New Jersey has very different needs from a hospital-supply manufacturer in Texas packaging 500 mL sterile solutions.
Application areas in the United States are expanding into contract development and manufacturing organizations, hospital product suppliers, consumer health brands, veterinary pharma, and medical consumables. Locations with strong life sciences ecosystems, such as Massachusetts, North Carolina, and California, are also showing greater interest in flexible sterile packaging platforms that can support both legacy and newer products.
Traditional vial and ampoule lines remain important in sterile manufacturing, especially for injectable biologics, lyophilized products, and glass-dependent formulations. However, for the right liquid products, BFS can outperform conventional lines in simplicity and contamination control. Traditional systems require multiple upstream and downstream steps: container procurement, washing, depyrogenation or sterilization, transfer, filling, stoppering or sealing, and often more operator interventions.
BFS replaces many of those steps with one integrated cycle. That does not mean BFS is universally better; it means the best choice depends on the formulation, packaging material requirements, market channel, and production economics.
Comparison PointBFS MachineVial LineAmpoule LineBest Use CaseBuyer TakeawayContainer sourceFormed on machinePreformed glass or plasticPreformed glassBFS for integrated packagingLess supply chain dependencyOperator interventionLowModerateModerateBFS for aseptic simplificationLower handling riskMaterial typeMainly plasticGlass or plasticGlassVials for glass-required drugsCheck formulation compatibilityFormat flexibilityStrong for molded designsStrong across closuresMore limitedDepends on product strategyCustom design is a BFS strengthThroughput potentialHighHigh but multi-stepModerate to highBFS for unit-dose scaleGood for large volume demandTypical applicationsRespiratory, eye care, solutionsInjectables, biologicsLegacy sterile liquidsProduct-driven choiceNo universal winnerThe comparison table clarifies the buying decision: BFS is usually strongest where plastic containers are acceptable and where unit-dose or high-volume sterile liquids dominate the product mix. Traditional vial lines remain essential where glass, stoppers, or specialized injectable presentations are required.
var ctx2 = document.getElementById(‘barChartIndustryDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Respiratory’, ‘Ophthalmic’, ‘Hospital Solutions’, ‘OTC Sterile Liquids’, ‘Diagnostics’, ‘Veterinary’],datasets: [{label: ‘Estimated U.S. BFS Demand by Segment’,data: [92, 84, 71, 63, 49, 38],backgroundColor: [‘rgba(255, 99, 132, 0.7)’,’rgba(54, 162, 235, 0.7)’,’rgba(255, 206, 86, 0.7)’,’rgba(75, 192, 192, 0.7)’,’rgba(153, 102, 255, 0.7)’,’rgba(255, 159, 64, 0.7)’]}]},options: {responsive: true,maintainAspectRatio: false}});This bar chart highlights where BFS demand is strongest in the U.S. market. Respiratory and ophthalmic remain leading segments, but hospital solutions and sterile OTC categories continue to grow.
Adoption of BFS technology has accelerated as U.S. manufacturers rethink supply chain resilience, domestic production capacity, and contamination prevention. After years of depending on more fragmented sterile packaging flows, many companies are now prioritizing integrated production architectures that support faster scale-up and cleaner process design.
CDMOs are among the most active adopters because they need flexible platforms to attract multiple clients. Hospital product manufacturers also see BFS as a way to supply routine sterile liquids more efficiently. At the same time, brands in consumer health are using BFS to create preservative-free single-use products with convenient patient handling.
2026 trends are likely to push adoption further. These include expanded automation, AI-assisted process monitoring, stronger environmental reporting, and greater focus on domestic manufacturing security. Sustainability is also shaping procurement discussions. Although BFS uses plastic, it can reduce packaging complexity and waste in certain formats when compared with multi-component container systems. Buyers increasingly ask about resin efficiency, energy consumption, scrap reduction, and recyclable secondary packaging.
var ctx3 = document.getElementById(‘areaChartTrendShift’).getContext(‘2d’);var chart3 = new Chart(ctx3, {type: ‘line’,data: {labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’],datasets: [{label: ‘Shift Toward Integrated Sterile Packaging’,data: [22, 28, 36, 47, 59, 72],fill: true,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,borderColor: ‘rgb(75, 192, 192)’,tension: 0.35}]},options: {responsive: true,maintainAspectRatio: false}});The area chart illustrates the broader shift toward integrated sterile production systems. BFS benefits from this trend because it fits the demand for fewer interventions, stronger process control, and greater manufacturing resilience.
Selecting a BFS supplier in the United States market should go beyond price comparison. Buyers should assess regulatory understanding, equipment durability, mold design expertise, automation architecture, after-sales responsiveness, spare parts planning, FAT and SAT discipline, and experience with validation support.
When evaluating suppliers, U.S. pharmaceutical companies often compare domestic integrators, European equipment makers, and qualified Asian engineering firms. The right partner is usually the one that can combine technical know-how with practical project execution, not simply the one with the lowest quote.
Supplier Evaluation FactorWhat to VerifyWhy It MattersRed FlagGood SignBuyer ActionRegulatory familiarityFDA cGMP project referencesSupports complianceGeneric answersStructured URS responseAsk for U.S.-oriented case detailsEngineering depthUtility and layout integrationMachine must fit the plantMachine-only mindsetProcess-based planningRequest layout reviewManufacturing qualityFabrication standards and materialsLong equipment lifePoor documentationTraceable production recordsAudit the factory if possibleValidation supportIQ/OQ/PQ documentation scopeSpeeds start-upMinimal support packageComprehensive protocolsInclude in contractSpare parts serviceLead times and stockingReduces downtimeNo plan for critical partsRecommended spare kitNegotiate lifecycle packageTraining capabilityOperator and maintenance trainingImproves ramp-upOne-time handover onlyStructured training matrixRequire on-site and remote supportManufacturing capability matters as much as sales messaging. IVEN Pharmatech Engineering, for example, has multiple specialized manufacturing plants in Shanghai focused on pharmaceutical filling and packaging systems, water treatment systems, intelligent logistics, and blood collection tube equipment. For U.S. buyers, this breadth can be useful when a BFS project is part of a wider sterile facility investment rather than a stand-alone purchase. You can explore broader integrated project capabilities through its turnkey pharmaceutical engineering solutions and review available equipment categories in the product portfolio.
BFS machine investment in the United States can vary widely depending on capacity, mold complexity, automation, utility scope, cleanroom integration, validation package depth, and downstream packaging needs. A basic project budget should include the main machine, molds, utilities, installation, commissioning, validation, training, spare parts, room modifications, and ongoing consumables.
Many buyers underestimate indirect costs. For example, upstream formulation transfer, HVAC balancing, water system readiness, compressed air quality, leak testing, vision inspection, and serialization can materially affect total project cost. At the same time, many also underestimate the long-term savings of BFS in labor reduction, fewer purchased containers, higher speed, and lower contamination event risk.
Budget ItemLow Complexity ProjectMid Complexity ProjectHigh Complexity ProjectWhy Cost ChangesPlanning NoteMain BFS machineModerateHighVery highOutput and automation levelCore capital itemMolds and change partsModerateModerate to highHighContainer designs and SKUsOften underestimatedUtilities integrationLow to moderateModerateHighExisting site readinessCheck WFI, air, HVAC, powerValidation packageModerateModerateHighDocumentation depthCritical for regulated launchDownstream packagingLowModerateHighInspection and cartoning scopeMay equal major line costTraining and serviceLowModerateModerateProject complexity and locationDo not cut this line itemROI analysis usually depends on six variables: annual output, selling price per unit, labor savings, scrap rate, uptime, and avoided quality failures. For a busy U.S. plant near Chicago or Atlanta shipping nationwide, logistics efficiency and lower packaging component sourcing complexity may also improve returns. A BFS line running consistently at high utilization can show attractive economics over time, especially in unit-dose categories.
Service capability also influences ROI. A supplier that supports feasibility analysis, engineering design, installation, commissioning, validation, documentation, training, and post-start optimization can shorten time to market. IVEN is relevant here because its lifecycle support model extends from project consulting through technical transfer and after-sales assistance. Companies considering a new sterile line can contact the engineering team to discuss project scope, capacity targets, and site constraints.
var ctx4 = document.getElementById(‘comparisonChartSupplierFactors’).getContext(‘2d’);var chart4 = new Chart(ctx4, {type: ‘bar’,data: {labels: [‘Compliance Support’, ‘Customization’, ‘Factory Integration’, ‘Lifecycle Service’, ‘Cost Efficiency’, ‘Lead Time Reliability’],datasets: [{label: ‘Supplier/Product Evaluation Score’,data: [90, 86, 88, 92, 81, 79],backgroundColor: ‘rgba(153, 102, 255, 0.75)’}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart reflects the practical factors many U.S. buyers use when scoring BFS suppliers. While initial cost matters, compliance support and lifecycle service often determine the real value of a project.
Investing in BFS technology can deliver substantial benefits, but it requires careful planning. The most common risk is assuming the machine alone guarantees sterile production success. In reality, product compatibility, resin selection, extractables and leachables assessment, validation planning, clean utility stability, mold design, and operator training all affect outcomes.
Key considerations include:
One frequent mistake is buying oversized equipment for future demand that may never materialize. Another is under-specifying automation and then discovering labor savings do not meet expectations. A third is failing to align the BFS project with the plant’s broader water, HVAC, and material flow infrastructure.
For U.S. projects, imported equipment can also raise practical questions around shipping schedules, customs clearance, site acceptance timing, and technical support coverage. Buyers should plan logistics well, especially for deliveries entering through major gateways such as Long Beach, Newark, Houston, or Savannah. A detailed project timeline with FAT, shipping, installation, SAT, and validation milestones is essential.
Risk AreaTypical ProblemImpactPrevention MethodOwnerPriorityProduct compatibilityResin not ideal for formulationStability concernsEarly compatibility studiesQA and formulation teamHighUtility readinessAir or water quality gapsDelayed start-upPre-installation auditEngineeringHighValidation scopeIncomplete protocolsRegulatory delaysDefine IQ/OQ/PQ earlyValidation teamHighCapacity planningMachine too large or too smallPoor ROIDemand-based modelingOperations and financeMediumSupply chainSpare parts delaysDowntime riskCritical spares packageMaintenanceMediumTraining gapsImproper operationYield lossStructured training planSupplier and plant managementHighThe table above shows that most BFS risks are manageable if addressed during design and procurement rather than after delivery. Strong front-end engineering usually prevents expensive downstream corrections.
A useful case pattern in the U.S. market involves sterile manufacturers expanding from one flagship product into multiple unit-dose SKUs. Companies that succeed typically standardize molds where possible, invest in robust visual inspection, and choose suppliers able to support long-term process optimization rather than only machine installation.
What products are best suited to BFS machines?BFS is especially well suited to sterile liquid products such as inhalation solutions, eye drops, saline, irrigation solutions, and other unit-dose or multi-dose plastic container formats where integrated aseptic packaging is beneficial.
Is BFS accepted in the United States pharmaceutical market?Yes. BFS is an established pharmaceutical packaging technology used in regulated markets, including the United States, when properly designed, validated, and operated under cGMP requirements.
Can BFS replace all vial filling lines?No. BFS is excellent for many sterile liquids, but it does not replace vial lines for every product. Glass-dependent drugs, certain injectables, and lyophilized formulations often still require traditional vial technology.
How long does a BFS project usually take?Project timelines vary based on customization, factory readiness, validation scope, and logistics. A full project can take many months from URS to commercial production, particularly if facility modifications are needed.
What should U.S. buyers request from suppliers?Buyers should request detailed technical proposals, FAT scope, validation documentation, spare parts recommendations, training plans, utility requirements, lead times, service response commitments, and project references relevant to sterile production.
Does BFS support sustainable manufacturing goals?It can support sustainability goals when designed properly. Buyers should assess resin utilization, energy efficiency, scrap management, container weight optimization, and secondary packaging reduction rather than assuming a simple yes or no answer.
What should be included in supplier due diligence?Factory audits, reference checks, documentation review, engineering capability assessment, service support evaluation, and confirmation of experience with regulated pharmaceutical projects should all be included.
Why consider an integrated engineering partner instead of only a machine vendor?Because sterile production performance depends on utilities, layout, validation, training, and downstream handling. An integrated partner can reduce interface risk between the BFS machine and the rest of the plant.
For United States manufacturers planning sterile capacity expansion, BFS technology remains one of the most practical options for reducing contamination risk while improving speed and packaging efficiency. The strongest business case usually appears when product fit, factory infrastructure, supplier competence, and lifecycle support are aligned from the beginning. Companies looking for a partner with engineering, manufacturing, and service capabilities across pharmaceutical equipment and turnkey delivery can review company background, explore integrated project services, browse the equipment range, or request a project discussion for a U.S.-focused BFS evaluation.