Pharmaceutical Water System Issues in the United States
Pharmaceutical water treatment problems are not minor utility issues; they are core production risks for drug manufacturers in the United States. In sterile plants producing injectables, vaccines, biologics, ophthalmics, dialysis fluids, and oral liquids, water quality directly affects product safety, batch release, equipment reliability, and FDA inspection readiness. A properly designed pharmaceutical water system makes it possible to produce Purified Water, Water for Injection, and clean steam with stable conductivity, TOC, microbial, and endotoxin performance. A poorly designed or poorly maintained system leads to biofilm growth, conductivity excursions, sanitization failures, membrane fouling, corrosion, downtime, and expensive deviations. For U.S. pharmaceutical facilities operating in Boston, New Jersey, North Carolina, Texas, California, and the Midwest, pharmaceutical water treatment is essential infrastructure because it supports pharmacopeia compliance, protects GMP operations, and improves long-term manufacturing efficiency.
In the U.S. market, where facilities often face aging utility systems, stricter data integrity expectations, rising energy costs, and pressure to localize supply chains, manufacturers increasingly evaluate whether their current water system architecture still fits modern production needs. That evaluation often includes not only technical performance but also lifecycle cost, validation burden, sustainability, supplier responsiveness, and integration with digital plant management. For companies planning a new greenfield site or upgrading an existing utility block, understanding common pharmaceutical water treatment problems is the first step toward choosing the right solution.
Quick Answer: Why Pharmaceutical Water Treatment Matters for U.S. Drug Manufacturers

The short answer is simple: pharmaceutical water treatment problems can stop production, trigger investigations, and put regulatory compliance at risk. In GMP pharmaceutical facilities, water is often the largest raw material by volume. It is used in formulation, rinsing, cleaning, sterilization support, buffer preparation, equipment feed, and utility generation. If water purity drifts outside established limits, the impact can cascade across multiple departments at once.
For U.S. manufacturers, especially those supplying hospital injectables, biosimilars, cell and gene therapy support fluids, and contract manufacturing services, the water system must consistently meet pharmacopoeial standards and internal alert/action limits. This means the system cannot be viewed as a generic industrial treatment skid. It must be designed as a validated pharmaceutical utility, with appropriate pretreatment, membrane protection, continuous circulation, sanitary materials, hot or chemical sanitization strategy, and a well-defined control philosophy.
| Problem Area | Typical Cause | Operational Effect | Quality Risk | Common U.S. Impact | Recommended Response |
|---|---|---|---|---|---|
| Microbial excursion | Dead legs, poor circulation, weak sanitization | Sampling failures | Batch hold or rejection | Deviation and FDA scrutiny | Loop redesign and sanitization review |
| High conductivity | RO failure, EDI instability, feedwater variation | Off-spec water | Utility out of release limits | Production interruption | Membrane diagnostics and feed pretreatment upgrade |
| High TOC | Organics breakthrough, resin issues, contamination | Alert or action limit event | Cleaning validation concern | Extended investigations | Source analysis and component replacement |
| Endotoxin increase | Biofilm or poor WFI storage control | Restricted WFI use | Sterile product risk | Critical QA escalation | Thermal sanitization and loop remediation |
| Low flow/pressure | Scaling, fouling, pump wear | Inadequate point-of-use supply | Cleaning effectiveness issue | Line delays | Hydraulic balancing and maintenance plan |
| Frequent downtime | Undersized system or weak automation | Utility unreliability | GMP disruption | Higher cost per batch | Capacity redesign and controls modernization |
The table above shows why pharmaceutical water treatment problems should be handled as strategic manufacturing issues rather than routine maintenance tasks. In many U.S. facilities, one excursion can affect multiple suites, especially in campuses where a centralized PW or WFI system serves several production areas.
What Is a Pharmaceutical Water Treatment System and Why Do Pharma Manufacturers Need It?

A pharmaceutical water treatment system is a validated utility system designed to convert incoming potable or pretreated municipal water into high-purity pharmaceutical-grade water suitable for GMP use. Depending on the application, the system may produce Purified Water, Water for Injection, or feed water for purified steam generation. It typically includes pretreatment, reverse osmosis, electrodeionization or distillation, storage, distribution loops, instrumentation, automation, and sanitization features.
Unlike conventional industrial water treatment, pharmaceutical design emphasizes hygienic construction and reproducibility. The system must support traceability, calibrated online monitoring, alarm management, documented maintenance, qualification protocols, and validated operating ranges. This is why U.S. life science companies in hubs such as Philadelphia, Raleigh-Durham, Indianapolis, and San Diego evaluate water systems with the same rigor used for process equipment.
Manufacturers need these systems for several reasons:
- To meet USP and internal GMP water quality requirements
- To support sterile and non-sterile product manufacturing
- To reduce contamination and deviation risk
- To improve cleaning consistency for vessels, lines, and fillers
- To maintain uninterrupted production in high-value facilities
- To pass customer, FDA, and third-party audits with confidence
When companies expand capacity, launch new injectables, or retrofit old facilities, they often discover that many recurring pharmaceutical water treatment problems come from legacy design choices. These may include oversized storage tanks with poor turnover, ambient loops vulnerable to microbial growth, or underspecified pretreatment unable to handle seasonal changes in municipal source water.
For this reason, many buyers now prefer integrated engineering partners that can link process need, utility design, qualification, and long-term support. Companies exploring that approach often review turnkey engineering capability, equipment selection, and validation support together rather than purchasing utilities as isolated skids. More detail on integrated facility solutions can be found at pharmaceutical turnkey project solutions.
Main Applications and Benefits in GMP Pharmaceutical Facilities

Pharmaceutical water systems serve far more than one process step. In a compliant facility, they influence manufacturing, cleaning, laboratory operations, and utility support. The main applications depend on dosage form, risk profile, and plant layout.
| Application | Water Grade Commonly Used | Main U.S. Industry Segment | Benefit | Risk if Water Fails | Priority Level |
|---|---|---|---|---|---|
| Injectable formulation | WFI | Sterile injectables | Patient safety and low endotoxin control | Batch rejection | Critical |
| Vial and ampoule final rinse | WFI or PW depending on stage | Parenteral filling | Container cleanliness | Particulate and microbial concern | Critical |
| CIP preparation | PW | Biologics and oral liquids | Repeatable cleaning outcomes | Cleaning validation deviation | High |
| Buffer and media support | PW or WFI | Biopharma | Stable process inputs | Process variability | High |
| Equipment rinsing | PW | Solid dosage and liquids | Reduced residue carryover | Cross-contamination concern | High |
| Purified steam feed | WFI feed quality | Sterile plants | Reliable sterilization support | SIP performance issues | Critical |
The biggest benefits include quality assurance, lower deviation rates, better cleaning reproducibility, and stronger inspection readiness. A robust system also reduces hidden costs such as emergency maintenance, overtime, repeat sanitization, excess sampling, and delayed production scheduling.
In the United States, contract development and manufacturing organizations often place special value on flexible systems because one utility block may need to support multiple client products and cleaning cycles. A system that performs consistently across varied production patterns is often worth more than a lower-cost system that only works under narrow operating assumptions.
Another major benefit is lifecycle visibility. Advanced automation can trend conductivity, TOC, flow, temperature, pressure, and sanitization data over time, allowing plants to identify early performance drift. This is especially useful in larger manufacturing corridors such as New Jersey and Massachusetts, where high-value production time makes predictive maintenance financially attractive.
Different Types: RO, EDI, Distillation, and Hybrid Systems
Different pharmaceutical facilities need different water generation architectures. The right choice depends on required water grade, plant utility philosophy, feedwater quality, sustainability targets, and capacity. Understanding each type helps buyers reduce future pharmaceutical water treatment problems.
| System Type | Best Use Case | Main Advantages | Main Limitations | Typical U.S. Buyer | Comments |
|---|---|---|---|---|---|
| RO | Pretreatment and primary purification | Good salt rejection, scalable, energy efficient | Membrane fouling risk | Solid dose, oral liquid, utility upgrade projects | Usually not used alone for high-risk GMP needs |
| RO + EDI | Purified Water generation | Continuous high purity, low chemical use | Needs stable pretreatment and feed control | Modern PW systems | Popular in U.S. GMP plants |
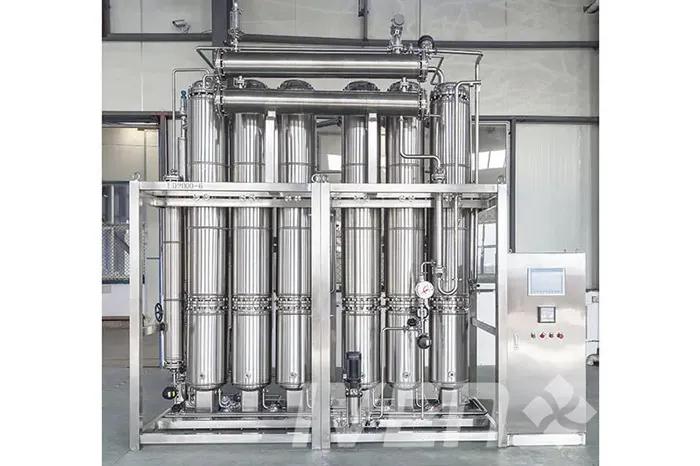
| Multi-effect distillation | WFI generation | Strong microbial and endotoxin control | Higher capital cost, steam demand | Sterile injectable plants | Well established for WFI |
| Vapor compression distillation | Medium-large WFI demand | Efficient thermal generation | Mechanical complexity | Large biotech and parenteral campuses | Useful where steam strategy supports it |
| Hybrid RO + EDI + distillation | Sites needing PW and WFI | Integrated quality control across grades | More complex validation | Greenfield multi-product plants | Common in full utility planning |
| Hybrid membrane + hot loop | High sanitation control PW systems | Reduced microbial risk in distribution | Higher operating energy than ambient loops | Risk-sensitive manufacturers | Useful in humid climates or variable usage plants |
RO systems remove dissolved salts and many contaminants efficiently, but they need proper pretreatment to manage hardness, chlorine, organics, and particulate load. EDI is often added after RO to polish water continuously without the chemical regeneration burden associated with traditional ion exchange. Distillation remains a preferred choice for WFI in many sterile facilities due to strong control over pyrogens and microorganisms.
Hybrid systems are increasingly attractive in the U.S. because they balance compliance, sustainability, and resilience. For example, a biologics site near Research Triangle Park may use double-pass RO and EDI for PW, paired with a multi-effect still and purified steam generator for aseptic operations. That configuration provides operational flexibility while separating risk by application.
For buyers seeking equipment options across water generation, distillation, and related pharmaceutical utility systems, a broader product overview is available through pharmaceutical equipment and water system solutions.
Pharmaceutical Water Treatment vs Traditional Water Treatment Methods: Which One to Choose?
Traditional industrial water treatment focuses on general usability: boiler protection, cooling tower makeup, process washing, or food-grade support. Pharmaceutical water treatment is different because it must produce water that is fit for validated GMP use. The gap between these approaches is one reason some companies underestimate pharmaceutical water treatment problems during facility planning.
Traditional systems often prioritize basic hardness removal, chlorine control, and filtration. Pharmaceutical systems add hygienic design, sanitary welding, sloped piping, dead-leg control, continuous recirculation, sanitary pumps, validated instruments, and documented alarm history. They are built for auditable control, not only for raw performance.
| Comparison Factor | Traditional Water Treatment | Pharmaceutical Water Treatment | Business Consequence | Recommended Choice | Why It Matters |
|---|---|---|---|---|---|
| Design standard | Industrial utility focus | GMP and pharmacopeia focus | Compliance gap risk | Pharma system | Supports regulated production |
| Materials of construction | Broader material range | Sanitary stainless steel and hygienic components | Contamination risk varies | Pharma system | Improves cleanability |
| Instrumentation | Basic process monitoring | Critical online quality monitoring | Poor trend visibility if absent | Pharma system | Enables data-driven control |
| Documentation | Standard O&M manuals | DQ/IQ/OQ/PQ-oriented package | Longer validation time if missing | Pharma system | Supports qualification |
| Sanitization strategy | Limited or periodic cleaning | Validated hot or chemical sanitization | Higher microbial risk otherwise | Pharma system | Protects loop integrity |
| Regulatory suitability | Low for sterile manufacturing | High when properly qualified | Inspection vulnerability | Pharma system | Required for serious GMP operations |
For non-GMP support activities, a conventional industrial system may be enough. But for product-contact or critical cleaning uses, U.S. drug manufacturers should choose a pharmaceutical-grade solution. The cost of under-specifying the system is usually far greater than the initial savings. A few avoided deviations can justify the higher capital expenditure.
This distinction is especially important when retrofitting older facilities in legacy industrial zones around Chicago, St. Louis, or parts of New Jersey, where an existing utility room may have been designed for another industry and later adapted to pharmaceutical use.
Market Overview and Future Trends in U.S. Pharmaceutical Manufacturing
The United States remains one of the world’s largest pharmaceutical manufacturing markets, with strong investment in injectables, biologics, advanced therapies, and domestic supply chain resilience. Water systems are benefiting from this trend because new capacity nearly always requires upgraded GMP utility infrastructure.
Demand is strongest in regions with dense pharmaceutical clusters, including Boston-Cambridge, New Jersey, the Philadelphia corridor, North Carolina’s Research Triangle, Indianapolis, Texas, and Southern California. Expansion in these areas is driven by sterile fill-finish capacity, CDMO growth, biosimilar production, and investment in resilient domestic manufacturing following global supply disruptions.
The line chart above illustrates a realistic growth trend for the U.S. market as more facilities modernize aging water infrastructure and build specialized sterile capacity.
The bar chart shows that injectables, biologics, and CDMO operations are expected to drive the strongest demand for pharmaceutical water systems because they rely on highly controlled, auditable water quality.
The area chart highlights the shift from basic standalone skids toward digitally monitored hybrid systems with improved energy efficiency, sanitation automation, and predictive maintenance capability.
Looking toward 2026, three trends stand out:
- More digital integration through SCADA, remote diagnostics, and data analytics for trend-based maintenance
- Greater emphasis on sustainability, including lower reject water loss, energy recovery, and optimized heat use
- Stronger regulatory focus on documented control of microbial risk, lifecycle maintenance, and data integrity
Policy pressure in the United States will continue to favor domestic manufacturing reliability, especially for essential medicines and sterile products. That means utility robustness will become a board-level concern in many projects, not only an engineering detail.
How to Choose a Reliable Manufacturer or Supplier
Choosing a supplier for a pharmaceutical water system in the United States should go beyond price comparison. A reliable supplier must understand regulations, process risk, qualification, and long-term service. Plants in Newark, Houston, Baltimore, Savannah, and Los Angeles may have different logistical considerations, but the buying criteria remain broadly similar.
Start by evaluating the supplier in three areas: technological capabilities, manufacturing capabilities, and service capabilities.
Technological capabilities: The supplier should be able to design RO, EDI, distillation, storage, distribution, and clean steam systems with strong sanitary engineering principles. It should also understand how to tailor the system for injectables, biologics, oral liquids, or medical consumables. A supplier with cross-category engineering experience can better anticipate interface problems between process equipment and utilities. IVEN Pharmatech Engineering, for example, positions itself as an engineering partner for pharmaceutical innovation and has experience with water treatment, WFI distillation, purified steam generation, filling lines, and integrated pharmaceutical projects designed around international GMP expectations.
Manufacturing capabilities: Buyers should confirm whether the supplier has dedicated production resources, quality control, and enough capacity to fabricate systems consistently. A supplier with specialized manufacturing plants and experience delivering complete utility packages may offer better consistency than a trading company that outsources core assemblies. This matters when U.S. buyers need sanitary construction quality, stable lead times, and traceable component control.
Service capabilities: A water system is not complete at shipment. U.S. projects often require FAT support, installation guidance, commissioning, IQ/OQ/PQ documentation assistance, training, spare parts planning, and remote or on-site troubleshooting. Suppliers able to support feasibility, layout review, customization, startup, validation, and after-sales service reduce implementation risk significantly. For direct project discussions, buyers can use contact IVEN Pharmatech Engineering.
The comparison chart reflects the features U.S. buyers should prioritize when screening vendors. A supplier with lower equipment price but weaker validation or service support often becomes the costlier choice over the system lifecycle.
When reviewing supplier background, it is also useful to examine broader company capability and project history. An overview is available at about IVEN Pharmatech Engineering.
Investment Cost, Budget Planning, and ROI Analysis
Capital cost varies widely based on water grade, capacity, redundancy, automation, and qualification scope. A compact PW system for a smaller oral liquid facility may be far less expensive than a fully integrated PW + WFI + purified steam block for a large sterile injectable plant. In the U.S. market, buyers should also include freight, site preparation, utility hookup, validation documentation, local installation support, spare parts, operator training, and contingency for cleanroom interface works.
| Cost Item | Low Complexity Project | Medium Complexity Project | High Complexity Project | Budget Note | ROI Impact |
|---|---|---|---|---|---|
| Core generation equipment | Moderate | High | Very high | Main hardware cost center | Drives quality and uptime |
| Pretreatment package | Low | Moderate | High | Depends on municipal water quality | Reduces membrane failure cost |
| Storage and loop distribution | Moderate | High | Very high | Often underestimated in retrofit projects | Strong effect on microbial control |
| Automation and monitoring | Moderate | Moderate to high | High | Needed for data trending | Improves maintenance efficiency |
| Qualification and documentation | Low to moderate | Moderate | High | Critical for GMP release | Faster startup and fewer deviations |
| Service and training | Low | Moderate | Moderate | Protects early operation phase | Speeds stabilization |
ROI should be evaluated through avoided losses, not just through utility consumption. A well-designed system can reduce batch delays, investigations, sanitization labor, unplanned downtime, and replacement frequency for membranes or valves. In high-margin sterile manufacturing, even one prevented contamination event can justify a substantial portion of the investment.
Budget planning should also consider future expansion. Many U.S. plants underestimate how quickly capacity is consumed once a new client or product is added. Designing for modular growth may offer a better return than building a system that is immediately optimized only for current demand.
A practical ROI model should include:
- Expected annual production value protected by the system
- Historical deviation and downtime cost
- Maintenance labor and spare parts trend
- Energy and water consumption per cubic meter
- Validation and requalification effort
- Potential capacity expansion over three to five years
Key Considerations and Potential Risks When Investing
The most expensive pharmaceutical water treatment problems often originate before the equipment is ever installed. Poor URS definition, incomplete feedwater analysis, inadequate layout planning, or unrealistic startup timelines can create years of recurring trouble.
Key risks include undersizing, overcomplicated control logic, poor hygienic piping design, insufficient turnover in tanks and loops, and a mismatch between water demand pattern and actual system capacity. Facilities near coastal logistics hubs such as Long Beach, Houston, or Savannah must also consider freight timing, component lead times, and commissioning windows when planning upgrades.
| Investment Risk | How It Appears | Likely Root Cause | Business Effect | Mitigation Strategy | Priority |
|---|---|---|---|---|---|
| Wrong technology selection | Frequent quality drift | Poor process mapping | High operating cost | Detailed URS and design review | Critical |
| Feedwater variability ignored | Membrane fouling and instability | Incomplete source water study | Unexpected downtime | Seasonal water analysis and pretreatment design | High |
| Weak loop design | Biofilm hotspots | Dead legs and poor circulation | Microbial excursions | Sanitary piping audit | Critical |
| Low documentation quality | Validation delays | Supplier capability gap | Late project start | Review FAT and qualification package early | High |
| Insufficient service support | Slow troubleshooting | No local or remote response plan | Longer outages | Service agreement and spare parts plan | High |
| Expansion not planned | Capacity shortage after launch | Short-term budgeting only | Repeat capex sooner than expected | Modular design roadmap | Medium |
A useful U.S. case example is a sterile fill-finish expansion where the plant upgraded fillers but kept an aging ambient PW loop with poor turnover. Production scale increased, but water quality stability worsened because the system was no longer aligned with usage profile. The problem was not only age; it was design mismatch. By adding better recirculation control, point-of-use rationalization, and a more robust sanitization program, the site reduced recurring microbial alerts and improved release confidence.
Another example involves a contract manufacturer in the Northeast that selected a low-cost imported industrial-style skid for a GMP application. The equipment could meet basic conductivity targets but lacked proper sanitary execution and qualification support. The result was a long startup delay, custom remediation work, and much higher total cost than planned. The lesson is clear: in pharmaceutical water systems, lifecycle fitness matters more than entry price.
FAQ
What are the most common pharmaceutical water treatment problems?
The most common issues are microbial contamination, endotoxin risk, conductivity drift, TOC excursions, membrane fouling, poor sanitization performance, corrosion, and loop design flaws such as dead legs.
Does every U.S. pharmaceutical plant need WFI?
No. The required water grade depends on the product and process. Many applications use Purified Water, while sterile injectable applications often require WFI or other higher-control utilities based on process design and regulatory expectations.
Is RO plus EDI enough for GMP use?
For many Purified Water applications, yes, if the system is properly designed, qualified, monitored, and maintained. For WFI applications, additional technology such as distillation may be required depending on the plant’s utility strategy and compliance framework.
How often should a pharmaceutical water system be sanitized?
That depends on system design, water grade, operating temperature, microbial trend, and risk assessment. Some systems use routine hot sanitization, while others rely on controlled chemical cycles. Frequency must be justified and documented.
How long does a new system project usually take in the United States?
A project can range from several months for a small upgrade to more than a year for a fully integrated new utility block with qualification. Lead time depends on scope, customization, site readiness, documentation, and commissioning schedule.
What should be included in supplier evaluation?
Review technical design ability, compliance knowledge, fabrication quality, automation depth, FAT execution, documentation package, validation support, spare parts planning, and service responsiveness.
Can an overseas supplier support a U.S. pharmaceutical project effectively?
Yes, if the supplier has strong GMP engineering experience, robust documentation, multilingual support, structured commissioning processes, and the ability to coordinate installation and validation around U.S. project requirements.
What makes IVEN Pharmatech Engineering relevant for U.S. buyers?
Its value lies in combining pharmaceutical engineering knowledge with equipment manufacturing, customized system integration, and full-lifecycle project support. The company has experience across filling, water treatment, logistics, and turnkey delivery, which helps reduce interface risk for complex projects.
Where can I start if I am planning a new pharmaceutical facility or utility upgrade?
Start with process mapping, water usage forecasting, source water analysis, and a clear user requirement specification. If you want to discuss integrated engineering, equipment customization, or turnkey implementation, review turnkey pharmaceutical project capabilities and then request a technical consultation.
In summary, pharmaceutical water treatment problems should be treated as strategic GMP risks for manufacturers in the United States. The best systems are not just compliant on paper; they are engineered for stable real-world operation, validated startup, practical maintenance, and future expansion. As the U.S. market moves toward smarter, cleaner, and more resilient manufacturing by 2026, investment in the right pharmaceutical water infrastructure will continue to be a competitive advantage.
About the Author
We are IVEN Pharmatech Engineering, a team dedicated to delivering turnkey pharmaceutical and medical solutions worldwide. With decades of experience, we specialize in advanced machinery, integrated factory design, and full lifecycle support to help our clients achieve efficient, compliant, and high-quality production.
Share
Related Insights
-
United States Guide to Multi-Chamber IV Bag Integrity
In the United States, multi-chamber IV bag delamination prevention refers to the design, material selection, sealing control, sterilization validation, and manufacturing discipline required to keep layered bag films bonded and functional throughout filling, storage, transport, and clinical use. For pharmaceutical companies, this matters because multi-chamber IV systems allow unstable or incompatible ingredients to remain separated until activation, helping improve shelf life, dosing accuracy, workflow efficiency, and patient safety in hospitals, infusion centers, and emergency care settings.
As the U.S. market continues to demand ready-to-use sterile products, advanced admixture systems, and safer parenteral packaging, delamination prevention has become a strategic issue rather than a narrow packaging defect topic. Manufacturers serving large healthcare networks in cities such as New York, Chicago, Houston, Los Angeles, and Philadelphia must ensure that bags can tolerate sterilization, pallet movement, cold-chain fluctuations where relevant, and long-haul logistics through major trade gateways such as the Port of Los Angeles, Port of Long Beach, Port of Houston, Savannah, and Newark.
For companies evaluating equipment, turnkey plants, or expansion projects, delamination prevention should be assessed at the full system level: film structure, port design, chamber geometry, welding parameters, filling temperature, overpouch protection, leak testing, accelerated aging, and compliance with U.S. FDA cGMP expectations. Businesses seeking integrated engineering support can review the background of IVEN Pharmatech Engineering and compare whether a supplier has the regulatory and process depth needed for high-value IV solution projects in the United States.
Multi-chamber IV bag delamination prevention enables pharmaceutical manufacturers to produce advanced IV solutions that keep active ingredients separate until the point of use, reducing incompatibility risk and preserving formulation stability. In practical terms, prevention involves choosing the right co-extruded or laminated film system, controlling seal integrity, managing thermal stress during sterilization, validating chamber-opening performance, and confirming long-term package compatibility with the solution.
When done well, the result is a sterile container system that can withstand manufacturing, warehousing, truck transport across the United States, and hospital handling without internal layer separation, cloudy interfaces, weak seals, or compromised barrier performance. This is especially important for two-chamber and three-chamber bags used for amino acid and glucose combinations, lipid-containing nutrition systems, electrolyte blends, and drug reconstitution formats.
For U.S. buyers, delamination prevention is not only a packaging quality goal. It is closely linked to product approval success, lower deviation rates, reduced product recalls, better production yield, and stronger confidence from hospital procurement teams. Advanced equipment suppliers that combine process engineering with compliance-oriented factory design can make a major difference in this area.
Delamination Risk AreaMain CauseOperational ImpactClinical ImpactPrevention MethodPriority LevelFilm layer separationPoor resin compatibilityBag rejectionPotential sterility concernValidated film specificationHighSeal zone weaknessIncorrect heat profileLeak failuresAdministration interruptionSeal mapping and in-process controlHighSterilization damageExcess thermal stressHigher scrap rateReduced shelf confidenceAutoclave cycle optimizationHighPort interface stressMismatch of materialsTransport failuresUse error riskPort-to-film compatibility testingMediumStorage degradationOxygen/moisture exposureShorter shelf lifeStability reductionBarrier film design and overpouchMediumActivation failureWeak internal frangible designBatch inconsistencyImproper mixingBurst strength validationHighThe table above shows that delamination is rarely an isolated event. It is often the visible symptom of deeper issues in film architecture, sealing precision, or sterilization balance.
Multi-chamber IV bag delamination prevention is the set of engineering measures used to maintain structural integrity in IV bags made with multiple bonded layers and multiple internal compartments. These bags typically contain separate formulations that are mixed only before administration. The “prevention” side focuses on avoiding separation between film layers, preventing channel leaks, and preserving chamber performance throughout the product life cycle.
The main advantages begin with formulation flexibility. Many active ingredients are unstable when premixed for extended periods. By storing them in separate chambers, manufacturers can deliver more advanced ready-to-activate products without sacrificing stability. Delamination prevention then ensures that the package can support this function reliably.
Another advantage is reduced compounding burden in healthcare settings. In large U.S. hospitals from Boston to San Diego, pharmacy departments face staffing pressure, shortage risks, and strict sterile compounding controls. Multi-chamber bags can reduce on-site preparation steps, improve standardization, and shorten preparation time in emergency or critical care scenarios.
There are also commercial advantages. A stable multi-chamber packaging platform can support differentiated products, longer market reach, and improved export logistics. For manufacturers considering expansion, a turnkey engineering partner with IV solution expertise can help align bag technology, water systems, filling lines, sterilization, and compliance documents. Companies reviewing complete plant planning may find value in integrated turnkey pharmaceutical project capabilities when building or upgrading U.S.-oriented production capacity.
AdvantageDescriptionBenefit for ManufacturerBenefit for HospitalBenefit for PatientU.S. RelevanceIngredient separationKeeps unstable components apartBetter product portfolioLess manual compoundingImproved safetyHighLonger stability windowSupports shelf-life performanceLower wasteMore inventory flexibilityConsistent therapyHighReady-to-activate formatSimple mixing before useDifferentiated product designFaster workflowQuicker administrationHighLower contamination exposureFewer preparation stepsQuality reputationReduced handling riskHigher assuranceHighScalable productionCompatible with automated linesHigher throughputSupply reliabilityBetter accessMediumRegulatory alignmentSupports validated sterile systemsSmoother inspectionsTrusted sourcingSafer treatmentHighIn the U.S. context, these advantages matter most for injectable pharmaceuticals, nutrition support, hospital pharmacy distribution, emergency medicine, and contract manufacturing organizations serving branded or generic sterile products.
Clinically, multi-chamber IV bags are used where stability, speed, and standardized mixing are important. Common applications include parenteral nutrition, electrolyte therapy, perioperative fluids, reconstitution-dependent formulations, and selected specialty infusions. In trauma centers, teaching hospitals, and integrated delivery networks, these products can support faster preparation while reducing compounding variability.
In intensive care units, pharmacists and nurses value systems that reduce aseptic manipulation steps. In oncology-supportive care, nutrition support, or post-operative therapy, a well-designed multi-chamber bag can simplify administration. Pediatric and neonatal applications require especially strict validation because dosage precision and compatibility margins are tighter.
Delamination prevention directly supports clinical reliability. If film layers separate or seal areas weaken, the bag may fail during storage, transport, or activation. Hospitals in the United States increasingly assess packaging robustness because procurement teams want fewer recalls, fewer handling deviations, and stronger continuity of supply.
Major metropolitan hospital systems in cities such as Cleveland, Atlanta, Dallas, and Seattle often evaluate suppliers not only on price but on documentation quality, sterility assurance, change-control discipline, and package performance data. For this reason, the best production programs combine packaging development with validation protocols, extractables and leachables assessment where needed, simulation transport testing, and post-sterilization integrity confirmation.
Hospital ApplicationTypical UseWhy Multi-Chamber HelpsDelamination ConcernValidation FocusBenefit LevelParenteral nutritionSeparate nutrients before useBetter stabilityLayer stress during storageCompatibility and burst testsVery highCritical careRapid standardized infusionFaster workflowActivation reliabilityFrangible opening testsHighEmergency medicineImmediate treatment preparationReduced manual mixingTransport durabilityDrop and vibration testsHighPerioperative careRoutine fluid managementConsistent setupSeal edge weaknessSeal integrity mappingMediumHome infusion supportSimplified administrationUser convenienceShelf-life stressAging studiesMediumPediatric supportCareful formulation handlingSafer preparationSmall-volume design sensitivityDose accuracy and bag functionHighThe table above highlights how the packaging function and the clinical function are tightly connected. In U.S. practice, that link increasingly influences supplier qualification and long-term purchasing decisions.
var ctx1 = document.getElementById(‘lineChart’).getContext(‘2d’);var lineChart = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026′,’2027′,’2028’],datasets: [{label: ‘U.S. Multi-Chamber IV Bag Market Growth Index’,data: [78,84,91,99,108,118,129,141],borderColor: ‘rgb(54, 162, 235)’,backgroundColor: ‘rgba(54, 162, 235, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart illustrates a realistic growth trajectory for the U.S. multi-chamber IV bag segment, supported by demand for ready-to-use sterile formats, reduced compounding burden, and more specialized injectable products.
There is no single universal approach to preventing delamination. The right strategy depends on the formulation, sterilization method, target shelf life, chamber design, and distribution conditions. In the United States, non-PVC soft bag systems remain highly relevant because they can support flexible design, lower breakage risk compared with rigid containers, and suitable performance for many infusion products.
Common film options include multilayer polyolefin structures, co-extruded films, and high-barrier combinations designed to resist heat, moisture transfer, and oxygen ingress. Engineers must balance clarity, toughness, sterilization tolerance, port compatibility, and frangible function. Material science is central here: if layers have poor adhesion or incompatible thermal behavior, the bag may appear acceptable after forming but fail after autoclaving or aging.
Prevention methods typically include optimized resin selection, tie-layer design, sealability studies, edge geometry refinement, and strict incoming material qualification. Some systems also rely on protective overwraps and oxygen absorbers depending on product sensitivity. Manufacturers evaluating line equipment should ensure the machine design supports precise forming, filling, sealing, and cooling control. Detailed equipment choices can be explored through a broad portfolio of pharmaceutical machinery solutions relevant to IV production projects.
Bag or Film TypeTypical Material BaseStrengthsDelamination Risk ProfileBest-Fit ApplicationsU.S. Buying NoteCo-extruded polyolefin bagMulti-layer PP/PE blendsGood heat resistanceModerate if layer adhesion is poorGeneral IV and chambered systemsPopular for modern soft bagsHigh-barrier multilayer bagPolyolefin with barrier layerImproved shelf protectionHigher complexitySensitive formulationsNeeds strong validationNon-PVC flexible bagSpecialized polyolefin filmLow extractable concerns profileDepends on seal designLarge-volume parenteralsWidely considered in U.S. tendersTwo-chamber bagFlexible multilayer filmSimple activationFrangible area criticalReconstitution and nutritionBalance ease and durabilityThree-chamber bagAdvanced multilayer structureHigh formulation flexibilityMore seal interfacesComplex nutrition systemsHigher engineering requirementOverpouched bag systemBag plus secondary barrier wrapExtra protection in logisticsLower storage-related riskLong-distance distributionUseful for national supply chainsThe table shows why material selection should never be separated from process capability. A sophisticated film can still fail in practice if the forming, sealing, or sterilization window is too narrow.
Single-chamber IV bags remain essential in U.S. healthcare because they are simpler, lower cost, and ideal for many standard infusion products. However, multi-chamber bags address a different need: they preserve separation until the point of use. That makes them more valuable for unstable combinations, products with reconstitution steps, and advanced nutrition support.
From a production viewpoint, multi-chamber bags require more sophisticated tooling, more control points, stronger validation, and tighter packaging-process integration. They may also have higher capital costs because internal seal design, activation testing, and product-specific validation are more complex.
From a supply-chain viewpoint, single-chamber bags are easier to manufacture at very high volume, but multi-chamber systems can reduce downstream handling and compounding in hospitals. In markets where labor availability is constrained and sterile workflow simplification is valuable, multi-chamber products offer meaningful total-cost advantages despite higher packaging complexity.
Comparison FactorMulti-Chamber IV BagsSingle-Chamber IV BagsOperational ImplicationClinical ImplicationStrategic ConclusionFormulation separationYesNoMore complex productionBetter compatibility controlStrong advantage for unstable productsPackaging designAdvancedSimplerHigher validation demandMore use flexibilityDepends on product typeUnit costHigherLowerMore CAPEX and QA effortPossible workflow savingsTotal cost should be assessedActivation stepRequiredUsually not requiredNeed usability testingSupports fresh mixingGood for sensitive therapiesDelamination sensitivityHigher concernLower concernMaterial engineering criticalPackage reliability essentialPrevention is a mustHospital labor savingsPotentially significantLimitedSupports ready-to-use strategiesReduces handling stepsImportant in U.S. hospital systemsvar ctx2 = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Stability Support’,’Production Complexity’,’Hospital Convenience’,’CAPEX Need’,’Formulation Flexibility’,’Validation Depth’],datasets: [{label: ‘Multi-Chamber’,data: [92,88,90,82,95,91],backgroundColor: ‘rgba(153, 102, 255, 0.75)’},{label: ‘Single-Chamber’,data: [62,45,68,50,48,60],backgroundColor: ‘rgba(255, 159, 64, 0.75)’}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart demonstrates why multi-chamber bags increasingly attract investment in the United States despite higher complexity. They solve higher-value formulation and hospital workflow problems.
The U.S. market is being shaped by several forces: hospital demand for ready-to-use sterile formats, resilience planning after supply disruptions, interest in domestic or near-market manufacturing, and ongoing investment in advanced injectable products. Health systems want products that reduce pharmacy workload and improve supply continuity. Manufacturers want platforms that support differentiated products and efficient expansion.
There is also rising interest in production lines that can deliver higher automation, stronger digital batch records, and more consistent process control. For delamination prevention, automation helps by reducing process variability in web handling, filling, sealing, cooling, and transport. Inline vision systems, seal inspection, and statistical process trending are becoming more important.
Another trend is regulatory readiness. U.S. buyers increasingly ask whether a supplier can support documentation aligned with FDA expectations, including FAT/SAT packages, validation support, and traceable quality systems. This is where engineering firms with broad compliance exposure stand out. IVEN Pharmatech Engineering, for example, has built its reputation around pharmaceutical engineering, with experience spanning IV solutions, water systems, packaging lines, and full-factory integration designed to meet international GMP frameworks relevant to U.S. projects.
var ctx3 = document.getElementById(‘barChart’).getContext(‘2d’);var barChart = new Chart(ctx3, {type: ‘bar’,data: {labels: [‘Hospital Systems’,’CMOs’,’Generic Injectables’,’Nutrition Products’,’Emergency Stock’,’Home Infusion’],datasets: [{label: ‘Estimated U.S. Demand Index 2026’,data: [94,81,87,78,85,73],backgroundColor: ‘rgba(255, 99, 132, 0.75)’}]},options: {responsive: true,maintainAspectRatio: false}});The bar chart indicates that hospital systems, generic injectable producers, and emergency stock programs are likely to remain major demand drivers.
var ctx4 = document.getElementById(‘areaChart’).getContext(‘2d’);var areaChart = new Chart(ctx4, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026′,’2027′,’2028’],datasets: [{label: ‘Shift Toward Advanced Flexible IV Packaging’,data: [22,27,33,40,49,58,66,74],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,fill: true,tension: 0.35}]},options: {responsive: true,maintainAspectRatio: false}});The area chart reflects a broader trend shift toward higher-value flexible packaging systems with stronger functionality, better logistics performance, and closer integration with hospital workflow needs.
Choosing a reliable supplier in the United States market requires more than checking machine speed or price. Buyers should evaluate technology, manufacturing discipline, validation support, spare parts planning, and after-sales responsiveness. For multi-chamber IV bag delamination prevention, the supplier must understand packaging science and pharmaceutical process control as one connected system.
Start with technological capabilities. Ask whether the supplier can support film evaluation, seal parameter development, chamber design optimization, sterilization matching, and integrity testing. A company with deep IV solution know-how should be able to discuss soft bag lines, water-for-injection systems, solution preparation, filling, sterilization interfaces, and quality risk management rather than only selling a forming machine.
Next, review manufacturing capabilities. Buyers should ask where equipment is produced, how critical components are qualified, what level of stainless-steel durability is standard, and whether previous installations have demonstrated long service life. IVEN Pharmatech Engineering is known for specialized manufacturing resources in pharmaceutical filling and packaging, water treatment, intelligent conveying, and related medical production equipment, which can be important when building an integrated project rather than sourcing isolated machines.
Finally, evaluate service capabilities. U.S. projects often require feasibility input, engineering layout work, installation planning, commissioning, validation support, operator training, and long-term maintenance. A supplier with lifecycle services can reduce risk during start-up and scale-up. If you need a project-specific discussion, a direct consultation with the supplier’s technical team is more useful than relying on general brochures.
Supplier Evaluation PointWhat to AskWhy It MattersGood SignWarning SignDecision ImpactFilm and package knowledgeCan they guide material selection?Core to delamination preventionProvides test matrix and data approachFocuses only on equipment speedHighRegulatory readinessDo they understand U.S. cGMP needs?Supports qualificationStructured documentation supportMinimal validation awarenessHighProject experienceHave they built IV solution lines before?Reduces startup riskMultiple reference installationsOnly generic packaging experienceHighManufacturing depthDo they produce key systems in-house?Improves control and coordinationSpecialized production facilitiesHeavy outsourcing without oversightMediumService modelWhat happens after delivery?Protects ROICommissioning, training, validation helpParts-only supportHighScalabilityCan the line grow with demand?Supports future expansionModular engineering designRigid one-size setupMediumThis table is useful because supplier mistakes in sterile packaging projects are expensive and difficult to correct after installation. Strong technical due diligence is essential.
Investment costs vary widely based on production scale, degree of automation, cleanroom scope, utilities, water systems, sterilization equipment, packaging inspection, and validation requirements. In the U.S. market, a project budget should include far more than the forming-filling-sealing line itself. Engineering design, utility integration, IQ/OQ/PQ support, film qualification trials, warehouse planning, and operator training all affect the final investment.
A realistic ROI analysis should compare added packaging complexity against product differentiation, hospital demand, reduced waste, improved shelf-life performance, and the possibility of premium positioning. Companies should also consider whether multi-chamber capability can open new contract manufacturing business, especially for healthcare systems seeking resilient domestic supply channels.
From a budgeting perspective, one of the biggest mistakes is underestimating validation, materials testing, and process development time. Delamination prevention is not solved by equipment purchase alone; it requires engineering trials and stability-oriented package qualification. Firms that invest early in process understanding usually reduce deviation costs later.
Cost CategoryTypical Budget WeightWhat It IncludesHidden RiskROI EffectPlanning AdviceCore production lineHighForming, filling, sealing equipmentUnder-specifying automationMajor throughput driverMatch line to future capacityUtilities and water systemsHighPW/WFI, steam, HVAC, compressed airIntegration gapsCritical for compliancePlan as one systemSterilization and coolingMedium to highAutoclaves, handling, validationFilm stress problemsDirect effect on yieldRun film-specific studiesPackaging materialsMediumFilm, ports, overpouch, cartonsInconsistent suppliersAffects shelf life and scrapQualify multiple sources carefullyValidation and QAMediumIQ/OQ/PQ, integrity studies, stabilityDelayed launchProtects market entryBudget early, not lateTraining and serviceMediumOperations, maintenance, troubleshootingWeak startup executionImproves uptimeDemand lifecycle supportIn many projects, the best ROI comes from reducing failure costs rather than chasing the lowest initial capital outlay. Preventing even a limited number of rejected batches can materially improve the economics of a multi-chamber program.
The biggest risk is assuming that delamination prevention is only a film supplier issue. In reality, the risk spans material sourcing, design transfer, machine settings, sterilization load pattern, warehouse temperature exposure, and shipping conditions. A bag that performs well in pilot lots may fail at commercial scale if tension control, seal cooling, or autoclave loading are inconsistent.
Another key consideration is regulatory change readiness. By 2026 and beyond, U.S. buyers will likely place even greater emphasis on data integrity, process monitoring, traceability, and resilient supply chains. Sustainability will also matter more. Manufacturers will need to evaluate material efficiency, lower-waste line design, energy use in sterilization, and packaging reduction without compromising barrier or strength performance.
Policy trends may also support advanced domestic production capacity, especially for essential medicines and critical hospital supplies. That could increase demand for turnkey facilities and flexible packaging lines capable of producing sophisticated sterile formats at scale. Companies entering this space should plan for modular expansion, digital quality systems, and robust change-control procedures.
Case experience shows that success often comes from integrated execution. A supplier with strong technological capabilities can help optimize bag design and process windows. A supplier with strong manufacturing capabilities can ensure durable, precision-built equipment. A supplier with strong service capabilities can support commissioning, training, validation, and post-startup optimization. This combined model lowers risk much more effectively than fragmented procurement.
Risk AreaExample ProblemShort-Term EffectLong-Term EffectMitigation StrategyPriorityMaterial mismatchFilm fails after sterilizationBatch rejectionLaunch delayJoint film-process qualificationHighWeak process developmentUnstable seal windowHigh scrapRecurring deviationsDOE and control strategyHighInsufficient validationIncomplete data packageApproval delayAudit findingsStructured IQ/OQ/PQ planningHighSupply chain disruptionPort or resin delaysMaterial shortageCustomer dissatisfactionDual sourcing and stock policyMediumLimited service supportSlow troubleshootingExtended downtimeHigher operating costService agreement and trainingMediumSustainability pressureHigher energy and packaging burdenCost pressureProcurement disadvantageEfficient utilities and lighter designMediumFor companies serving the United States, the safest path is to choose a partner that can connect engineering, manufacturing, and compliance. IVEN Pharmatech Engineering is often considered in this context because it combines IV solution equipment knowledge, integrated factory engineering, and service support across feasibility, installation, validation, and training. That kind of end-to-end coordination can be especially valuable for projects where delamination prevention is tied directly to commercial success.
What causes delamination in multi-chamber IV bags?The most common causes are poor layer adhesion, incompatible film materials, incorrect sealing temperatures, sterilization stress, port-interface mismatch, and long-term storage exposure. Delamination can also emerge when scale-up changes are made without revalidation.
Why is delamination prevention so important in the United States?Because U.S. hospitals, regulators, and procurement teams expect high package reliability, traceable quality, and strong sterility assurance. A delamination event can trigger batch loss, recalls, supply interruption, and reputational damage.
Are multi-chamber bags always better than single-chamber bags?No. They are better when formulation separation is necessary or when hospital workflow benefits justify the extra complexity. Single-chamber bags remain the right choice for many standard products.
Which film materials are commonly used?Co-extruded polyolefin and other multilayer non-PVC films are common, especially where thermal resistance and compatibility are required. The correct material depends on the formulation and sterilization profile.
How should a buyer evaluate a supplier?Assess technical depth, IV solution project experience, regulatory understanding, manufacturing quality, lifecycle service, and the ability to integrate packaging, utilities, validation, and training. A general equipment seller is rarely enough for a high-value sterile project.
Can a turnkey project model reduce delamination risk?Yes. A well-managed turnkey approach can align film choice, equipment configuration, clean utilities, line layout, validation planning, and operator training from the start, which reduces mismatch-related risk.
What future trends should investors watch through 2026?Expect stronger use of digital process monitoring, more sustainability targets, more resilient domestic production planning, tighter data traceability, and higher demand for advanced ready-to-use sterile packaging in the U.S. market.
Where can I discuss a project in more detail?For companies assessing a new line, upgrade, or full-factory project, the most efficient next step is a technical conversation tailored to capacity, formulation, compliance, and budget goals through a direct project inquiry.
In summary, multi-chamber IV bag delamination prevention is a strategic capability for pharmaceutical manufacturers targeting advanced sterile products in the United States. It improves package reliability, supports product stability, reduces hospital preparation burden, and strengthens long-term competitiveness. The strongest outcomes come from combining material science, precise equipment, compliance-ready engineering, and full lifecycle support.
-
United States Micro Blood Tube Filling Equipment Guide
Medical device manufacturers in the United States are under constant pressure to deliver safer, cleaner, and more consistent blood collection products to hospitals, physician offices, urgent care networks, and diagnostic laboratories. In that environment, micro blood tube machine additive filling has become a strategic production solution rather than a simple equipment purchase. It allows companies to automate additive dosing, capillary or microtube handling, drying or coating control, capping, inspection, labeling, and packing with repeatable accuracy. For organizations supplying pediatric blood collection, point-of-care testing, and small-volume diagnostic workflows, the right automated filling line can significantly improve quality assurance, reduce manual variability, and support scalable manufacturing for the U.S. market.
For buyers evaluating production expansion, compliance readiness, and long-term operating cost, the decision is not just about speed. It is about matching machine design with FDA expectations, process validation, additive chemistry, packaging format, and downstream logistics. Companies serving major healthcare corridors such as Boston, Chicago, Houston, Atlanta, and Los Angeles often need equipment that can integrate into highly regulated facilities and still support output growth. This guide explains how micro blood tube machine additive filling works, where it is used, what configurations are available, how it compares with manual assembly lines, what the U.S. market outlook looks like, and how to assess suppliers and investment returns.
When global manufacturers seek a partner with broad pharmaceutical and medical device engineering experience, many also look for integrated project capability. IVEN Pharmatech Engineering is known in the sector for combining production equipment knowledge with regulated-facility engineering, which is especially relevant when a buyer is building not only a line but also a compliant manufacturing system. Companies that need a wider factory solution can also review its turnkey engineering capabilities or explore available product categories through its equipment portfolio.
In direct terms, micro blood tube machine additive filling is an automated production process used to dispense anticoagulants, clot activators, separation gel, or other specialty reagents into small blood collection tubes with high precision. It is designed for medical device manufacturers producing capillary blood collection consumables, especially products intended for pediatric use, low-volume draws, or decentralized testing settings.
In the United States, this type of automation matters because quality failures in blood collection tubes can lead to specimen rejection, testing delays, inaccurate diagnostics, and costly recalls. A well-designed line helps control critical parameters such as additive volume, coating uniformity, contamination risk, capping force, drying conditions, and final inspection. The result is higher throughput, more predictable batch consistency, and stronger documentation for quality systems.
For medical device companies supplying hospital networks in New York, laboratory groups in New Jersey, research centers in California, or distribution hubs around Memphis and Dallas, automated micro blood tube filling also improves supply reliability. Rather than depending on labor-intensive manual steps, manufacturers can create stable, validated production with electronic recipes, in-process monitoring, and traceability features that support U.S. regulatory expectations.
Key BenefitWhy It MattersTypical Impact on U.S. ProductionAccurate additive dosingMaintains specimen integrity and intended tube performanceReduces out-of-spec batches and customer complaintsAutomated tube handlingLimits manual contact and contamination riskImproves cleanliness and GMP alignmentIntegrated inspectionChecks fill status, cap placement, and cosmetic qualitySupports release decisions and lower rejection ratesHigh-speed outputMeets large hospital and lab demandEnables supply contracts with regional healthcare groupsBatch traceabilityTracks raw materials, settings, and resultsSupports audits, CAPA, and investigationsLower labor dependenceReduces variability from hand assemblyHelps offset rising labor costs in the United StatesThe table above shows why buyers increasingly view micro blood tube machine additive filling as both a quality investment and a capacity investment. The strongest business case usually appears when a manufacturer needs repeatability, validated output, and scalable production for hospital and laboratory contracts.
A micro blood tube machine additive filling line is specialized equipment used to process miniature blood collection tubes by automatically feeding tubes, orienting them, dosing chemical additives, drying or distributing the additive when necessary, assembling caps or closures, inspecting product quality, and preparing finished units for packaging. Depending on product design, the line may handle EDTA, heparin, sodium citrate, clot activators, or custom formulations used in diagnostics.
The operating principle is straightforward but technically demanding. Empty microtubes are first loaded through a hopper, unscrambler, or conveyor infeed. The tubes are then positioned for filling, usually through indexing plates or precision nests that stabilize small-format parts. A dosing system, often using peristaltic pumps, ceramic pumps, or high-precision liquid filling modules, dispenses the required additive volume into each tube. Some products require only a liquid addition; others require internal coating and controlled drying to ensure the final tube performs correctly during blood collection.
After filling, the line may include spinning, vibration, or internal wetting control to spread the reagent evenly. Drying stations, low-particle air management, and environmental controls can be included for additives that must achieve a stable internal coating. Closure application follows, often with cap insertion, snap-fit assembly, or push cap loading. Final stations may include visual inspection, leak checking, code printing, labeling, tray packing, bagging, or carton loading.
In facilities serving the U.S. market, machine validation is just as important as machine motion. Equipment should support IQ, OQ, and PQ activities, recipe management, and data recording aligned with quality systems. This is where technological capability becomes decisive. IVEN Pharmatech Engineering is recognized for integrating pharmaceutical-grade process thinking into equipment design, including regulated manufacturing logic, intelligent control architecture, and customization for high-compliance production environments.
Process StepMain FunctionTypical Equipment ModuleTube feedingTransfers empty microtubes into the lineHopper, bowl feeder, unscramblerOrientationPositions tubes accurately for dosingIndex wheel, nest conveyor, precision fixtureAdditive fillingDispenses reagent into each tubePeristaltic or ceramic pump filling unitCoating or mixingSpreads additive on internal surfaces if requiredRotation, vibration, or air-assisted stationDryingRemoves solvent or stabilizes coatingControlled air or thermal drying tunnelCapping and inspectionCloses and verifies finished tube qualityCap feeder, press station, camera inspectionThis process map helps buyers understand where performance differences arise. A supplier that only focuses on fill speed may not deliver enough control at the coating, drying, or inspection stages. For many U.S. manufacturers, those downstream controls determine whether the line can actually maintain commercial quality.
The main applications for micro blood tube machine additive filling are found in pediatric blood collection, capillary sampling systems, decentralized healthcare testing, laboratory consumables, and specialty diagnostic kits. As more care shifts closer to the patient, including retail clinics and home-adjacent testing support, demand for consistent micro-collection products continues to grow.
Hospitals and lab systems in the United States increasingly need tube products tailored for neonatal care, oncology monitoring, geriatrics, and situations where limited blood volume must be collected without compromising analytical performance. Automated additive filling helps maintain the intended blood-to-additive ratio and reduces the variability that can occur when products are assembled manually.
Production benefits extend beyond quality. Companies can shorten lead times, reduce dependence on skilled manual operators, improve line balance, and simplify process validation. High-volume manufacturers distributing through East Coast hubs like Newark and Savannah or West Coast gateways such as Los Angeles and Long Beach often benefit from automation because consistent output supports inventory planning and contract fulfillment.
Application AreaTypical End UserProduction BenefitPediatric blood collectionChildren’s hospitals and clinicsHigh consistency for small-volume drawsNeonatal screening supportHospital laboratoriesReliable tube chemistry and low rejection ratesPoint-of-care sample preparationUrgent care and decentralized testing centersFast supply replenishment and scalable outputResearch and clinical trialsBiotech and CRO facilitiesControlled additive specifications for protocolsRoutine diagnosticsReference labs and hospital lab networksStable batch-to-batch performanceSpecialty diagnostic kitsOEM medical device brandsCustom filling recipes and product differentiationThe table shows that the same core machine can serve different markets if it is configurable enough. For OEM medical device companies, that flexibility creates a strategic advantage because they can support both standard and customized SKUs without building separate production systems.
var ctxBar = document.getElementById(‘barDemandChart’).getContext(‘2d’);var barDemandChart = new Chart(ctxBar, { type: ‘bar’, data: { labels: [‘Hospital Labs’, ‘Reference Labs’, ‘Pediatric Care’, ‘Urgent Care’, ‘Biotech Research’, ‘OEM Device Brands’], datasets: [{ label: ‘Estimated U.S. Demand Index’, data: [92, 88, 76, 64, 58, 71], backgroundColor: [‘#4e79a7′,’#59a14f’,’#f28e2b’,’#e15759′,’#76b7b2′,’#af7aa1′] }] }, options: { responsive: true, maintainAspectRatio: false }});The demand chart illustrates why mainstream laboratory channels remain the largest volume drivers, while pediatric, OEM, and urgent care segments present strong growth niches. For manufacturers, this means a line should be selected not only for current output but also for future market positioning.
Not all micro blood tube machine additive filling systems are built the same. Buyers in the United States typically encounter four broad categories: semi-automatic bench or compact units, standard fully automatic filling lines, integrated filling-plus-capping lines, and high-end turnkey systems combining filling, drying, inspection, labeling, and packaging.
Semi-automatic machines are often chosen for pilot production, R&D work, or lower-volume specialty products. Standard automatic lines are used when manufacturers need stable throughput with better labor efficiency. Integrated lines appeal to companies that want a smaller footprint and fewer transfer points. Turnkey systems are generally selected by larger medical consumable manufacturers that need comprehensive validation, material flow planning, and factory-level integration.
Configuration variables include number of filling heads, additive type compatibility, drying method, cap feeder design, in-line vision inspection, cleanroom adaptation, MES or SCADA connectivity, and downstream packaging. A company planning to supply multiple states or national contracts should consider whether future capacity expansion can be achieved through modular upgrades.
Manufacturing capability also matters. IVEN Pharmatech Engineering supports buyers through specialized production resources dedicated to pharmaceutical filling and packaging machinery, intelligent conveying systems, water treatment systems, and vacuum blood collection tube equipment. That broader manufacturing base can be useful when a project requires coordination across several linked systems instead of a stand-alone machine.
Machine TypeBest ForOutput LevelKey AdvantageSemi-automatic fillerR&D and small batchesLowLower entry cost and flexibilityBasic automatic fillerGrowing production linesMediumImproved dosing consistencyFilling and capping lineRoutine commercial manufacturingMedium to highReduced manual handling stepsIntegrated fill-dry-cap-inspect lineRegulated high-volume outputHighStrong quality control and efficiencyTurnkey production systemNew factory projectsHighFull process coordination and validation supportCustom OEM configurationSpecial tube formats or additivesVariableTailored process and product fitThe best configuration depends on product mix, batch size, and the maturity of the buyer’s quality system. A standard automatic line may be enough for one product family, but a broader U.S. launch often benefits from inspection modules, recipe controls, and packaging integration that reduce risk over time.
Manual assembly lines can still be found in smaller operations, especially when product volumes are low or the manufacturer is in an early development stage. However, as soon as a company needs repeatability at commercial scale, the disadvantages of manual processing become difficult to ignore. Human dispensing inconsistency, handling contamination, ergonomic fatigue, training variability, and limited traceability all affect output quality.
By contrast, automated micro blood tube machine additive filling lines control dose volume, cycle timing, capping alignment, and inspection criteria with much greater precision. They also generate cleaner documentation for process validation and quality review. In a U.S. environment where labor costs, turnover, and compliance expectations are all rising, automation often delivers a stronger long-term operating model.
FactorAutomated Filling LineManual Assembly LineDosing accuracyHigh and programmableOperator dependentProduction speedStable medium to high outputLow to moderateTraceabilityElectronic and batch-linkedMostly paper-based or fragmentedContamination controlBetter through limited handlingHigher exposure riskLabor requirementLower per unit producedHigher and more variableScalabilityStrong with modular expansionWeak for national demand growthThe differences above explain why many U.S. manufacturers move away from manual assembly once they begin supplying large hospital systems or national laboratory distributors. Manual lines can still be useful for development or backup work, but they are rarely ideal for sustained commercial production.
var ctxComp = document.getElementById(‘comparisonChart’).getContext(‘2d’);var comparisonChart = new Chart(ctxComp, { type: ‘bar’, data: { labels: [‘Accuracy’, ‘Throughput’, ‘Traceability’, ‘Labor Efficiency’, ‘Compliance Readiness’, ‘Scalability’], datasets: [ { label: ‘Automated Line Score’, data: [95, 90, 93, 88, 94, 91], backgroundColor: ‘#6f4ef2’ }, { label: ‘Manual Line Score’, data: [62, 48, 41, 35, 54, 39], backgroundColor: ‘#c9b8ff’ } ] }, options: { responsive: true, maintainAspectRatio: false }});This comparison chart makes the strategic gap clear. Even when manual assembly appears less expensive upfront, the total production model is usually weaker once quality risk, labor intensity, and documentation burdens are considered.
The U.S. market outlook for micro blood tube machine additive filling is supported by several converging trends: rising demand for diagnostic testing, higher use of pediatric and low-volume collection formats, supply chain regionalization, and increasing emphasis on domestic or near-market manufacturing resilience. Healthcare systems want more dependable access to critical consumables, and manufacturers want better control over quality and lead times.
Growth opportunities are especially visible in states with strong life science infrastructure, including Massachusetts, New Jersey, North Carolina, California, Texas, and Indiana. Contract manufacturing organizations, OEM device brands, and diagnostic kit developers are all evaluating whether they should internalize more consumable production or upgrade older lines. Ports and logistics corridors also matter. Companies importing components through Long Beach, Houston, or Savannah often seek more automated final assembly in the United States to reduce finished goods risk.
Looking toward 2026, the market is expected to favor machines with digital traceability, lower reagent waste, faster format changeover, and better cleanroom compatibility. Policy pressure around supply security and sustainability will likely encourage production systems that reduce scrap, energy waste, and water use while supporting documented quality performance.
var ctxLine = document.getElementById(‘lineGrowthChart’).getContext(‘2d’);var lineGrowthChart = new Chart(ctxLine, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Estimated U.S. Market Value Index’, data: [100, 108, 117, 127, 139, 152], borderColor: ‘#1f77b4’, backgroundColor: ‘rgba(31,119,180,0.08)’, fill: false, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});The line chart shows a realistic upward trajectory rather than explosive growth. That pattern is typical for medical manufacturing equipment markets driven by compliance, installed base replacement, and incremental expansion rather than short-term hype.
var ctxArea = document.getElementById(‘areaTrendChart’).getContext(‘2d’);var areaTrendChart = new Chart(ctxArea, { type: ‘line’, data: { labels: [‘2021’, ‘2022’, ‘2023’, ‘2024’, ‘2025’, ‘2026’], datasets: [{ label: ‘Share of Automated Production in New Installations’, data: [52, 57, 63, 69, 74, 80], borderColor: ‘#2ca02c’, backgroundColor: ‘rgba(44,160,44,0.25)’, fill: true, tension: 0.25 }] }, options: { responsive: true, maintainAspectRatio: false }});The area chart highlights a shift from basic filling equipment toward more integrated automation. By 2026, buyers are likely to prioritize machine intelligence, inspection automation, and data readiness over simple mechanical speed alone.
Choosing the right supplier requires more than comparing quotations. U.S. buyers should evaluate technical fit, regulatory understanding, documentation quality, spare parts strategy, after-sales service, and the supplier’s ability to adapt the machine to actual production conditions. A low-cost machine that cannot be validated or maintained efficiently may become far more expensive than a higher-priced but better-supported system.
Start with process capability. Ask the supplier to define dosing accuracy, speed range, format compatibility, additive handling limits, and cleaning procedures. Then move into compliance support. Can the supplier provide FAT protocols, SAT support, validation documentation structure, electrical and software records, and material certificates where required? For FDA-facing operations, clarity in these areas is essential.
Service capability is another major differentiator. IVEN Pharmatech Engineering is often evaluated favorably by international buyers because it combines equipment supply with broader lifecycle support such as engineering consultation, installation, commissioning, validation assistance, training, and ongoing optimization. That model can reduce project coordination risk, especially for buyers setting up a new production area or expanding a multi-line facility.
Finally, assess whether the supplier can support U.S. operating realities. Lead times, remote diagnostics, replacement parts availability, and communication responsiveness all matter. If your facility is in Phoenix, Cleveland, Philadelphia, or the Research Triangle, downtime costs can be significant, so practical service readiness should be weighted heavily.
Selection CriterionWhat to AskWhy It MattersTechnical performanceWhat dosing accuracy and speed are guaranteed?Determines production capability and quality stabilityRegulatory supportAre IQ/OQ/PQ documents and FAT protocols available?Helps streamline validation in the United StatesMaterial and build qualityWhich contact materials and control components are used?Affects durability, cleanability, and lifecycle costCustomization abilityCan the machine handle our tube format and additive?Prevents poor fit with real production needsAfter-sales serviceHow are parts, training, and support delivered?Reduces downtime and operational riskProject experienceHas the supplier completed regulated or turnkey projects?Signals stronger execution and integration capabilityThe best purchasing decision usually comes from balancing machine performance, validation readiness, and support depth. This is especially important for companies planning long production runs or nationwide distribution.
Investment cost for micro blood tube machine additive filling varies widely based on automation level, speed, inspection content, customization, and facility integration needs. A compact semi-automatic system may suit a development lab, while a validated high-speed line with drying, vision inspection, and packaging integration requires a much larger capital budget. U.S. buyers should consider the total installed cost, not just the machine base price.
Total budget typically includes equipment, shipping, import handling, site preparation, utilities, cleanroom modifications, qualification, training, spare parts, and start-up scrap. If the project includes broader process integration, additional costs may involve conveyors, packing lines, water systems, or digital manufacturing interfaces. Buyers in inland markets such as St. Louis or Minneapolis may also see different freight and installation planning than buyers near coastal entry points.
ROI is usually driven by labor savings, yield improvement, lower batch rejection, faster order fulfillment, and the ability to take on higher-volume contracts. In many cases, the strongest return does not come from labor reduction alone. It comes from converting quality consistency into customer retention and regulatory confidence.
Budget ItemLow Automation ProjectHigh Automation ProjectBase equipmentLowerHigherInstallation and commissioningModerateModerate to highValidation supportBasicExtensiveInspection systemsLimited or manualIntegrated vision and reject controlLabor cost over timeHigherLower per unitExpansion potentialLimitedStrongThe table above should be read as a budgeting framework rather than a fixed quotation. For many U.S. companies, a higher initial investment becomes more attractive once three- to five-year operating costs are modeled against expected demand.
A practical ROI checklist includes the following questions: How many operators can be reallocated? What is the current scrap or rework rate? How much does a failed batch cost? What annual growth is expected? Can the line support multiple SKUs? How quickly can validation be completed? If these answers are quantified early, the investment case becomes much clearer.
The biggest investment risks are usually poor process fit, underestimated validation effort, weak service support, and unrealistic throughput assumptions. Some buyers purchase a line based mainly on nominal speed, then discover that actual production output is limited by additive viscosity, drying time, cap supply quality, or inspection reject frequency. That is why factory acceptance testing with representative materials is so important.
Another risk is under-planning for U.S. regulatory and documentation needs. A line may be mechanically sound yet still create delays if software records, calibration strategy, or change control expectations are not addressed properly. Sustainability is also becoming more relevant. By 2026, many buyers will be evaluating energy efficiency, compressed air use, reagent waste reduction, and recyclable packaging compatibility as part of procurement decisions.
There are also supply chain risks. Imported lines can face shipping delays, customs variability, or spare parts lead-time issues if support planning is weak. Buyers should ask for critical spare parts lists, recommended inventory, remote support procedures, and escalation contacts before finalizing the purchase. If you need project-specific guidance, direct communication with the supplier through the contact page can help clarify engineering scope, timelines, and support expectations.
From a strategic standpoint, the safest path is often to work with a supplier that understands both equipment and plant-level execution. Companies with proven experience across regulated production lines, factory layout logic, and commissioning workflows are generally better equipped to manage hidden project risks.
1. What additives can a micro blood tube machine additive filling line handle?Most lines can be configured for EDTA, heparin, sodium citrate, clot activators, and certain customized formulations. Compatibility depends on viscosity, required fill volume, coating behavior, and cleaning requirements.
2. Is this equipment suitable for the United States regulatory environment?Yes, if it is designed with appropriate documentation, validation support, and quality control features. Buyers should confirm alignment with FDA-oriented quality systems, traceability expectations, and facility requirements.
3. How much output can a line produce?Output depends on tube design, number of heads, additive type, drying time, and packaging integration. A realistic supplier discussion should focus on validated net output, not only theoretical speed.
4. Can the machine be customized for different tube sizes and caps?In many cases, yes. Format parts, recipes, capping modules, and handling fixtures can often be adapted for different microtube dimensions and closure styles.
5. What industries benefit most from this equipment?Medical consumables manufacturing, diagnostic device production, clinical research supply, hospital consumable OEMs, and specialty laboratory product manufacturers all benefit from automated additive filling.
6. How long does implementation usually take?Lead time varies by complexity. A standard line may move faster, while a highly customized or turnkey system may require more engineering, FAT review, shipping time, installation, and validation effort.
7. What should I request from a supplier before purchasing?Ask for URS alignment, layout drawings, utility requirements, sample testing plans, accuracy data, FAT scope, spare parts list, training plan, and validation document examples.
8. Is turnkey support valuable for new U.S. facilities?Very much so. When a supplier can support engineering, installation, commissioning, and qualification in addition to equipment supply, project coordination becomes more efficient and risk is reduced.
9. What future trends will matter most by 2026?Expect stronger demand for machine connectivity, predictive maintenance, electronic batch support, low-waste dosing systems, sustainable design, and flexible automation that supports both standard and custom microtube products.
10. Why do some buyers prefer integrated engineering partners?Because equipment alone is only one part of success. Buyers often need help with layout, utilities, validation planning, scale-up, and long-term technical support. A partner that can deliver across those stages usually provides better project security.
In summary, micro blood tube machine additive filling is becoming a critical capability for medical device companies that want dependable quality, scalable production, and stronger competitiveness in the United States. The right system should be chosen not only for output, but also for compliance readiness, additive process control, service support, and long-term return on investment. For organizations evaluating broader regulated manufacturing projects, suppliers with strong technological depth, specialized manufacturing resources, and lifecycle service capability can offer a significant advantage.
-
Vacuum Blood Tube Line Troubleshooting in United States
For medical device companies in the United States, vacuum blood tube line troubleshooting is a practical way to maintain stable output, reduce rejects, and produce high-quality blood collection tubes for hospitals, labs, and diagnostic networks. A well-managed automated line supports reliable vacuum control, additive dosing, stopper fitting, labeling, inspection, and packaging while helping teams meet strict quality and regulatory expectations.
As demand for blood collection consumables grows across major healthcare centers in New York, Chicago, Houston, Los Angeles, Boston, Atlanta, and Philadelphia, manufacturers are under pressure to deliver consistent tube performance at scale. Problems such as vacuum instability, stopper leakage, inaccurate additive filling, labeling offsets, contamination risk, and downtime can quickly affect supply commitments. That is why line diagnostics, preventive maintenance, validation, and supplier support are increasingly important for U.S. factories and contract manufacturers.
Companies looking for integrated equipment and project support often evaluate partners with strong engineering depth, global compliance experience, and practical field service. IVEN Pharmatech Engineering is known in this space for pharmaceutical and medical consumables engineering, including vacuum blood collection tube production systems, and supports customers with customized manufacturing solutions for regulated environments.
Vacuum blood tube line troubleshooting is the systematic identification, analysis, and correction of faults across an automated blood collection tube manufacturing process. In practical terms, it covers every key station: tube feeding, washing or air cleaning, additive dosing, drying where required, stopper insertion, vacuum generation, cap assembly, labeling, lot coding, online inspection, tray loading, and final packaging.
For U.S. medical device manufacturers, the biggest value comes from three outcomes. First, troubleshooting protects product quality by reducing defects such as under-vacuum tubes, stopper looseness, additive deviation, particulate contamination, and barcode read failure. Second, it improves equipment availability by reducing unplanned downtime and shortening changeover recovery. Third, it supports regulatory readiness by creating documented corrective actions, trend records, and validation evidence that can be aligned with FDA-oriented quality systems.
In a high-volume plant serving hospital systems, diagnostic chains, or OEM buyers, even a small defect rate can translate into large scrap costs. A line producing millions of tubes per month needs consistent process capability. When troubleshooting is built into the production strategy, manufacturers can detect early warning signs from sensors, PLC alarms, vacuum decay data, vision inspection trends, and maintenance logs before a larger failure disrupts output.
Production IssueTypical Root CauseOperational ImpactTroubleshooting MethodCorrective ActionExpected ResultLow vacuum levelSeal leakage or unstable vacuum pumpBlood draw volume inconsistencyVacuum decay test and seal inspectionReplace worn seals and recalibrate vacuum systemStable tube draw performanceStopper misfitCap feeder misalignmentLeaks and rejectsMechanical alignment checkAdjust feeder rails and insertion pressureBetter closure integrityAdditive fill variationDosing pump driftClinical performance riskWeight verification and pump auditRecalibrate dosing moduleMore accurate additive volumeLabel skewTube rotation instabilityPoor presentation and scan issuesVision system reviewAdjust label applicator timingHigher label accuracyParticle contaminationAir cleanliness or handling issueQuality nonconformanceEnvironmental monitoring reviewImprove air control and cleaning SOPsCleaner production conditionsFrequent downtimeWorn moving parts or poor maintenanceOutput lossDowntime Pareto analysisPreventive maintenance upgradeHigher OEEThe table above shows why troubleshooting is not limited to emergency repair. It is a full production discipline connecting process engineering, quality assurance, machine design, utilities, and operator training.
A vacuum blood collection tube line is an integrated production system used to manufacture evacuated tubes for blood sampling. It typically includes tube handling, chemical dosing, drying, rubber stopper or cap assembly, vacuum creation, leak testing, printing or labeling, inspection, and packaging. Troubleshooting within this environment means finding where the process deviates from specification and restoring it with minimum disruption.
The workflow usually starts with data. Modern lines generate alarm logs, cycle counts, reject rates, servo position data, vacuum readings, and vision inspection images. A troubleshooting engineer reviews these signals to determine whether a fault is mechanical, electrical, pneumatic, software-based, environmental, or material-related. For example, if vacuum values drift only during night shifts, the issue may relate to utility fluctuation, operator settings, or ambient conditions rather than the vacuum module itself.
On advanced equipment, troubleshooting is often layered into the control architecture. Sensors detect tube presence, stopper depth, dosing accuracy, cap position, and label placement. Vision systems identify cosmetic and dimensional defects. PLC and HMI systems record alarm history. In more connected factories, SCADA or MES platforms compare batches, operators, and line performance across shifts or plants.
Strong technological capability matters here. IVEN Pharmatech Engineering has built multiple generations of vacuum blood collection tube equipment and applies engineering knowledge from broader pharmaceutical machinery and utility systems. This cross-disciplinary capability is useful because tube line performance depends not only on the machine itself but also on clean utilities, process consistency, automation stability, and validation documentation.
Line SectionMain FunctionCommon FaultDiagnostic SignalPriority LevelRecommended ResponseTube feedingSupply empty tubesJam or orientation errorFeeder alarm and line stopHighCheck guides, sensors, and tube dimensionsAdditive dosingDispense reagentOverfill or underfillWeight deviation trendCriticalCalibrate pump and inspect nozzlesDrying stationPrepare coated tubeIncomplete dryingResidue or adhesion issueMediumVerify temperature and airflow profileStopper insertionSeal tube openingShallow insertionLeak or height varianceCriticalAdjust force, tooling, and stopper feedVacuum generationCreate set negative pressureVacuum inconsistencyOnline pressure dataCriticalInspect seals, pump, and chamber timingInspection and labelingConfirm quality and identityReject spikesVision images and scanner alarmsHighRe-teach camera and stabilize rotationThis table illustrates how troubleshooting works in practice: each station has a defined purpose, measurable signals, and targeted corrective actions. The best production teams create standard fault trees and escalation paths so that small issues are solved quickly before they escalate into scrap, missed shipments, or customer complaints.
Vacuum blood tube line troubleshooting is especially valuable for manufacturers serving clinical laboratories, hospital procurement groups, phlebotomy supply distributors, and OEM private-label brands. The U.S. market expects dependable fill volume, additive integrity, sterility control where applicable, label traceability, and transport-ready packaging. Troubleshooting supports these goals by keeping the line within validated limits.
Applications span serum tubes, plasma tubes, EDTA tubes, citrate tubes, glucose tubes, heparin tubes, and specialty collection formats. Each product type has different dosing, drying, material compatibility, and vacuum requirements. A troubleshooting framework helps plants switch among SKUs while controlling changeover risk. This is especially important in multi-product facilities near logistics centers such as New Jersey, Dallas-Fort Worth, Memphis, and Southern California, where rapid replenishment and distribution efficiency matter.
Operationally, the benefits include lower scrap, fewer customer returns, improved overall equipment effectiveness, faster root cause closure, better preventive maintenance planning, and smoother audits. Financially, those benefits can be substantial because blood tube production is typically margin-sensitive and high-volume. Even a 1% improvement in usable output can represent meaningful annual savings.
Manufacturing capability is another selection factor. IVEN operates specialized manufacturing plants dedicated to pharmaceutical filling and packaging machinery, water treatment systems, intelligent logistics equipment, and vacuum blood collection tube production equipment. For buyers in the United States, this indicates a supplier base with focused production resources rather than a purely trading model.
var ctx1 = document.getElementById(‘lineChartMarket’).getContext(‘2d’);var chart1 = new Chart(ctx1, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026’],datasets: [{label: ‘U.S. blood tube line demand index’,data: [82, 88, 96, 108, 119, 131],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.15)’,fill: false,tension: 0.3}]},options: {responsive: true,maintainAspectRatio: false}});The line chart above reflects a realistic demand index trend for automated blood collection tube manufacturing solutions in the United States. Growth is being driven by decentralized testing, aging populations, laboratory network expansion, inventory resilience planning, and continued replacement of labor-intensive processes.
Today’s market offers several equipment configurations depending on scale, tube material, product mix, and automation goals. Smaller lines may focus on semi-automatic dosing and stopper insertion for regional or niche suppliers. Medium-throughput systems often combine automatic feeding, dosing, vacuuming, capping, and inspection. Full automatic lines integrate robotics, in-line quality checks, reject segregation, digital batch records, and packaging interfaces.
Configuration decisions should also reflect local utility conditions, labor profile, validation strategy, and future expansion plans. A plant in the Midwest serving national hospital groups may need highly repeatable large-batch performance. A contract manufacturer on the East Coast may need flexible changeovers for multiple brands. A new facility near Houston or Savannah may prioritize export-ready packaging and scalable logistics.
Line TypeTypical Output RangeBest ForAutomation LevelTroubleshooting ComplexityMain AdvantageSemi-automatic lineLow to moderateSmall producers and pilot plantsMediumLowerLower upfront investmentStandard automatic lineModerate to highRegional medical consumable manufacturersHighMediumBalanced cost and productivityHigh-speed integrated lineHigh to very highNational suppliers and OEM programsVery highHighMaximum throughputMulti-SKU flexible lineModerate to highMixed product portfoliosHighHighFast product changeoverRobotic inspection lineModerate to highQuality-focused premium productionVery highMediumBetter defect detectionTurnkey plant integrationProject-specificNew factoriesCustomCustomOne-source coordinationThe table shows that there is no single ideal line for every buyer. The right choice depends on throughput, labor costs, facility layout, validation depth, and customer commitments. Manufacturers considering a new project can review integrated solution options through turnkey engineering services when a full-factory approach is preferred.
Manual or heavily labor-dependent assembly lines may appear less expensive at first, but they create higher variation risk in vacuum accuracy, additive dosing, cap placement, inspection consistency, and traceability. Automated lines, by contrast, support repeatable parameter control and produce more usable data for troubleshooting and continuous improvement.
In the United States, where labor costs, compliance expectations, and supply reliability standards are high, automated blood tube production typically offers better long-term economics. Troubleshooting on automated lines also becomes more structured because alarms, sensors, and trend data make root causes easier to isolate than on manual systems, where issues may remain hidden until final inspection or customer use.
var ctx2 = document.getElementById(‘barChartDemand’).getContext(‘2d’);var chart2 = new Chart(ctx2, {type: ‘bar’,data: {labels: [‘Hospital systems’,’Diagnostic labs’,’OEM brands’,’Distributors’,’Research centers’,’Export buyers’],datasets: [{label: ‘Estimated demand share by buyer type (%)’,data: [28, 24, 16, 14, 8, 10],backgroundColor: [‘rgb(255, 99, 132)’,’rgb(54, 162, 235)’,’rgb(255, 206, 86)’,’rgb(75, 192, 192)’,’rgb(153, 102, 255)’,’rgb(255, 159, 64)’]}]},options: {responsive: true,maintainAspectRatio: false}});The bar chart suggests where demand pressure often comes from. Hospital systems and diagnostic laboratories remain primary end-market drivers, so production lines must be designed for stable supply and consistent quality.
FactorAutomated LineManual LineQuality EffectCost EffectStrategic ImplicationVacuum consistencyHighVariableBetter draw accuracyLower rejectsPreferred for regulated scaleAdditive controlPrecise dosingOperator dependentMore uniform chemistryLower reworkSupports broader product rangeTraceabilityDigital records possibleLimitedImproves investigation qualityReduces compliance riskUseful for auditsLabor intensityLower per unitHigher per unitLess handling variationBetter over timeImportant in U.S. labor marketsTroubleshooting speedFaster with dataSlowerShorter downtimeHigher uptimeSupports service commitmentsScalabilityStrongLimitedStable during growthBetter ROI at volumePreferred for expansionThis comparison explains why many manufacturers are replacing legacy assembly methods. Automation does require stronger engineering and maintenance support, but the payback usually improves as volume rises and compliance demands tighten.
The U.S. market for blood collection consumables remains attractive because testing volumes are tied to routine care, chronic disease monitoring, emergency services, oncology, infectious disease screening, and preventive health programs. Domestic production interest has also increased as buyers seek resilient sourcing, shorter lead times, and better control over supply chains.
Manufacturers near logistics corridors such as the Port of Los Angeles, Port of Long Beach, Port of Savannah, Port of New York and New Jersey, and Memphis air cargo networks can use this advantage to serve both domestic and export markets. Proximity to polymer suppliers, rubber component sources, packaging vendors, and contract sterilization or testing services can further strengthen competitiveness.
Future opportunity is not only about volume. It is also about upgrading technology, digitalization, and sustainability. By 2026, many buyers will expect more predictive maintenance, remote diagnostics, machine vision enhancement, electronic batch data integration, and energy-conscious production design. Policy trends may also push more localized manufacturing and stronger documentation for quality risk management.
var ctx3 = document.getElementById(‘areaChartTrend’).getContext(‘2d’);var chart3 = new Chart(ctx3, {type: ‘line’,data: {labels: [‘2021′,’2022′,’2023′,’2024′,’2025′,’2026’],datasets: [{label: ‘Shift from manual to automated production (%)’,data: [38, 43, 49, 56, 63, 71],borderColor: ‘rgb(75, 192, 192)’,backgroundColor: ‘rgba(75, 192, 192, 0.25)’,fill: true,tension: 0.35}]},options: {responsive: true,maintainAspectRatio: false}});The area chart above shows the expected shift toward automation. While actual adoption varies by product segment and factory size, the overall direction is clear: more data-driven production, fewer manual interventions, and stronger process control.
For companies assessing product solutions, available equipment categories can be explored through medical and pharmaceutical production equipment offerings. This helps buyers compare systems across automation level, output, and integration scope.
Selecting the right supplier for a vacuum blood tube line goes far beyond price. U.S. buyers should evaluate engineering capability, project execution experience, quality system understanding, installed base, spare parts planning, software transparency, validation support, and after-sales responsiveness. It is important to ask not only what the line can produce on paper, but also how the supplier handles troubleshooting after installation.
A reliable manufacturer should provide clear FAT and SAT protocols, utility requirement documentation, line layout drawings, maintenance schedules, recommended spare parts lists, alarm logic descriptions, and training plans. For FDA-oriented environments, documentation quality is especially important because poor records create long-term operational headaches.
Service capability can make the difference between a smooth ramp-up and prolonged instability. IVEN is recognized for lifecycle support that can include feasibility advice, engineering design, equipment customization, installation, commissioning, validation assistance, documentation, training, and after-sales response. For a U.S. customer, this broader service model can reduce project risk compared with buying isolated machines from unrelated vendors.
Selection CriterionWhat to AskWhy It MattersWarning SignPreferred EvidenceBuyer BenefitEngineering depthCan the supplier customize layout and process?Fit with facility and SKU needsOnly standard brochures3D layouts and case examplesBetter project fitCompliance understandingDo they support regulated documentation?Audit readinessWeak document packageDQ, IQ, OQ support examplesLess validation delayInstalled baseHow many similar lines are operating?Reduces technical uncertaintyNo comparable referencesProven project listHigher confidenceTroubleshooting supportHow are faults handled after startup?Protects uptimeUnclear escalation pathService SLA and remote support planFaster recoverySpare parts readinessWhich critical parts are stocked?Prevents long outagesLong undefined lead timesRecommended stock listLower downtime riskTraining qualityWho trains operators and maintenance staff?Supports stable operationMinimal training scopeStructured training documentsQuicker ramp-upWhen comparing suppliers, many U.S. buyers also value global project experience. A company that has completed complex international installations is usually better prepared to manage layout optimization, compliance discussions, cross-functional coordination, and timeline control.
Investment in a vacuum blood collection tube line can vary widely depending on speed, automation level, vision systems, leak testing sophistication, packaging integration, cleanroom requirements, utilities, and validation scope. Budgeting should therefore include both direct equipment cost and the hidden costs of commissioning, spare parts, operator training, line balancing, qualification, and production stabilization.
In the United States, buyers should also consider site preparation, electrical and HVAC adaptation, compressed air quality, environmental monitoring, software integration, and local service response planning. A low initial quotation can become expensive if the line experiences prolonged startup problems or lacks documentation needed for qualification.
ROI is often driven by labor reduction, scrap reduction, output increase, and stronger delivery reliability. If a plant currently depends on manual steps, automation can dramatically improve yield and consistency. Even for an existing automatic line, better troubleshooting tools can extend asset life and improve throughput.
Cost CategoryLow Complexity ProjectMid Complexity ProjectHigh Complexity ProjectBudget RiskPlanning TipCore production lineModerateHighVery highSpecification creepFreeze URS earlyInspection systemsBasic camera setupAdvanced visionMulti-point vision and traceabilitySoftware mismatchValidate defect criteria upfrontUtilities and cleanroom adaptationLow to moderateModerateHighSite underestimationAudit plant utilities before purchaseValidation and documentationBasicModerateExtensiveLaunch delayDefine document list in contractTraining and startupShortMediumLongOperator learning gapSchedule multi-phase trainingSpare parts and maintenance stockBasicRecommendedComprehensiveUnplanned downtimeBuild critical parts inventoryThe table above highlights that budget planning is not just about buying the machine. It is about funding stable production. A smart ROI model should compare total cost of ownership over three to seven years, including labor, scrap, maintenance, uptime, and capacity expansion.
var ctx4 = document.getElementById(‘comparisonChartSupplier’).getContext(‘2d’);var chart4 = new Chart(ctx4, {type: ‘bar’,data: {labels: [‘Customization’,’Validation support’,’Output stability’,’After-sales service’,’Documentation’,’Turnkey ability’],datasets: [{label: ‘Integrated supplier capability score’,data: [88, 84, 90, 86, 82, 89],backgroundColor: ‘rgb(153, 102, 255)’},{label: ‘Basic equipment vendor score’,data: [62, 55, 70, 58, 50, 42],backgroundColor: ‘rgb(201, 203, 207)’}]},options: {responsive: true,maintainAspectRatio: false}});This comparison chart reflects a common market reality: integrated engineering suppliers tend to outperform basic equipment vendors in areas that most affect long-term project success, especially troubleshooting support, documentation, and expansion planning.
Before investing, manufacturers should assess product portfolio fit, expected throughput, plant utilities, cleanroom strategy, staffing capability, and customer quality expectations. One frequent risk is buying a line optimized for a single SKU while the business actually needs flexible changeovers. Another is underestimating how much troubleshooting knowledge is required to sustain output after the supplier leaves the site.
Material compatibility is also critical. Tube polymer quality, stopper composition, additives, label stock, and packaging materials all affect line behavior. Inconsistent incoming materials often create problems that appear to be machine faults. Therefore, a complete troubleshooting plan should include vendor qualification and incoming quality control, not only equipment maintenance.
There are also scheduling risks. Delays in cleanroom readiness, utility installation, or qualification protocol approval can postpone startup and reduce ROI. Buyers should create a project governance plan that aligns procurement, engineering, quality, validation, and production teams from the beginning.
Sustainability is becoming more relevant as well. By 2026, many U.S. buyers will favor solutions with lower energy use, reduced compressed air waste, smarter reject handling, and more efficient packaging logistics. Digital monitoring can support this by showing where energy and material losses occur during production.
A practical risk-mitigation step is to work with suppliers that can support layout review, engineering coordination, and performance optimization after installation. Manufacturers interested in discussing project scope or service support can use the contact page for technical consultation to start a requirements review.
Consider a U.S. manufacturer serving hospital networks in the Northeast. The plant experiences rising reject rates from stopper leakage and inconsistent vacuum levels during seasonal humidity changes. A structured troubleshooting program identifies three combined causes: stopper dimensional variation from a supplier lot, insertion tooling wear, and utility fluctuation in compressed air pressure. After replacing wear parts, tightening incoming component inspection, and stabilizing utilities, the plant improves usable output and reduces complaint risk.
In another example, a Midwest producer supplying OEM private-label tubes struggles with labeling accuracy after expanding into multiple SKUs. Vision system trend data shows that tube rotation speed varies during format changeovers. By adjusting servo settings, updating operator setup instructions, and adding recipe verification, the company shortens changeover time and reduces relabeling costs.
Local supply considerations in the United States include access to plastics processors, elastomer component vendors, label converters, packaging suppliers, and validation consultants. Plants near Chicago, Indianapolis, Charlotte, Dallas, or New Jersey often benefit from strong transport links and broad industrial support networks. However, imported equipment buyers should still plan for U.S.-based spare stocking, remote diagnostics access, and clear escalation procedures to avoid long recovery times.
From an engineering standpoint, our company focus is on practical performance across the full production lifecycle. IVEN Pharmatech Engineering combines technological capability in automation and process integration, manufacturing capability through specialized production facilities, and service capability that supports project planning, installation, commissioning, and operational optimization. Rather than presenting equipment as an isolated asset, the approach is to align machinery, utilities, facility design, and documentation with the customer’s real production goals.
That matters for American buyers because the market increasingly values dependable execution, not just machine specifications. A line must start well, run consistently, and remain supportable for years. Suppliers with long-term engineering perspective are usually better positioned to assist with expansion, validation updates, product changeovers, and troubleshooting optimization as market needs evolve.
What are the most common vacuum blood tube line problems?The most common issues are unstable vacuum levels, stopper leakage, additive dosing deviation, tube jams, labeling errors, vision inspection false rejects, and unplanned downtime caused by wear parts or utility instability.
How often should a blood tube production line be serviced?Daily checks, weekly cleaning verification, monthly calibration review, and scheduled preventive maintenance based on cycle count are common best practices. Critical modules such as vacuum systems, dosing pumps, and insertion tooling need closer monitoring.
Is troubleshooting mainly a maintenance task?No. Effective troubleshooting involves maintenance, production, quality assurance, validation, utilities, and materials management. Many recurring faults come from process settings or component variation rather than a simple machine breakdown.
Can automated lines handle multiple tube types?Yes, many can, but flexibility depends on line design, recipe management, tooling changeover, and operator training. Multi-SKU production should be planned at the purchase stage.
What documentation should a U.S. buyer request from a supplier?Request URS alignment documents, FAT and SAT protocols, equipment manuals, spare parts lists, alarm lists, electrical drawings, software backup procedures, calibration plans, and validation support files where required.
How long does ROI usually take?It depends on throughput, labor savings, reject reduction, and market demand. For high-volume production, automated lines can provide a compelling return over several years, especially when compared with manual assembly or unstable older equipment.
What should be included in a troubleshooting SOP?The SOP should define fault categories, alarm response steps, escalation roles, data review requirements, root cause tools, verification checks, documentation rules, and criteria for restarting production after corrective action.
Why is supplier service important after commissioning?Because many performance issues only appear during real production conditions, including raw material changes, shift differences, and product mix variation. Strong after-sales support helps protect uptime and reduce the learning curve.
What 2026 trends should buyers watch?Predictive maintenance, better machine vision, remote diagnostics, MES connectivity, stronger data integrity controls, energy-efficient utilities, more sustainable packaging design, and increased demand for domestic or regionally resilient manufacturing.
How can a new factory reduce startup risk?Use a detailed URS, choose a supplier with integrated engineering capability, validate utilities early, define documentation expectations in the contract, train operators before SAT, and maintain a critical spare parts inventory from day one.
In summary, vacuum blood tube line troubleshooting is not just about fixing faults. It is a core operating capability for any U.S. manufacturer that wants consistent blood collection tube quality, scalable output, and dependable supply to hospitals and laboratories. With the right line design, skilled support, disciplined data review, and strong supplier partnership, manufacturers can reduce risk, improve ROI, and prepare for the technology and compliance demands that will shape the market through 2026 and beyond.